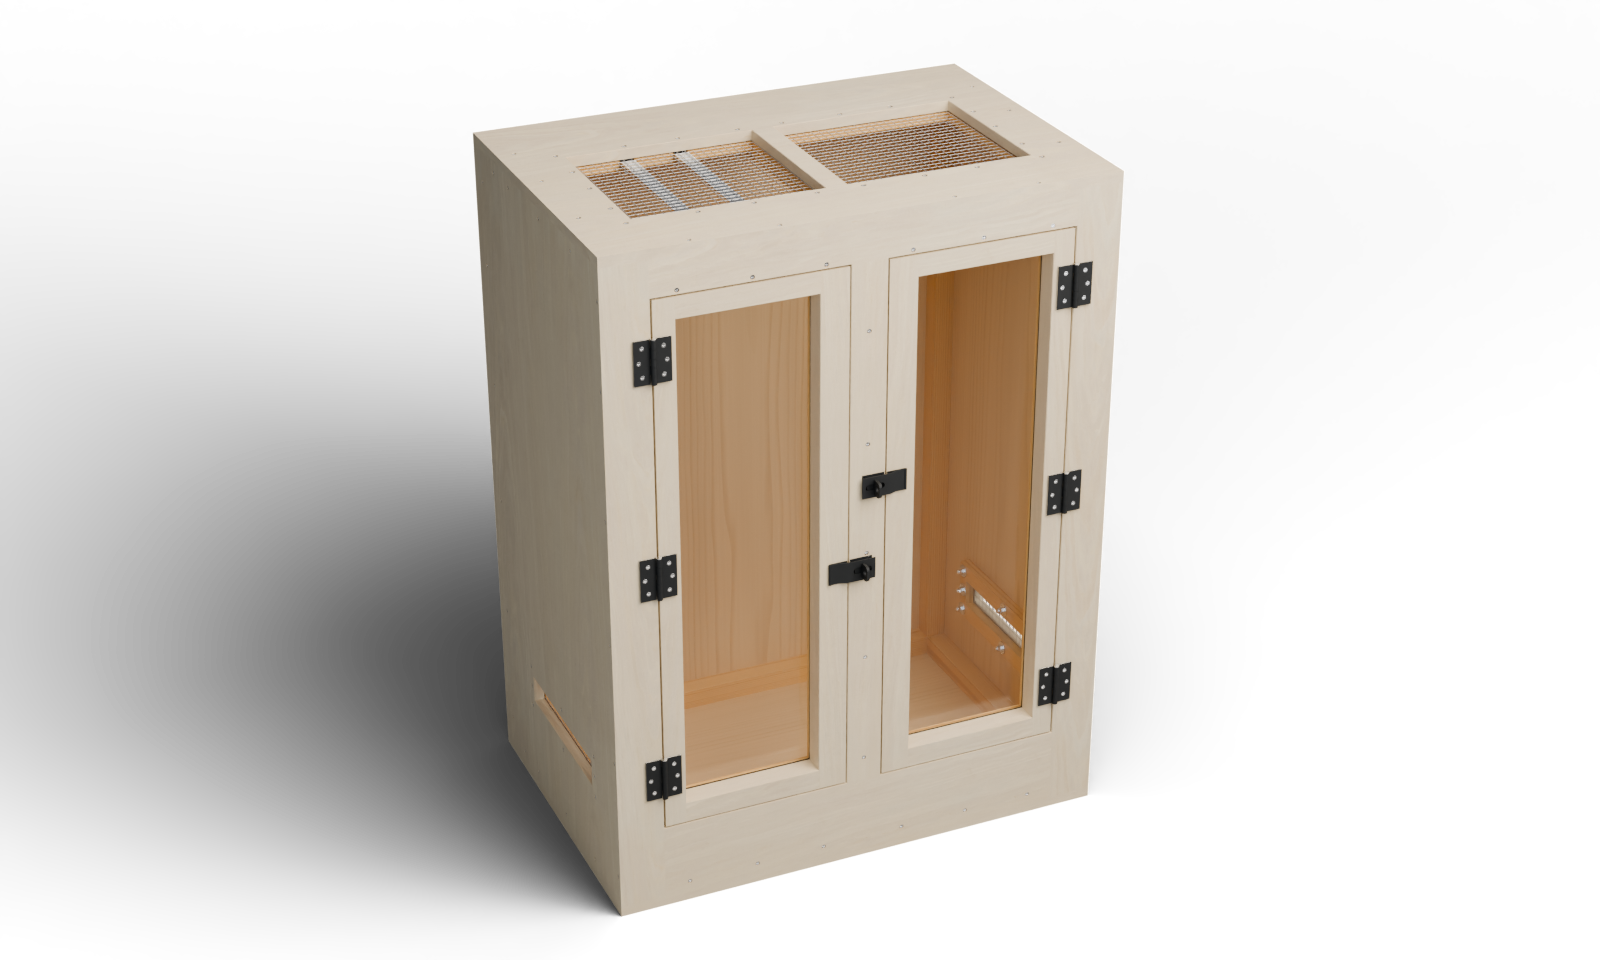
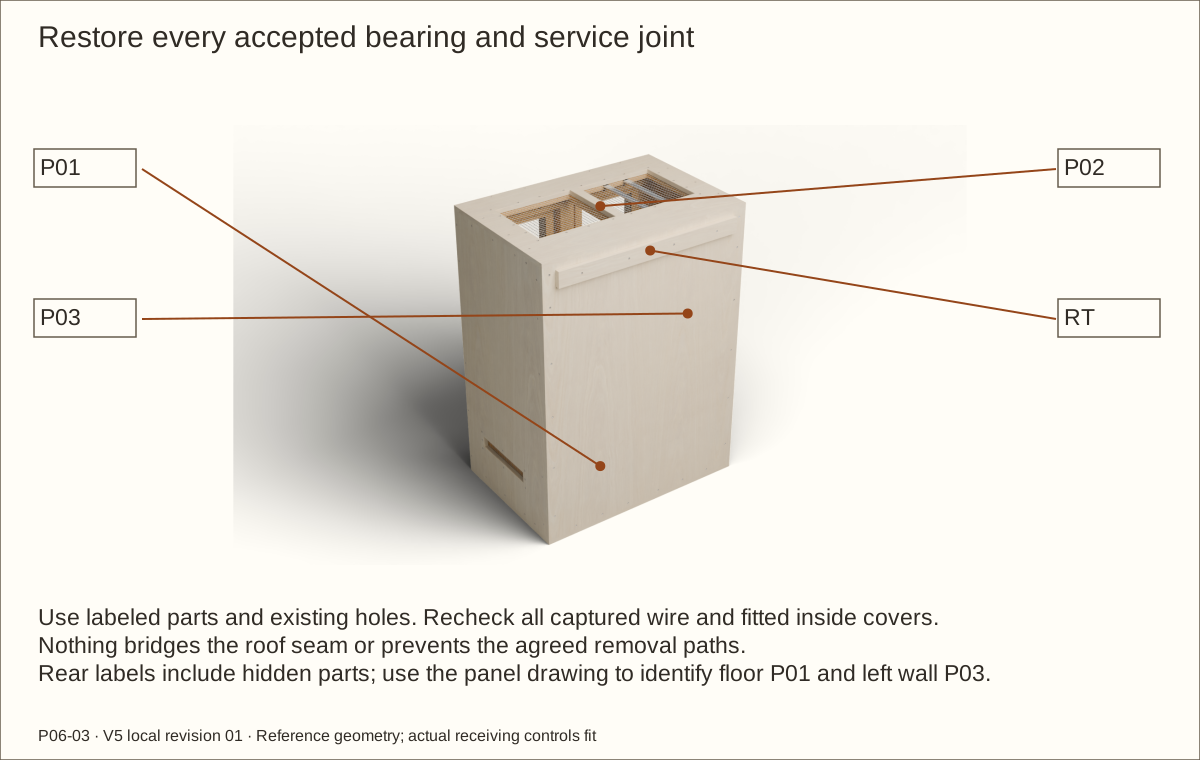
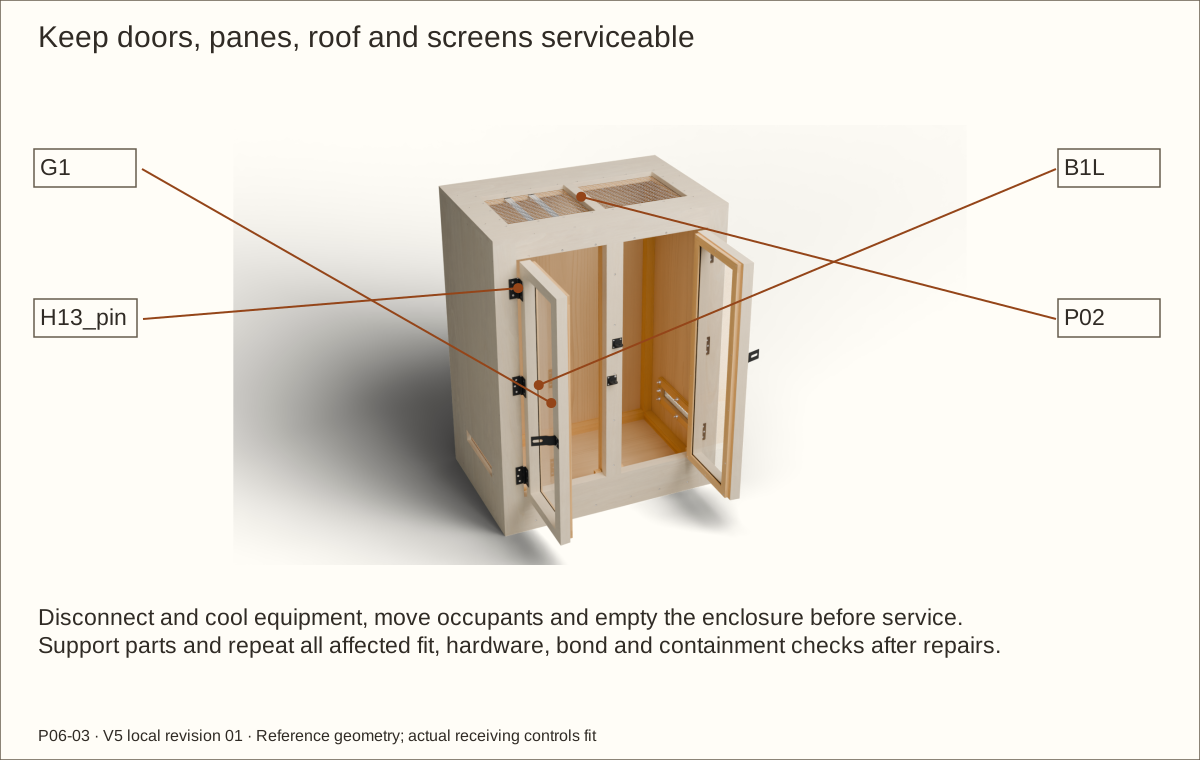
Full exterior veneer: the roof, faces, edges and reveals are included in this guide’s coordinated veneer schedule and geometry. Supplier balance, bond and actual-stack acceptance remain required. Natural grain and color vary.
About these previews
Rendered from this enclosure’s actual reference geometry. Veneer layers preserve service seams and bare hardware seats. The 3D viewer shows maple; these choices change the main picture. Texture scans by Jenelle van Heerden via Poly Haven, CC0 illustrate appearance and are not delivered veneer samples.
Two tall laminated acrylic doors with independent hasps, a removable screened roof, fixed central roof rib, inside screen captures and an external receiver for two site restraints. Follow 54 pictured operations with checks before continuing.
Construction holds: received stock/hardware, custom hinge-pad mounting, veneer balance/bond, solid-pad glazing, site restraints, prototype construction, physical tests and qualified review remain open.
Receive and trial exact products before dependent final cuts. This is P06-03’s own 36 × 24 × 48-inch (914.4 × 609.6 × 1219.2 mm) tall case with two-layer laminated doors, six removable-pin hinges and separate front/rear solid neoprene glazing pads. Recalculate affected parts if stock or hardware changes.
Measurement
Reference
Bare case
36 × 24 × 48 in (914.4 × 609.6 × 1219.2 mm)
Reference covered wood
36.061 in (915.95 mm) × 24.061 in (611.15 mm) × 48.061 in (1220.75 mm)
Maximum covered wood
36.092 in (916.74 mm) × 24.092 in (611.94 mm) × 48.092 in (1221.54 mm)
Rear receiver projection
3/4 in (19.05 mm) beyond the rear case; hardware needs additional space
Each fitted bare door
13.20325 in (335.36 mm) × 38.219 in (970.76 mm)
Bare door gaps
Hinge/top/bottom 3/16 in (4.76 mm); latch 5/32 in (3.97 mm)
Minimum finished operating gap
1/16 in (1.59 mm); containment acceptance is separate
Each acrylic pane
Width 10.547 in (267.89 mm); height 36.094 in (916.79 mm); thickness 0.22 in (5.59 mm)
Service allowance
4 in (101.6 mm) above upper pin and 16 in (406.4 mm) in front; enlarge for actual tools/helpers
Complete cured veneer layer
Reference 0.0305 in (0.77 mm); maximum 0.046 in (1.17 mm)
Datums: X starts at outside LEFT, Y at outside FRONT and Z at FLOOR UNDERSIDE, unless a local part edge is named. Exact decimals are retained for fitting. in means inches; mm means millimetres. Hardware projects beyond covered wood.
Tools, terms and workholding
Prepare a padded flat bench, helpers, clamps, straight cauls, tape, square, caliper and marking knife. Use supported saw/router/jigsaw setups, a chisel, block plane, sliding bevel and stopped drills. Mill narrow strips from long supported stock using a guarded carrier or machining service.
Use root-matched pilots, clearance bits, actual 82-degree head seats and fitting Phillips drivers. Two thin hand tools must fit the received locknut and closed cover. Metal needs a vise, supported saw/drill and files. Veneer needs a sharp knife, straightedge, cutting board and supplier-approved scraper. The restraint installation needs the maker’s specified tools and verified wall support.
Wear eye/hearing protection, control dust and ventilate coatings. Protect hands while handling sharp mesh and metal; keep gloves, fingers and loose clothing away from rotating tools. Support the work and waste.
Term
Meaning
Cleat / ledger / column
Screw-receiving strip / horizontal support / vertical bearing support
Stile / rail
Vertical / horizontal frame member
Caul / lamination
Straight board spreading clamp pressure / overlapping layers glued together
Recess / back bevel
Shallow pocket / rear edge sloping inward while front size stays fixed
Pressure-sensitive adhesive / relative humidity / bill of materials
Neoprene / nylock
Here, plain solid pane cushioning / a nylon-insert locknut
Use the actual-stock worksheet
Record plywood thickness: t = ______ in / ______ mm. These equations preserve the bare 36 × 24 × 48-inch (914.4 × 609.6 × 1219.2 mm) case. They assume the accepted front and support sections; changed sections require revision of dependent work.
Part or opening
Equation, inches
Reference
P01 floor and P02 roof
36 × 24
36 × 24 in (914.4 × 609.6 mm)
Side and back height
48 − 2t
46.594 in (1183.49 mm)
Back width
36 − 2t
34.594 in (878.69 mm)
Each front opening width
(36 − 2t − 3 × 2.5) ÷ 2
13.547 in (344.09 mm)
Front opening height
48 − 2t − 5.5 − 2.5
38.594 in (980.29 mm)
Bare leaf width
Measured opening − 3/16 − 5/32
13.20325 in (335.36 mm)
Bare leaf height
Measured opening − 3/16 − 3/16
38.219 in (970.76 mm)
CLB/CLT/CRB/CRT side cleats
24 − t − 4.5
18.797 in (477.44 mm)
CFB/CBB/RF/RB cross members
36 − 2t − 3
31.594 in (802.49 mm)
RC rib length
24 − t − 1.5
21.797 in (553.64 mm)
CC column length
Actual bearing gap; 48 − 2t − 3 − 1.334
42.26 in (1073.4 mm)
Cured glazing contact pocket
Actual pane + both solid pad faces
0.345 in (8.76 mm) reference
Transfer actual bearing gaps with a story stick. Do not round away stock changes or use nominal lumber dimensions for final fitting. Glazing spacer, cured coatings and complete veneer allowances are independent measured inputs.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: No shell load rating, stacking permission or species approval is provided.
Plan full support, restraints and service space
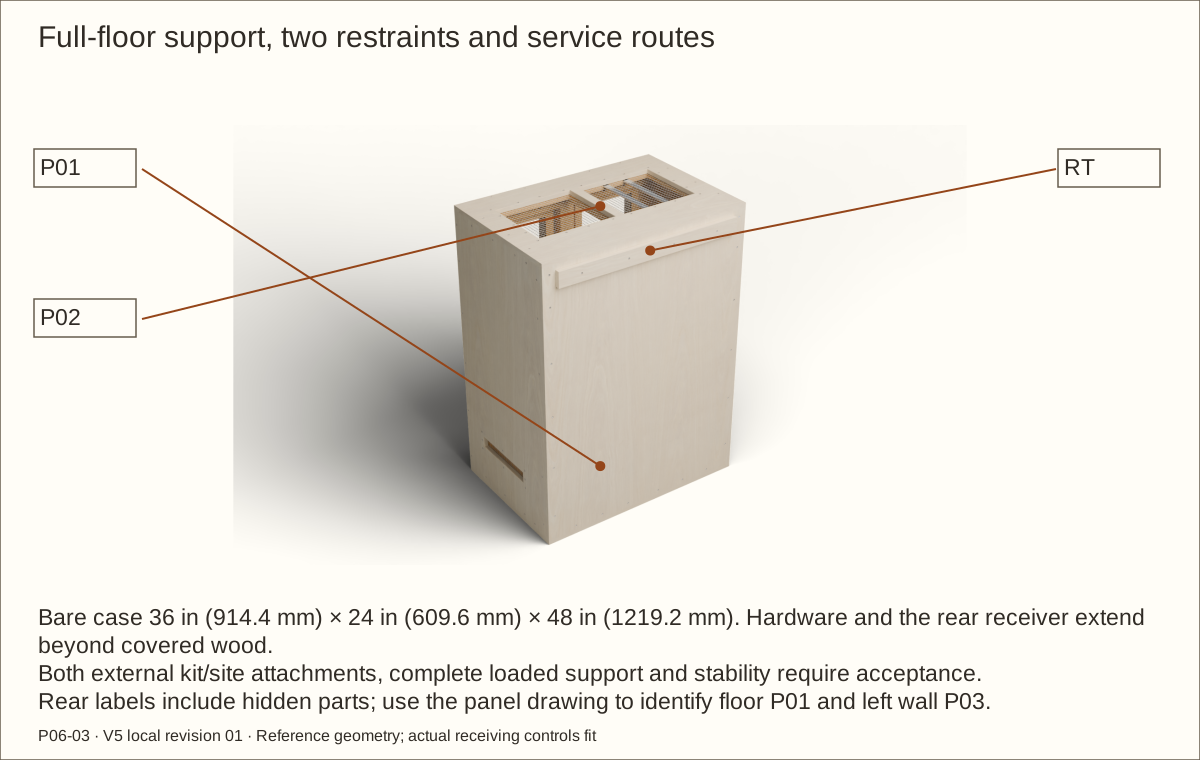
The bare case is 36 in (914.4 mm) wide × 24 in (609.6 mm) deep × 48 in (1219.2 mm) high. Maximum covered wood is 36.092 in (916.74 mm) × 24.092 in (611.94 mm) × 48.092 in (1221.54 mm); the rear receiver adds 3/4 in (19.05 mm) depth and hardware projects farther.
Provide level support beneath the entire finished floor. Record actual loaded weight and obtain an assessment of the support, stability and site wall attachment for both external restraints.
Reserve both outward door sectors, at least 16 in (406.4 mm) in front and 4 in (101.6 mm) above the upper hinge pin, with extra space for actual hands, tools and helpers. Rehearse roof lifting and a supported door-removal route.
Check before continuing: The support, wall attachment and maintenance routes are recorded.
Parts: P03 · Left side; FA · Front outer stile; G1 · Door 1 OPTIX pane
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Measure and label the received stock
Reference plywood thickness is 0.703 in (17.86 mm). Measure corners and centre of each sheet; cutting plans use a conservative 96 in (2438.4 mm) × 48 in (1219.2 mm) stock area.
Verify solid pine at 3/4 in (19.05 mm) × 5 1/2 in (139.7 mm) × 96 in (2438.4 mm) and the separate 1 1/2 in (38.1 mm) square stock. Full-width sill pieces need sound 5 1/2 in (139.7 mm) edges. Check acrylic, plain neoprene, mesh, steel, pads and all hardware.
Acclimate as suppliers require. Mark INSIDE, FRONT, LEFT or RIGHT, part ID, grain direction and the measuring corner. Save matching offcuts and reject damaged bearing areas.
Check before continuing: Received gauges, sound edges and datums are recorded.
Required wait: Use confirmed material acclimation requirements; no arbitrary duration is assumed.
Parts: Accepted material samples and the named workshop setup
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Never feed short loose pieces through a planer or trap waste against a blade.
Prepare safe supported tool setups
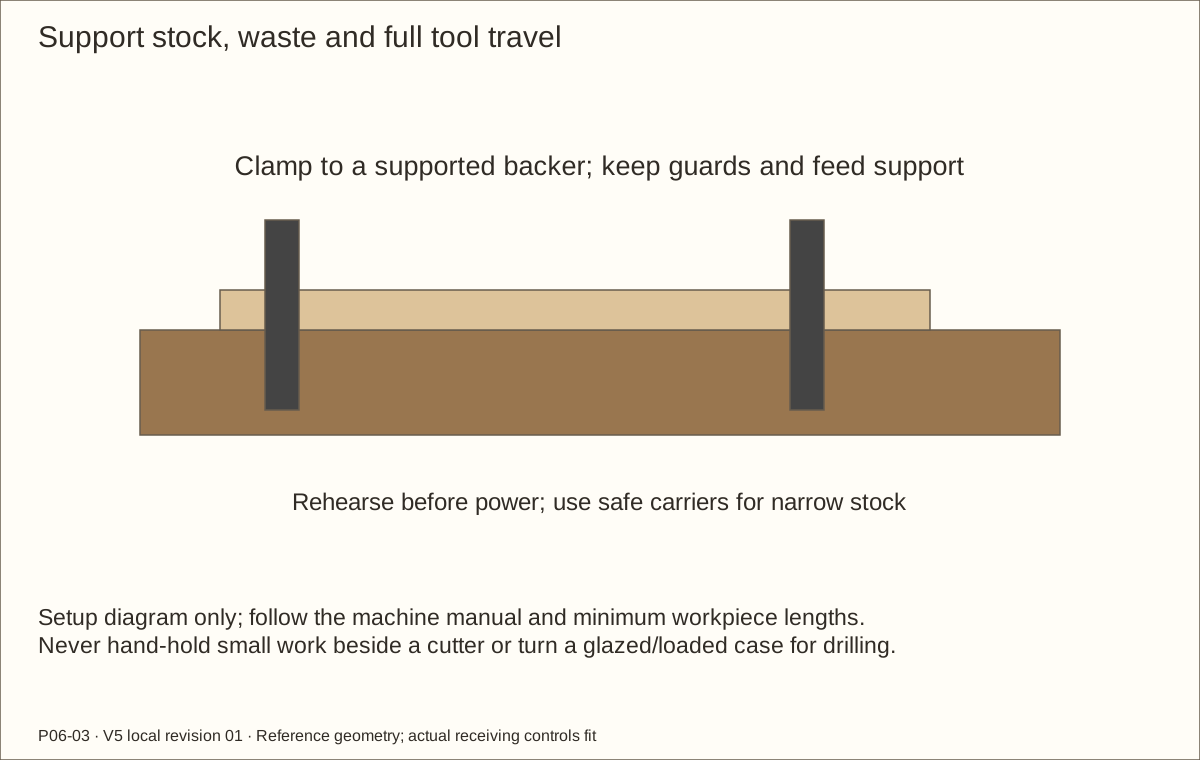
Use a flat padded bench, clamps, straight cauls and supported infeed/outfeed. A caul spreads clamp pressure. Rehearse the largest panel and tall empty-case turn with helpers.
Use the actual tool guards, riving knife, push aids and minimum feed lengths. Mill narrow strips from long supported stock with a guarded carrier or use a machining service.
Clamp drill/router work and waste to a backer. Disconnect power before setting cutters, guides or depth stops.
Check before continuing: Every operation has stable support and a safe hand path.
Before you begin: Do not enlarge factory hinge or hasp holes to force an unsuitable screw to fit.
Trial pilots, clearance holes and head seats
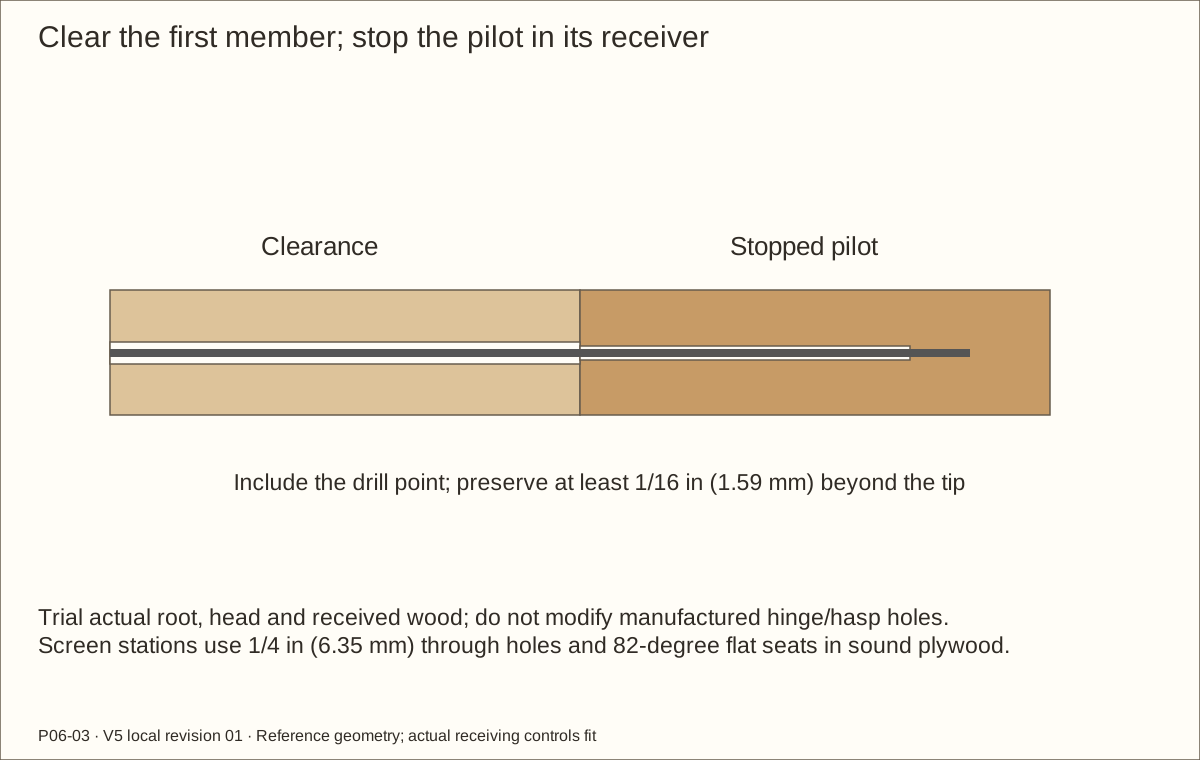
A clearance hole lets the first member pass freely over the screw. A smaller pilot guides its thread in the receiving wood. Trial the actual screw in matching offcuts.
Reference #6 clearance/pilot diameters are 5/32 in (3.97 mm) / 3/32 in (2.38 mm); #8 uses 11/64 in (4.37 mm) / 7/64 in (2.78 mm); #10 wood screws use 13/64 in (5.16 mm) / 1/8 in (3.18 mm). Actual root diameter, wood and trial results govern.
Screen screws use 1/4 in (6.35 mm) through holes and 82-degree flat-head seats. Include the drill point in stopped depth and retain at least 1/16 in (1.59 mm) sound wood beyond each tip.
Check before continuing: Heads seat without splits, crushed bearing wood or exposed points.
Parts: H11_fixed · 1798A21 fixed leaf with knuckles; H11_moving · 1798A21 moving leaf with knuckles; SP-H11-fixed · Rigid full-leaf bearing pad H11 fixed; SP-H11-moving · Rigid full-leaf bearing pad H11 moving
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Six hinges are specified; their count is not a proven tall-door weight rating.
Trial the hinges, bearing pads and hasps
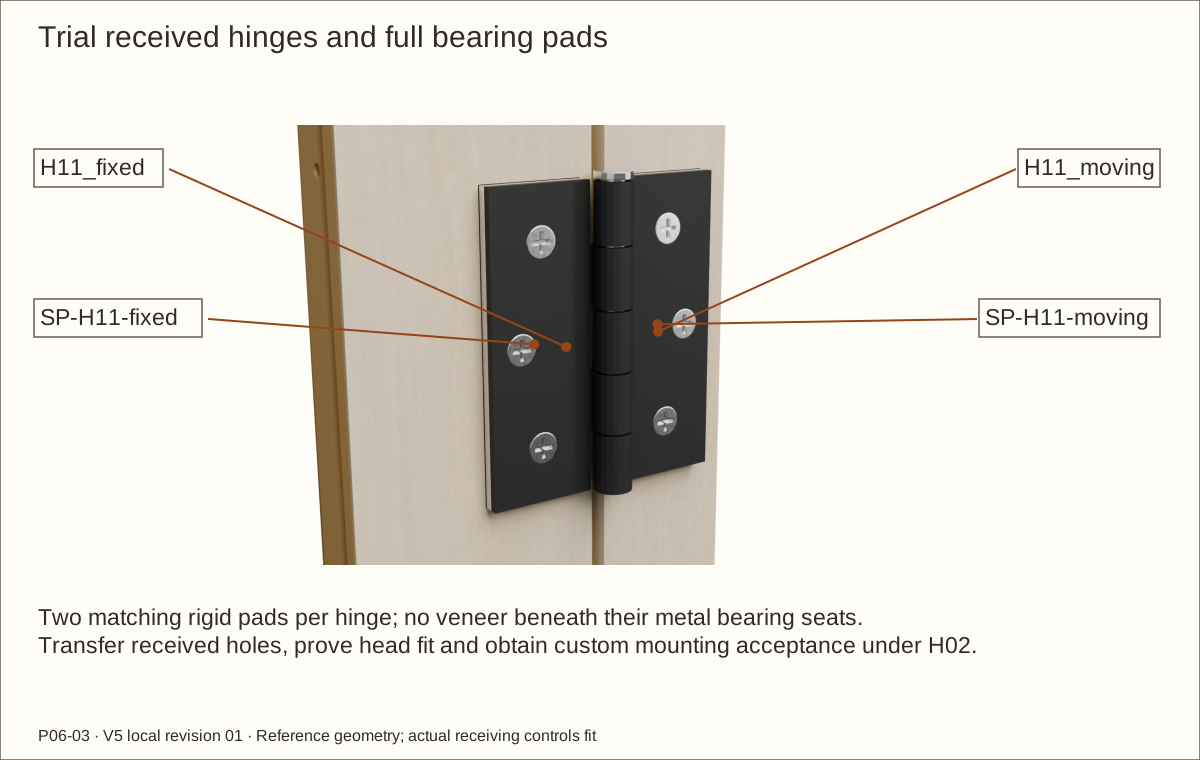
Trial the exact 1798A21 hinge on matching laminated fixed/moving offcuts, with equal 3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm) rigid aluminium pads. Minimum reference pad thickness is 7/64 in (2.78 mm); custom mounting acceptance remains H02.
Keep the barrel forward and the pin removable upward. Transfer actual holes and trial the listed #8 × 1 1/4 in (31.75 mm) heads. Both leaves and pads need full bare-wood bearing and adequate screw engagement.
Trial each N305-979 narrow base on a moving 2 in (50.8 mm) source latch stile, and its square swivel plate on the fixed 2 1/2 in (63.5 mm) centre member. Account for later trimming and veneer; support every hole and plate.
Check before continuing: Actual seating, margins, head fit, pin path and supported swing are accepted.
Parts: D1A · Door 1 A; D1B · Door 1 B; D1E · Door 1 E; D1G · Door 1 G
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Make a full-size laminated-door veneer trial
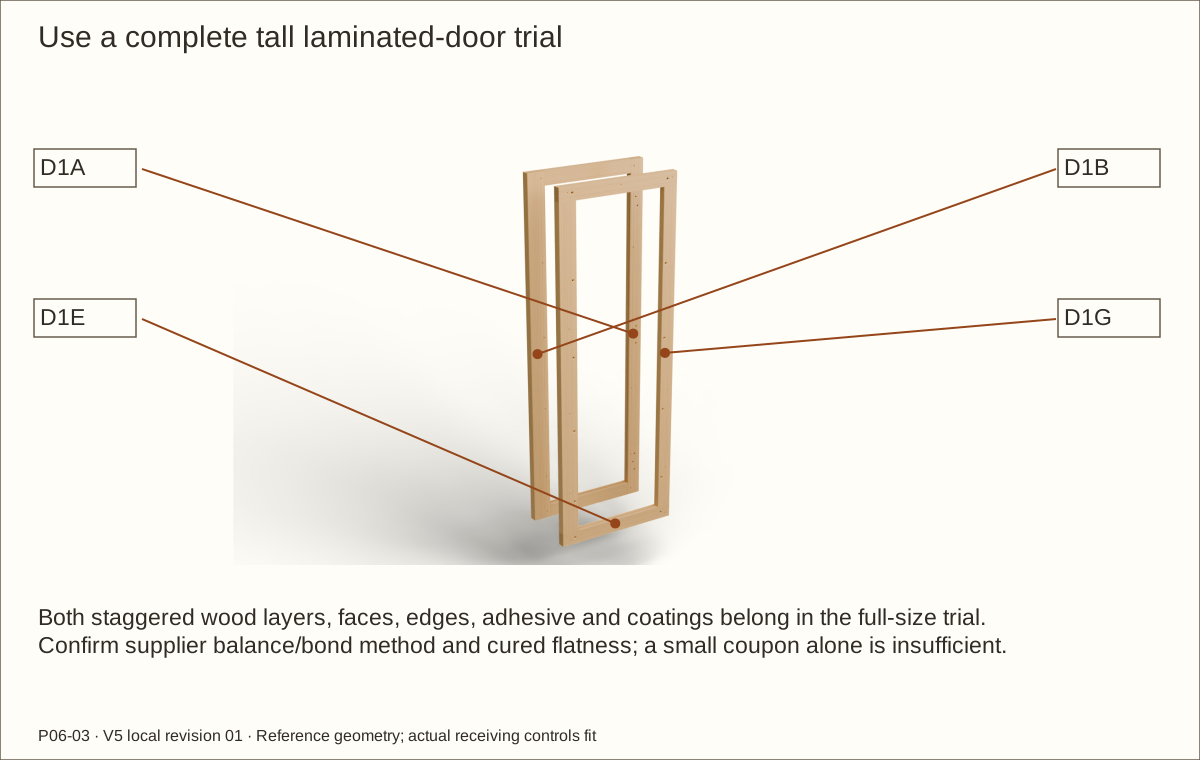
Use reserved pine to make a complete representative tall door with both staggered layers. Apply the accepted face, edge, adhesive, sealer and finish system; a small coupon cannot prove full-door balance.
Follow supplier balancing, pressure and dwell instructions. Measure the complete cured layer including adhesive and coating: no specified face may exceed 0.046 in (1.17 mm).
Record flatness, bond and hardware operation under intended conditions. Any extra balancing layer or changed stock gauge requires a coordinated revision.
Check before continuing: The cured full-size trial remains flat and fits the accepted hardware.
Required wait: Supplier adhesive dwell and full coating cure are separate waits.
Parts: Q1L · Door 1 spacer L; B1L · Door 1 retaining bead L; G1 · Door 1 OPTIX pane; N1FL · Door 1 F cushion L; N1RL · Door 1 R cushion L
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: No adhesive foam, forced compression, glued pane or water-seal claim.
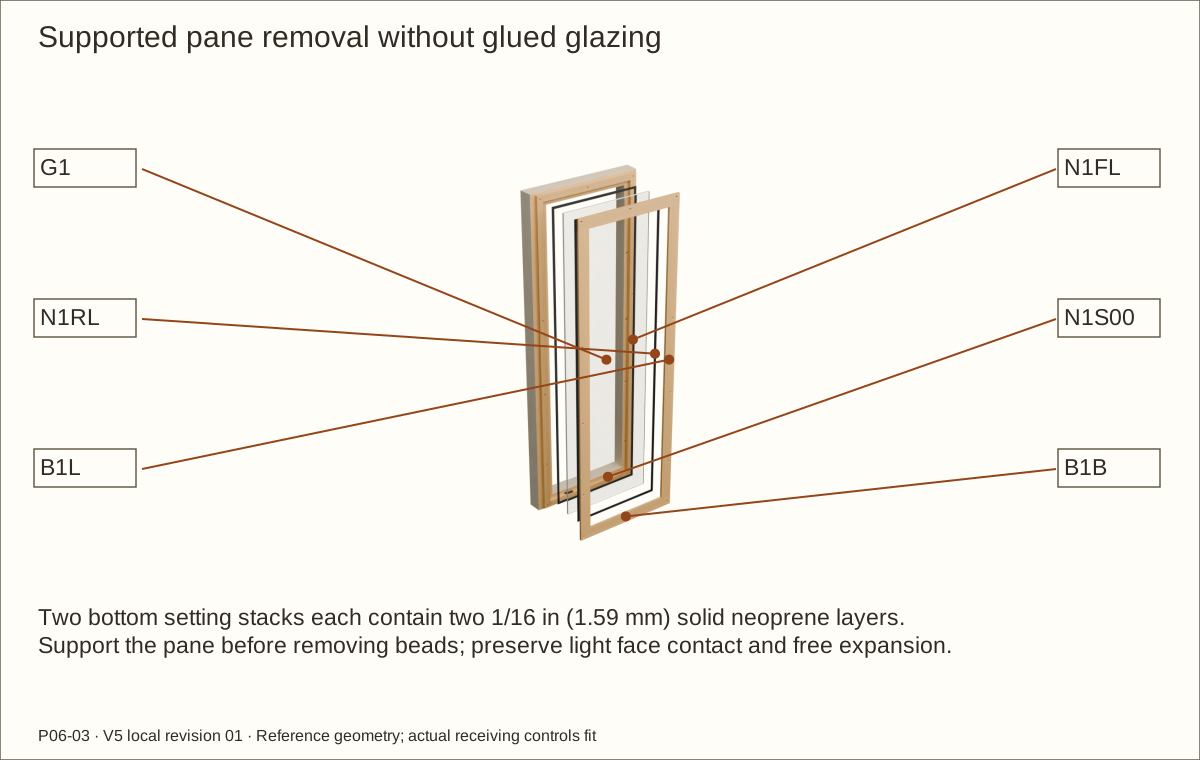
Trial the solid-pad glazing stack after cure
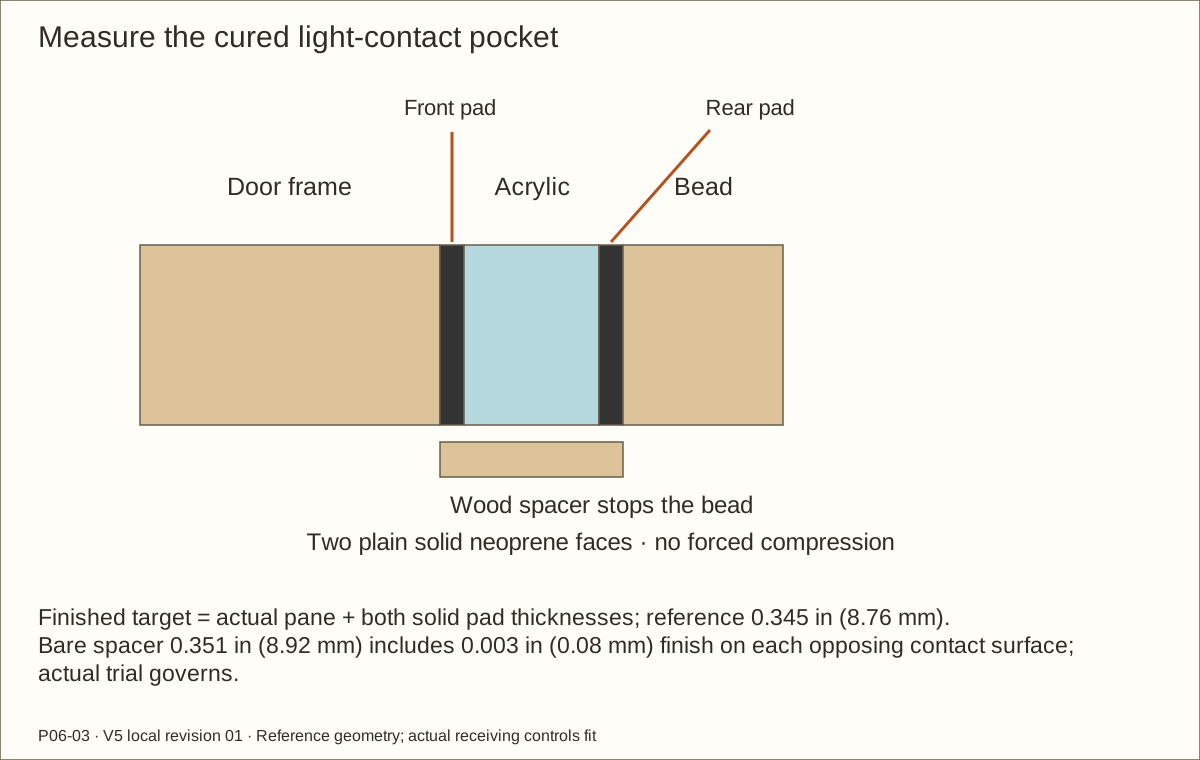
Build a matching sample with the separate rear spacer and 1/4 in (6.35 mm) retaining bead. Mill from 3/8 in (9.53 mm) rough spacer stock; reference bare depth is 0.351 in (8.92 mm).
The finished contact distance must match actual acrylic plus two plain solid neoprene faces. Reference 0.22 in (5.59 mm) pane plus two 1/16 in (1.59 mm) pads totals 0.345 in (8.76 mm); the extra 0.006 in (0.15 mm) bare depth allows 0.003 in (0.08 mm) finish on both opposing wood surfaces.
Trial fully cured surfaces with light contact, no bow or forced compression, and 1/8 in (3.18 mm) free pane-edge allowance. Resolve real coating/pad thickness and compatibility before dependent cuts.
Check before continuing: The bead stops on its wood spacer while the pane remains supported and unbowed.
Required wait: Complete coating cure before measuring the contact fit.
Parts: P01 · Floor; P02 · Roof; P03 · Left side; P04 · Right side; P05 · Back
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
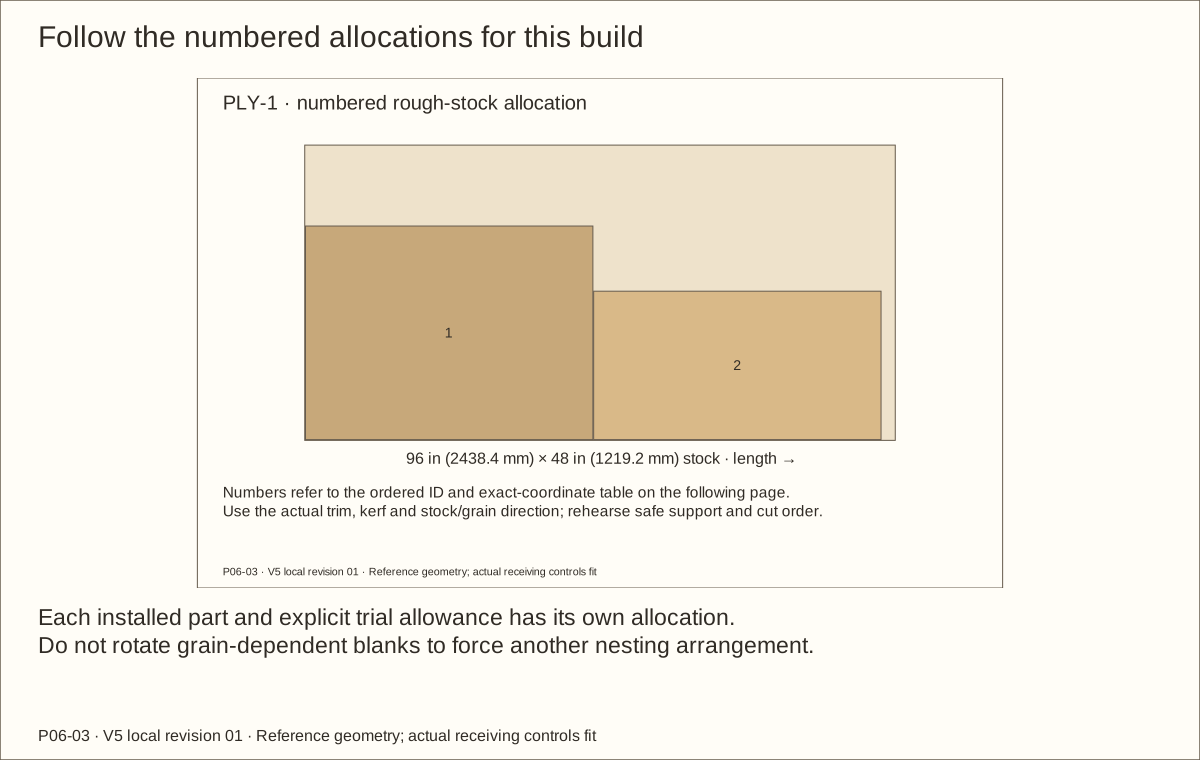
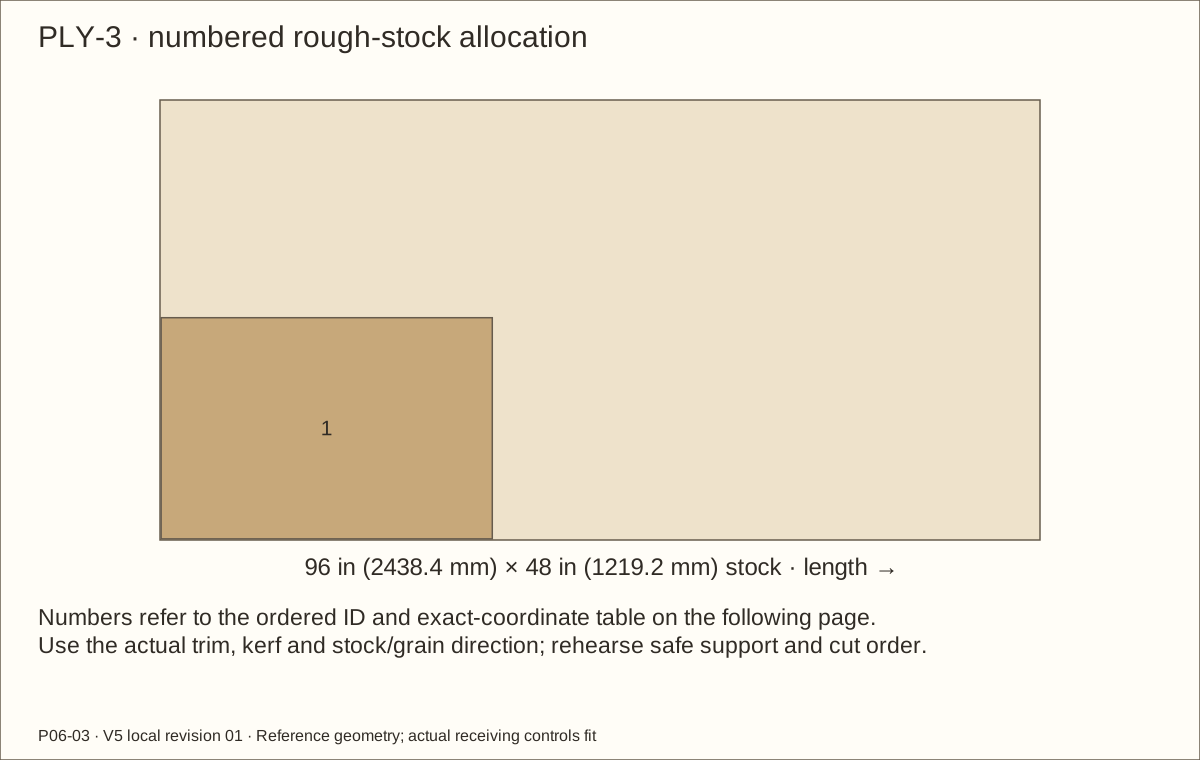
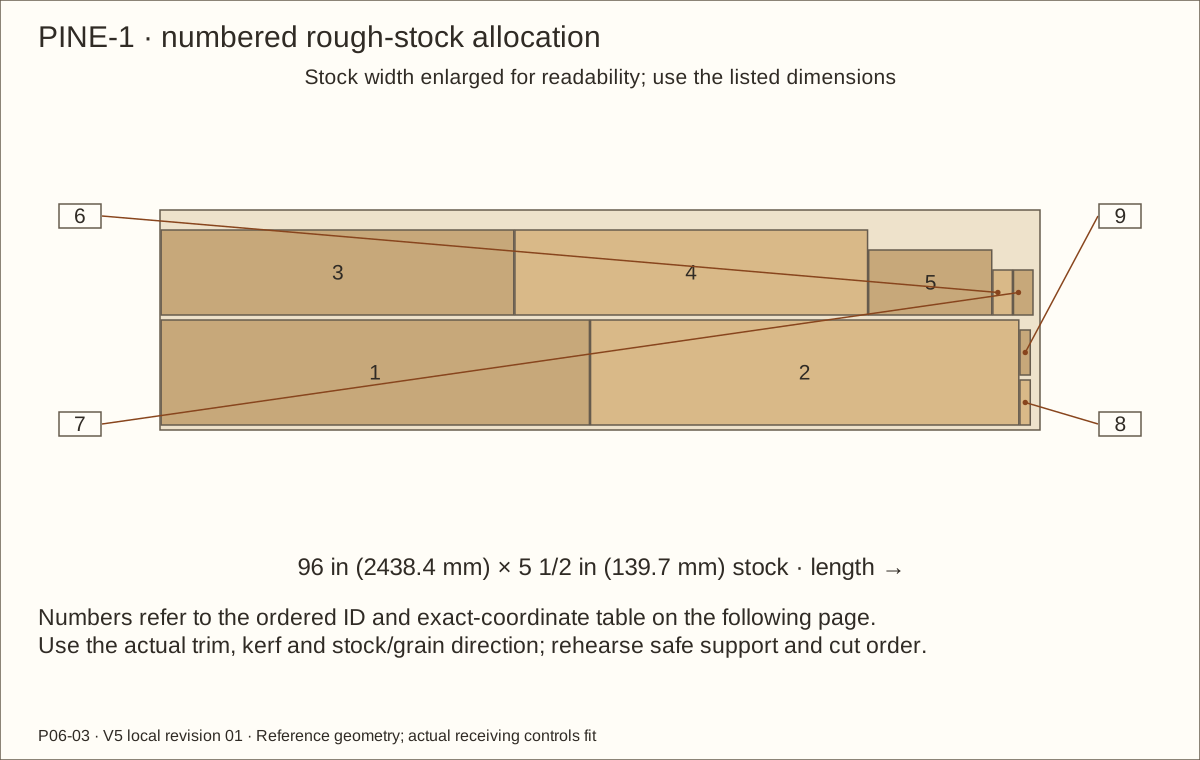
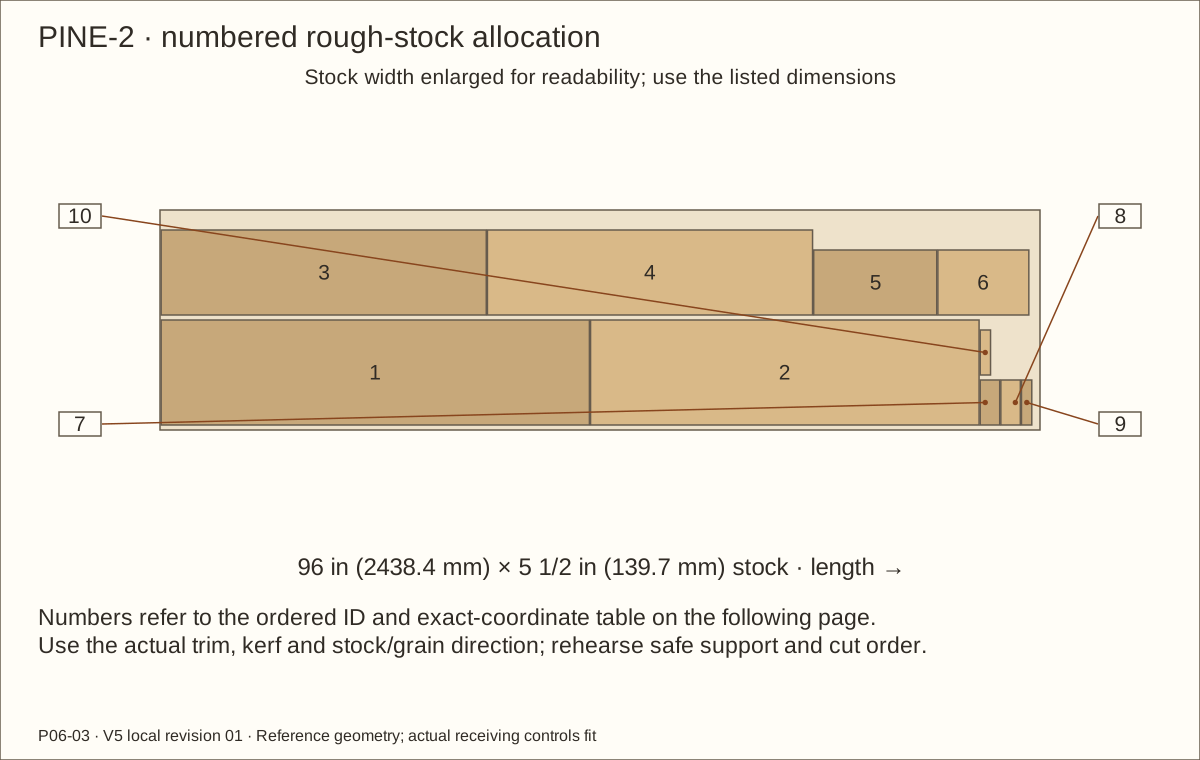
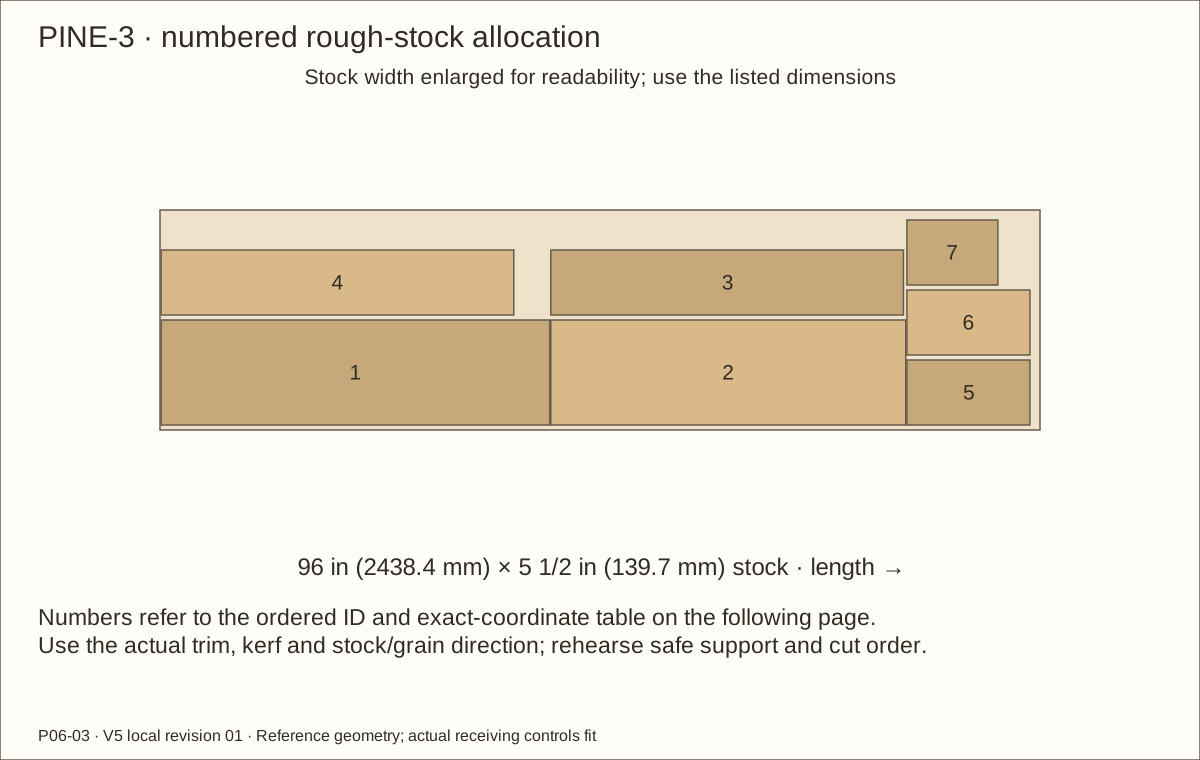
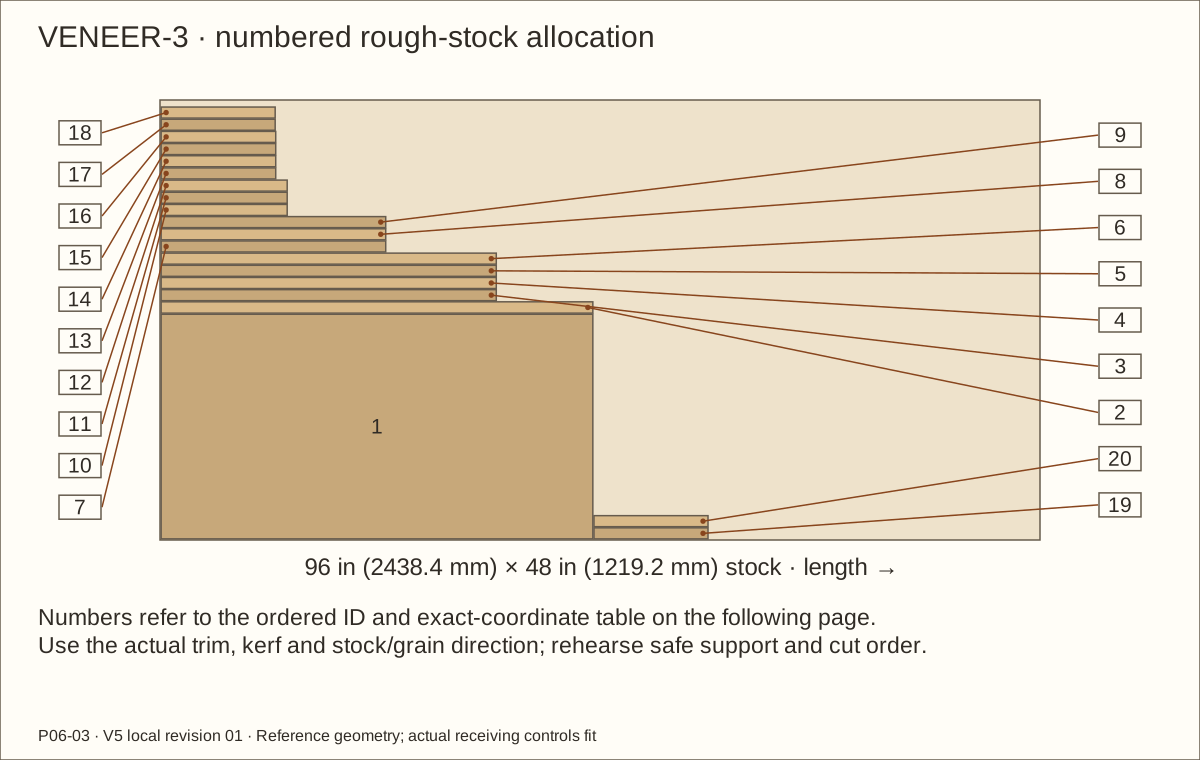
Allocate and rough-cut labeled blanks
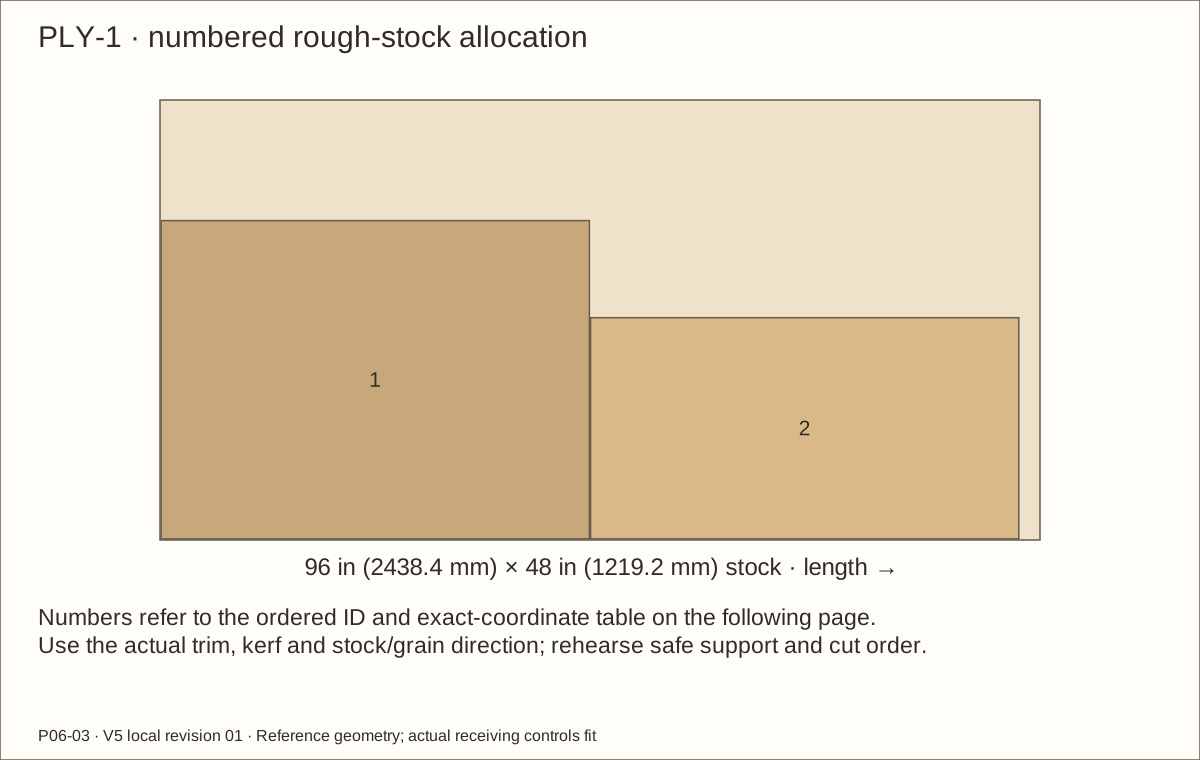
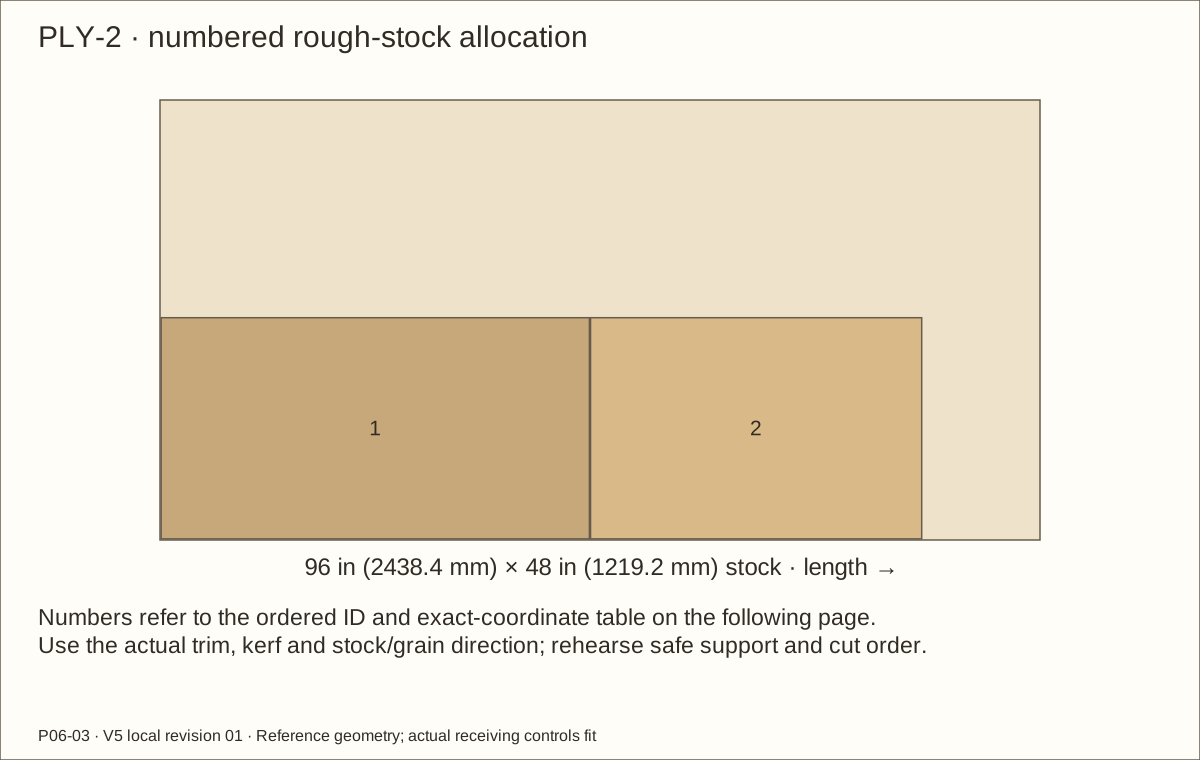
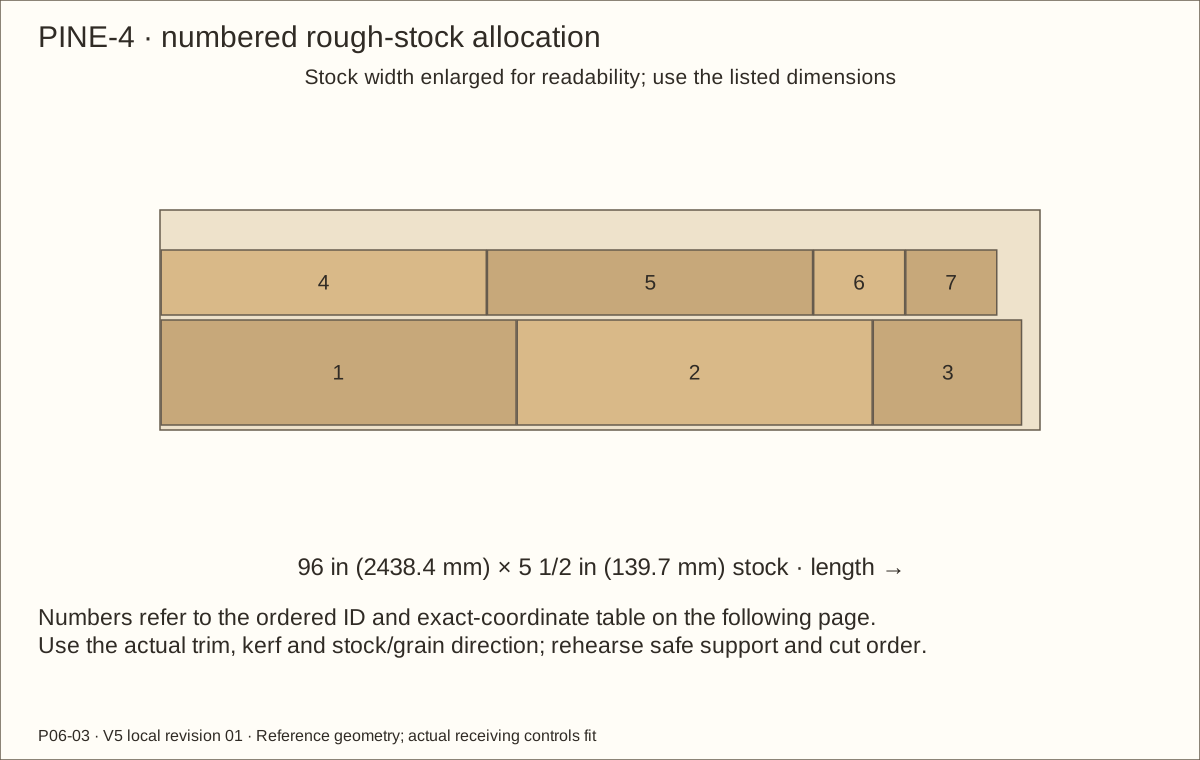
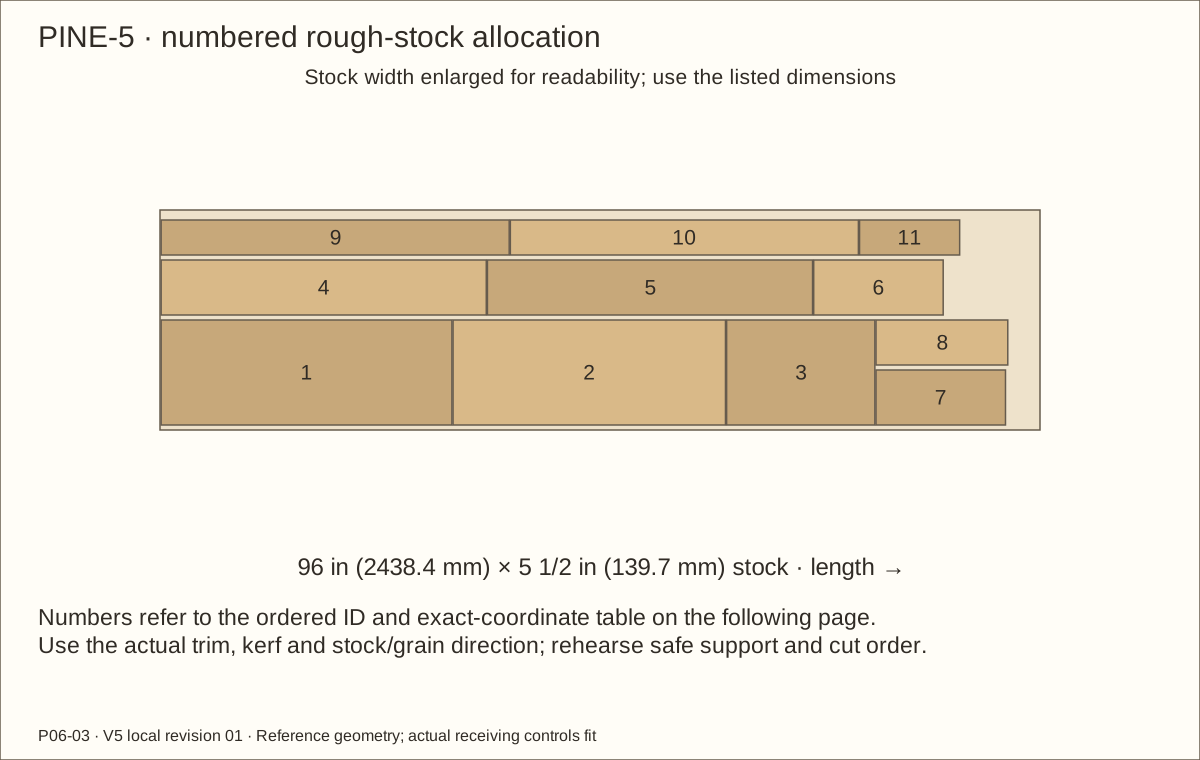
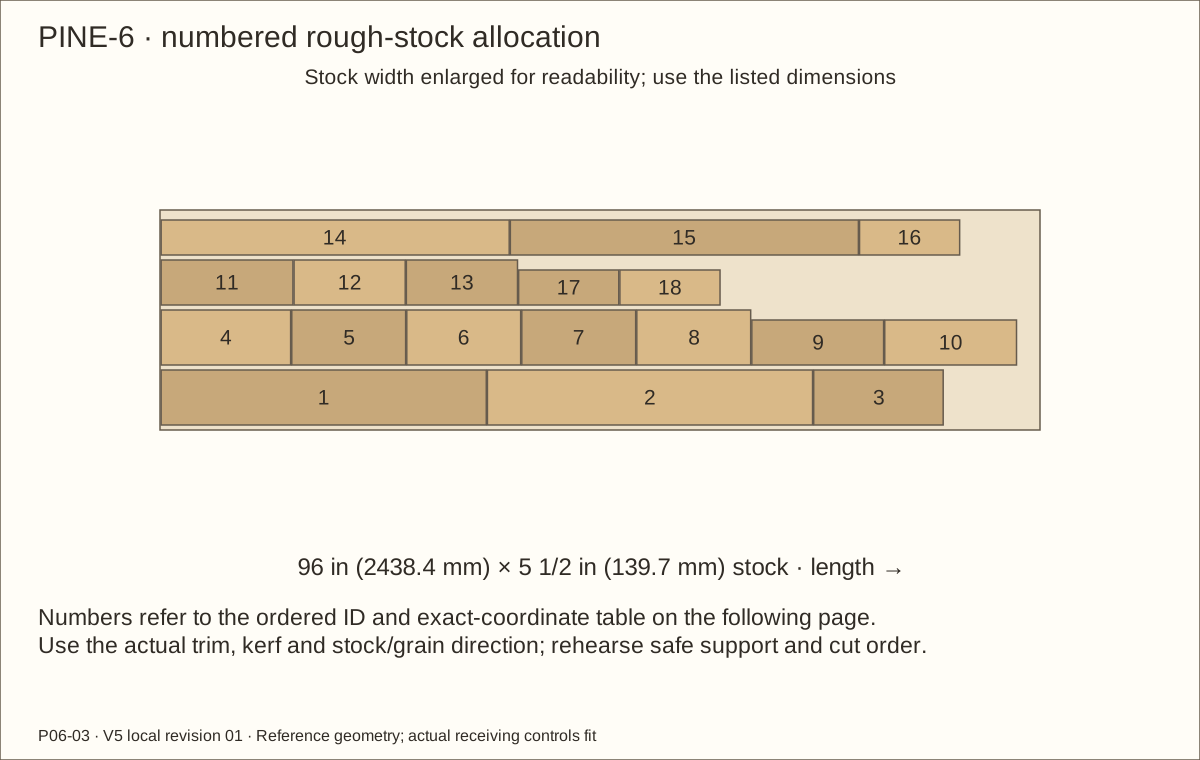
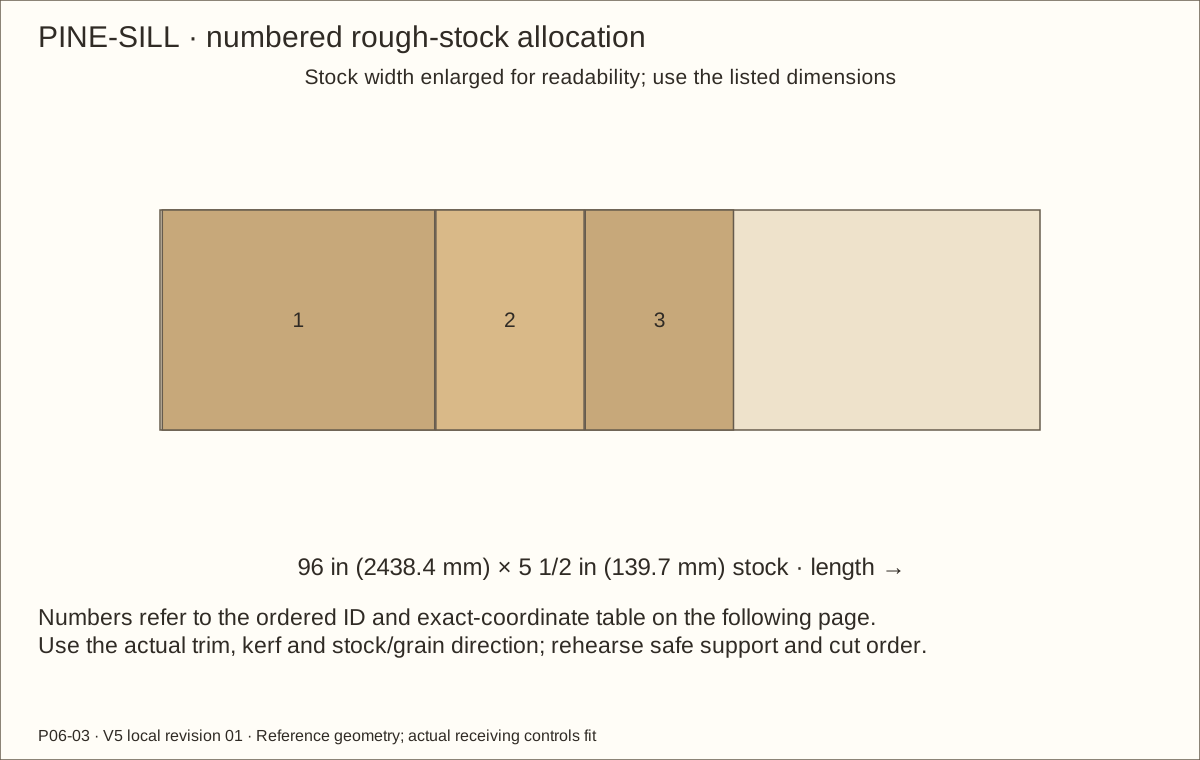
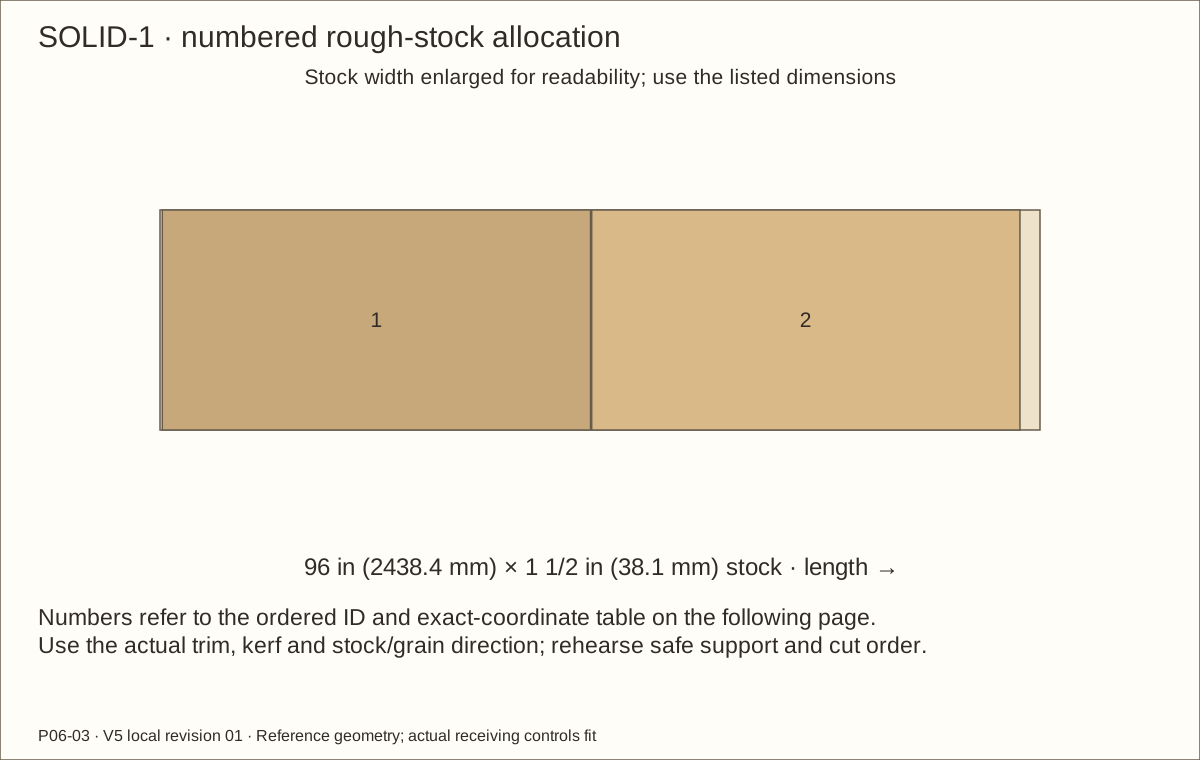
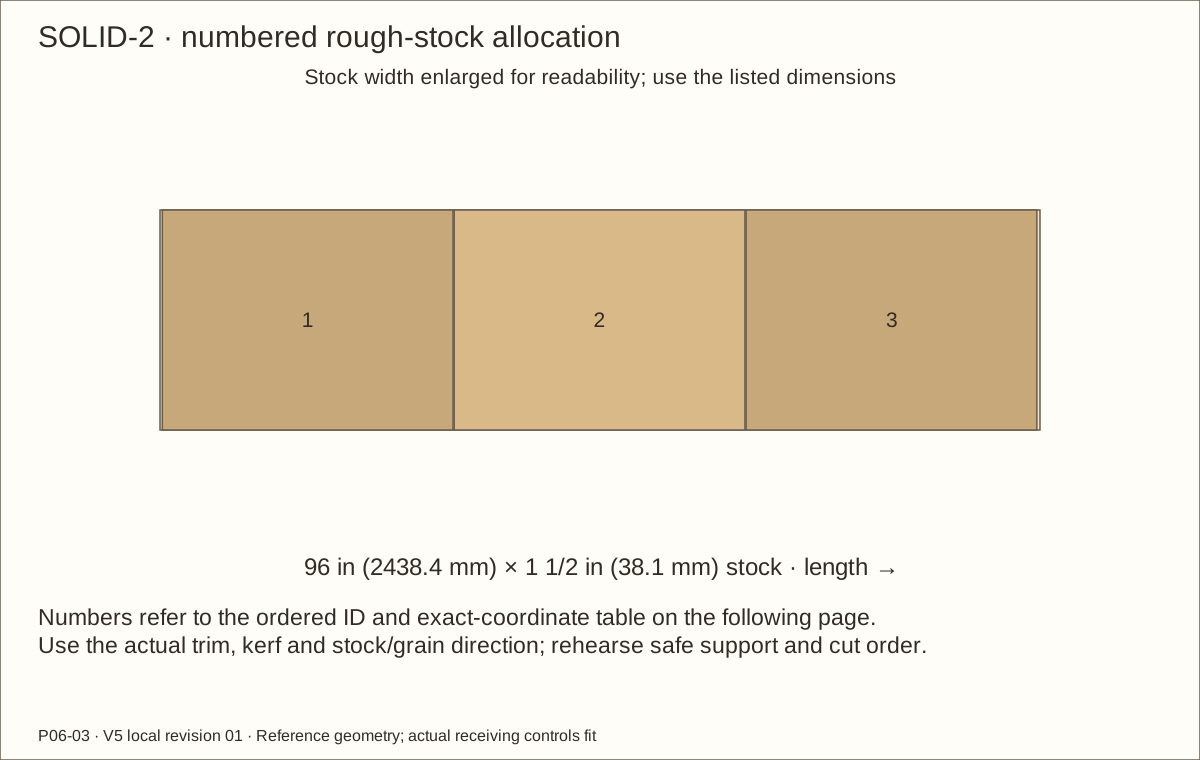
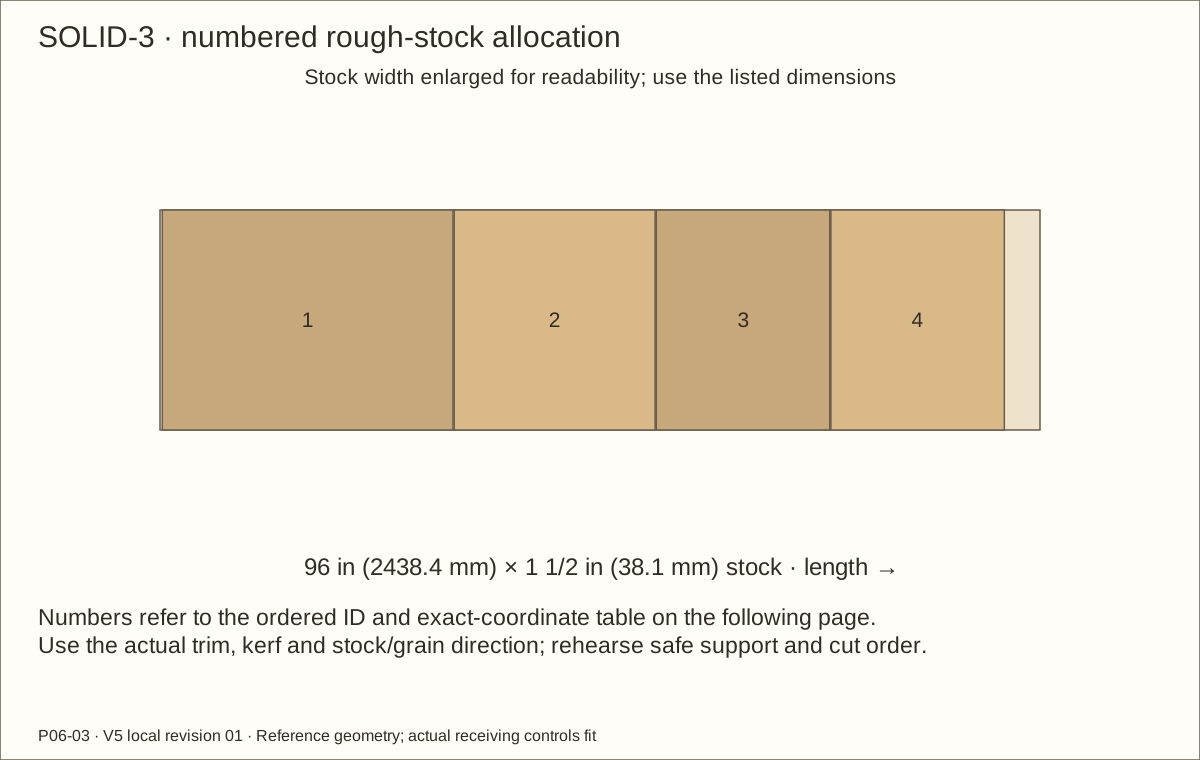
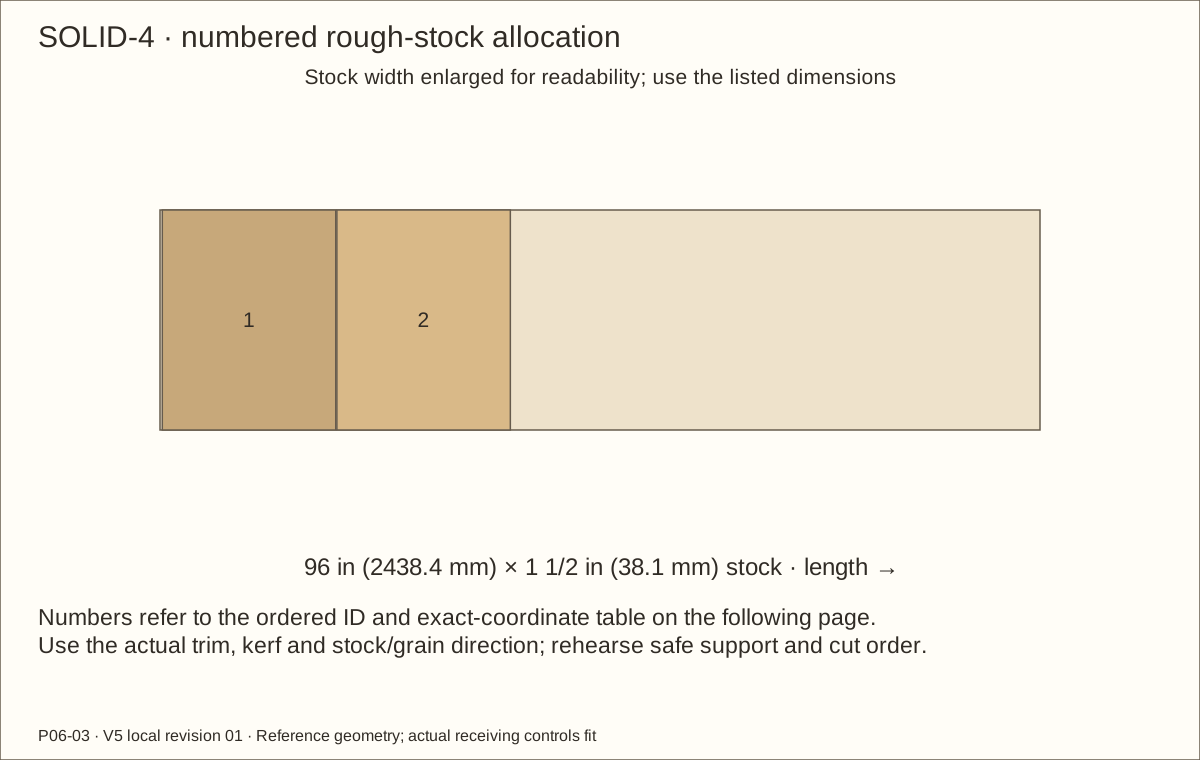
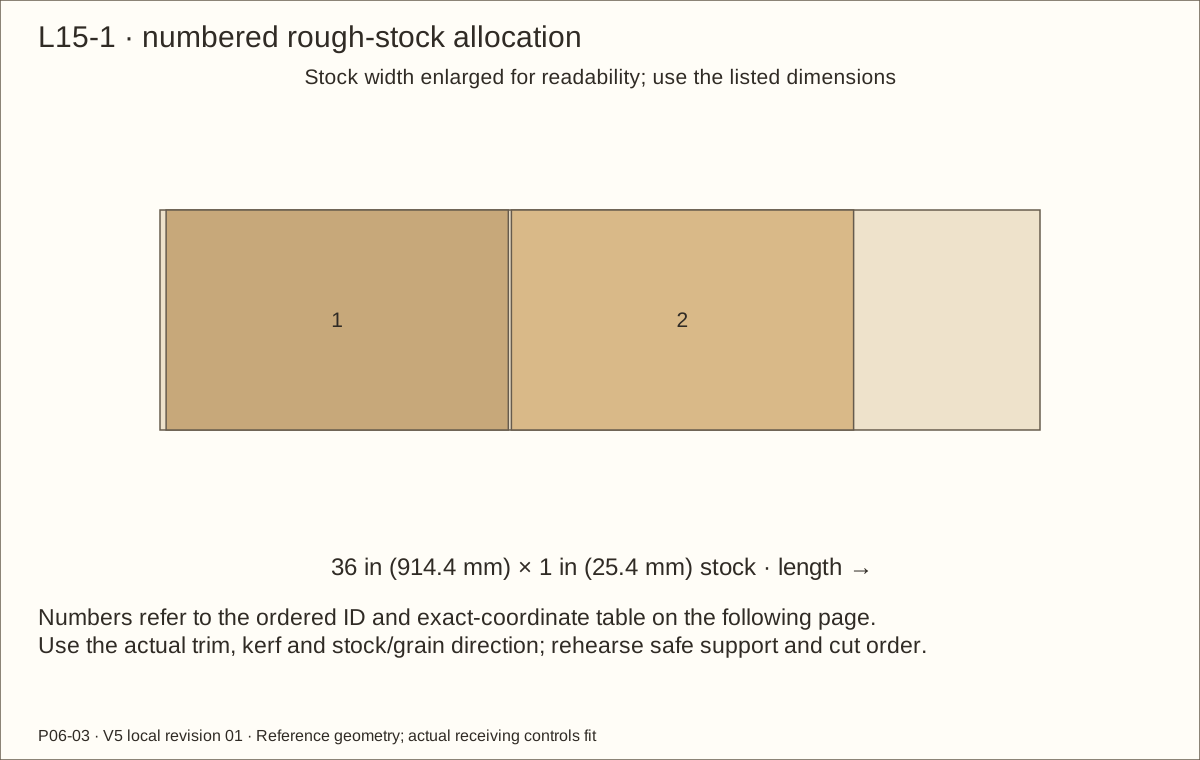
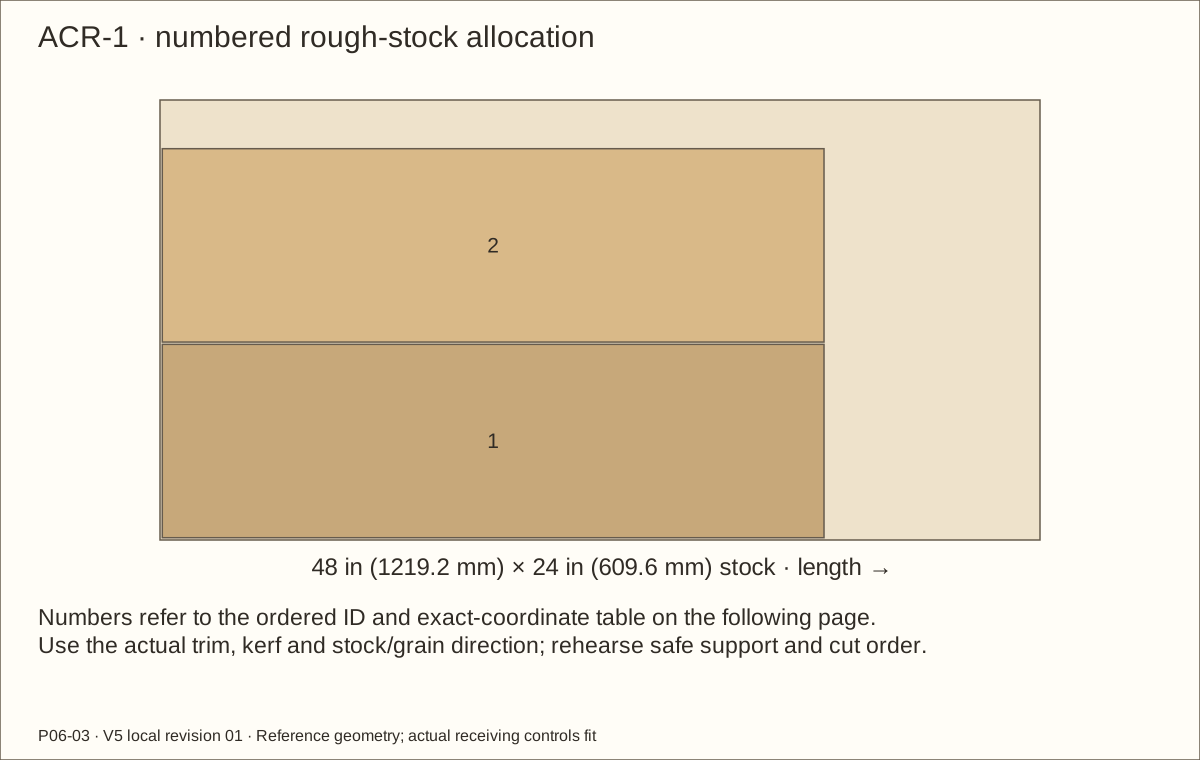
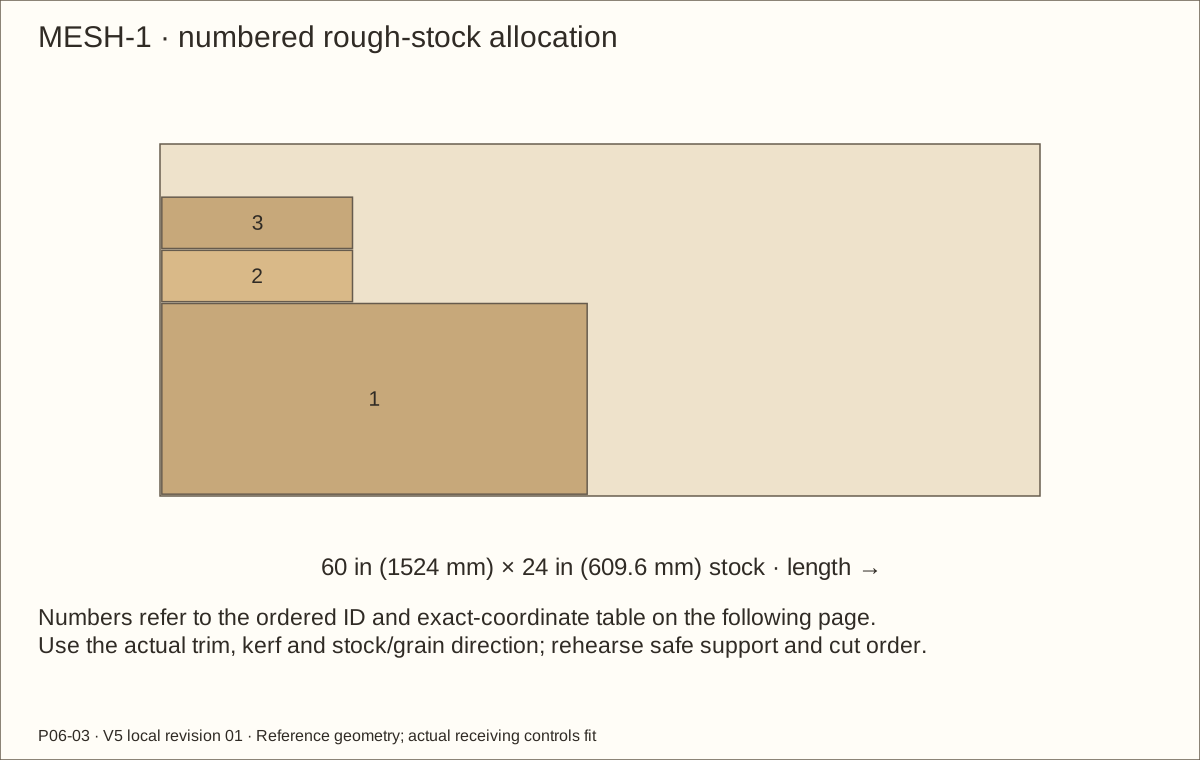
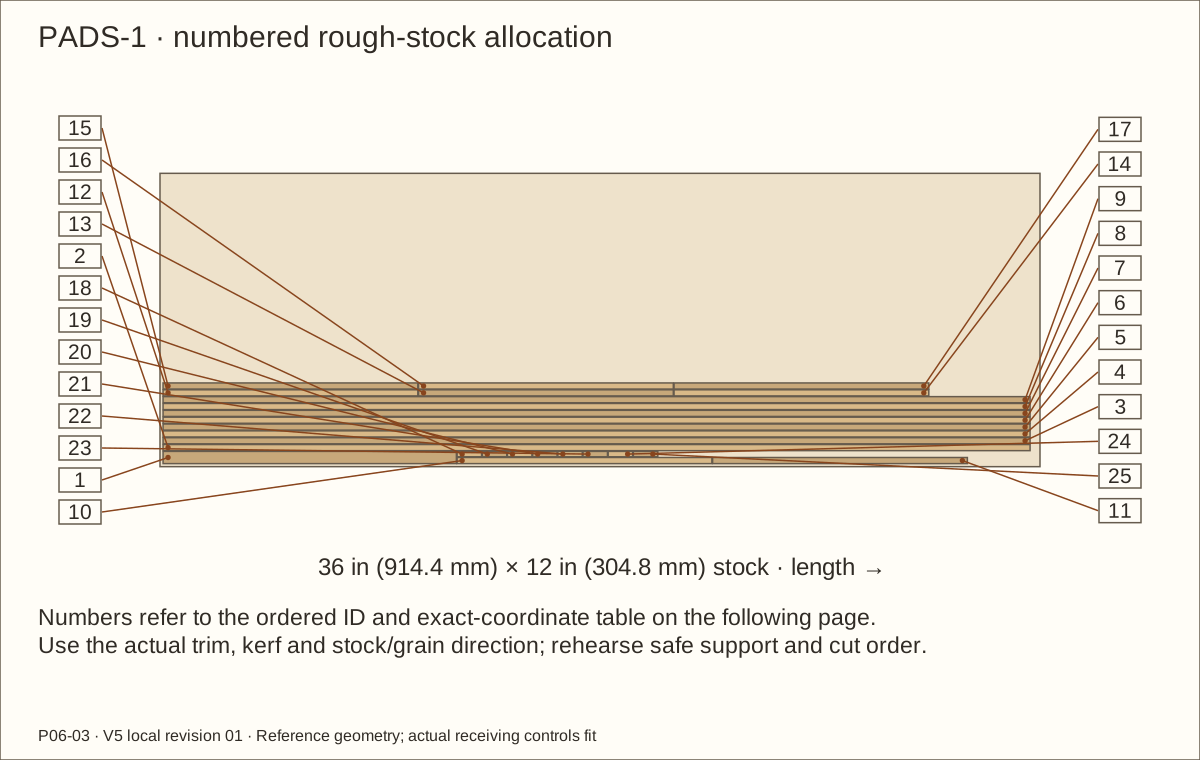
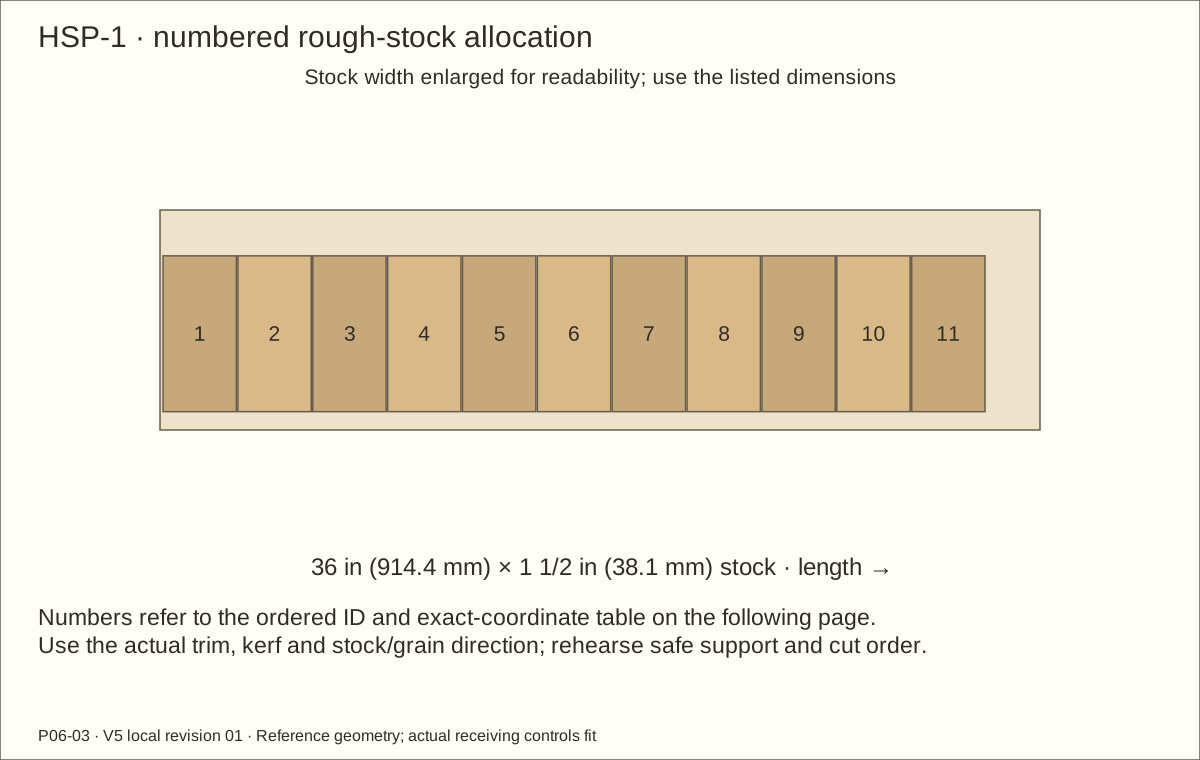
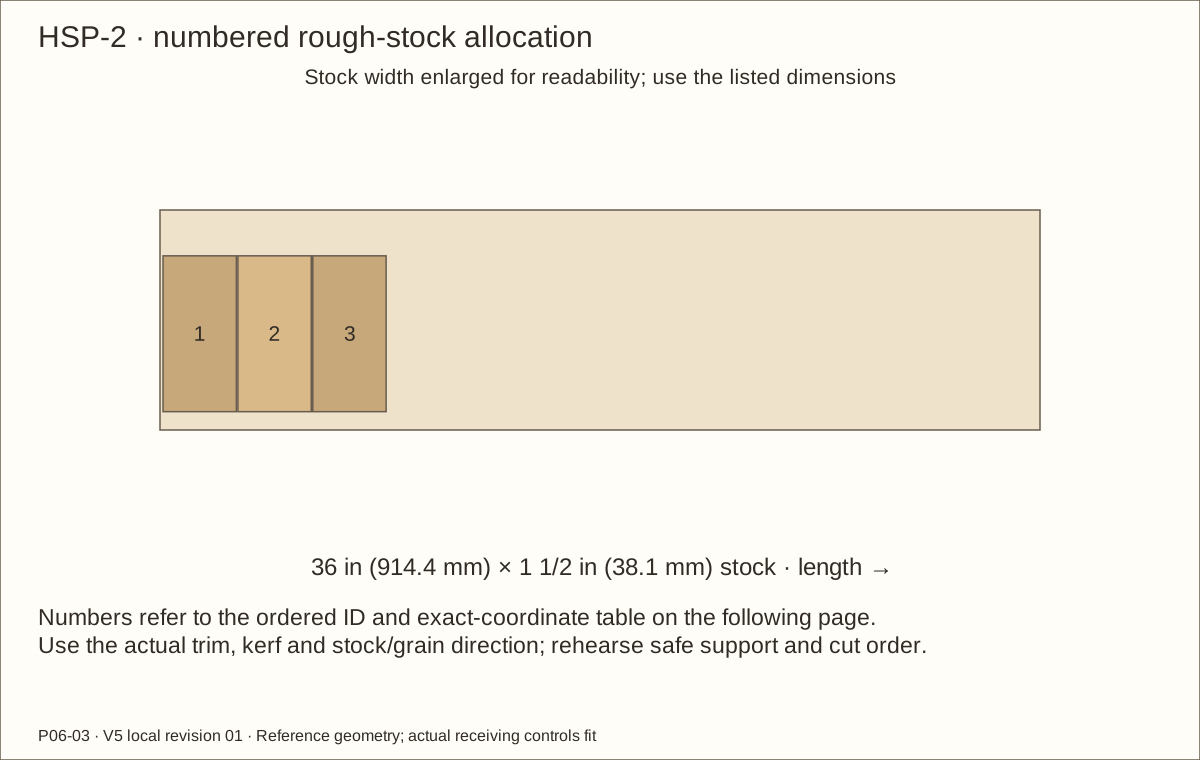
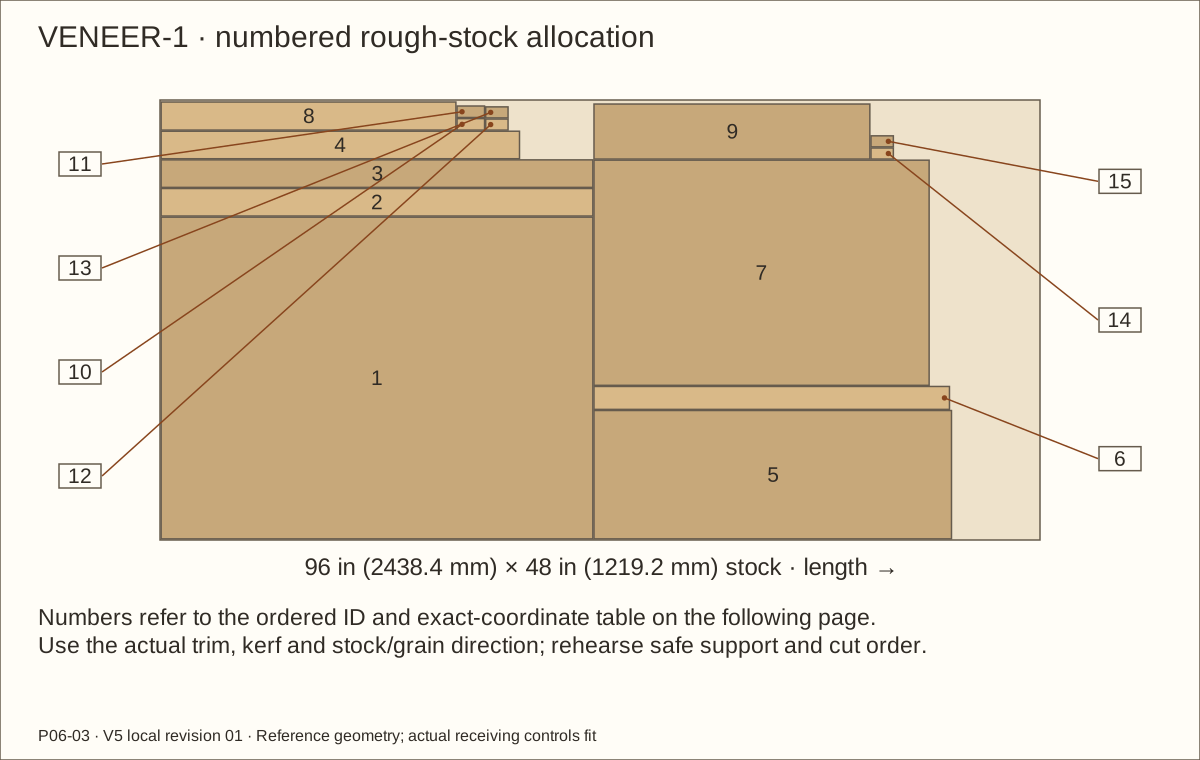
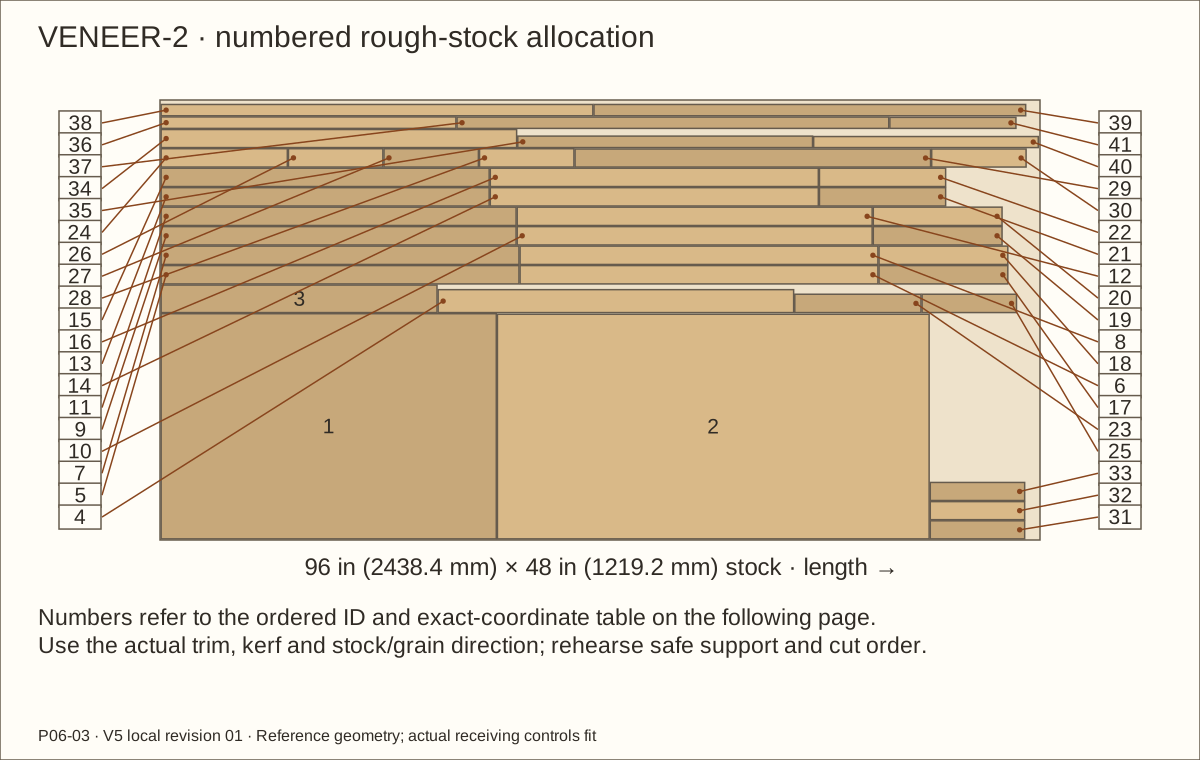
Follow the numbered stock layouts with their exact coordinates, grain, trim and kerf. The reference wood kerf is 1/8 in (3.18 mm); revise allocation for the actual blade or defective stock.
Keep installed blanks separate from two complete trial pine boards, the solid-stock trial and the full-size veneer trial. The full-width sill board has end trim but no spare rip width.
Pine strip allocations include 1/8 in (3.18 mm) extra rip width beyond the cut table’s pre-fit sizes. Trim to those sizes before final fitting. Make long supported cuts before narrowing strips; label each blank. Exact final decimals govern fitting; rounded tape equivalents are only orientation.
Check before continuing: Every installed part and trial allowance has a feasible assigned blank.
Parts: P01 · Floor; P02 · Roof; P03 · Left side; P04 · Right side; P05 · Back
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
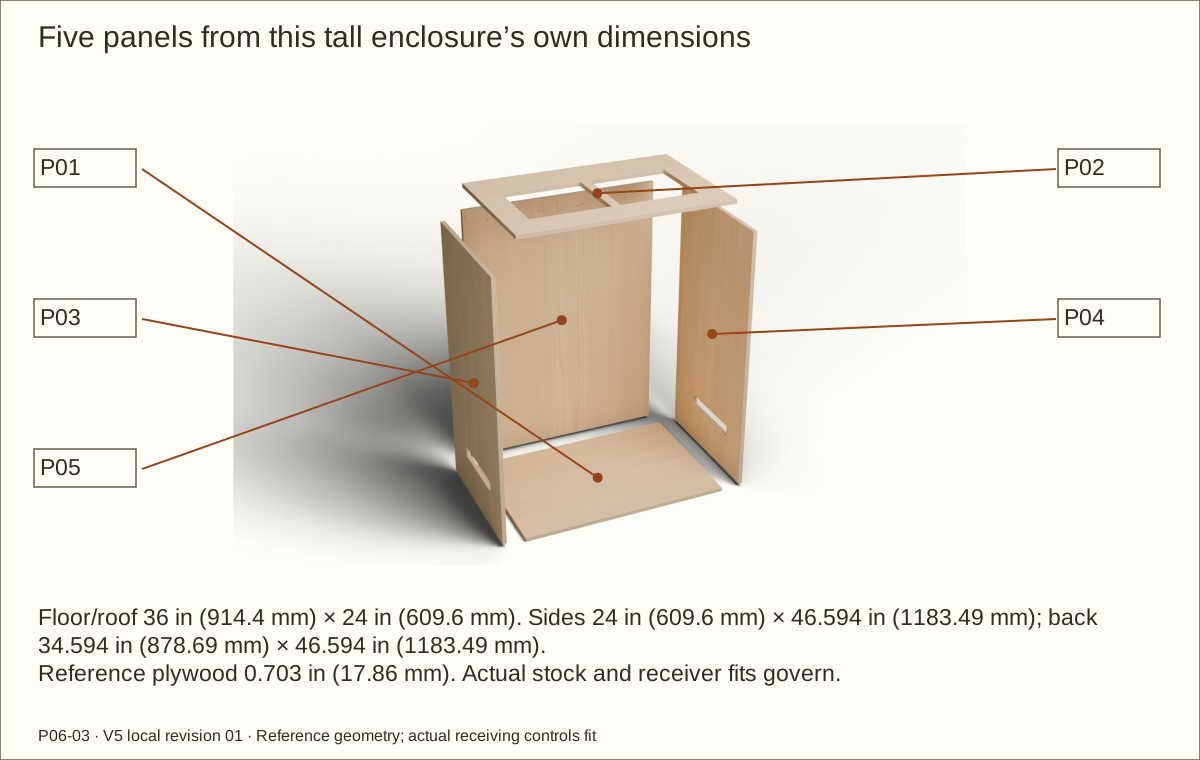
Fit the five case panels
Fit P01 floor and P02 roof at 36 in (914.4 mm) × 24 in (609.6 mm). P03/P04 sides are 24 in (609.6 mm) deep × 46.594 in (1183.49 mm) high between the reference 0.703 in (17.86 mm) floor and roof.
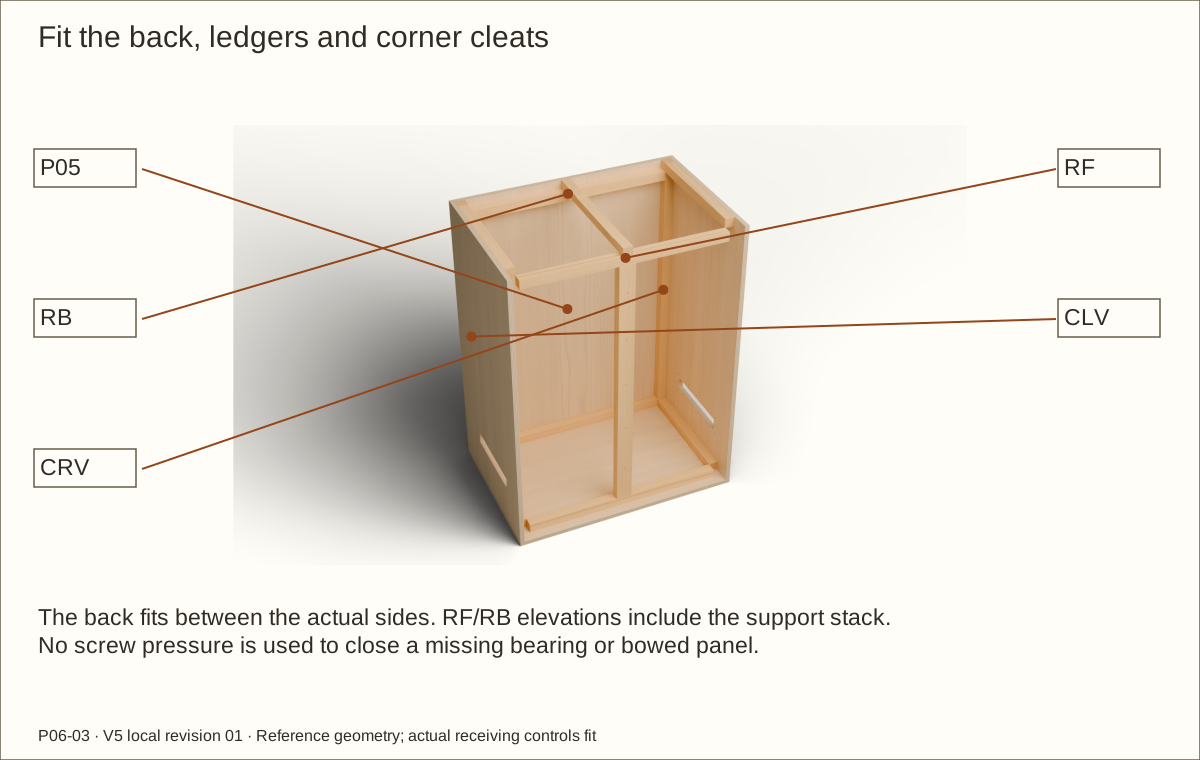
Fit P05 back between the actual sides: reference 34.594 in (878.69 mm) wide × 46.594 in (1183.49 mm) high. Transfer the measured clear gaps with a story stick, a strip marked directly from the assembly.
Check the bare width/depth/height chains close at 36 in (914.4 mm) / 24 in (609.6 mm) / 48 in (1219.2 mm). Keep joint edges square and remove splinters without rounding the measuring faces.
Check before continuing: The dry panels close to the intended bare envelope.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Unsupported waste can tear the face, fall or pinch the cutter.
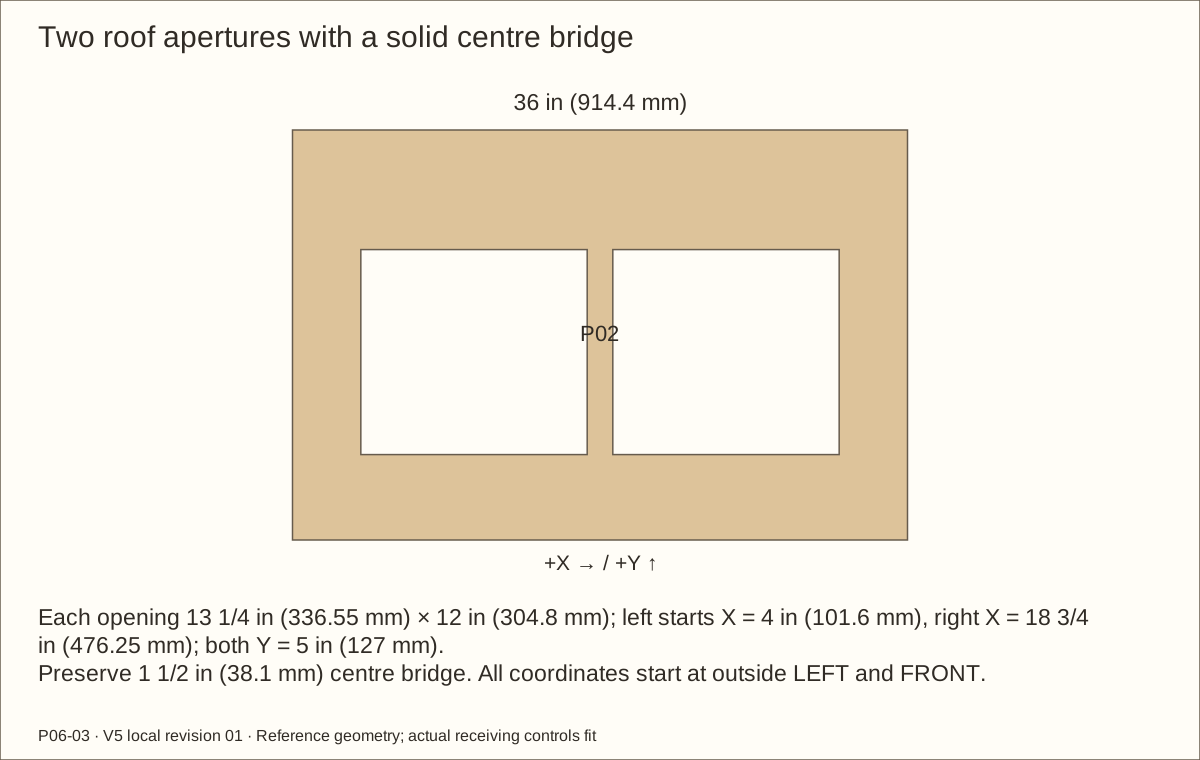
Cut the two roof openings
Mark each opening 13 1/4 in (336.55 mm) wide × 12 in (304.8 mm) deep. The left opening starts at X = 4 in (101.6 mm) and Y = 5 in (127 mm); the right starts at X = 18 3/4 in (476.25 mm) and Y = 5 in (127 mm), from outside LEFT and FRONT.
Preserve the 1 1/2 in (38.1 mm) centre roof bridge. Clamp both the roof and waste; use supported starter and guided cuts for the actual saw/router.
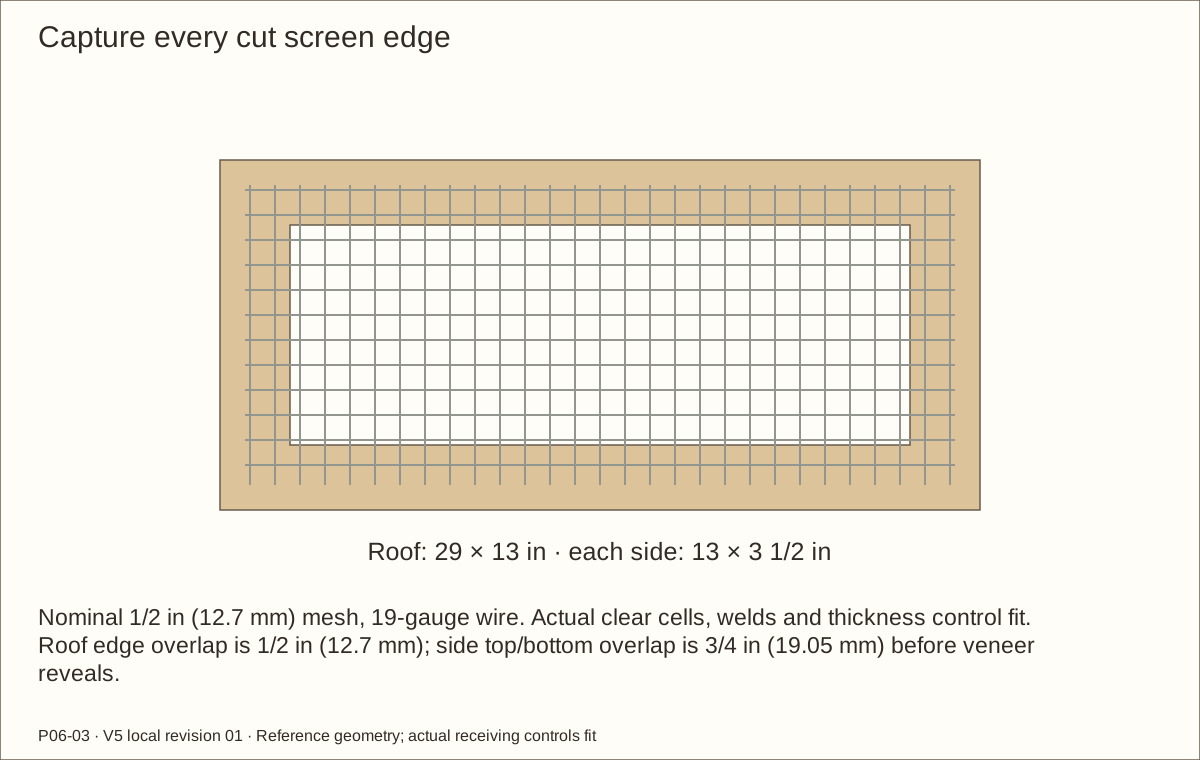
Compare diagonals and the two openings. Dry-position the single 29 in (736.6 mm) × 13 in (330.2 mm) mesh blank below both, beginning at X = 3 1/2 in (88.9 mm) and Y = 4 1/2 in (114.3 mm).
Check before continuing: Both openings, border and centre bridge match their own datums.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
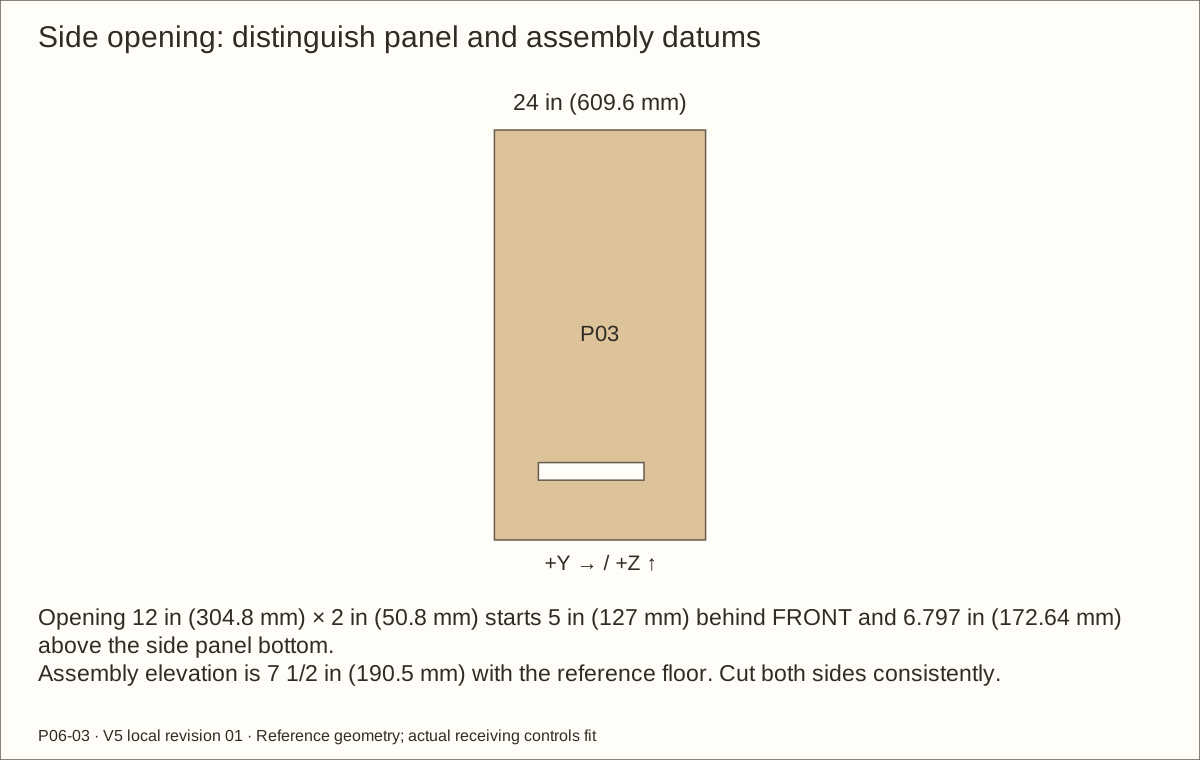
Cut matching side ventilation openings
Mark each 12 in (304.8 mm)-long × 2 in (50.8 mm)-high opening, starting 5 in (127 mm) behind the side FRONT edge and 6.797 in (172.64 mm) above the panel bottom.
With the reference floor fitted, the opening bottom is 7 1/2 in (190.5 mm) above floor underside. Keep panel-local and assembly datums distinct.
Support the waste during cutting. Compare paired sides and dry-position each revised 13 in (330.2 mm) × 3 1/2 in (88.9 mm) mesh blank and four inside battens.
Check before continuing: The two apertures and mesh overlaps agree.
Parts: CLB · L side B cleat; CRB · R side B cleat; CFB · F floor cleat; CBB · B floor cleat; RF · F roof ledger; RB · B roof ledger; CCa · Front bearing column layer A; CCb · Front bearing column layer B; RC · Roof centre rib
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Fit cleats, ledgers and the bearing column
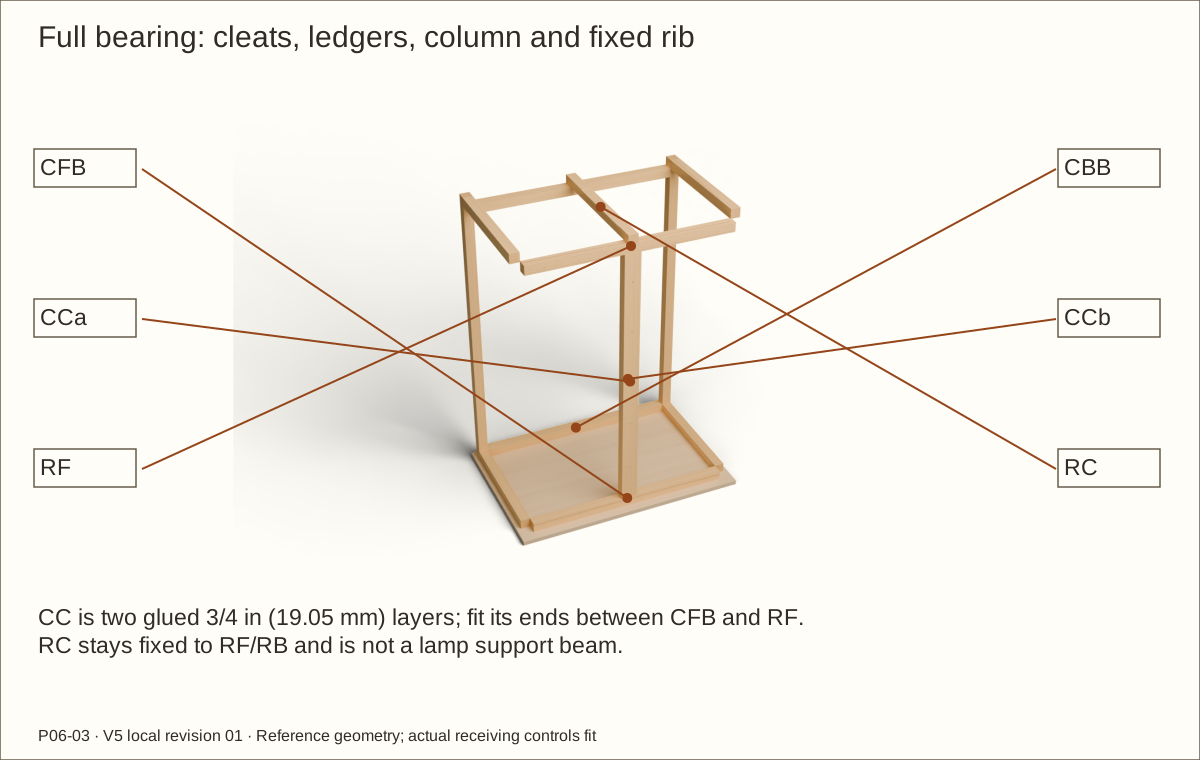
A cleat receives joint screws; a ledger supports a horizontal member. Fit the named 1 1/2 in (38.1 mm) square pine cleats and ledgers to their actual gaps. Use the complete cut schedule.
Glue two 2 1/2 in (63.5 mm)-wide × 3/4 in (19.05 mm)-thick CC layers into a 1 1/2 in (38.1 mm)-deep column. Reference length is 42.26 in (1073.4 mm) between the front floor cleat and RF ledger. Fit actual bearings without gaps.
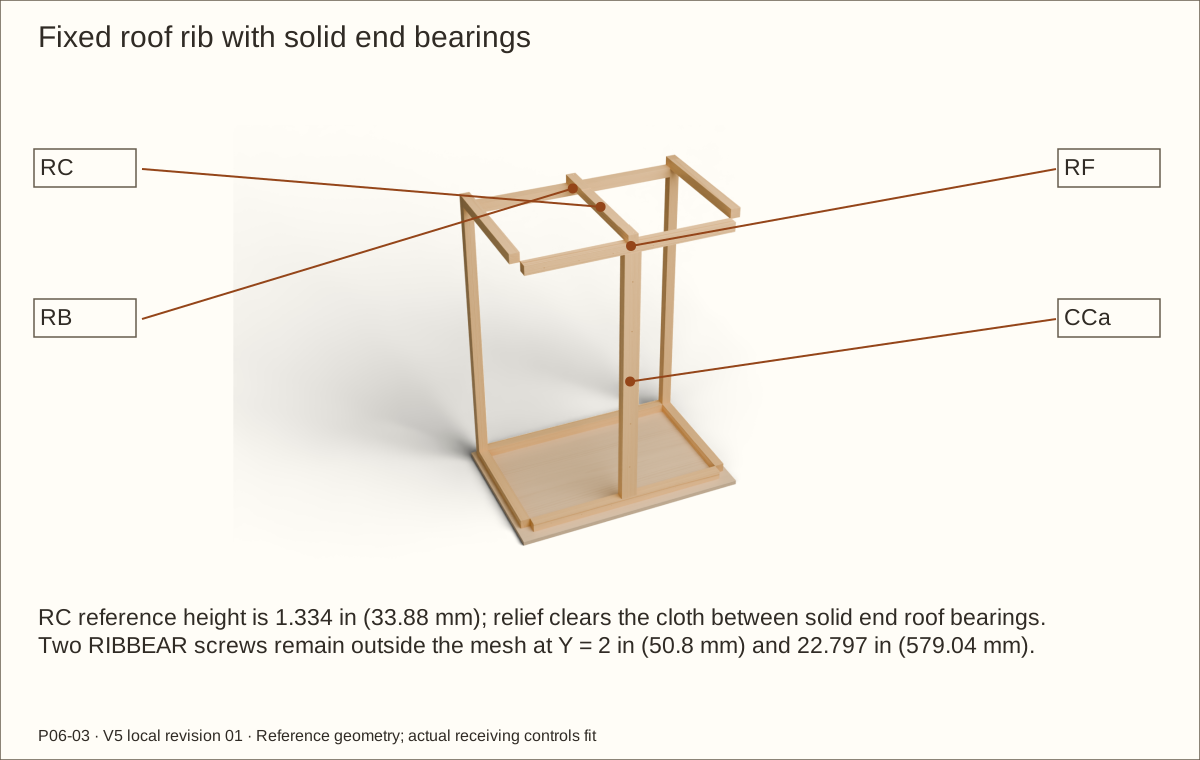
RC is the fixed central roof rib, reference 21.797 in (553.64 mm) long × 1 1/2 in (38.1 mm) wide × 1.334 in (33.88 mm) high before its screen relief. Keep it distinct from the removable roof captures and optional fixture strips.
Check before continuing: Every intended bearing fits fully without a hidden short part.
Required wait: Keep the laminated column clamped for the maker-required period: stressed joints require 24 hours. Do not stress it for at least 24 hours; allow longer when conditions require. Use the glue conditions explained in OP15.
Parts: FA · Front outer stile; FB · Front outer stile; FC · Front sill rail; FD · Front head rail; FE · Front centre stile; FF · Rear centre stile
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Dry-stack the fixed front layers
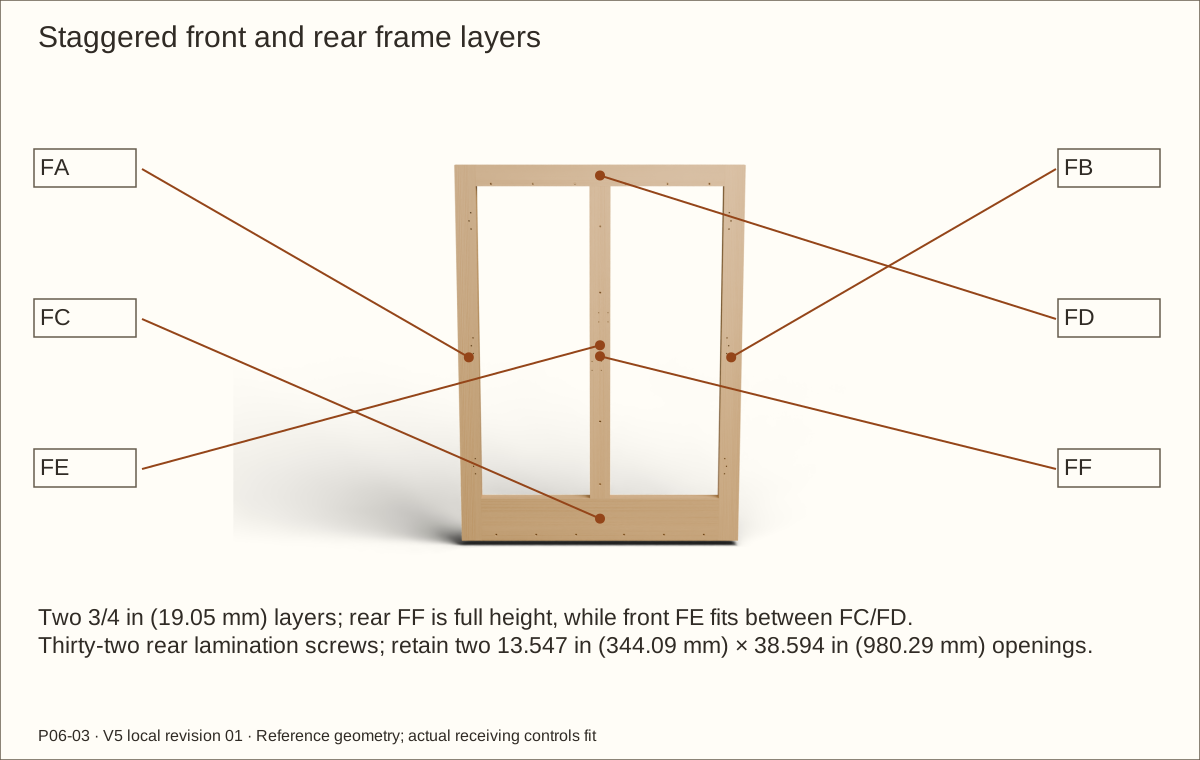
Front FA/FB are full-height outer stiles, the vertical members. Fit FC sill and FD header between them; FE fills between those rails at centre.
The rear layer staggers the joints: FF is full height at centre, FGL/FGR are sill halves and FHL/FHR header halves, with FI/FJ between the rear rails.
Dry-stack square and flush on a flat bench. Each opening is reference 13.547 in (344.09 mm) wide × 38.594 in (980.29 mm) high. Label the layer and orientation before separating.
Check before continuing: The two flush openings are square and all joints overlap correctly.
Parts: FA · Front outer stile; FB · Front outer stile; FC · Front sill rail; FD · Front head rail; FE · Front centre stile; FF · Rear centre stile
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Glue and screw the fixed front
Apply Titebond III only to clean bare mating faces. Use the maker spread and working time; the conservative application minimum is 47°F (8.3°C).
Clamp both layers flat and square with cauls. Install the 32 rear-entry #8 × 1 1/4 in (31.75 mm) frame-lamination screws at their station coordinates; clear the rear layer and stop the pilot in the front layer.
Remove squeeze-out from later pane, veneer and hardware areas. Recheck diagonals and flatness before leaving the assembly clamped.
Check before continuing: All overlapping joints seat, screw tips are buried and the frame remains flat.
Required wait: Maker guidance: 30–60 minutes clamping for unstressed joints; stressed joints require 24 hours. Do not stress these assemblies for at least 24 hours; cold conditions can require longer.
Parts: D1A · Door 1 A; D1B · Door 1 B; D1C · Door 1 C; D1D · Door 1 D; D1E · Door 1 E; D1F · Door 1 F; D1G · Door 1 G; D1H · Door 1 H
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Cut and dry-stack both laminated doors
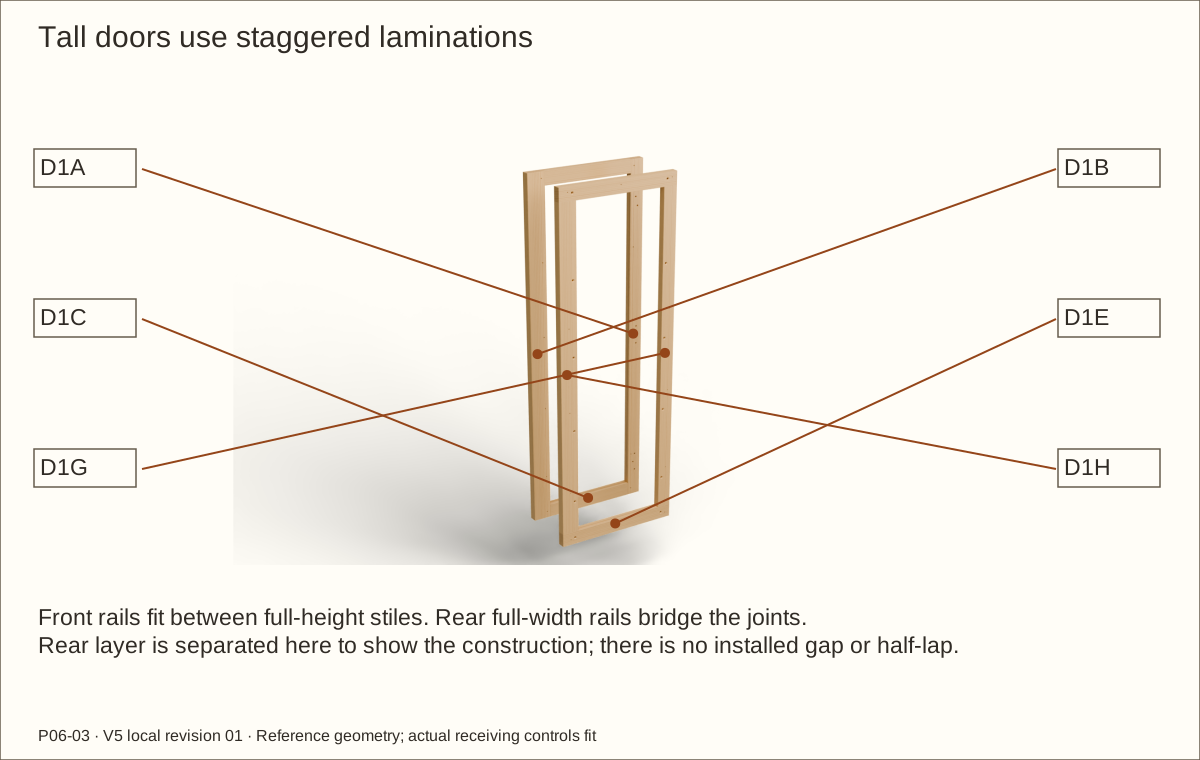
Each door uses two 3/4 in (19.05 mm) pine layers. Front rails C/D fit between full-height A/B stiles. Rear full-width rails E/F bridge those joints; short rear stiles G/H fit between them.
Keep the 2 in (50.8 mm) latch stile at centre and 1 1/2 in (38.1 mm) hinge stile outside. Mirror that relationship on Door 2. These are staggered laminations, not half-laps.
Dry-stack the original 13.297 in (337.74 mm) × 38.344 in (973.94 mm) outside frame with its 9.797 in (248.84 mm) × 35.344 in (897.74 mm) viewing opening. Fit the outside perimeter only after glue cure.
Check before continuing: Both layer stacks are square, flush and correctly handed.
Parts: D1A · Door 1 A; D1B · Door 1 B; D1E · Door 1 E; D1F · Door 1 F; D2A · Door 2 A; D2B · Door 2 B
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Glue and fasten the tall door layers
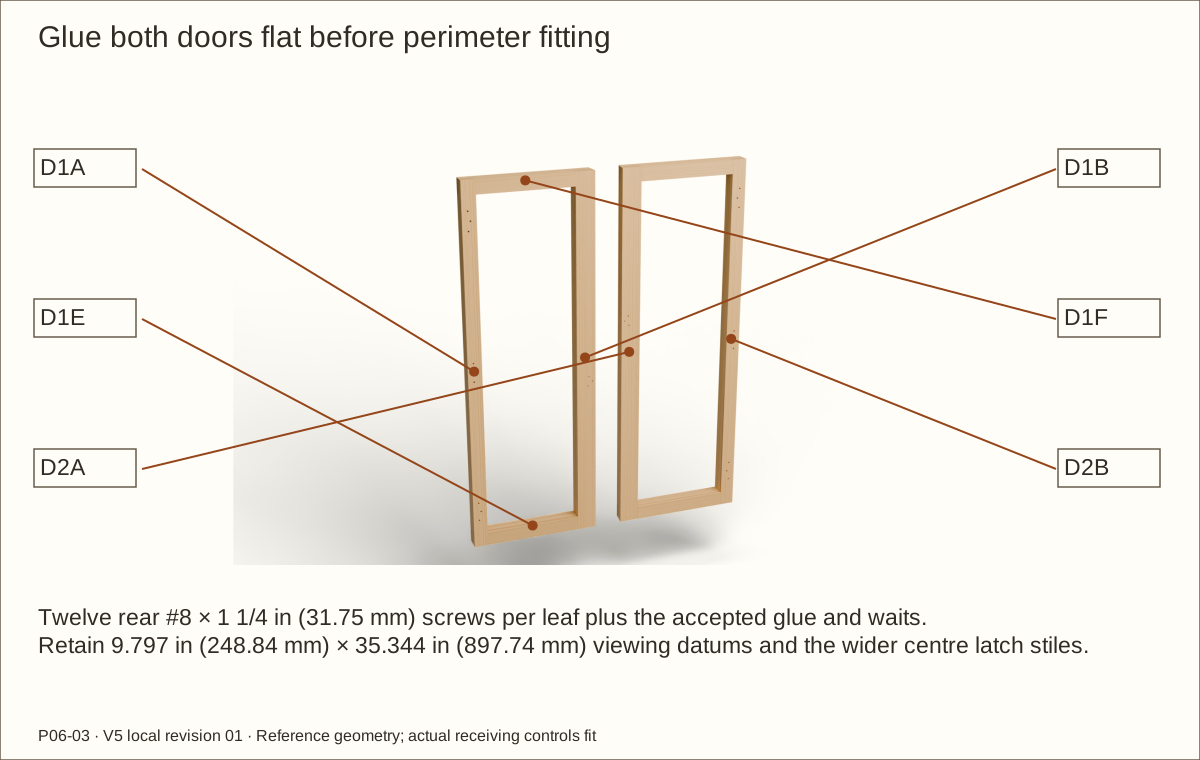
Glue the bare mating layers and clamp each frame flat on cauls. Compare diagonals without forcing a twisted member into position.
Install twelve #8 × 1 1/4 in (31.75 mm) rear-entry lamination screws per leaf at the listed DL stations. Make rear clearance holes and stopped pilots with the pane absent.
Clear squeeze-out from future contacts. Keep viewing opening datums and the wide centre latch stiles unchanged.
Check before continuing: Each complete leaf stays flat, with seated overlapping joints and buried tips.
Required wait: Keep the confirmed clamp and 24-hour minimum no-stress wait before trimming or hanging.
Parts: D1A · Door 1 A; D1B · Door 1 B; D1E · Door 1 E; D1F · Door 1 F; FE · Front centre stile
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: The unmodified source 1/8 in (3.18 mm) gaps do not provide sufficient full-veneer allowance.
Fit bare gaps for all veneer layers
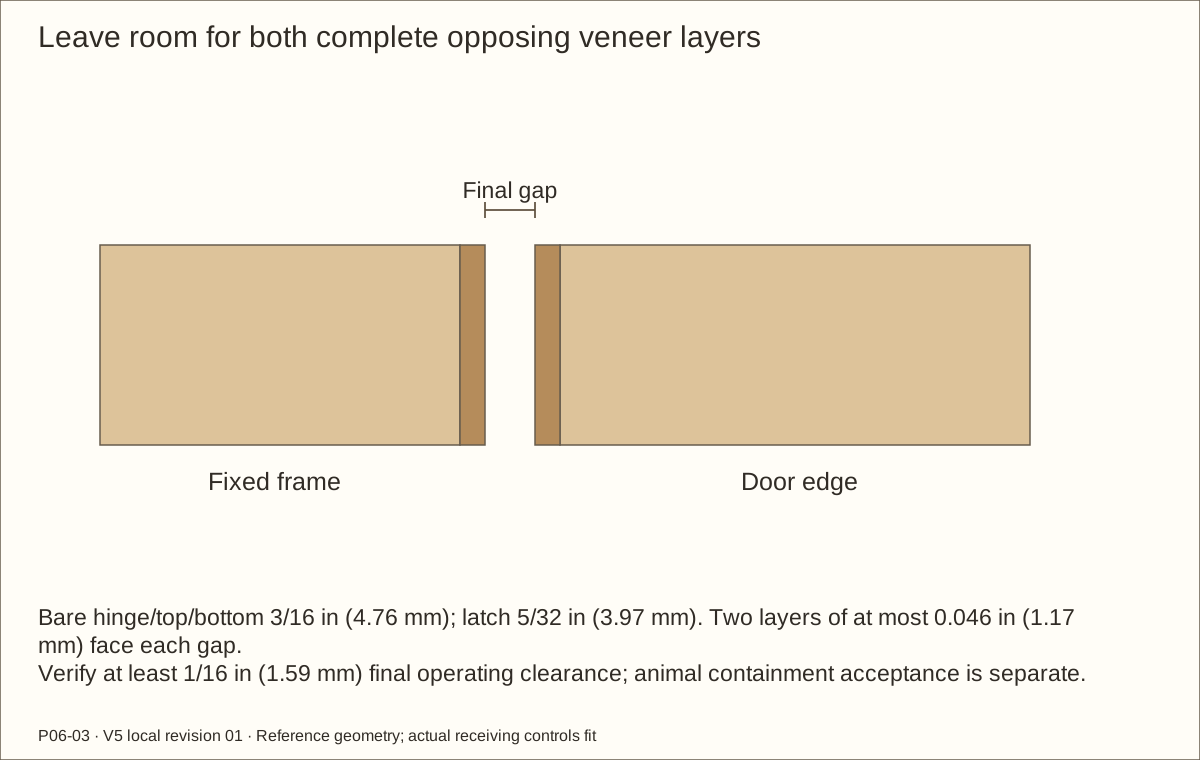
After cure, remove 1/16 in (1.59 mm) from the original hinge edge and each top/bottom edge, and 1/32 in (0.79 mm) from the latch edge. Preserve the viewing and rear-glazing datums.
Reference fitted bare leaves are 13.20325 in (335.36 mm) wide × 38.219 in (970.76 mm) high. Fit actual openings for 3/16 in (4.76 mm) hinge/top/bottom gaps and 5/32 in (3.97 mm) latch gaps.
Two maximum 0.046 in (1.17 mm) opposing finished layers leave 0.06425 in (1.63 mm) at the latch. Verify at least 1/16 in (1.59 mm) final gap everywhere, with separate animal containment acceptance.
Check before continuing: The bare perimeter allows the complete accepted veneer and finish.
Parts: D1B · Door 1 B; D1H · Door 1 H; D2A · Door 2 A; D2G · Door 2 G
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Bevel each rear latch edge
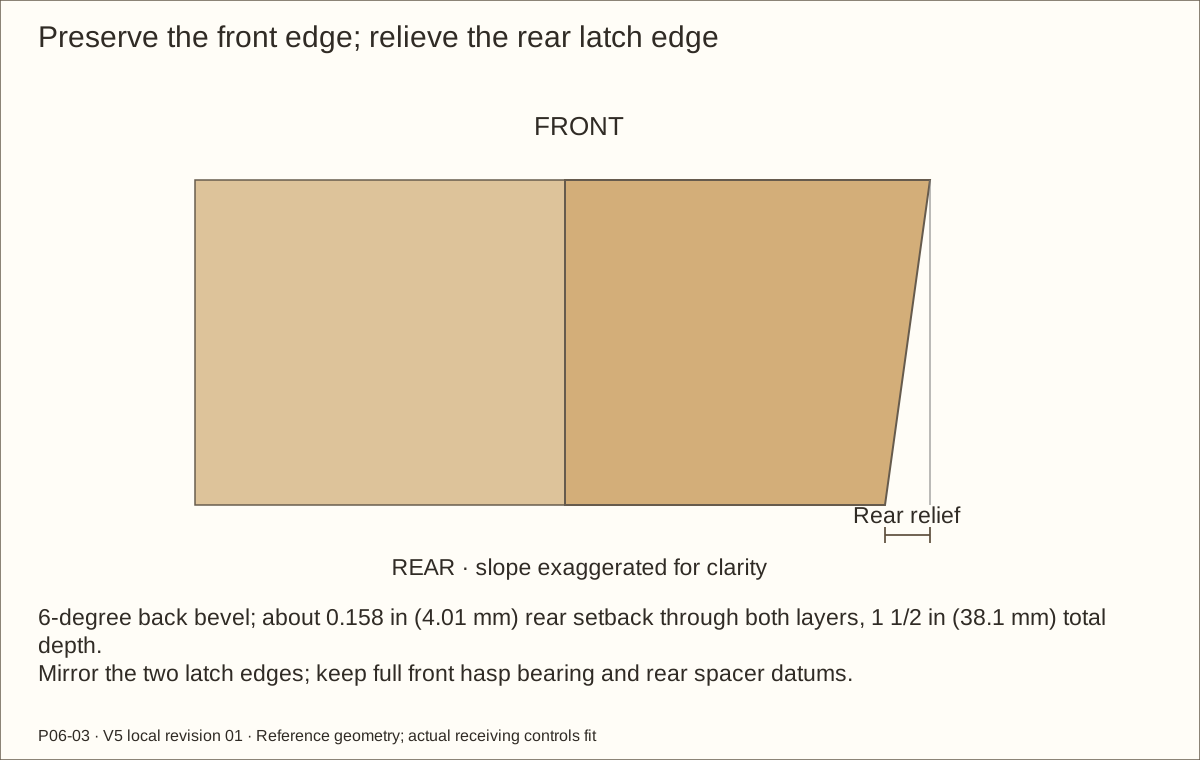
A back bevel slopes inward at the rear while preserving the front edge. Trial a 6-degree bevel on the left door’s right edge and the right door’s left edge.
Across the full 1 1/2 in (38.1 mm) depth, reference rear setback is about 0.158 in (4.01 mm). Preserve the laminated bond, front size, hasp bearing and glazing spacer positions.
Dry-swing supported leaves on accepted hardware. Later cover each sloping edge with its own veneer strip and trim it without bridging a joint.
Check before continuing: The rear latch edges clear without shortening the front faces.
Parts: Q1L · Door 1 spacer L; Q1B · Door 1 spacer B; B1L · Door 1 retaining bead L; B1B · Door 1 retaining bead B; G1 · Door 1 OPTIX pane
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Thin milling needs a guarded carrier or machining service, not short loose feeds.
Make the spacers, beads and acrylic panes
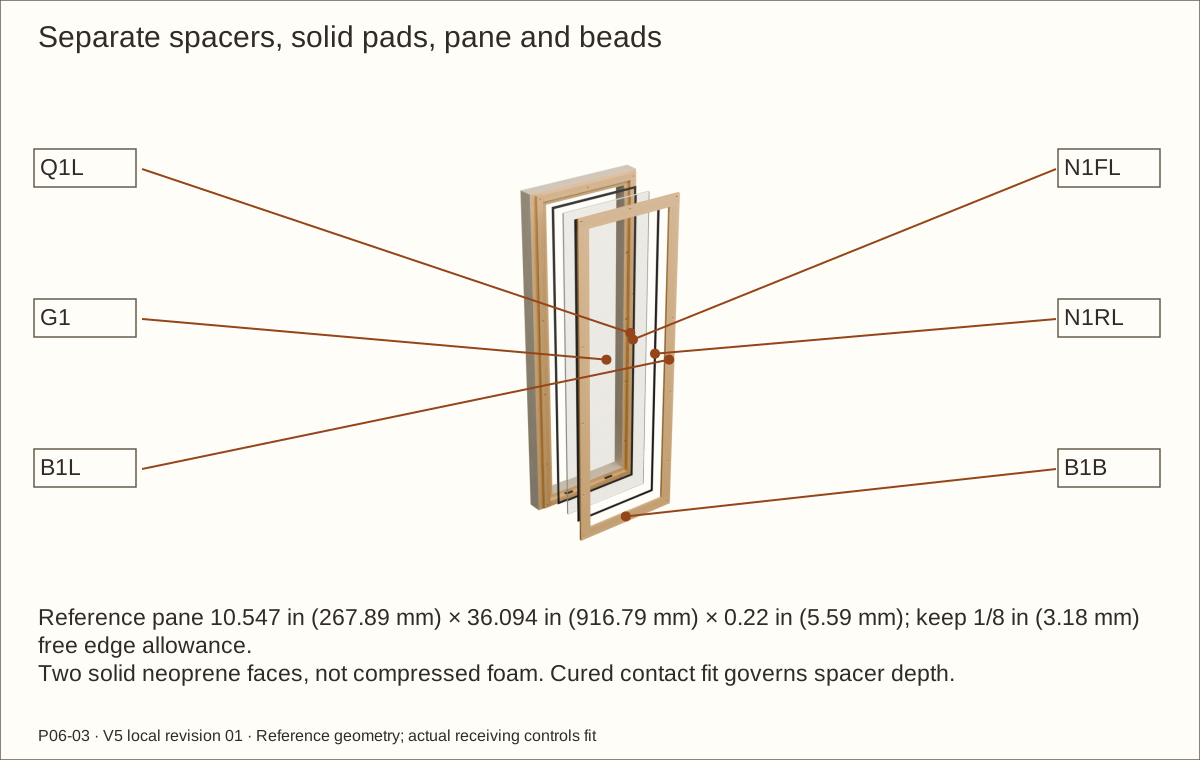
Mill supported long pine stock before ripping: spacers are 3/4 in (19.05 mm) wide and begin at 3/8 in (9.53 mm) rough thickness; beads are 1 1/4 in (31.75 mm) wide × 1/4 in (6.35 mm) thick. Use the accepted cured-stack depth.
Each reference pane is 10.547 in (267.89 mm) wide × 36.094 in (916.79 mm) high × 0.22 in (5.59 mm) thick. Confirm its actual pocket is 1/4 in (6.35 mm) larger overall in each direction, leaving 1/8 in (3.18 mm) at each edge.
Keep acrylic masking while cutting on a supported setup recommended by its maker. Clean debris with compatible products. Never drill through the pane.
Check before continuing: The correctly labeled panes fit freely inside their spacer frames.
Parts: Q1L · Door 1 spacer L; Q1R · Door 1 spacer R; B1L · Door 1 retaining bead L; B1R · Door 1 retaining bead R; B1B · Door 1 retaining bead B; B1T · Door 1 retaining bead T
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Transfer and trial the bead screws
Lay the supported door rear upward. Dry-fit spacers, actual solid pads and pane, then fit beads so their wood faces stop on the spacer faces.
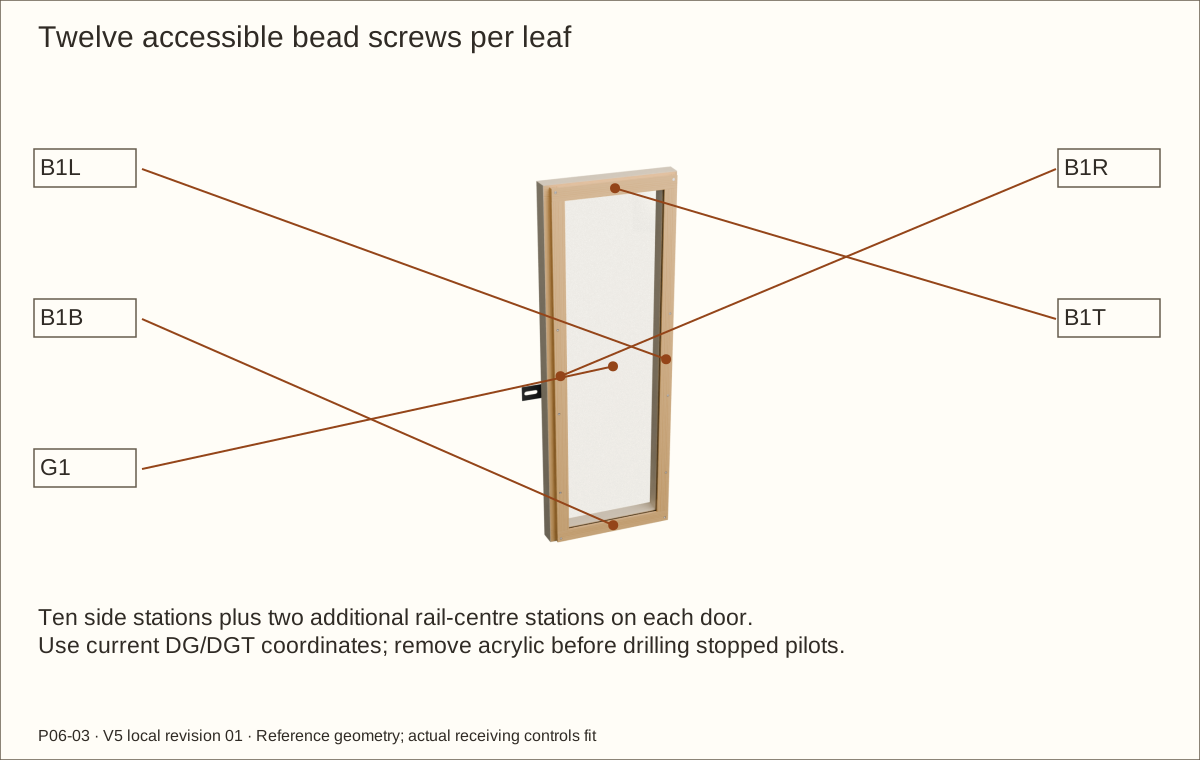
Each leaf has ten side stations and two additional centre rail stations: twelve #6 × 1 1/4 in (31.75 mm) screws per door, twenty-four total. Use DG/DGT station coordinates.
Remove the pane before drilling. Countersink the bead, clear the first members and stop the receiver pilot. Trial light contact, free edges and later pane removal without glue.
Check before continuing: All bead screws are accessible and the pane remains unbowed.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Cut the roof and side capture battens
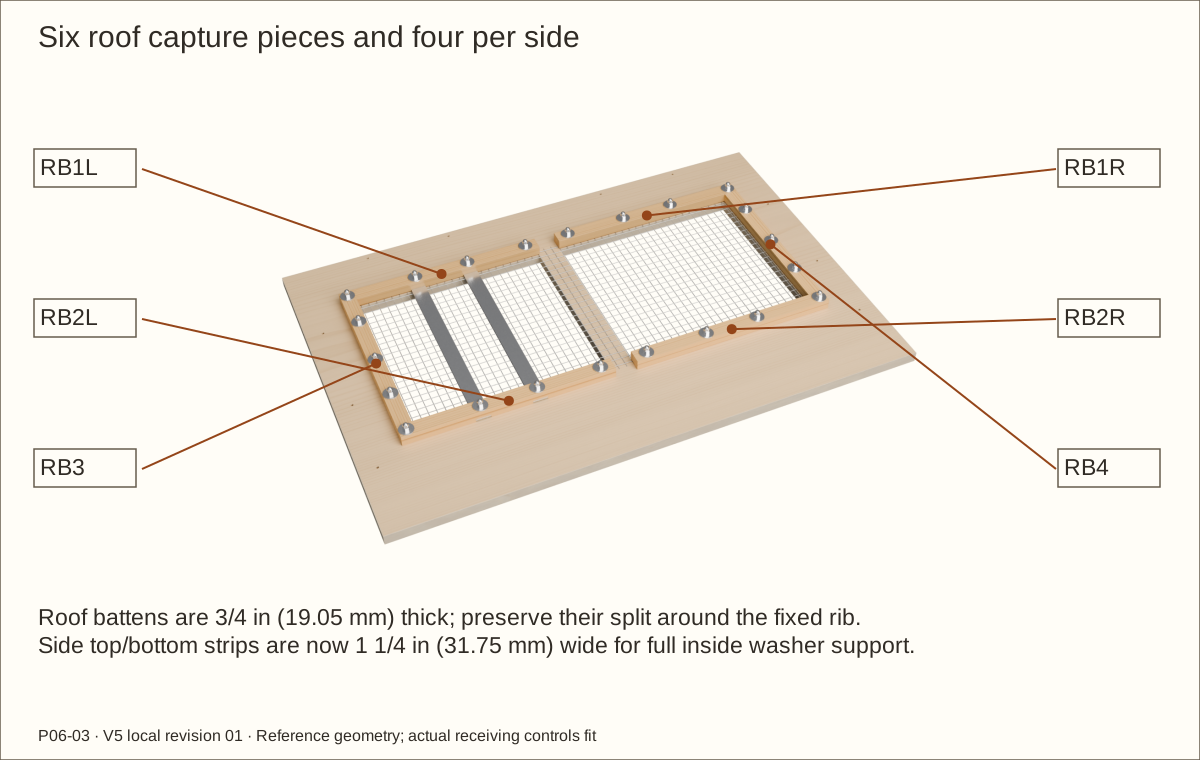
Cut the six 3/4 in (19.05 mm)-thick roof battens to the schedule, keeping the left steel-bearing halves distinct. Leave the centre split around fixed rib RC.
Each side has two 14 in (355.6 mm)-long × 1 1/4 in (31.75 mm)-wide lower/upper battens and two 2 in (50.8 mm)-long × 1 in (25.4 mm)-wide end battens. The wider outer strips preserve full washer bearing at revised drill positions.
Dry-position each piece against its own opening. Mark the plywood-facing face before machining its wire relief.
Check before continuing: All capture parts have the correct IDs, handed positions and full overlap.
Parts: RB1L · Roof capture batten; RB3 · Roof capture batten; VLB · L vent capture B; VLF · L vent capture F; RC · Roof centre rib
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Actual wire/crossing thickness controls this dependent cut; H03 remains open.
Machine fitted wire reliefs and wood lands
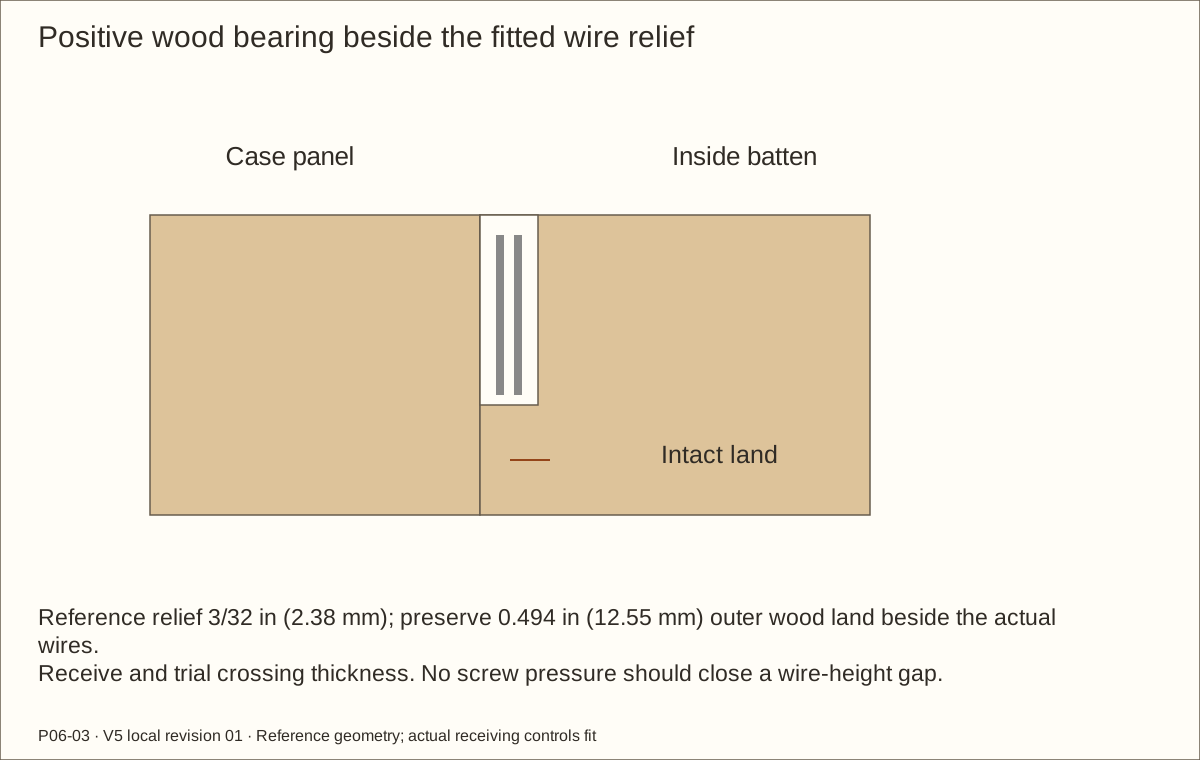
Measure actual welded crossing thickness. Reference relief is 3/32 in (2.38 mm) deep; it must clear the real wires while the outer wood lands seat directly against the case.
Route the specified partial-width reliefs with the piece clamped to a carrier/backer. Preserve the 0.494 in (12.55 mm) reference outer wood land. Do not groove away the entire bearing face.
Relieve the middle of RC under the crossing cloth but retain its solid end roof bearings. Trial every batten and rib interface with received mesh; no screw pressure should close a wire-height gap.
Check before continuing: All wood lands seat positively and no wire is crushed.
Parts: M01 · Roof mesh blank; ML · L vent mesh; MR · R vent mesh
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Wear suitable hand/eye protection for sharp mesh; keep gloves away from powered rotating tools.
Cut and identify the three mesh blanks
Cut roof M01 at 29 in (736.6 mm) × 13 in (330.2 mm). Cut ML/MR side blanks at 13 in (330.2 mm) × 3 1/2 in (88.9 mm); keep each flat and square without damaged welds.
Remove projecting sharp ends where the finished captured edge requires it. Keep the specified overlaps and register the actual grid against the station plan.
Reference 0.541 in (13.74 mm) pitch and 0.041 in (1.04 mm) wire describe nominal 1/2 in (12.7 mm) clear cells. Real cloth can differ; do not drill through a welded wire to force the drawing to fit.
Check before continuing: Mesh fits each relief with captured edges and clear planned screw passages.
Parts: LB1 · Steel strip below the left lamp area; LB2 · Steel strip below the left lamp area; RB1L · Roof capture batten; RB2L · Roof capture batten
Tools / setup: Metal vise, supported saw/drill, 1/4-inch bit, files and caliper
Before you begin: Reference strip geometry is not a tested roof or fixture load rating.
Fit and drill the two roof steel strips
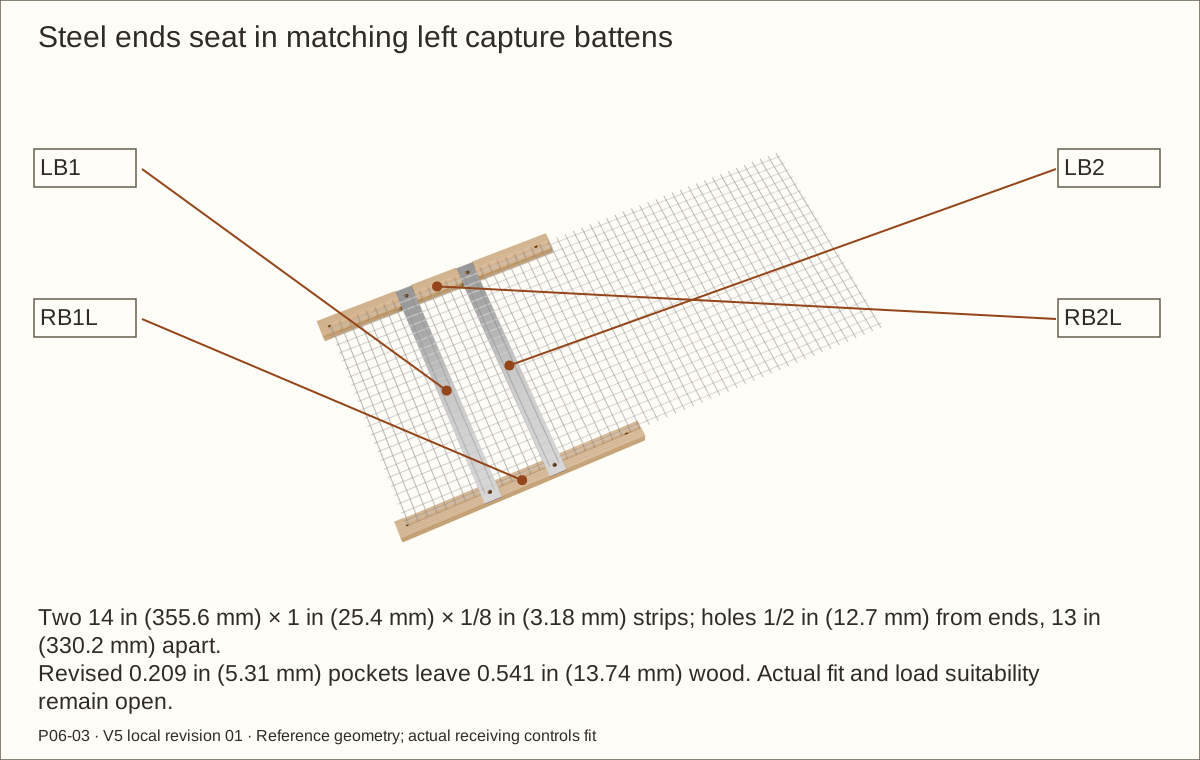
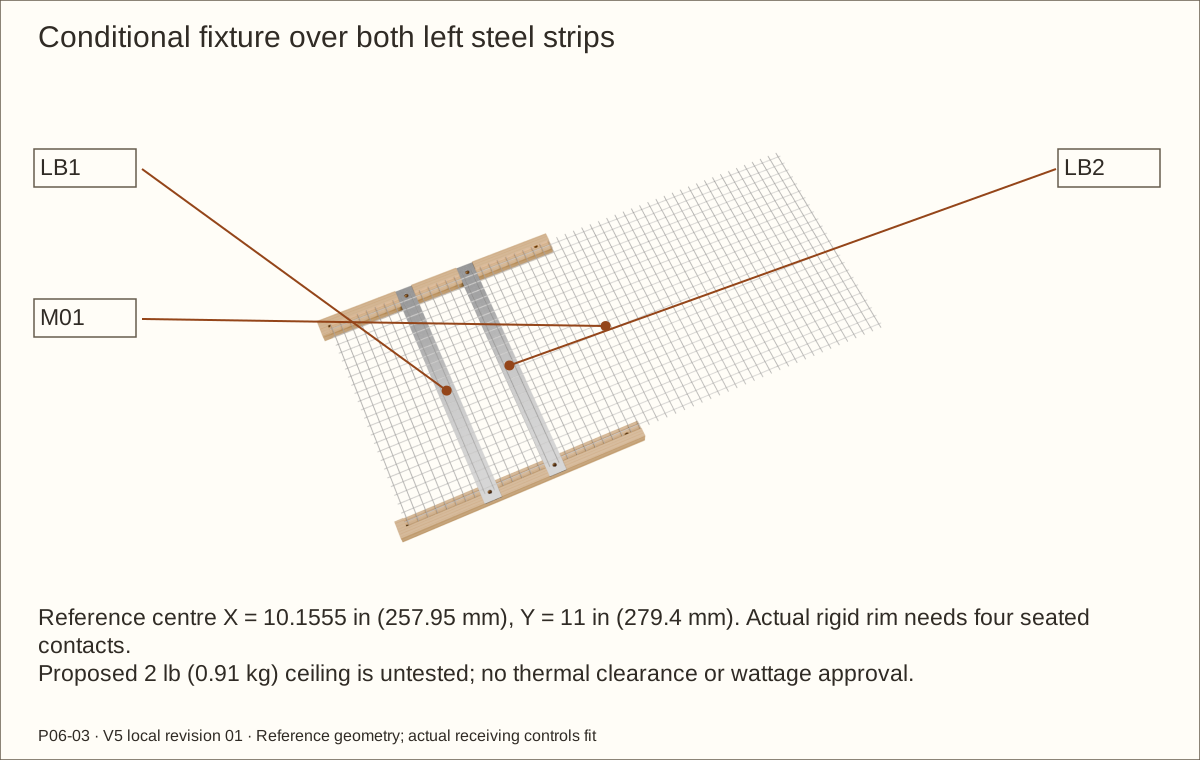
Cut two 14 in (355.6 mm) × 1 in (25.4 mm) × 1/8 in (3.18 mm) solid steel strips from the named bar. Deburr faces and ends; transfer two 1/4 in (6.35 mm) holes 1/2 in (12.7 mm) from each end, 13 in (330.2 mm) apart.
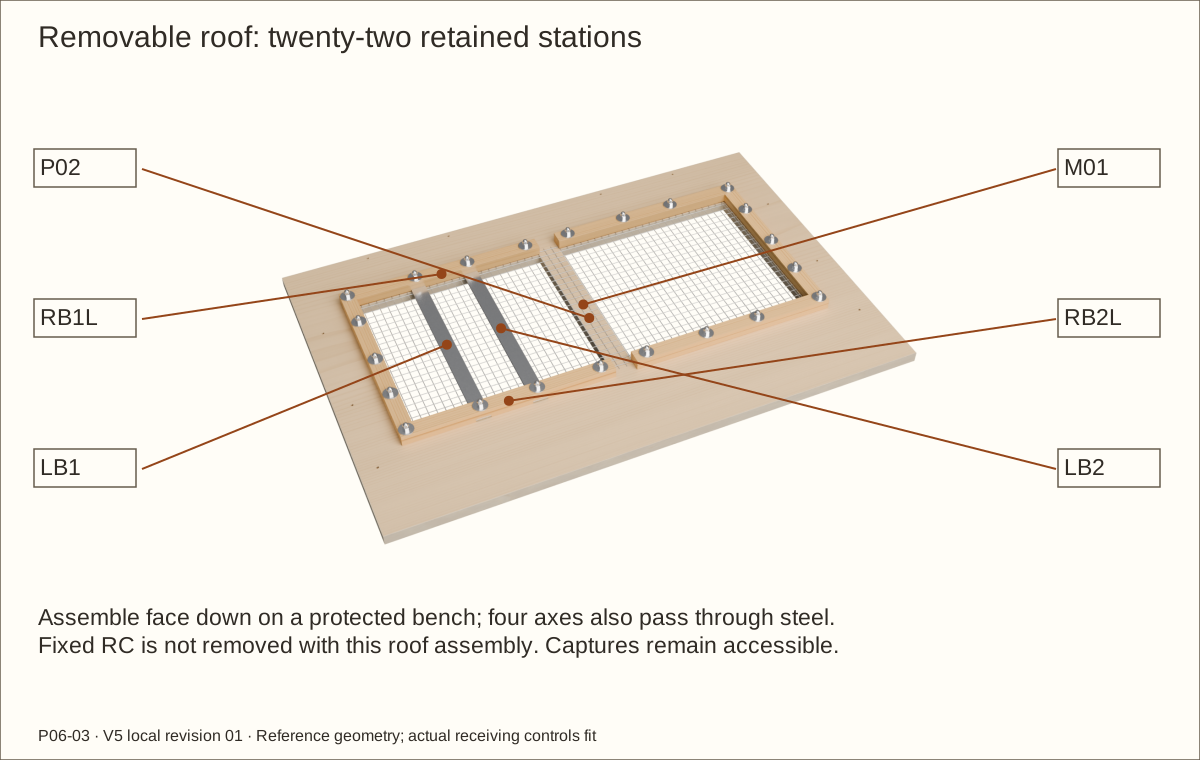
The revised strip centre axes are X = 8.262 in (209.85 mm) and 12.049 in (306.04 mm). Transfer those positions together to the matching left battens and roof stations.
Mill the received steel end seats to maintain its reference top elevation. Revised reference pockets are 0.209 in (5.31 mm) deep, leaving 0.541 in (13.74 mm) wood beneath; this remaining section needs physical/qualified acceptance.
Check before continuing: Both strips seat fully without rocking and the four bolt paths align.
Parts: P02 · Roof; P03 · Left side; P04 · Right side; M01 · Roof mesh blank; ML · L vent mesh; MR · R vent mesh
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Transfer the flush screen fixing stations
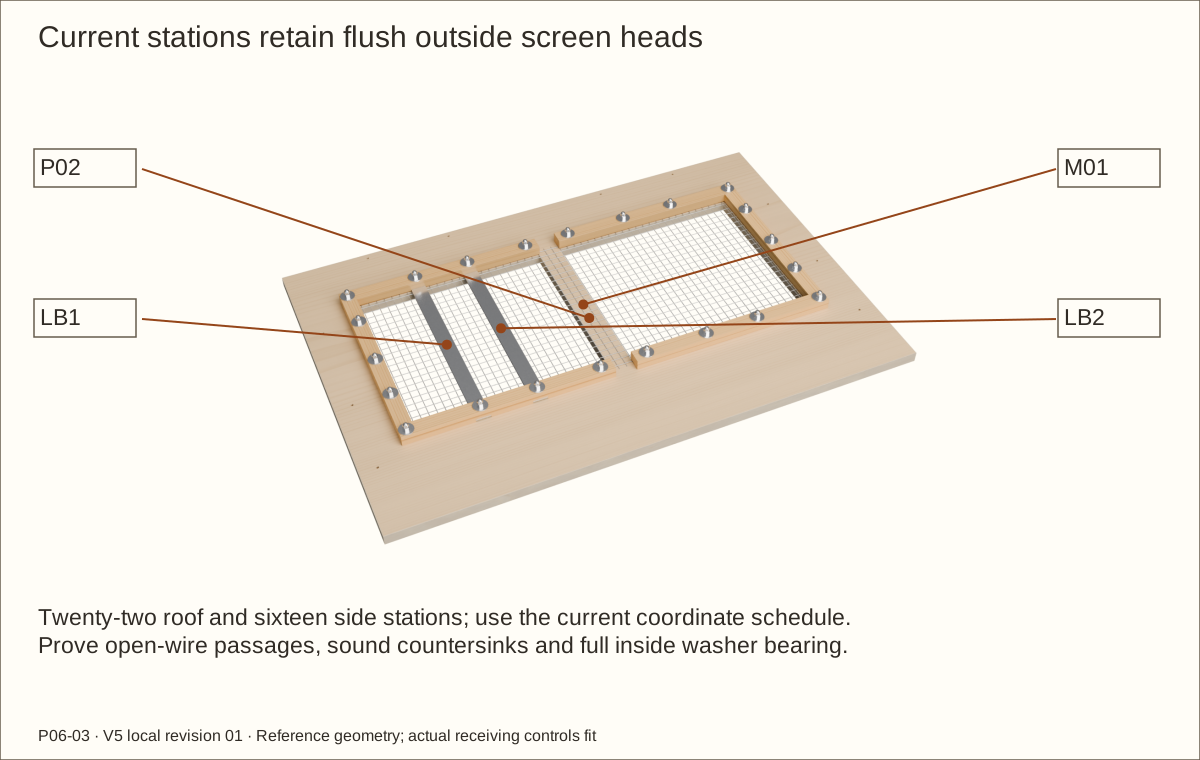
Clamp each real capture stack and transfer the current station coordinates: twenty-two roof and eight per side. Original IDs are labels; use their current X/Y/Z values.
Prove every 1/4 in (6.35 mm) passage clears an open wire cell and every inside 1 in (25.4 mm) washer seats completely on wood. The roof steel positions move with the revised axes.
Drill with backing, then trial 82-degree flat seats from outside in sound plywood. Leave a veneer service opening around each head; the head must bear in wood, not soft veneer.
Check before continuing: All thirty-eight passages, outside seats and inside bearing areas agree.
Parts: Accepted material samples and the named workshop setup
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: A cover is not a substitute for the locknut. No torque or clamp-load value is assumed.
Fit retained bolts and closed inside covers
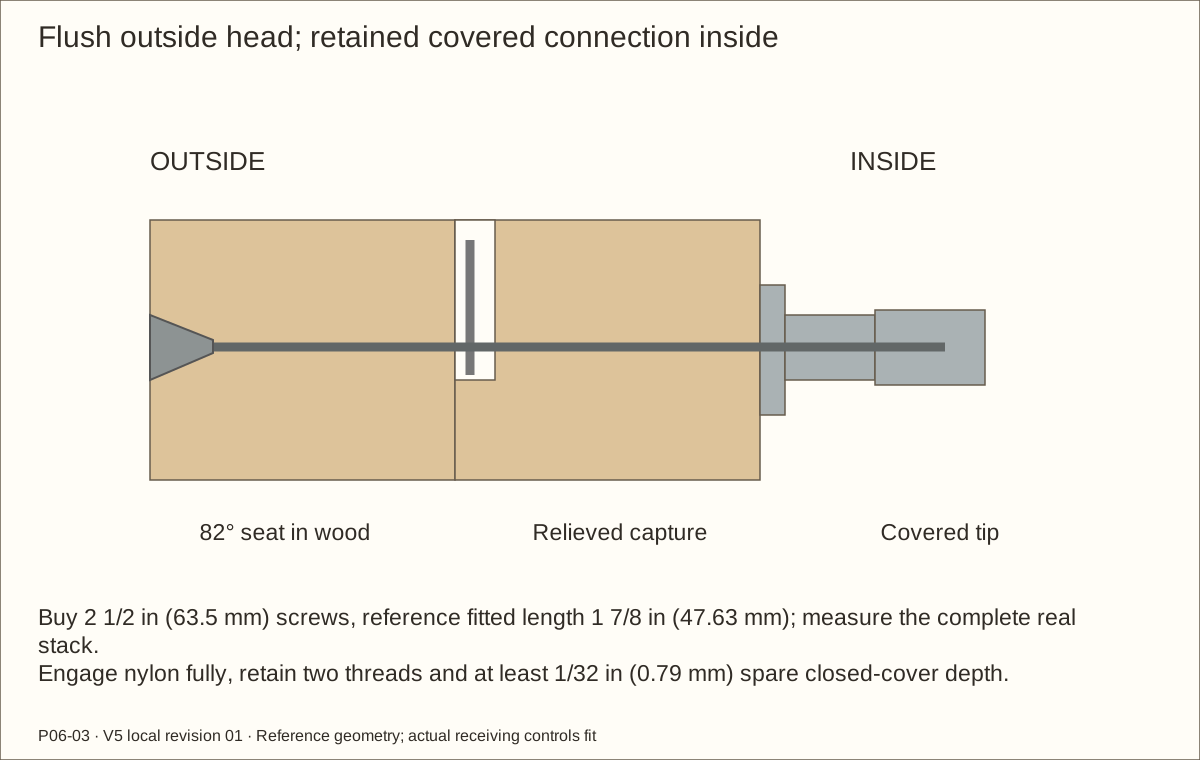
Buy #10-24 × 2 1/2 in (63.5 mm) flat-head screws. Reference fitted length is 1 7/8 in (47.63 mm) for the 1.453 in (36.91 mm) wood grip, inside washer, nylon locknut and closed cover.
Measure actual washer, locknut and cap depth before cutting. Fully engage nylon, leave at least two complete threads beyond it, and keep at least 1/32 in (0.79 mm) unused blind depth in the seated cover.
Trial on an offcut. Hold securely for trimming, deburr and clean threads; retain the locknut while seating the cover. Use two fitting hand tools and verify access.
Check before continuing: The cover seats without bottoming and no thread remains exposed.
Parts: P03 · Left side; ML · L vent mesh; VLB · L vent capture B; VLT · L vent capture T; VLF · L vent capture F; VLR · L vent capture R
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Assemble the two side captures
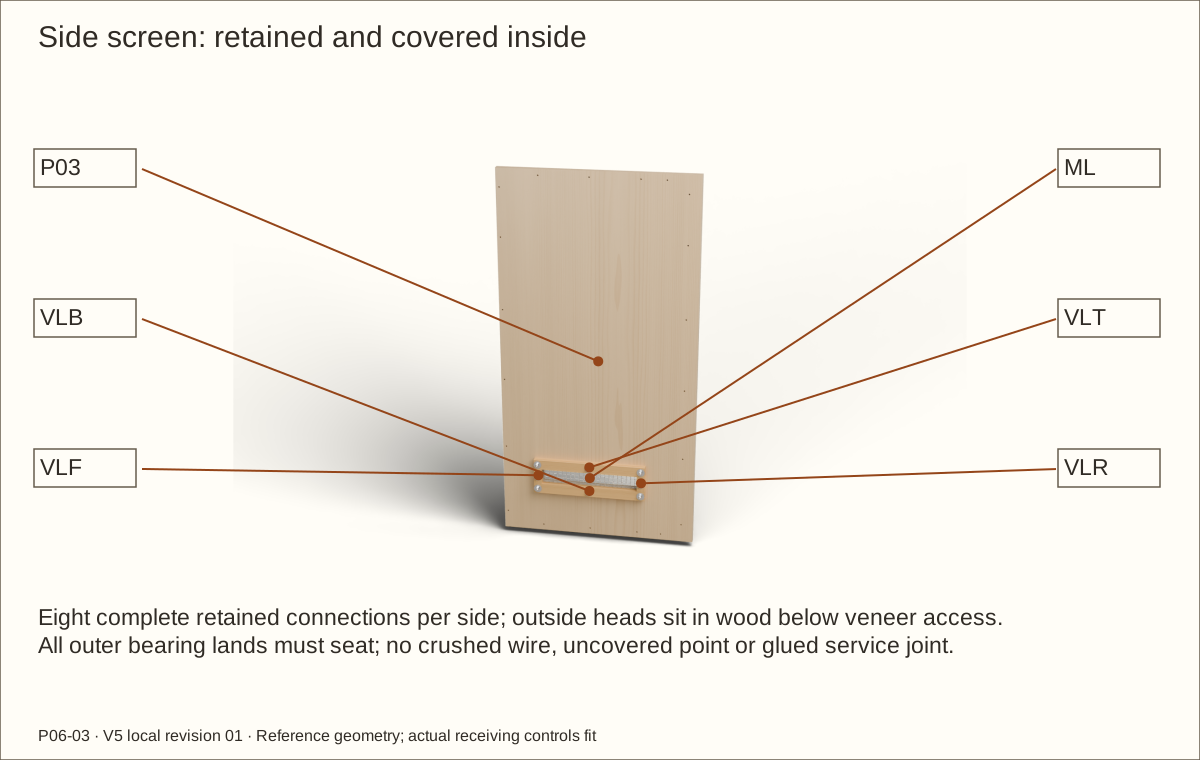
Lay each side exterior down on protection. Seat the mesh in its relief and fit all four inside battens with intact wood lands against the panel.
Insert the eight flush outside screws and install inside washers, nylon locknuts and fitted closed covers. Keep the actual wire uncut at each screw axis.
Check no sharp edge, wire distortion, loose screen or exposed tail. Keep the side service path accessible; do not glue the removable captures.
Check before continuing: Each side screen is retained and can be serviced with the agreed tools.
Parts: P03 · Left side; P04 · Right side; CLB · L side B cleat; CLT · L side T cleat; CRB · R side B cleat; CRT · R side T cleat; CLV · Rear corner cleat; CRV · Rear corner cleat
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Fit the side and rear cleats
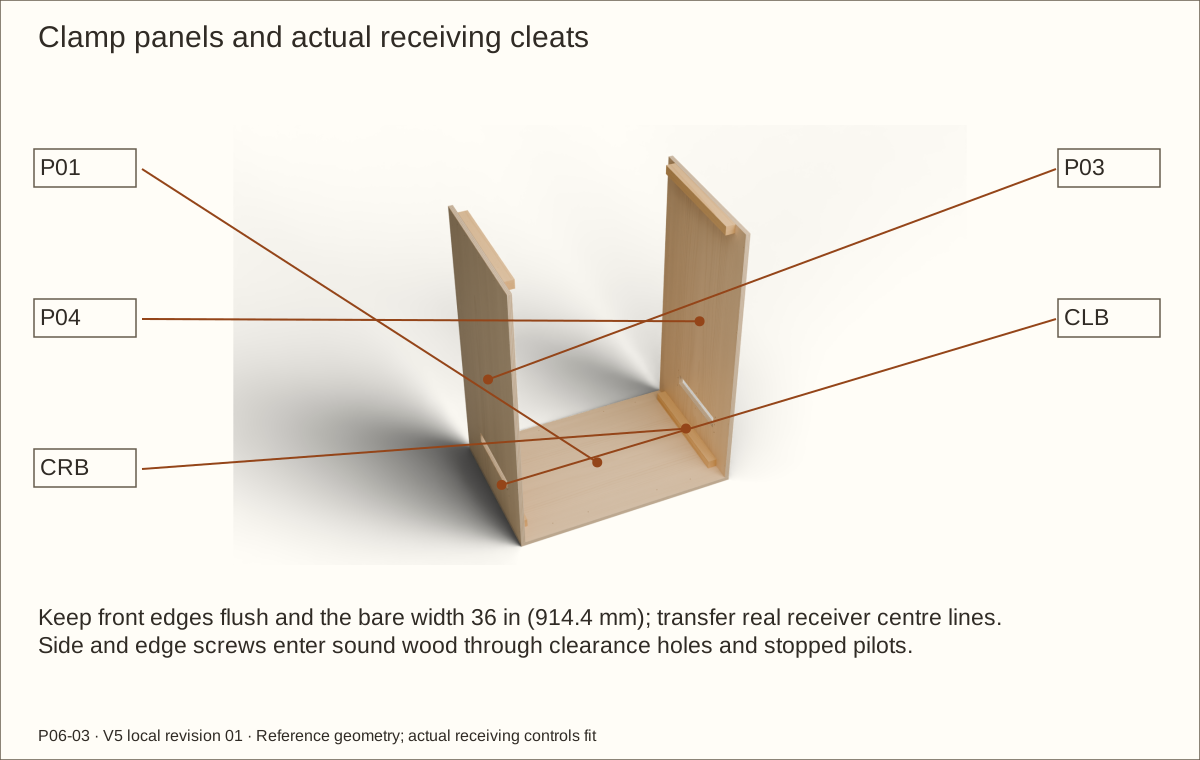
Align side floor and top cleat edges with the actual panel edges and locate rear corner cleats from their specified datums. Clamp the empty panels securely.
Use current SIDE/EDGE station coordinates and the indicated #8 × 1 3/4 in (44.45 mm) screws. Clear first members and stop the pilot in the actual solid receiver.
Keep the front/rear receptor rows at their measured levels. Do not pull a bowed panel flat with screw force or lose the 36 in (914.4 mm) bare width.
Check before continuing: Cleats are square, correctly placed and have buried screw points.
Parts: P05 · Back; CBB · B floor cleat; RF · F roof ledger; RB · B roof ledger; CLV · Rear corner cleat; CRV · Rear corner cleat
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Fit the back and horizontal ledgers
Fit P05 between the sides with its front/rear orientation correct. Install the lower rear cleat and the measured RF/RB roof ledgers from the support drawing.
Transfer actual wood receiver centres to the back screw rows and use their listed lengths. Check the rear restraint row enters RB through the correct stack.
Keep the RF relief and front column bearings oriented as drawn. Check that the case remains square on the supported bench.
Check before continuing: The back, cleats and ledgers agree with actual mating parts.
Parts: P01 · Floor; CFB · F floor cleat; CBB · B floor cleat; CLB · L side B cleat; CRB · R side B cleat
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Do not turn a glazed or loaded enclosure for this work.
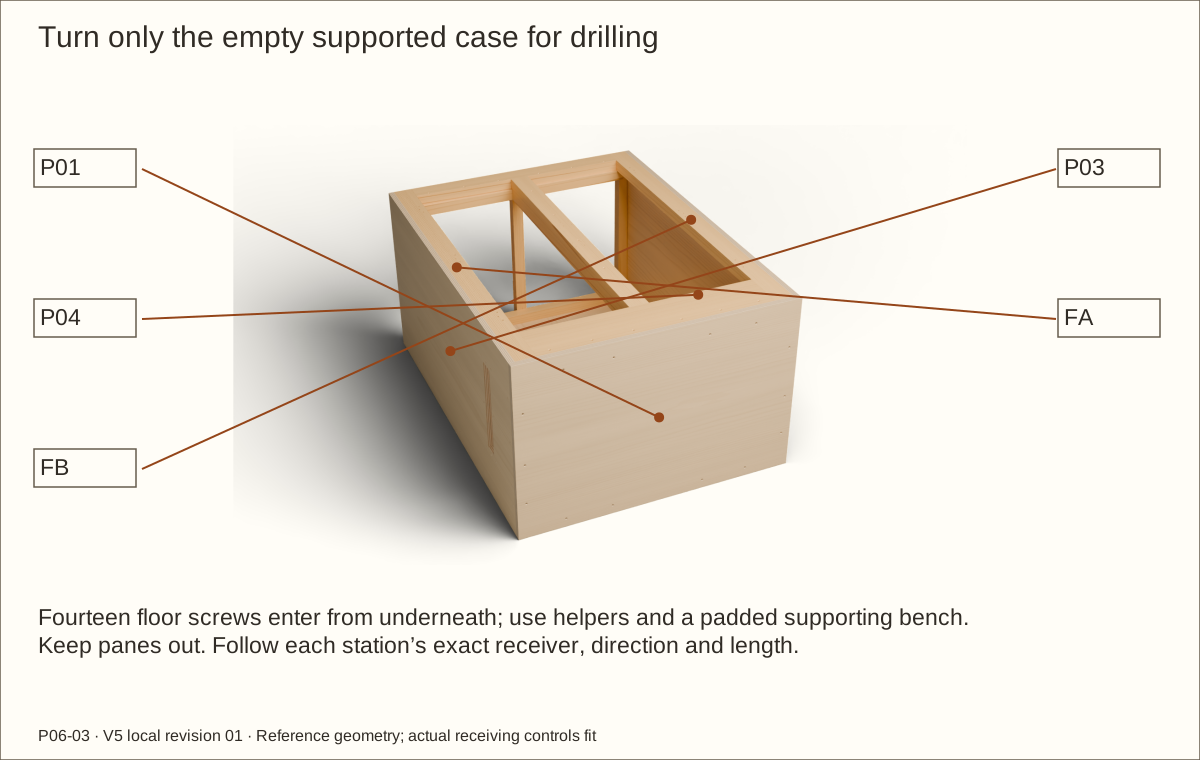
Attach the fully supported floor
Fit front floor cleat CFB between the side cleats. Clamp the floor to continuous support with the case square.
With helpers, turn the empty assembly onto padding for safe perpendicular drilling. Install fourteen #8 × 1 3/4 in (44.45 mm) floor screws from underneath at FLOOR stations.
Check each actual receiver, stopped pilot and buried tip before returning the empty case upright. The finished enclosure needs full-footprint support.
Check before continuing: The floor is square and every listed connection lands in sound receiving wood.
Parts: FA · Front outer stile; FB · Front outer stile; FC · Front sill rail; FD · Front head rail; FE · Front centre stile; CCa · Front bearing column layer A; CCb · Front bearing column layer B; CFB · F floor cleat; RF · F roof ledger
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
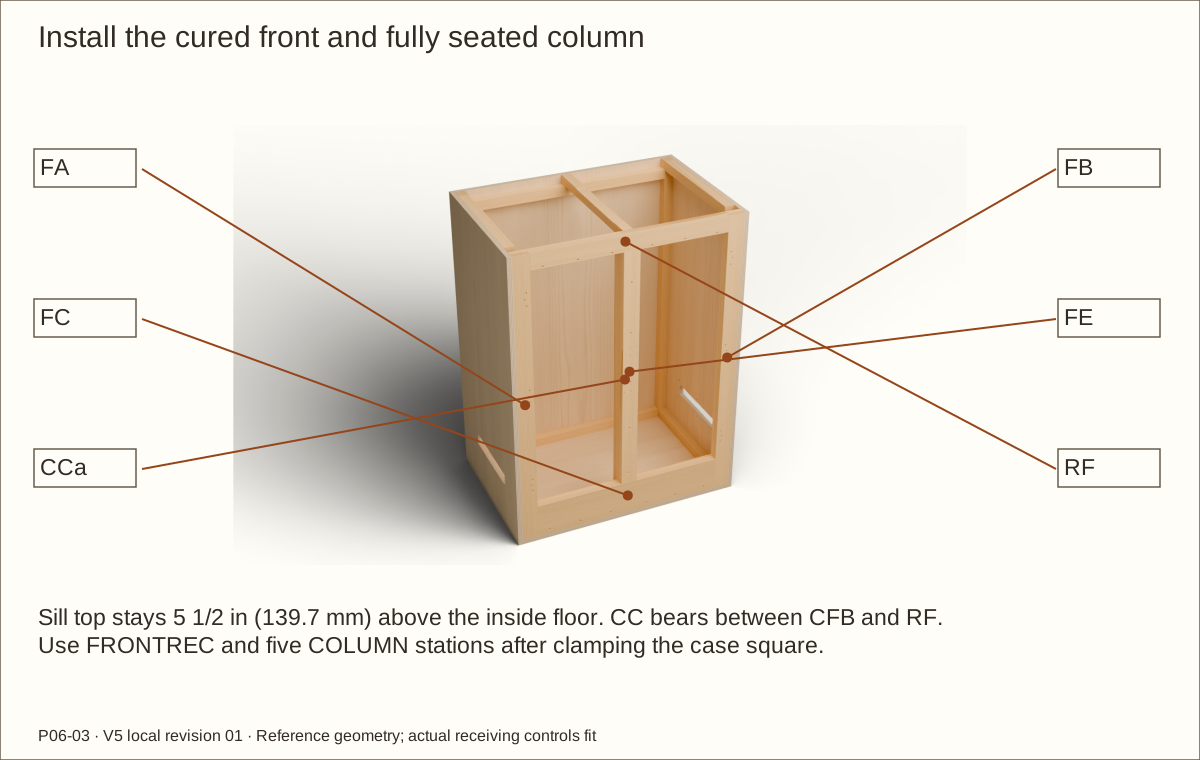
Install the cured front and bearing column
Fit the cured front flush with the side fronts and floor. The sill top remains 5 1/2 in (139.7 mm) above the inside floor.
Seat the laminated CC column fully on CFB and beneath RF. Reference column length 42.26 in (1073.4 mm) is fitted to the actual bearing gap; never hide a short bearing with screws.
Use the FRONTREC and five COLUMN #8 × 2 1/2 in (63.5 mm) stations. Clamp square and verify both openings and diagonals before drilling.
Check before continuing: The front is square and the column has full end contact.
Parts: RC · Roof centre rib; RF · F roof ledger; RB · B roof ledger; CCa · Front bearing column layer A
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Do not support a heat fixture on this central wood rib.
Fit the fixed central roof rib
Seat RC across RF and RB at the case centre. Its reference top reaches the roof underside on solid lands outside the mesh; the middle relief clears the cloth.
Install the two RIBBEAR #8 × 2 1/2 in (63.5 mm) screws downward at X = 18.3 in (464.82 mm), Y = 2 in (50.8 mm) and 22.797 in (579.04 mm). Those paths remain outside the mesh blank.
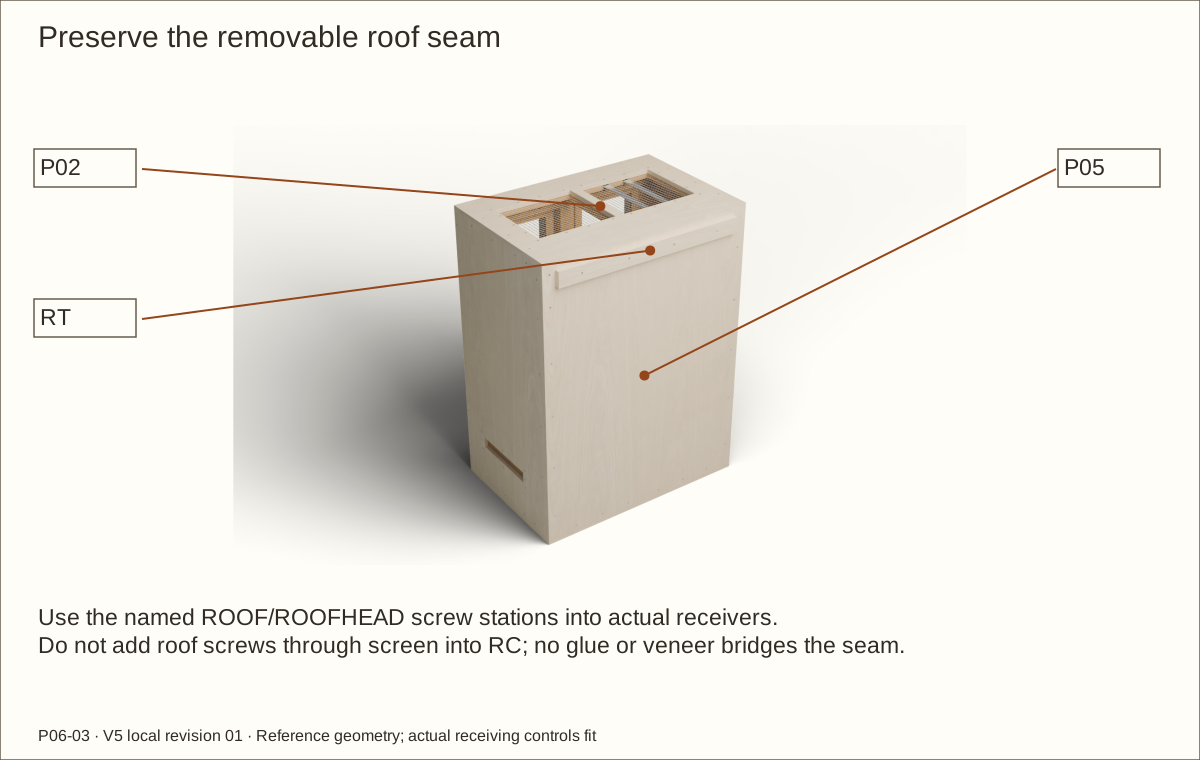
Recheck end contact, relief clearance and covered screw tips. RC stays with the case when the roof panel is removed.
Check before continuing: The rib is fixed to its ledgers and supports the intended roof bearings.
Parts: P02 · Roof; M01 · Roof mesh blank; RB1L · Roof capture batten; RB2L · Roof capture batten; LB1 · Steel strip below the left lamp area; LB2 · Steel strip below the left lamp area
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Assemble the removable roof capture
Support P02 face down on protection. Seat the single mesh blank, the two left steel strips and all six marked capture battens.
Fit twenty-two flush outside screws with inside washers, nylon locknuts and closed covers. Four stations also pass through the steel end bores.
Check every wood land seats, steel ends bear fully, caps have spare internal depth and the centre split clears fixed RC. Keep all service fixings accessible.
Check before continuing: The roof assembly has no loose screen, crushed wires, rocking strips or exposed threads.
Parts: SP-H11-fixed · Rigid full-leaf bearing pad H11 fixed; SP-H11-moving · Rigid full-leaf bearing pad H11 moving; H11_fixed · 1798A21 fixed leaf with knuckles; H11_moving · 1798A21 moving leaf with knuckles
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Make and fit the twelve hinge pads
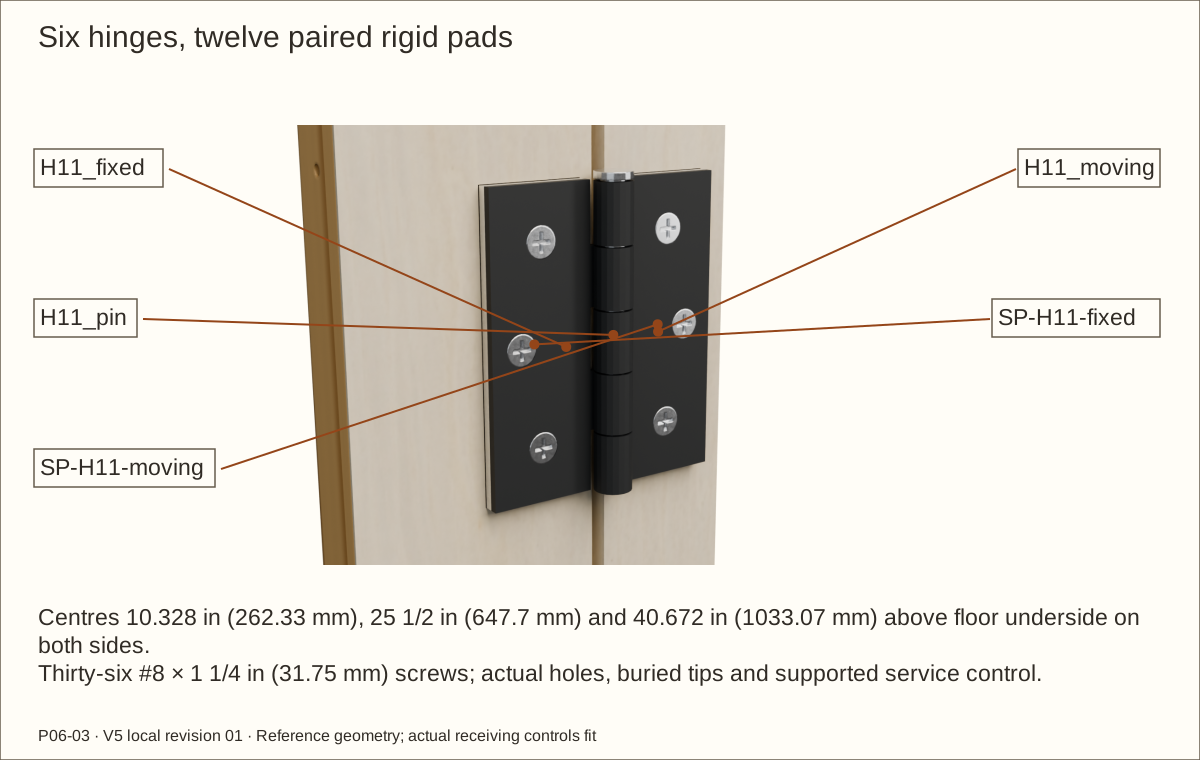
Cut twelve full-leaf 3 in (76.2 mm) × 1 1/16 in (26.99 mm) rigid aluminium pads from the allocated bars; two more pad blanks are reserved for trials. Deburr all edges.
Transfer each received leaf’s holes onto its matching pad. Maintain at least 7/64 in (2.78 mm) thickness and full bare-wood bearing under both fixed and moving leaves.
Mark pads and leaves as pairs. Do not hide an uneven seat with adhesive or veneer; receive qualified/supplier acceptance of the custom support and engagement.
Check before continuing: All six hinge pairs seat evenly with matching supported pads.
Parts: H11_fixed · 1798A21 fixed leaf with knuckles; H12_fixed · 1798A21 fixed leaf with knuckles; H13_fixed · 1798A21 fixed leaf with knuckles; D1A · Door 1 A
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Support door weight before withdrawing any pin; never rely on the last loose hinge.
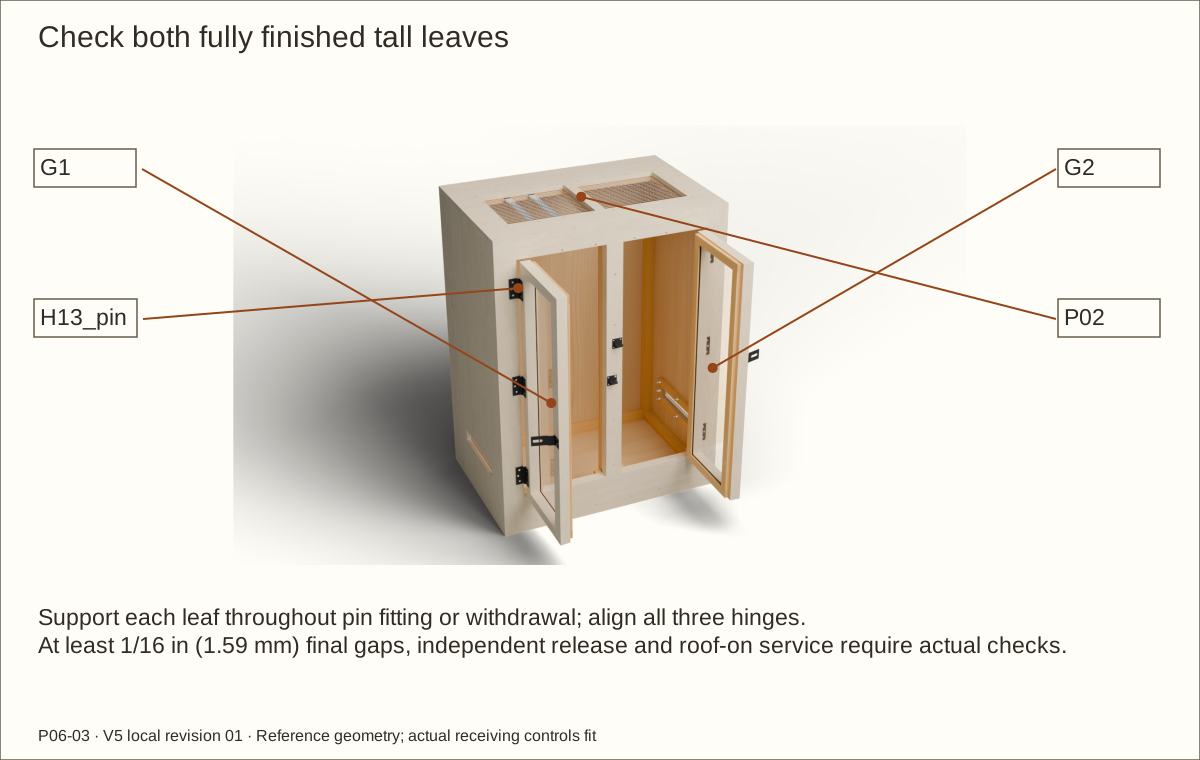
Hang the two supported tall doors
With a helper supporting each leaf, hold its finished bare gap spacers in the square opening. Align all three hinges on one straight axis.
Retain hinge centres at 10.328 in (262.33 mm), 25 1/2 in (647.7 mm) and 40.672 in (1033.07 mm) above floor underside. Use thirty-six #8 × 1 1/4 in (31.75 mm) hinge screws through the accepted heads, pads and stopped pilots.
Trial independent outward swing and supported pin removal with the roof fitted. Keep at least 4 in (101.6 mm) extraction clearance above the upper pin; actual pin/tool lengths govern.
Check before continuing: All hinges share an axis, tips remain buried and neither tall leaf binds.
Parts: FE · Front centre stile; L-HP-base · Hasp mounting leaf; L-ST-base · Swivel-staple mounting plate; R-HP-base · Hasp mounting leaf; R-ST-base · Swivel-staple mounting plate
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Transfer and fit the independent hasps
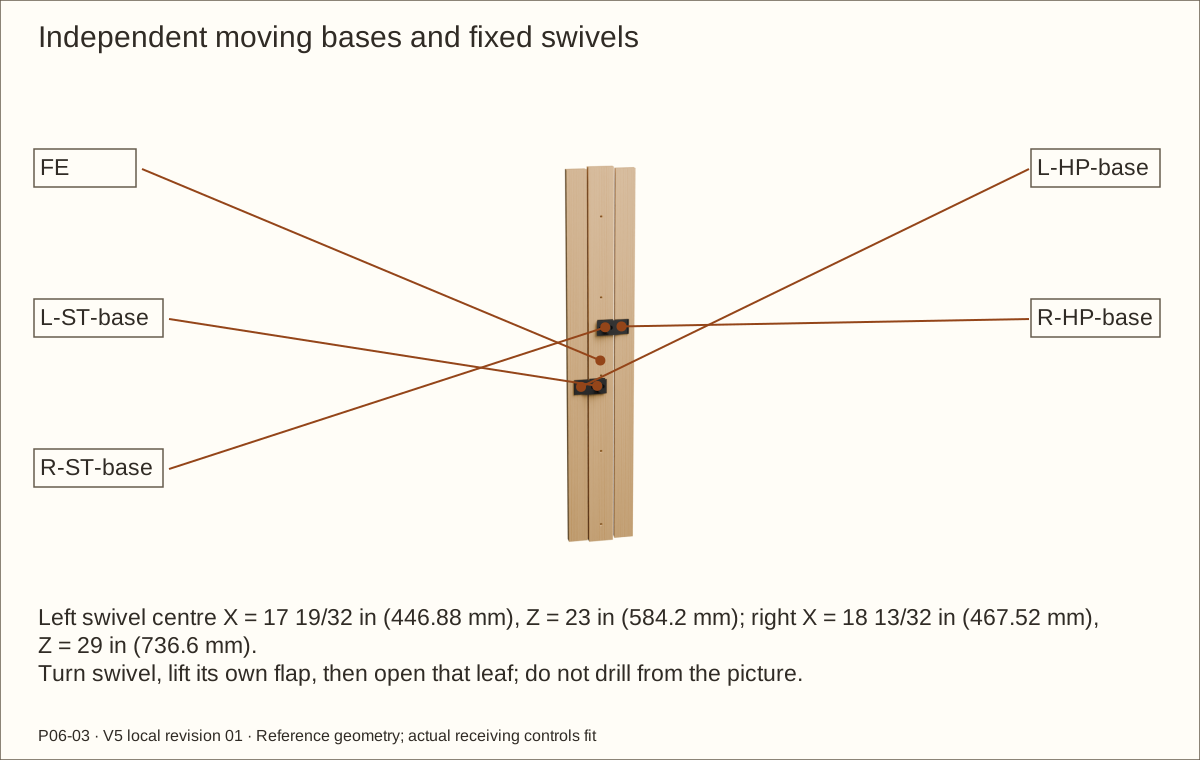
Put the narrow hinged bases on the moving latch stiles and square swivel plates on fixed FE. Left swivel centre: X = 17 19/32 in (446.88 mm), Z = 23 in (584.2 mm); right: X = 18 13/32 in (467.52 mm), Z = 29 in (736.6 mm).
Transfer the received seven-hole arrangement for each hasp, with full plate bearing and sound margins. Install fourteen #10 × 5/8 in (15.88 mm) screws at the accepted reference stations.
Turn one swivel to align with its slot, lift that flap fully outward, then open its own leaf while the other stays latched. Repeat the opposite side; no key is needed for everyday operation.
Check before continuing: Both closures secure and release independently without forcing the frame.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Fit the external restraint receiver
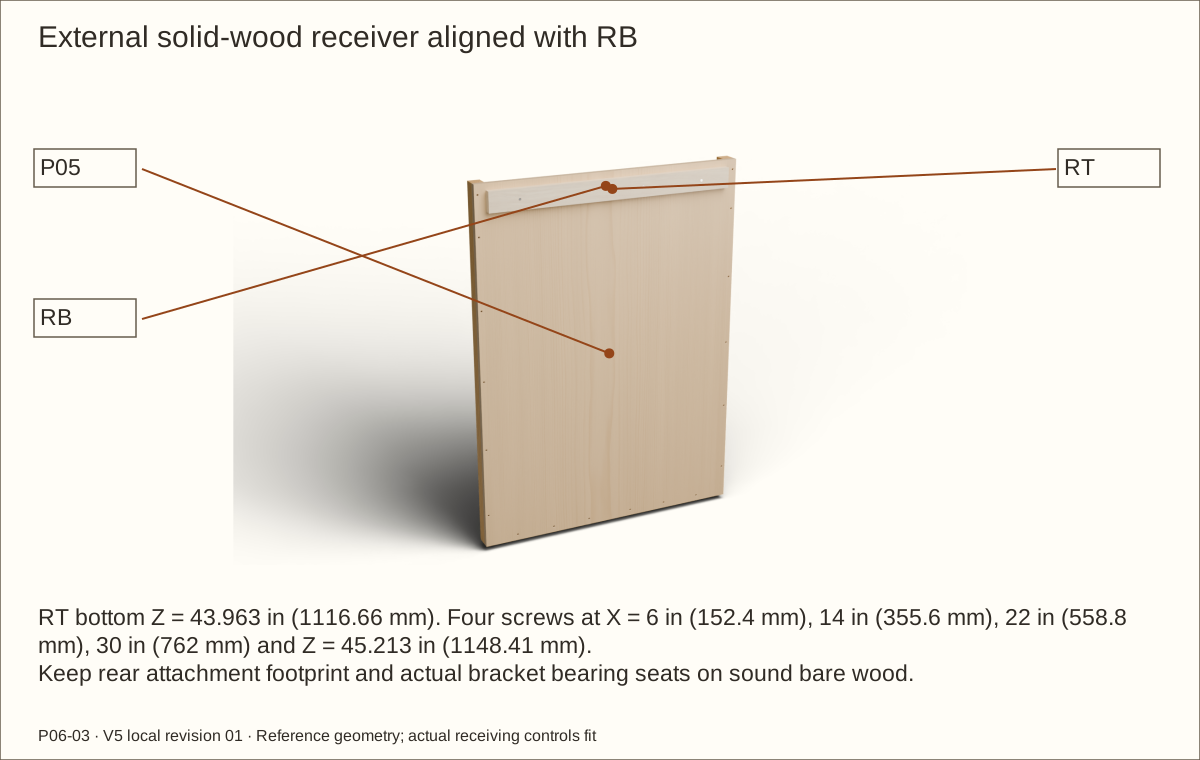
RT is an external 31.594 in (802.49 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm) pine receiver. Position its bottom at Z = 43.963 in (1116.66 mm), with the horizontal ends aligned to the rear ledger span.
Use four RESTRAINTREC #8 × 2 1/2 in (63.5 mm) screws at X = 6 in (152.4 mm), 14 in (355.6 mm), 22 in (558.8 mm) and 30 in (762 mm), Z = 45.213 in (1148.41 mm). They pass through RT and P05 into RB; transfer the actual receiver centre before drilling.
Keep RT’s attachment footprint bare against the back. Trial the real restraint brackets on an offcut before final receiver drilling; their final bare bearing seats depend on the received kit.
Check before continuing: RT bears fully and all four screws enter sound RB with covered tips.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: No kit catalogue rating is transferred to this unbuilt shell. Unknown walls remain a hold.
Rehearse the two external restraint kits
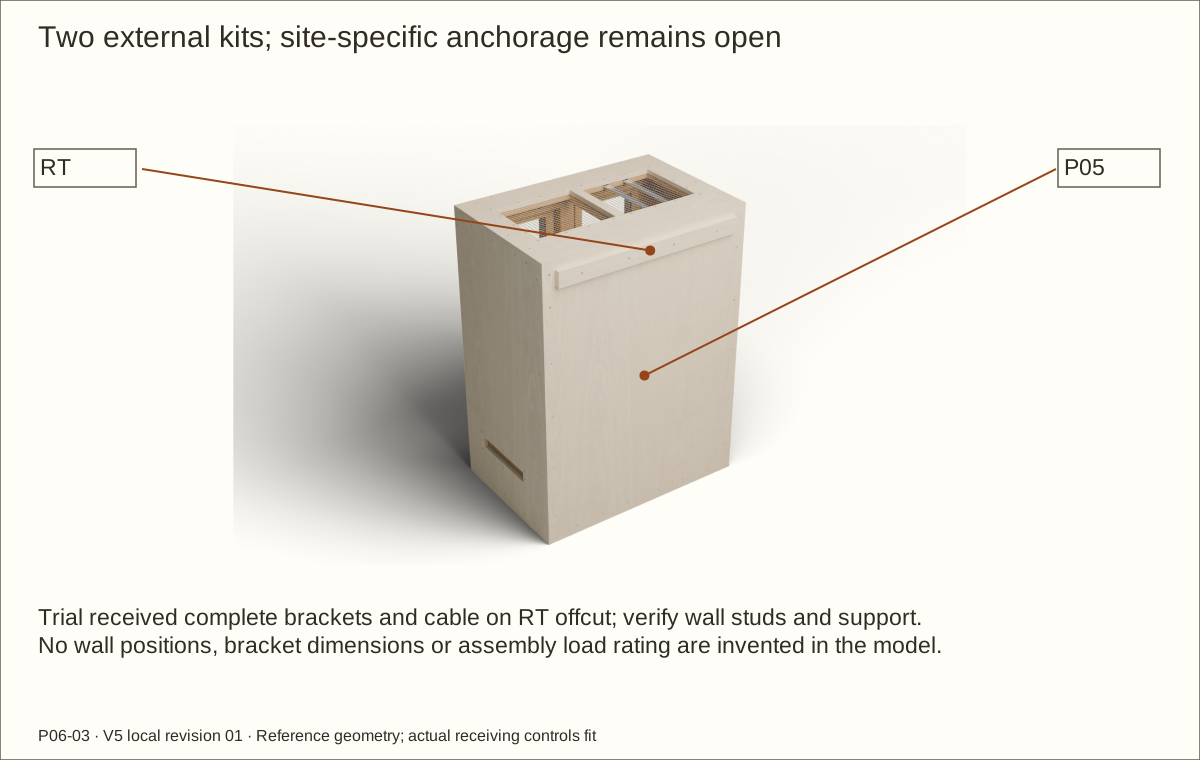
Receive two complete Hillman 9976524 kits. Identify their furniture brackets, wall brackets, cable, clevis pins, cotter pins and the specified screws.
Use the manufacturer’s actual stud-wall method with a verified wall/support. Trial furniture bracket placement and 5/8 in (15.88 mm) screws on matching RT stock, preserving a safe back cover.
Record the site-specific bracket positions, wall/stud assessment and access for later release. Keep every bracket and cable outside the containment shell; revise the plan for a different wall construction.
Check before continuing: A complete accepted anchorage plan exists before the tall enclosure enters service.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Check the complete uncoated dry assembly
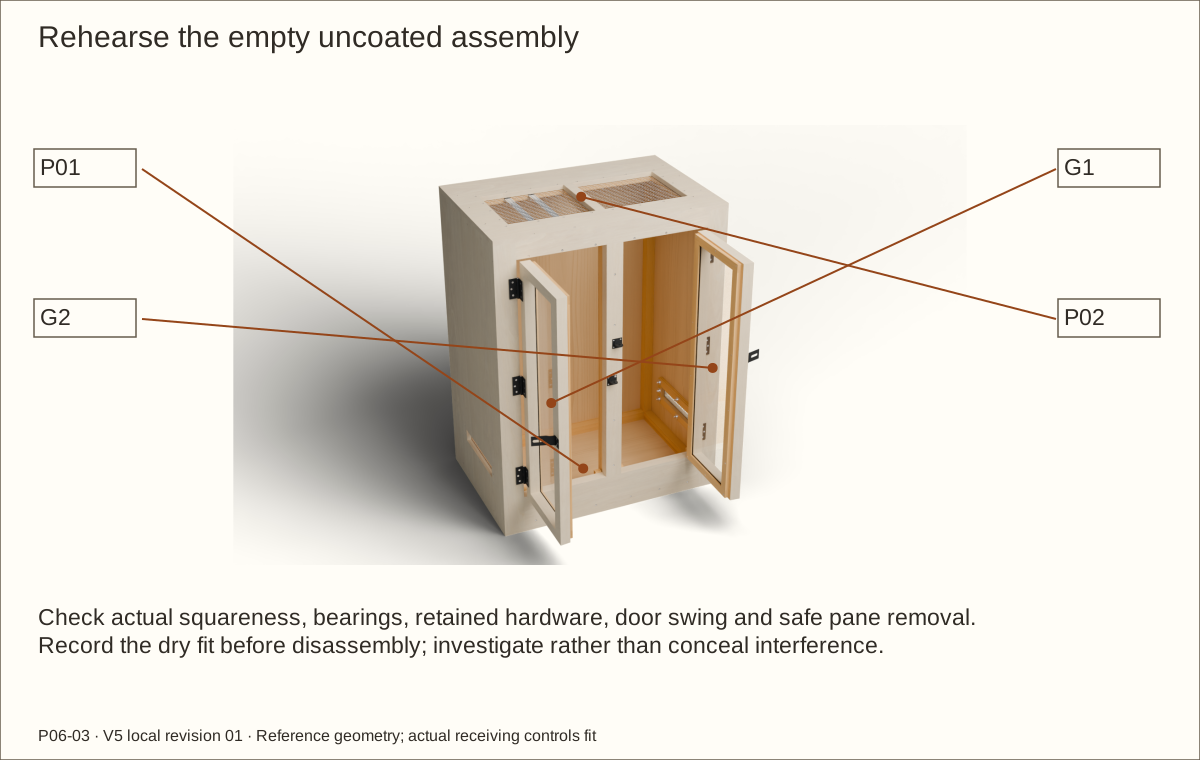
Check square, flatness, bearings, all screw receivers, captured mesh edges and retained tails. Record actual diagonal differences and investigate anything beyond the planned 1/16 in (1.59 mm) comparison target.
Trial both doors, their independent hasps and supported pin extraction. Trial pane/bead and screen removal with appropriate helpers and no animals or equipment inside.
Mark any interference and revise the affected specification before finishing. Do not hide binding, weak bearing or uncertain anchorage under veneer.
Check before continuing: The actual dry construction and all planned service paths are accepted.
Parts: P03 · Left side; FA · Front outer stile; D1A · Door 1 A
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Confirm cleaner and finish suitability for intended exposure; no animal-contact approval is inferred.
Prepare the wood and approved veneer surfaces
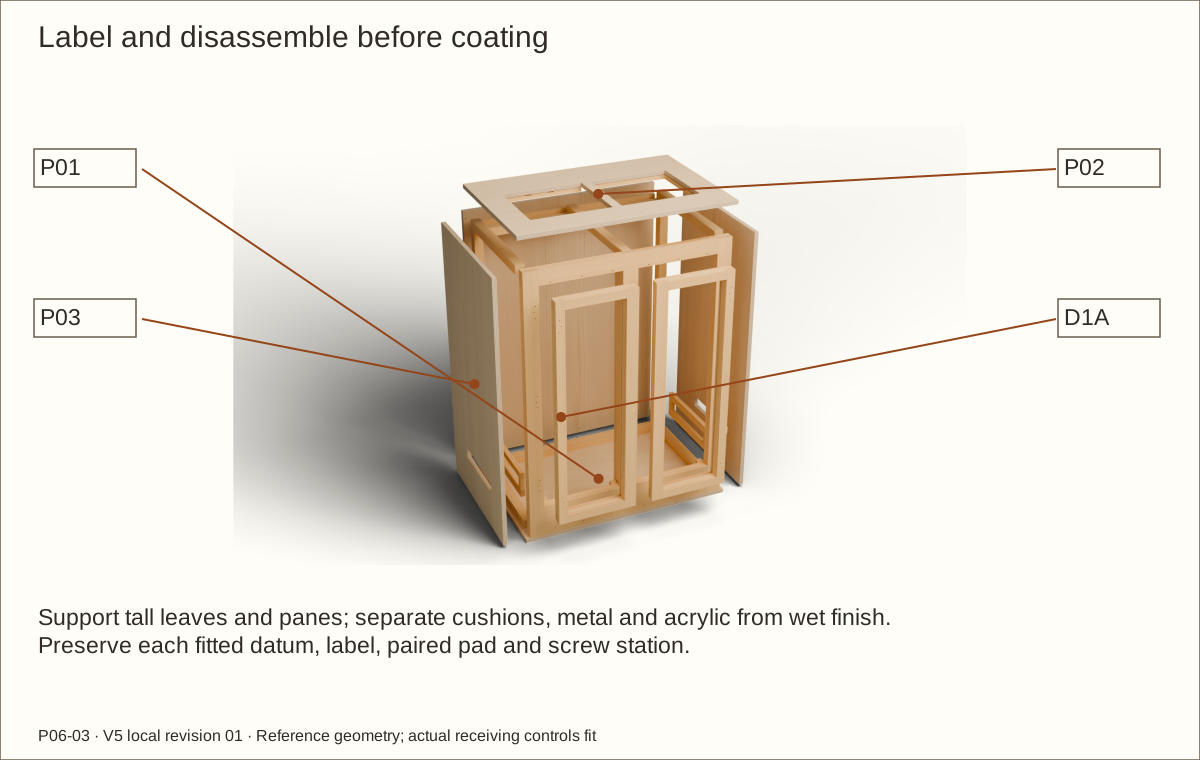
Follow the coating and veneer makers’ preparation instructions. Sand with grain on supported wood, remove dust and correct contamination before coating.
Mask bare structural glue/contact surfaces, receiver footprints and metal bearing seats. Keep service holes accessible and do not round the fitted door edges.
Prepare matching coupons along with the real parts so finish thickness, adhesion and required waits can be tracked.
Check before continuing: Surfaces are clean, compatible and ready for the confirmed system.
Parts: P03 · Left side; P02 · Roof; D1A · Door 1 A
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
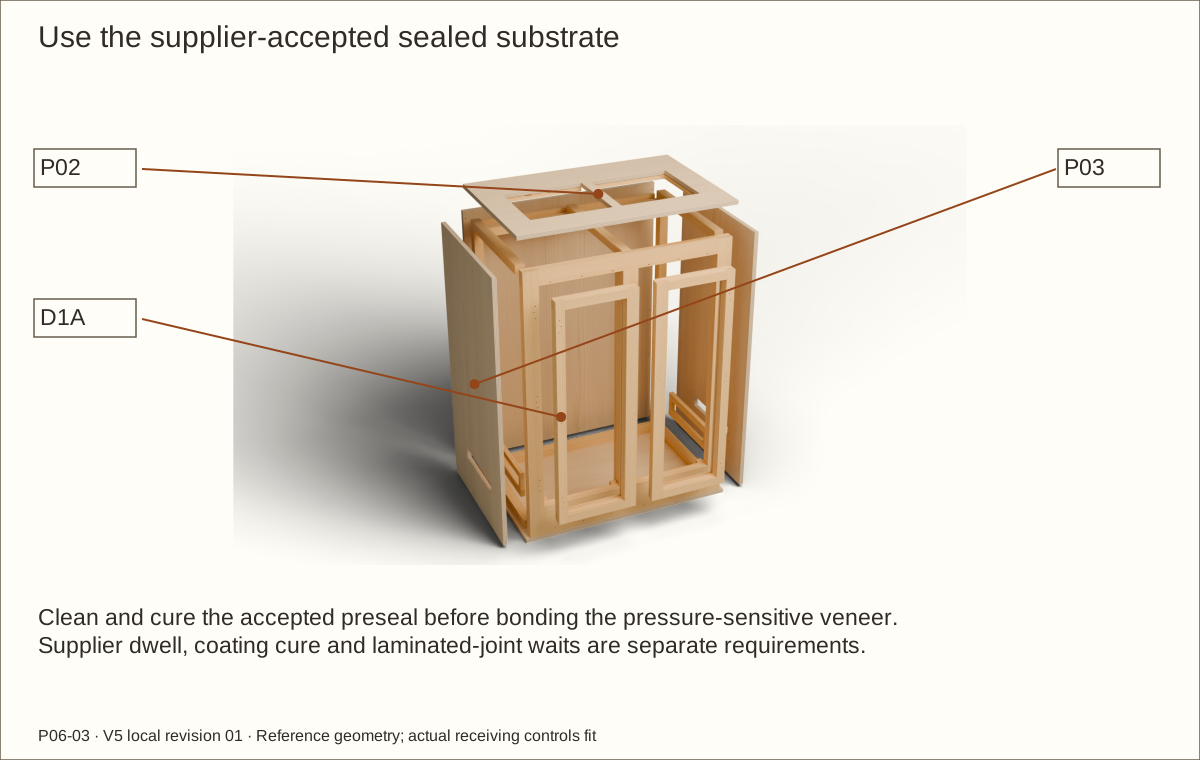
Preseal and wait for the veneer substrate
Use only the supplier-accepted preseal beneath the selected pressure-sensitive veneer. Keep the substrate smooth, sound and free of dust or silicone.
Apply and wait exactly as the veneer and coating suppliers require before bonding. The complete preseal/adhesive/backer/veneer/topcoat stack must stay within the accepted limit.
Recheck the cured trial coupon and the full-size door balance trial. Do not bond the production skins over a tacky or incompatible surface.
Check before continuing: The presealed substrate has reached the supplier-approved bonding condition.
Required wait: Use confirmed preseal cure before PSA application, separate from later topcoat cure.
Parts: P02 · Roof; P03 · Left side; P04 · Right side; P05 · Back; FA · Front outer stile; D1A · Door 1 A
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
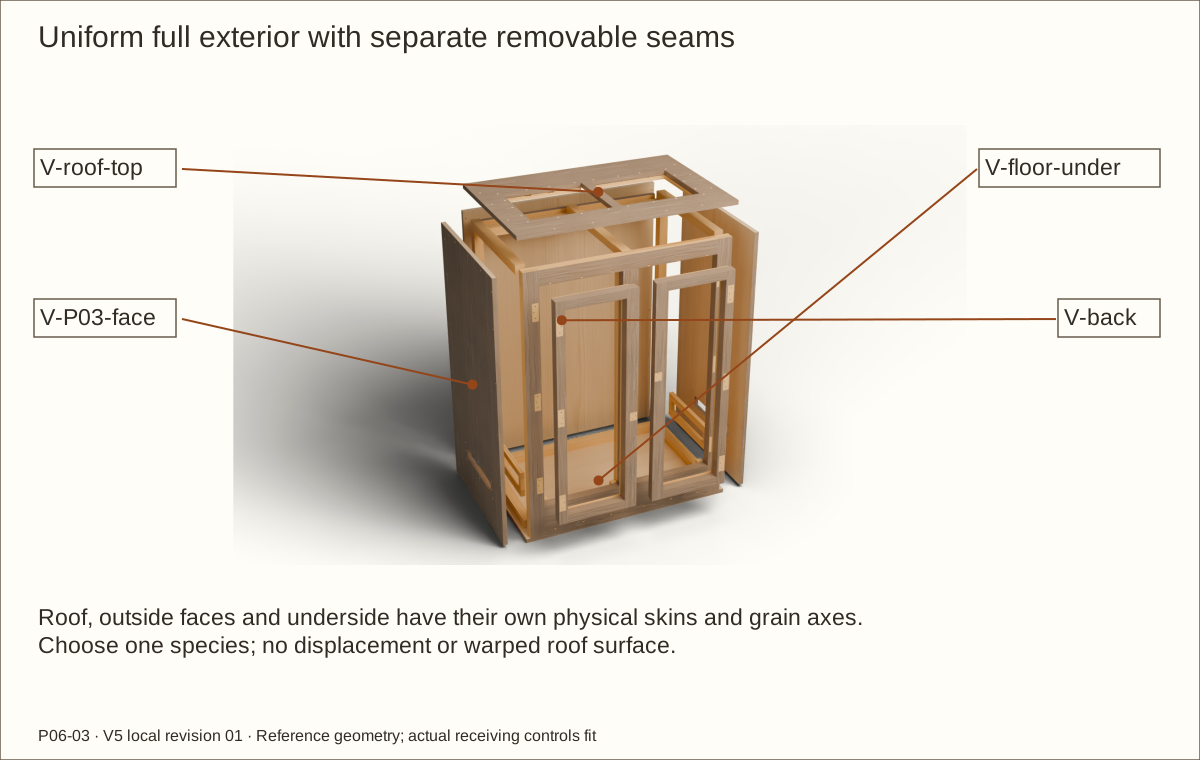
Apply the full exterior face veneer
Choose one species and use the exact V-part schedule. Align grain along each part’s assigned axis. Keep roof grain continuous on a flat plane; no raised or distorted texture is intended.
Cut the allocated oversize pieces, dry-register them and follow the veneer maker’s liner removal, pressure and scraper method without trapping air.
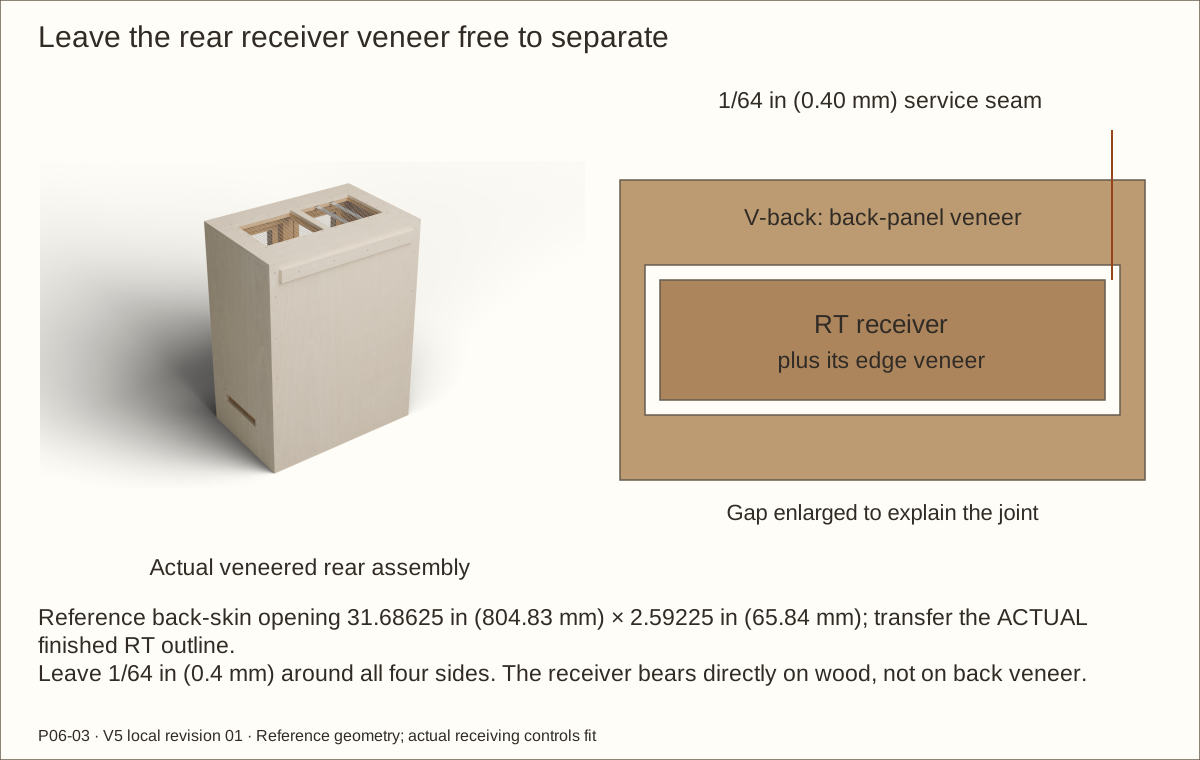
Cover roof, exterior walls, frame faces and underside. Keep separate removable seams and hardware bearing/service seats open. At RT, transfer its finished veneered outline to the back skin and leave a 1/64 in (0.4 mm) service seam all around; the reference opening is 31.68625 in (804.83 mm) × 2.59225 in (65.84 mm). Keep the receiver-to-back wood bearing bare.
Check before continuing: The faces are flat, bonded and correctly oriented without bridged service joints.
Required wait: Observe the supplier’s bonding pressure and dwell requirements; do not assume instant full strength.
Parts: P02 · Roof; P03 · Left side; RT · External rear restraint receiver; D1A · Door 1 A; D1B · Door 1 B
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Finish every exposed edge and reveal
Apply the separate edge and opening-reveal strips so plywood laminations and mixed bare edges are covered, including roof borders, door perimeters and the visible RT receiver.
Trim to actual parts with a sharp supported knife or approved trimming tool. Keep each bevel strip on its own sloping face and never bridge the roof seam or door clearance.
Leave the actual bare metal bearing pads, restraint bracket seats and fixing access openings functional. Recheck no edge lifts and the full cured layer remains at most 0.046 in (1.17 mm).
Check before continuing: Visible exterior wood is uniform; RT edge skins clear the back veneer by the planned 1/64 in (0.4 mm) service seam.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: Indoor non-immersed scope; no standing water, outdoor exposure or direct fixture hotspot approval.
Apply the accepted finish and allow full cure
Apply the selected Varathane Triple Thick satin according to current maker instructions, within 60–90°F (15.6–32.2°C) and below 85% relative humidity with suitable ventilation.
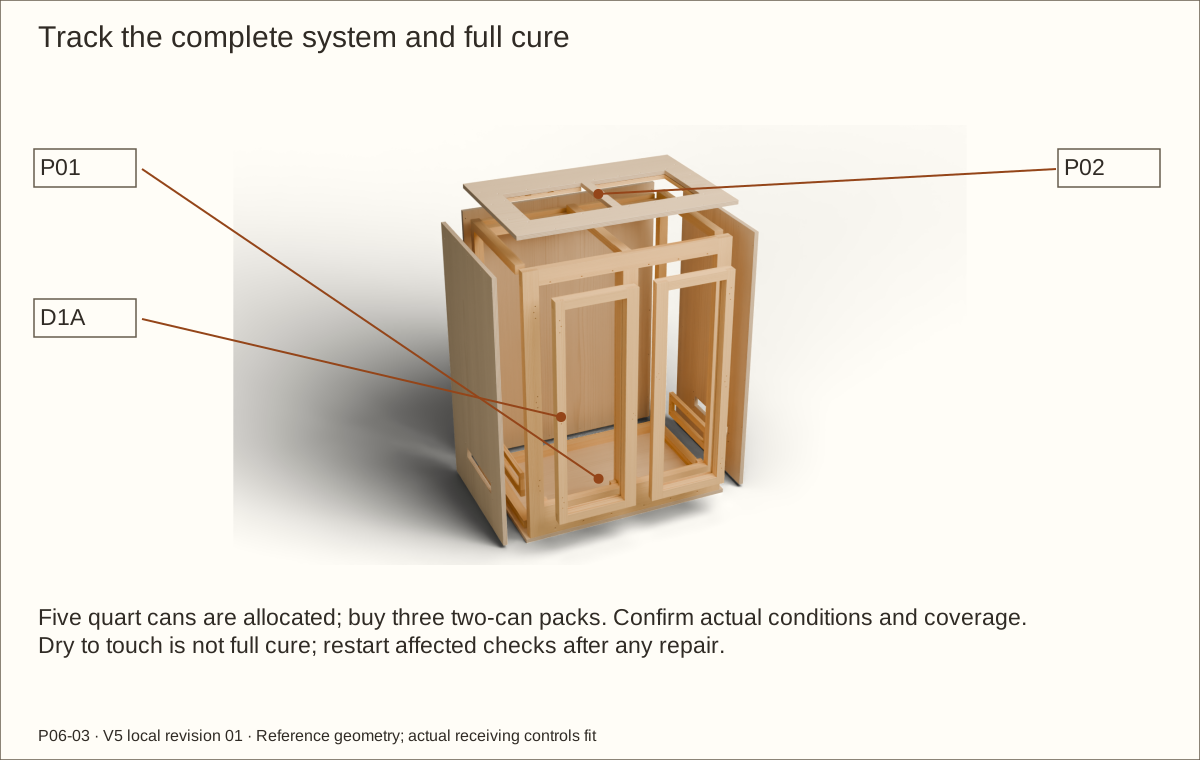
This revision allocates five quart cans including area/trial reserve; the listing sells two-can packs, so buy three packs. Recalculate for extra coats or a changed system.
Record last application/repair, temperature and humidity. Keep acrylic, neoprene, metal seats and threaded parts free of wet finish. Inspect and repair edges before the cure clock is considered complete.
Check before continuing: All surfaces and repairs are fully cured and the receiving coupon still meets fit limits.
Required wait: Maker full cure is seven days at 70°F (21.1°C) / 50% RH with ventilation; adverse conditions can require longer. Dry-to-touch is not full cure.
Parts: P01 · Floor; P02 · Roof; P03 · Left side; M01 · Roof mesh blank; ML · L vent mesh
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Reassemble the cured case and captures
Reassemble labeled parts in the accepted sequence using the existing holes. Restore every bearing contact and all fitted screen stacks.
Keep outside heads flush and inside locknuts/covers secure without crushing plywood or wires. Recheck actual cap spare depth and complete nylon engagement.
Check the roof sits on its intended solid bearings and still removes independently. No veneer or finish may bridge the removable seam.
Check before continuing: The cured shell retains its square, supported and serviceable dry-fit condition.
Parts: G1 · Door 1 OPTIX pane; N1FL · Door 1 F cushion L; N1RL · Door 1 R cushion L; N1S00 · Door 1 setting pad 0 layer 0; Q1L · Door 1 spacer L; B1L · Door 1 retaining bead L
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Fit cushions, panes and removable beads
Lay each supported door rear upward. Fit the plain front neoprene face strips and two setting-pad stacks, two 1/16 in (1.59 mm) layers at each bottom support position.
Set in the clean actual pane, retain the accepted 1/8 in (3.18 mm) perimeter allowance and add the separate rear solid strips. Fit labeled beads so they stop on their wood spacers.
Use the existing #6 stations with light, even contact. Check no bow, forced compression or rattling, and prove the supported pane can later be removed without cutting adhesive.
Check before continuing: Both cured glazing assemblies pass the recorded light-contact and expansion checks.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Refit supported doors and check final gaps
With helpers carrying each tall glazed leaf, refit the accepted hinges and pins. Support the leaf until every hinge is positively engaged according to received instructions.
Check at least 1/16 in (1.59 mm) finished gaps through the complete sweep, with the roof fitted. Test each swivel and flap independently before opening that door.
Repeat supported pin-removal and roof/pane service rehearsals after cure. Record any binding or frame change; do not shave through veneer as an unexplained repair.
Check before continuing: Both finished leaves secure, swing and remove with the accepted support and clearances.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Install and verify both site restraints
Place the empty finished enclosure on its assessed full-footprint support. Install both complete kits using the accepted site-specific bracket layout and manufacturer instructions.
Keep furniture brackets on solid RT, all components outside, and wall attachments in the assessed structural support. Insert and secure all supplied cable pins and retainers.
Have the loaded stability, attachment and maintenance release checked for this site. Record the result separately from digital validation; keep this hold open until completed.
Check before continuing: The actual support and two external restraint installations are accepted before use.
52. Commission the optional fixture and containment
Parts: LB1 · Steel strip below the left lamp area; LB2 · Steel strip below the left lamp area; M01 · Roof mesh blank
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Before you begin: The maker’s dimensional wording is ambiguous; receive and measure. Geometric wood margin is not a thermal clearance or operating wattage recommendation.
Commission the optional fixture and containment
The optional fixture is a receiving example, not a prescription. At the revised reference centre X = 10.1555 in (257.95 mm), Y = 11 in (279.4 mm), verify the actual rigid rim seats on both steel strips at all four contacts through the screen.
The proposed envelope is at most 6 in (152.4 mm) overall diameter with a 5 1/2 in (139.7 mm)–6 in (152.4 mm) rim and at most 2 lb assembled mass (0.91 kg). These are untested design limits, not confirmed product dimensions or a roof rating.
Keep the right roof heat-free. Follow actual equipment instructions, protect cords, use appropriate controls and measure temperatures/ventilation before animals. Check species-specific gaps and secure containment separately.
Check before continuing: Actual fixture fit, prototype load/thermal tests and animal-specific conditions are documented.
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Service screens, glazing and removable doors
Disconnect and cool equipment, secure occupants elsewhere and empty the enclosure before service. Keep the case supported and restrained as the accepted maintenance plan requires.
Support a tall door before withdrawing any pin; use the received sequence and helpers, keeping all weight supported. On the bench, support its pane before removing beads and loose cushions.
Remove roof and side captures through their verified paths with retained parts labeled. To reach the upper back-ledger screws, first support the empty case under the accepted site plan, release the restraint cables and remove RT. Restore both restraints before service use.
Refit the accepted stacks and repeat all affected gap, fastener, bond, load and containment checks after repair.
Check before continuing: Maintenance leaves no loose pane, exposed tail, damaged edge or unverified replacement.
Parts: Accepted material samples and the named workshop setup
Tools / setup: Tape, square, caliper, pencil and the tools named in this operation
Record each separate acceptance status
Record research, dimensions, calculations and digital validation against this exact versioned specification and model.
Record prototype construction, physical tests and qualified review only when performed, including actual measurements, equipment, date and reviewer. Leave unresolved fields open.
Keep the construction review packet and original source evidence. Record publication separately from all physical acceptance.
Check before continuing: The review packet separates research, digital validation, publication and remaining physical acceptance.
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
Plain 1/16 in (1.59 mm) solid neoprene, not self-adhesive foam. Sixteen face strips and eight setting-pad layers plus a trial coupon are explicitly nested; no assumed compression percentage or watertight seal.
Varathane 284473 clear satin, two quart cans per listed package. Quantities come from this revision’s area allowance. Observe maker application conditions and full cure; non-immersed indoor scope only, with compatibility approval still required.
Two complete 9976524 kits, with external RT attachment. Use received bracket/cable instructions and verified site studs/support. Do not transfer the catalogue kit rating to the unbuilt enclosure. Bracket seats remain bare sound wood; final layout is site-specific.
Materials and hardware · continued
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
Reference 0.703 in (17.86 mm) birch plywood; measure every sheet. Interior appearance plywood has no whole-enclosure structural or water-holding approval.
Actual 3/4 in (19.05 mm) × 5 1/2 in (139.7 mm) × 96 in (2438.4 mm) clear pine reference. Preserve solid full-width sill edges. Two extra boards are reserved for tall laminated-door and fitting trials; original historical count is superseded.
Own two tall panes; no drilled holes. Retain 1/8 in (3.18 mm) reference edge allowance after cured fitting, and actual pane + two solid neoprene light-contact layers.
Materials and hardware · continued
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
Actual 1 1/2 in (38.1 mm)-square solid pine reference for the source cleats, ledgers and newly fitted roof rib. Added trial stock is separate; no assembly load rating inferred.
HC2245 24 in (609.6 mm) × 60 in (1524 mm) roll, nominal 1/2 in (12.7 mm) mesh and 19-gauge wire. Reference grid is 0.541 in (13.74 mm) pitch with 0.041 in (1.04 mm) wire; receiving measurements control. Enlarged side blank overlap and positive relief lands are this revision’s cuts.
Six 1798A21 hinges, three per tall door. Twelve matched rigid pads move both leaves forward; actual screw engagement, full plate support, extraction and custom mounting acceptance are H02.
Materials and hardware · continued
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
Titebond III wood-lamination glue; follow maker temperature, clamp and no-stress waits. Not the veneer adhesive and not a structural or continuous-submersion approval.
Installed count plus explicit trial allowance for this build. Transfer actual root/head dimensions to stopped pilots; include drill-point length and preserve positive back cover. No load rating inferred.
Installed count plus explicit trial allowance for this build. Transfer actual root/head dimensions to stopped pilots; include drill-point length and preserve positive back cover. No load rating inferred.
Materials and hardware · continued
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
Installed count plus explicit trial allowance for this build. Transfer actual root/head dimensions to stopped pilots; include drill-point length and preserve positive back cover. No load rating inferred.
Installed count plus explicit trial allowance for this build. Transfer actual root/head dimensions to stopped pilots; include drill-point length and preserve positive back cover. No load rating inferred.
HASP · National Hardware black swivel-staple safety hasp, 3-1/4 inch Direct product listing
Two N305-979 hasps: narrow bases on moving latch stiles, swivels on fixed FE, staggered at 23 and 29 in (736.6 mm). Physical independent release, supplied shape and screw margins govern; no padlock required for ordinary opening.
Materials and hardware · continued
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
Fourteen #10 × 5/8 in (15.88 mm) screws installed, four trial allowance. Trial actual head seating in the hasp without altering manufactured holes, and keep positive wood behind tips.
Two 14 in (355.6 mm) × 1 in (25.4 mm) × 1/8 in (3.18 mm) steel strips from a 36 in (914.4 mm) bar. Current axes are 8.262 and 12.049 in (306.04 mm) from case left; 13 in (330.2 mm) hole centres. Revised 0.209 in (5.31 mm) seats leave 0.541 in (13.74 mm) wood below. This is reference geometry, not a tested load path.
Optional Fluker 27004 example only. Actual rigid rim must contact both steel strips at four points, assembled fixture mass must be measured, and roof/load/thermal testing remains open. The right roof stays heat-free; wattage ceiling is not an operating recommendation.
Materials and hardware · continued
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
Thirty-eight outside flat-head #10-24 82-degree screen screws. Buy 2 1/2 in (63.5 mm), reference fit to 1 7/8 in (47.63 mm) from the real stack. Retain full nylon engagement, two exposed threads and spare closed-cover depth.
One 1 in (25.4 mm)-OD, 1/4 in (6.35 mm)-bore washer inside each of 38 stations; no outside washer. Maintain full wood seating and inside tool access; dimensions are receiving checks.
One #10-24 nylon-insert locknut inside each station, plus two trial nuts. The closed cover does not replace the locknut. Received nut height/nylon engagement controls fitted length.
Materials and hardware · continued
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
One closed #10-24 cover per retained inside tail, plus two trial pieces. Measure blind depth, deburr and trial. It must seat without bottoming; hold the locknut while fitting.
Twelve 3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm) aluminum pads plus two trial pads. Minimum reference thickness 7/64 in (2.78 mm). Transfer actual holes; no veneer under the bearing pads. Qualified/supplier acceptance remains open.
VENEER-maple · Optional maple veneer, 48 × 96 inches, selected 3M PSA backing Direct product listing
maple-veneer-flat-cut Needed 3 + 0 trial units; 1 per package; buy 3 package(s) Choose one veneer species
One selected peel-and-stick backed wood veneer species, full exterior including roof and edges. Actual combined adhesive/backer/preseal/topcoat thickness must stay within 0.046 in (1.17 mm). Supplier balance/bond advice and full-size cured tall-door trial remain H01.
Materials and hardware · continued
Choose ONE veneer species: three 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. FINISH is a two-quart-can pack. Resolve H01–H06 before dependent work. No purchase or address-specific stock check has been made.
Product
Model and quantities
Fit / purchase condition
VENEER-oak · Optional white oak veneer, 48 × 96 inches, selected 3M PSA backing Direct product listing
oak-veneer-white-flat-cut Needed 3 + 0 trial units; 1 per package; buy 3 package(s) Choose one veneer species
One selected peel-and-stick backed wood veneer species, full exterior including roof and edges. Actual combined adhesive/backer/preseal/topcoat thickness must stay within 0.046 in (1.17 mm). Supplier balance/bond advice and full-size cured tall-door trial remain H01.
walnut-veneer-flat-cut Needed 3 + 0 trial units; 1 per package; buy 3 package(s) Choose one veneer species
One selected peel-and-stick backed wood veneer species, full exterior including roof and edges. Actual combined adhesive/backer/preseal/topcoat thickness must stay within 0.046 in (1.17 mm). Supplier balance/bond advice and full-size cured tall-door trial remain H01.
Cut list
Cut list
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
P01 · Floor
36 1/8 in (917.58 mm) × 24 1/8 in (612.78 mm) × 0.703 in (17.86 mm)
36 in (914.4 mm) × 24 in (609.6 mm) × 0.703 in (17.86 mm)
P02 · Roof
36 1/8 in (917.58 mm) × 24 1/8 in (612.78 mm) × 0.703 in (17.86 mm)
36 in (914.4 mm) × 24 in (609.6 mm) × 0.703 in (17.86 mm)
P03 · Left side
46.719 in (1186.66 mm) × 24 1/8 in (612.78 mm) × 0.703 in (17.86 mm)
46.594 in (1183.49 mm) × 24 in (609.6 mm) × 0.703 in (17.86 mm)
P04 · Right side
46.719 in (1186.66 mm) × 24 1/8 in (612.78 mm) × 0.703 in (17.86 mm)
46.594 in (1183.49 mm) × 24 in (609.6 mm) × 0.703 in (17.86 mm)
P05 · Back
46.719 in (1186.66 mm) × 34.719 in (881.86 mm) × 0.703 in (17.86 mm)
46.594 in (1183.49 mm) × 34.594 in (878.69 mm) × 0.703 in (17.86 mm)
FA · Front outer stile
46.719 in (1186.66 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
46.594 in (1183.49 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
FB · Front outer stile
46.719 in (1186.66 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
46.594 in (1183.49 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
FC · Front sill rail
29.719 in (754.86 mm) × 5 1/2 in (139.7 mm) × 3/4 in (19.05 mm)
29.594 in (751.69 mm) × 5 1/2 in (139.7 mm) × 3/4 in (19.05 mm)
FD · Front head rail
29.719 in (754.86 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
29.594 in (751.69 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
FE · Front centre stile
38.719 in (983.46 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
38.594 in (980.29 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
FF · Rear centre stile
46.719 in (1186.66 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
46.594 in (1183.49 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
FGL · Rear sill half
16.172 in (410.77 mm) × 5 1/2 in (139.7 mm) × 3/4 in (19.05 mm)
16.047 in (407.59 mm) × 5 1/2 in (139.7 mm) × 3/4 in (19.05 mm)
FHL · Rear head half
16.172 in (410.77 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
16.047 in (407.59 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
FGR · Rear sill half
16.172 in (410.77 mm) × 5 1/2 in (139.7 mm) × 3/4 in (19.05 mm)
16.047 in (407.59 mm) × 5 1/2 in (139.7 mm) × 3/4 in (19.05 mm)
FHR · Rear head half
16.172 in (410.77 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
16.047 in (407.59 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
FI · Rear outer stile
38.719 in (983.46 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
38.594 in (980.29 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
FJ · Rear outer stile
38.719 in (983.46 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
38.594 in (980.29 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
D1A · Door 1 A
38.469 in (977.11 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
38.219 in (970.76 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D1B · Door 1 B
38.469 in (977.11 mm) × 2 in (50.8 mm) × 3/4 in (19.05 mm)
38.219 in (970.76 mm) × 1 31/32 in (50.01 mm) × 3/4 in (19.05 mm)
D1C · Door 1 C
9.922 in (252.02 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
9.797 in (248.84 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
D1D · Door 1 D
9.922 in (252.02 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
9.797 in (248.84 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D1E · Door 1 E
13.422 in (340.92 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
13.20325 in (335.36 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D1F · Door 1 F
13.422 in (340.92 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
13.20325 in (335.36 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D1G · Door 1 G
35.469 in (900.91 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
35.344 in (897.74 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D1H · Door 1 H
35.469 in (900.91 mm) × 2 in (50.8 mm) × 3/4 in (19.05 mm)
35.344 in (897.74 mm) × 1 31/32 in (50.01 mm) × 3/4 in (19.05 mm)
G1 · Door 1 OPTIX pane
36.094 in (916.79 mm) × 10.547 in (267.89 mm) × 0.22 in (5.59 mm)
36.094 in (916.79 mm) × 10.547 in (267.89 mm) × 0.22 in (5.59 mm)
N1FB · Door 1 F cushion B
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N1FT · Door 1 F cushion T
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N1FL · Door 1 F cushion L
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N1FR · Door 1 F cushion R
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
N1RB · Door 1 R cushion B
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N1RT · Door 1 R cushion T
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N1RL · Door 1 R cushion L
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N1RR · Door 1 R cushion R
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N1S00 · Door 1 setting pad 0 layer 0
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
N1S01 · Door 1 setting pad 0 layer 1
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
N1S10 · Door 1 setting pad 1 layer 0
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
N1S11 · Door 1 setting pad 1 layer 1
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
Q1B · Door 1 spacer B
10.922 in (277.42 mm) × 3/4 in (19.05 mm) × 3/8 in (9.53 mm)
10.797 in (274.24 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
Q1T · Door 1 spacer T
10.922 in (277.42 mm) × 3/4 in (19.05 mm) × 3/8 in (9.53 mm)
10.797 in (274.24 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
Q1L · Door 1 spacer L
37.969 in (964.41 mm) × 3/4 in (19.05 mm) × 3/8 in (9.53 mm)
37.844 in (961.24 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
Q1R · Door 1 spacer R
37.969 in (964.41 mm) × 3/4 in (19.05 mm) × 3/8 in (9.53 mm)
37.844 in (961.24 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
B1B · Door 1 retaining bead B
12.422 in (315.52 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
12.297 in (312.34 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
B1T · Door 1 retaining bead T
12.422 in (315.52 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
12.297 in (312.34 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
B1L · Door 1 retaining bead L
35.469 in (900.91 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
35.344 in (897.74 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
B1R · Door 1 retaining bead R
35.469 in (900.91 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
35.344 in (897.74 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
D2A · Door 2 A
38.469 in (977.11 mm) × 2 in (50.8 mm) × 3/4 in (19.05 mm)
38.219 in (970.76 mm) × 1 31/32 in (50.01 mm) × 3/4 in (19.05 mm)
D2B · Door 2 B
38.469 in (977.11 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
38.219 in (970.76 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D2C · Door 2 C
9.922 in (252.02 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
9.797 in (248.84 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D2D · Door 2 D
9.922 in (252.02 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
9.797 in (248.84 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
D2E · Door 2 E
13.422 in (340.92 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
13.20325 in (335.36 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D2F · Door 2 F
13.422 in (340.92 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
13.20325 in (335.36 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
D2G · Door 2 G
35.469 in (900.91 mm) × 2 in (50.8 mm) × 3/4 in (19.05 mm)
35.344 in (897.74 mm) × 1 31/32 in (50.01 mm) × 3/4 in (19.05 mm)
D2H · Door 2 H
35.469 in (900.91 mm) × 1 1/2 in (38.1 mm) × 3/4 in (19.05 mm)
35.344 in (897.74 mm) × 1 7/16 in (36.51 mm) × 3/4 in (19.05 mm)
G2 · Door 2 OPTIX pane
36.094 in (916.79 mm) × 10.547 in (267.89 mm) × 0.22 in (5.59 mm)
36.094 in (916.79 mm) × 10.547 in (267.89 mm) × 0.22 in (5.59 mm)
N2FB · Door 2 F cushion B
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N2FT · Door 2 F cushion T
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N2FL · Door 2 F cushion L
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N2FR · Door 2 F cushion R
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N2RB · Door 2 R cushion B
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
N2RT · Door 2 R cushion T
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N2RL · Door 2 R cushion L
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N2RR · Door 2 R cushion R
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
N2S00 · Door 2 setting pad 0 layer 0
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
N2S01 · Door 2 setting pad 0 layer 1
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
N2S10 · Door 2 setting pad 1 layer 0
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
N2S11 · Door 2 setting pad 1 layer 1
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
Q2B · Door 2 spacer B
10.922 in (277.42 mm) × 3/4 in (19.05 mm) × 3/8 in (9.53 mm)
10.797 in (274.24 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
Q2T · Door 2 spacer T
10.922 in (277.42 mm) × 3/4 in (19.05 mm) × 3/8 in (9.53 mm)
10.797 in (274.24 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
Q2L · Door 2 spacer L
37.969 in (964.41 mm) × 3/4 in (19.05 mm) × 3/8 in (9.53 mm)
37.844 in (961.24 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
Q2R · Door 2 spacer R
37.969 in (964.41 mm) × 3/4 in (19.05 mm) × 3/8 in (9.53 mm)
37.844 in (961.24 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
B2B · Door 2 retaining bead B
12.422 in (315.52 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
12.297 in (312.34 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
B2T · Door 2 retaining bead T
12.422 in (315.52 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
12.297 in (312.34 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
B2L · Door 2 retaining bead L
35.469 in (900.91 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
35.344 in (897.74 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
B2R · Door 2 retaining bead R
35.469 in (900.91 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
35.344 in (897.74 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
CLB · L side B cleat
18.922 in (480.62 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
18.797 in (477.44 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CLT · L side T cleat
18.922 in (480.62 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
18.797 in (477.44 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CLV · Rear corner cleat
46.719 in (1186.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
46.594 in (1183.49 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CRB · R side B cleat
18.922 in (480.62 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
18.797 in (477.44 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CRT · R side T cleat
18.922 in (480.62 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
18.797 in (477.44 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
CRV · Rear corner cleat
46.719 in (1186.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
46.594 in (1183.49 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CFB · F floor cleat
31.719 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31.594 in (802.49 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CBB · B floor cleat
31.719 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31.594 in (802.49 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
RF · F roof ledger
31.719 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31.594 in (802.49 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
RB · B roof ledger
31.719 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31.594 in (802.49 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CCa · Front bearing column layer A
42.385 in (1076.58 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
42.26 in (1073.4 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
CCb · Front bearing column layer B
42.385 in (1076.58 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
42.26 in (1073.4 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
RC · Roof centre rib
21.922 in (556.82 mm) × 1 1/2 in (38.1 mm) × 1.334 in (33.88 mm)
21.797 in (553.64 mm) × 1 1/2 in (38.1 mm) × 1.334 in (33.88 mm)
M01 · Roof mesh blank
29 in (736.6 mm) × 13 in (330.2 mm) × 0.084 in (2.13 mm)
29 in (736.6 mm) × 13 in (330.2 mm) × 0.084 in (2.13 mm)
RB1L · Roof capture batten
14 3/8 in (365.13 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
14 1/4 in (361.95 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
RB1R · Roof capture batten
14 3/8 in (365.13 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
14 1/4 in (361.95 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
RB2L · Roof capture batten
14 3/8 in (365.13 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
14 1/4 in (361.95 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
RB2R · Roof capture batten
14 3/8 in (365.13 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
14 1/4 in (361.95 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
RB3 · Roof capture batten
12 1/8 in (307.98 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
12 in (304.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
RB4 · Roof capture batten
12 1/8 in (307.98 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
12 in (304.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
ML · L vent mesh
13 in (330.2 mm) × 3 1/2 in (88.9 mm) × 0.084 in (2.13 mm)
13 in (330.2 mm) × 3 1/2 in (88.9 mm) × 0.084 in (2.13 mm)
VLB · L vent capture B
14 1/8 in (358.78 mm) × 1 1/4 in (31.75 mm) × 3/4 in (19.05 mm)
14 in (355.6 mm) × 1 1/4 in (31.75 mm) × 3/4 in (19.05 mm)
VLT · L vent capture T
14 1/8 in (358.78 mm) × 1 1/4 in (31.75 mm) × 3/4 in (19.05 mm)
14 in (355.6 mm) × 1 1/4 in (31.75 mm) × 3/4 in (19.05 mm)
VLF · L vent capture F
2 1/8 in (53.98 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
2 in (50.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VLR · L vent capture R
2 1/8 in (53.98 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
2 in (50.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
MR · R vent mesh
13 in (330.2 mm) × 3 1/2 in (88.9 mm) × 0.084 in (2.13 mm)
13 in (330.2 mm) × 3 1/2 in (88.9 mm) × 0.084 in (2.13 mm)
VRB · R vent capture B
14 1/8 in (358.78 mm) × 1 1/4 in (31.75 mm) × 3/4 in (19.05 mm)
14 in (355.6 mm) × 1 1/4 in (31.75 mm) × 3/4 in (19.05 mm)
VRT · R vent capture T
14 1/8 in (358.78 mm) × 1 1/4 in (31.75 mm) × 3/4 in (19.05 mm)
14 in (355.6 mm) × 1 1/4 in (31.75 mm) × 3/4 in (19.05 mm)
VRF · R vent capture F
2 1/8 in (53.98 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
2 in (50.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VRR · R vent capture R
2 1/8 in (53.98 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
2 in (50.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
S10 · Door bottom stop
1 1/8 in (28.58 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
1 in (25.4 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
S11 · Door bottom stop
1 1/8 in (28.58 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
1 in (25.4 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
S20 · Door bottom stop
1 1/8 in (28.58 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
1 in (25.4 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
S21 · Door bottom stop
1 1/8 in (28.58 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
1 in (25.4 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
RT · External rear restraint receiver
31.719 in (805.66 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
31.594 in (802.49 mm) × 2 1/2 in (63.5 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
LB1 · Steel strip below the left lamp area
14 in (355.6 mm) × 1 in (25.4 mm) × 1/8 in (3.18 mm)
14 in (355.6 mm) × 1 in (25.4 mm) × 1/8 in (3.18 mm)
LB2 · Steel strip below the left lamp area
14 in (355.6 mm) × 1 in (25.4 mm) × 1/8 in (3.18 mm)
14 in (355.6 mm) × 1 in (25.4 mm) × 1/8 in (3.18 mm)
SP-H11-fixed · Rigid full-leaf bearing pad H11 fixed
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H11-moving · Rigid full-leaf bearing pad H11 moving
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H12-fixed · Rigid full-leaf bearing pad H12 fixed
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H12-moving · Rigid full-leaf bearing pad H12 moving
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H13-fixed · Rigid full-leaf bearing pad H13 fixed
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H13-moving · Rigid full-leaf bearing pad H13 moving
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H21-moving · Rigid full-leaf bearing pad H21 moving
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H21-fixed · Rigid full-leaf bearing pad H21 fixed
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
SP-H22-moving · Rigid full-leaf bearing pad H22 moving
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H22-fixed · Rigid full-leaf bearing pad H22 fixed
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H23-moving · Rigid full-leaf bearing pad H23 moving
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H23-fixed · Rigid full-leaf bearing pad H23 fixed
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
V-floor-under · Exterior veneer · floor-under
36.561 in (928.65 mm) × 24.561 in (623.85 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 24.061 in (611.15 mm) × 0.0305 in (0.77 mm)
V-roof-top · Exterior veneer · roof-top
36.561 in (928.65 mm) × 24.561 in (623.85 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 24.061 in (611.15 mm) × 0.0305 in (0.77 mm)
V-P01-front · Exterior veneer · P01-front
36.561 in (928.65 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P01-back · Exterior veneer · P01-back
36.561 in (928.65 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P01-left · Exterior veneer · P01-left
24 1/2 in (622.3 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
24 in (609.6 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P01-right · Exterior veneer · P01-right
24 1/2 in (622.3 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
24 in (609.6 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
V-P02-front · Exterior veneer · P02-front
36.561 in (928.65 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P02-back · Exterior veneer · P02-back
36.561 in (928.65 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P02-left · Exterior veneer · P02-left
24 1/2 in (622.3 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
24 in (609.6 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P02-right · Exterior veneer · P02-right
24 1/2 in (622.3 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
24 in (609.6 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03-face · Exterior veneer · P03-face
47.094 in (1196.19 mm) × 24 1/2 in (622.3 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 24 in (609.6 mm) × 0.0305 in (0.77 mm)
V-P03-front · Exterior veneer · P03-front
47.094 in (1196.19 mm) × 1.2335 in (31.33 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 0.7335 in (18.63 mm) × 0.0305 in (0.77 mm)
V-P03-back · Exterior veneer · P03-back
47.094 in (1196.19 mm) × 1.2335 in (31.33 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 0.7335 in (18.63 mm) × 0.0305 in (0.77 mm)
V-P03-vent-near · Exterior veneer · P03-vent-near
2.439 in (61.95 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
1.939 in (49.25 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03-vent-far · Exterior veneer · P03-vent-far
2.439 in (61.95 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
1.939 in (49.25 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
12 1/2 in (317.5 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
12 in (304.8 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
V-P03-vent-top · Exterior veneer · P03-vent-top
12 1/2 in (317.5 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
12 in (304.8 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P04-face · Exterior veneer · P04-face
47.094 in (1196.19 mm) × 24 1/2 in (622.3 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 24 in (609.6 mm) × 0.0305 in (0.77 mm)
V-P04-front · Exterior veneer · P04-front
47.094 in (1196.19 mm) × 1.2335 in (31.33 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 0.7335 in (18.63 mm) × 0.0305 in (0.77 mm)
V-P04-back · Exterior veneer · P04-back
47.094 in (1196.19 mm) × 1.2335 in (31.33 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 0.7335 in (18.63 mm) × 0.0305 in (0.77 mm)
V-P04-vent-near · Exterior veneer · P04-vent-near
2.439 in (61.95 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
1.939 in (49.25 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P04-vent-far · Exterior veneer · P04-vent-far
2.439 in (61.95 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
1.939 in (49.25 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
12 1/2 in (317.5 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
12 in (304.8 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P04-vent-top · Exterior veneer · P04-vent-top
12 1/2 in (317.5 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
12 in (304.8 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-back · Exterior veneer · back
47.094 in (1196.19 mm) × 35.094 in (891.39 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 34.594 in (878.69 mm) × 0.0305 in (0.77 mm)
V-RT-back · Exterior veneer · RT-back
32.155 in (816.74 mm) × 3.061 in (77.75 mm) × 0.0305 in (0.77 mm)
31.655 in (804.04 mm) × 2.561 in (65.05 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
V-RT-left · Exterior veneer · RT-left
3 in (76.2 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
2 1/2 in (63.5 mm) × 3/4 in (19.05 mm) × 0.0305 in (0.77 mm)
V-RT-right · Exterior veneer · RT-right
3 in (76.2 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
2 1/2 in (63.5 mm) × 3/4 in (19.05 mm) × 0.0305 in (0.77 mm)
V-RT-bottom · Exterior veneer · RT-bottom
32.155 in (816.74 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
31.655 in (804.04 mm) × 3/4 in (19.05 mm) × 0.0305 in (0.77 mm)
V-RT-top · Exterior veneer · RT-top
32.155 in (816.74 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
31.655 in (804.04 mm) × 3/4 in (19.05 mm) × 0.0305 in (0.77 mm)
12.439 in (315.95 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
11.939 in (303.25 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
13 3/4 in (349.25 mm) × 1.203 in (30.56 mm) × 0.0305 in (0.77 mm)
13 1/4 in (336.55 mm) × 0.703 in (17.86 mm) × 0.0305 in (0.77 mm)
V-FA-front · Exterior veneer · FA-front
47.094 in (1196.19 mm) × 3 in (76.2 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 2 1/2 in (63.5 mm) × 0.0305 in (0.77 mm)
V-FB-front · Exterior veneer · FB-front
47.094 in (1196.19 mm) × 3 in (76.2 mm) × 0.0305 in (0.77 mm)
46.594 in (1183.49 mm) × 2 1/2 in (63.5 mm) × 0.0305 in (0.77 mm)
V-FC-front · Exterior veneer · FC-front
30.094 in (764.39 mm) × 6 in (152.4 mm) × 0.0305 in (0.77 mm)
29.594 in (751.69 mm) × 5 1/2 in (139.7 mm) × 0.0305 in (0.77 mm)
V-FD-front · Exterior veneer · FD-front
30.094 in (764.39 mm) × 3 in (76.2 mm) × 0.0305 in (0.77 mm)
29.594 in (751.69 mm) × 2 1/2 in (63.5 mm) × 0.0305 in (0.77 mm)
V-FE-front · Exterior veneer · FE-front
39.094 in (992.99 mm) × 3 in (76.2 mm) × 0.0305 in (0.77 mm)
38.594 in (980.29 mm) × 2 1/2 in (63.5 mm) × 0.0305 in (0.77 mm)
V-L-jamb-left · Exterior veneer · L-jamb-left
39.033 in (991.44 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
38.533 in (978.74 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-L-jamb-right · Exterior veneer · L-jamb-right
39.033 in (991.44 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
38.533 in (978.74 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-L-sill · Exterior veneer · L-sill
14.047 in (356.79 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
13.547 in (344.09 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
V-L-head · Exterior veneer · L-head
14.047 in (356.79 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
13.547 in (344.09 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-R-jamb-left · Exterior veneer · R-jamb-left
39.033 in (991.44 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
38.533 in (978.74 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-R-jamb-right · Exterior veneer · R-jamb-right
39.033 in (991.44 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
38.533 in (978.74 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-R-sill · Exterior veneer · R-sill
14.047 in (356.79 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
13.547 in (344.09 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-R-head · Exterior veneer · R-head
14.047 in (356.79 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
13.547 in (344.09 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-D1A-front · Exterior veneer · D1A-front
38.78 in (985.01 mm) × 1.968 in (49.99 mm) × 0.0305 in (0.77 mm)
38.28 in (972.31 mm) × 1.468 in (37.29 mm) × 0.0305 in (0.77 mm)
V-D1B-front · Exterior veneer · D1B-front
38.78 in (985.01 mm) × 2.49925 in (63.48 mm) × 0.0305 in (0.77 mm)
38.28 in (972.31 mm) × 1.99925 in (50.78 mm) × 0.0305 in (0.77 mm)
V-D1C-front · Exterior veneer · D1C-front
10.297 in (261.54 mm) × 1.968 in (49.99 mm) × 0.0305 in (0.77 mm)
9.797 in (248.84 mm) × 1.468 in (37.29 mm) × 0.0305 in (0.77 mm)
V-D1D-front · Exterior veneer · D1D-front
10.297 in (261.54 mm) × 1.968 in (49.99 mm) × 0.0305 in (0.77 mm)
9.797 in (248.84 mm) × 1.468 in (37.29 mm) × 0.0305 in (0.77 mm)
V-D1-hinge-edge · Exterior veneer · D1-hinge-edge
38.719 in (983.46 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
38.219 in (970.76 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
V-D1-latch-edge · Exterior veneer · D1-latch-edge
38.719 in (983.46 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
38.219 in (970.76 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-D1-bottom · Exterior veneer · D1-bottom
13.76425 in (349.61 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
13.26425 in (336.91 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-D1-top · Exterior veneer · D1-top
13.76425 in (349.61 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
13.26425 in (336.91 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
10.297 in (261.54 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
9.797 in (248.84 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-D1-window-top · Exterior veneer · D1-window-top
10.297 in (261.54 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
9.797 in (248.84 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-D2A-front · Exterior veneer · D2A-front
38.78 in (985.01 mm) × 2.49925 in (63.48 mm) × 0.0305 in (0.77 mm)
38.28 in (972.31 mm) × 1.99925 in (50.78 mm) × 0.0305 in (0.77 mm)
V-D2B-front · Exterior veneer · D2B-front
38.78 in (985.01 mm) × 1.968 in (49.99 mm) × 0.0305 in (0.77 mm)
38.28 in (972.31 mm) × 1.468 in (37.29 mm) × 0.0305 in (0.77 mm)
V-D2C-front · Exterior veneer · D2C-front
10.297 in (261.54 mm) × 1.968 in (49.99 mm) × 0.0305 in (0.77 mm)
9.797 in (248.84 mm) × 1.468 in (37.29 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID; length follows grain. Start with the stock layouts: pine strip allocations include an extra 1/8 in (3.18 mm) rip allowance. Trim to these pre-fit sizes, then fit to the assembly. Sills use full factory width. Finished sizes are reference geometry; V-parts include the cured veneer stack. Q spacers start 3/8 in (9.53 mm) thick; fit their listed depth after the cured-stack trial. Solid neoprene has no assumed compression.
Part
Pre-fit length × width × stock thickness
Finished length × width × thickness
V-D2D-front · Exterior veneer · D2D-front
10.297 in (261.54 mm) × 1.968 in (49.99 mm) × 0.0305 in (0.77 mm)
9.797 in (248.84 mm) × 1.468 in (37.29 mm) × 0.0305 in (0.77 mm)
V-D2-hinge-edge · Exterior veneer · D2-hinge-edge
38.719 in (983.46 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
38.219 in (970.76 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-D2-latch-edge · Exterior veneer · D2-latch-edge
38.719 in (983.46 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
38.219 in (970.76 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-D2-bottom · Exterior veneer · D2-bottom
13.76425 in (349.61 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
13.26425 in (336.91 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-D2-top · Exterior veneer · D2-top
13.76425 in (349.61 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
13.26425 in (336.91 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Crosscut full-width factory-squared sill blanks. Confirm delivered width is sound and at least 5 1/2 in (139.7 mm); no rip allowance is available. Reject undersize/defective edges.
SOLID-1 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Crosscut supported long stock; fit the stated final section using safe guarded fixtures. Tool minimum feed lengths govern.
SOLID-2 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Crosscut supported long stock; fit the stated final section using safe guarded fixtures. Tool minimum feed lengths govern.
SOLID-3 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Crosscut supported long stock; fit the stated final section using safe guarded fixtures. Tool minimum feed lengths govern.
SOLID-4 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Crosscut supported long stock; fit the stated final section using safe guarded fixtures. Tool minimum feed lengths govern.
L15-1 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Ordered rectangular stock allocation; use the exact coordinates and the material-specific cutting instructions.
ACR-1 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and stock direction
Ordered rectangular stock allocation; use the exact coordinates and the material-specific cutting instructions.
MESH-1 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and stock direction
Ordered rectangular stock allocation; use the exact coordinates and the material-specific cutting instructions.
PADS-1 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Ordered rectangular stock allocation; use the exact coordinates and the material-specific cutting instructions.
HSP-1 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and stock direction
Ordered rectangular stock allocation; use the exact coordinates and the material-specific cutting instructions.
HSP-2 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and stock direction
Ordered rectangular stock allocation; use the exact coordinates and the material-specific cutting instructions.
VENEER-1 · rough-stock cutting plan
Small pieces use the numbered coordinate tables; identify each blank by its exact stock X / Y.
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Dedicated full-length pine for a complete two-layer tall-door balance trial, hardware/offcut/glazing and screen-seat coupons. No installed parts consume this allocation.
TRIAL-PINE-2 · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Dedicated full-length pine for a complete two-layer tall-door balance trial, hardware/offcut/glazing and screen-seat coupons. No installed parts consume this allocation.
TRIAL-SOLID · rough-stock cutting plan
Numbers match the ordered ID table; use exact stock coordinates and grain direction
Separate solid stock for received-screw and bearing trials; remainder reserved for defects or refitting.
Workshop drawings and measurements
PLY-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · P05
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
46.719 in (1186.66 mm) × 34.719 in (881.86 mm)
2 · P03
46.969 in (1193.01 mm) / 1/8 in (3.18 mm)
46.719 in (1186.66 mm) × 24 1/8 in (612.78 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PLY-2 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · P04
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
46.719 in (1186.66 mm) × 24 1/8 in (612.78 mm)
2 · P01
46.969 in (1193.01 mm) / 1/8 in (3.18 mm)
36 1/8 in (917.58 mm) × 24 1/8 in (612.78 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PLY-3 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · P02
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
36 1/8 in (917.58 mm) × 24 1/8 in (612.78 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PINE-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · FA
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
46.719 in (1186.66 mm) × 2 5/8 in (66.68 mm)
2 · FB
46.969 in (1193.01 mm) / 1/8 in (3.18 mm)
46.719 in (1186.66 mm) × 2 5/8 in (66.68 mm)
3 · D1B
1/8 in (3.18 mm) / 2 7/8 in (73.03 mm)
38.469 in (977.11 mm) × 2 1/8 in (53.98 mm)
4 · D2A
38.719 in (983.46 mm) / 2 7/8 in (73.03 mm)
38.469 in (977.11 mm) × 2 1/8 in (53.98 mm)
5 · D1E
77.313 in (1963.75 mm) / 2 7/8 in (73.03 mm)
13.422 in (340.92 mm) × 1 5/8 in (41.28 mm)
6 · VLF
90.86 in (2307.84 mm) / 2 7/8 in (73.03 mm)
2 1/8 in (53.98 mm) × 1 1/8 in (28.58 mm)
7 · VLR
93.11 in (2364.99 mm) / 2 7/8 in (73.03 mm)
2 1/8 in (53.98 mm) × 1 1/8 in (28.58 mm)
8 · S10
93.813 in (2382.85 mm) / 1/8 in (3.18 mm)
1 1/8 in (28.58 mm) × 1 1/8 in (28.58 mm)
9 · S11
93.813 in (2382.85 mm) / 1 3/8 in (34.93 mm)
1 1/8 in (28.58 mm) × 1 1/8 in (28.58 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PINE-2 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · FF
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
46.719 in (1186.66 mm) × 2 5/8 in (66.68 mm)
2 · CCa
46.969 in (1193.01 mm) / 1/8 in (3.18 mm)
42.385 in (1076.58 mm) × 2 5/8 in (66.68 mm)
3 · D1H
1/8 in (3.18 mm) / 2 7/8 in (73.03 mm)
35.469 in (900.91 mm) × 2 1/8 in (53.98 mm)
4 · D2G
35.719 in (907.26 mm) / 2 7/8 in (73.03 mm)
35.469 in (900.91 mm) × 2 1/8 in (53.98 mm)
5 · D1F
71.313 in (1811.35 mm) / 2 7/8 in (73.03 mm)
13.422 in (340.92 mm) × 1 5/8 in (41.28 mm)
6 · D1C
84.86 in (2155.44 mm) / 2 7/8 in (73.03 mm)
9.922 in (252.02 mm) × 1 5/8 in (41.28 mm)
7 · VRF
89.479 in (2272.77 mm) / 1/8 in (3.18 mm)
2 1/8 in (53.98 mm) × 1 1/8 in (28.58 mm)
8 · VRR
91.729 in (2329.92 mm) / 1/8 in (3.18 mm)
2 1/8 in (53.98 mm) × 1 1/8 in (28.58 mm)
9 · S20
93.979 in (2387.07 mm) / 1/8 in (3.18 mm)
1 1/8 in (28.58 mm) × 1 1/8 in (28.58 mm)
10 · S21
89.479 in (2272.77 mm) / 1 3/8 in (34.93 mm)
1 1/8 in (28.58 mm) × 1 1/8 in (28.58 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PINE-3 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · CCb
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
42.385 in (1076.58 mm) × 2 5/8 in (66.68 mm)
2 · FE
42.635 in (1082.93 mm) / 1/8 in (3.18 mm)
38.719 in (983.46 mm) × 2 5/8 in (66.68 mm)
3 · D1A
42.635 in (1082.93 mm) / 2 7/8 in (73.03 mm)
38.469 in (977.11 mm) × 1 5/8 in (41.28 mm)
4 · D2B
1/8 in (3.18 mm) / 2 7/8 in (73.03 mm)
38.469 in (977.11 mm) × 1 5/8 in (41.28 mm)
5 · D2E
81.479 in (2069.57 mm) / 1/8 in (3.18 mm)
13.422 in (340.92 mm) × 1 5/8 in (41.28 mm)
6 · D2F
81.479 in (2069.57 mm) / 1 7/8 in (47.63 mm)
13.422 in (340.92 mm) × 1 5/8 in (41.28 mm)
7 · D1D
81.479 in (2069.57 mm) / 3 5/8 in (92.08 mm)
9.922 in (252.02 mm) × 1 5/8 in (41.28 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PINE-4 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · FI
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
38.719 in (983.46 mm) × 2 5/8 in (66.68 mm)
2 · FJ
38.969 in (989.81 mm) / 1/8 in (3.18 mm)
38.719 in (983.46 mm) × 2 5/8 in (66.68 mm)
3 · FHL
77.813 in (1976.45 mm) / 1/8 in (3.18 mm)
16.172 in (410.77 mm) × 2 5/8 in (66.68 mm)
4 · D1G
1/8 in (3.18 mm) / 2 7/8 in (73.03 mm)
35.469 in (900.91 mm) × 1 5/8 in (41.28 mm)
5 · D2H
35.719 in (907.26 mm) / 2 7/8 in (73.03 mm)
35.469 in (900.91 mm) × 1 5/8 in (41.28 mm)
6 · D2C
71.313 in (1811.35 mm) / 2 7/8 in (73.03 mm)
9.922 in (252.02 mm) × 1 5/8 in (41.28 mm)
7 · D2D
81.36 in (2066.54 mm) / 2 7/8 in (73.03 mm)
9.922 in (252.02 mm) × 1 5/8 in (41.28 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PINE-5 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · RT
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
31.719 in (805.66 mm) × 2 5/8 in (66.68 mm)
2 · FD
31.969 in (812.01 mm) / 1/8 in (3.18 mm)
29.719 in (754.86 mm) × 2 5/8 in (66.68 mm)
3 · FHR
61.813 in (1570.05 mm) / 1/8 in (3.18 mm)
16.172 in (410.77 mm) × 2 5/8 in (66.68 mm)
4 · B1L
1/8 in (3.18 mm) / 2 7/8 in (73.03 mm)
35.469 in (900.91 mm) × 1 3/8 in (34.93 mm)
5 · B1R
35.719 in (907.26 mm) / 2 7/8 in (73.03 mm)
35.469 in (900.91 mm) × 1 3/8 in (34.93 mm)
6 · VLB
71.313 in (1811.35 mm) / 2 7/8 in (73.03 mm)
14 1/8 in (358.78 mm) × 1 3/8 in (34.93 mm)
7 · VLT
78.11 in (1983.99 mm) / 1/8 in (3.18 mm)
14 1/8 in (358.78 mm) × 1 3/8 in (34.93 mm)
8 · RB1L
78.11 in (1983.99 mm) / 1 5/8 in (41.28 mm)
14 3/8 in (365.13 mm) × 1 1/8 in (28.58 mm)
9 · Q1L
1/8 in (3.18 mm) / 4 3/8 in (111.13 mm)
37.969 in (964.41 mm) × 7/8 in (22.23 mm)
10 · Q1R
38.219 in (970.76 mm) / 4 3/8 in (111.13 mm)
37.969 in (964.41 mm) × 7/8 in (22.23 mm)
11 · Q1B
76.313 in (1938.35 mm) / 4 3/8 in (111.13 mm)
10.922 in (277.42 mm) × 7/8 in (22.23 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PINE-6 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · B2L
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
35.469 in (900.91 mm) × 1 3/8 in (34.93 mm)
2 · B2R
35.719 in (907.26 mm) / 1/8 in (3.18 mm)
35.469 in (900.91 mm) × 1 3/8 in (34.93 mm)
3 · VRB
71.313 in (1811.35 mm) / 1/8 in (3.18 mm)
14 1/8 in (358.78 mm) × 1 3/8 in (34.93 mm)
4 · VRT
1/8 in (3.18 mm) / 1 5/8 in (41.28 mm)
14 1/8 in (358.78 mm) × 1 3/8 in (34.93 mm)
5 · B1B
14 3/8 in (365.13 mm) / 1 5/8 in (41.28 mm)
12.422 in (315.52 mm) × 1 3/8 in (34.93 mm)
6 · B1T
26.922 in (683.82 mm) / 1 5/8 in (41.28 mm)
12.422 in (315.52 mm) × 1 3/8 in (34.93 mm)
7 · B2B
39.469 in (1002.51 mm) / 1 5/8 in (41.28 mm)
12.422 in (315.52 mm) × 1 3/8 in (34.93 mm)
8 · B2T
52.016 in (1321.21 mm) / 1 5/8 in (41.28 mm)
12.422 in (315.52 mm) × 1 3/8 in (34.93 mm)
9 · RB1R
64.563 in (1639.9 mm) / 1 5/8 in (41.28 mm)
14 3/8 in (365.13 mm) × 1 1/8 in (28.58 mm)
10 · RB2L
79.063 in (2008.2 mm) / 1 5/8 in (41.28 mm)
14 3/8 in (365.13 mm) × 1 1/8 in (28.58 mm)
11 · RB2R
1/8 in (3.18 mm) / 3 1/8 in (79.38 mm)
14 3/8 in (365.13 mm) × 1 1/8 in (28.58 mm)
12 · RB3
14 5/8 in (371.48 mm) / 3 1/8 in (79.38 mm)
12 1/8 in (307.98 mm) × 1 1/8 in (28.58 mm)
13 · RB4
26 7/8 in (682.63 mm) / 3 1/8 in (79.38 mm)
12 1/8 in (307.98 mm) × 1 1/8 in (28.58 mm)
14 · Q2L
1/8 in (3.18 mm) / 4 3/8 in (111.13 mm)
37.969 in (964.41 mm) × 7/8 in (22.23 mm)
15 · Q2R
38.219 in (970.76 mm) / 4 3/8 in (111.13 mm)
37.969 in (964.41 mm) × 7/8 in (22.23 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PINE-6 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
16 · Q1T
76.313 in (1938.35 mm) / 4 3/8 in (111.13 mm)
10.922 in (277.42 mm) × 7/8 in (22.23 mm)
17 · Q2B
39 1/8 in (993.78 mm) / 3 1/8 in (79.38 mm)
10.922 in (277.42 mm) × 7/8 in (22.23 mm)
18 · Q2T
50.172 in (1274.37 mm) / 3 1/8 in (79.38 mm)
10.922 in (277.42 mm) × 7/8 in (22.23 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PINE-SILL · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · FC
1/4 in (6.35 mm) / 0 in (0 mm)
29.719 in (754.86 mm) × 5 1/2 in (139.7 mm)
2 · FGL
30.094 in (764.39 mm) / 0 in (0 mm)
16.172 in (410.77 mm) × 5 1/2 in (139.7 mm)
3 · FGR
46.391 in (1178.33 mm) / 0 in (0 mm)
16.172 in (410.77 mm) × 5 1/2 in (139.7 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
SOLID-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · CLV
1/4 in (6.35 mm) / 0 in (0 mm)
46.719 in (1186.66 mm) × 1 1/2 in (38.1 mm)
2 · CRV
47.094 in (1196.19 mm) / 0 in (0 mm)
46.719 in (1186.66 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
SOLID-2 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · CFB
1/4 in (6.35 mm) / 0 in (0 mm)
31.719 in (805.66 mm) × 1 1/2 in (38.1 mm)
2 · CBB
32.094 in (815.19 mm) / 0 in (0 mm)
31.719 in (805.66 mm) × 1 1/2 in (38.1 mm)
3 · RF
63.938 in (1624.03 mm) / 0 in (0 mm)
31.719 in (805.66 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
SOLID-3 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · RB
1/4 in (6.35 mm) / 0 in (0 mm)
31.719 in (805.66 mm) × 1 1/2 in (38.1 mm)
2 · RC
32.094 in (815.19 mm) / 0 in (0 mm)
21.922 in (556.82 mm) × 1 1/2 in (38.1 mm)
3 · CLB
54.141 in (1375.18 mm) / 0 in (0 mm)
18.922 in (480.62 mm) × 1 1/2 in (38.1 mm)
4 · CLT
73.188 in (1858.98 mm) / 0 in (0 mm)
18.922 in (480.62 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
SOLID-4 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · CRB
1/4 in (6.35 mm) / 0 in (0 mm)
18.922 in (480.62 mm) × 1 1/2 in (38.1 mm)
2 · CRT
19.297 in (490.14 mm) / 0 in (0 mm)
18.922 in (480.62 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
L15-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · LB1
1/4 in (6.35 mm) / 0 in (0 mm)
14 in (355.6 mm) × 1 in (25.4 mm)
2 · LB2
14 3/8 in (365.13 mm) / 0 in (0 mm)
14 in (355.6 mm) × 1 in (25.4 mm)
Stock 36 in (914.4 mm) × 1 in (25.4 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
ACR-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · G1
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
36.094 in (916.79 mm) × 10.547 in (267.89 mm)
2 · G2
1/8 in (3.18 mm) / 10.797 in (274.24 mm)
36.094 in (916.79 mm) × 10.547 in (267.89 mm)
Stock 48 in (1219.2 mm) × 24 in (609.6 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
MESH-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · M01
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
29 in (736.6 mm) × 13 in (330.2 mm)
2 · ML
1/8 in (3.18 mm) / 13 1/4 in (336.55 mm)
13 in (330.2 mm) × 3 1/2 in (88.9 mm)
3 · MR
1/8 in (3.18 mm) / 16 7/8 in (428.63 mm)
13 in (330.2 mm) × 3 1/2 in (88.9 mm)
Stock 60 in (1524 mm) × 24 in (609.6 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
PADS-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · TRIAL-contact
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
12 in (304.8 mm) × 1/2 in (12.7 mm)
2 · N1FL
1/8 in (3.18 mm) / 0.655 in (16.64 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm)
3 · N1FR
1/8 in (3.18 mm) / 0.935 in (23.75 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm)
4 · N1RL
1/8 in (3.18 mm) / 1.215 in (30.86 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm)
5 · N1RR
1/8 in (3.18 mm) / 1.495 in (37.97 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm)
6 · N2FL
1/8 in (3.18 mm) / 1.775 in (45.09 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm)
7 · N2FR
1/8 in (3.18 mm) / 2.055 in (52.2 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm)
8 · N2RL
1/8 in (3.18 mm) / 2.335 in (59.31 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm)
9 · N2RR
1/8 in (3.18 mm) / 2.615 in (66.42 mm)
35.469 in (900.91 mm) × 1/4 in (6.35 mm)
10 · N1FB
12.155 in (308.74 mm) / 1/8 in (3.18 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm)
11 · N1FT
22.607 in (574.22 mm) / 1/8 in (3.18 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm)
12 · N1RB
1/8 in (3.18 mm) / 2.895 in (73.53 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm)
13 · N1RT
10.577 in (268.66 mm) / 2.895 in (73.53 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm)
14 · N2FB
21.029 in (534.14 mm) / 2.895 in (73.53 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm)
15 · N2FT
1/8 in (3.18 mm) / 3.175 in (80.64 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm)
Stock 36 in (914.4 mm) × 12 in (304.8 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 0.03 in (0.76 mm). Keep each blank labeled.
PADS-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
16 · N2RB
10.577 in (268.66 mm) / 3.175 in (80.64 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm)
17 · N2RT
21.029 in (534.14 mm) / 3.175 in (80.64 mm)
10.422 in (264.72 mm) × 1/4 in (6.35 mm)
18 · N1S00
12.155 in (308.74 mm) / 0.405 in (10.29 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
19 · N1S01
13.185 in (334.9 mm) / 0.405 in (10.29 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
20 · N1S10
14.215 in (361.06 mm) / 0.405 in (10.29 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
21 · N1S11
15.245 in (387.22 mm) / 0.405 in (10.29 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
22 · N2S00
16.275 in (413.39 mm) / 0.405 in (10.29 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
23 · N2S01
17.305 in (439.55 mm) / 0.405 in (10.29 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
24 · N2S10
18.335 in (465.71 mm) / 0.405 in (10.29 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
25 · N2S11
19.365 in (491.87 mm) / 0.405 in (10.29 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
Stock 36 in (914.4 mm) × 12 in (304.8 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 0.03 in (0.76 mm). Keep each blank labeled.
HSP-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · SP-H11-fixed
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
2 · SP-H11-moving
3 3/16 in (80.96 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
3 · SP-H12-fixed
6 1/4 in (158.75 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
4 · SP-H12-moving
9 5/16 in (236.54 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
5 · SP-H13-fixed
12 3/8 in (314.33 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
6 · SP-H13-moving
15 7/16 in (392.11 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
7 · SP-H21-moving
18 1/2 in (469.9 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
8 · SP-H21-fixed
21 9/16 in (547.69 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
9 · SP-H22-moving
24 5/8 in (625.48 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
10 · SP-H22-fixed
27 11/16 in (703.26 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
11 · SP-H23-moving
30 3/4 in (781.05 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
Stock 36 in (914.4 mm) × 1 1/2 in (38.1 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/16 in (1.59 mm). Keep each blank labeled.
HSP-2 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · SP-H23-fixed
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
2 · TRIAL-HSP1
3 3/16 in (80.96 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
3 · TRIAL-HSP2
6 1/4 in (158.75 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
Stock 36 in (914.4 mm) × 1 1/2 in (38.1 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/16 in (1.59 mm). Keep each blank labeled.
VENEER-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · V-back
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
47.094 in (1196.19 mm) × 35.094 in (891.39 mm)
2 · V-FA-front
1/8 in (3.18 mm) / 35.344 in (897.74 mm)
47.094 in (1196.19 mm) × 3 in (76.2 mm)
3 · V-FB-front
1/8 in (3.18 mm) / 38.469 in (977.11 mm)
47.094 in (1196.19 mm) × 3 in (76.2 mm)
4 · V-FE-front
1/8 in (3.18 mm) / 41.594 in (1056.49 mm)
39.094 in (992.99 mm) × 3 in (76.2 mm)
5 · TRIAL-full-door
47.344 in (1202.54 mm) / 1/8 in (3.18 mm)
39 in (990.6 mm) × 14 in (355.6 mm)
6 · V-D1B-front
47.344 in (1202.54 mm) / 14 1/4 in (361.95 mm)
38.78 in (985.01 mm) × 2.49925 in (63.48 mm)
7 · V-floor-under
47.344 in (1202.54 mm) / 16.87425 in (428.61 mm)
36.561 in (928.65 mm) × 24.561 in (623.85 mm)
8 · V-RT-back
1/8 in (3.18 mm) / 44.719 in (1135.86 mm)
32.155 in (816.74 mm) × 3.061 in (77.75 mm)
9 · V-FC-front
47.344 in (1202.54 mm) / 41.56025 in (1055.63 mm)
30.094 in (764.39 mm) × 6 in (152.4 mm)
10 · V-RT-left
32.405 in (823.09 mm) / 44.719 in (1135.86 mm)
3 in (76.2 mm) × 1 1/4 in (31.75 mm)
11 · V-RT-right
32.405 in (823.09 mm) / 46.094 in (1170.79 mm)
3 in (76.2 mm) × 1 1/4 in (31.75 mm)
12 · V-P03-vent-near
35.53 in (902.46 mm) / 44.719 in (1135.86 mm)
2.439 in (61.95 mm) × 1.203 in (30.56 mm)
13 · V-P03-vent-far
35.53 in (902.46 mm) / 46.047 in (1169.59 mm)
2.439 in (61.95 mm) × 1.203 in (30.56 mm)
14 · V-P04-vent-near
77.563 in (1970.1 mm) / 41.56025 in (1055.63 mm)
2.439 in (61.95 mm) × 1.203 in (30.56 mm)
15 · V-P04-vent-far
77.563 in (1970.1 mm) / 42.88825 in (1089.36 mm)
2.439 in (61.95 mm) × 1.203 in (30.56 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
VENEER-2 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · V-roof-top
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
36.561 in (928.65 mm) × 24.561 in (623.85 mm)
2 · V-P03-face
36.811 in (935 mm) / 1/8 in (3.18 mm)
47.094 in (1196.19 mm) × 24 1/2 in (622.3 mm)
3 · V-FD-front
1/8 in (3.18 mm) / 24.811 in (630.2 mm)
30.094 in (764.39 mm) × 3 in (76.2 mm)
4 · V-D2A-front
30.344 in (770.74 mm) / 24.811 in (630.2 mm)
38.78 in (985.01 mm) × 2.49925 in (63.48 mm)
5 · V-L-jamb-left
1/8 in (3.18 mm) / 27.936 in (709.57 mm)
39.033 in (991.44 mm) × 2 in (50.8 mm)
6 · V-L-jamb-right
39.283 in (997.79 mm) / 27.936 in (709.57 mm)
39.033 in (991.44 mm) × 2 in (50.8 mm)
7 · V-R-jamb-left
1/8 in (3.18 mm) / 30.061 in (763.55 mm)
39.033 in (991.44 mm) × 2 in (50.8 mm)
8 · V-R-jamb-right
39.283 in (997.79 mm) / 30.061 in (763.55 mm)
39.033 in (991.44 mm) × 2 in (50.8 mm)
9 · V-D1-hinge-edge
1/8 in (3.18 mm) / 32.186 in (817.52 mm)
38.719 in (983.46 mm) × 2 in (50.8 mm)
10 · V-D1-latch-edge
38.969 in (989.81 mm) / 32.186 in (817.52 mm)
38.719 in (983.46 mm) × 2 in (50.8 mm)
11 · V-D2-hinge-edge
1/8 in (3.18 mm) / 34.311 in (871.5 mm)
38.719 in (983.46 mm) × 2 in (50.8 mm)
12 · V-D2-latch-edge
38.969 in (989.81 mm) / 34.311 in (871.5 mm)
38.719 in (983.46 mm) × 2 in (50.8 mm)
13 · V-D1-window-left
1/8 in (3.18 mm) / 36.436 in (925.47 mm)
35.783 in (908.89 mm) × 2 in (50.8 mm)
14 · V-D1-window-right
36.033 in (915.24 mm) / 36.436 in (925.47 mm)
35.783 in (908.89 mm) × 2 in (50.8 mm)
15 · V-D2-window-left
1/8 in (3.18 mm) / 38.561 in (979.45 mm)
35.783 in (908.89 mm) × 2 in (50.8 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
VENEER-2 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
16 · V-D2-window-right
36.033 in (915.24 mm) / 38.561 in (979.45 mm)
35.783 in (908.89 mm) × 2 in (50.8 mm)
17 · V-L-sill
78.441 in (1992.4 mm) / 27.936 in (709.57 mm)
14.047 in (356.79 mm) × 2 in (50.8 mm)
18 · V-L-head
78.441 in (1992.4 mm) / 30.061 in (763.55 mm)
14.047 in (356.79 mm) × 2 in (50.8 mm)
19 · V-R-sill
77.813 in (1976.45 mm) / 32.186 in (817.52 mm)
14.047 in (356.79 mm) × 2 in (50.8 mm)
20 · V-R-head
77.813 in (1976.45 mm) / 34.311 in (871.5 mm)
14.047 in (356.79 mm) × 2 in (50.8 mm)
21 · V-D1-bottom
71.941 in (1827.3 mm) / 36.436 in (925.47 mm)
13.76425 in (349.61 mm) × 2 in (50.8 mm)
22 · V-D1-top
71.941 in (1827.3 mm) / 38.561 in (979.45 mm)
13.76425 in (349.61 mm) × 2 in (50.8 mm)
23 · V-D2-bottom
69.249 in (1758.92 mm) / 24.811 in (630.2 mm)
13.76425 in (349.61 mm) × 2 in (50.8 mm)
24 · V-D2-top
1/8 in (3.18 mm) / 40.686 in (1033.42 mm)
13.76425 in (349.61 mm) × 2 in (50.8 mm)
25 · V-D1-window-bottom
83.13825 in (2111.71 mm) / 24.811 in (630.2 mm)
10.297 in (261.54 mm) × 2 in (50.8 mm)
26 · V-D1-window-top
14.01425 in (355.96 mm) / 40.686 in (1033.42 mm)
10.297 in (261.54 mm) × 2 in (50.8 mm)
27 · V-D2-window-bottom
24.43625 in (620.68 mm) / 40.686 in (1033.42 mm)
10.297 in (261.54 mm) × 2 in (50.8 mm)
28 · V-D2-window-top
34.85825 in (885.4 mm) / 40.686 in (1033.42 mm)
10.297 in (261.54 mm) × 2 in (50.8 mm)
29 · V-D2B-front
45.28025 in (1150.12 mm) / 40.686 in (1033.42 mm)
38.78 in (985.01 mm) × 1.968 in (49.99 mm)
30 · V-D1C-front
84.18525 in (2138.31 mm) / 40.686 in (1033.42 mm)
10.297 in (261.54 mm) × 1.968 in (49.99 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
VENEER-2 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
31 · V-D1D-front
84.03 in (2134.36 mm) / 1/8 in (3.18 mm)
10.297 in (261.54 mm) × 1.968 in (49.99 mm)
32 · V-D2C-front
84.03 in (2134.36 mm) / 2.218 in (56.34 mm)
10.297 in (261.54 mm) × 1.968 in (49.99 mm)
33 · V-D2D-front
84.03 in (2134.36 mm) / 4.311 in (109.5 mm)
10.297 in (261.54 mm) × 1.968 in (49.99 mm)
34 · V-D1A-front
1/8 in (3.18 mm) / 42.811 in (1087.4 mm)
38.78 in (985.01 mm) × 1.968 in (49.99 mm)
35 · V-RT-bottom
39.03 in (991.36 mm) / 42.811 in (1087.4 mm)
32.155 in (816.74 mm) × 1 1/4 in (31.75 mm)
36 · V-RT-top
1/8 in (3.18 mm) / 44.904 in (1140.56 mm)
32.155 in (816.74 mm) × 1 1/4 in (31.75 mm)
37 · V-P03-front
32.405 in (823.09 mm) / 44.904 in (1140.56 mm)
47.094 in (1196.19 mm) × 1.2335 in (31.33 mm)
38 · V-P03-back
1/8 in (3.18 mm) / 46.279 in (1175.49 mm)
47.094 in (1196.19 mm) × 1.2335 in (31.33 mm)
39 · V-P04-front
47.344 in (1202.54 mm) / 46.279 in (1175.49 mm)
47.094 in (1196.19 mm) × 1.2335 in (31.33 mm)
40 · V-P01-left
71.31 in (1811.27 mm) / 42.811 in (1087.4 mm)
24 1/2 in (622.3 mm) × 1.203 in (30.56 mm)
41 · V-roof-opening-1-front
79.624 in (2022.45 mm) / 44.904 in (1140.56 mm)
13 3/4 in (349.25 mm) × 1.203 in (30.56 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
VENEER-3 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · V-P04-face
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
47.094 in (1196.19 mm) × 24 1/2 in (622.3 mm)
2 · V-P04-back
1/8 in (3.18 mm) / 24 3/4 in (628.65 mm)
47.094 in (1196.19 mm) × 1.2335 in (31.33 mm)
3 · V-P01-front
1/8 in (3.18 mm) / 26.1085 in (663.16 mm)
36.561 in (928.65 mm) × 1.203 in (30.56 mm)
4 · V-P01-back
1/8 in (3.18 mm) / 27.4365 in (696.89 mm)
36.561 in (928.65 mm) × 1.203 in (30.56 mm)
5 · V-P02-front
1/8 in (3.18 mm) / 28.7645 in (730.62 mm)
36.561 in (928.65 mm) × 1.203 in (30.56 mm)
6 · V-P02-back
1/8 in (3.18 mm) / 30.0925 in (764.35 mm)
36.561 in (928.65 mm) × 1.203 in (30.56 mm)
7 · V-P01-right
1/8 in (3.18 mm) / 31.4205 in (798.08 mm)
24 1/2 in (622.3 mm) × 1.203 in (30.56 mm)
8 · V-P02-left
1/8 in (3.18 mm) / 32.7485 in (831.81 mm)
24 1/2 in (622.3 mm) × 1.203 in (30.56 mm)
9 · V-P02-right
1/8 in (3.18 mm) / 34.0765 in (865.54 mm)
24 1/2 in (622.3 mm) × 1.203 in (30.56 mm)
10 · V-roof-opening-1-back
1/8 in (3.18 mm) / 35.4045 in (899.27 mm)
13 3/4 in (349.25 mm) × 1.203 in (30.56 mm)
11 · V-roof-opening-2-front
1/8 in (3.18 mm) / 36.7325 in (933.01 mm)
13 3/4 in (349.25 mm) × 1.203 in (30.56 mm)
12 · V-roof-opening-2-back
1/8 in (3.18 mm) / 38.0605 in (966.74 mm)
13 3/4 in (349.25 mm) × 1.203 in (30.56 mm)
13 · V-P03-vent-bottom
1/8 in (3.18 mm) / 39.3885 in (1000.47 mm)
12 1/2 in (317.5 mm) × 1.203 in (30.56 mm)
14 · V-P03-vent-top
1/8 in (3.18 mm) / 40.7165 in (1034.2 mm)
12 1/2 in (317.5 mm) × 1.203 in (30.56 mm)
15 · V-P04-vent-bottom
1/8 in (3.18 mm) / 42.0445 in (1067.93 mm)
12 1/2 in (317.5 mm) × 1.203 in (30.56 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
VENEER-3 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
16 · V-P04-vent-top
1/8 in (3.18 mm) / 43.3725 in (1101.66 mm)
12 1/2 in (317.5 mm) × 1.203 in (30.56 mm)
17 · V-roof-opening-1-left
1/8 in (3.18 mm) / 44.7005 in (1135.39 mm)
12.439 in (315.95 mm) × 1.203 in (30.56 mm)
18 · V-roof-opening-1-right
1/8 in (3.18 mm) / 46.0285 in (1169.12 mm)
12.439 in (315.95 mm) × 1.203 in (30.56 mm)
19 · V-roof-opening-2-left
47.344 in (1202.54 mm) / 1/8 in (3.18 mm)
12.439 in (315.95 mm) × 1.203 in (30.56 mm)
20 · V-roof-opening-2-right
47.344 in (1202.54 mm) / 1.453 in (36.91 mm)
12.439 in (315.95 mm) × 1.203 in (30.56 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); End trim 1/8 in (3.18 mm); edge trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
TRIAL-PINE-1 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · TRIAL-tall-door-and-fit-1
1/4 in (6.35 mm) / 0 in (0 mm)
95 in (2413 mm) × 5 1/2 in (139.7 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
TRIAL-PINE-2 · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · TRIAL-tall-door-and-fit-2
1/4 in (6.35 mm) / 0 in (0 mm)
95 in (2413 mm) × 5 1/2 in (139.7 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
TRIAL-SOLID · rough blank positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembled fastener stations.
Number / ID
Stock X / Y
Rough length × width
1 · TRIAL-bearing-and-pilots
1/4 in (6.35 mm) / 0 in (0 mm)
30 in (762 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); End trim 1/4 in (6.35 mm); edge trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm). Keep each blank labeled.
Use the exact fastener stations
Fastener IDs are stable source labels; embedded numbers are not current coordinates. Use the station columns. Assembly X / Y / Z start at outside LEFT / outside FRONT / FLOOR UNDERSIDE. Direction gives the driver axis. Transfer actual clamped receiver centrelines. Include the drill point in stopped depth. Hardware samples control purchased holes and seating.
Install frame and door lamination screws on the bench before their assemblies enter the shell. The thirty-six #8 flat-head hinge screws pass through received countersunk leaves and matched rigid pads. Veneer leaves all bearing and service seats open.
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
FL1.9529999999999998-01 · SCREW8-125
FGL → FA
1.953 / 1.5 / 1.953 in 49.61 / 38.10 / 49.61 mm
−Y · 1 1/4 in (31.75 mm)
FL1.9529999999999998-02 · SCREW8-125
FGL → FA
1.953 / 1.5 / 4.953 in 49.61 / 38.10 / 125.81 mm
−Y · 1 1/4 in (31.75 mm)
FL1.9529999999999998-03 · SCREW8-125
FI → FA
1.953 / 1.5 / 10 in 49.61 / 38.10 / 254.00 mm
−Y · 1 1/4 in (31.75 mm)
FL1.9529999999999998-04 · SCREW8-125
FI → FA
1.953 / 1.5 / 18 in 49.61 / 38.10 / 457.20 mm
−Y · 1 1/4 in (31.75 mm)
FL1.9529999999999998-05 · SCREW8-125
FI → FA
1.953 / 1.5 / 26 in 49.61 / 38.10 / 660.40 mm
−Y · 1 1/4 in (31.75 mm)
FL1.9529999999999998-06 · SCREW8-125
FI → FA
1.953 / 1.5 / 34 in 49.61 / 38.10 / 863.60 mm
−Y · 1 1/4 in (31.75 mm)
FL1.9529999999999998-07 · SCREW8-125
FI → FA
1.953 / 1.5 / 42 in 49.61 / 38.10 / 1066.80 mm
−Y · 1 1/4 in (31.75 mm)
FL1.9529999999999998-08 · SCREW8-125
FHL → FA
1.953 / 1.5 / 46.047 in 49.61 / 38.10 / 1169.59 mm
−Y · 1 1/4 in (31.75 mm)
FL18-01 · SCREW8-125
FF → FC
18 / 1.5 / 1.953 in 457.20 / 38.10 / 49.61 mm
−Y · 1 1/4 in (31.75 mm)
FL18-02 · SCREW8-125
FF → FC
18 / 1.5 / 4.953 in 457.20 / 38.10 / 125.81 mm
−Y · 1 1/4 in (31.75 mm)
FL18-03 · SCREW8-125
FF → FE
18 / 1.5 / 10 in 457.20 / 38.10 / 254.00 mm
−Y · 1 1/4 in (31.75 mm)
FL18-04 · SCREW8-125
FF → FE
18 / 1.5 / 18 in 457.20 / 38.10 / 457.20 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 13–24
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
FL18-05 · SCREW8-125
FF → FE
18 / 1.5 / 26 in 457.20 / 38.10 / 660.40 mm
−Y · 1 1/4 in (31.75 mm)
FL18-06 · SCREW8-125
FF → FE
18 / 1.5 / 34 in 457.20 / 38.10 / 863.60 mm
−Y · 1 1/4 in (31.75 mm)
FL18-07 · SCREW8-125
FF → FE
18 / 1.5 / 42 in 457.20 / 38.10 / 1066.80 mm
−Y · 1 1/4 in (31.75 mm)
FL18-08 · SCREW8-125
FF → FD
18 / 1.5 / 46.047 in 457.20 / 38.10 / 1169.59 mm
−Y · 1 1/4 in (31.75 mm)
FL34.047-01 · SCREW8-125
FGR → FB
34.047 / 1.5 / 1.953 in 864.79 / 38.10 / 49.61 mm
−Y · 1 1/4 in (31.75 mm)
FL34.047-02 · SCREW8-125
FGR → FB
34.047 / 1.5 / 4.953 in 864.79 / 38.10 / 125.81 mm
−Y · 1 1/4 in (31.75 mm)
FL34.047-03 · SCREW8-125
FJ → FB
34.047 / 1.5 / 10 in 864.79 / 38.10 / 254.00 mm
−Y · 1 1/4 in (31.75 mm)
FL34.047-04 · SCREW8-125
FJ → FB
34.047 / 1.5 / 18 in 864.79 / 38.10 / 457.20 mm
−Y · 1 1/4 in (31.75 mm)
FL34.047-05 · SCREW8-125
FJ → FB
34.047 / 1.5 / 26 in 864.79 / 38.10 / 660.40 mm
−Y · 1 1/4 in (31.75 mm)
FL34.047-06 · SCREW8-125
FJ → FB
34.047 / 1.5 / 34 in 864.79 / 38.10 / 863.60 mm
−Y · 1 1/4 in (31.75 mm)
FL34.047-07 · SCREW8-125
FJ → FB
34.047 / 1.5 / 42 in 864.79 / 38.10 / 1066.80 mm
−Y · 1 1/4 in (31.75 mm)
FL34.047-08 · SCREW8-125
FHR → FB
34.047 / 1.5 / 46.047 in 864.79 / 38.10 / 1169.59 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 25–36
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
FR3.453-01 · SCREW8-125
FGL → FC
6 / 1.5 / 3.453 in 152.40 / 38.10 / 87.71 mm
−Y · 1 1/4 in (31.75 mm)
FR3.453-02 · SCREW8-125
FGL → FC
11 / 1.5 / 3.453 in 279.40 / 38.10 / 87.71 mm
−Y · 1 1/4 in (31.75 mm)
FR3.453-03 · SCREW8-125
FGR → FC
25 / 1.5 / 3.453 in 635.00 / 38.10 / 87.71 mm
−Y · 1 1/4 in (31.75 mm)
FR3.453-04 · SCREW8-125
FGR → FC
30 / 1.5 / 3.453 in 762.00 / 38.10 / 87.71 mm
−Y · 1 1/4 in (31.75 mm)
FR46.047-01 · SCREW8-125
FHL → FD
6 / 1.5 / 46.047 in 152.40 / 38.10 / 1169.59 mm
−Y · 1 1/4 in (31.75 mm)
FR46.047-02 · SCREW8-125
FHL → FD
11 / 1.5 / 46.047 in 279.40 / 38.10 / 1169.59 mm
−Y · 1 1/4 in (31.75 mm)
FR46.047-03 · SCREW8-125
FHR → FD
25 / 1.5 / 46.047 in 635.00 / 38.10 / 1169.59 mm
−Y · 1 1/4 in (31.75 mm)
FR46.047-04 · SCREW8-125
FHR → FD
30 / 1.5 / 46.047 in 762.00 / 38.10 / 1169.59 mm
−Y · 1 1/4 in (31.75 mm)
DL1-01 · SCREW8-125
D1E → D1A
4.453 / 1.5 / 7.078 in 113.11 / 38.10 / 179.78 mm
−Y · 1 1/4 in (31.75 mm)
DL1-02 · SCREW8-125
D1G → D1A
4.453 / 1.5 / 11.328 in 113.11 / 38.10 / 287.73 mm
−Y · 1 1/4 in (31.75 mm)
DL1-03 · SCREW8-125
D1G → D1A
4.453 / 1.5 / 19.328 in 113.11 / 38.10 / 490.93 mm
−Y · 1 1/4 in (31.75 mm)
DL1-04 · SCREW8-125
D1G → D1A
4.453 / 1.5 / 27.328 in 113.11 / 38.10 / 694.13 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 37–48
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
DL1-05 · SCREW8-125
D1G → D1A
4.453 / 1.5 / 35.328 in 113.11 / 38.10 / 897.33 mm
−Y · 1 1/4 in (31.75 mm)
DL1-06 · SCREW8-125
D1F → D1A
4.453 / 1.5 / 43.922 in 113.11 / 38.10 / 1115.62 mm
−Y · 1 1/4 in (31.75 mm)
DL1-07 · SCREW8-125
D1E → D1B
15 / 1.5 / 7.078 in 381.00 / 38.10 / 179.78 mm
−Y · 1 1/4 in (31.75 mm)
DL1-08 · SCREW8-125
D1H → D1B
15 / 1.5 / 11.328 in 381.00 / 38.10 / 287.73 mm
−Y · 1 1/4 in (31.75 mm)
DL1-09 · SCREW8-125
D1H → D1B
15 / 1.5 / 19.328 in 381.00 / 38.10 / 490.93 mm
−Y · 1 1/4 in (31.75 mm)
DL1-10 · SCREW8-125
D1H → D1B
15 / 1.5 / 27.328 in 381.00 / 38.10 / 694.13 mm
−Y · 1 1/4 in (31.75 mm)
DL1-11 · SCREW8-125
D1H → D1B
15 / 1.5 / 35.328 in 381.00 / 38.10 / 897.33 mm
−Y · 1 1/4 in (31.75 mm)
DL1-12 · SCREW8-125
D1F → D1B
15 / 1.5 / 43.922 in 381.00 / 38.10 / 1115.62 mm
−Y · 1 1/4 in (31.75 mm)
DG1-01 · SCREW6-125
B1B + Q1L → D1E
3.953 / 2.101 / 6.953 in 100.41 / 53.37 / 176.61 mm
−Y · 1 1/4 in (31.75 mm)
DG1-02 · SCREW6-125
B1L + Q1L → D1G
3.953 / 2.101 / 12.453 in 100.41 / 53.37 / 316.31 mm
−Y · 1 1/4 in (31.75 mm)
DG1-03 · SCREW6-125
B1L + Q1L → D1G
3.953 / 2.101 / 21.453 in 100.41 / 53.37 / 544.91 mm
−Y · 1 1/4 in (31.75 mm)
DG1-04 · SCREW6-125
B1L + Q1L → D1G
3.953 / 2.101 / 30.453 in 100.41 / 53.37 / 773.51 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 49–60
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
DG1-05 · SCREW6-125
B1T + Q1L → D1F
3.953 / 2.101 / 44.047 in 100.41 / 53.37 / 1118.79 mm
−Y · 1 1/4 in (31.75 mm)
DG1-06 · SCREW6-125
B1B + Q1R → D1E
15.5 / 2.101 / 6.953 in 393.70 / 53.37 / 176.61 mm
−Y · 1 1/4 in (31.75 mm)
DG1-07 · SCREW6-125
B1R + Q1R → D1H
15.5 / 2.101 / 12.453 in 393.70 / 53.37 / 316.31 mm
−Y · 1 1/4 in (31.75 mm)
DG1-08 · SCREW6-125
B1R + Q1R → D1H
15.5 / 2.101 / 21.453 in 393.70 / 53.37 / 544.91 mm
−Y · 1 1/4 in (31.75 mm)
DG1-09 · SCREW6-125
B1R + Q1R → D1H
15.5 / 2.101 / 30.453 in 393.70 / 53.37 / 773.51 mm
−Y · 1 1/4 in (31.75 mm)
DG1-10 · SCREW6-125
B1T + Q1R → D1F
15.5 / 2.101 / 44.047 in 393.70 / 53.37 / 1118.79 mm
−Y · 1 1/4 in (31.75 mm)
DGT1-01 · SCREW6-125
B1B + Q1B → D1E
9.7265 / 2.101 / 6.953 in 247.05 / 53.37 / 176.61 mm
−Y · 1 1/4 in (31.75 mm)
DGT1-02 · SCREW6-125
B1T + Q1T → D1F
9.7265 / 2.101 / 44.047 in 247.05 / 53.37 / 1118.79 mm
−Y · 1 1/4 in (31.75 mm)
DL2-01 · SCREW8-125
D2E → D2A
21 / 1.5 / 7.078 in 533.40 / 38.10 / 179.78 mm
−Y · 1 1/4 in (31.75 mm)
DL2-02 · SCREW8-125
D2G → D2A
21 / 1.5 / 11.328 in 533.40 / 38.10 / 287.73 mm
−Y · 1 1/4 in (31.75 mm)
DL2-03 · SCREW8-125
D2G → D2A
21 / 1.5 / 19.328 in 533.40 / 38.10 / 490.93 mm
−Y · 1 1/4 in (31.75 mm)
DL2-04 · SCREW8-125
D2G → D2A
21 / 1.5 / 27.328 in 533.40 / 38.10 / 694.13 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 61–72
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
DL2-05 · SCREW8-125
D2G → D2A
21 / 1.5 / 35.328 in 533.40 / 38.10 / 897.33 mm
−Y · 1 1/4 in (31.75 mm)
DL2-06 · SCREW8-125
D2F → D2A
21 / 1.5 / 43.922 in 533.40 / 38.10 / 1115.62 mm
−Y · 1 1/4 in (31.75 mm)
DL2-07 · SCREW8-125
D2E → D2B
31.547 / 1.5 / 7.078 in 801.29 / 38.10 / 179.78 mm
−Y · 1 1/4 in (31.75 mm)
DL2-08 · SCREW8-125
D2H → D2B
31.547 / 1.5 / 11.328 in 801.29 / 38.10 / 287.73 mm
−Y · 1 1/4 in (31.75 mm)
DL2-09 · SCREW8-125
D2H → D2B
31.547 / 1.5 / 19.328 in 801.29 / 38.10 / 490.93 mm
−Y · 1 1/4 in (31.75 mm)
DL2-10 · SCREW8-125
D2H → D2B
31.547 / 1.5 / 27.328 in 801.29 / 38.10 / 694.13 mm
−Y · 1 1/4 in (31.75 mm)
DL2-11 · SCREW8-125
D2H → D2B
31.547 / 1.5 / 35.328 in 801.29 / 38.10 / 897.33 mm
−Y · 1 1/4 in (31.75 mm)
DL2-12 · SCREW8-125
D2F → D2B
31.547 / 1.5 / 43.922 in 801.29 / 38.10 / 1115.62 mm
−Y · 1 1/4 in (31.75 mm)
DG2-01 · SCREW6-125
B2B + Q2L → D2E
20.5 / 2.101 / 6.953 in 520.70 / 53.37 / 176.61 mm
−Y · 1 1/4 in (31.75 mm)
DG2-02 · SCREW6-125
B2L + Q2L → D2G
20.5 / 2.101 / 12.453 in 520.70 / 53.37 / 316.31 mm
−Y · 1 1/4 in (31.75 mm)
DG2-03 · SCREW6-125
B2L + Q2L → D2G
20.5 / 2.101 / 21.453 in 520.70 / 53.37 / 544.91 mm
−Y · 1 1/4 in (31.75 mm)
DG2-04 · SCREW6-125
B2L + Q2L → D2G
20.5 / 2.101 / 30.453 in 520.70 / 53.37 / 773.51 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 73–84
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
DG2-05 · SCREW6-125
B2T + Q2L → D2F
20.5 / 2.101 / 44.047 in 520.70 / 53.37 / 1118.79 mm
−Y · 1 1/4 in (31.75 mm)
DG2-06 · SCREW6-125
B2B + Q2R → D2E
32.047 / 2.101 / 6.953 in 813.99 / 53.37 / 176.61 mm
−Y · 1 1/4 in (31.75 mm)
DG2-07 · SCREW6-125
B2R + Q2R → D2H
32.047 / 2.101 / 12.453 in 813.99 / 53.37 / 316.31 mm
−Y · 1 1/4 in (31.75 mm)
DG2-08 · SCREW6-125
B2R + Q2R → D2H
32.047 / 2.101 / 21.453 in 813.99 / 53.37 / 544.91 mm
−Y · 1 1/4 in (31.75 mm)
DG2-09 · SCREW6-125
B2R + Q2R → D2H
32.047 / 2.101 / 30.453 in 813.99 / 53.37 / 773.51 mm
−Y · 1 1/4 in (31.75 mm)
DG2-10 · SCREW6-125
B2T + Q2R → D2F
32.047 / 2.101 / 44.047 in 813.99 / 53.37 / 1118.79 mm
−Y · 1 1/4 in (31.75 mm)
DGT2-01 · SCREW6-125
B2B + Q2B → D2E
26.2735 / 2.101 / 6.953 in 667.35 / 53.37 / 176.61 mm
−Y · 1 1/4 in (31.75 mm)
DGT2-02 · SCREW6-125
B2T + Q2T → D2F
26.2735 / 2.101 / 44.047 in 667.35 / 53.37 / 1118.79 mm
−Y · 1 1/4 in (31.75 mm)
STOP10 · SCREW8-125
S10 → FGL
3.828 / 2.25 / 5.828 in 97.23 / 57.15 / 148.03 mm
−Y · 1 1/4 in (31.75 mm)
STOP11 · SCREW8-125
S11 → FGL
16.125 / 2.25 / 5.828 in 409.57 / 57.15 / 148.03 mm
−Y · 1 1/4 in (31.75 mm)
STOP20 · SCREW8-125
S20 → FGR
19.875 / 2.25 / 5.828 in 504.82 / 57.15 / 148.03 mm
−Y · 1 1/4 in (31.75 mm)
STOP21 · SCREW8-125
S21 → FGR
32.172 / 2.25 / 5.828 in 817.17 / 57.15 / 148.03 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 85–96
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
SIDEL0.375-01 · SCREW8-175
P03 → FA
0 / 0.375 / 3 in 0.00 / 9.52 / 76.20 mm
+X · 1 3/4 in (44.45 mm)
SIDEL0.375-02 · SCREW8-175
P03 → FA
0 / 0.375 / 12 in 0.00 / 9.52 / 304.80 mm
+X · 1 3/4 in (44.45 mm)
SIDEL0.375-03 · SCREW8-175
P03 → FA
0 / 0.375 / 21 in 0.00 / 9.52 / 533.40 mm
+X · 1 3/4 in (44.45 mm)
SIDEL0.375-04 · SCREW8-175
P03 → FA
0 / 0.375 / 30 in 0.00 / 9.52 / 762.00 mm
+X · 1 3/4 in (44.45 mm)
SIDEL0.375-05 · SCREW8-175
P03 → FA
0 / 0.375 / 39 in 0.00 / 9.52 / 990.60 mm
+X · 1 3/4 in (44.45 mm)
SIDEL0.375-06 · SCREW8-175
P03 → FA
0 / 0.375 / 45 in 0.00 / 9.52 / 1143.00 mm
+X · 1 3/4 in (44.45 mm)
SIDEL22.547-01 · SCREW8-175
P03 → CLV
0 / 22.547 / 3 in 0.00 / 572.69 / 76.20 mm
+X · 1 3/4 in (44.45 mm)
SIDEL22.547-02 · SCREW8-175
P03 → CLV
0 / 22.547 / 12 in 0.00 / 572.69 / 304.80 mm
+X · 1 3/4 in (44.45 mm)
SIDEL22.547-03 · SCREW8-175
P03 → CLV
0 / 22.547 / 21 in 0.00 / 572.69 / 533.40 mm
+X · 1 3/4 in (44.45 mm)
SIDEL22.547-04 · SCREW8-175
P03 → CLV
0 / 22.547 / 30 in 0.00 / 572.69 / 762.00 mm
+X · 1 3/4 in (44.45 mm)
SIDEL22.547-05 · SCREW8-175
P03 → CLV
0 / 22.547 / 39 in 0.00 / 572.69 / 990.60 mm
+X · 1 3/4 in (44.45 mm)
SIDEL22.547-06 · SCREW8-175
P03 → CLV
0 / 22.547 / 45 in 0.00 / 572.69 / 1143.00 mm
+X · 1 3/4 in (44.45 mm)
Fastener stations · 97–108
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
EDGEL1.4529999999999998-01 · SCREW8-175
P03 → CLB
0 / 5 / 1.453 in 0.00 / 127.00 / 36.91 mm
+X · 1 3/4 in (44.45 mm)
EDGEL1.4529999999999998-02 · SCREW8-175
P03 → CLB
0 / 11 / 1.453 in 0.00 / 279.40 / 36.91 mm
+X · 1 3/4 in (44.45 mm)
EDGEL1.4529999999999998-03 · SCREW8-175
P03 → CLB
0 / 17 / 1.453 in 0.00 / 431.80 / 36.91 mm
+X · 1 3/4 in (44.45 mm)
EDGEL1.4529999999999998-04 · SCREW8-175
P03 → CLB
0 / 20 / 1.453 in 0.00 / 508.00 / 36.91 mm
+X · 1 3/4 in (44.45 mm)
EDGEL46.547-01 · SCREW8-175
P03 → CLT
0 / 5 / 46.547 in 0.00 / 127.00 / 1182.29 mm
+X · 1 3/4 in (44.45 mm)
EDGEL46.547-02 · SCREW8-175
P03 → CLT
0 / 11 / 46.547 in 0.00 / 279.40 / 1182.29 mm
+X · 1 3/4 in (44.45 mm)
EDGEL46.547-03 · SCREW8-175
P03 → CLT
0 / 17 / 46.547 in 0.00 / 431.80 / 1182.29 mm
+X · 1 3/4 in (44.45 mm)
EDGEL46.547-04 · SCREW8-175
P03 → CLT
0 / 20 / 46.547 in 0.00 / 508.00 / 1182.29 mm
+X · 1 3/4 in (44.45 mm)
SIDER0.375-01 · SCREW8-175
P04 → FB
36 / 0.375 / 3 in 914.40 / 9.52 / 76.20 mm
−X · 1 3/4 in (44.45 mm)
SIDER0.375-02 · SCREW8-175
P04 → FB
36 / 0.375 / 12 in 914.40 / 9.52 / 304.80 mm
−X · 1 3/4 in (44.45 mm)
SIDER0.375-03 · SCREW8-175
P04 → FB
36 / 0.375 / 21 in 914.40 / 9.52 / 533.40 mm
−X · 1 3/4 in (44.45 mm)
SIDER0.375-04 · SCREW8-175
P04 → FB
36 / 0.375 / 30 in 914.40 / 9.52 / 762.00 mm
−X · 1 3/4 in (44.45 mm)
Fastener stations · 109–120
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
SIDER0.375-05 · SCREW8-175
P04 → FB
36 / 0.375 / 39 in 914.40 / 9.52 / 990.60 mm
−X · 1 3/4 in (44.45 mm)
SIDER0.375-06 · SCREW8-175
P04 → FB
36 / 0.375 / 45 in 914.40 / 9.52 / 1143.00 mm
−X · 1 3/4 in (44.45 mm)
SIDER22.547-01 · SCREW8-175
P04 → CRV
36 / 22.547 / 3 in 914.40 / 572.69 / 76.20 mm
−X · 1 3/4 in (44.45 mm)
SIDER22.547-02 · SCREW8-175
P04 → CRV
36 / 22.547 / 12 in 914.40 / 572.69 / 304.80 mm
−X · 1 3/4 in (44.45 mm)
SIDER22.547-03 · SCREW8-175
P04 → CRV
36 / 22.547 / 21 in 914.40 / 572.69 / 533.40 mm
−X · 1 3/4 in (44.45 mm)
SIDER22.547-04 · SCREW8-175
P04 → CRV
36 / 22.547 / 30 in 914.40 / 572.69 / 762.00 mm
−X · 1 3/4 in (44.45 mm)
SIDER22.547-05 · SCREW8-175
P04 → CRV
36 / 22.547 / 39 in 914.40 / 572.69 / 990.60 mm
−X · 1 3/4 in (44.45 mm)
SIDER22.547-06 · SCREW8-175
P04 → CRV
36 / 22.547 / 45 in 914.40 / 572.69 / 1143.00 mm
−X · 1 3/4 in (44.45 mm)
EDGER1.4529999999999998-01 · SCREW8-175
P04 → CRB
36 / 5 / 1.453 in 914.40 / 127.00 / 36.91 mm
−X · 1 3/4 in (44.45 mm)
EDGER1.4529999999999998-02 · SCREW8-175
P04 → CRB
36 / 11 / 1.453 in 914.40 / 279.40 / 36.91 mm
−X · 1 3/4 in (44.45 mm)
EDGER1.4529999999999998-03 · SCREW8-175
P04 → CRB
36 / 17 / 1.453 in 914.40 / 431.80 / 36.91 mm
−X · 1 3/4 in (44.45 mm)
EDGER1.4529999999999998-04 · SCREW8-175
P04 → CRB
36 / 20 / 1.453 in 914.40 / 508.00 / 36.91 mm
−X · 1 3/4 in (44.45 mm)
Fastener stations · 121–132
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
EDGER46.547-01 · SCREW8-175
P04 → CRT
36 / 5 / 46.547 in 914.40 / 127.00 / 1182.29 mm
−X · 1 3/4 in (44.45 mm)
EDGER46.547-02 · SCREW8-175
P04 → CRT
36 / 11 / 46.547 in 914.40 / 279.40 / 1182.29 mm
−X · 1 3/4 in (44.45 mm)
EDGER46.547-03 · SCREW8-175
P04 → CRT
36 / 17 / 46.547 in 914.40 / 431.80 / 1182.29 mm
−X · 1 3/4 in (44.45 mm)
EDGER46.547-04 · SCREW8-175
P04 → CRT
36 / 20 / 46.547 in 914.40 / 508.00 / 1182.29 mm
−X · 1 3/4 in (44.45 mm)
BACK1.1404999999999998-01 · SCREW8-175
P05 → CLV
1.1405 / 24 / 5 in 28.97 / 609.60 / 127.00 mm
−Y · 1 3/4 in (44.45 mm)
BACK1.1404999999999998-02 · SCREW8-175
P05 → CLV
1.1405 / 24 / 14 in 28.97 / 609.60 / 355.60 mm
−Y · 1 3/4 in (44.45 mm)
BACK1.1404999999999998-03 · SCREW8-175
P05 → CLV
1.1405 / 24 / 23 in 28.97 / 609.60 / 584.20 mm
−Y · 1 3/4 in (44.45 mm)
BACK1.1404999999999998-04 · SCREW8-175
P05 → CLV
1.1405 / 24 / 32 in 28.97 / 609.60 / 812.80 mm
−Y · 1 3/4 in (44.45 mm)
BACK1.1404999999999998-05 · SCREW8-175
P05 → CLV
1.1405 / 24 / 41 in 28.97 / 609.60 / 1041.40 mm
−Y · 1 3/4 in (44.45 mm)
BACK1.1404999999999998-06 · SCREW8-175
P05 → CLV
1.1405 / 24 / 46 in 28.97 / 609.60 / 1168.40 mm
−Y · 1 3/4 in (44.45 mm)
BACK34.8595-01 · SCREW8-175
P05 → CRV
34.8595 / 24 / 5 in 885.43 / 609.60 / 127.00 mm
−Y · 1 3/4 in (44.45 mm)
BACK34.8595-02 · SCREW8-175
P05 → CRV
34.8595 / 24 / 14 in 885.43 / 609.60 / 355.60 mm
−Y · 1 3/4 in (44.45 mm)
Fastener stations · 133–144
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
BACK34.8595-03 · SCREW8-175
P05 → CRV
34.8595 / 24 / 23 in 885.43 / 609.60 / 584.20 mm
−Y · 1 3/4 in (44.45 mm)
BACK34.8595-04 · SCREW8-175
P05 → CRV
34.8595 / 24 / 32 in 885.43 / 609.60 / 812.80 mm
−Y · 1 3/4 in (44.45 mm)
BACK34.8595-05 · SCREW8-175
P05 → CRV
34.8595 / 24 / 41 in 885.43 / 609.60 / 1041.40 mm
−Y · 1 3/4 in (44.45 mm)
BACK34.8595-06 · SCREW8-175
P05 → CRV
34.8595 / 24 / 46 in 885.43 / 609.60 / 1168.40 mm
−Y · 1 3/4 in (44.45 mm)
FLOOR1.1404999999999998-01 · SCREW8-175
P01 → CLB
1.1405 / 6.5 / 0 in 28.97 / 165.10 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOOR1.1404999999999998-02 · SCREW8-175
P01 → CLB
1.1405 / 13.5 / 0 in 28.97 / 342.90 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOOR1.1404999999999998-03 · SCREW8-175
P01 → CLB
1.1405 / 19 / 0 in 28.97 / 482.60 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
ROOF1.1404999999999998-01 · SCREW8-175
P02 → CLT
1.1405 / 6.5 / 48 in 28.97 / 165.10 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
ROOF1.1404999999999998-02 · SCREW8-175
P02 → CLT
1.1405 / 13.5 / 48 in 28.97 / 342.90 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
ROOF1.1404999999999998-03 · SCREW8-175
P02 → CLT
1.1405 / 19 / 48 in 28.97 / 482.60 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
FLOOR34.8595-01 · SCREW8-175
P01 → CRB
34.8595 / 6.5 / 0 in 885.43 / 165.10 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOOR34.8595-02 · SCREW8-175
P01 → CRB
34.8595 / 13.5 / 0 in 885.43 / 342.90 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
Fastener stations · 145–156
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
FLOOR34.8595-03 · SCREW8-175
P01 → CRB
34.8595 / 19 / 0 in 885.43 / 482.60 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
ROOF34.8595-01 · SCREW8-175
P02 → CRT
34.8595 / 6.5 / 48 in 885.43 / 165.10 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
ROOF34.8595-02 · SCREW8-175
P02 → CRT
34.8595 / 13.5 / 48 in 885.43 / 342.90 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
ROOF34.8595-03 · SCREW8-175
P02 → CRT
34.8595 / 19 / 48 in 885.43 / 482.60 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
FLOORFB2.0-01 · SCREW8-175
P01 → CFB
6 / 2 / 0 in 152.40 / 50.80 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOORFB2.0-02 · SCREW8-175
P01 → CFB
12 / 2 / 0 in 304.80 / 50.80 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOORFB2.0-03 · SCREW8-175
P01 → CFB
24 / 2 / 0 in 609.60 / 50.80 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOORFB2.0-04 · SCREW8-175
P01 → CFB
30 / 2 / 0 in 762.00 / 50.80 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOORFB22.847-01 · SCREW8-175
P01 → CBB
6 / 22.847 / 0 in 152.40 / 580.31 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOORFB22.847-02 · SCREW8-175
P01 → CBB
12 / 22.847 / 0 in 304.80 / 580.31 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOORFB22.847-03 · SCREW8-175
P01 → CBB
24 / 22.847 / 0 in 609.60 / 580.31 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
FLOORFB22.847-04 · SCREW8-175
P01 → CBB
30 / 22.847 / 0 in 762.00 / 580.31 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
Fastener stations · 157–168
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
ROOFHEAD-01 · SCREW8-175
P02 → FD
6 / 0.375 / 48 in 152.40 / 9.52 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
ROOFHEAD-02 · SCREW8-175
P02 → FD
12 / 0.375 / 48 in 304.80 / 9.52 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
ROOFHEAD-03 · SCREW8-175
P02 → FD
24 / 0.375 / 48 in 609.60 / 9.52 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
ROOFHEAD-04 · SCREW8-175
P02 → FD
30 / 0.375 / 48 in 762.00 / 9.52 / 1219.20 mm
−Z · 1 3/4 in (44.45 mm)
RIBBEAR-01 · SCREW8-250
RC → RF
18.3 / 2 / 47.297 in 464.82 / 50.80 / 1201.34 mm
−Z · 2 1/2 in (63.5 mm)
RIBBEAR-02 · SCREW8-250
RC → RB
18.3 / 22.797 / 47.297 in 464.82 / 579.04 / 1201.34 mm
−Z · 2 1/2 in (63.5 mm)
COLUMN-01 · SCREW8-250
FE + FF + CCa → CCb
18 / 0 / 8 in 457.20 / 0.00 / 203.20 mm
+Y · 2 1/2 in (63.5 mm)
COLUMN-02 · SCREW8-250
FE + FF + CCa → CCb
18 / 0 / 16 in 457.20 / 0.00 / 406.40 mm
+Y · 2 1/2 in (63.5 mm)
COLUMN-03 · SCREW8-250
FE + FF + CCa → CCb
18 / 0 / 24 in 457.20 / 0.00 / 609.60 mm
+Y · 2 1/2 in (63.5 mm)
COLUMN-04 · SCREW8-250
FE + FF + CCa → CCb
18 / 0 / 32 in 457.20 / 0.00 / 812.80 mm
+Y · 2 1/2 in (63.5 mm)
COLUMN-05 · SCREW8-250
FE + FF + CCa → CCb
18 / 0 / 40 in 457.20 / 0.00 / 1016.00 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC1.4529999999999998-01 · SCREW8-250
FC + FGL → CFB
5 / 0 / 1.453 in 127.00 / 0.00 / 36.91 mm
+Y · 2 1/2 in (63.5 mm)
Fastener stations · 169–180
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
FRONTREC1.4529999999999998-02 · SCREW8-250
FC + FGL → CFB
10 / 0 / 1.453 in 254.00 / 0.00 / 36.91 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC1.4529999999999998-03 · SCREW8-250
FC + FGL → CFB
15 / 0 / 1.453 in 381.00 / 0.00 / 36.91 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC1.4529999999999998-04 · SCREW8-250
FC + FGR → CFB
21 / 0 / 1.453 in 533.40 / 0.00 / 36.91 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC1.4529999999999998-05 · SCREW8-250
FC + FGR → CFB
26 / 0 / 1.453 in 660.40 / 0.00 / 36.91 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC1.4529999999999998-06 · SCREW8-250
FC + FGR → CFB
31 / 0 / 1.453 in 787.40 / 0.00 / 36.91 mm
+Y · 2 1/2 in (63.5 mm)
BACKREC1.4529999999999998-01 · SCREW8-175
P05 → CBB
5 / 24 / 1.453 in 127.00 / 609.60 / 36.91 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC1.4529999999999998-02 · SCREW8-175
P05 → CBB
10 / 24 / 1.453 in 254.00 / 609.60 / 36.91 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC1.4529999999999998-03 · SCREW8-175
P05 → CBB
15 / 24 / 1.453 in 381.00 / 609.60 / 36.91 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC1.4529999999999998-04 · SCREW8-175
P05 → CBB
21 / 24 / 1.453 in 533.40 / 609.60 / 36.91 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC1.4529999999999998-05 · SCREW8-175
P05 → CBB
26 / 24 / 1.453 in 660.40 / 609.60 / 36.91 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC1.4529999999999998-06 · SCREW8-175
P05 → CBB
31 / 24 / 1.453 in 787.40 / 609.60 / 36.91 mm
−Y · 1 3/4 in (44.45 mm)
FRONTREC45.047-01 · SCREW8-250
FD + FHL → RF
5 / 0 / 45.047 in 127.00 / 0.00 / 1144.19 mm
+Y · 2 1/2 in (63.5 mm)
Fastener stations · 181–192
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
FRONTREC45.047-02 · SCREW8-250
FD + FHL → RF
10 / 0 / 45.047 in 254.00 / 0.00 / 1144.19 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC45.047-03 · SCREW8-250
FD + FHL → RF
15 / 0 / 45.047 in 381.00 / 0.00 / 1144.19 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC45.047-04 · SCREW8-250
FD + FHR → RF
21 / 0 / 45.047 in 533.40 / 0.00 / 1144.19 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC45.047-05 · SCREW8-250
FD + FHR → RF
26 / 0 / 45.047 in 660.40 / 0.00 / 1144.19 mm
+Y · 2 1/2 in (63.5 mm)
FRONTREC45.047-06 · SCREW8-250
FD + FHR → RF
31 / 0 / 45.047 in 787.40 / 0.00 / 1144.19 mm
+Y · 2 1/2 in (63.5 mm)
BACKREC45.047-01 · SCREW8-175
P05 → RB
5 / 24 / 45.047 in 127.00 / 609.60 / 1144.19 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC45.047-02 · SCREW8-175
P05 → RB
10 / 24 / 45.047 in 254.00 / 609.60 / 1144.19 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC45.047-03 · SCREW8-175
P05 → RB
15 / 24 / 45.047 in 381.00 / 609.60 / 1144.19 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC45.047-04 · SCREW8-175
P05 → RB
21 / 24 / 45.047 in 533.40 / 609.60 / 1144.19 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC45.047-05 · SCREW8-175
P05 → RB
26 / 24 / 45.047 in 660.40 / 609.60 / 1144.19 mm
−Y · 1 3/4 in (44.45 mm)
BACKREC45.047-06 · SCREW8-175
P05 → RB
31 / 24 / 45.047 in 787.40 / 609.60 / 1144.19 mm
−Y · 1 3/4 in (44.45 mm)
RESTRAINTREC1 · SCREW8-250
RT + P05 → RB
6 / 24.75 / 45.213 in 152.40 / 628.65 / 1148.41 mm
−Y · 2 1/2 in (63.5 mm)
Fastener stations · 193–204
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
RESTRAINTREC2 · SCREW8-250
RT + P05 → RB
14 / 24.75 / 45.213 in 355.60 / 628.65 / 1148.41 mm
−Y · 2 1/2 in (63.5 mm)
RESTRAINTREC3 · SCREW8-250
RT + P05 → RB
22 / 24.75 / 45.213 in 558.80 / 628.65 / 1148.41 mm
−Y · 2 1/2 in (63.5 mm)
RESTRAINTREC4 · SCREW8-250
RT + P05 → RB
30 / 24.75 / 45.213 in 762.00 / 628.65 / 1148.41 mm
−Y · 2 1/2 in (63.5 mm)
HINGE11F1 · SCREW8-125
SP-H11-fixed + FA → FI
2.5455 / -0.205 / 9.358 in 64.66 / -5.21 / 237.69 mm
+Y · 1 1/4 in (31.75 mm)
HINGE11F2 · SCREW8-125
SP-H11-fixed + FA → FI
2.3255 / -0.205 / 10.328 in 59.07 / -5.21 / 262.33 mm
+Y · 1 1/4 in (31.75 mm)
HINGE11F3 · SCREW8-125
SP-H11-fixed + FA → FI
2.5455 / -0.205 / 11.298 in 64.66 / -5.21 / 286.97 mm
+Y · 1 1/4 in (31.75 mm)
HINGE11M1 · SCREW8-125
SP-H11-moving + D1A → D1G
3.9855 / -0.205 / 9.358 in 101.23 / -5.21 / 237.69 mm
+Y · 1 1/4 in (31.75 mm)
HINGE11M2 · SCREW8-125
SP-H11-moving + D1A → D1G
4.2055 / -0.205 / 10.328 in 106.82 / -5.21 / 262.33 mm
+Y · 1 1/4 in (31.75 mm)
HINGE11M3 · SCREW8-125
SP-H11-moving + D1A → D1G
3.9855 / -0.205 / 11.298 in 101.23 / -5.21 / 286.97 mm
+Y · 1 1/4 in (31.75 mm)
HINGE12F1 · SCREW8-125
SP-H12-fixed + FA → FI
2.5455 / -0.205 / 24.53 in 64.66 / -5.21 / 623.06 mm
+Y · 1 1/4 in (31.75 mm)
HINGE12F2 · SCREW8-125
SP-H12-fixed + FA → FI
2.3255 / -0.205 / 25.5 in 59.07 / -5.21 / 647.70 mm
+Y · 1 1/4 in (31.75 mm)
HINGE12F3 · SCREW8-125
SP-H12-fixed + FA → FI
2.5455 / -0.205 / 26.47 in 64.66 / -5.21 / 672.34 mm
+Y · 1 1/4 in (31.75 mm)
Fastener stations · 205–216
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
HINGE12M1 · SCREW8-125
SP-H12-moving + D1A → D1G
3.9855 / -0.205 / 24.53 in 101.23 / -5.21 / 623.06 mm
+Y · 1 1/4 in (31.75 mm)
HINGE12M2 · SCREW8-125
SP-H12-moving + D1A → D1G
4.2055 / -0.205 / 25.5 in 106.82 / -5.21 / 647.70 mm
+Y · 1 1/4 in (31.75 mm)
HINGE12M3 · SCREW8-125
SP-H12-moving + D1A → D1G
3.9855 / -0.205 / 26.47 in 101.23 / -5.21 / 672.34 mm
+Y · 1 1/4 in (31.75 mm)
HINGE13F1 · SCREW8-125
SP-H13-fixed + FA → FI
2.5455 / -0.205 / 39.702 in 64.66 / -5.21 / 1008.43 mm
+Y · 1 1/4 in (31.75 mm)
HINGE13F2 · SCREW8-125
SP-H13-fixed + FA → FI
2.3255 / -0.205 / 40.672 in 59.07 / -5.21 / 1033.07 mm
+Y · 1 1/4 in (31.75 mm)
HINGE13F3 · SCREW8-125
SP-H13-fixed + FA → FI
2.5455 / -0.205 / 41.642 in 64.66 / -5.21 / 1057.71 mm
+Y · 1 1/4 in (31.75 mm)
HINGE13M1 · SCREW8-125
SP-H13-moving + D1A → D1G
3.9855 / -0.205 / 39.702 in 101.23 / -5.21 / 1008.43 mm
+Y · 1 1/4 in (31.75 mm)
HINGE13M2 · SCREW8-125
SP-H13-moving + D1A → D1G
4.2055 / -0.205 / 40.672 in 106.82 / -5.21 / 1033.07 mm
+Y · 1 1/4 in (31.75 mm)
HINGE13M3 · SCREW8-125
SP-H13-moving + D1A → D1G
3.9855 / -0.205 / 41.642 in 101.23 / -5.21 / 1057.71 mm
+Y · 1 1/4 in (31.75 mm)
HINGE21M1 · SCREW8-125
SP-H21-moving + D2B → D2H
32.0145 / -0.205 / 9.358 in 813.17 / -5.21 / 237.69 mm
+Y · 1 1/4 in (31.75 mm)
HINGE21M2 · SCREW8-125
SP-H21-moving + D2B → D2H
31.7945 / -0.205 / 10.328 in 807.58 / -5.21 / 262.33 mm
+Y · 1 1/4 in (31.75 mm)
HINGE21M3 · SCREW8-125
SP-H21-moving + D2B → D2H
32.0145 / -0.205 / 11.298 in 813.17 / -5.21 / 286.97 mm
+Y · 1 1/4 in (31.75 mm)
Fastener stations · 217–228
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
HINGE21F1 · SCREW8-125
SP-H21-fixed + FB → FJ
33.4545 / -0.205 / 9.358 in 849.74 / -5.21 / 237.69 mm
+Y · 1 1/4 in (31.75 mm)
HINGE21F2 · SCREW8-125
SP-H21-fixed + FB → FJ
33.6745 / -0.205 / 10.328 in 855.33 / -5.21 / 262.33 mm
+Y · 1 1/4 in (31.75 mm)
HINGE21F3 · SCREW8-125
SP-H21-fixed + FB → FJ
33.4545 / -0.205 / 11.298 in 849.74 / -5.21 / 286.97 mm
+Y · 1 1/4 in (31.75 mm)
HINGE22M1 · SCREW8-125
SP-H22-moving + D2B → D2H
32.0145 / -0.205 / 24.53 in 813.17 / -5.21 / 623.06 mm
+Y · 1 1/4 in (31.75 mm)
HINGE22M2 · SCREW8-125
SP-H22-moving + D2B → D2H
31.7945 / -0.205 / 25.5 in 807.58 / -5.21 / 647.70 mm
+Y · 1 1/4 in (31.75 mm)
HINGE22M3 · SCREW8-125
SP-H22-moving + D2B → D2H
32.0145 / -0.205 / 26.47 in 813.17 / -5.21 / 672.34 mm
+Y · 1 1/4 in (31.75 mm)
HINGE22F1 · SCREW8-125
SP-H22-fixed + FB → FJ
33.4545 / -0.205 / 24.53 in 849.74 / -5.21 / 623.06 mm
+Y · 1 1/4 in (31.75 mm)
HINGE22F2 · SCREW8-125
SP-H22-fixed + FB → FJ
33.6745 / -0.205 / 25.5 in 855.33 / -5.21 / 647.70 mm
+Y · 1 1/4 in (31.75 mm)
HINGE22F3 · SCREW8-125
SP-H22-fixed + FB → FJ
33.4545 / -0.205 / 26.47 in 849.74 / -5.21 / 672.34 mm
+Y · 1 1/4 in (31.75 mm)
HINGE23M1 · SCREW8-125
SP-H23-moving + D2B → D2H
32.0145 / -0.205 / 39.702 in 813.17 / -5.21 / 1008.43 mm
+Y · 1 1/4 in (31.75 mm)
HINGE23M2 · SCREW8-125
SP-H23-moving + D2B → D2H
31.7945 / -0.205 / 40.672 in 807.58 / -5.21 / 1033.07 mm
+Y · 1 1/4 in (31.75 mm)
HINGE23M3 · SCREW8-125
SP-H23-moving + D2B → D2H
32.0145 / -0.205 / 41.642 in 813.17 / -5.21 / 1057.71 mm
+Y · 1 1/4 in (31.75 mm)
Fastener stations · 229–240
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
HINGE23F1 · SCREW8-125
SP-H23-fixed + FB → FJ
33.4545 / -0.205 / 39.702 in 849.74 / -5.21 / 1008.43 mm
+Y · 1 1/4 in (31.75 mm)
HINGE23F2 · SCREW8-125
SP-H23-fixed + FB → FJ
33.6745 / -0.205 / 40.672 in 855.33 / -5.21 / 1033.07 mm
+Y · 1 1/4 in (31.75 mm)
HINGE23F3 · SCREW8-125
SP-H23-fixed + FB → FJ
33.4545 / -0.205 / 41.642 in 849.74 / -5.21 / 1057.71 mm
+Y · 1 1/4 in (31.75 mm)
L-HP1 · HASP-SCREW
L-HP-base → D1B
16.27375 / -0.07 / 23 in 413.35 / -1.78 / 584.20 mm
+Y · 5/8 in (15.88 mm)
L-HP2 · HASP-SCREW
L-HP-base → D1B
15.90375 / -0.07 / 23.5 in 403.96 / -1.78 / 596.90 mm
+Y · 5/8 in (15.88 mm)
L-HP3 · HASP-SCREW
L-HP-base → D1B
15.80375 / -0.07 / 22.5 in 401.42 / -1.78 / 571.50 mm
+Y · 5/8 in (15.88 mm)
L-ST1 · HASP-SCREW
L-ST-base → FE
18.15375 / -0.07 / 22.44 in 461.11 / -1.78 / 569.98 mm
+Y · 5/8 in (15.88 mm)
L-ST2 · HASP-SCREW
L-ST-base → FE
17.03375 / -0.07 / 22.44 in 432.66 / -1.78 / 569.98 mm
+Y · 5/8 in (15.88 mm)
L-ST3 · HASP-SCREW
L-ST-base → FE
18.15375 / -0.07 / 23.56 in 461.11 / -1.78 / 598.42 mm
+Y · 5/8 in (15.88 mm)
L-ST4 · HASP-SCREW
L-ST-base → FE
17.03375 / -0.07 / 23.56 in 432.66 / -1.78 / 598.42 mm
+Y · 5/8 in (15.88 mm)
R-HP1 · HASP-SCREW
R-HP-base → D2A
19.72625 / -0.07 / 29 in 501.05 / -1.78 / 736.60 mm
+Y · 5/8 in (15.88 mm)
R-HP2 · HASP-SCREW
R-HP-base → D2A
20.09625 / -0.07 / 29.5 in 510.44 / -1.78 / 749.30 mm
+Y · 5/8 in (15.88 mm)
Fastener stations · 241–252
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
R-HP3 · HASP-SCREW
R-HP-base → D2A
20.19625 / -0.07 / 28.5 in 512.98 / -1.78 / 723.90 mm
+Y · 5/8 in (15.88 mm)
R-ST1 · HASP-SCREW
R-ST-base → FE
17.84625 / -0.07 / 28.44 in 453.29 / -1.78 / 722.38 mm
+Y · 5/8 in (15.88 mm)
R-ST2 · HASP-SCREW
R-ST-base → FE
18.96625 / -0.07 / 28.44 in 481.74 / -1.78 / 722.38 mm
+Y · 5/8 in (15.88 mm)
R-ST3 · HASP-SCREW
R-ST-base → FE
17.84625 / -0.07 / 29.56 in 453.29 / -1.78 / 750.82 mm
+Y · 5/8 in (15.88 mm)
R-ST4 · HASP-SCREW
R-ST-base → FE
18.96625 / -0.07 / 29.56 in 481.74 / -1.78 / 750.82 mm
+Y · 5/8 in (15.88 mm)
BR01 · BOLT
P02 + RB1L → interior washer + locknut + cover
3.5 / 4.5 / 48 in 88.90 / 114.30 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR02 · BOLT
P02 + RB1L → interior washer + locknut + cover
8.262 / 4.5 / 48 in 209.85 / 114.30 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR03 · BOLT
P02 + RB1L → interior washer + locknut + cover
12.049 / 4.5 / 48 in 306.04 / 114.30 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR04 · BOLT
P02 + RB1L → interior washer + locknut + cover
16.377 / 4.5 / 48 in 415.98 / 114.30 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR05 · BOLT
P02 + RB1R → interior washer + locknut + cover
19.623 / 4.5 / 48 in 498.42 / 114.30 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR06 · BOLT
P02 + RB1R → interior washer + locknut + cover
23.951 / 4.5 / 48 in 608.36 / 114.30 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR07 · BOLT
P02 + RB1R → interior washer + locknut + cover
27.738 / 4.5 / 48 in 704.55 / 114.30 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
Fastener stations · 253–264
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
BR08 · BOLT
P02 + RB1R → interior washer + locknut + cover
32.5 / 4.5 / 48 in 825.50 / 114.30 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR09 · BOLT
P02 + RB2L → interior washer + locknut + cover
3.5 / 17.5 / 48 in 88.90 / 444.50 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR10 · BOLT
P02 + RB2L → interior washer + locknut + cover
8.262 / 17.5 / 48 in 209.85 / 444.50 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR11 · BOLT
P02 + RB2L → interior washer + locknut + cover
12.049 / 17.5 / 48 in 306.04 / 444.50 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR12 · BOLT
P02 + RB2L → interior washer + locknut + cover
16.377 / 17.5 / 48 in 415.98 / 444.50 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR13 · BOLT
P02 + RB2R → interior washer + locknut + cover
19.623 / 17.5 / 48 in 498.42 / 444.50 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR14 · BOLT
P02 + RB2R → interior washer + locknut + cover
23.951 / 17.5 / 48 in 608.36 / 444.50 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR15 · BOLT
P02 + RB2R → interior washer + locknut + cover
27.738 / 17.5 / 48 in 704.55 / 444.50 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR16 · BOLT
P02 + RB2R → interior washer + locknut + cover
32.5 / 17.5 / 48 in 825.50 / 444.50 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR17 · BOLT
P02 + RB3 → interior washer + locknut + cover
3.5 / 7.231 / 48 in 88.90 / 183.67 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR18 · BOLT
P02 + RB3 → interior washer + locknut + cover
3.5 / 11.025 / 48 in 88.90 / 280.03 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR19 · BOLT
P02 + RB3 → interior washer + locknut + cover
3.5 / 14.277 / 48 in 88.90 / 362.64 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
Fastener stations · 265–276
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
BR20 · BOLT
P02 + RB4 → interior washer + locknut + cover
32.5 / 7.231 / 48 in 825.50 / 183.67 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR21 · BOLT
P02 + RB4 → interior washer + locknut + cover
32.5 / 11.025 / 48 in 825.50 / 280.03 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BR22 · BOLT
P02 + RB4 → interior washer + locknut + cover
32.5 / 14.277 / 48 in 825.50 / 362.64 / 1219.20 mm
−Z · 1 7/8 in (47.63 mm)
BVL01 · BOLT
P03 + VLB → interior washer + locknut + cover
0 / 4.5 / 6.875 in 0.00 / 114.30 / 174.62 mm
+X · 1 7/8 in (47.63 mm)
BVL02 · BOLT
P03 + VLB → interior washer + locknut + cover
0 / 11 / 6.875 in 0.00 / 279.40 / 174.62 mm
+X · 1 7/8 in (47.63 mm)
BVL03 · BOLT
P03 + VLB → interior washer + locknut + cover
0 / 17.5 / 6.875 in 0.00 / 444.50 / 174.62 mm
+X · 1 7/8 in (47.63 mm)
BVL04 · BOLT
P03 + VLT → interior washer + locknut + cover
0 / 4.5 / 10.125 in 0.00 / 114.30 / 257.18 mm
+X · 1 7/8 in (47.63 mm)
BVL05 · BOLT
P03 + VLT → interior washer + locknut + cover
0 / 11 / 10.125 in 0.00 / 279.40 / 257.18 mm
+X · 1 7/8 in (47.63 mm)
BVL06 · BOLT
P03 + VLT → interior washer + locknut + cover
0 / 17.5 / 10.125 in 0.00 / 444.50 / 257.18 mm
+X · 1 7/8 in (47.63 mm)
BVL07 · BOLT
P03 + VLF → interior washer + locknut + cover
0 / 4.5 / 8.5 in 0.00 / 114.30 / 215.90 mm
+X · 1 7/8 in (47.63 mm)
BVL08 · BOLT
P03 + VLR → interior washer + locknut + cover
0 / 17.5 / 8.5 in 0.00 / 444.50 / 215.90 mm
+X · 1 7/8 in (47.63 mm)
BVR01 · BOLT
P04 + VRB → interior washer + locknut + cover
36 / 4.5 / 6.875 in 914.40 / 114.30 / 174.62 mm
−X · 1 7/8 in (47.63 mm)
Fastener stations · 277–283
Use the assembly datums. First members receive clearance holes; receivers get stopped pilots. Screen screws enter outside at an 82° flush seat. Flat-head length includes the head. Received screws and full-stack trials govern.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
BVR02 · BOLT
P04 + VRB → interior washer + locknut + cover
36 / 11 / 6.875 in 914.40 / 279.40 / 174.62 mm
−X · 1 7/8 in (47.63 mm)
BVR03 · BOLT
P04 + VRB → interior washer + locknut + cover
36 / 17.5 / 6.875 in 914.40 / 444.50 / 174.62 mm
−X · 1 7/8 in (47.63 mm)
BVR04 · BOLT
P04 + VRT → interior washer + locknut + cover
36 / 4.5 / 10.125 in 914.40 / 114.30 / 257.18 mm
−X · 1 7/8 in (47.63 mm)
BVR05 · BOLT
P04 + VRT → interior washer + locknut + cover
36 / 11 / 10.125 in 914.40 / 279.40 / 257.18 mm
−X · 1 7/8 in (47.63 mm)
BVR06 · BOLT
P04 + VRT → interior washer + locknut + cover
36 / 17.5 / 10.125 in 914.40 / 444.50 / 257.18 mm
−X · 1 7/8 in (47.63 mm)
BVR07 · BOLT
P04 + VRF → interior washer + locknut + cover
36 / 4.5 / 8.5 in 914.40 / 114.30 / 215.90 mm
−X · 1 7/8 in (47.63 mm)
BVR08 · BOLT
P04 + VRR → interior washer + locknut + cover
36 / 17.5 / 8.5 in 914.40 / 444.50 / 215.90 mm
−X · 1 7/8 in (47.63 mm)
Machining removals
Local X / Y / Z begin at the named part’s minimum assembled-coordinate corner. Read its orientation drawing. These cut volumes are clipped to the wood; stopped bore, countersink, bevel and actual-recess checks remain additional operations.
Cut / part
Local X / Y / Z
Removal size X × Y × Z
P02-CUT1 / P02
4 in (101.6 mm) / 5 in (127 mm) / 0 in (0 mm)
13 1/4 in (336.55 mm) × 12 in (304.8 mm) × 0.703 in (17.86 mm)
P02-CUT2 / P02
18 3/4 in (476.25 mm) / 5 in (127 mm) / 0 in (0 mm)
13 1/4 in (336.55 mm) × 12 in (304.8 mm) × 0.703 in (17.86 mm)
P03-CUT1 / P03
0 in (0 mm) / 5 in (127 mm) / 6.797 in (172.64 mm)
0.703 in (17.86 mm) × 12 in (304.8 mm) × 2 in (50.8 mm)
P04-CUT1 / P04
0 in (0 mm) / 5 in (127 mm) / 6.797 in (172.64 mm)
0.703 in (17.86 mm) × 12 in (304.8 mm) × 2 in (50.8 mm)
RF-CUT1 / RF
0 in (0 mm) / 0 in (0 mm) / 0 in (0 mm)
31.594 in (802.49 mm) × 1/32 in (0.79 mm) × 1/4 in (6.35 mm)
RC-CUT1 / RC
0 in (0 mm) / 2.994 in (76.05 mm) / 1.24025 in (31.5 mm)
1 1/2 in (38.1 mm) × 13.012 in (330.5 mm) × 3/32 in (2.38 mm)
RB1L-CUT1 / RB1L
4.762 in (120.95 mm) / 0 in (0 mm) / 0.541 in (13.74 mm)
1 in (25.4 mm) × 1 in (25.4 mm) × 0.209 in (5.31 mm)
RB1L-CUT2 / RB1L
8.549 in (217.14 mm) / 0 in (0 mm) / 0.541 in (13.74 mm)
1 in (25.4 mm) × 1 in (25.4 mm) × 0.209 in (5.31 mm)
Machining removals · continued
Local X / Y / Z begin at the named part’s minimum assembled-coordinate corner. Read its orientation drawing. These cut volumes are clipped to the wood; stopped bore, countersink, bevel and actual-recess checks remain additional operations.
Cut / part
Local X / Y / Z
Removal size X × Y × Z
RB1L-CUT3 / RB1L
0.494 in (12.55 mm) / 0.494 in (12.55 mm) / 21/32 in (16.67 mm)
13.756 in (349.4 mm) × 0.506 in (12.85 mm) × 3/32 in (2.38 mm)
RB1R-CUT1 / RB1R
0 in (0 mm) / 0.494 in (12.55 mm) / 21/32 in (16.67 mm)
13.756 in (349.4 mm) × 0.506 in (12.85 mm) × 3/32 in (2.38 mm)
RB2L-CUT1 / RB2L
4.762 in (120.95 mm) / 0 in (0 mm) / 0.541 in (13.74 mm)
1 in (25.4 mm) × 1 in (25.4 mm) × 0.209 in (5.31 mm)
RB2L-CUT2 / RB2L
8.549 in (217.14 mm) / 0 in (0 mm) / 0.541 in (13.74 mm)
1 in (25.4 mm) × 1 in (25.4 mm) × 0.209 in (5.31 mm)
RB2L-CUT3 / RB2L
0.494 in (12.55 mm) / 0 in (0 mm) / 21/32 in (16.67 mm)
13.756 in (349.4 mm) × 0.506 in (12.85 mm) × 3/32 in (2.38 mm)
RB2R-CUT1 / RB2R
0 in (0 mm) / 0 in (0 mm) / 21/32 in (16.67 mm)
13.756 in (349.4 mm) × 0.506 in (12.85 mm) × 3/32 in (2.38 mm)
RB3-CUT1 / RB3
0.494 in (12.55 mm) / 0 in (0 mm) / 21/32 in (16.67 mm)
0.506 in (12.85 mm) × 12 in (304.8 mm) × 3/32 in (2.38 mm)
RB4-CUT1 / RB4
0 in (0 mm) / 0 in (0 mm) / 21/32 in (16.67 mm)
0.506 in (12.85 mm) × 12 in (304.8 mm) × 3/32 in (2.38 mm)
Machining removals · continued
Local X / Y / Z begin at the named part’s minimum assembled-coordinate corner. Read its orientation drawing. These cut volumes are clipped to the wood; stopped bore, countersink, bevel and actual-recess checks remain additional operations.
Cut / part
Local X / Y / Z
Removal size X × Y × Z
VLB-CUT1 / VLB
0 in (0 mm) / 0.494 in (12.55 mm) / 0.494 in (12.55 mm)
3/32 in (2.38 mm) × 13.012 in (330.5 mm) × 0.756 in (19.2 mm)
VLT-CUT1 / VLT
0 in (0 mm) / 0.494 in (12.55 mm) / 0 in (0 mm)
3/32 in (2.38 mm) × 13.012 in (330.5 mm) × 0.756 in (19.2 mm)
VLF-CUT1 / VLF
0 in (0 mm) / 0.494 in (12.55 mm) / 0 in (0 mm)
3/32 in (2.38 mm) × 0.506 in (12.85 mm) × 2 in (50.8 mm)
VLR-CUT1 / VLR
0 in (0 mm) / 0 in (0 mm) / 0 in (0 mm)
3/32 in (2.38 mm) × 0.506 in (12.85 mm) × 2 in (50.8 mm)
VRB-CUT1 / VRB
21/32 in (16.67 mm) / 0.494 in (12.55 mm) / 0.494 in (12.55 mm)
3/32 in (2.38 mm) × 13.012 in (330.5 mm) × 0.756 in (19.2 mm)
VRT-CUT1 / VRT
21/32 in (16.67 mm) / 0.494 in (12.55 mm) / 0 in (0 mm)
3/32 in (2.38 mm) × 13.012 in (330.5 mm) × 0.756 in (19.2 mm)
VRF-CUT1 / VRF
21/32 in (16.67 mm) / 0.494 in (12.55 mm) / 0 in (0 mm)
3/32 in (2.38 mm) × 0.506 in (12.85 mm) × 2 in (50.8 mm)
VRR-CUT1 / VRR
21/32 in (16.67 mm) / 0 in (0 mm) / 0 in (0 mm)
3/32 in (2.38 mm) × 0.506 in (12.85 mm) × 2 in (50.8 mm)
Machining removals · continued
Local X / Y / Z begin at the named part’s minimum assembled-coordinate corner. Read its orientation drawing. These cut volumes are clipped to the wood; stopped bore, countersink, bevel and actual-recess checks remain additional operations.
Cut / part
Local X / Y / Z
Removal size X × Y × Z
S10-CUT1 / S10
0 in (0 mm) / 0 in (0 mm) / 3/4 in (19.05 mm)
1 in (25.4 mm) × 1/32 in (0.79 mm) × 1/4 in (6.35 mm)
S11-CUT1 / S11
0 in (0 mm) / 0 in (0 mm) / 3/4 in (19.05 mm)
1 in (25.4 mm) × 1/32 in (0.79 mm) × 1/4 in (6.35 mm)
S20-CUT1 / S20
0 in (0 mm) / 0 in (0 mm) / 3/4 in (19.05 mm)
1 in (25.4 mm) × 1/32 in (0.79 mm) × 1/4 in (6.35 mm)
S21-CUT1 / S21
0 in (0 mm) / 0 in (0 mm) / 3/4 in (19.05 mm)
1 in (25.4 mm) × 1/32 in (0.79 mm) × 1/4 in (6.35 mm)
Inspection records
Receiving and physical acceptance record
Leave blank until measured or performed. A render, calculation or digital check does not fill these fields.
Required checkpoint
Actual result / date / reviewer
H01 · Received stock and full veneer system Measure real stock and total finished layer; maximum 0.046 in (1.17 mm). Obtain balance/bond/finish advice and trial a full-size laminated tall door. At least 1/16 in (1.59 mm) finished door gaps; extra balance layers require a revision.
___________________
___________________
___________________
H02 · Six hinges, pads and two hasps Receive 1798A21 hinges and N305-979 hasps; trial paired rigid pads, transferred holes, screw engagement and full bearing. Obtain custom mounting acceptance. Check independent release, swing and supported pin removal with roof fitted. No tall-door weight rating inferred.
___________________
___________________
___________________
Glue time: __________ · Last coating/repair: __________ Temperature / humidity: __________ · Full cure due: __________ Confirmed PSA dwell: __________ · Physical acceptance: __________
Receiving and physical acceptance record
Leave blank until measured or performed. A render, calculation or digital check does not fill these fields.
Required checkpoint
Actual result / date / reviewer
H03 · Screen capture, steel seats and 38 flush fixings Trial actual wire, 3/32 in (2.38 mm) relief, positive wood bearing, all clear cell axes, 82-degree plywood seats, inside tool access and cap depth. Revised steel pockets leave 0.541 in (13.74 mm) reference wood below; establish their suitability and actual stack before cutting. No clamp torque or load rating established.
___________________
___________________
___________________
H04 · Cured solid-pad glazing Measure actual acrylic and two solid neoprene faces; mill finished contact pocket for light contact and free expansion. Reference bare spacer 0.351 in (8.92 mm) includes .003 coating at each opposing contact surface. No forced compression, pane bow, drilled panes or water-seal claim.
___________________
___________________
___________________
Glue time: __________ · Last coating/repair: __________ Temperature / humidity: __________ · Full cure due: __________ Confirmed PSA dwell: __________ · Physical acceptance: __________
Receiving and physical acceptance record
Leave blank until measured or performed. A render, calculation or digital check does not fill these fields.
Required checkpoint
Actual result / date / reviewer
H05 · Coatings, bond and exposure Dry indoor non-immersed reference. Confirm veneer/preseal/topcoat/cleaner compatibility, supplier waits and full cure. No animal toxicology or water-holding approval.
___________________
___________________
___________________
H06 · Restraints, support, fixture and containment Two complete kits on external RT and verified site wall/support; no generic bracket layout or assembly tipping rating. Full base support, loaded stability, prototype roof loading and fixture thermal tests remain open. Right roof heat-free; actual animal-specific ventilation, gaps and cleaning need review.
___________________
___________________
___________________
Glue time: __________ · Last coating/repair: __________ Temperature / humidity: __________ · Full cure due: __________ Confirmed PSA dwell: __________ · Physical acceptance: __________
Sources, limits and maintenance
Product research and practical acceptance are separate. Current identity observations and exact document hashes are in the review packet.
Separate statuses: research, dimensions, calculations and digital validation have their own evidence. No prototype has been built. Physical testing and qualified review have not been performed. Publication does not replace these construction checks.
This is an indoor non-immersed wooden shell. Keep wet features in separate removable leakproof containers. Disconnect equipment, secure occupants elsewhere and empty the enclosure before service. Use the pictured removal sequence and repeat affected checks after repair.
Full veneer is included in the schedule and model, subject to supplier balance, bond and cured-stack acceptance. The maple, white-oak and walnut scans by Jenelle van Heerden via Poly Haven illustrate appearance; natural grain and colour vary by delivered sheet.