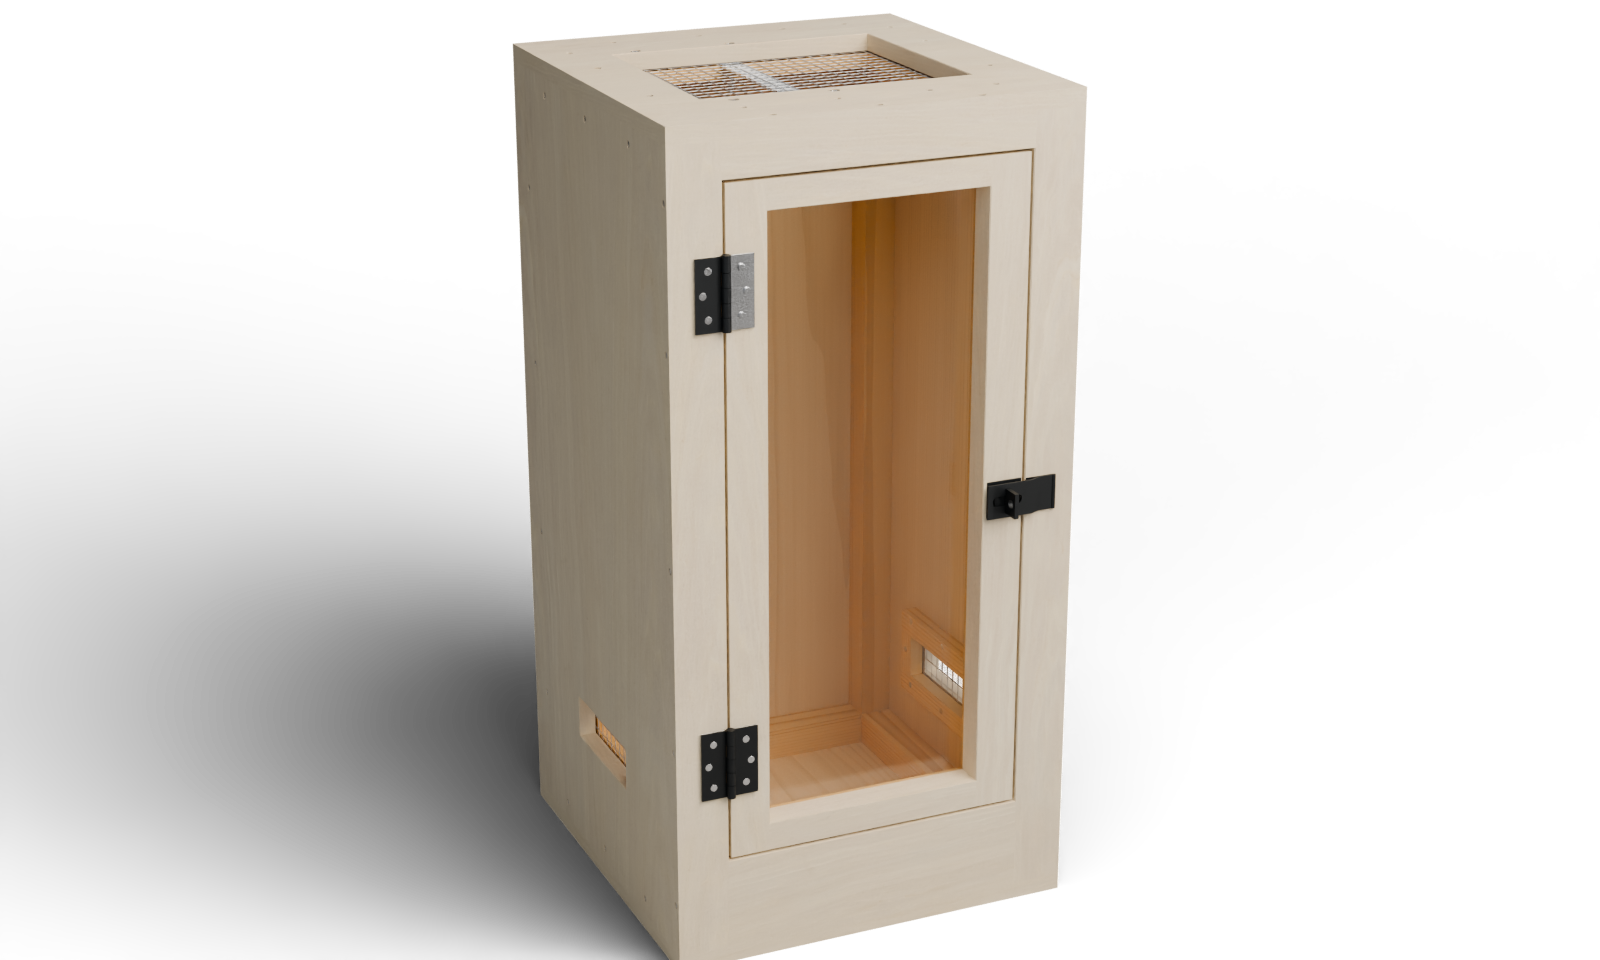
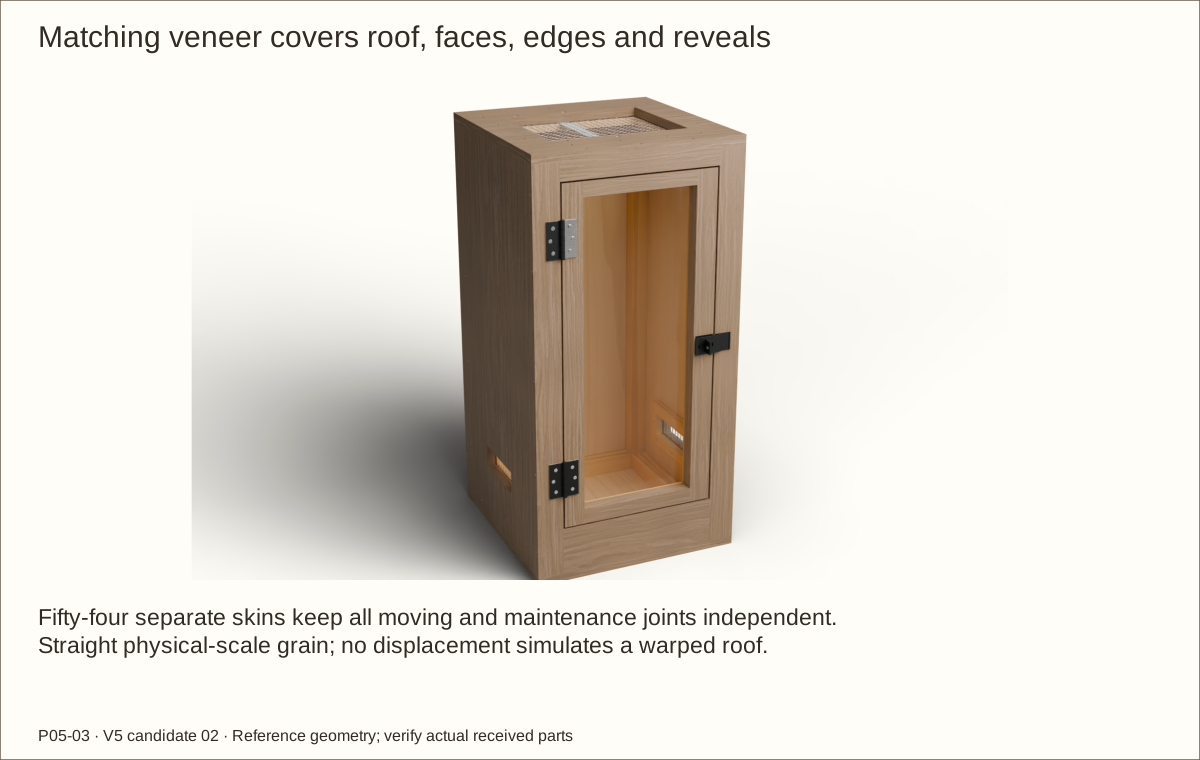
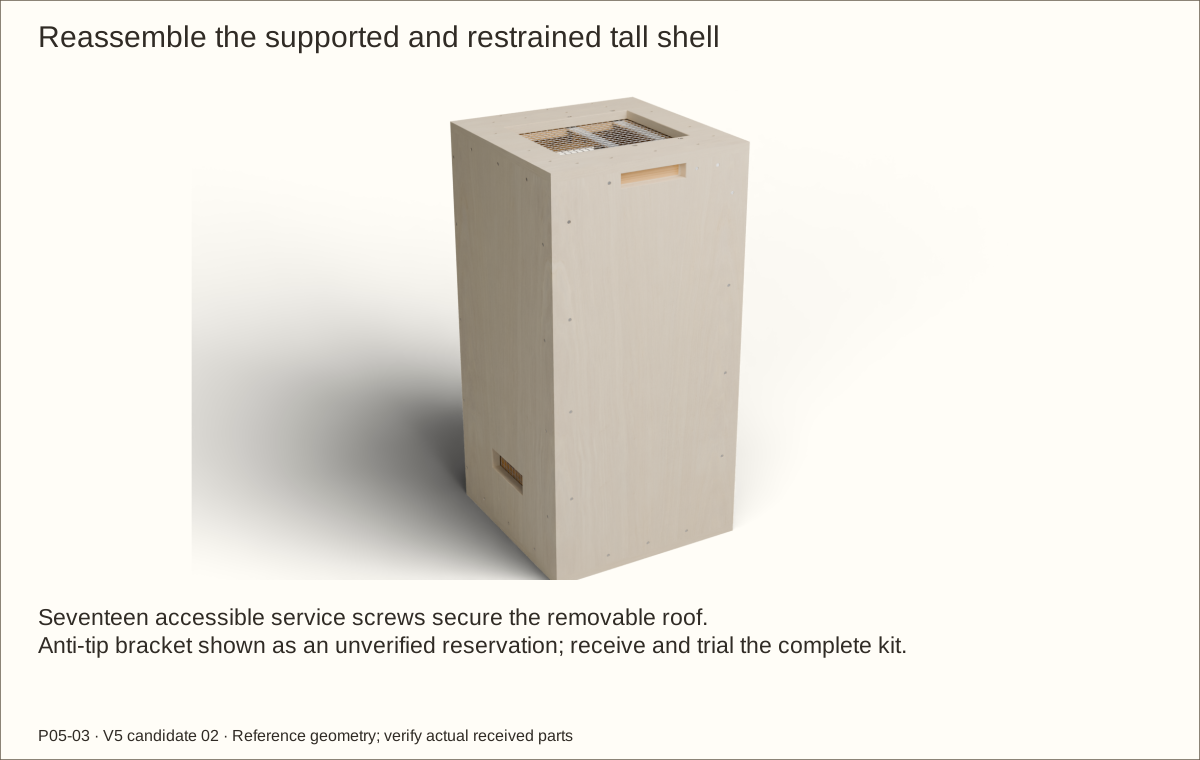
Full exterior veneer: the roof, faces, edges and reveals are included in this guide’s coordinated veneer schedule and geometry. Supplier balance, bond and actual-stack acceptance remain required. Natural grain and color vary.
About these previews
Rendered from this enclosure’s actual reference geometry. Veneer layers preserve service seams and bare hardware seats. The 3D viewer shows maple; these choices change the main picture. Texture scans by Jenelle van Heerden via Poly Haven, CC0 illustrate appearance and are not delivered veneer samples.
One hinged acrylic door with a swivel-staple hasp, a removable screened roof and low screened inlets. Follow 55 pictured operations with checks before continuing.
Before construction: supplier acceptance of the hinge spacers, received hardware and finish trials, prototype construction, physical testing and qualified review remain open. Publication approved; construction holds remain.
Receive and trial actual materials before dependent final cuts. This design retains P05-03’s single-door construction and its own hardware. Changed plywood, veneer, acrylic or hardware requires the corresponding fit checks.
Measurement
Reference
Bare exterior
18 × 18 × 36 in (457.2 × 457.2 × 914.4 mm)
Reference covered wooden body
18.061 in (458.75 mm) × 18.061 in (458.75 mm) × 36.061 in (915.95 mm)
Maximum covered wooden body
18.092 in (459.54 mm) × 18.092 in (459.54 mm) × 36.092 in (916.74 mm)
Door, bare wood
13.185 in (334.9 mm) × 28.685 in (728.6 mm)
Bare door gaps
Hinge/top/bottom 3/16 in (4.76 mm); latch 3/16 in (4.76 mm)
Minimum finished closed reveal
1/16 in (1.59 mm); receiving and animal-specific containment review required
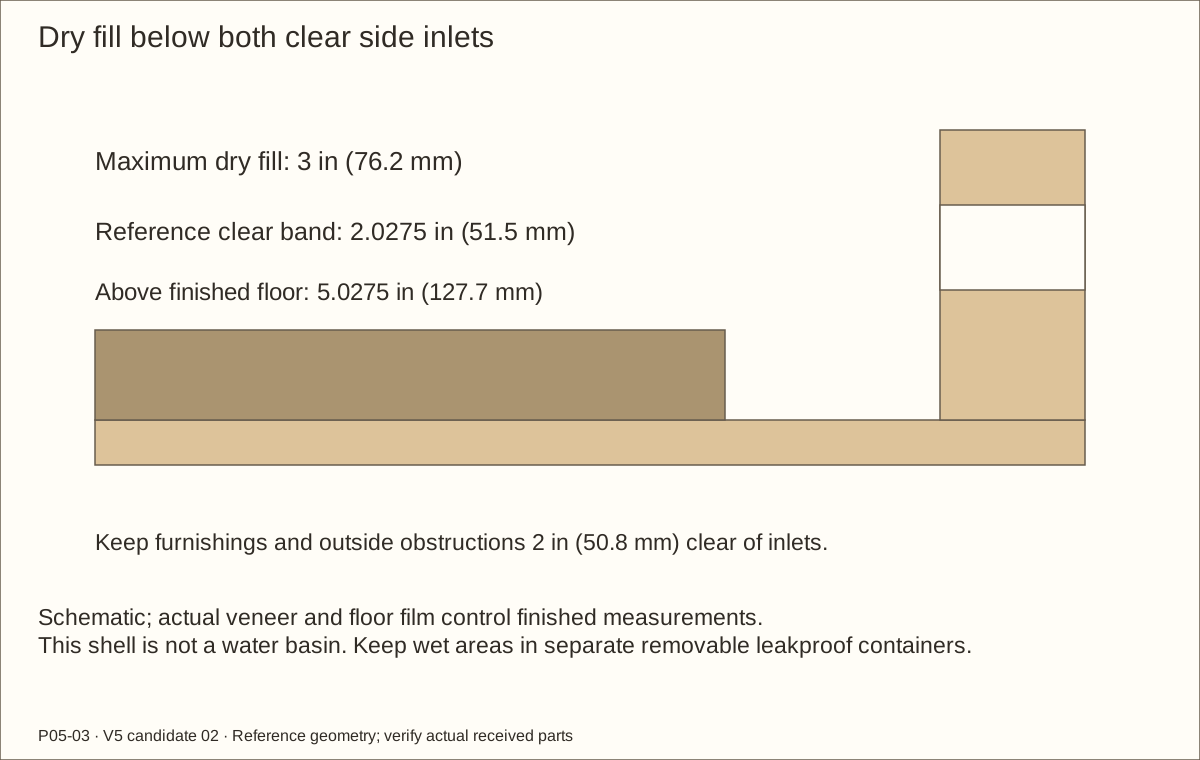
3 in (76.2 mm); reference 2.0275 in (51.5 mm) clear below finished inlets
Hinge service
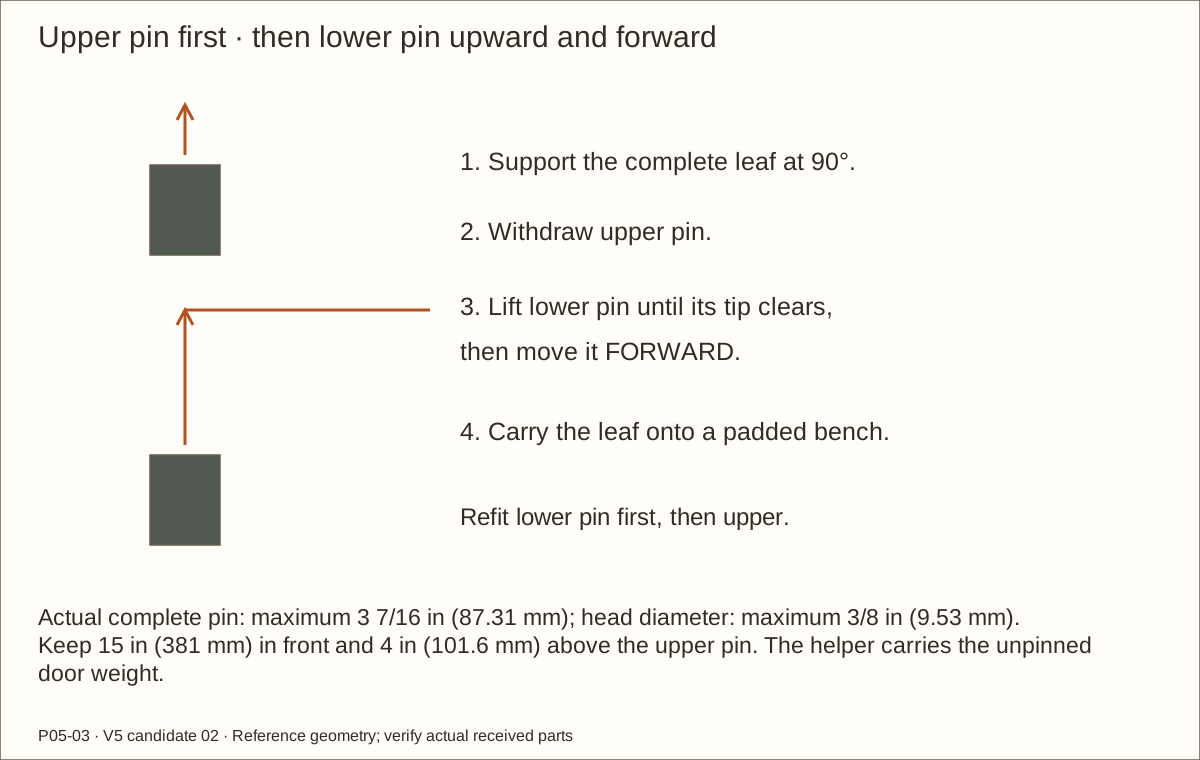
15 in (381 mm) clear in front and 4 in (101.6 mm) above upper pin
Veneer stack
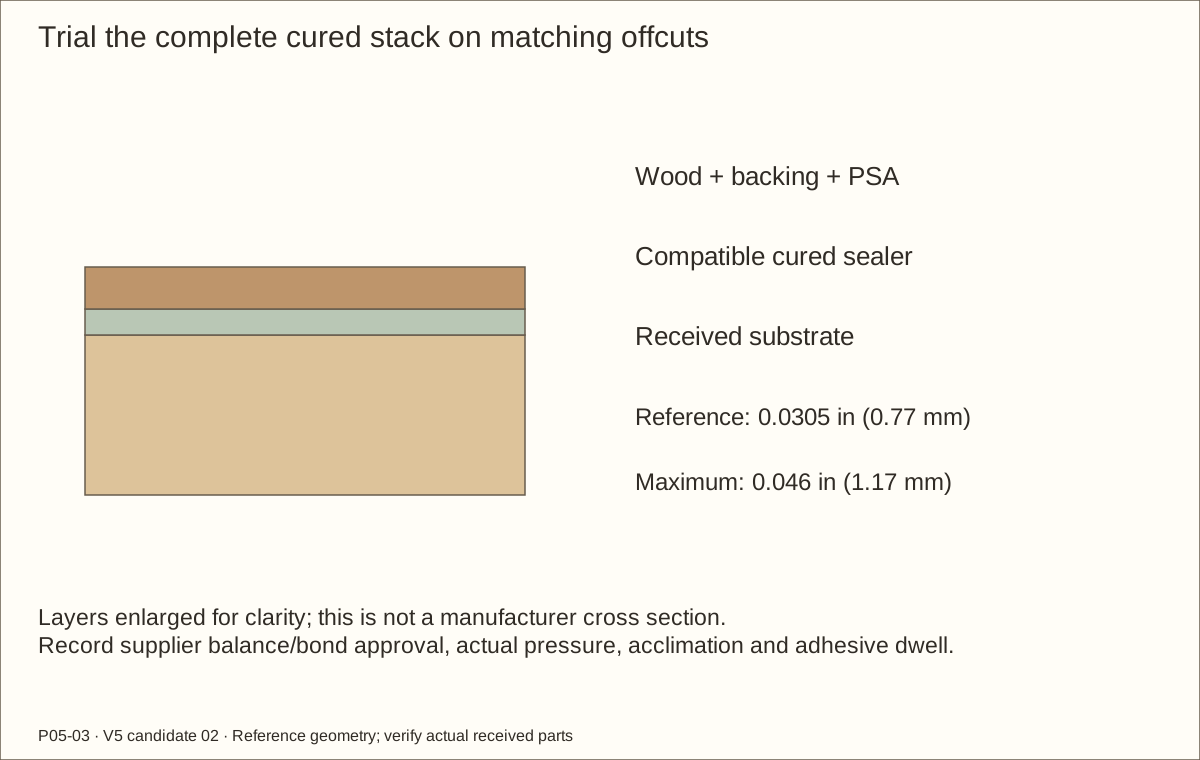
Reference 0.0305 in (0.77 mm); maximum 0.046 in (1.17 mm)
Measurement language: in means inches; mm means millimetres. Width × depth × height describes the outside body. Exact decimals are kept for mating parts. X starts at outside LEFT, Y at outside FRONT and Z at FLOOR UNDERSIDE unless a drawing names a local edge. Hardware projects beyond the wooden envelope.
Tools, terms and workholding
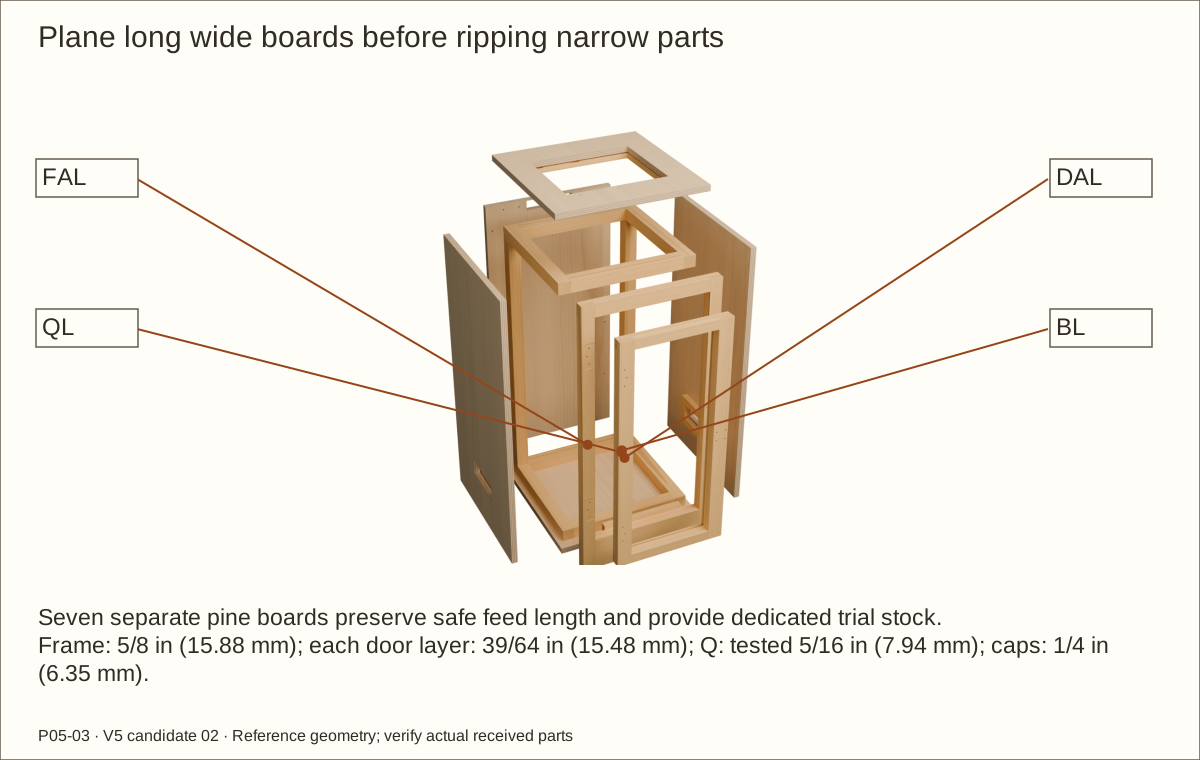
Use a flat supporting bench, helpers, clamps, straight cauls, tape, square, caliper, marking knife, measuring strips/dividers and stopped drill setups. Cutting needs supported saw and guided router/jigsaw arrangements, a chisel, block plane and sliding bevel. Plane wide stock before ripping narrow strips.
Prepare actual-root-matched wood pilots, clearance bits and matching countersink. Metal needs a vise, appropriate saw/bits, backing block and files. Mesh needs snips and edge protection. Acrylic needs a suitable sharp blade, full support and compatible edge finishing. Veneer needs a sharp knife, straightedge, cutting board and manufacturer-approved scraper.
Wear eye/hearing protection, control wood dust and ventilate finishes. Protect hands from cut mesh and metal; keep gloves, loose clothing and fingers away from rotating machinery. Clamp work and waste; never hold a short part under a drill.
Term
Plain meaning
Cleat / ledger
Wood strip receiving screws / strip supporting an upper panel
Stile / rail
Vertical / horizontal member of a frame
Lamination / caul
Layers glued together / straight board spreading clamp pressure
Pilot / clearance hole
Thread-guiding hole in receiver / free passage through first member
Countersink / arris
Conical flat-head seat / meeting edge of two faces
Named measuring surface / width removed by a saw cut
PSA / RH / BOM
Pressure-sensitive adhesive / relative humidity / bill of materials
Actual-stock fitting worksheet
Reference plywood t is 0.72 in (18.29 mm). Measure uniform stock and save real gauges. Exact reference decimals are not instructions to round a mating cut. Mixed thickness or changed fit needs a coordinated revision.
Part / fit
Rule or reference
Actual / checked
Floor / roof
18 × 18 in (457.2 × 457.2 mm)
________
Side height / back height
36 in (914.4 mm) minus twice t
________
Back / fixed-frame width
18 in (457.2 mm) minus twice t
________
Side horizontal cleats
18 in minus t minus 1 1/4 in; reference 16.03 in (407.16 mm)
________
Rear upright cleats
Side height minus 3 in (76.2 mm); reference 31.56 in (801.62 mm)
________
Cross cleats
Back width minus 3 in (76.2 mm); reference 13.56 in (344.42 mm)
________
Fixed frame / door layers
5/8 in (15.88 mm) / 39/64 in (15.48 mm) each
________
Door perimeter
Actual opening minus 3/8 in (9.53 mm) in both width and height
________
Glazing / screens / restraint
Actual cured coupon, cloth crossings/cells and complete kit control
________
Transfer clamped receiver centre lines. Reference stations do not automatically move with different stock. Recheck all opening datums, hasp support, glazing, veneer gaps and hardware paths before dependent cuts or drilling; record revised marks and measurements.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Do not stack, overhang the support or leave the tall shell unsupported. This is an unbuilt reference candidate.
Plan support, restraint and service space
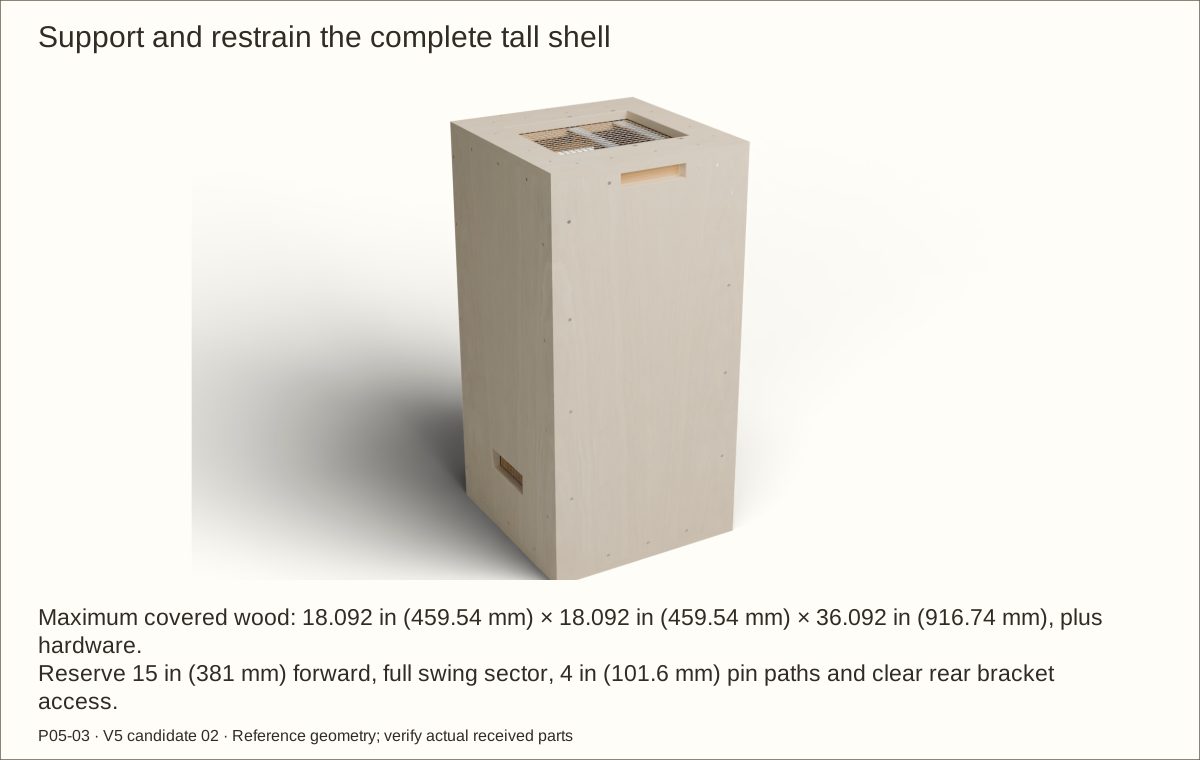
Plan continuous, rigid, level support for the whole base. The bare case is 18 in (457.2 mm) wide × 18 in (457.2 mm) deep × 36 in (914.4 mm) high; the maximum veneered wood envelope is 18.092 in (459.54 mm) × 18.092 in (459.54 mm) × 36.092 in (916.74 mm), plus projecting hardware.
Reserve 15 in (381 mm) in front, the complete door swing sector, 4 in (101.6 mm) above each pin and clear roof lifting space. Plan the rear cable route and direct access to both restraint-bracket screws.
Record completed shell, contents and equipment weights. Have the supporting furniture, floor, stability and complete anti-tip load path checked for that actual load. Plan helpers and a clear transport route.
Check before continuing: Full-base support, working space and the wall connection have a documented plan.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: A product listing or rendered finish is not acceptance of the assembled enclosure.
Resolve the eight receiving holds
Match exact product models and pack quantities. Resolve H01–H08 before their dependent cuts: hinges, hasp, veneer, glazing, screens/bolts, coating, support/equipment and the tall-shell restraint.
Choose ONE maple, white-oak or walnut veneer system. Ask its supplier to confirm the backing, pressure-sensitive adhesive (PSA), substrate/sealer, balancing, application pressure, acclimation and dwell for this indoor use.
Record actual products and answers. The complete cured veneer stack is reference 0.0305 in (0.77 mm), maximum 0.046 in (1.17 mm). Added balancing layers or substitutions require coordinated changes to the affected cuts, gaps and hardware.
Check before continuing: Required supplier and qualified-review answers are recorded before dependent work.
Parts: Plywood, pine, acrylic, EPDM, cloth, steel and hardware
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Nominal lumber names are not finished dimensions.
Measure stock and save physical gauges
Measure the plywood at corners and centre; the reference is 0.72 in (18.29 mm). Save labeled offcuts as thickness gauges. Inspect all boards for twist, bow, split ends or voids at bearing and screw locations.
Measure actual acrylic, both plain EPDM layers, cloth crossings, metal and hardware. Keep unknown package screws separate; use the scheduled lengths after root and head-seat trials.
Record actual values in the fitting worksheet. Exact decimals describe the reference geometry; use actual clamped receivers and gauges for mating lengths, without rounding a tight cut to a nearby tape fraction.
Check before continuing: Products, condition and measured thicknesses are recorded.
Parts: Actual screws and matched wood/metal offcuts
Tools / setup: Drill, caliper, actual bits/countersink, stop, clamps and backing board
Before you begin: Clamp small work; never hold it by hand under a drill.
Prove screw pilots and head seats
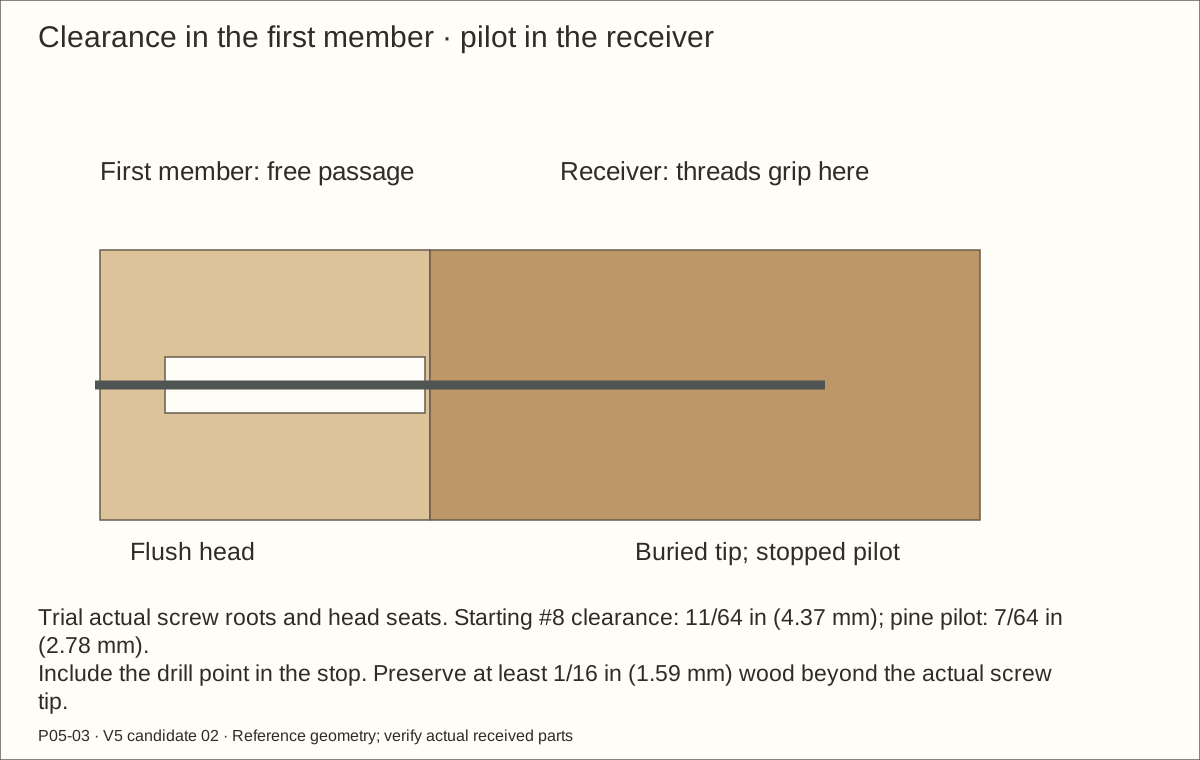
Clamp an actual stack over a backing board. A clearance hole passes the first part freely; a smaller pilot guides threads into the receiver. Begin #8 trials with 11/64 in (4.37 mm) clearance and a 7/64 in (2.78 mm) pine pilot, then match the received screw root.
Test the actual countersink angle and stop with a flush head. For #10 hasp screws, reference clearance is 13/64 in (5.16 mm) and pilot 1/8 in (3.18 mm); #4 cap screws use 1/8 in (3.18 mm) clearance and a root-matched pilot. Do not alter purchased metal countersinks.
Mark the intended tip and set a physical drill stop including the bit point. Preserve at least 1/16 in (1.59 mm) solid cover beyond each actual tip and the greater cover specified for hardware. Inspect both sides after a trial drive.
Check before continuing: No splitting, stripping, exposed points, crushed wood or proud heads.
Parts: 1798A21 pair; four SP spacers; full-height offcuts
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Custom spacer mounting and hinge capacity remain H01 until accepted.
Trial the complete hinge mounting
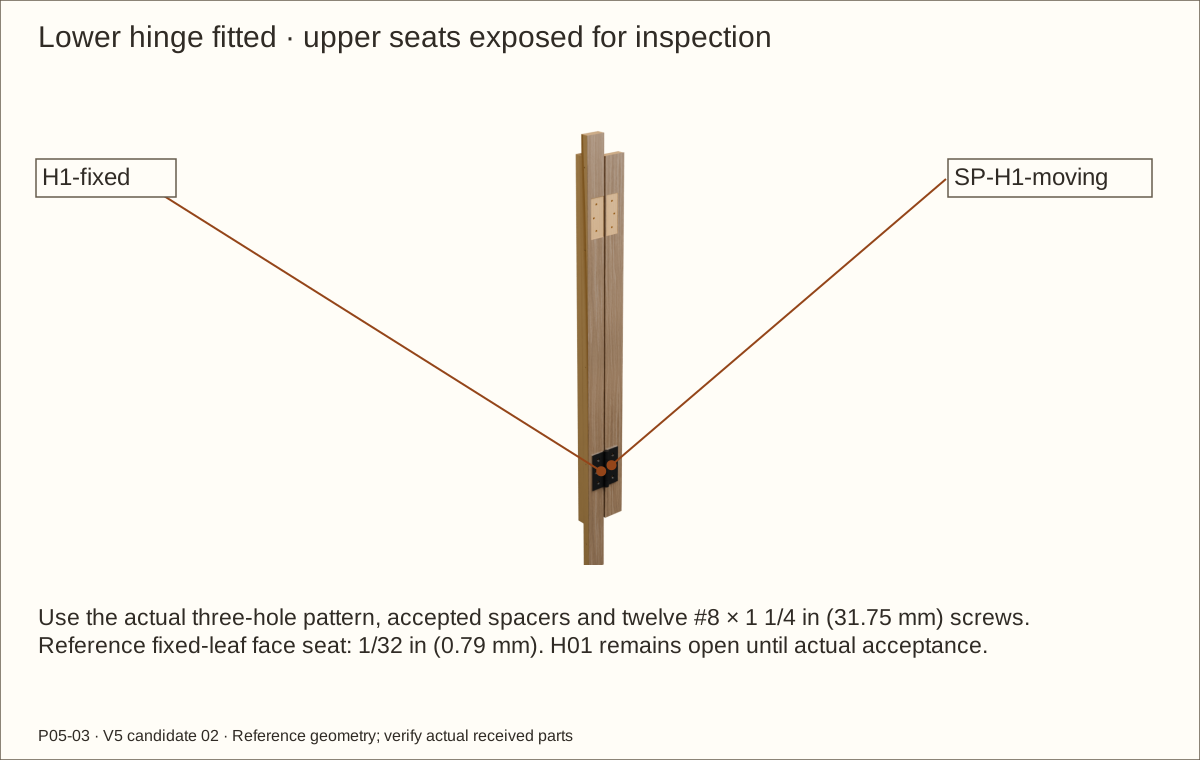
On the dedicated matching offcuts reproduce the 3/16 in (4.76 mm) bare hinge gap, 1/32 in (0.79 mm) door setback and hinge centres 20 in (508 mm) apart. Trace the fixed leaves and make flat 1/32 in (0.79 mm) face seats only under those fixed leaves.
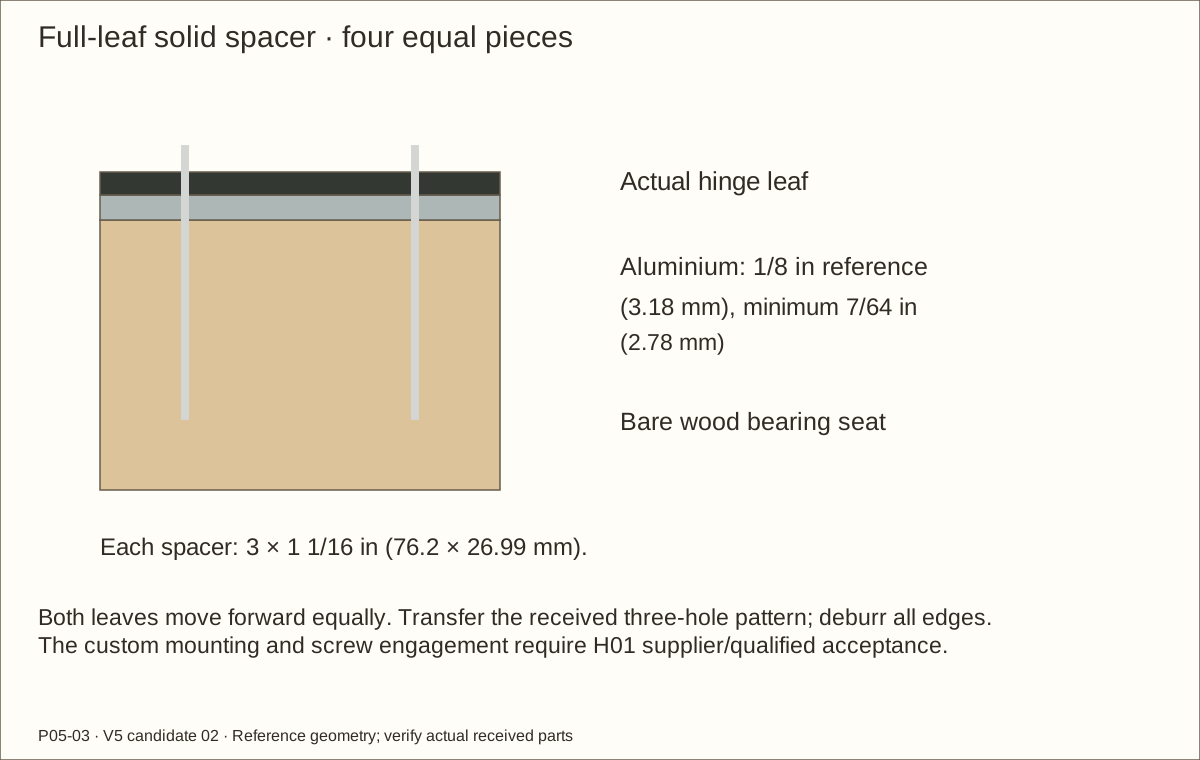
Trial equal full-leaf aluminium spacers under BOTH leaves: reference 1/8 in (3.18 mm), minimum 7/64 in (2.78 mm). Each is 3 in (76.2 mm) × 1 1/16 in (26.99 mm). Transfer the received three-hole patterns; require flat full bearing and supplier or qualified acceptance of this mounting.
Use twelve scheduled #8 × 1 1/4 in (31.75 mm) screws after the head/root trial. The reference wood engagement is 1.045 in (26.54 mm) and rear cover 0.17375 in (4.41 mm). Set the actual stopped pilots from the real stack, including the point; do not reuse old one-inch screws.
Check before continuing: Both leaves are coplanar, pin axes straight, heads flush and tips buried.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Prove coated swing and pin removal
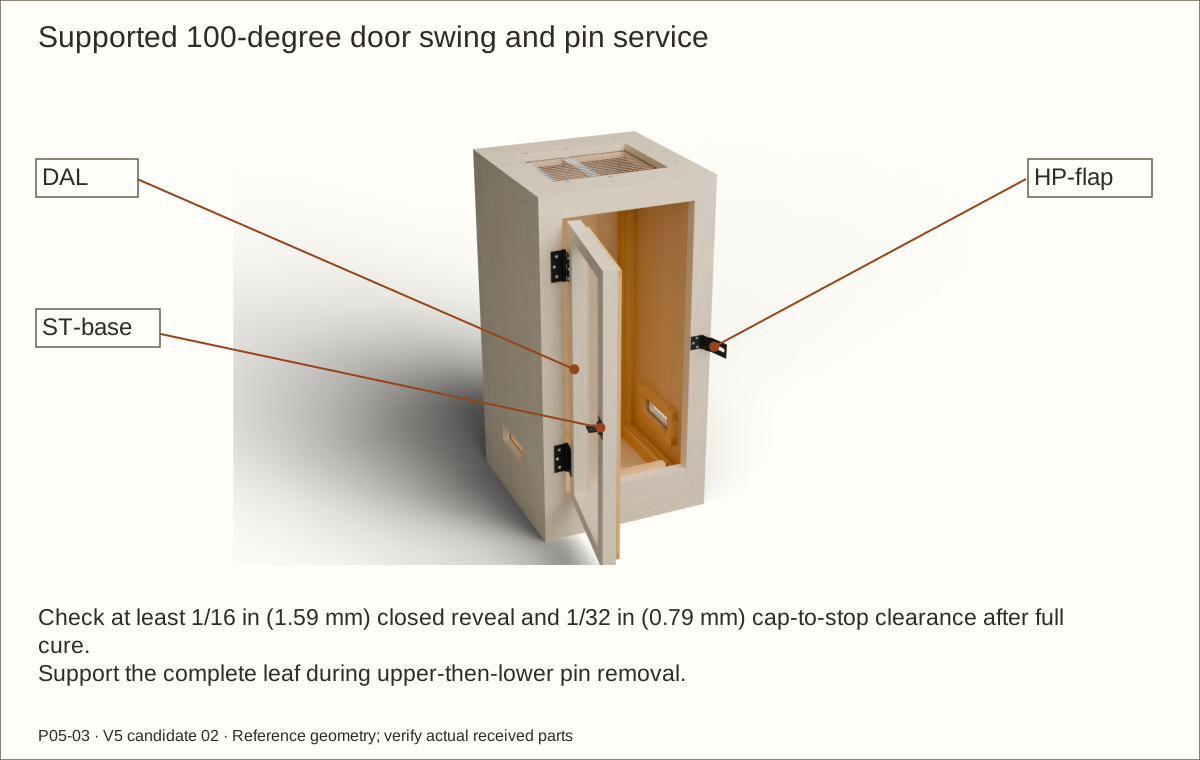
Finish the trial wood and veneer using the accepted system, fully cure, then refit. Require at least 1/16 in (1.59 mm) closed reveal and free movement through 100° without leaf, head, barrel or wood contact.
With a helper supporting the leaf at about 90°, withdraw the upper pin first. Withdraw the lower pin until its tip clears, then move it forward. Reserve 4 in (101.6 mm) along each extraction path; actual pin length must be no more than 3 7/16 in (87.31 mm) and head no more than 3/8 in (9.53 mm).
Refit lower pin then upper, without hammering misaligned knuckles. Correct identities, rocking seats and alignment before final work. Keep the accepted sample and measured settings.
Check before continuing: The roof-on removal path, complete swing and reinstallation are proved on actual hardware.
Required wait: Full coating cure and the supplier-confirmed veneer dwell before this fitted trial.
Parts: N305-979; seven #10 × 5/8 in (15.88 mm) screws
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: The approximate digital formed flap is not manufacturer CAD; actual release remains H02.
Trial the keyless hasp on matching stiles
Reproduce the fixed stile, retained door latch edge, 3/16 in (4.76 mm) bare gap and 1/32 in (0.79 mm) setback. The narrow hinged base goes on FAR; the square swivel plate goes on DAR. Only the fixed base receives a traced 1/32 in (0.79 mm) face seat.
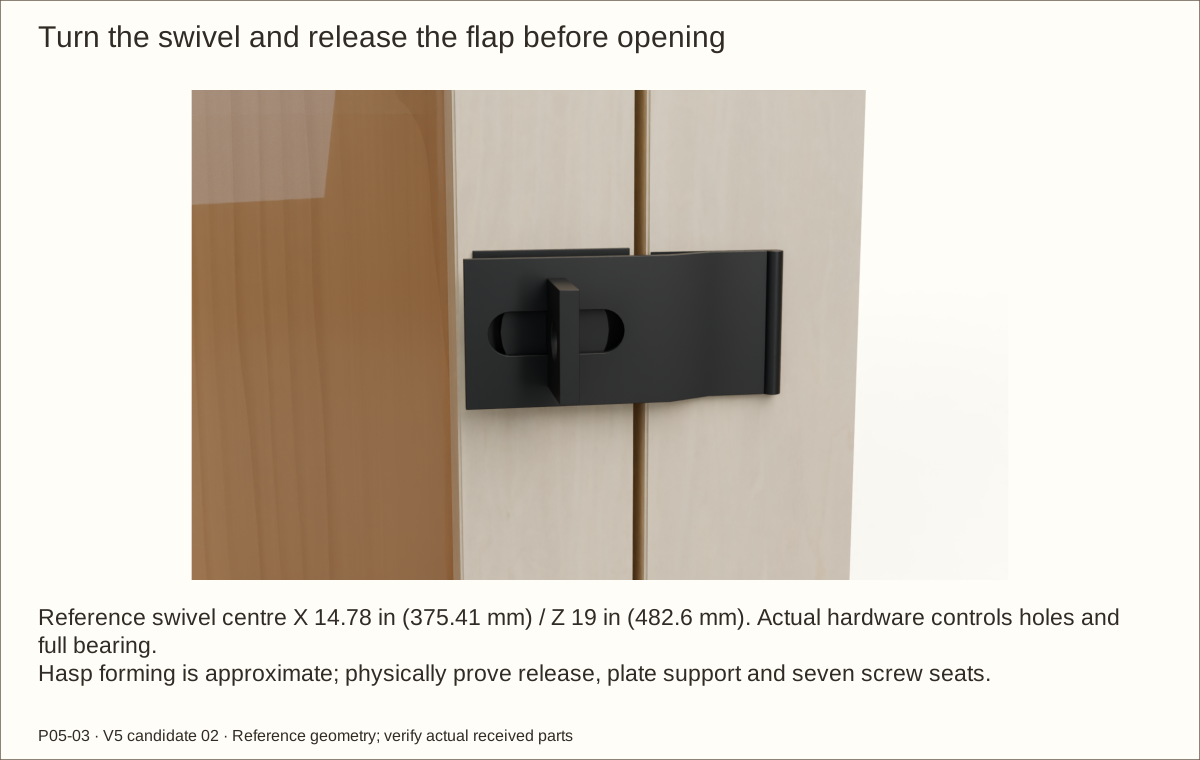
Fit the received plates with their entire backs on solid wood. The reference moving-plate outer margin is only 0.0175 in (0.44 mm); require actual full bearing and hole centres at least 1/4 in (6.35 mm) from wood edges and other shafts. Do not drill from the picture.
Trial all seven separate #10 × 5/8 in (15.88 mm) screws and stopped pilots, retaining at least 1/2 in (12.7 mm) rear cover. Turn the swivel to align with the slot, release the flap fully, open, then close and turn across the slot by hand. Repeat after full cure.
Check before continuing: Both plates bear fully and the actual hasp releases without pulling the leaf sideways.
8. Trial the complete anti-tip kit and access window
Parts: Hillman 9976524 complete kit; plywood and square-pine offcuts
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Bracket dimensions and holes are not published in the current evidence. Do not invent them or enlarge the window to force a fit.
Trial the complete anti-tip kit and access window
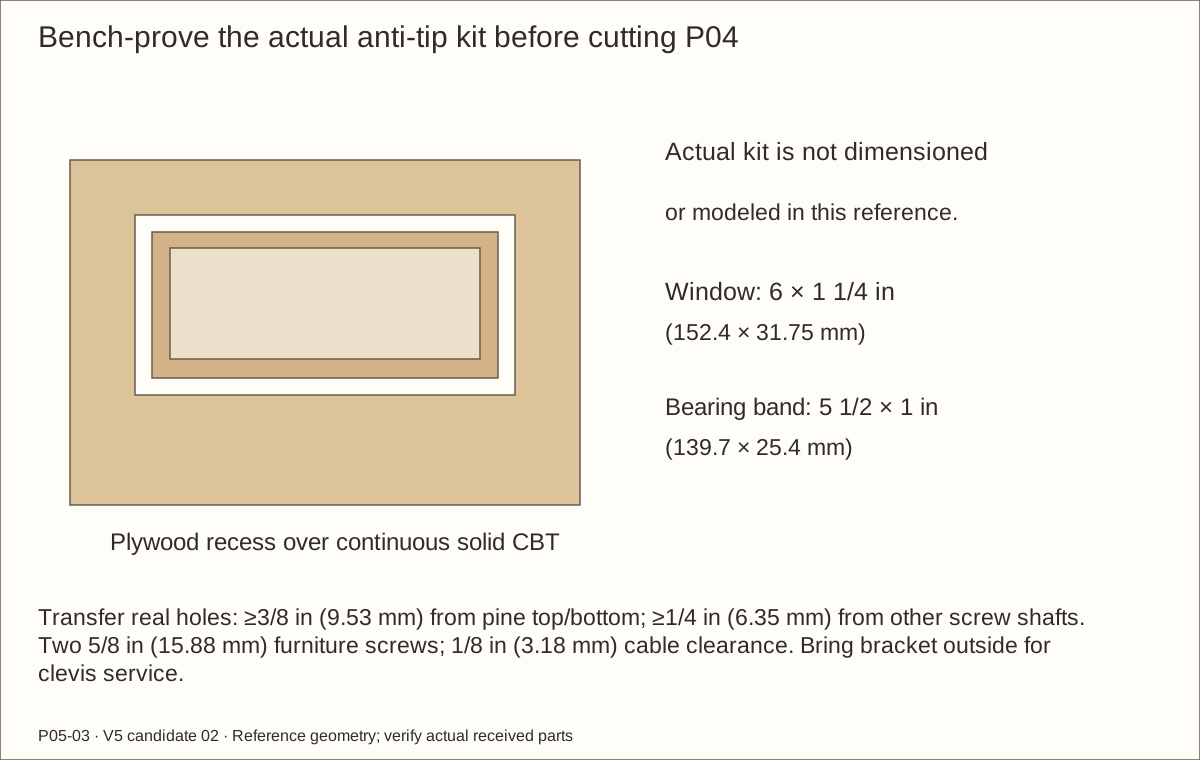
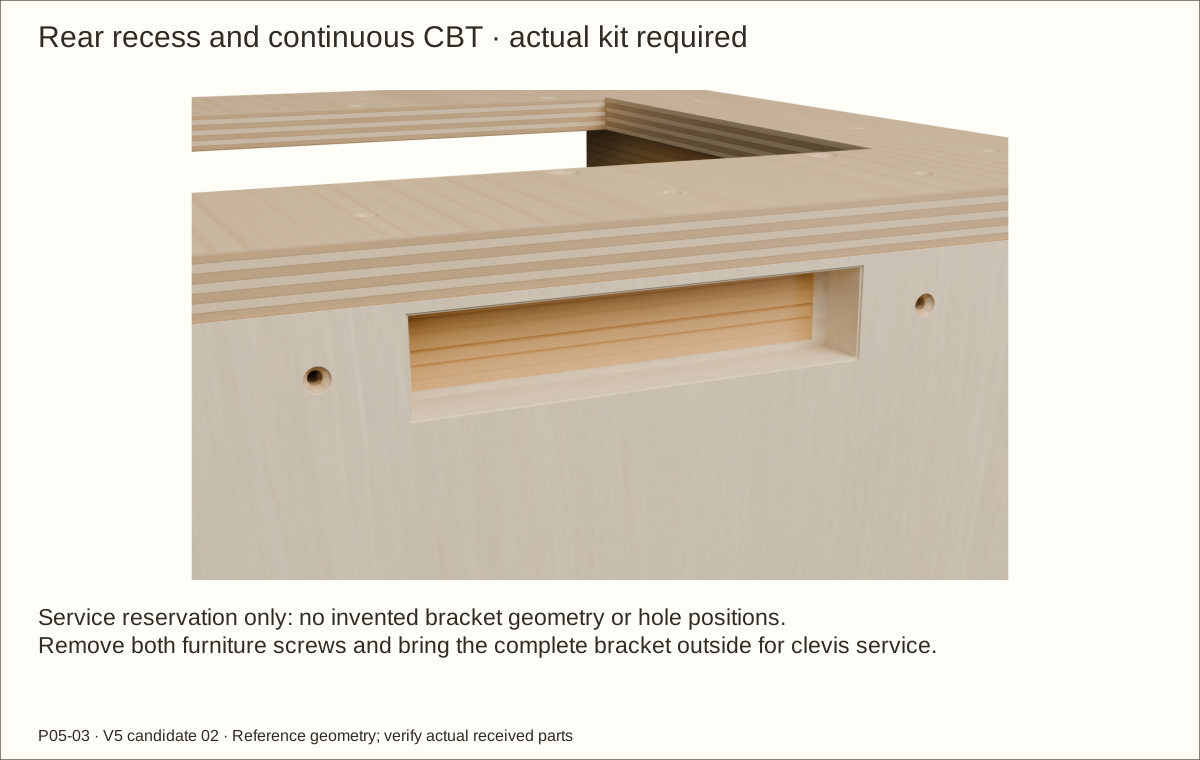
Bench-assemble the furniture bracket, cable eye, clevis and cotter. Make a 6 in (152.4 mm) × 1 1/4 in (31.75 mm) plywood window over continuous 1 1/2 in (38.1 mm) square pine; include the accepted veneer on the window reveals.
Orient the actual bracket horizontally with its entire base inside a centred 5 1/2 in (139.7 mm) × 1 in (25.4 mm) band. Keep its screw centres at least 3/8 in (9.53 mm) from the pine top/bottom. Transfer the real holes; trial the two supplied 5/8 in (15.88 mm) furniture screws with root-matched pilots stopped at 5/8 in (15.88 mm) maximum including the point.
Require full direct wood bearing, at least 7/8 in (22.23 mm) rear wood, straight driver access to both heads and 1/8 in (3.18 mm) cable clearance. Prove the complete bracket can enter and leave the recess. For clevis service, remove the two accessible furniture screws and bring the bracket outside.
Check before continuing: The actual kit, tools and removal fit pass before P04 is cut.
Parts: Door offcut, actual pane, two EPDM layers, Q spacer and B cap
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Do not resolve a failed cushion fit by tightening harder.
Make the cured glazing test piece
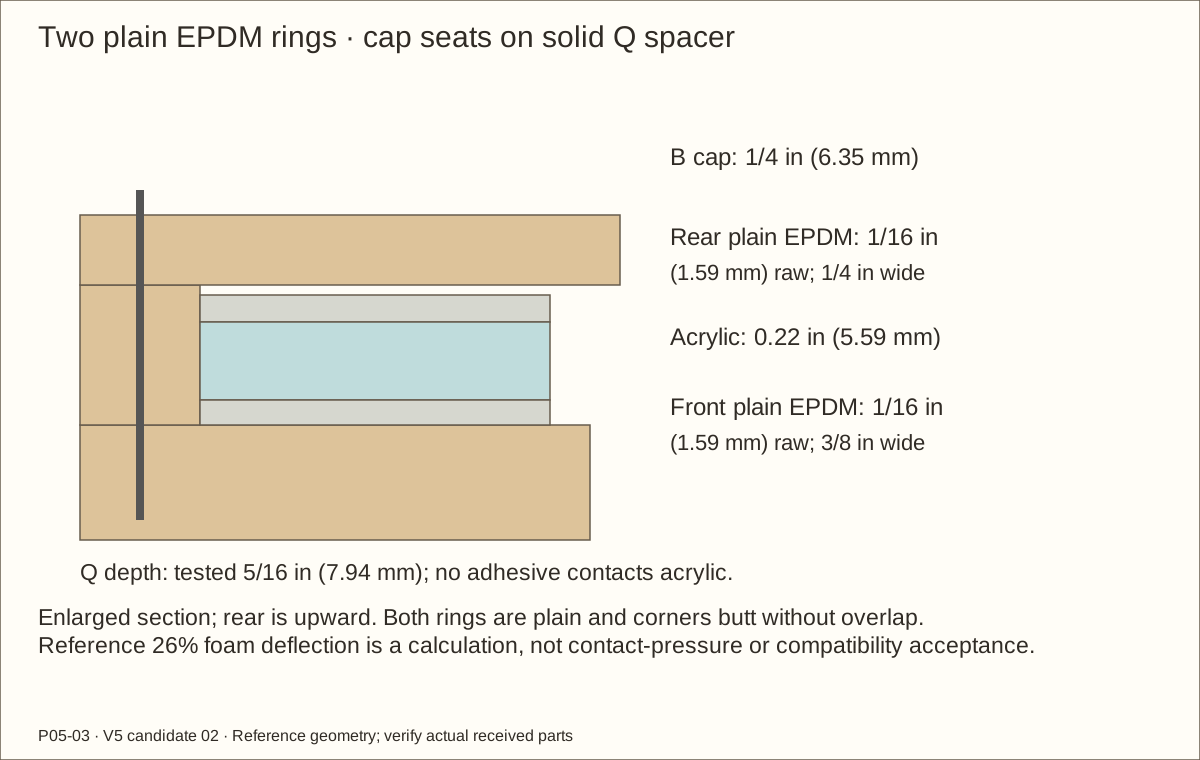
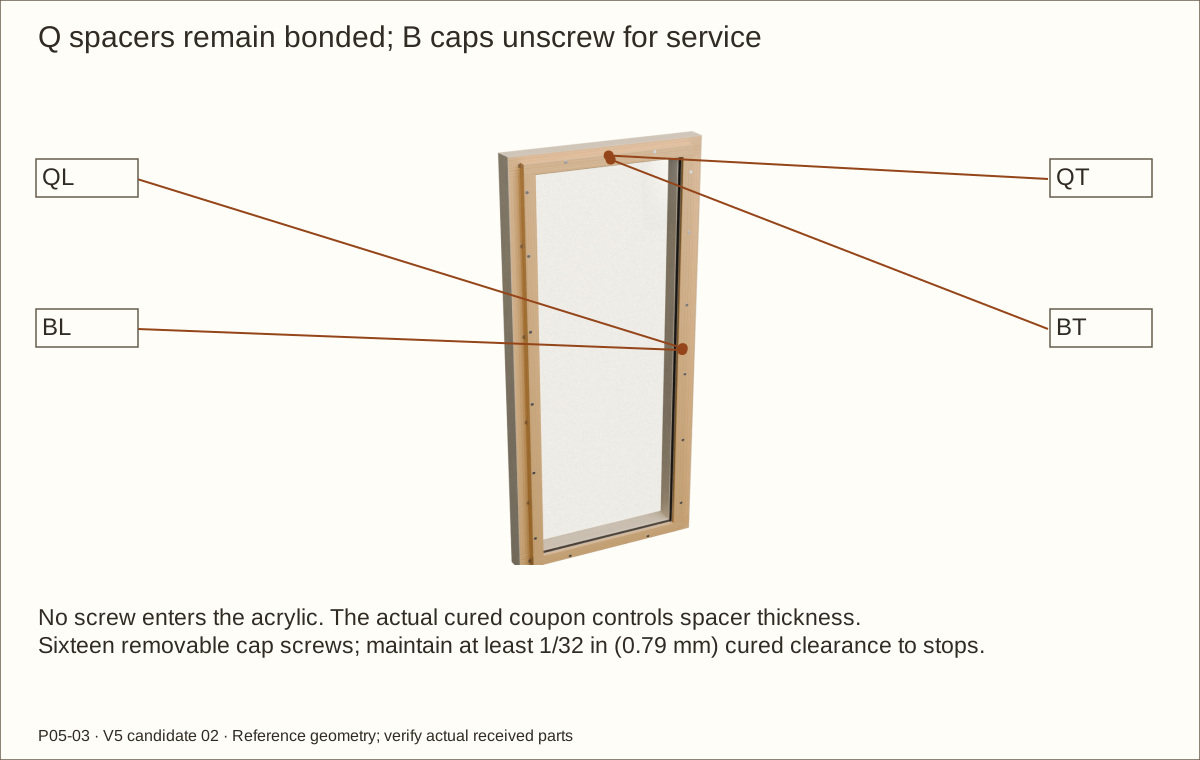
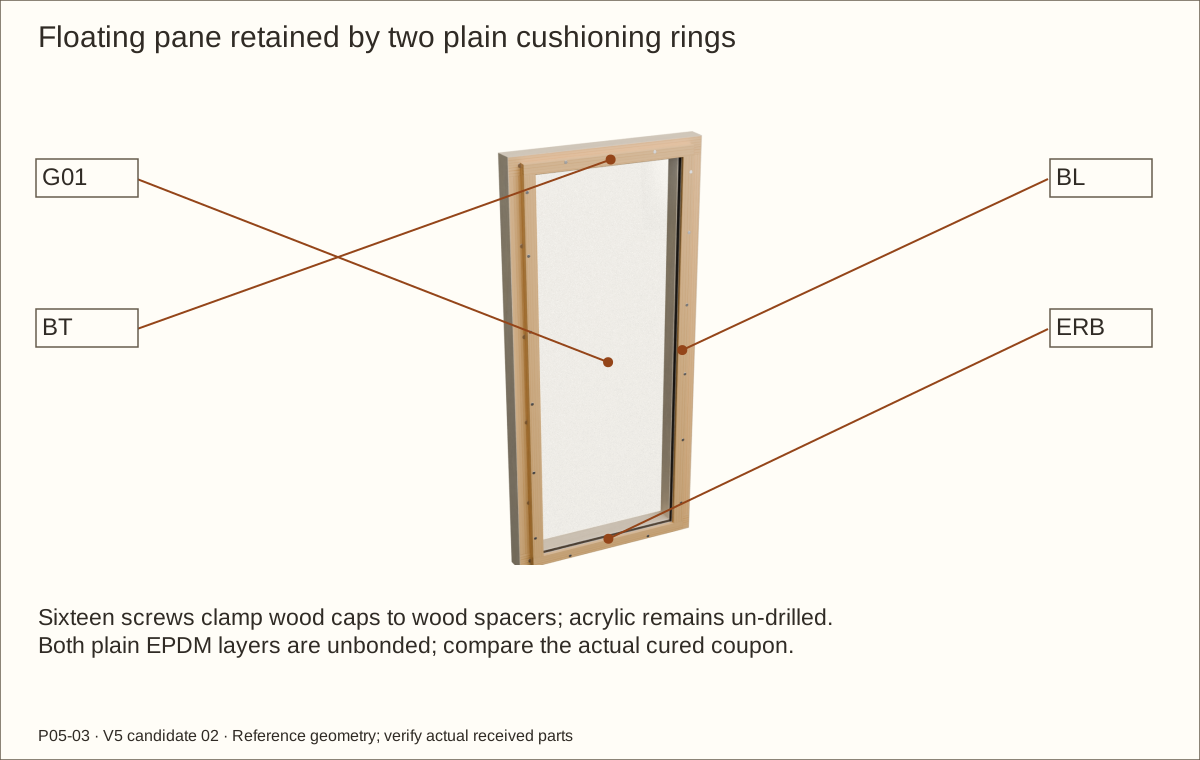
Make a small complete sample with the same bare glue lands, coating, full cure and actual products as the final door. Start with a 5/16 in (7.94 mm) spacer and 1/4 in (6.35 mm) cap. Both plain EPDM layers are 1/16 in (1.59 mm) raw thickness; no adhesive contacts the pane.
Hand-seat the cap on its solid Q land. The reference 0.22 in (5.59 mm) pane leaves 0.04625 in (1.17 mm) for each cushion, a calculated 26% deflection. This does not measure pressure or prove material compatibility.
Require flat, quiet acrylic, even cushioning and free edges. Correct overlap, proud heads or uneven lands first. If it fails, obtain product-specific fitting advice and prove the revised stack before final spacer planing or glue. Record the accepted setting on a measuring strip.
Check before continuing: The retained cured sample seats without bow, rattle or forced screw pressure.
Required wait: Complete glue hold, finish cure and any specified conditioning before measuring.
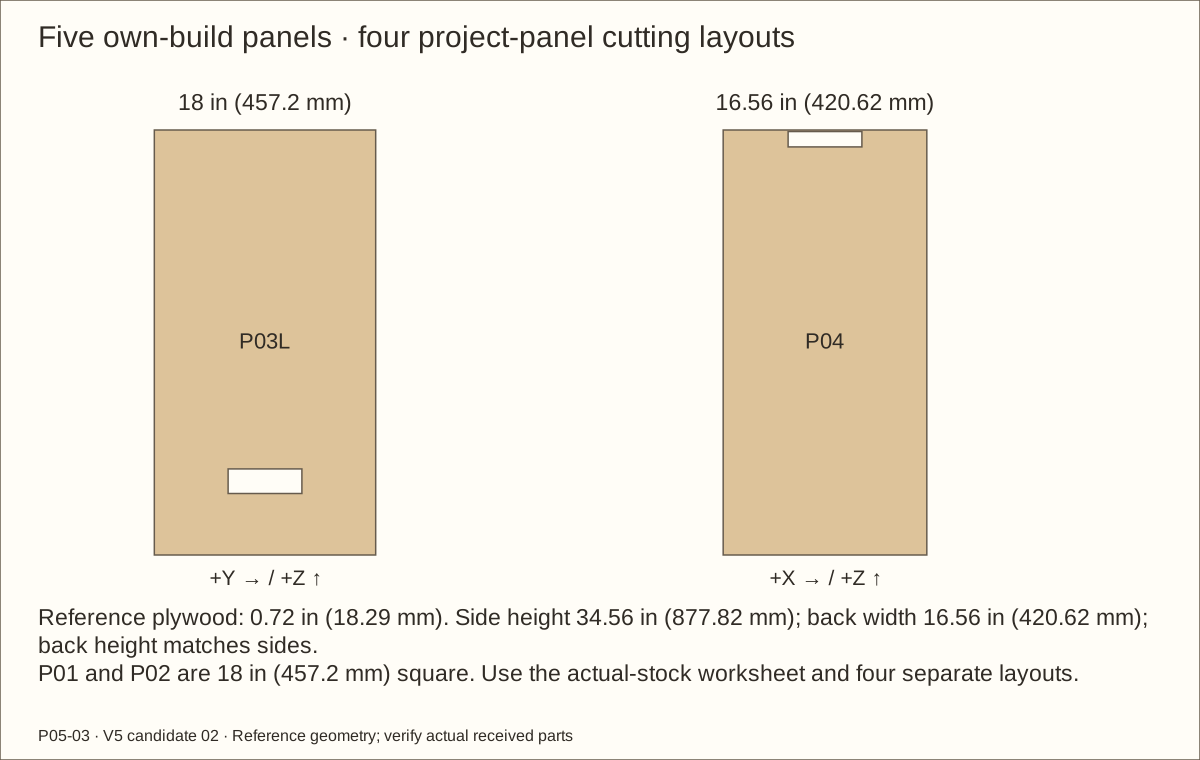
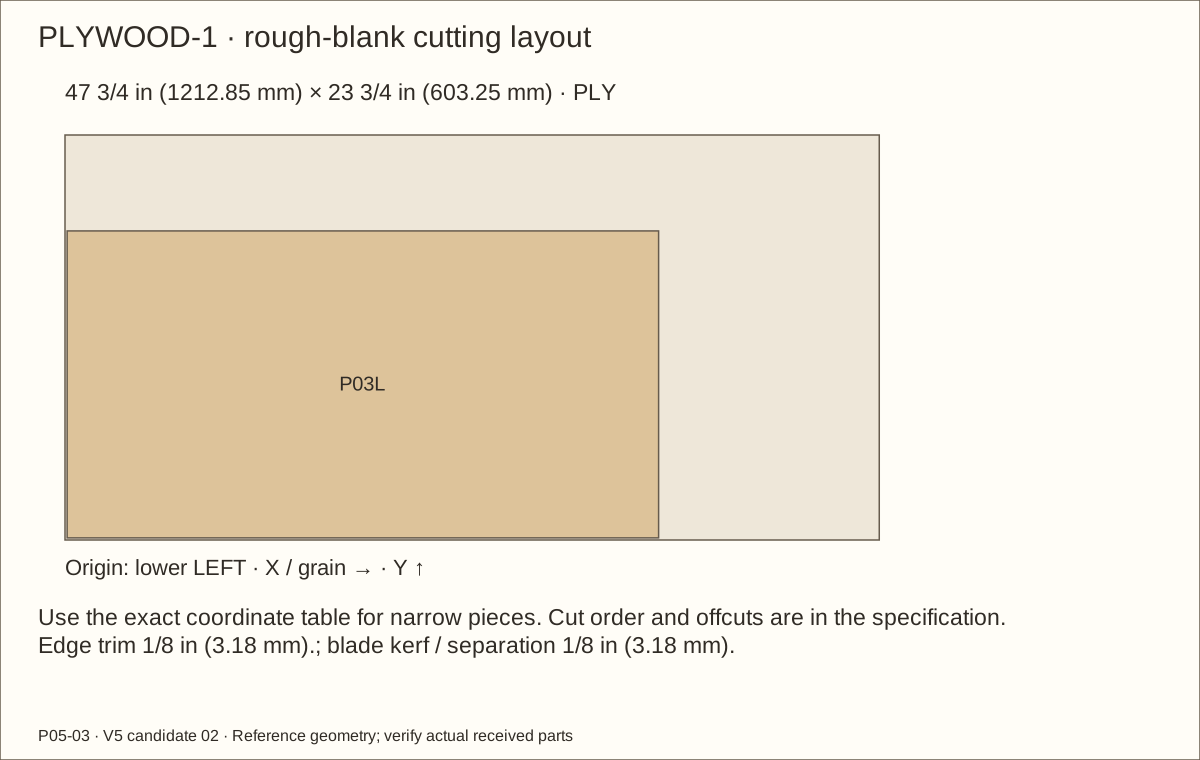
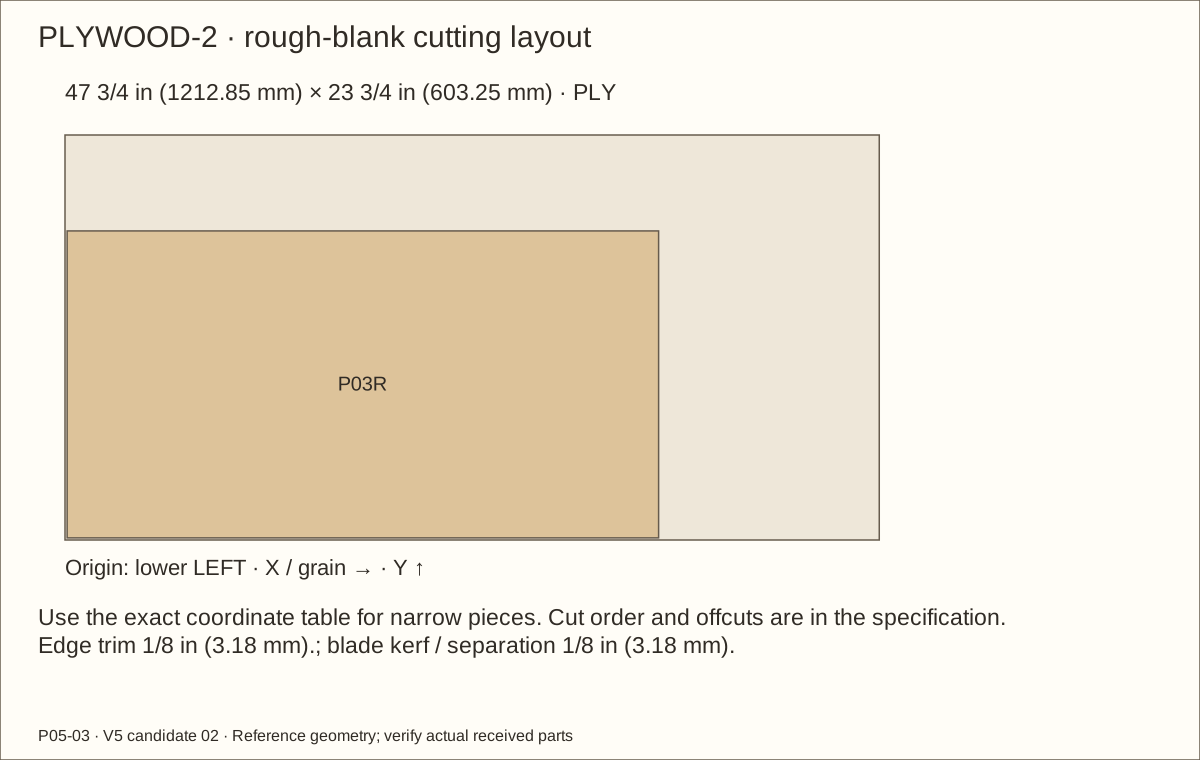
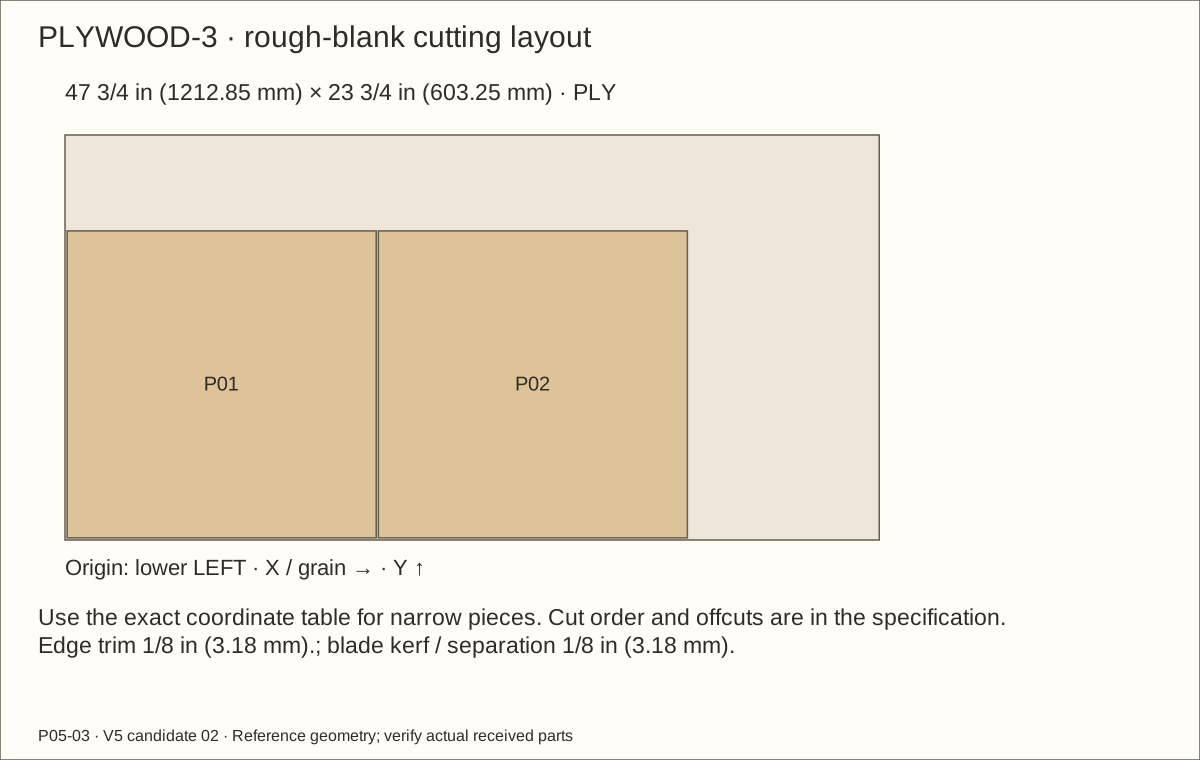
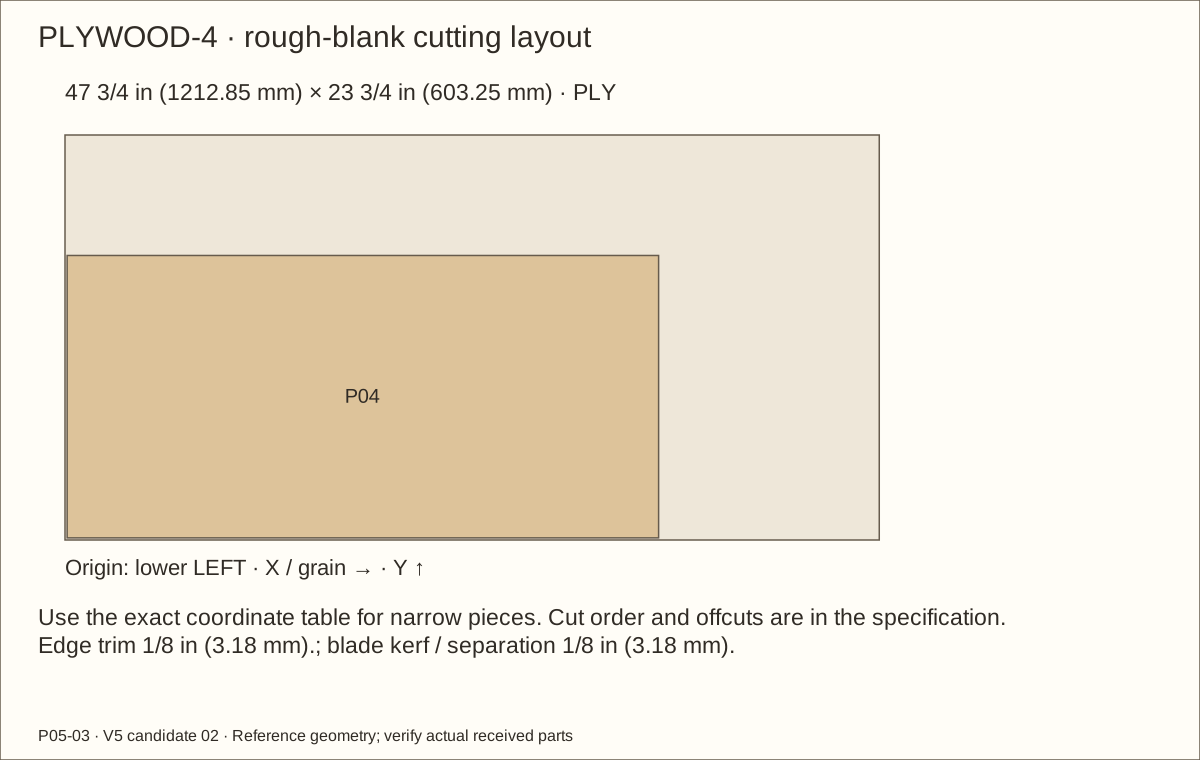
Follow the FOUR 23 3/4 in (603.25 mm) × 47 3/4 in (1212.85 mm) project-panel layouts with their edge trims and 1/8 in (3.18 mm) kerfs. Finish P01 and P02 at 18 in (457.2 mm) square. Support the sheet and waste throughout every cut.
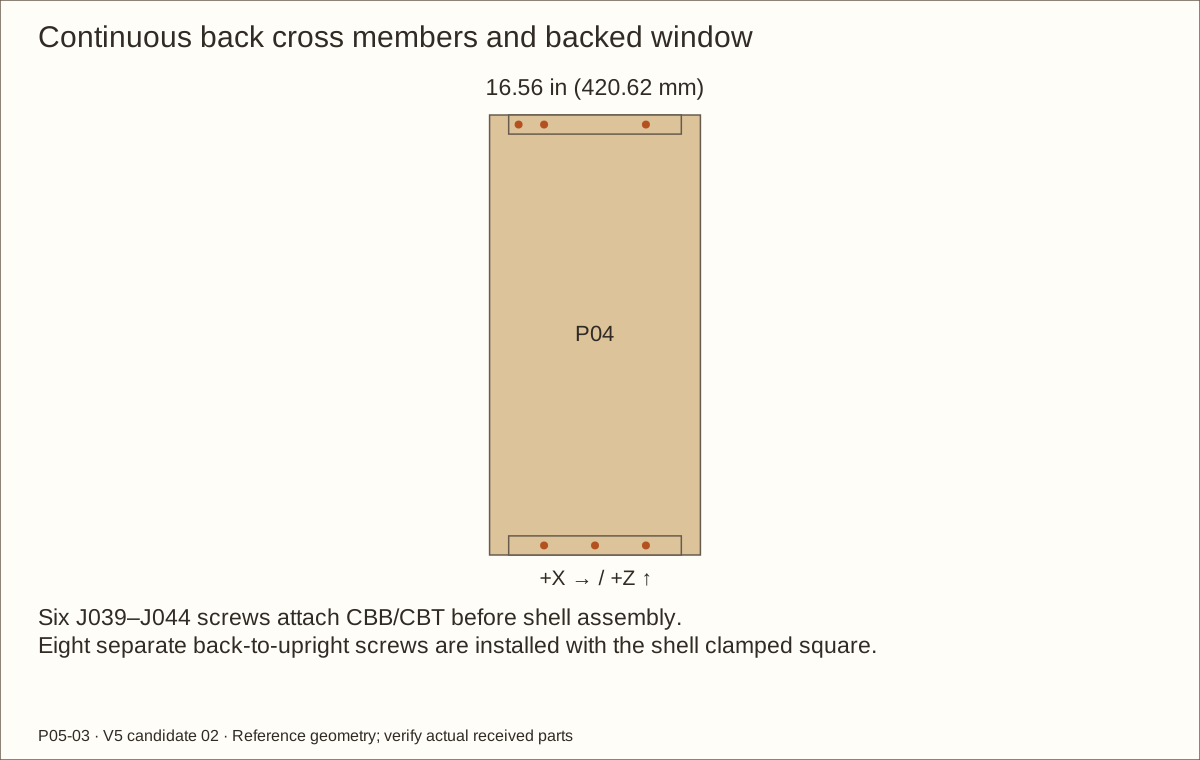
Side height is 36 in (914.4 mm) minus twice the actual plywood thickness; reference 34.56 in (877.82 mm). Fit P04 between the sides: width is 18 in (457.2 mm) minus twice that thickness, reference 16.56 in (420.62 mm), and height matches the sides.
Label FRONT, LEFT/RIGHT, inside/outside and each part ID. Compare diagonals and dry-clamped mating edges. Preserve the physical gauges and do not cut openings until the required product trials pass.
Check before continuing: Five square, matching panels form the intended bare envelope.
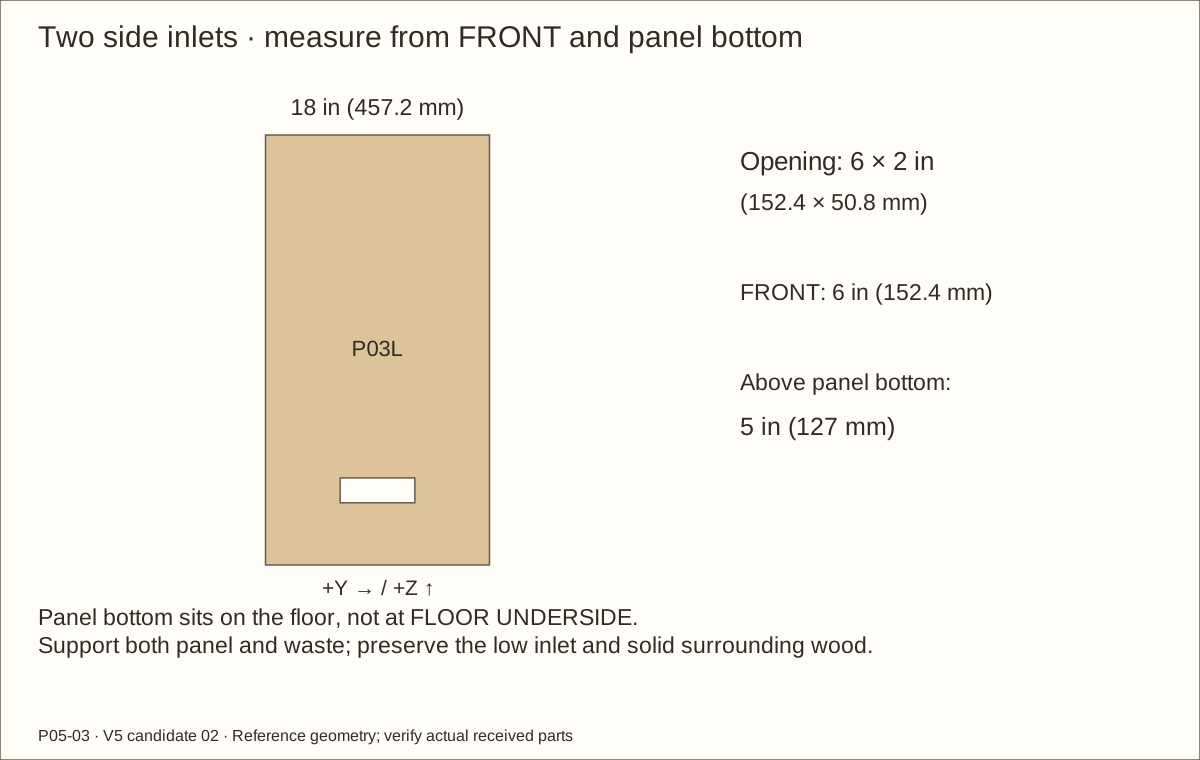
On EACH side mark 6 in (152.4 mm) and 12 in (304.8 mm) from FRONT, and 5 in (127 mm) and 7 in (177.8 mm) above its lower cut edge. Join the lines for a 6 in (152.4 mm) × 2 in (50.8 mm) through-opening.
Clamp the panel flat with independent waste support. Drill a starter inside the waste, then use controlled jigsaw/router passes to the lines. Square routed corners without extending cuts into sound wood.
Smooth splinters and mirror the faces while retaining the same front/bottom datums. The panel bottom rests on the floor, so these local heights differ from the assembly floor-underside coordinates.
Check before continuing: Both openings match and remain clear of the planned supports.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Cut the roof opening and backed rear recess
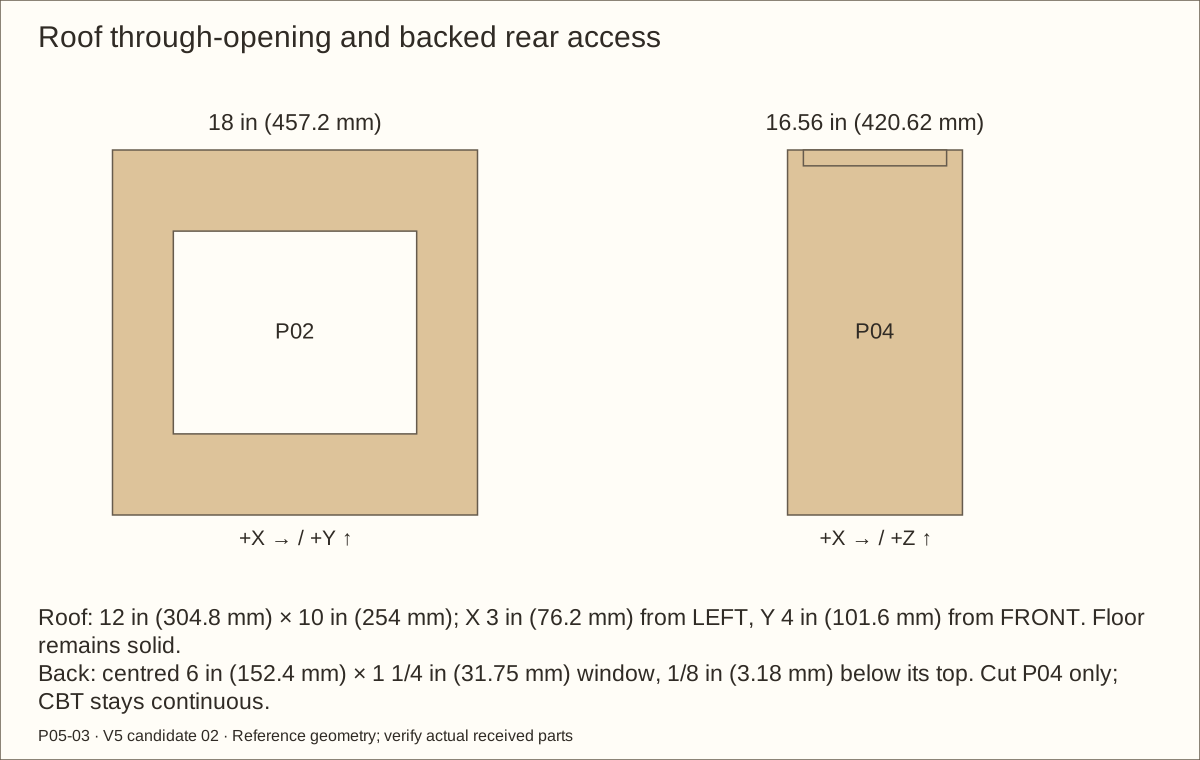
On P02 mark X at 3 in (76.2 mm) and 15 in (381 mm) from LEFT, Y at 4 in (101.6 mm) and 14 in (355.6 mm) from FRONT. Cut the resulting 12 in (304.8 mm) × 10 in (254 mm) roof opening with supported waste. Keep P01 solid.
After the complete anti-tip sample passes, centre the 6 in (152.4 mm) × 1 1/4 in (31.75 mm) rear window across P04. Its top is 1/8 in (3.18 mm) below the panel top and its bottom 1 3/8 in (34.93 mm) below that edge.
Cut only the back plywood. Continuous CBT later backs the entire recess with 1/8 in (3.18 mm) overlap above and below. Smooth the window without rounding away its bearing or arbitrarily enlarging the opening.
Check before continuing: Roof opening and rear window match their named datums; the floor stays solid.
Tools / setup: Thickness planer with safe support, caliper, supported saw, stops and clamps
Before you begin: Never feed short or narrow finished strips into a thickness planer.
Mill long, wide pine before ripping
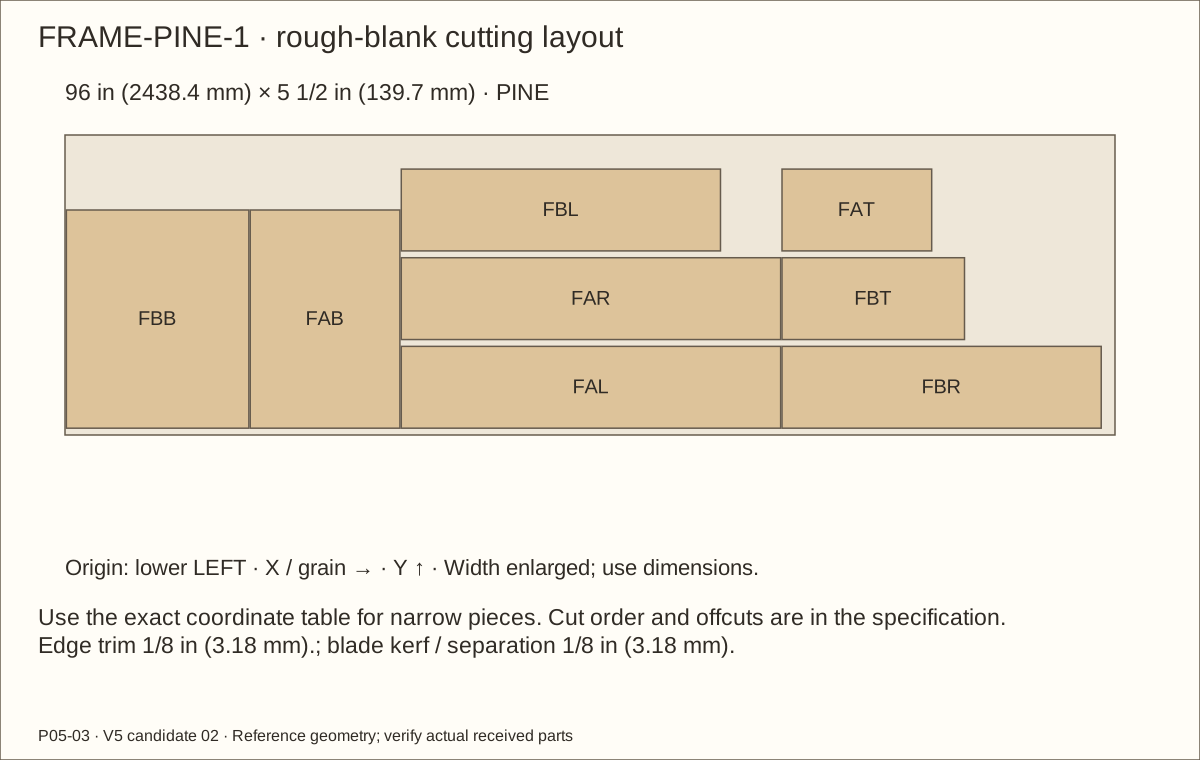
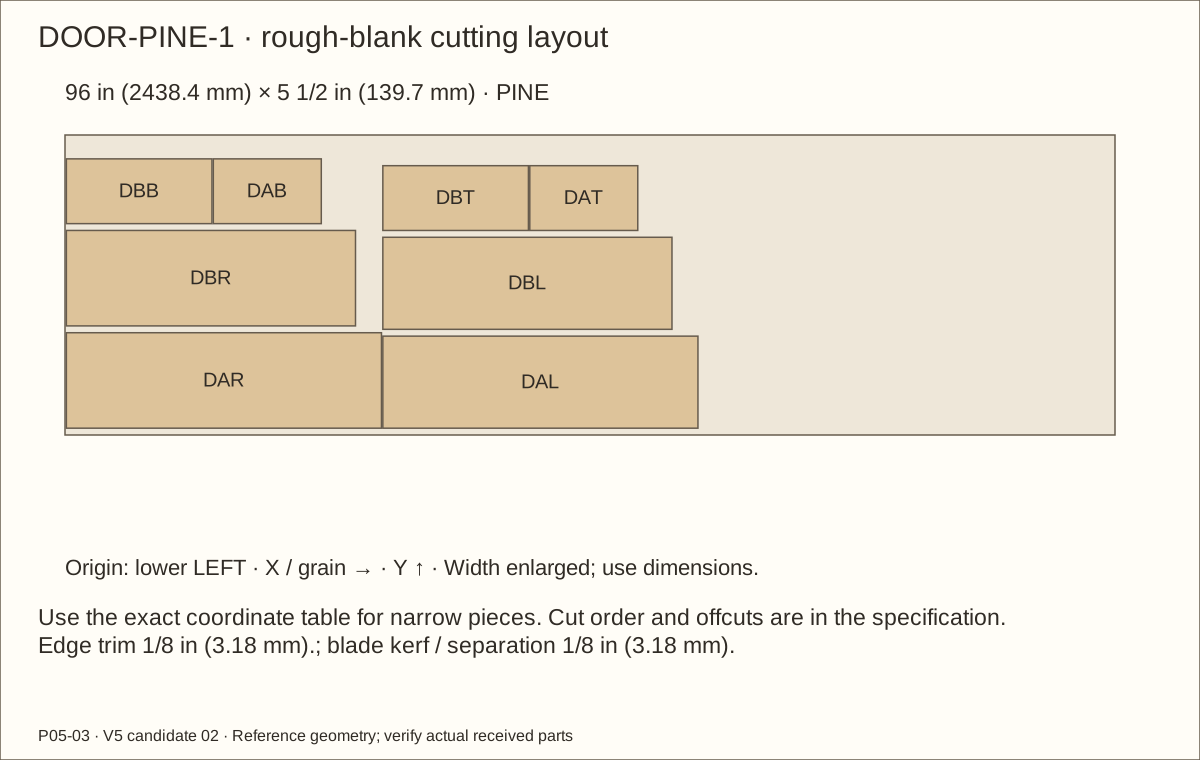
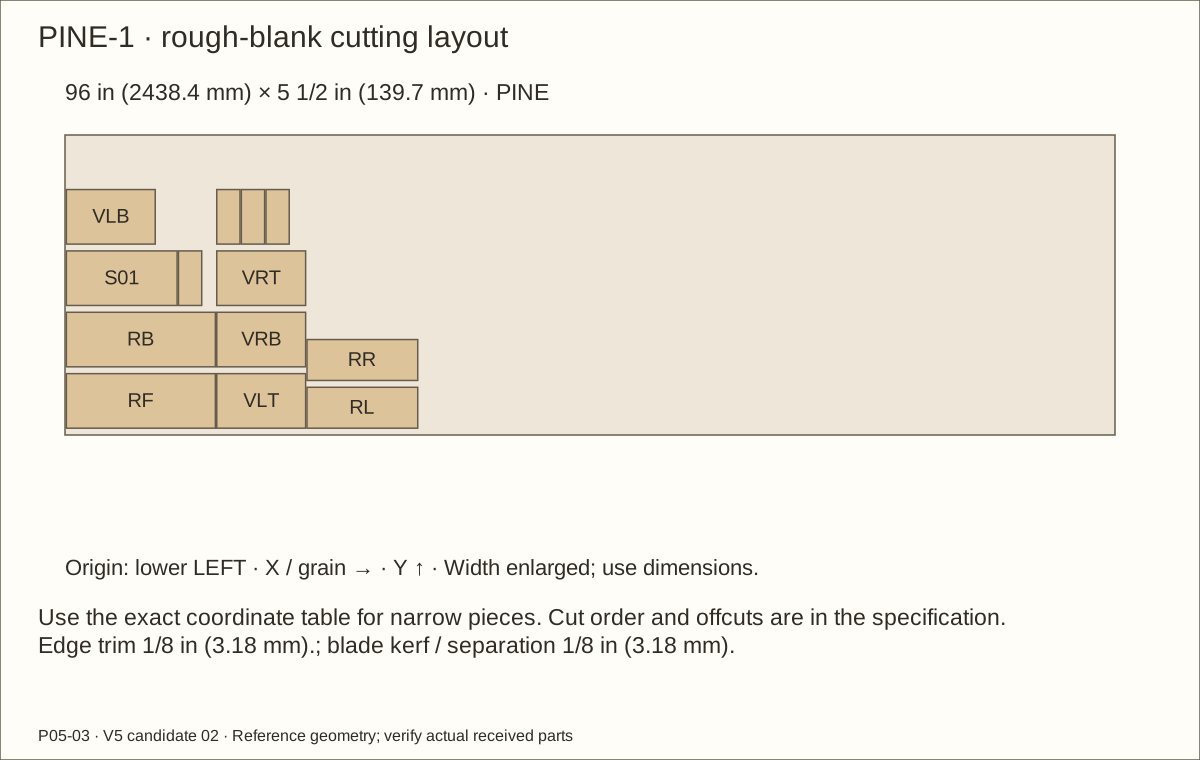
Keep each board wide and long through thicknessing. Plane FRAME-PINE to 5/8 in (15.88 mm) and DOOR-PINE to 39/64 in (15.48 mm). The two-layer door rear aligns with the stops while its front is 1/32 in (0.79 mm) behind the fixed-frame front.
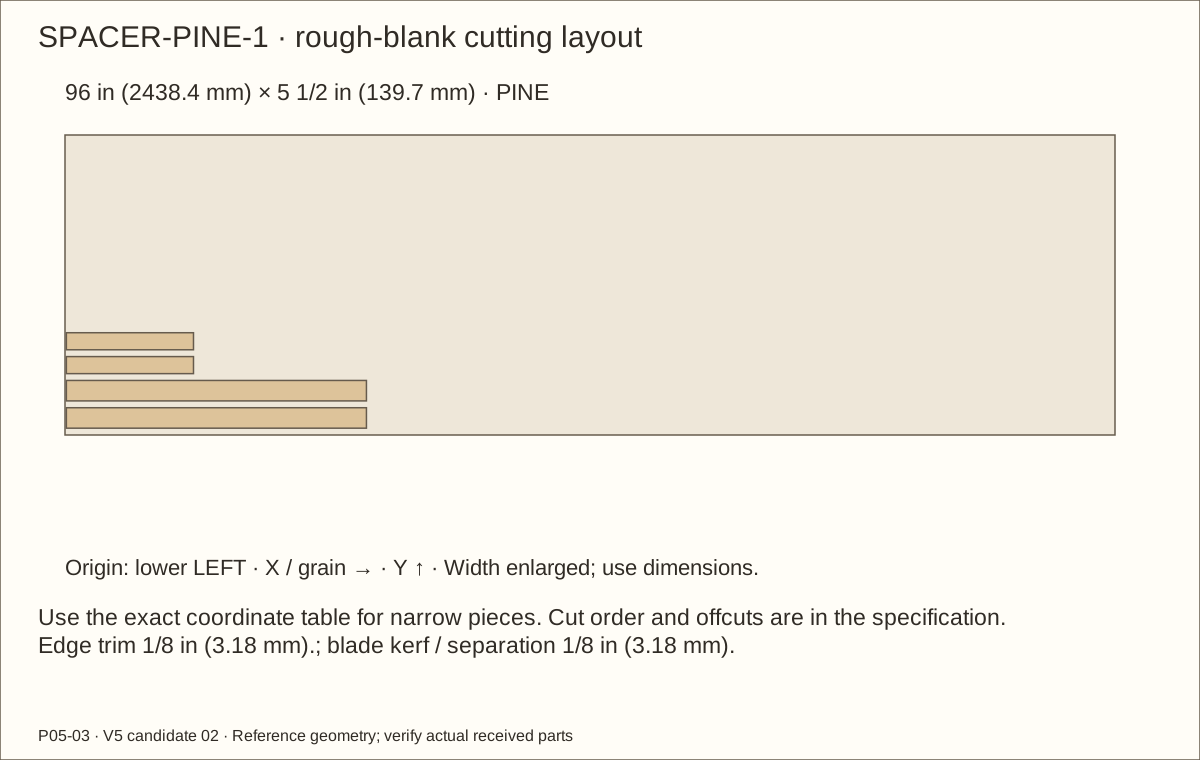
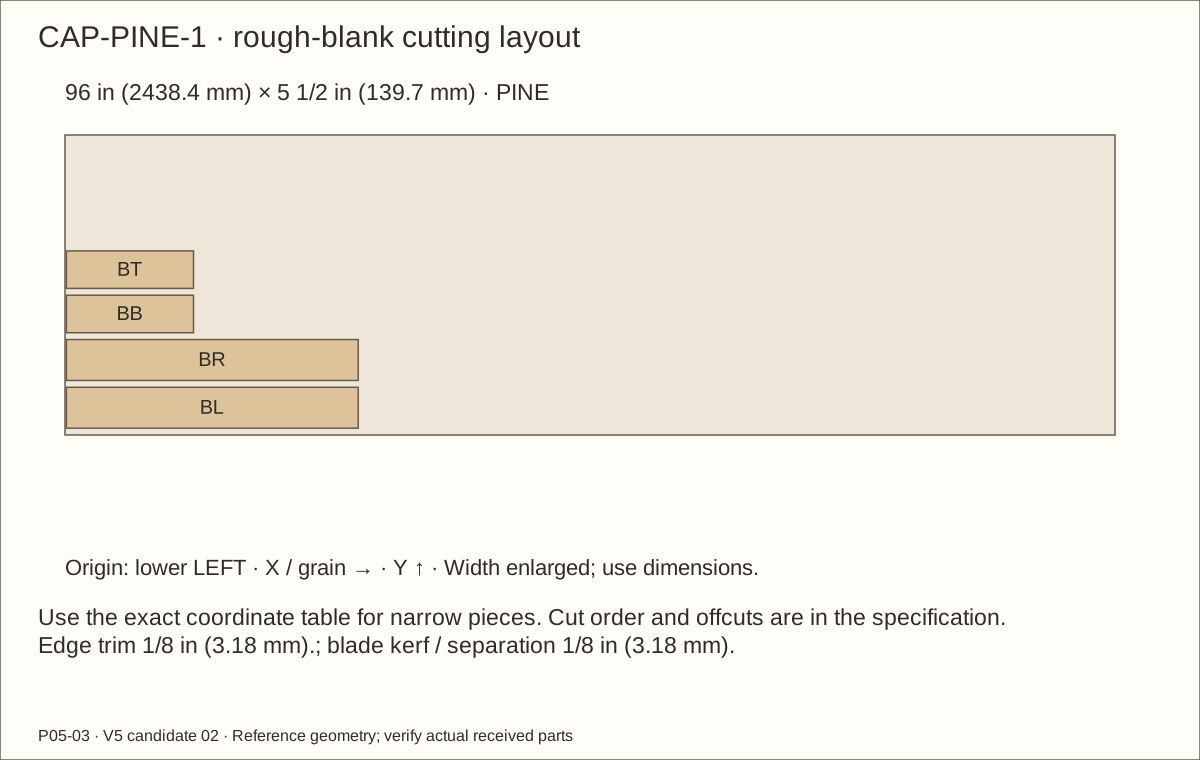
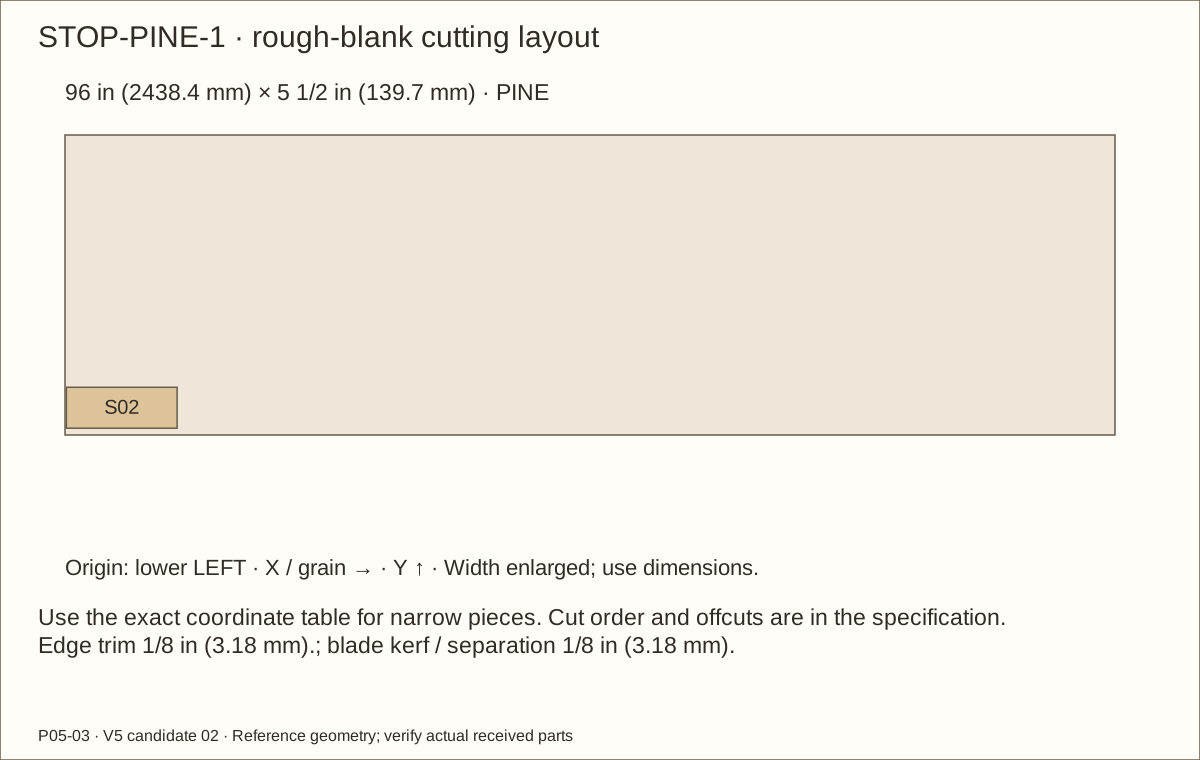
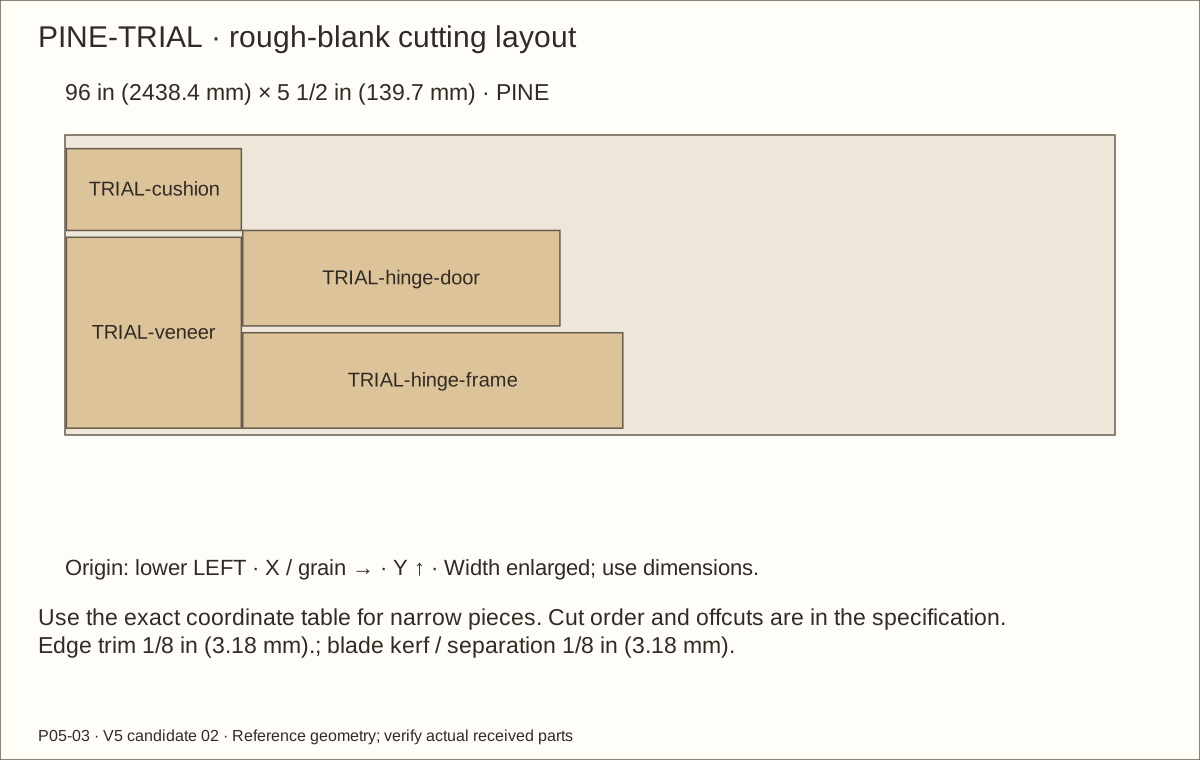
Use separate boards for the 3/4 in (19.05 mm) captures/lower stop, tested 5/16 in (7.94 mm) Q spacers, 1/4 in (6.35 mm) caps and 1/2 in (12.7 mm) upper stop. A seventh board supplies full-height hinge and veneer/cushion trials. These conservative purchases preserve safe planer feed length.
Follow machine minimum feed dimensions, use suitable dust control and support, then rip and crosscut labeled pieces to their own layout. Rout pockets on supported wide blanks before making short finished strips.
Check before continuing: Every blank has the required measured thickness and grain direction.
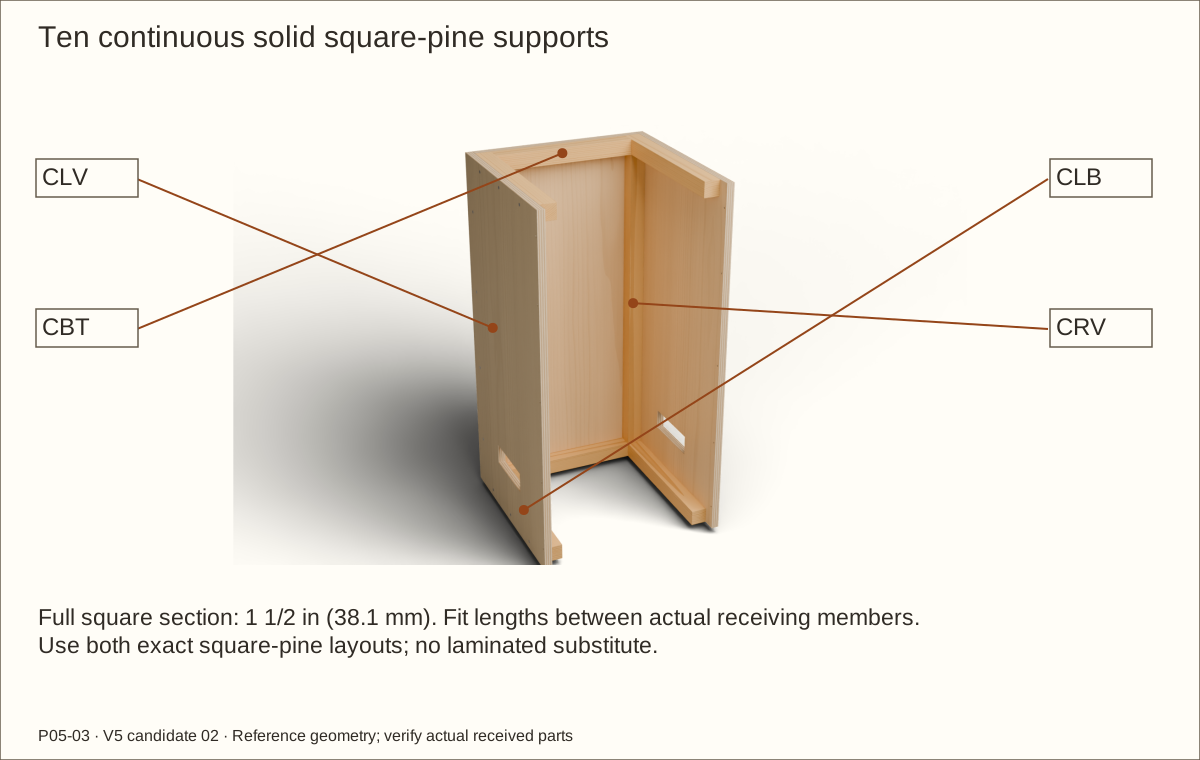
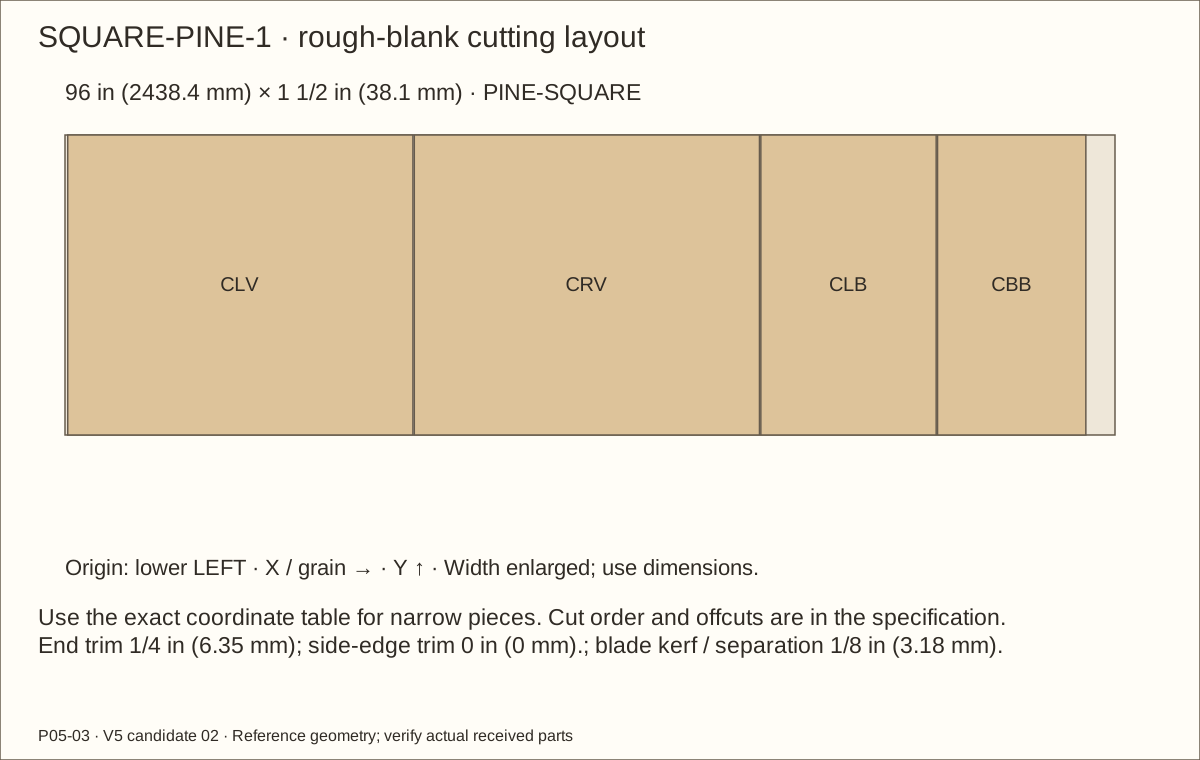
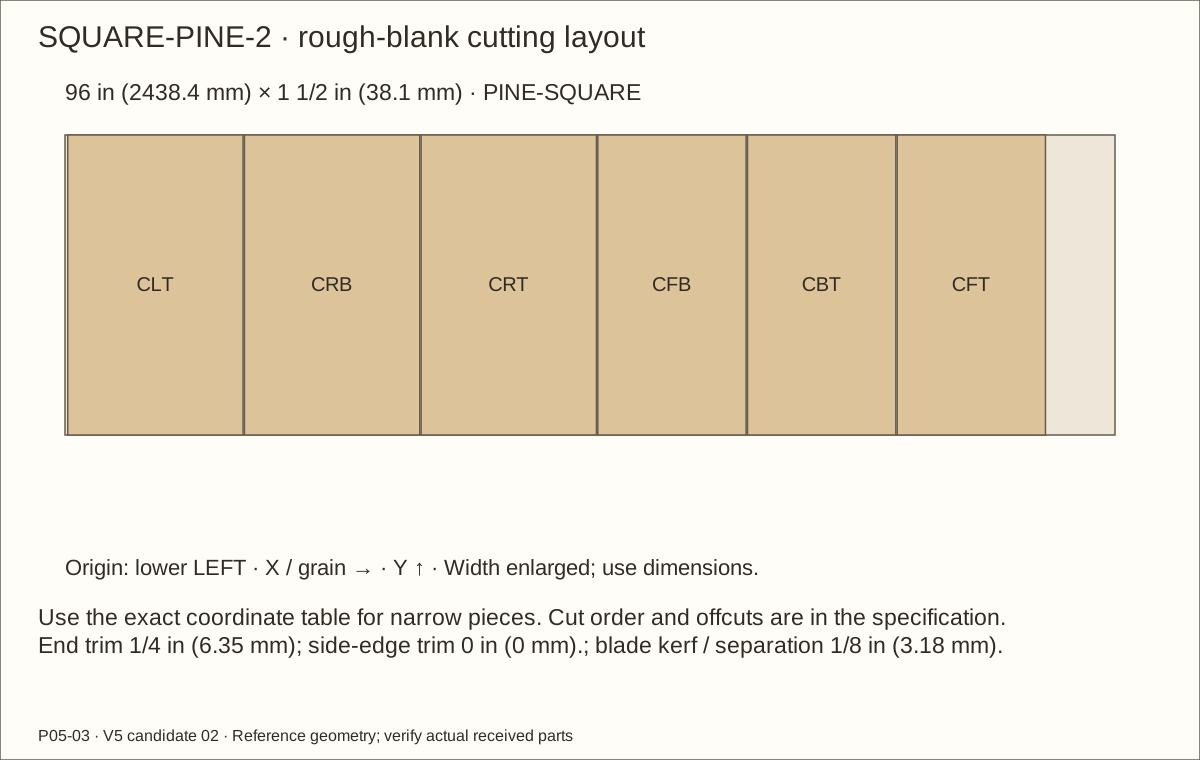
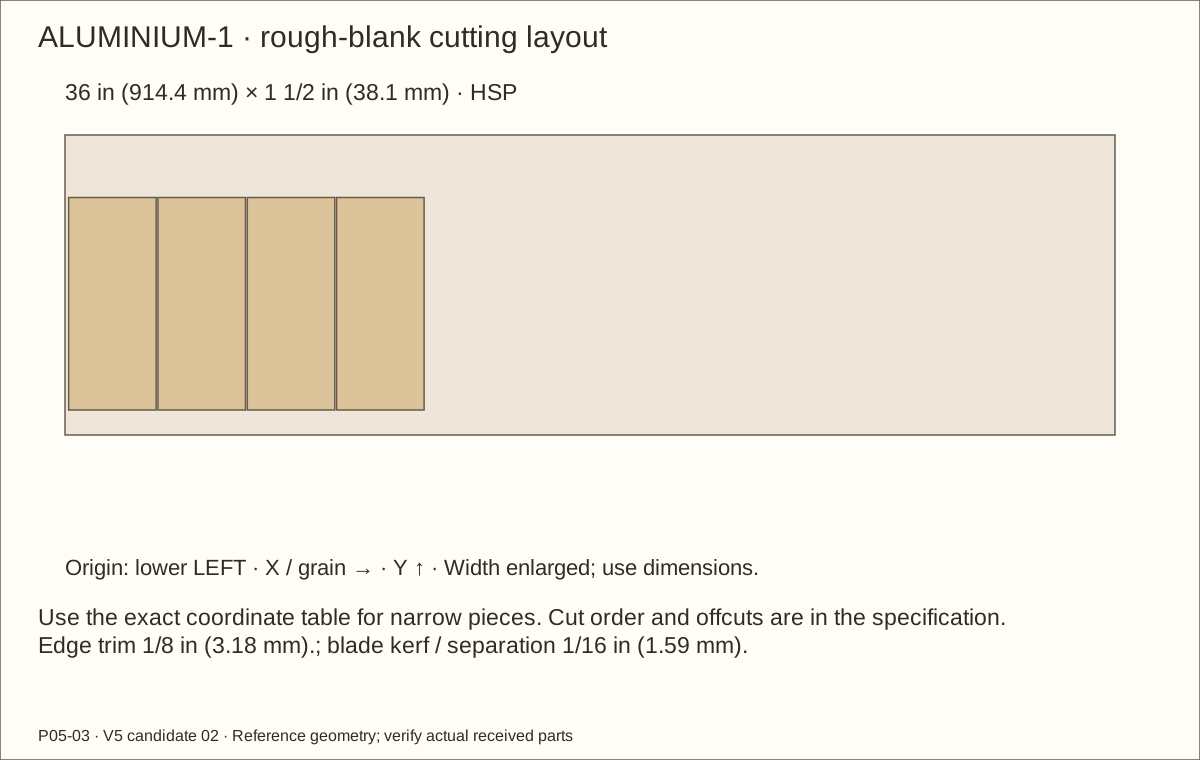
Use two solid 1 1/2 in (38.1 mm) square-pine sticks and the exact kerf-aware groups. Stick one: CLV, CRV, CLB, CBB. Stick two: CLT, CRB, CRT, CFB, CBT, CFT.
Reference rear uprights are 31.56 in (801.62 mm); side horizontals 16.03 in (407.16 mm); cross members 13.56 in (344.42 mm). Fit between real receivers using panel-thickness and square-stock offcuts. Preserve the full solid section.
Check square ends, label every member and test each dry fit. Do not force long supports into the shell or replace solid cleats with laminated scraps.
Check before continuing: All ten supports fit without distorting the panels.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Lay out the crossed fixed-frame layers
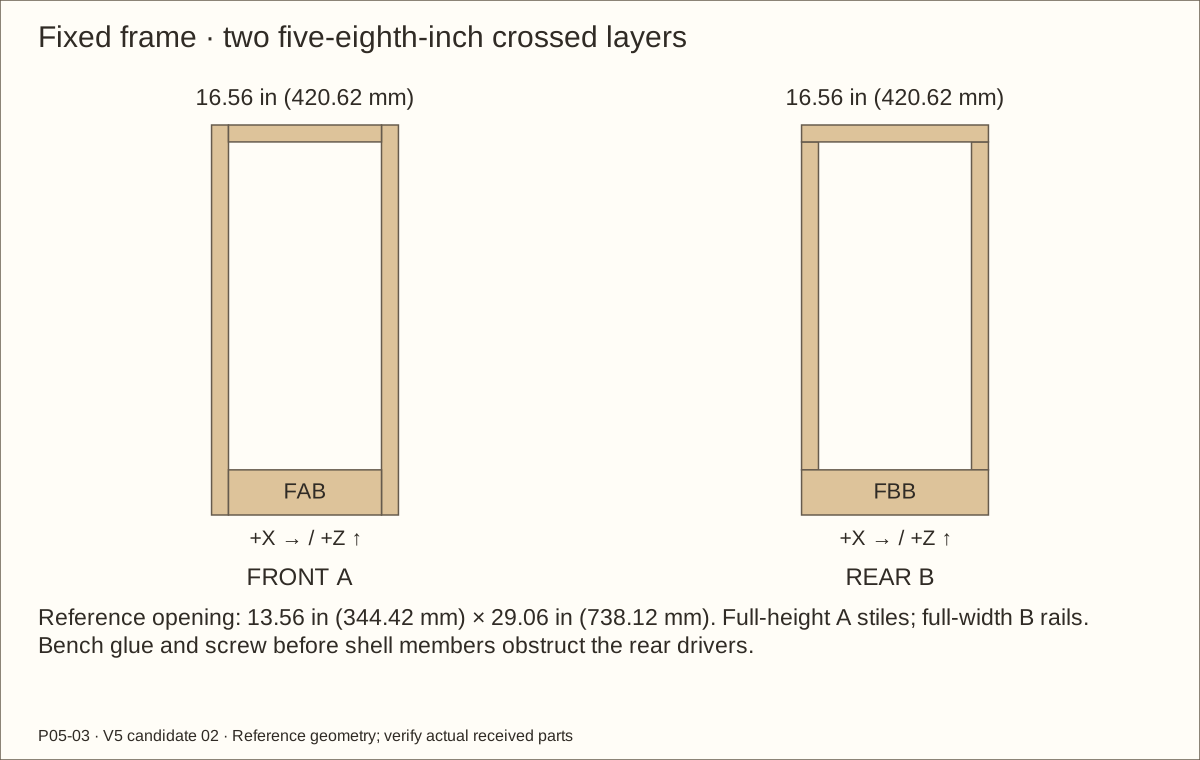
Dry-lay each 5/8 in (15.88 mm) layer on a flat bench. Front layer A has full-height 1 1/2 in (38.1 mm) stiles, a 4 in (101.6 mm) bottom rail and 1 1/2 in (38.1 mm) top rail between them. Rear layer B has full-width rails and stiles between.
Fit the perimeter to actual panels. Reference outside size is 16.56 in (420.62 mm) × 34.56 in (877.82 mm); the clear opening is 13.56 in (344.42 mm) × 29.06 in (738.12 mm). Each layer bridges the other layer’s butt seams.
Place actual plywood gauges beyond the bottom and left edges; their outer faces reproduce cabinet floor/side datums for the station drawing. Check both diagonals and full face contact before glue.
Check before continuing: The flat square layers have crossed seams and the intended opening.
Parts: Fixed frame; twenty #8 × 1 in (25.4 mm) screws; Titebond III
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: The glue maker excludes structural/load-bearing use and continuous immersion.
Glue and screw the frame on the bench
Apply glue to clean bare mating wood above 47°F (8.3°C). At 70°F (21°C), 50% relative humidity, the maker gives 8–10 minutes open time and 20–25 minutes total assembly time. Clamp with straight cauls that spread pressure.
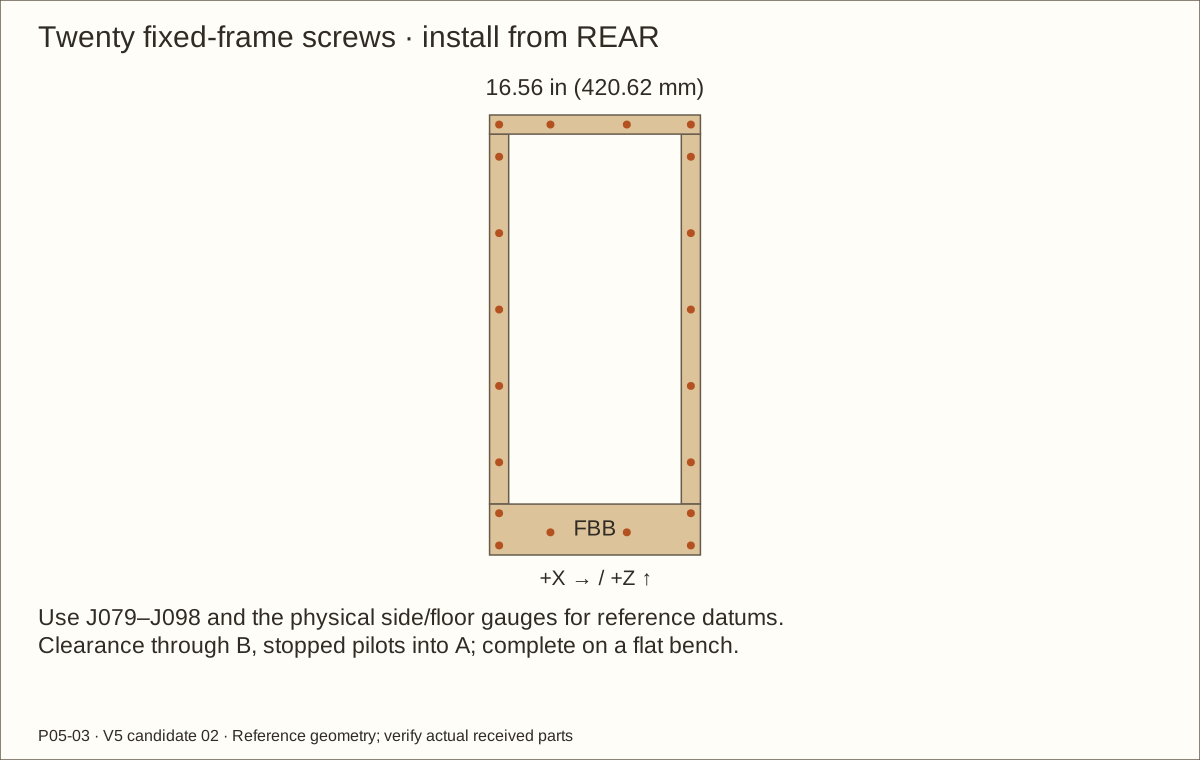
Use the twenty exact J079–J098 stations. From REAR, clearance-drill layer B and make stopped root-matched pilots into A; reference pilot extension into A is 7/16 in (11.11 mm) including the point. Nominal screw engagement is 3/8 in (9.53 mm) and rear cover 1/4 in (6.35 mm).
Drive flush without burying heads; compare diagonals and remove squeeze-out. Complete these screws on the bench before shell members block their driver paths.
Check before continuing: Twenty flush screws and full glued contact preserve the square frame.
Required wait: This build uses a 24-hour clamp/unstressed hold before machining or installation; extend for conditions and current maker instructions.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
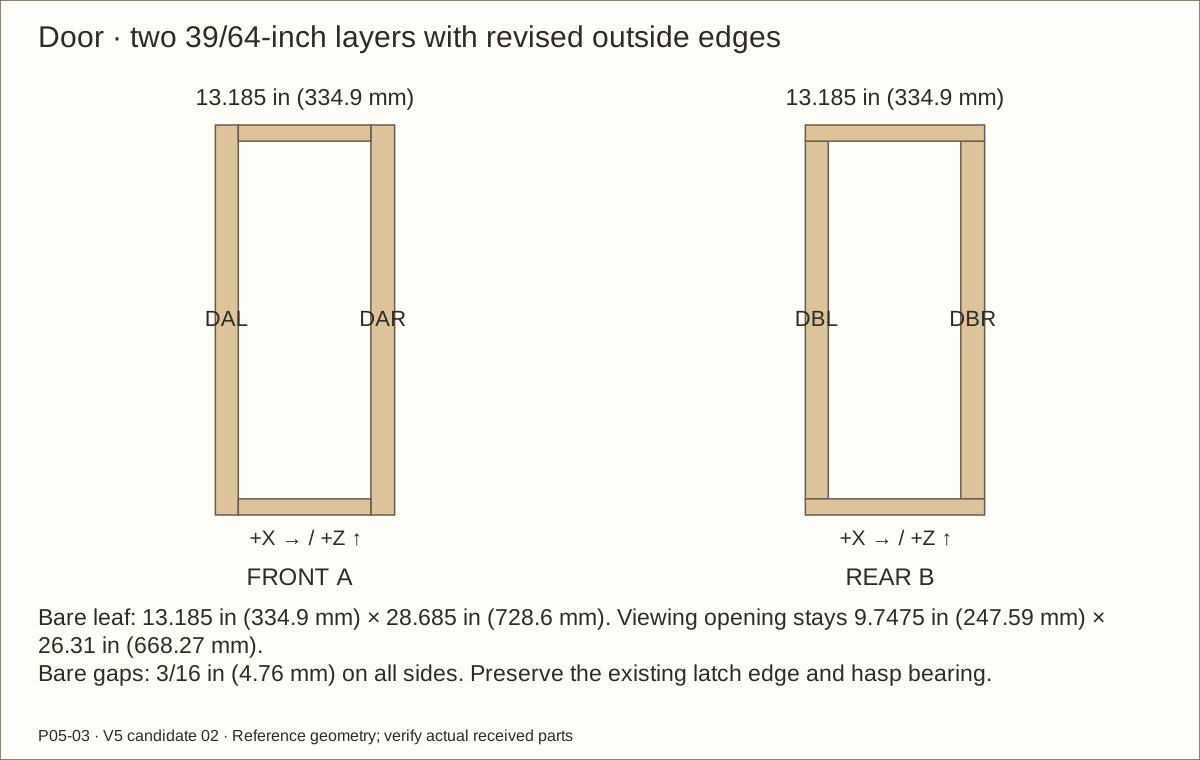
Fit the revised bare door perimeter
Dry-lay the two 39/64 in (15.48 mm) layers with full-height A stiles and full-width B rails. Fit 3/16 in (4.76 mm) BARE gaps on all four sides to allow veneer on opposing surfaces.
Reference bare leaf is 13.185 in (334.9 mm) wide × 28.685 in (728.6 mm) high. Preserve the original viewing opening, 9.7475 in (247.59 mm) × 26.31 in (668.27 mm), and the original latch edge. Trim only hinge, top and bottom per the revised parts.
Use actual opening gauges and the exact cut schedule. Do not copy rounded old overall door sizes or trim the latch edge further: the square hasp plate has a narrow bearing margin.
Check before continuing: The bare leaf fits with equal planned gaps and unchanged glazing datums.
Parts: Door layers; fourteen #8 × 1 in (25.4 mm) screws
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
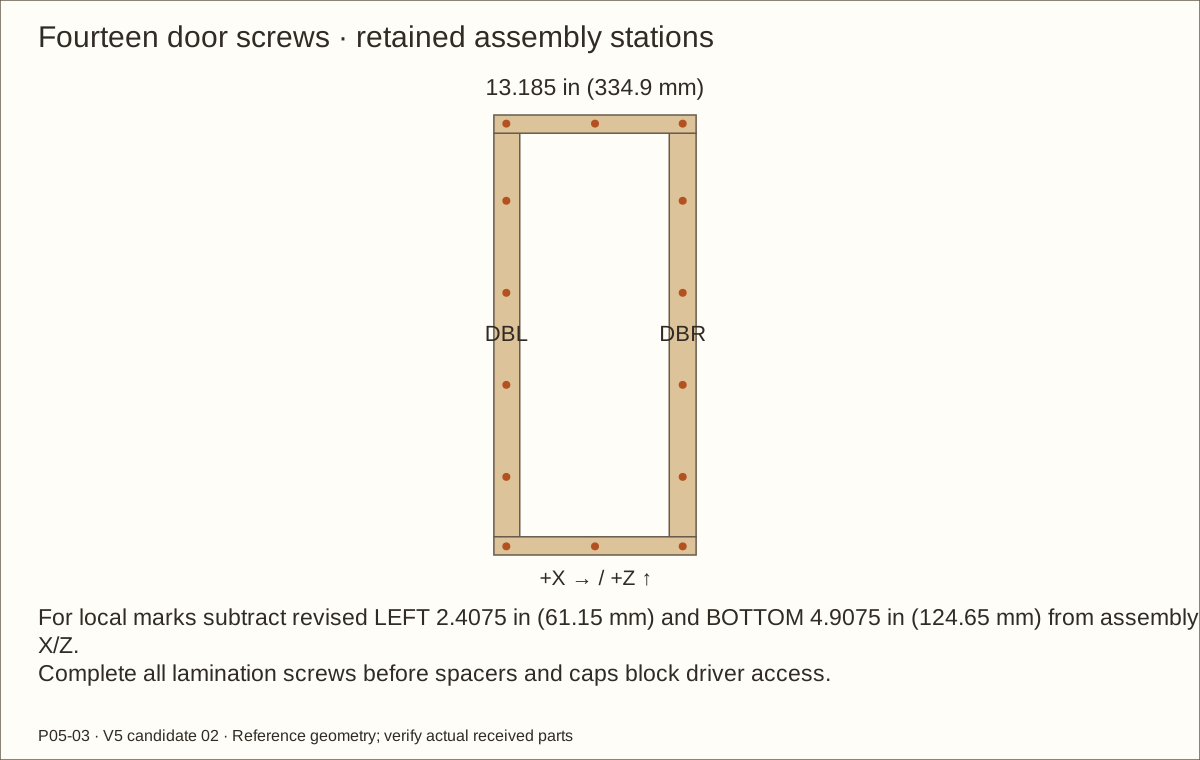
Glue and screw the door before retainers
Glue clean bare mating faces and clamp flat under the fixed-frame glue conditions. Keep all seams crossed; measure both diagonals without using acrylic as a brace.
Use J099–J112 from REAR. On the loose leaf, subtract its revised left X 2.4075 in (61.15 mm) and bottom Z 4.9075 in (124.65 mm) from assembly coordinates to obtain local marks. Do not reuse offsets from the old door perimeter.
Clearance-drill rear layer B and blind-pilot A after the actual screw test. Reference engagement is 25/64 in (9.92 mm) and cover 7/32 in (5.56 mm). Fit all fourteen flush screws before Q spacers and B caps obstruct the driver.
Check before continuing: All screws land in the intended wood and the door remains flat.
Required wait: Keep clamped and unstressed for the 24-hour build hold before machining or hanging.
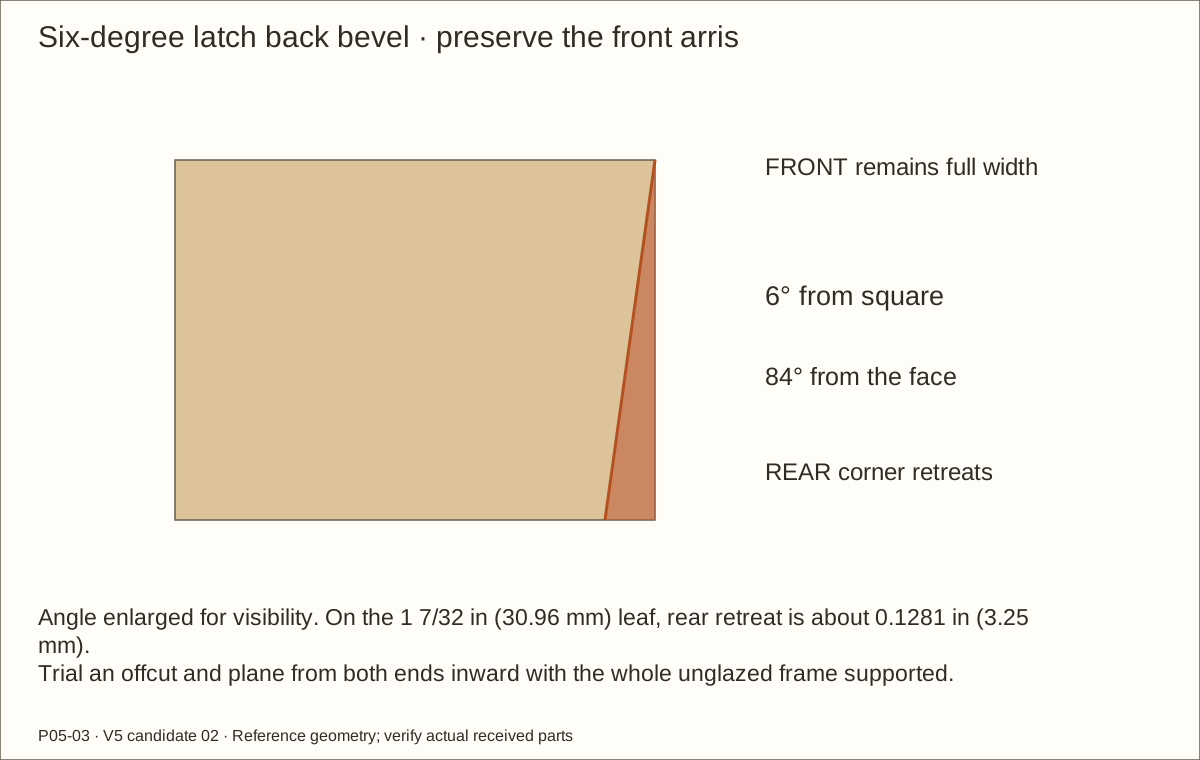
Mark FRONT and REAR. Preserve the front latch arris, the corner between its front face and edge. Set a sliding bevel 6° from square, or 84° from the face.
Trial a laminated offcut first. Across the 1 7/32 in (30.96 mm) leaf thickness the rear edge retreats about 0.1281 in (3.25 mm). Use the angle and straightedge, not a rounded tape offset, to control the cut.
Clamp the whole leaf in padded jaws and plane light passes from both ends inward. Keep the hinge edge square. Recheck the opening, hasp bearing and all bare gaps before finishing.
Check before continuing: The rear latch corner clears while the front edge and viewing opening remain intact.
Parts: P03L/P03R; six side supports; twenty shell screws
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
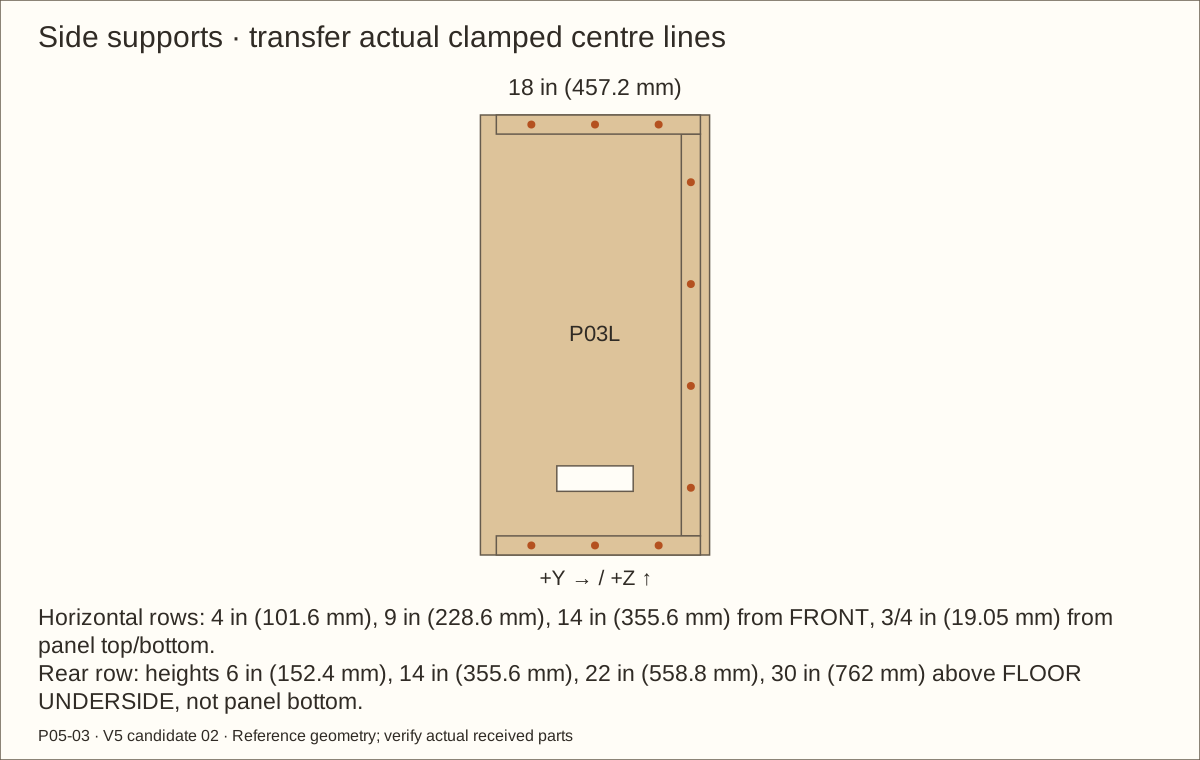
Attach the side-panel supports
Lay each panel inner face up. Top and bottom supports begin 1 1/4 in (31.75 mm) behind FRONT and finish flush with the panel top/bottom. Fit the rear upright between them; use actual back plywood as a gauge to reserve the rear rebate.
Clamp every support, then transfer its centreline. Side horizontal rows use 4 in (101.6 mm), 9 in (228.6 mm) and 14 in (355.6 mm) from FRONT; rear-upright rows use assembly heights 6 in (152.4 mm), 14 in (355.6 mm), 22 in (558.8 mm) and 30 in (762 mm) above the floor-underside gauge.
Use J001–J020: clearance through plywood and stopped pilots into solid pine. Reference shell screws are #8 × 1 3/4 in (44.45 mm); pilot depth into pine is at most 1 1/8 in (28.58 mm) including its point after the actual trial. Seat flush.
Check before continuing: Support faces sit square, rear rebates are reserved and side inlets stay clear.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Attach the continuous back supports
Use square-pine offcuts at both back-panel side edges to fit CBB/CBT between the rear uprights. Reference length is 13.56 in (344.42 mm). Align them flush with the panel bottom/top.
Keep CBT continuous behind the entire rear restraint window. Mark J039–J044 using the left/floor plywood gauges: lower X at 5 in (127 mm), 9 in (228.6 mm) and 13 in (330.2 mm); upper X at 3 in (76.2 mm), 5 in (127 mm) and 13 in (330.2 mm), each row 3/4 in (19.05 mm) from its panel edge.
Clamp, clearance-drill the panel, stopped-pilot the pine and fit six #8 × 1 3/4 in (44.45 mm) screws flush. The separate eight back-to-upright screws go in during shell assembly.
Check before continuing: Both cross members bear fully and CBT backs the whole access recess.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Do not leave the tall partly fastened shell standing unsupported.
Stand and brace the shell around the floor
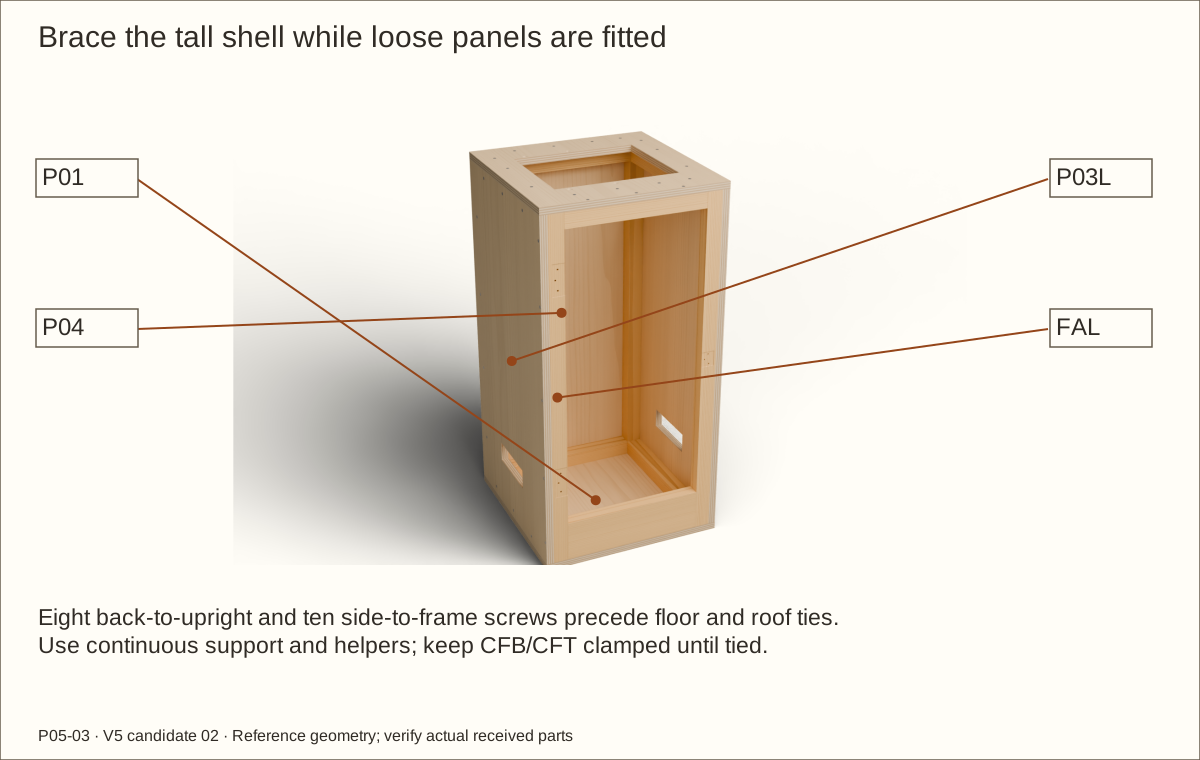
On continuous flat support, stand the sides on P01 with a helper carrying loose panels. Fit P04 between them, rear face flush to side rear edges. Clamp and brace; compare diagonals.
Fit the laminated front frame between sides with its front face flush. Fit CFB/CFT directly behind it between the side supports; keep those cross members clamped until floor and roof ties are installed.
Fit J021–J038: eight back-to-upright screws at heights 8 in (203.2 mm), 16 in (406.4 mm), 24 in (609.6 mm), 32 in (812.8 mm) and ten side-to-frame screws at 3 in (76.2 mm), 10 in (254 mm), 18 in (457.2 mm), 27 in (685.8 mm), 33 in (838.2 mm). The side-front row is 5/16 in (7.94 mm) behind FRONT. Use exact transferred receiver lines and stopped pilots.
Check before continuing: The shell is square, supported and braced with no forced joints.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Fasten the floor on broad padded support
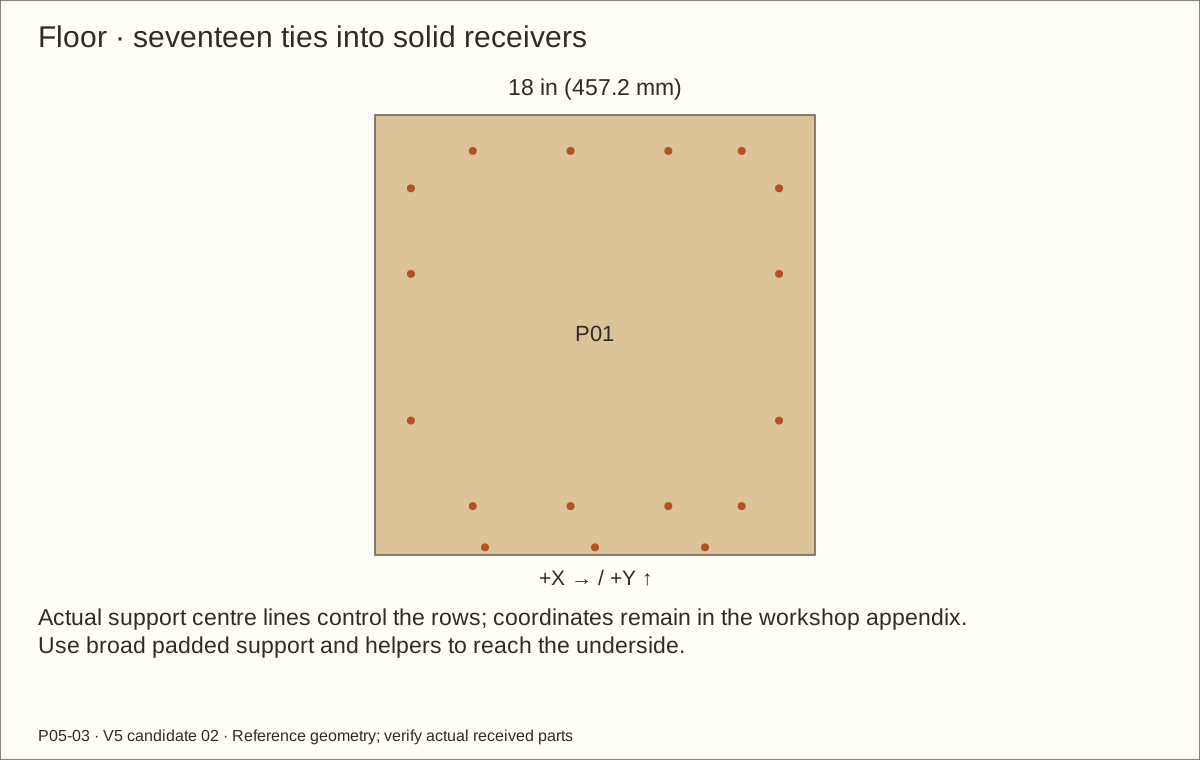
Transfer the actual side and cross-cleat centre lines onto P01 before closing the shell. Use J045–J061: six side-support, four front-cross, four rear-cross and three front-frame ties.
With helpers, support the clamped shell on a broad padded surface to access the underside. Never balance it on one narrow edge. Keep every loose member restrained while changing orientation.
Clearance-drill plywood, make stopped pilots into pine and drive only to flush. Check diagonals before final seating and mark every matched position for disassembly.
Check before continuing: The floor bears continuously and all seventeen ties enter sound receivers.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Dry-fit the removable roof
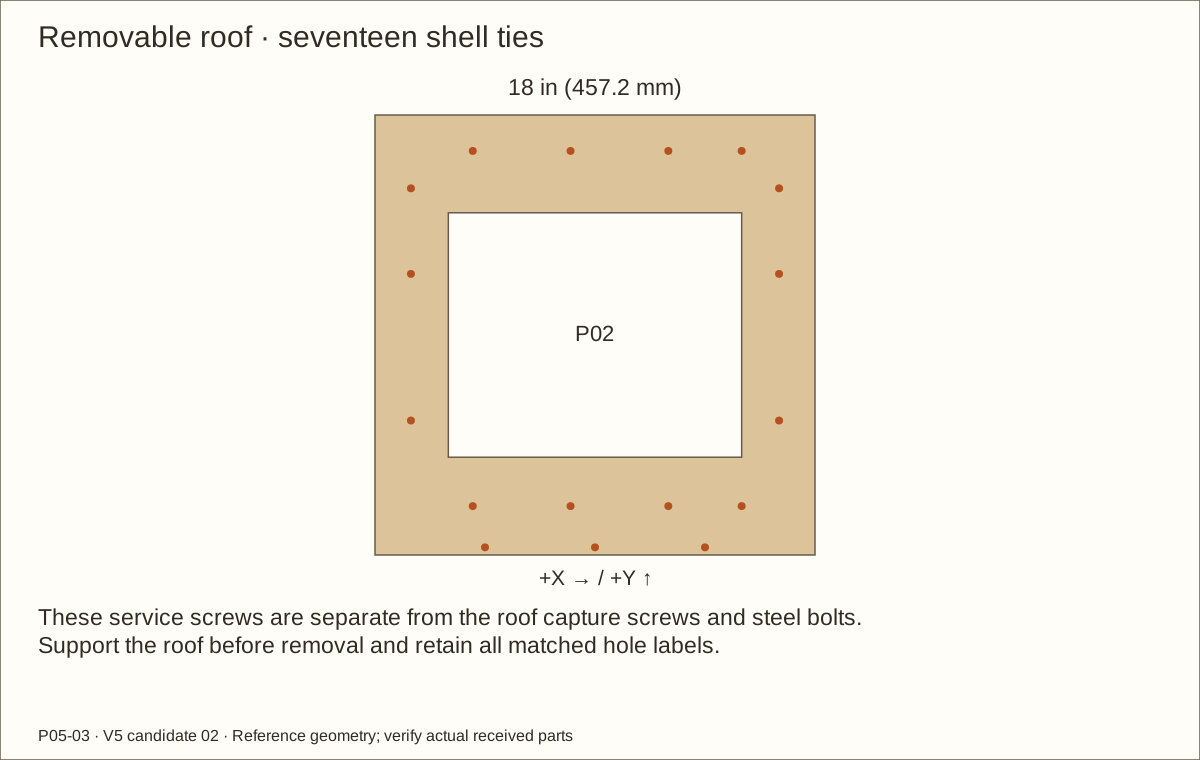
Transfer the actual support centre lines to the matching roof. Use J062–J078 with the same row families as the floor; all holes stay outside the roof opening.
Fit from above while the shell stays square and fully supported. Use actual-root-matched stopped pilots and #8 × 1 3/4 in (44.45 mm) screws flush in P02. Preserve the labels and matched holes.
Support and remove the roof again for inside capture work. Confirm it seats freely without using screws to pull bowed stock flat.
Check before continuing: The roof seats and removes cleanly; seventeen labeled service screws remain accessible.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: The kit’s rating does not rate the CBT/roof/back assembly; H08 includes the full load path.
Transfer the actual restraint bracket holes
Centre the tested preassembled bracket on CBT inside the 5 1/2 in (139.7 mm) × 1 in (25.4 mm) band. Its backing must bear directly on solid wood; veneer is omitted only beneath the actual bearing footprint.
Compare every actual shaft with the scheduled back/roof screws, retaining at least 1/4 in (6.35 mm) shaft separation. Shift horizontally only within the accepted band, then repeat the complete fit trial and record its final location.
Use the two supplied 5/8 in (15.88 mm) furniture screws and proven stopped pilots. Repeat both straight driver approaches, cable clearance and bracket withdrawal. Remove the kit for finishing; the two 1 1/2 in (38.1 mm) wall screws are not furniture screws.
Check before continuing: Actual holes and service paths are recorded before finishing.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Fit the tested spacer and cap stock
Repeat the retained cured coupon with final materials before planing Q stock. Reference Q depth is 5/16 in (7.94 mm); side widths 3/8 in (9.53 mm) and end widths 5/16 in (7.94 mm). Caps are 1/4 in (6.35 mm) thick, sides 3/4 in (19.05 mm) wide and ends 11/16 in (17.46 mm) wide.
Lay pieces against the exact viewing-opening datums. Side spacers leave 1/8 in (3.18 mm) raw pane edge float; the pane bears 3/8 in (9.53 mm) on the front door and the caps overlap it 1/4 in (6.35 mm).
Dry-fit the end caps clear of both stops: reference bare clearance 1/16 in (1.59 mm), minimum after cure 1/32 in (0.79 mm). Label each matched part and do not force a different spacer depth without revising the coupled stack.
Check before continuing: The tested stack, opening, pane float and stop clearance agree.
Parts: Q spacers, B caps; sixteen #4 × 1 in (25.4 mm) screws
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Glue Q spacers and drill removable caps
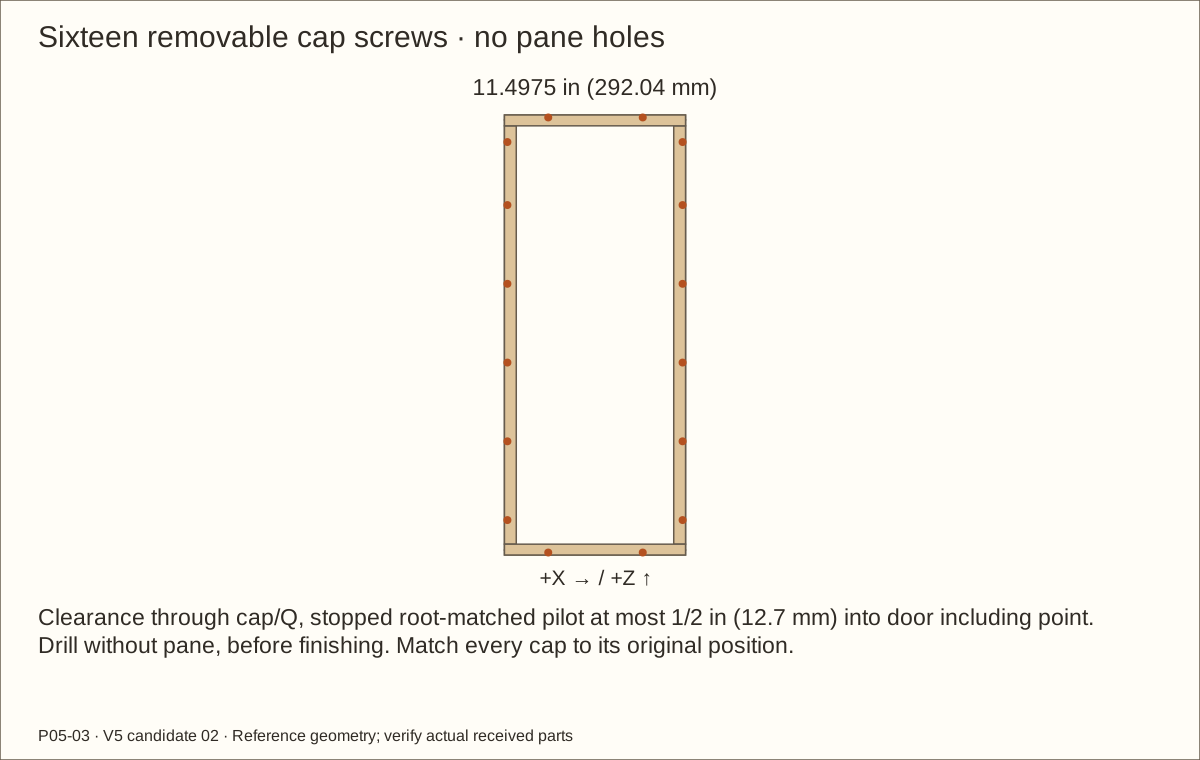
Glue the Q front lands to clean bare door wood, keeping glue out of the pocket. Clamp flat. After the glue hold, clamp the caps on their hard Q lands without acrylic.
Use J149–J164. Side rows follow Q centre lines at assembly heights 7 1/2 in (190.5 mm), 12 1/2 in (317.5 mm), 17 1/2 in (444.5 mm), 22 1/2 in (571.5 mm), 27 1/2 in (698.5 mm), 31 1/2 in (800.1 mm); end rows use X 6 in (152.4 mm) and 12 in (304.8 mm). Transfer from the revised loose-door setup datums.
Drill 1/8 in (3.18 mm) clearance through cap and Q only, then a received-root pilot at most 1/2 in (12.7 mm) into the door including the point. Fit #4 × 1 in (25.4 mm) heads flush; nominal door engagement is 7/16 in (11.11 mm). Remove and label caps for coating.
Check before continuing: Sixteen screws pass through wood only; caps remain removable.
Required wait: At least the 24-hour unstressed glue hold before drilling or loading the spacers.
Parts: S01 and S02; six #8 × 1 1/4 in (31.75 mm) screws
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Fit lower and upper closing stops
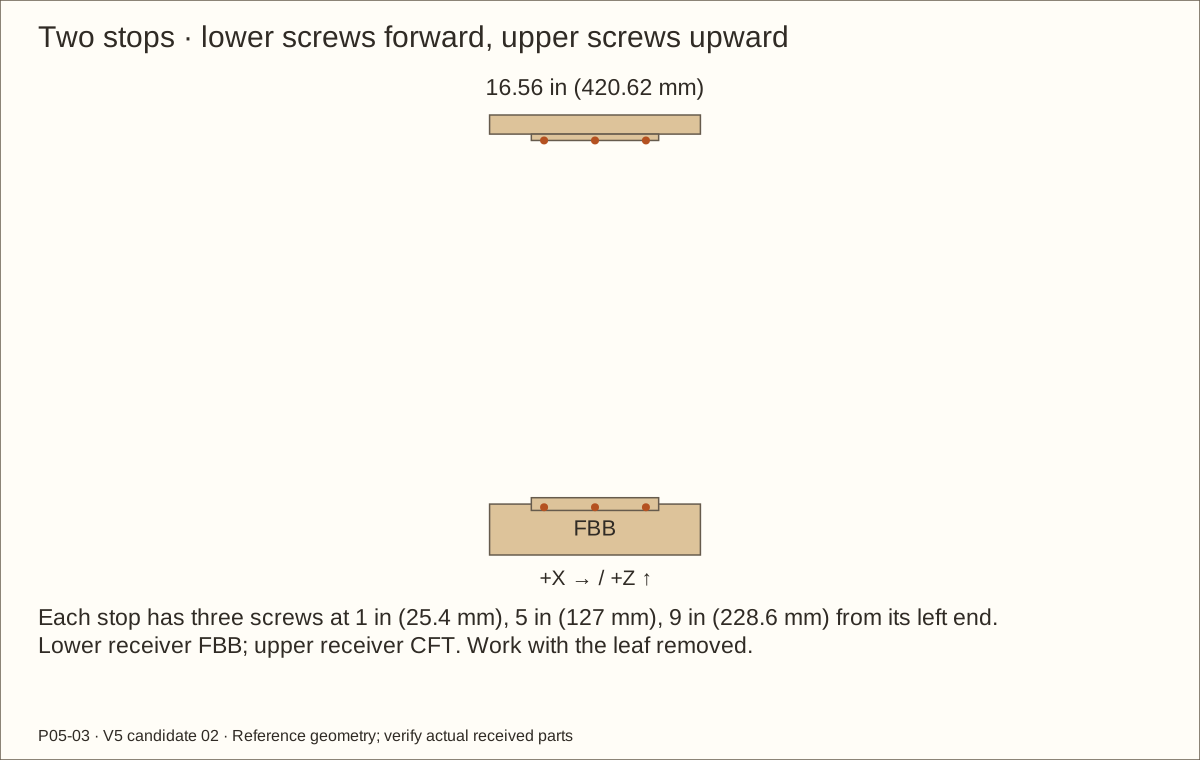
Centre the 10 in (254 mm) lower S01 with its top 1/2 in (12.7 mm) above the lower rail top and its front against FBB. Centre upper S02 with its top against CFT underside and its front aligned with the frame rear.
Mark each stop 1 in (25.4 mm), 5 in (127 mm) and 9 in (228.6 mm) from its left end. S01 screws enter toward FRONT, 1/4 in (6.35 mm) above its lower edge. S02 screws enter UP at the centre of its 3/4 in (19.05 mm) depth.
Clearance-drill the stops; blind-pilot their named receivers. Fit J143–J148 while the leaf is removed. Reference engagement is 1/2 in (12.7 mm) in FBB and 3/4 in (19.05 mm) in CFT. Check the actual leaf and cap clearance against both stops.
Check before continuing: Stops support closing without touching the retainers or forcing the pane.
Tools / setup: Vise, supported metal saw/drill, backing, files and caliper
Make the four equal hinge spacers
Cut four 3 in (76.2 mm) × 1 1/16 in (26.99 mm) full-leaf spacers from the scheduled 1 1/2 in (38.1 mm) × 36 in (914.4 mm) × 1/8 in (3.18 mm) bar using supported work and a vise. Keep the accepted thickness equal for both leaves of both hinges.
Transfer actual three-hole patterns from the accepted sample; drill clamped over backing with suitable metal bits. Deburr holes and all edges until each part sits flat with no sharp burr.
Keep at least 7/64 in (2.78 mm) measured thickness. Recheck flat bearing, accepted screw head seating and engagement; label fixed/moving and upper/lower positions.
Check before continuing: Four matched spacers reproduce the accepted hardware trial.
Parts: Two hinges, four spacers, twelve #8 × 1 1/4 in (31.75 mm) screws
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Any planing must preserve glazing bearing, screw-edge distances and the hasp’s narrow latch-edge support.
Hang the bare leaf with revised gaps
Lay the supported shell on its back. Block the door against both stops with 3/16 in (4.76 mm) bare gaps all round. Reference hinge centres are 9 5/16 in (236.54 mm) and 29 5/16 in (744.54 mm) above FLOOR UNDERSIDE.
Transfer the proven fixed-leaf seats and real hole patterns. Keep all shafts at least 1/4 in (6.35 mm) from existing shafts. If actual patterns conflict, move both hinges vertically together no more than 1/4 in (6.35 mm), retain their 20 in (508 mm) spacing and repeat the entire trial before drilling.
Fit equal spacers, twelve scheduled screws and aligned pins. Remove shims; test supported swing, stop contact and roof-on pin service. Do not bend hinges or enlarge metal holes to correct fit.
Check before continuing: The unglazed leaf moves freely and all plates have full bearing.
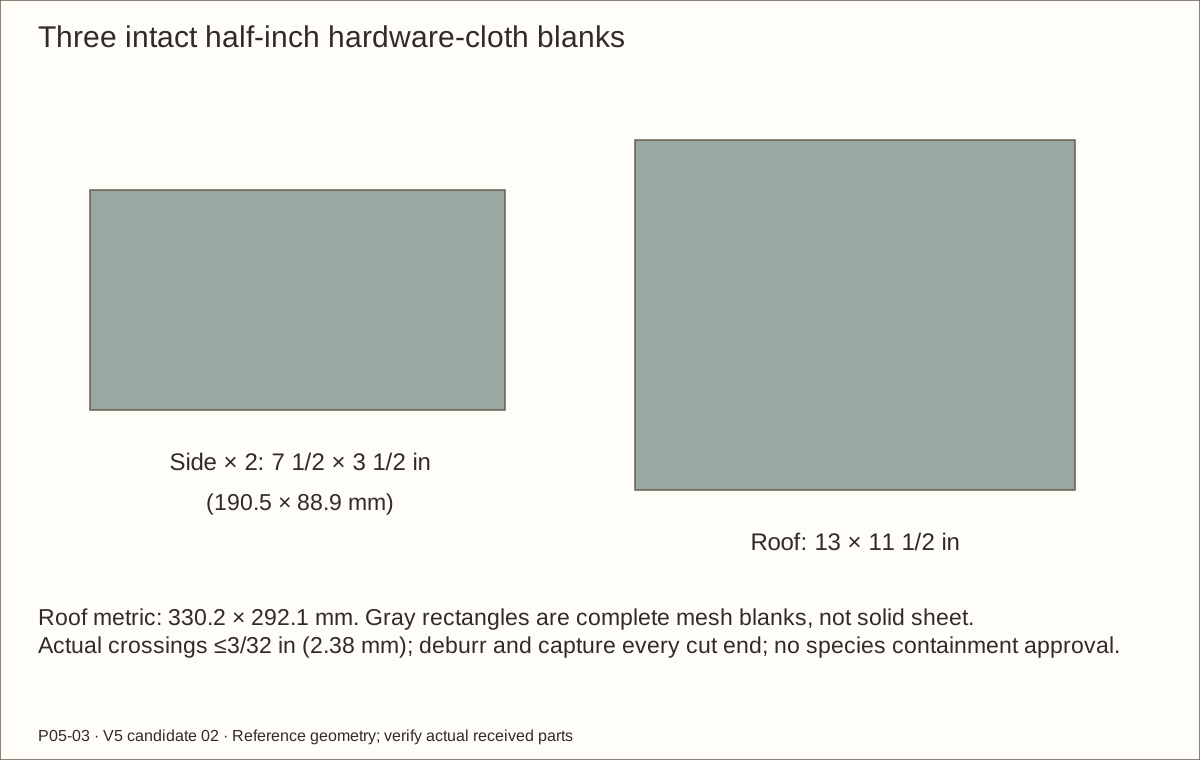
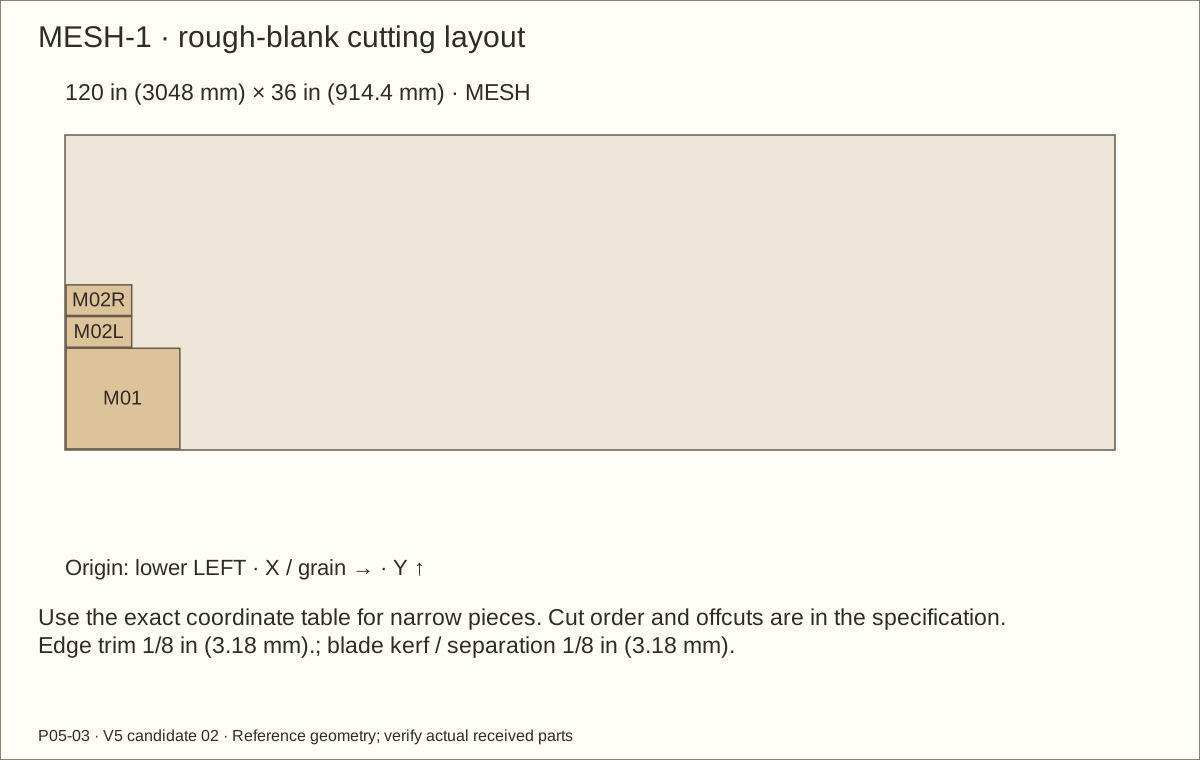
Cut two side blanks 7 1/2 in (190.5 mm) × 3 1/2 in (88.9 mm) and one roof blank 13 in (330.2 mm) × 11 1/2 in (292.1 mm). Keep the reference half-inch clear openings and intact crossings; measure actual wire and pitch.
Control each cut edge, collect every clipping and file sharp ends. Wear appropriate hand protection while handling cut mesh, keeping it away from rotating tools.
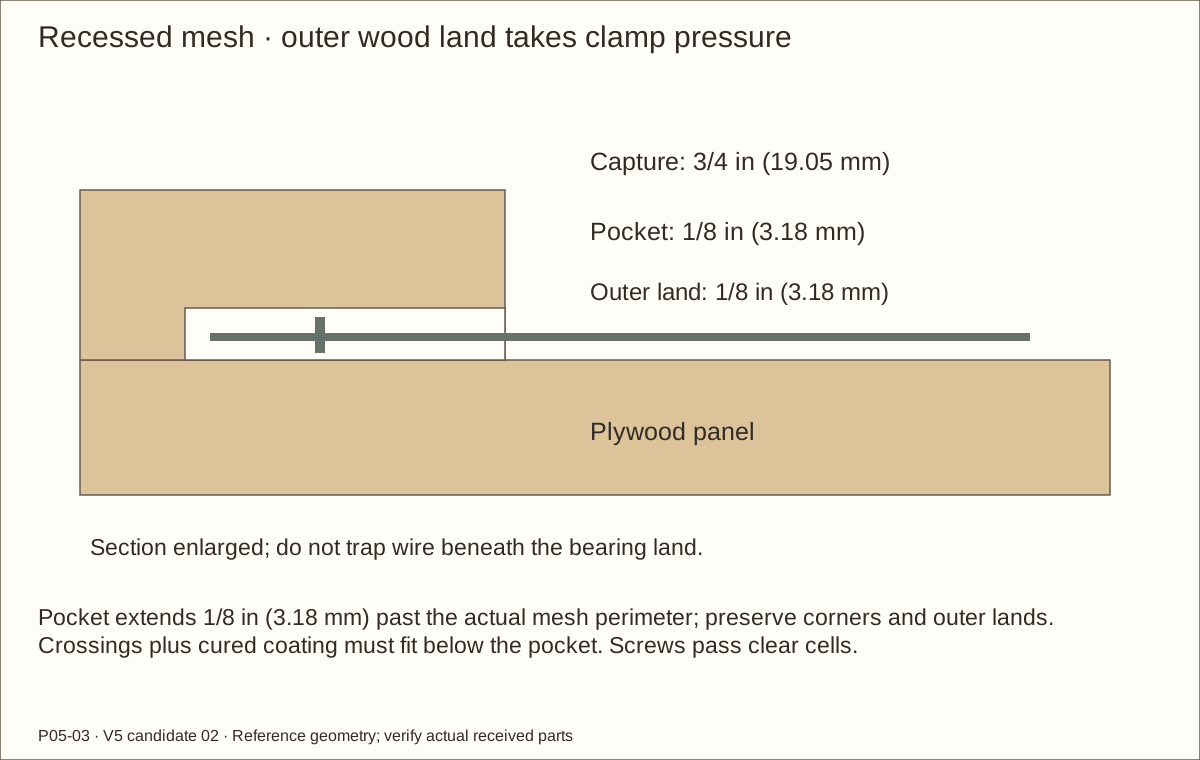
Actual crossings must be no more than 3/32 in (2.38 mm) and fit below the cured 1/8 in (3.18 mm) capture pocket. The listed aperture is not approval for any particular animal or feeder.
Check before continuing: All three labeled blanks are flat and their cut edges will be fully captured.
Use 1 in (25.4 mm) wide × 3/4 in (19.05 mm) thick battens. Centre each screen over its 6 in (152.4 mm) × 2 in (50.8 mm) inlet with 3/4 in (19.05 mm) overlap. Batten outer perimeter is 8 in (203.2 mm) × 4 in (101.6 mm) and extends 1/4 in (6.35 mm) beyond the mesh cuts.
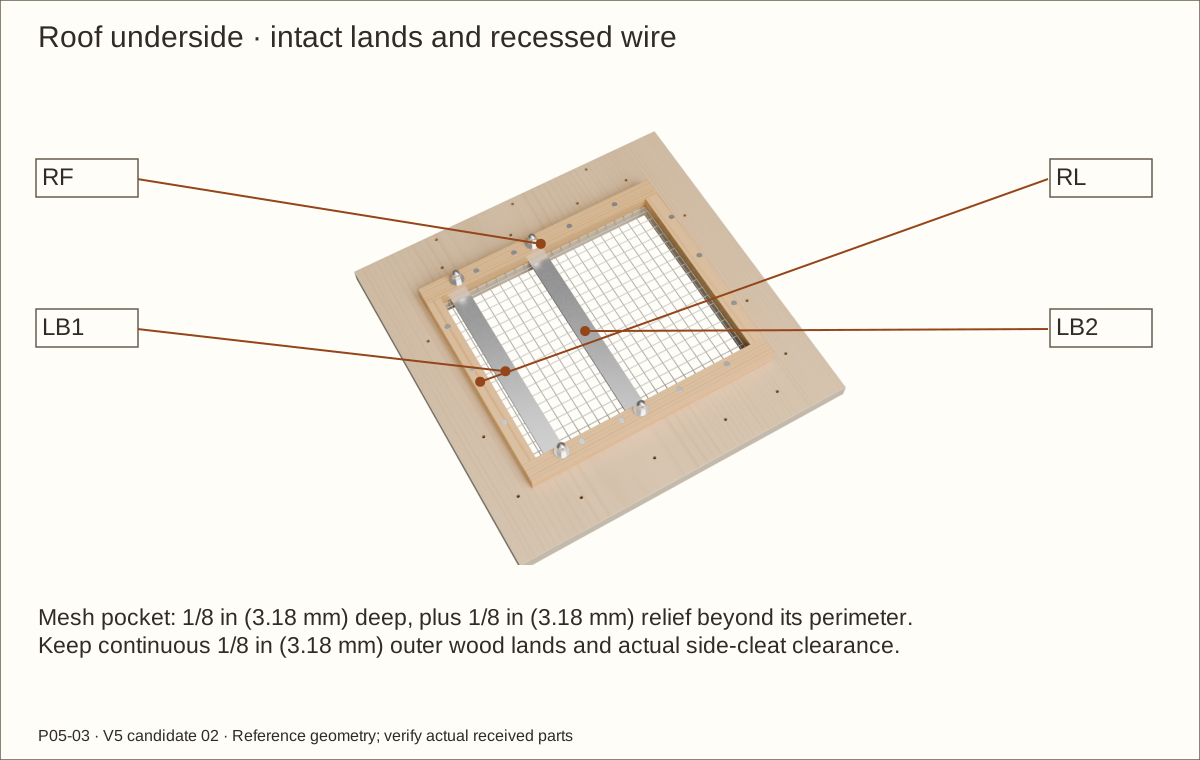
On supported wide blanks rout the panel-facing pocket 1/8 in (3.18 mm) deep over the mesh footprint plus 1/8 in (3.18 mm) around it. Preserve a continuous 1/8 in (3.18 mm) outer wood land, including corner joints, before final small-part cuts.
Dry-clamp the actual screen beneath the battens. Wood lands must sit flat with no wire beneath them. Confirm the measured crossing plus cured film fits without lifting a land.
Check before continuing: Every edge and corner has continuous solid bearing around the captured wire.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Transfer open-cell side screw paths
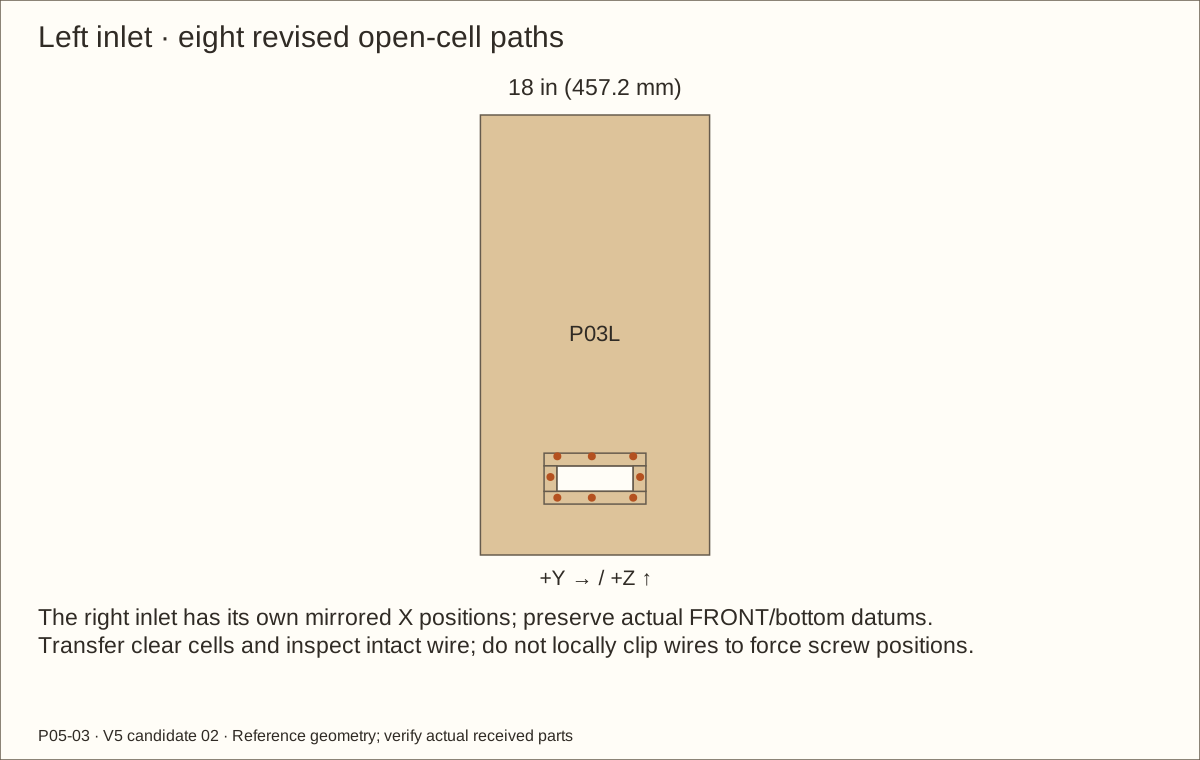
On each actual screen centre every scheduled screw in a clear cell. Use the revised J113–J128 reference positions and check the real pitch before transfer. Do not drill a wire or clip it locally to make a screw fit.
With the side panel supported inner-face-up, remove the mesh before drilling. Clearance-drill battens and make root-tested plywood pilots stopped at no more than 9/16 in (14.29 mm) including the point.
Refit the screen and eight screws per side, flush without crushing. Nominal plywood engagement is 1/2 in (12.7 mm). Inspect every land/corner and keep all cut wire inside the pocket.
Check before continuing: Sixteen open-cell paths and complete edge capture are verified.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Recess the roof capture frame
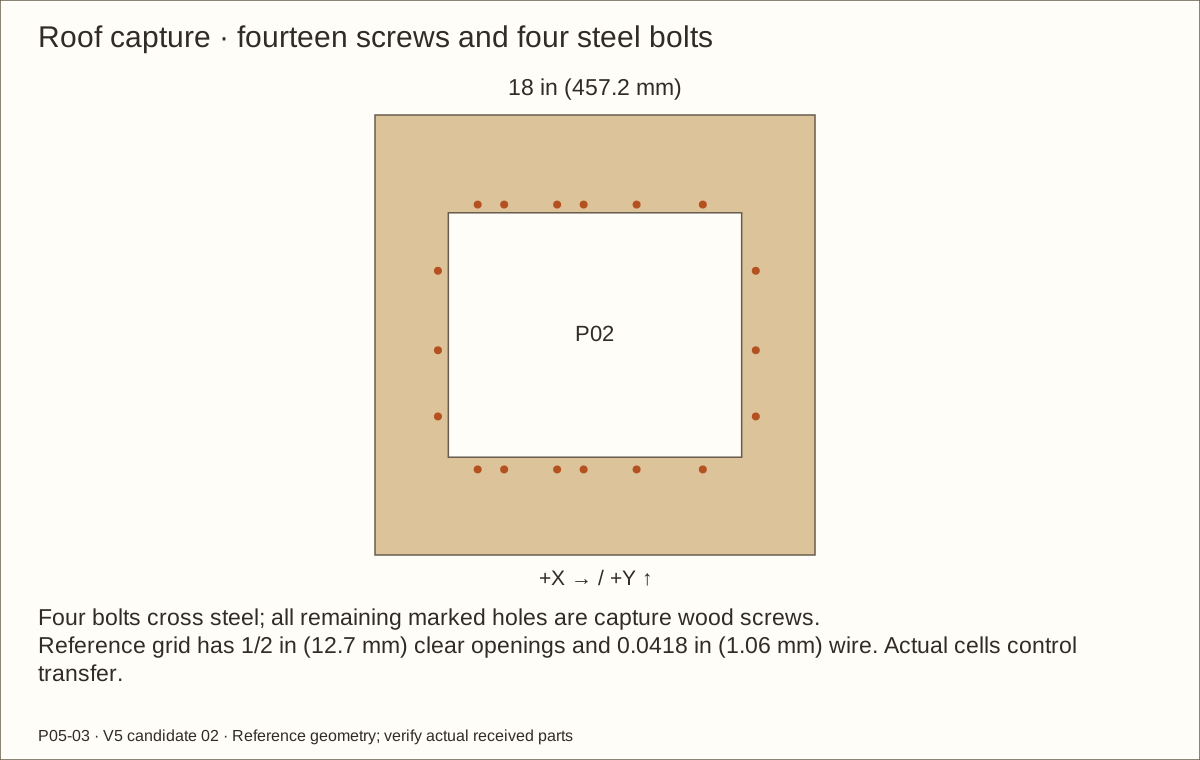
Work on the detached roof inside-face-up, retaining LEFT/FRONT labels. Centre M01 over the opening: 1/2 in (12.7 mm) overlap left/right and 3/4 in (19.05 mm) front/rear.
RF/RB are 13 1/2 in (342.9 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm); RL/RR are 10 in (254 mm) × 3/4 in (19.05 mm) × 3/4 in (19.05 mm). Rout their panel-facing pockets 1/8 in (3.18 mm) deep over the actual mesh footprint plus 1/8 in (3.18 mm) perimeter relief.
Preserve continuous 1/8 in (3.18 mm) outer lands and check cured crossing clearance. Side battens must clear the shell top supports when the roof is refitted.
Check before continuing: Roof screen and captures fit without trapped wire or interference.
35. Cut steel strips and transfer real cell centres
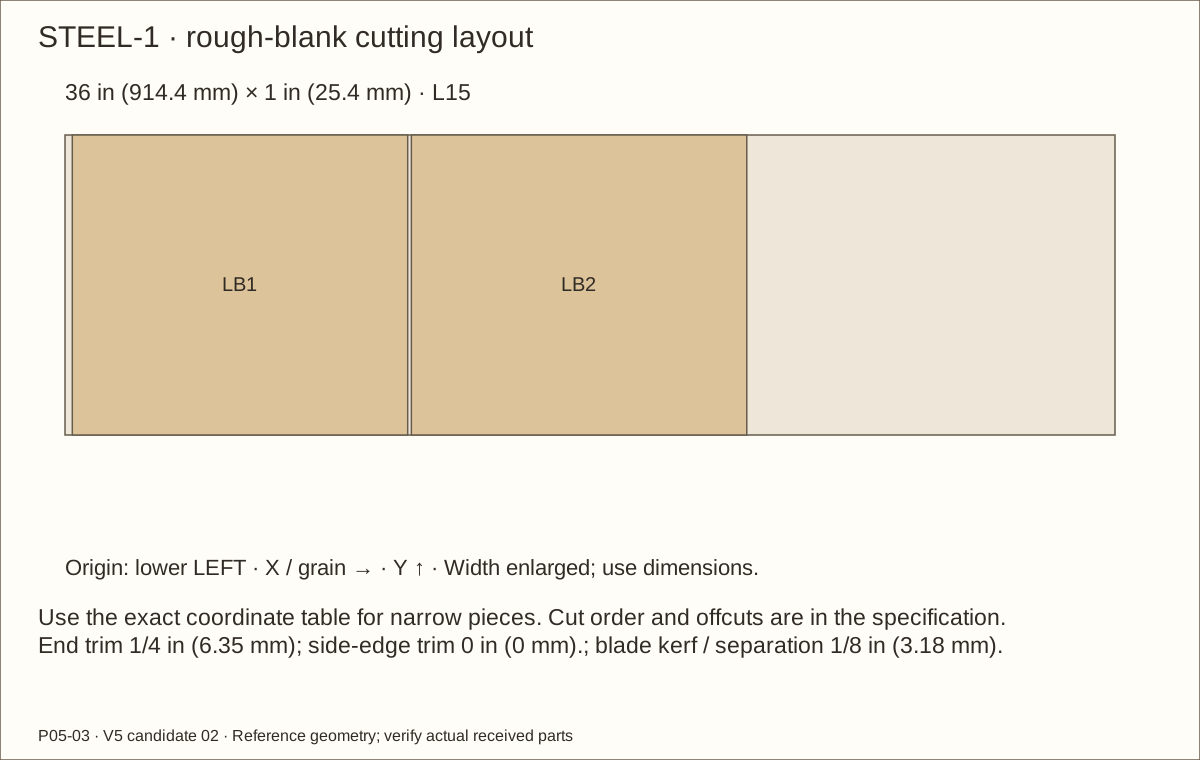
Parts: LB1/LB2; 1 in (25.4 mm) × 1/8 in (3.18 mm) steel bar
Tools / setup: Vise, supported metal saw/drill, backing, files and caliper
Cut steel strips and transfer real cell centres
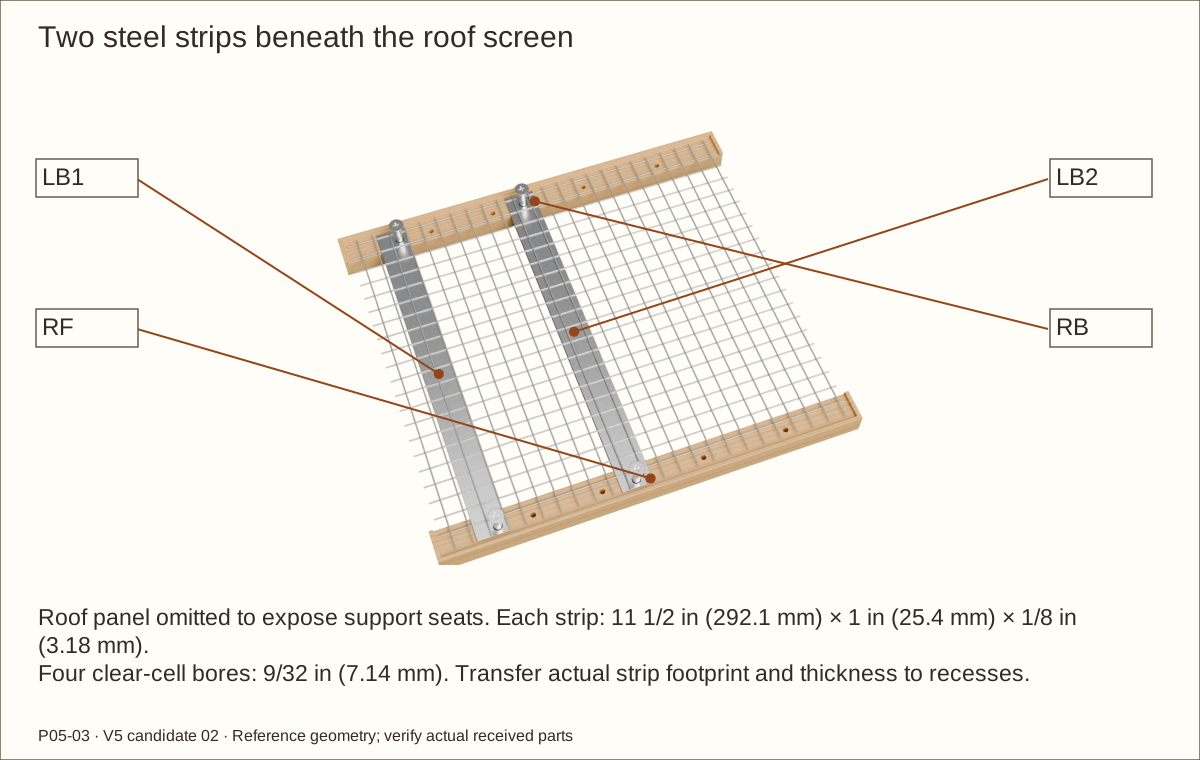
Cut two 11 1/2 in (292.1 mm) lengths from the 36 in (914.4 mm) bar; deburr every edge. Their width centres remain X 4 in (101.6 mm) and 8 1/2 in (215.9 mm) from roof LEFT, with ends Y 3 1/4 in (82.55 mm) and 14 3/4 in (374.65 mm) from FRONT.
Clamp actual cloth and strips, then transfer FOUR clear cell centres within their supported end areas. The reference bolt coordinates are X 4.2004 in (106.69 mm) and 8.5348 in (216.78 mm); Y 3 1/2 in (88.9 mm) and 14.336 in (364.13 mm). These shifted holes follow the reference grid and are not a substitute for actual mesh transfer.
Remove mesh, clamp metal over backing and drill 9/32 in (7.14 mm) clearance. Deburr both faces. Transfer the actual strip footprints to RF/RB and recess them beneath the wire by the measured steel thickness; keep more than 1/2 in (12.7 mm) solid wood below.
Check before continuing: Both strips touch the mesh underside and their four holes avoid wire.
Before you begin: H05 requires the offcut trial; H07 requires acceptance of the changed bearing and clamp force. A render does not establish connection capacity.
Countersink the four exterior roof heads
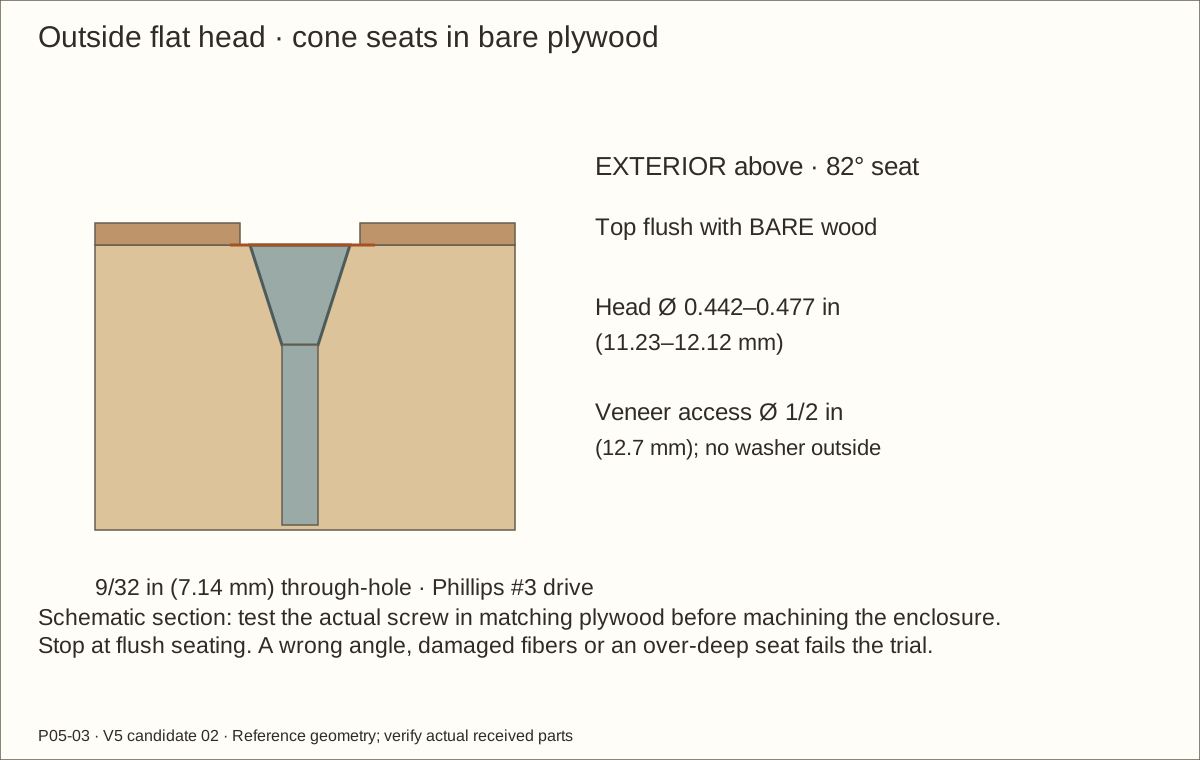
After actual open-cell transfer, separate the roof, cloth, steel and captures. Drill the four 9/32 in (7.14 mm) clearance holes through supported plywood. Use matching scrap for a complete head-seat trial before touching P02.
Clamp the bare roof on a sacrificial backing board. On the OUTSIDE face only, use an 82° countersink in shallow cuts. Stop the drill and test the actual head each time until its top is flush with bare plywood. No washer goes outside.
Published head diameter is 0.442 in (11.23 mm) – 0.477 in (12.12 mm) and head-height envelope 0.153 in (3.89 mm); the latter leaves 0.567 in (14.4 mm) of reference 0.72 in (18.29 mm) plywood. Stop at actual seating, never use that envelope as a drilling-depth target. Reject crushed fibers, voids, splitting, an oversized cone or a head sunk below the face.
Keep a 1/2 in (12.7 mm) circular access opening in the later roof veneer at each head. Test the actual Phillips #3 tool through it; veneer must neither carry clamping load nor cover a service head.
Check before continuing: All four actual heads seat flush without damage, and the exterior tool reaches each one.
37. Assemble and cover the four roof bolt sets · measure first
Parts: Four L16 flat-head screws; four L17 washers; four L18 Keps nuts; four CAPS covers
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: No torque or load rating is established. Stop if a head turns in damaged wood, the nut cannot retain the joint or a cap loosens; resolve H05/H07 before use.
Assemble and cover the four roof bolt sets · measure first
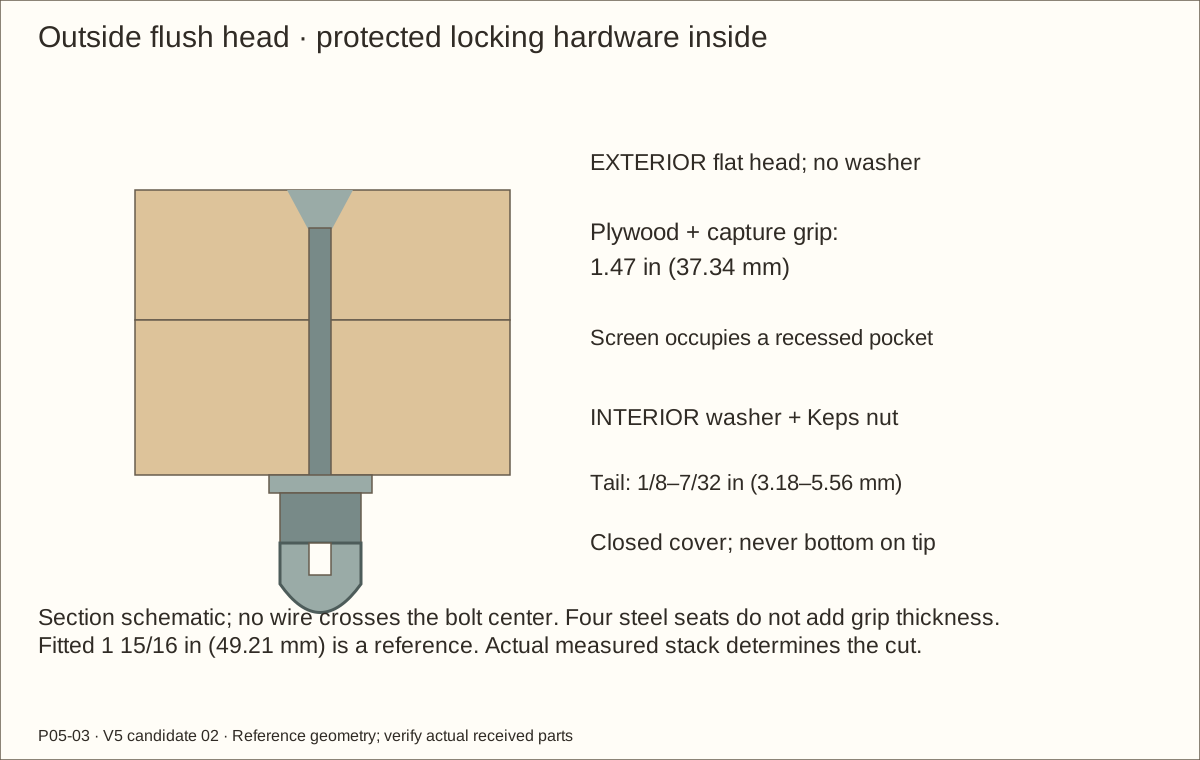
Work with the detached roof supported on the padded bench. From OUTSIDE inward: flat head in its bare-plywood seat, plywood, open mesh cell, recessed steel, capture batten, ONE washer, Keps nut and separate closed cover. Keep all wood lands flat and wire clear.
Measure the actual grip, washer and complete Keps nut. Reference grip is 1.47 in (37.34 mm), washer 1/16 in (1.59 mm) and Keps height 1/4 in (6.35 mm), but the Keps height is unverified. Fitted overall screw length 1 15/16 in (49.21 mm) includes the flat head and gives reference tail 0.155 in (3.94 mm). Use the measured stack, not this reference, to set the cut.
Require 1/8 in (3.18 mm) – 7/32 in (5.56 mm) tail beyond the fully seated primary nut, at least two complete threads after a chamfer no larger than 1/64 in (0.4 mm), and at least 1/32 in (0.79 mm) unused depth in the measured blind cap. Verify the screw has complete threads throughout the nut and cover engagement.
Check before continuing: Record the measured grip, nut height, tail, usable thread and blind-cap clearance before cutting.
37. Assemble and cover the four roof bolt sets · fit and secure
Parts: Four L16 flat-head screws; four L17 washers; four L18 Keps nuts; four CAPS covers
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: No torque or load rating is established. Stop if a head turns in damaged wood, the nut cannot retain the joint or a cap loosens; resolve H05/H07 before use.
Assemble and cover the four roof bolt sets · fit and secure
If shortening is needed, mark and remove the screw. Hold it in a vise, cut with a suitable metal saw, file and remove every burr and chip off-assembly. Protect newly exposed steel only with a supplier-accepted corrosion treatment compatible with this use; then prove clean thread fit. Never cut over the enclosure.
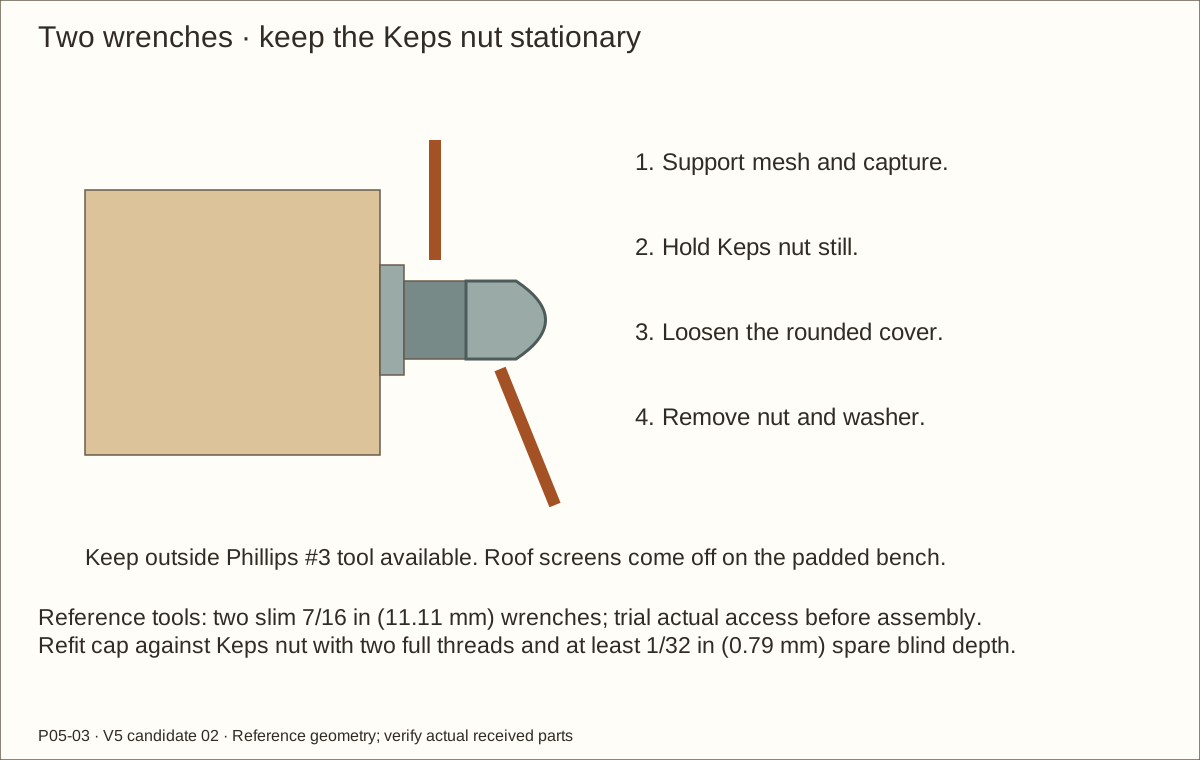
Reassemble slowly by hand, stopping if threads bind. Hold the primary Keps nut stationary with a thin 7/16 in (11.11 mm) wrench while snugging the cover with a second wrench; keep Phillips #3 at the exterior head. The cap seats against the nut without bottoming or adding wood compression. Trial the actual wrench pair and no-larger-than-3/4 in (19.05 mm) socket with the roof detached.
Check before continuing: All lands seat without crushing; primary nuts retain the connection, caps cover every sharp end, and actual tools can remove them.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Fit the roof capture screws on the bench
Use J129–J142 with the detached roof inside-up. Transfer actual open cells from the revised drawing: eight screws in RF/RB and six in RL/RR, separate from the four support bolts.
Remove screen before drilling. Clearance-drill captures, stopped-pilot plywood at no more than 9/16 in (14.29 mm) including the point and trial actual head seating. Refit mesh and screws flush.
Inspect all lands, wire ends, strip bearings, bolt engagement and covers. Refit the roof with its seventeen shell screws; verify side capture clearance and free roof removal.
Check before continuing: The complete roof assembly seats without obstructed drivers or trapped mesh.
Parts: N305-979; seven #10 × 5/8 in (15.88 mm) screws
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: A padlock is optional secondary security and is not included.
Fit and operate the swivel hasp
Block the door at the accepted gaps. Reference swivel centre is X 14.78 in (375.41 mm) from LEFT and Z 19 in (482.6 mm) above FLOOR UNDERSIDE. Transfer the actual offcut-proved hardware; never use the image as a drill template.
Trace the fixed FAR base and its 1/32 in (0.79 mm) face seat. Check full support of both plates and every shaft against frame, door and glazing screws before stopped pilots. Fit three fixed-base and four moving-plate screws with at least 1/2 in (12.7 mm) rear wood cover.
Turn the swivel, swing the flap completely clear and open through the full arc. Close without pulling sideways; turn across the slot to retain the flap. Grip sound wood when moving the leaf, never the acrylic or flap.
Check before continuing: Hand release and retention work without edge contact or plate rocking.
Tools / setup: Dust-controlled sanding, vacuum, lint-free cloth and ventilation
Before you begin: Resolve H03/H06 for substrate balance, bond and floor exposure before coating.
Disassemble and prepare every wood surface
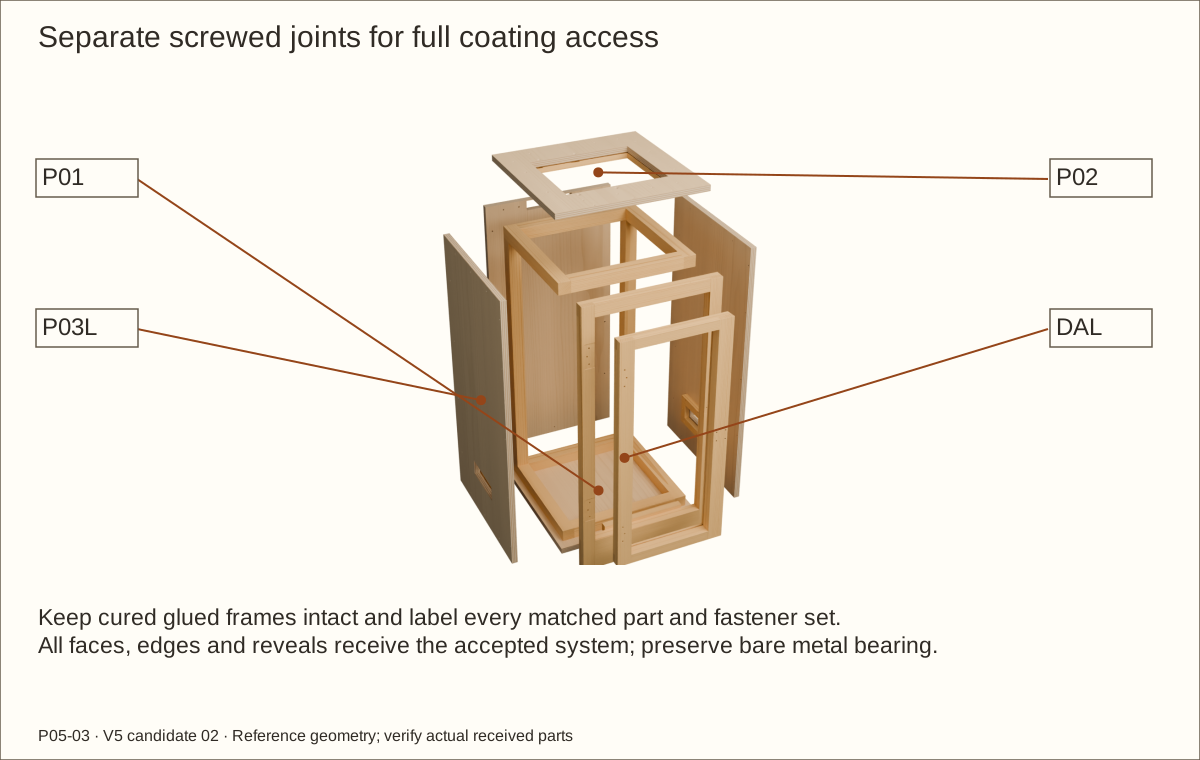
After all dry fits pass, label and remove hardware, screens, caps and glazing. Keep cured glued frames/Q spacers intact; separate screwed joints so every wood face and reveal is reachable.
Sand clean dry wood from 120 through 220 grit, vacuum and wipe with a lint-free cloth. Keep bare metal bearing seats and removable head-access areas identified; do not sand away fitted datums.
Confirm the complete coating/veneer/cleaning system, including the manufacturer’s floor-use exclusion. No acceptance of abrasion, permanent wet contact, immersion or animal exposure is implied.
Check before continuing: All surfaces are clean, accessible and correctly labeled.
Parts: Varathane 284473 satin; accepted substrate system
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Seal the accepted substrate and fully cure
Match received cans to manufacturer 284473 and seller 284473-7482. Stir, do not shake. Apply one uniform coat along grain with a quality synthetic brush at 60–90°F (15.6–32.2°C) and below 85% relative humidity, following the current label.
Coat disassembled wood faces, edges and reveals as the accepted system directs, excluding bare bond/metal seats. Reference coverage includes trial pieces, preseal, veneer topcoat and loss; buy the scheduled two-can packs and recalculate for extra coats.
Record last application time, temperature and humidity. If another coat is needed, follow the two-hour reference recoat and 220-grit sanding instructions. Inspect flatness and defects after full cure.
Check before continuing: The accepted substrate is sound and fully cured before PSA application.
Required wait: At least seven days after the final or repaired coat at 70°F (21°C), 50% relative humidity; extend for conditions/current instructions. Touch-dry and 48-hour light use are not full cure.
42. Trial veneer adhesion and balanced construction
Parts: Received species, backing/PSA and cured matching offcuts
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Appearance textures do not certify adhesion, species, color or delivered grain.
Trial veneer adhesion and balanced construction
Acclimate and prepare the veneer under supplier-confirmed conditions. Apply the full wood/backing/adhesive/sealer/topcoat system to matching samples with the required pressure and dwell.
Measure the complete cured addition: reference 0.0305 in (0.77 mm), maximum 0.046 in (1.17 mm). Check bond, edge lift, flatness and the supplier’s balancing requirement through conditioning and the proposed cleaner trial.
Repeat the finished door/hinge/hasp and glazing samples. If a backer or new coating thickness is required, revise both dimensional and purchasing schedules before final application.
Check before continuing: Supplier acceptance and actual sample results are recorded.
Required wait: Actual supplier acclimation, pressing and dwell; no invented universal wait.
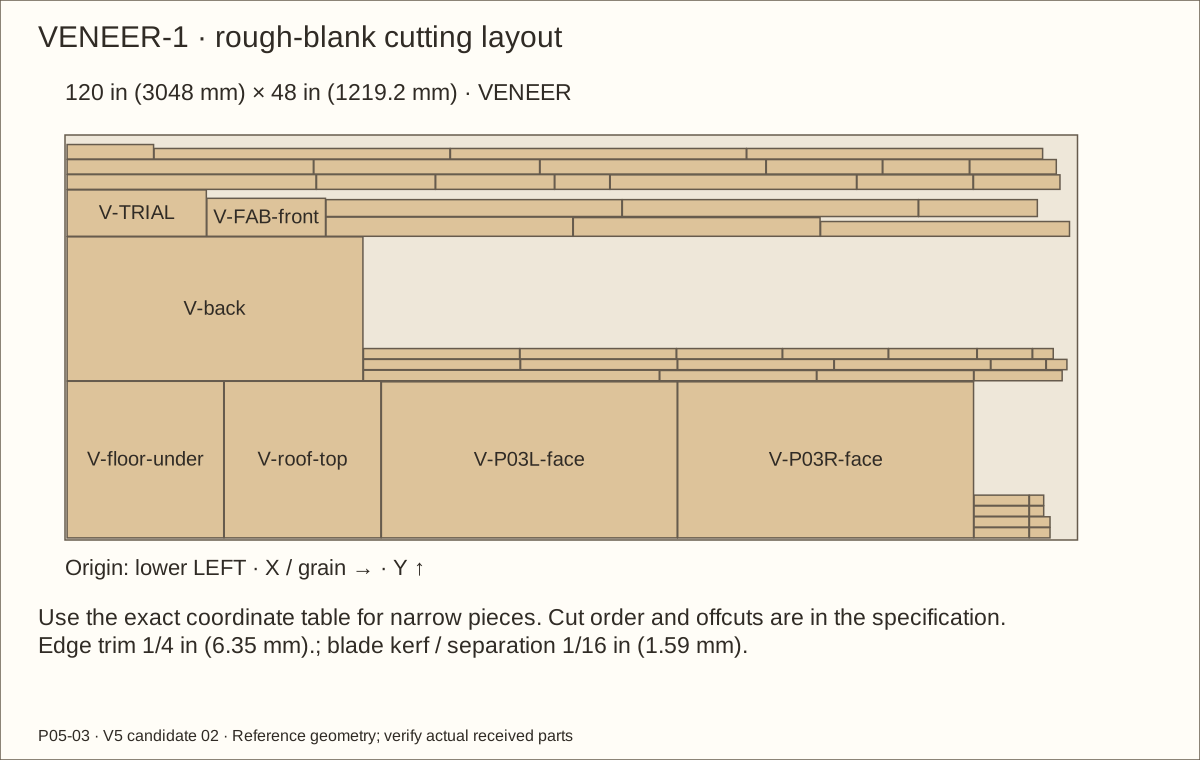
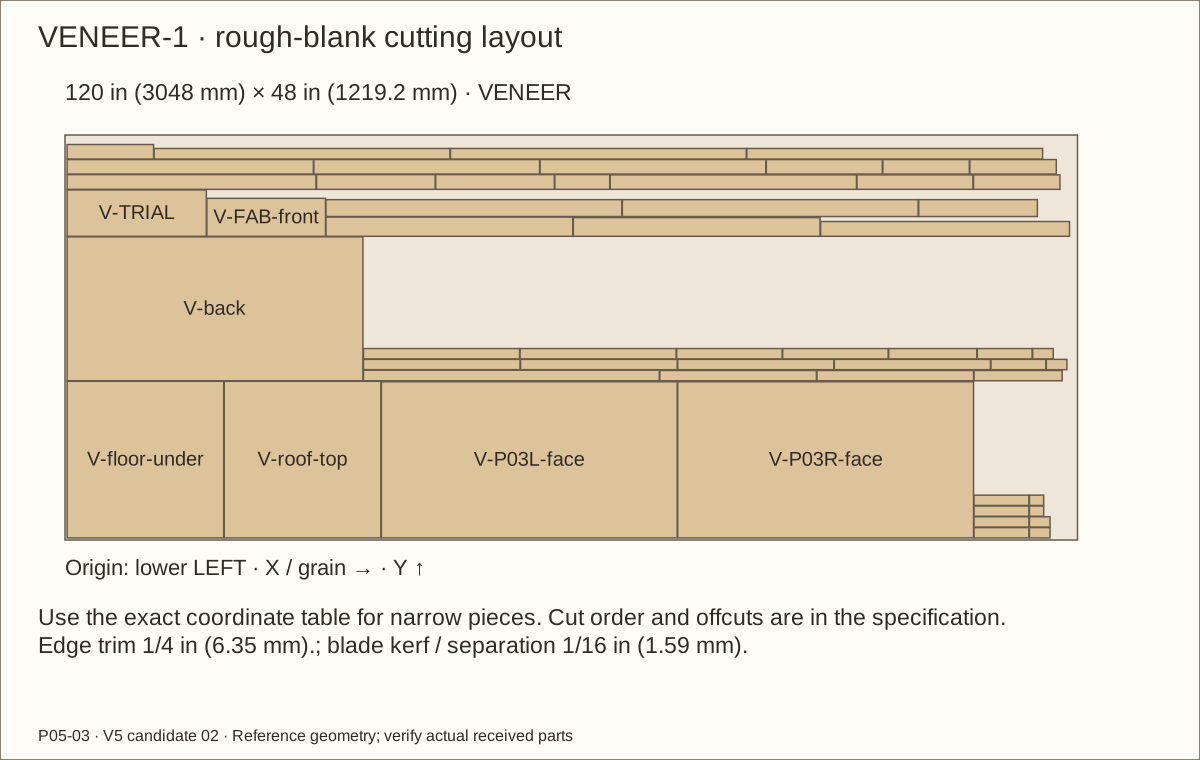
Follow VENEER-1 and its exact coordinate table, including the separate trial blank. Keep every skin ID, grain arrow and parent part together. Rough blanks include trimming allowance.
Use a sharp knife, straightedge and cutting board; make supported controlled passes. Cover the roof, underside, outer faces, plywood edges and opening reveals with separate pieces.
Dry-arrange neighboring grain and preserve all door, roof and maintenance seams. Do not wrap one sheet across an opening or join moving assemblies.
Check before continuing: All fifty-four skins and the trial blank are identified and fit their allocation.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
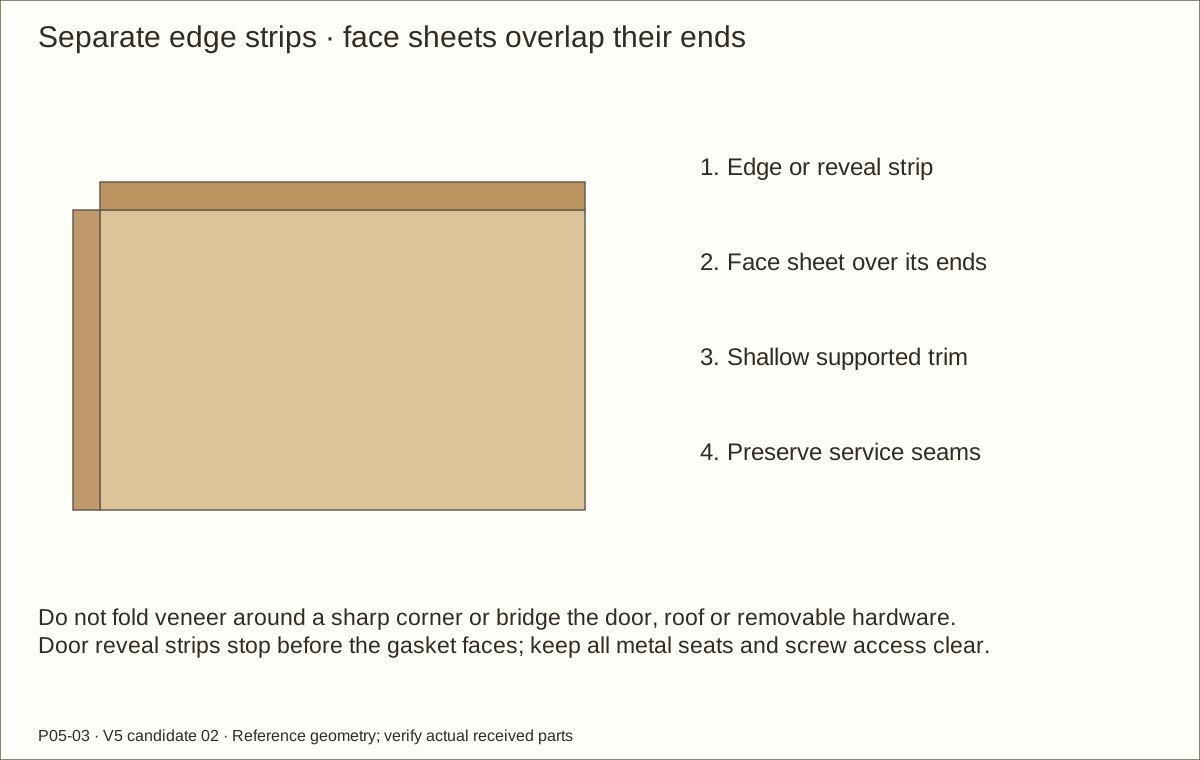
Apply edge and opening-reveal strips first
Apply each strip to the accepted cured substrate using the supplier’s pressure tool and method. Work progressively to exclude bubbles; avoid stretching thin veneer around sharp corners.
Trim shallow supported passes flush to the intended boundary. Face skins overlap the ends of the edge strips. Keep the rear door gasket lands unveneered.
Preserve the window’s actual bare bracket-bearing seat, all hinge/hasp seats, screw-head service circles and interior washer bearing seats. Keep material away from pins, holes and moving seams.
Check before continuing: All visible raw edges are covered while bearing and service paths remain usable.
Required wait: Supplier-confirmed dwell before the next finishing or assembly step.
Parts: Roof, floor underside, sides, back, fixed frame and door
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Apply the matching exterior face skins
Apply the named face pieces with physical grain direction matching the dry arrangement. The roof and front edge receive the same chosen species as the side faces; no bare plywood edge remains visible.
Trim each removable assembly independently. Leave the screw-access circles and actual metal seats open; veneer must not carry bolt/hinge clamping pressure or bridge service seams.
Check bubbles, bond, flush edge joints and flatness in raking light. The finished door must retain at least 1/16 in (1.59 mm) closed reveal around its whole perimeter; reference maximum-stack clearance is 0.0955 in (2.43 mm).
Check before continuing: The exterior is uniform, flat and independently serviceable.
Required wait: Supplier-confirmed adhesive dwell before topcoating.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Topcoat and record the final full cure
After the accepted PSA dwell, apply the compatible finish along the grain. Check narrow reveals and corners for runs, and all removable seams for bridges.
Follow the received coating instructions, adding coat area to the allowance if another coat is needed. Sand 220 grit before a further coat and use the stated recoat timing under actual conditions.
Record the final or repaired coat time and conditions. Inspect bond, flatness and clearance again after full cure; odor or touch-dry checks cannot replace the required wait.
Check before continuing: The complete accepted exterior is cured, flat and free of lifted edges.
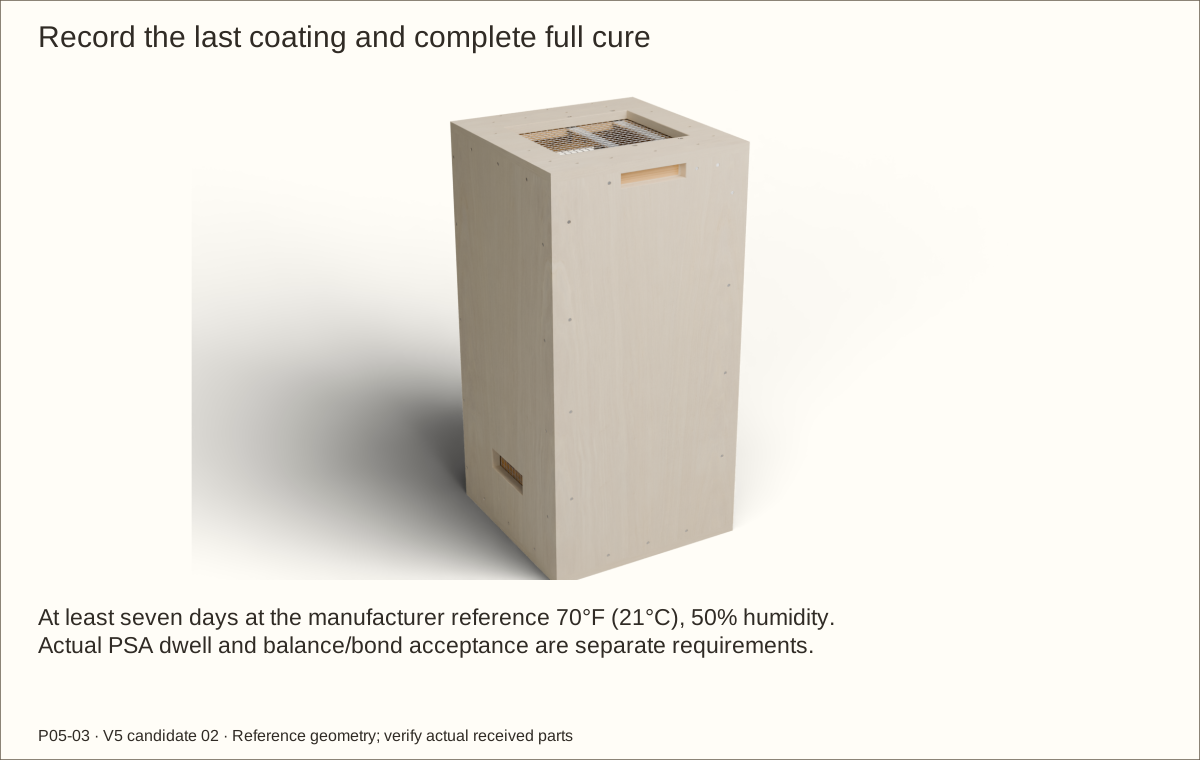
Required wait: At least seven days after the last coat at the manufacturer’s reference 70°F (21°C), 50% relative humidity, longer as required.
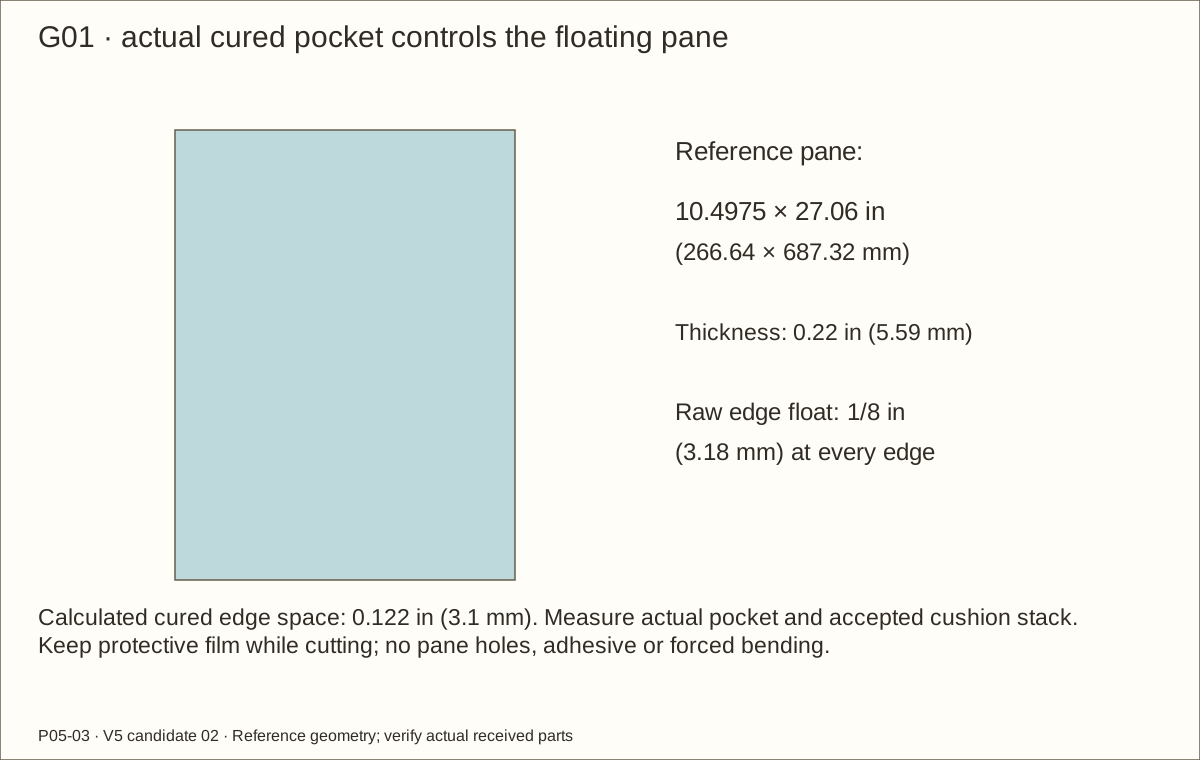
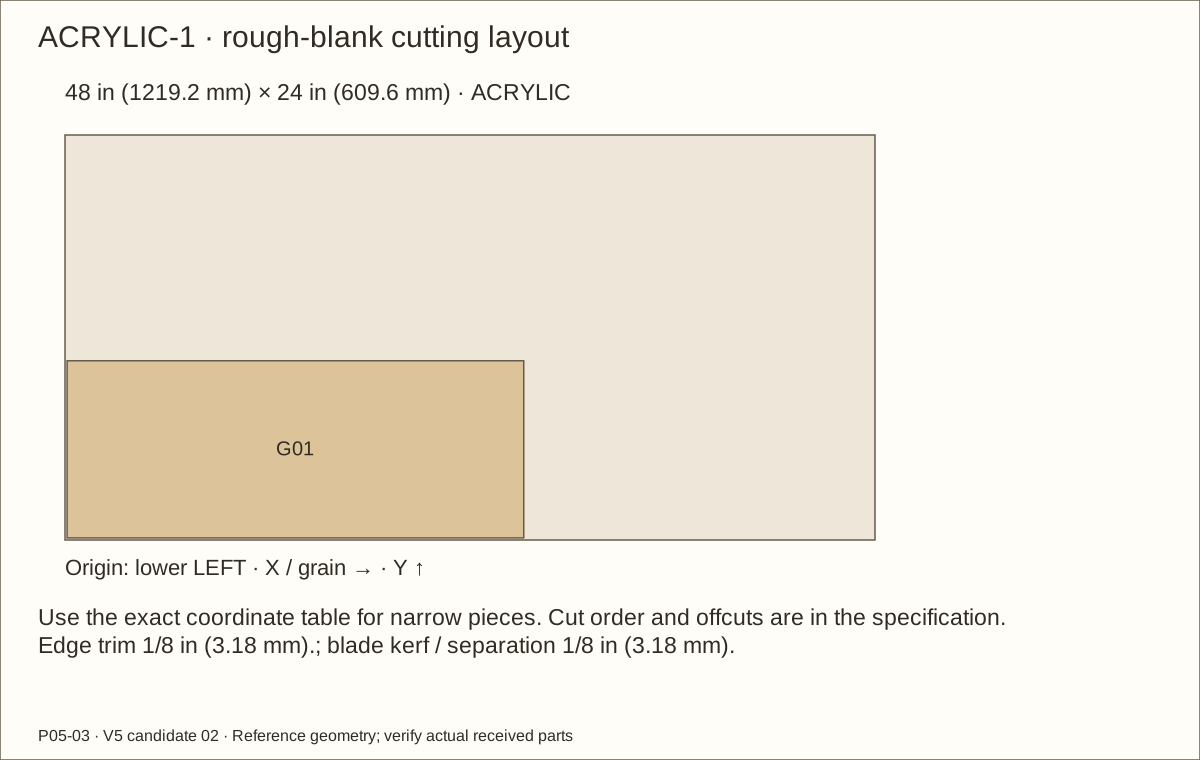
Measure the cured pocket at room temperature. Reference pane is 10.4975 in (266.64 mm) × 27.06 in (687.32 mm) × 0.22 in (5.59 mm); raw edge allowance is 1/8 in (3.18 mm), calculated 0.122 in (3.1 mm) beside each coated edge. Use the actual accepted stack and opening.
Retain protective film during cutting. Use a supported guided saw and sharp acrylic-suitable blade with backed edges and controlled feed, following the sheet maker’s fabrication guide. Do not force score-and-snap at this thickness.
Deburr without losing the edge allowance, clean compatibly and dry-fit freely. No holes, adhesive or forced bending are used to secure the pane.
Check before continuing: The pane lies flat with free expansion edges and no chips or cracks.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Cut both plain EPDM rings
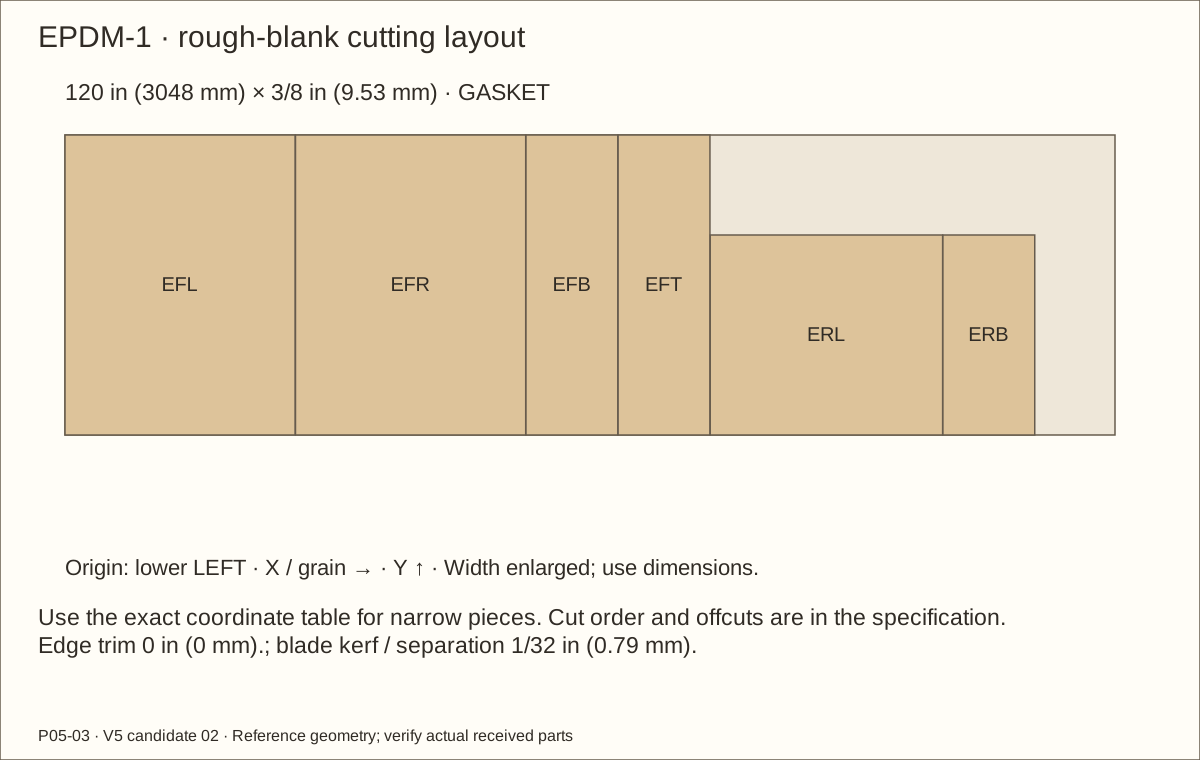
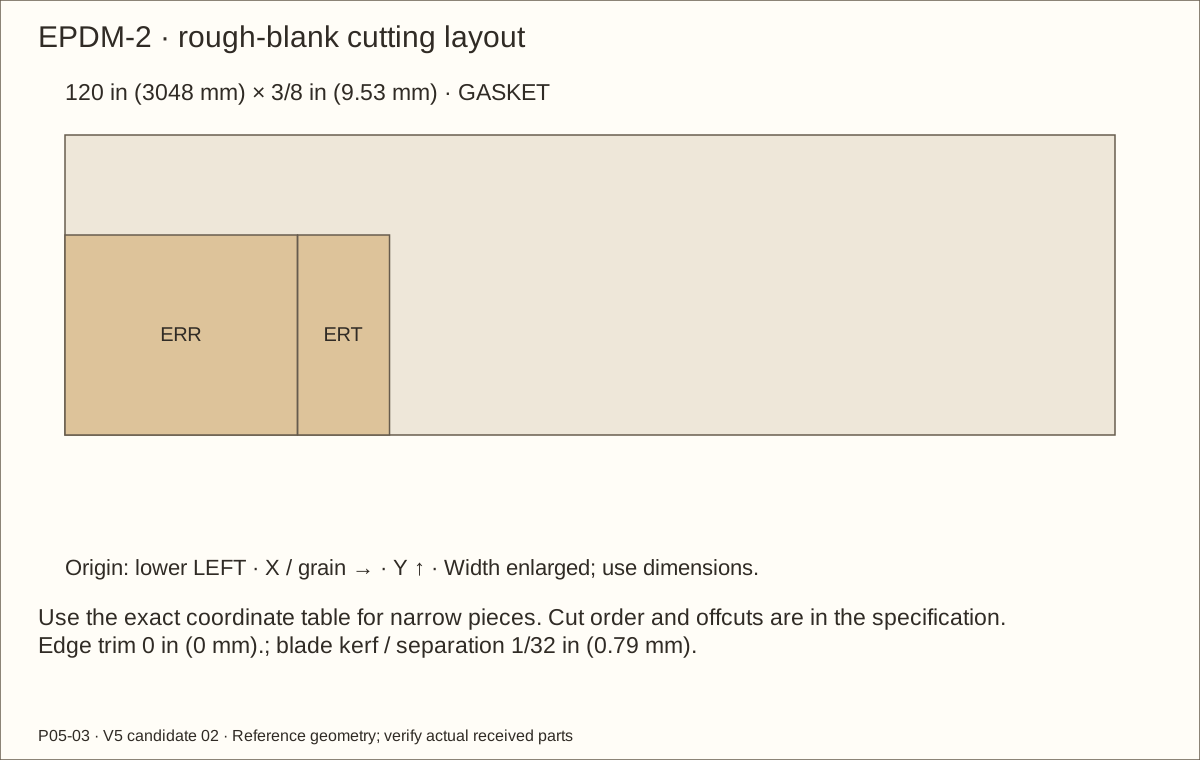
From two plain 120 in (3048 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm) strips, cut EACH ring’s two horizontal lengths to 10.4975 in (266.64 mm). Front vertical lengths are 26.31 in (668.27 mm); rear vertical lengths are 26.56 in (674.62 mm).
Keep the front ring 3/8 in (9.53 mm) wide; trim the rear ring to 1/4 in (6.35 mm) wide. Total length is 147.73 in (3752.34 mm) before cutting loss. Label every piece and butt corners without overlap.
Place strips unbonded as in the accepted sample; no adhesive touches acrylic. Recheck actual thickness, contact compatibility and the fully cured pocket before final capture.
Check before continuing: Two correctly sized plain rings lie evenly with no overlapping corners.
Parts: Matched shell, screens, strips and covered bolt sets
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Reassemble the cured shell and roof
Follow the matched shell labels on full padded support. Do not bridge seams with veneer or coating; keep head access and all metal seats clear.
Refit the screens and steel with four flush exterior flat heads and one washer, Keps nut and fitted blind cover per connection inside. Repeat the actual head-seat, open-cell, tail, thread and cap-clearance checks from the earlier pictured roof operations.
Use two thin wrenches to keep the primary nut stationary while snugging the cover. Refit the supported roof with its seventeen separate shell screws and prove removal remains free.
Check before continuing: The cured shell is square, supported and serviceable.
Parts: Door, two EPDM rings, G01, Q spacers and B caps
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Do not machine a new pocket or guess a shim to force a failed actual stack.
Capture the pane on a padded bench
Lay the door front-down on a clean padded level bench. Place the front ring, centre the pane with equal edge float, then position the rear ring and four caps.
Fit all sixteen #4 screws progressively and evenly by hand until caps seat on Q hard lands. Compare with the accepted coupon; no extra torque is used to pressure or bend the pane.
Check both faces for bow, all edges for movement space and carefully support/turn the leaf to check rattle. Remove protective film when clean assembly is ready. Correct displaced strips or raised lands before proceeding.
Check before continuing: The pane is flat, quiet and removable without destroying the leaf.
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Digital fit does not establish hinge load capacity.
Hang the glazed leaf and check final movement
With helpers carrying the complete glazed leaf, align knuckles and insert the lower pin first, then upper. Never lift by acrylic or hammer a misaligned pin.
Release swivel/flap and check the complete 100° swing. Close against both stops; require at least 1/16 in (1.59 mm) actual perimeter reveal and 1/32 in (0.79 mm) retainer-to-stop clearance. Inspect plate bearing and every screw seat.
Repeat roof-on pin withdrawal, leaf removal and reinstall under controlled support. Refinish any repaired wood and complete the full cure again before use.
Check before continuing: The actual finished leaf opens, secures and removes freely.
Parts: Proved kit, CBT holes and documented stud-wall connection
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: The kit’s advertised rating is not a rating of this enclosure or its supporting furniture.
Install the supported tall-shell restraint
Refit the preassembled furniture bracket directly to the accepted bare CBT seat with its two 5/8 in (15.88 mm) screws. Confirm firm seating, both driver paths and bracket removal with the roof on.
Place the whole finished base on rated continuous level support. Identify sound wood studs and concealed services before the documented wall attachment; verify actual covering thickness, screw engagement and cable reach. Drywall alone is not a receiver.
Use the kit’s two 1 1/2 in (38.1 mm) screws only for its documented wall connection. Seat both clevis/cotter retainers, keep cable at least 1/8 in (3.18 mm) from recess edges and preserve inspection access. Other wall types need their own documented attachment and review.
Check before continuing: Actual support, wall connection, cable route and full load path are accepted.
53. Qualify optional equipment on the left supports
Parts: Actual fixture, bulb, controls and thermal plan
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Internal equipment is only an alternative when its maker permits that guarded mounting; this guide selects no animal or lamp.
Qualify optional equipment on the left supports
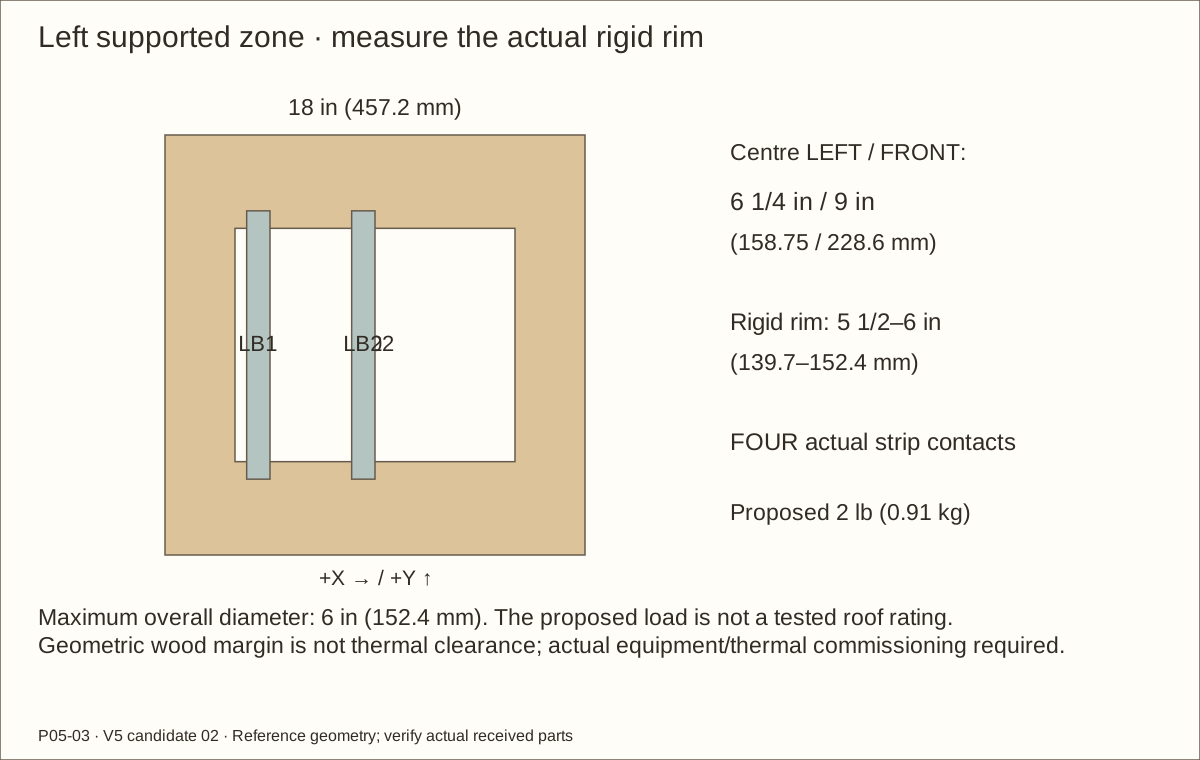
For permitted screen-top placement, centre the received fixture X 6 1/4 in (158.75 mm) from roof LEFT and Y 9 in (228.6 mm) from FRONT. Require a flat rigid rim 5 1/2 in (139.7 mm) – 6 in (152.4 mm) across, overall diameter no more than 6 in (152.4 mm) and FOUR actual contacts over both steel strips through the screen.
Weigh fixture plus bulb: 2 lb (0.91 kg) is a proposed untested limit. The Fluker Mini Sun Dome is an example to measure, not a guaranteed fit or bulb prescription. No hanging load or lamp on unsupported mesh.
Keep the roof beyond X 9 1/2 in (241.3 mm) free of heat fixtures; provide shade and measure the real temperature gradient. The nominal geometric wood margin is not thermal clearance. Follow exact maker clearances and keep heat off wood, finish, acrylic and cable.
Check before continuing: Actual fixture fit, support and thermal conditions have documented acceptance.
Parts: Supported restrained shell and species-specific equipment plan
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: This indoor moderate-humidity shell has no immersion, species or measured ventilation approval.
Commission the empty enclosure
Inspect all surfaces for sharp wire, exposed points, loose parts, cracked wood and incomplete finish. Keep dry substrate no more than 3 in (76.2 mm) above the finished floor; the reference clear inlet band above it is 2.0275 in (51.5 mm).
Keep furnishings and outside obstructions at least 2 in (50.8 mm) clear of both inlets and preserve the roof airflow path. Select controls, probes, lighting and furnishings for the intended species and measure conditions empty before occupancy.
Record prototype construction, physical stability/load/service tests, environmental measurements and qualified review separately. Resolve H01–H08 and animal/feeder containment before use. Keep wet areas in separate removable leakproof containers.
Check before continuing: Every commissioning record and receiving hold has a clear disposition.
Parts: Supported empty enclosure and matched tools
Tools / setup: Tape, square, pencil, clamps and the tools named in the operation
Before you begin: Use only accepted cleaners; inspect bonds, corrosion, cushions and fasteners after moving, cleaning or equipment changes.
Service the roof, screens, pane and restraint
Relocate the animal to suitable temporary housing, disconnect/cool equipment and empty the enclosure. Keep the full base supported. Hold the roof while removing its seventeen screws and lift the complete assembly.
Remove the supported leaf by upper then lower pin. On a padded bench remove sixteen cap screws, caps and rings, then lift the floating pane. Control loose mesh before removing capture screws or roof bolt sets; protect sharp ends.
With the roof detached on a padded bench, hold each exterior flat head with Phillips #3. Hold the inside Keps nut still with one thin 7/16 in (11.11 mm) wrench and loosen its cover with a second wrench. Only then remove the nut and washer while supporting captures, steel and sharp mesh. Refit and repeat the measured tail, full-thread, cap-clearance and flush-head checks.
For restraint service, keep the shell supported, release the wall end, remove both furniture screws and bring the bracket outside before removing its clevis. Refit in the proved order and repeat all bearing, tail, gap, closure, restraint and commissioning checks after service.
Check before continuing: Maintained assemblies return to their checked condition before reuse.
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
Four own-build 23 3/4 in (603.25 mm) × 47 3/4 in (1212.85 mm) project-panel layouts. Actual thickness reference 0.72 in (18.29 mm); use physical offcut gauges for dependent dimensions. Inspect measured sheet dimensions before cutting.
L51244618 Needed 7; 1 per package; buy 7 package(s)
Separate numbered boards for frame, door, 3/4 in (19.05 mm) parts, spacers, caps, upper stop and dedicated trials. Plane each long wide blank to its listed thickness before ripping; conservative purchases preserve safe feed length.
Ten solid 1½-inch square-pine cleats on two exact kerf-aware layouts. Fit between actual panels and members.
Materials and hardware · continued
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
21232102 Needed 1; 1 per package; buy 1 package(s)
Own un-drilled reference 10.4975 in (266.64 mm) × 27.06 in (687.32 mm) × 0.22 in (5.59 mm) pane. Exact lengths follow actual opening and 3/8 in (9.53 mm) bearing, with 1/8 in (3.18 mm) raw edge float. Do not round mating cuts.
Own half-inch 19-gauge HC23610 cloth. Reference 0.0418 in (1.06 mm) wire/.5418″ pitch; actual wire and crossings ≤3/32 in (2.38 mm) must fit cured 1/8 in (3.18 mm) pockets. Transfer actual open cells; no loose clipped wire. No animal/feeder containment approval.
Two 1798A21 hinges; equal 1/8 in (3.18 mm) full-leaf aluminium spacers, minimum 7/64 in (2.78 mm), require mounting acceptance. Use twelve scheduled #8 × 1¼-inch retention screws after head/angle fit trial; reserve four inches for each pin. Do not use unknown package screws.
Materials and hardware · continued
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
Complete 11-piece Hillman9976524 kit. Its two 5/8 in (15.88 mm) furniture screws fasten directly to CBT through the access recess; two 1½-inch screws are for the documented stud-wall connection. Real bracket dimensions, hole transfer, cable route and full assembly load path remain H08. No kit rating transfers to this enclosure.
284473-7482 Needed 3; 2 per package; buy 2 package(s)
100.66 square feet including trial/loss; 3 quarts, two quart cans per pack. Full cure at least seven days under manufacturer conditions. Floor-use exclusion and complete-system acceptance remain H06.
Materials and hardware · continued
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
35053 Needed 34; 100 per package; buy 1 package(s)
Dry-fit laminate joints; exterior/heated animal exposure not approved
SCREW-RETENTION · Power Pro #8 × 1¼″ stainless flat-head wood screws Direct product listing
42487 Needed 48; 45 per package; buy 2 package(s)
Thirty mesh-batten screws and six stop screws; nominal shaft/receiver checks only Pre-drill; seat flush without overdriving; verify actual screw head on offcut
Materials and hardware · continued
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
40005 Needed 16; 100 per package; buy 1 package(s)
Sixteen cap screws; cap and spacer are clearance-drilled, threads enter door wood only Interior moderate-humidity service; dry fit received head on offcut; no pane drilling
ZUSAESR-S-25 Needed 2; 1 per package; buy 2 package(s)
Two plain 120 in (3048 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm) EPDM strips; trim rear widths to 1/4 in (6.35 mm). Two rings total 147.73 in (3752.34 mm) before kerf. No adhesive contacts acrylic. Nominal 26% deflection is a reference, not measured pressure; fully cured test piece controls pocket.
H04 · National Hardware black swivel-staple safety hasp, 3-1/4 inch Direct product listing
N305-979 Needed 1; 1 per package; buy 1 package(s)
Original hasp position retained: square-plate reference outer wood margin 0.0175 in (0.44 mm). Actual plate/holes must be fully supported. Approximate formed-profile overlap remains a digital limitation; full received-hardware release trial required.
Materials and hardware · continued
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
Buy four individual screws. 82-degree head, Phillips #3, published head diameter 0.442 in (11.23 mm) – 0.477 in (12.12 mm) and height 0.153 in (3.89 mm). Length includes head. Fit removed screw to actual grip + inside washer + Keps nut + 1/8 in (3.18 mm) – 7/32 in (5.56 mm) tail. Reference fitted overall length 1 15/16 in (49.21 mm); never shorten in the assembled enclosure. Protect cut steel after supplier-approved corrosion treatment; prove complete threads, seated cap and countersunk bearing. No exterior washer.
Materials and hardware · continued
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
Product
Model and quantity
Fit / purchase condition
L17 · Hillman 1/4-inch zinc-plated flat washers, 3/4-inch OD × 1/16 inch thick Direct product listing
270055 Needed 4; 1 per package; buy 4 package(s)
Four retained Hillman270055 washers, one inside each roof capture. Reference 3/4 in (19.05 mm) OD × 1/16 in (1.59 mm) thickness; actual measurements control the fitted screw. No exterior washer.
Four retained Hillman880483 Keps nuts; buy two packs of two. Primary retention stays inside. Actual height, tooth seating and 7/16 in (11.11 mm) wrench fit must be measured; 1/4 in (6.35 mm) height is only a reference. Hold this nut stationary while installing/removing its cover.
Four 3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm) full-leaf aluminium spacers; actual manufacturer leaf footprint controls. H01 mounting acceptance open.
Materials and hardware · continued
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
Full exterior faces, roof, edges, reveals and trial. Written balance, substrate/finish and service-environment acceptance required.
Materials and hardware · continued
Choose ONE veneer species: one 48 × 120 in (1219.2 × 3048 mm) sheet. Seven separate wide pine boards preserve safe thickness-planing length and include dedicated trials. Two solid square-pine sticks supply ten supports. Buy the calculated two-quart coating packs. Resolve H01–H08 first; no local inventory or complete affiliate cart is verified.
91875A130 Needed 4; 25 per package; buy 1 package(s)
Four retained zinc-plated 91875A130 blind covers; buy one pack of 25. Catalog thread depth 1/4 in (6.35 mm), flats 7/16 in (11.11 mm), height 15/32 in (11.91 mm). Fit 1/8 in (3.18 mm) – 7/32 in (5.56 mm) tail before at most 1/64 in (0.4 mm) chamfer, leaving at least two complete threads and 1/32 in (0.79 mm) blind clearance. Hold Keps nut with one thin wrench while snugging cover with another; no extra wood compression.
Cut list
Cut list
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
P01 · Floor
18 1/8 in (460.38 mm) × 18 in (457.2 mm)
18 in (457.2 mm) × 18 in (457.2 mm) × 0.72 in (18.29 mm)
P02 · Roof
18 1/8 in (460.38 mm) × 18 in (457.2 mm)
18 in (457.2 mm) × 18 in (457.2 mm) × 0.72 in (18.29 mm)
P03L · L side
34.685 in (881 mm) × 18 in (457.2 mm)
34.56 in (877.82 mm) × 18 in (457.2 mm) × 0.72 in (18.29 mm)
P03R · R side
34.685 in (881 mm) × 18 in (457.2 mm)
34.56 in (877.82 mm) × 18 in (457.2 mm) × 0.72 in (18.29 mm)
P04 · Back
34.685 in (881 mm) × 16.56 in (420.62 mm)
34.56 in (877.82 mm) × 16.56 in (420.62 mm) × 0.72 in (18.29 mm)
FAL · Front L stile layer A
34.685 in (881 mm) × 1 1/2 in (38.1 mm)
34.56 in (877.82 mm) × 1 1/2 in (38.1 mm) × 5/8 in (15.88 mm)
FAR · Front R stile layer A
34.685 in (881 mm) × 1 1/2 in (38.1 mm)
34.56 in (877.82 mm) × 1 1/2 in (38.1 mm) × 5/8 in (15.88 mm)
FAB · Front B rail layer A
13.685 in (347.6 mm) × 4 in (101.6 mm)
13.56 in (344.42 mm) × 4 in (101.6 mm) × 5/8 in (15.88 mm)
FAT · Front T rail layer A
13.685 in (347.6 mm) × 1 1/2 in (38.1 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm) × 5/8 in (15.88 mm)
FBL · Front L stile layer B
29.185 in (741.3 mm) × 1 1/2 in (38.1 mm)
29.06 in (738.12 mm) × 1 1/2 in (38.1 mm) × 5/8 in (15.88 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
FBR · Front R stile layer B
29.185 in (741.3 mm) × 1 1/2 in (38.1 mm)
29.06 in (738.12 mm) × 1 1/2 in (38.1 mm) × 5/8 in (15.88 mm)
FBB · Front B rail layer B
16.685 in (423.8 mm) × 4 in (101.6 mm)
16.56 in (420.62 mm) × 4 in (101.6 mm) × 5/8 in (15.88 mm)
FBT · Front T rail layer B
16.685 in (423.8 mm) × 1 1/2 in (38.1 mm)
16.56 in (420.62 mm) × 1 1/2 in (38.1 mm) × 5/8 in (15.88 mm)
DAL · Door L stile layer A
28.81 in (731.77 mm) × 1 11/16 in (42.86 mm)
28.685 in (728.6 mm) × 1 11/16 in (42.86 mm) × 39/64 in (15.48 mm)
DAR · Door R stile layer A
28.81 in (731.77 mm) × 1 3/4 in (44.45 mm)
28.685 in (728.6 mm) × 1 3/4 in (44.45 mm) × 39/64 in (15.48 mm)
DAB · Door B rail layer A
9.8725 in (250.76 mm) × 1 3/16 in (30.16 mm)
9.7475 in (247.59 mm) × 1 3/16 in (30.16 mm) × 39/64 in (15.48 mm)
DAT · Door T rail layer A
9.8725 in (250.76 mm) × 1 3/16 in (30.16 mm)
9.7475 in (247.59 mm) × 1 3/16 in (30.16 mm) × 39/64 in (15.48 mm)
DBL · Door L stile layer B
26.435 in (671.45 mm) × 1 11/16 in (42.86 mm)
26.31 in (668.27 mm) × 1 11/16 in (42.86 mm) × 39/64 in (15.48 mm)
DBR · Door R stile layer B
26.435 in (671.45 mm) × 1 3/4 in (44.45 mm)
26.31 in (668.27 mm) × 1 3/4 in (44.45 mm) × 39/64 in (15.48 mm)
DBB · Door B rail layer B
13.31 in (338.07 mm) × 1 3/16 in (30.16 mm)
13.185 in (334.9 mm) × 1 3/16 in (30.16 mm) × 39/64 in (15.48 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
DBT · Door T rail layer B
13.31 in (338.07 mm) × 1 3/16 in (30.16 mm)
13.185 in (334.9 mm) × 1 3/16 in (30.16 mm) × 39/64 in (15.48 mm)
G01 · Captured acrylic
27.06 in (687.32 mm) × 10.4975 in (266.64 mm)
27.06 in (687.32 mm) × 10.4975 in (266.64 mm) × 0.22 in (5.59 mm)
QL · Q glazing side L
27.435 in (696.85 mm) × 3/8 in (9.53 mm)
27.31 in (693.67 mm) × 3/8 in (9.53 mm) × 5/16 in (7.94 mm)
QR · Q glazing side R
27.435 in (696.85 mm) × 3/8 in (9.53 mm)
27.31 in (693.67 mm) × 3/8 in (9.53 mm) × 5/16 in (7.94 mm)
QB · Q glazing end B
11.6225 in (295.21 mm) × 5/16 in (7.94 mm)
11.4975 in (292.04 mm) × 5/16 in (7.94 mm) × 5/16 in (7.94 mm)
QT · Q glazing end T
11.6225 in (295.21 mm) × 5/16 in (7.94 mm)
11.4975 in (292.04 mm) × 5/16 in (7.94 mm) × 5/16 in (7.94 mm)
BL · B glazing side L
26.685 in (677.8 mm) × 3/4 in (19.05 mm)
26.56 in (674.62 mm) × 3/4 in (19.05 mm) × 1/4 in (6.35 mm)
BR · B glazing side R
26.685 in (677.8 mm) × 3/4 in (19.05 mm)
26.56 in (674.62 mm) × 3/4 in (19.05 mm) × 1/4 in (6.35 mm)
BB · B glazing end B
11.6225 in (295.21 mm) × 11/16 in (17.46 mm)
11.4975 in (292.04 mm) × 11/16 in (17.46 mm) × 1/4 in (6.35 mm)
BT · B glazing end T
11.6225 in (295.21 mm) × 11/16 in (17.46 mm)
11.4975 in (292.04 mm) × 11/16 in (17.46 mm) × 1/4 in (6.35 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
EFB · F EPDM B
10.4975 in (266.64 mm) × 3/8 in (9.53 mm)
10.4975 in (266.64 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
EFT · F EPDM T
10.4975 in (266.64 mm) × 3/8 in (9.53 mm)
10.4975 in (266.64 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
EFL · F EPDM L
26.31 in (668.27 mm) × 3/8 in (9.53 mm)
26.31 in (668.27 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
EFR · F EPDM R
26.31 in (668.27 mm) × 3/8 in (9.53 mm)
26.31 in (668.27 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
ERB · R EPDM B
10.4975 in (266.64 mm) × 1/4 in (6.35 mm)
10.4975 in (266.64 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
ERT · R EPDM T
10.4975 in (266.64 mm) × 1/4 in (6.35 mm)
10.4975 in (266.64 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
ERL · R EPDM L
26.56 in (674.62 mm) × 1/4 in (6.35 mm)
26.56 in (674.62 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
ERR · R EPDM R
26.56 in (674.62 mm) × 1/4 in (6.35 mm)
26.56 in (674.62 mm) × 1/4 in (6.35 mm) × 1/16 in (1.59 mm)
CLV · CLV solid pine cleat
31.56 in (801.62 mm) × 1 1/2 in (38.1 mm)
31.56 in (801.62 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CLB · CLB solid pine cleat
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm)
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
CLT · CLT solid pine cleat
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm)
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CRV · CRV solid pine cleat
31.56 in (801.62 mm) × 1 1/2 in (38.1 mm)
31.56 in (801.62 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CRB · CRB solid pine cleat
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm)
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CRT · CRT solid pine cleat
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm)
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CBB · CBB solid pine cleat
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CFB · CFB solid pine cleat
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CBT · CBT solid pine cleat
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CFT · CFT solid pine cleat
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
S01 · Lower door stop
10 1/8 in (257.18 mm) × 1 in (25.4 mm)
10 in (254 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
S02 · Upper stop beneath front roof cleat
10 1/8 in (257.18 mm) × 3/4 in (19.05 mm)
10 in (254 mm) × 3/4 in (19.05 mm) × 1/2 in (12.7 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
VLB · Inlet L B batten
8 1/8 in (206.38 mm) × 1 in (25.4 mm)
8 in (203.2 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VLT · Inlet L T batten
8 1/8 in (206.38 mm) × 1 in (25.4 mm)
8 in (203.2 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VLSF · Inlet L side F batten
2 1/8 in (53.98 mm) × 1 in (25.4 mm)
2 in (50.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VLSB · Inlet L side B batten
2 1/8 in (53.98 mm) × 1 in (25.4 mm)
2 in (50.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VRB · Inlet R B batten
8 1/8 in (206.38 mm) × 1 in (25.4 mm)
8 in (203.2 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VRT · Inlet R T batten
8 1/8 in (206.38 mm) × 1 in (25.4 mm)
8 in (203.2 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VRSF · Inlet R side F batten
2 1/8 in (53.98 mm) × 1 in (25.4 mm)
2 in (50.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
VRSB · Inlet R side B batten
2 1/8 in (53.98 mm) × 1 in (25.4 mm)
2 in (50.8 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
RF · Roof F batten
13 5/8 in (346.08 mm) × 1 in (25.4 mm)
13 1/2 in (342.9 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
RB · Roof B batten
13 5/8 in (346.08 mm) × 1 in (25.4 mm)
13 1/2 in (342.9 mm) × 1 in (25.4 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
RL · Roof L batten
10 1/8 in (257.18 mm) × 3/4 in (19.05 mm)
10 in (254 mm) × 3/4 in (19.05 mm) × 3/4 in (19.05 mm)
RR · Roof R batten
10 1/8 in (257.18 mm) × 3/4 in (19.05 mm)
10 in (254 mm) × 3/4 in (19.05 mm) × 3/4 in (19.05 mm)
LB1 · Left lamp steel support strip
11 1/2 in (292.1 mm) × 1 in (25.4 mm)
11 1/2 in (292.1 mm) × 1 in (25.4 mm) × 1/8 in (3.18 mm)
LB2 · Left lamp steel support strip
11 1/2 in (292.1 mm) × 1 in (25.4 mm)
11 1/2 in (292.1 mm) × 1 in (25.4 mm) × 1/8 in (3.18 mm)
M01 · Roof mesh
13 in (330.2 mm) × 11 1/2 in (292.1 mm)
13 in (330.2 mm) × 11 1/2 in (292.1 mm) × 3/32 in (2.38 mm)
M02L · L inlet mesh
7 1/2 in (190.5 mm) × 3 1/2 in (88.9 mm)
7 1/2 in (190.5 mm) × 3 1/2 in (88.9 mm) × 3/32 in (2.38 mm)
M02R · R inlet mesh
7 1/2 in (190.5 mm) × 3 1/2 in (88.9 mm)
7 1/2 in (190.5 mm) × 3 1/2 in (88.9 mm) × 3/32 in (2.38 mm)
SP-H1-fixed · Full-leaf aluminium spacer H1 fixed
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
SP-H2-fixed · Full-leaf aluminium spacer H2 fixed
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
3 in (76.2 mm) × 1 1/16 in (26.99 mm) × 1/8 in (3.18 mm)
V-floor-under · Exterior veneer · floor-under
18.561 in (471.45 mm) × 18.561 in (471.45 mm)
18.061 in (458.75 mm) × 18.061 in (458.75 mm) × 0.0305 in (0.77 mm)
V-roof-top · Exterior veneer · roof-top
18.561 in (471.45 mm) × 18.561 in (471.45 mm)
18.061 in (458.75 mm) × 18.061 in (458.75 mm) × 0.0305 in (0.77 mm)
V-P01-front · Exterior veneer · P01-front
18.561 in (471.45 mm) × 1.22 in (30.99 mm)
18.061 in (458.75 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P01-back · Exterior veneer · P01-back
18.561 in (471.45 mm) × 1.22 in (30.99 mm)
18.061 in (458.75 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P01-left · Exterior veneer · P01-left
18 1/2 in (469.9 mm) × 1.22 in (30.99 mm)
18 in (457.2 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P01-right · Exterior veneer · P01-right
18 1/2 in (469.9 mm) × 1.22 in (30.99 mm)
18 in (457.2 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P02-front · Exterior veneer · P02-front
18.561 in (471.45 mm) × 1.22 in (30.99 mm)
18.061 in (458.75 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P02-back · Exterior veneer · P02-back
18.561 in (471.45 mm) × 1.22 in (30.99 mm)
18.061 in (458.75 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P02-left · Exterior veneer · P02-left
18 1/2 in (469.9 mm) × 1.22 in (30.99 mm)
18 in (457.2 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
V-P02-right · Exterior veneer · P02-right
18 1/2 in (469.9 mm) × 1.22 in (30.99 mm)
18 in (457.2 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P03L-face · Exterior veneer · P03L-face
35.06 in (890.52 mm) × 18 1/2 in (469.9 mm)
34.56 in (877.82 mm) × 18 in (457.2 mm) × 0.0305 in (0.77 mm)
V-P03L-front · Exterior veneer · P03L-front
35.06 in (890.52 mm) × 1.2505 in (31.76 mm)
34.56 in (877.82 mm) × 0.7505 in (19.06 mm) × 0.0305 in (0.77 mm)
V-P03L-back · Exterior veneer · P03L-back
35.06 in (890.52 mm) × 1.2505 in (31.76 mm)
34.56 in (877.82 mm) × 0.7505 in (19.06 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P03L-vent-top · Exterior veneer · P03L-vent-top
6 1/2 in (165.1 mm) × 1.22 in (30.99 mm)
6 in (152.4 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P03R-face · Exterior veneer · P03R-face
35.06 in (890.52 mm) × 18 1/2 in (469.9 mm)
34.56 in (877.82 mm) × 18 in (457.2 mm) × 0.0305 in (0.77 mm)
V-P03R-front · Exterior veneer · P03R-front
35.06 in (890.52 mm) × 1.2505 in (31.76 mm)
34.56 in (877.82 mm) × 0.7505 in (19.06 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
V-P03R-back · Exterior veneer · P03R-back
35.06 in (890.52 mm) × 1.2505 in (31.76 mm)
34.56 in (877.82 mm) × 0.7505 in (19.06 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-P03R-vent-top · Exterior veneer · P03R-vent-top
6 1/2 in (165.1 mm) × 1.22 in (30.99 mm)
6 in (152.4 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-back · Exterior veneer · back
35.06 in (890.52 mm) × 17.06 in (433.32 mm)
34.56 in (877.82 mm) × 16.56 in (420.62 mm) × 0.0305 in (0.77 mm)
V-roof-left · Exterior veneer · roof-left
10.439 in (265.15 mm) × 1.22 in (30.99 mm)
9.939 in (252.45 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-roof-right · Exterior veneer · roof-right
10.439 in (265.15 mm) × 1.22 in (30.99 mm)
9.939 in (252.45 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-roof-front · Exterior veneer · roof-front
12 1/2 in (317.5 mm) × 1.22 in (30.99 mm)
12 in (304.8 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
V-roof-back · Exterior veneer · roof-back
12 1/2 in (317.5 mm) × 1.22 in (30.99 mm)
12 in (304.8 mm) × 0.72 in (18.29 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
6 in (152.4 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
V-FAL-front · Exterior veneer · FAL-front
35.06 in (890.52 mm) × 2 in (50.8 mm)
34.56 in (877.82 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-FAR-front · Exterior veneer · FAR-front
35.06 in (890.52 mm) × 2 in (50.8 mm)
34.56 in (877.82 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-FAB-front · Exterior veneer · FAB-front
14.06 in (357.12 mm) × 4 1/2 in (114.3 mm)
13.56 in (344.42 mm) × 4 in (101.6 mm) × 0.0305 in (0.77 mm)
V-FAT-front · Exterior veneer · FAT-front
14.06 in (357.12 mm) × 2 in (50.8 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-jamb-FAL · Exterior veneer · jamb-FAL
29.499 in (749.27 mm) × 1 3/4 in (44.45 mm)
28.999 in (736.57 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
V-jamb-FAR · Exterior veneer · jamb-FAR
29.499 in (749.27 mm) × 1 3/4 in (44.45 mm)
28.999 in (736.57 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
V-sill · Exterior veneer · sill
14.06 in (357.12 mm) × 1 3/4 in (44.45 mm)
13.56 in (344.42 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
V-head · Exterior veneer · head
14.06 in (357.12 mm) × 1 3/4 in (44.45 mm)
13.56 in (344.42 mm) × 1 1/4 in (31.75 mm) × 0.0305 in (0.77 mm)
V-DAL-front · Exterior veneer · DAL-front
29.246 in (742.85 mm) × 2.218 in (56.34 mm)
28.746 in (730.15 mm) × 1.718 in (43.64 mm) × 0.0305 in (0.77 mm)
V-DAR-front · Exterior veneer · DAR-front
29.246 in (742.85 mm) × 2.2805 in (57.92 mm)
28.746 in (730.15 mm) × 1.7805 in (45.22 mm) × 0.0305 in (0.77 mm)
V-DAB-front · Exterior veneer · DAB-front
10.2475 in (260.29 mm) × 1.718 in (43.64 mm)
9.7475 in (247.59 mm) × 1.218 in (30.94 mm) × 0.0305 in (0.77 mm)
V-DAT-front · Exterior veneer · DAT-front
10.2475 in (260.29 mm) × 1.718 in (43.64 mm)
9.7475 in (247.59 mm) × 1.218 in (30.94 mm) × 0.0305 in (0.77 mm)
28.685 in (728.6 mm) × 1 7/32 in (30.96 mm) × 0.0305 in (0.77 mm)
V-door-bottom · Exterior veneer · door-bottom
13.746 in (349.15 mm) × 1 23/32 in (43.66 mm)
13.246 in (336.45 mm) × 1 7/32 in (30.96 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each ID. Length follows the allocated grain. Rough blanks include trimming; finished sizes describe the reference assembly. V-parts represent the complete cured veneer stack. Field-fit dependent lengths to received stock and finished pockets.
Part
Rough length × width
Finished length × width × thickness
V-door-top · Exterior veneer · door-top
13.746 in (349.15 mm) × 1 23/32 in (43.66 mm)
13.246 in (336.45 mm) × 1 7/32 in (30.96 mm) × 0.0305 in (0.77 mm)
V-DAL-reveal · Exterior veneer · DAL-reveal
26.749 in (679.42 mm) × 1 23/32 in (43.66 mm)
26.249 in (666.72 mm) × 1 7/32 in (30.96 mm) × 0.0305 in (0.77 mm)
V-DAR-reveal · Exterior veneer · DAR-reveal
26.749 in (679.42 mm) × 1 23/32 in (43.66 mm)
26.249 in (666.72 mm) × 1 7/32 in (30.96 mm) × 0.0305 in (0.77 mm)
V-DAB-reveal · Exterior veneer · DAB-reveal
10.2475 in (260.29 mm) × 1 23/32 in (43.66 mm)
9.7475 in (247.59 mm) × 1 7/32 in (30.96 mm) × 0.0305 in (0.77 mm)
V-DAT-reveal · Exterior veneer · DAT-reveal
10.2475 in (260.29 mm) × 1 23/32 in (43.66 mm)
9.7475 in (247.59 mm) × 1 7/32 in (30.96 mm) × 0.0305 in (0.77 mm)
Cutting diagrams
PLYWOOD-1 · rough-stock cutting plan
Use the labeled IDs with exact coordinates; retain grain, trim and kerf
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
P03L
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34.685 in (881 mm) × 18 in (457.2 mm)
Stock 47 3/4 in (1212.85 mm) × 23 3/4 in (603.25 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
PLYWOOD-2 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
P03R
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34.685 in (881 mm) × 18 in (457.2 mm)
Stock 47 3/4 in (1212.85 mm) × 23 3/4 in (603.25 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
PLYWOOD-3 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
P01
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
18 1/8 in (460.38 mm) × 18 in (457.2 mm)
P02
18 3/8 in (466.73 mm) / 1/8 in (3.18 mm)
18 1/8 in (460.38 mm) × 18 in (457.2 mm)
Stock 47 3/4 in (1212.85 mm) × 23 3/4 in (603.25 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
PLYWOOD-4 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
P04
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34.685 in (881 mm) × 16.56 in (420.62 mm)
Stock 47 3/4 in (1212.85 mm) × 23 3/4 in (603.25 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
FRAME-PINE-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
FBB
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
16.685 in (423.8 mm) × 4 in (101.6 mm)
FAB
16.935 in (430.15 mm) / 1/8 in (3.18 mm)
13.685 in (347.6 mm) × 4 in (101.6 mm)
FAL
30.745 in (780.92 mm) / 1/8 in (3.18 mm)
34.685 in (881 mm) × 1 1/2 in (38.1 mm)
FAR
30.745 in (780.92 mm) / 1 3/4 in (44.45 mm)
34.685 in (881 mm) × 1 1/2 in (38.1 mm)
FBL
30.745 in (780.92 mm) / 3 3/8 in (85.73 mm)
29.185 in (741.3 mm) × 1 1/2 in (38.1 mm)
FBR
65.555 in (1665.1 mm) / 1/8 in (3.18 mm)
29.185 in (741.3 mm) × 1 1/2 in (38.1 mm)
FBT
65.555 in (1665.1 mm) / 1 3/4 in (44.45 mm)
16.685 in (423.8 mm) × 1 1/2 in (38.1 mm)
FAT
65.555 in (1665.1 mm) / 3 3/8 in (85.73 mm)
13.685 in (347.6 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
DOOR-PINE-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
DAR
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
28.81 in (731.77 mm) × 1 3/4 in (44.45 mm)
DBR
1/8 in (3.18 mm) / 2 in (50.8 mm)
26.435 in (671.45 mm) × 1 3/4 in (44.45 mm)
DAL
29.06 in (738.12 mm) / 1/8 in (3.18 mm)
28.81 in (731.77 mm) × 1 11/16 in (42.86 mm)
DBL
29.06 in (738.12 mm) / 1 15/16 in (49.21 mm)
26.435 in (671.45 mm) × 1 11/16 in (42.86 mm)
DBB
1/8 in (3.18 mm) / 3 7/8 in (98.43 mm)
13.31 in (338.07 mm) × 1 3/16 in (30.16 mm)
DBT
29.06 in (738.12 mm) / 3 3/4 in (95.25 mm)
13.31 in (338.07 mm) × 1 3/16 in (30.16 mm)
DAB
13.56 in (344.42 mm) / 3 7/8 in (98.43 mm)
9.8725 in (250.76 mm) × 1 3/16 in (30.16 mm)
DAT
42.495 in (1079.37 mm) / 3 3/4 in (95.25 mm)
9.8725 in (250.76 mm) × 1 3/16 in (30.16 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
PINE-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
RF
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
13 5/8 in (346.08 mm) × 1 in (25.4 mm)
RB
1/8 in (3.18 mm) / 1 1/4 in (31.75 mm)
13 5/8 in (346.08 mm) × 1 in (25.4 mm)
S01
1/8 in (3.18 mm) / 2 3/8 in (60.33 mm)
10 1/8 in (257.18 mm) × 1 in (25.4 mm)
VLB
1/8 in (3.18 mm) / 3 1/2 in (88.9 mm)
8 1/8 in (206.38 mm) × 1 in (25.4 mm)
VLT
13 7/8 in (352.43 mm) / 1/8 in (3.18 mm)
8 1/8 in (206.38 mm) × 1 in (25.4 mm)
VRB
13 7/8 in (352.43 mm) / 1 1/4 in (31.75 mm)
8 1/8 in (206.38 mm) × 1 in (25.4 mm)
VRT
13 7/8 in (352.43 mm) / 2 3/8 in (60.33 mm)
8 1/8 in (206.38 mm) × 1 in (25.4 mm)
VLSF
13 7/8 in (352.43 mm) / 3 1/2 in (88.9 mm)
2 1/8 in (53.98 mm) × 1 in (25.4 mm)
VLSB
16 1/8 in (409.58 mm) / 3 1/2 in (88.9 mm)
2 1/8 in (53.98 mm) × 1 in (25.4 mm)
VRSF
18 3/8 in (466.73 mm) / 3 1/2 in (88.9 mm)
2 1/8 in (53.98 mm) × 1 in (25.4 mm)
VRSB
10 3/8 in (263.53 mm) / 2 3/8 in (60.33 mm)
2 1/8 in (53.98 mm) × 1 in (25.4 mm)
RL
22 1/8 in (561.98 mm) / 1/8 in (3.18 mm)
10 1/8 in (257.18 mm) × 3/4 in (19.05 mm)
RR
22 1/8 in (561.98 mm) / 1 in (25.4 mm)
10 1/8 in (257.18 mm) × 3/4 in (19.05 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
SPACER-PINE-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
QL
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
27.435 in (696.85 mm) × 3/8 in (9.53 mm)
QR
1/8 in (3.18 mm) / 5/8 in (15.88 mm)
27.435 in (696.85 mm) × 3/8 in (9.53 mm)
QB
1/8 in (3.18 mm) / 1 1/8 in (28.58 mm)
11.6225 in (295.21 mm) × 5/16 in (7.94 mm)
QT
1/8 in (3.18 mm) / 1 9/16 in (39.69 mm)
11.6225 in (295.21 mm) × 5/16 in (7.94 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
CAP-PINE-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
BL
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
26.685 in (677.8 mm) × 3/4 in (19.05 mm)
BR
1/8 in (3.18 mm) / 1 in (25.4 mm)
26.685 in (677.8 mm) × 3/4 in (19.05 mm)
BB
1/8 in (3.18 mm) / 1 7/8 in (47.63 mm)
11.6225 in (295.21 mm) × 11/16 in (17.46 mm)
BT
1/8 in (3.18 mm) / 2 11/16 in (68.26 mm)
11.6225 in (295.21 mm) × 11/16 in (17.46 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
STOP-PINE-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
S02
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
10 1/8 in (257.18 mm) × 3/4 in (19.05 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
SQUARE-PINE-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
CLV
1/4 in (6.35 mm) / 0 in (0 mm)
31.56 in (801.62 mm) × 1 1/2 in (38.1 mm)
CRV
31.935 in (811.15 mm) / 0 in (0 mm)
31.56 in (801.62 mm) × 1 1/2 in (38.1 mm)
CLB
63.62 in (1615.95 mm) / 0 in (0 mm)
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm)
CBB
79.775 in (2026.29 mm) / 0 in (0 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); End trim 1/4 in (6.35 mm); side-edge trim 0 in (0 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
SQUARE-PINE-2 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
CLT
1/4 in (6.35 mm) / 0 in (0 mm)
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm)
CRB
16.405 in (416.69 mm) / 0 in (0 mm)
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm)
CRT
32.56 in (827.02 mm) / 0 in (0 mm)
16.03 in (407.16 mm) × 1 1/2 in (38.1 mm)
CFB
48.715 in (1237.36 mm) / 0 in (0 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm)
CBT
62.4 in (1584.96 mm) / 0 in (0 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm)
CFT
76.085 in (1932.56 mm) / 0 in (0 mm)
13.56 in (344.42 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); End trim 1/4 in (6.35 mm); side-edge trim 0 in (0 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
ACRYLIC-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
G01
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
27.06 in (687.32 mm) × 10.4975 in (266.64 mm)
Stock 48 in (1219.2 mm) × 24 in (609.6 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
MESH-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
M01
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
13 in (330.2 mm) × 11 1/2 in (292.1 mm)
M02L
1/8 in (3.18 mm) / 11 3/4 in (298.45 mm)
7 1/2 in (190.5 mm) × 3 1/2 in (88.9 mm)
M02R
1/8 in (3.18 mm) / 15 3/8 in (390.53 mm)
7 1/2 in (190.5 mm) × 3 1/2 in (88.9 mm)
Stock 120 in (3048 mm) × 36 in (914.4 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
ALUMINIUM-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
SP-H1-fixed
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
SP-H1-moving
3 3/16 in (80.96 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
SP-H2-fixed
6 1/4 in (158.75 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
SP-H2-moving
9 5/16 in (236.54 mm) / 1/8 in (3.18 mm)
3 in (76.2 mm) × 1 1/16 in (26.99 mm)
Stock 36 in (914.4 mm) × 1 1/2 in (38.1 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/16 in (1.59 mm). The full cut order and offcuts are in the specification.
EPDM-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
EFL
0 in (0 mm) / 0 in (0 mm)
26.31 in (668.27 mm) × 3/8 in (9.53 mm)
EFR
26.34125 in (669.07 mm) / 0 in (0 mm)
26.31 in (668.27 mm) × 3/8 in (9.53 mm)
EFB
52.6825 in (1338.14 mm) / 0 in (0 mm)
10.4975 in (266.64 mm) × 3/8 in (9.53 mm)
EFT
63.21125 in (1605.57 mm) / 0 in (0 mm)
10.4975 in (266.64 mm) × 3/8 in (9.53 mm)
ERL
73.74 in (1873 mm) / 0 in (0 mm)
26.56 in (674.62 mm) × 1/4 in (6.35 mm)
ERB
100.33125 in (2548.41 mm) / 0 in (0 mm)
10.4975 in (266.64 mm) × 1/4 in (6.35 mm)
Stock 120 in (3048 mm) × 3/8 in (9.53 mm); Edge trim 0 in (0 mm).; kerf/separation 1/32 in (0.79 mm). The full cut order and offcuts are in the specification.
EPDM-2 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
ERR
0 in (0 mm) / 0 in (0 mm)
26.56 in (674.62 mm) × 1/4 in (6.35 mm)
ERT
26.59125 in (675.42 mm) / 0 in (0 mm)
10.4975 in (266.64 mm) × 1/4 in (6.35 mm)
Stock 120 in (3048 mm) × 3/8 in (9.53 mm); Edge trim 0 in (0 mm).; kerf/separation 1/32 in (0.79 mm). The full cut order and offcuts are in the specification.
PINE-TRIAL · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
TRIAL-veneer
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
16 in (406.4 mm) × 3 1/2 in (88.9 mm)
TRIAL-hinge-frame
16 1/4 in (412.75 mm) / 1/8 in (3.18 mm)
34 3/4 in (882.65 mm) × 1 3/4 in (44.45 mm)
TRIAL-hinge-door
16 1/4 in (412.75 mm) / 2 in (50.8 mm)
29 in (736.6 mm) × 1 3/4 in (44.45 mm)
TRIAL-cushion
1/8 in (3.18 mm) / 3 3/4 in (95.25 mm)
16 in (406.4 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); Edge trim 1/8 in (3.18 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
STEEL-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
LB1
1/4 in (6.35 mm) / 0 in (0 mm)
11 1/2 in (292.1 mm) × 1 in (25.4 mm)
LB2
11 7/8 in (301.63 mm) / 0 in (0 mm)
11 1/2 in (292.1 mm) × 1 in (25.4 mm)
Stock 36 in (914.4 mm) × 1 in (25.4 mm); End trim 1/4 in (6.35 mm); side-edge trim 0 in (0 mm).; kerf/separation 1/8 in (3.18 mm). The full cut order and offcuts are in the specification.
VENEER-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
V-floor-under
1/4 in (6.35 mm) / 1/4 in (6.35 mm)
18.561 in (471.45 mm) × 18.561 in (471.45 mm)
V-roof-top
18.8735 in (479.39 mm) / 1/4 in (6.35 mm)
18.561 in (471.45 mm) × 18.561 in (471.45 mm)
V-P03L-face
37.497 in (952.42 mm) / 1/4 in (6.35 mm)
35.06 in (890.52 mm) × 18 1/2 in (469.9 mm)
V-P03R-face
72.6195 in (1844.54 mm) / 1/4 in (6.35 mm)
35.06 in (890.52 mm) × 18 1/2 in (469.9 mm)
V-back
1/4 in (6.35 mm) / 18.8735 in (479.39 mm)
35.06 in (890.52 mm) × 17.06 in (433.32 mm)
V-TRIAL
1/4 in (6.35 mm) / 35.996 in (914.3 mm)
16 1/2 in (419.1 mm) × 5 1/2 in (139.7 mm)
V-FAB-front
16 13/16 in (427.04 mm) / 35.996 in (914.3 mm)
14.06 in (357.12 mm) × 4 1/2 in (114.3 mm)
V-DAR-front
30.935 in (785.75 mm) / 35.996 in (914.3 mm)
29.246 in (742.85 mm) × 2.2805 in (57.92 mm)
V-DAL-front
60.2435 in (1530.18 mm) / 35.996 in (914.3 mm)
29.246 in (742.85 mm) × 2.218 in (56.34 mm)
V-FAL-front
30.935 in (785.75 mm) / 38.339 in (973.81 mm)
35.06 in (890.52 mm) × 2 in (50.8 mm)
V-FAR-front
66.0575 in (1677.86 mm) / 38.339 in (973.81 mm)
35.06 in (890.52 mm) × 2 in (50.8 mm)
V-FAT-front
101.18 in (2569.97 mm) / 38.339 in (973.81 mm)
14.06 in (357.12 mm) × 2 in (50.8 mm)
V-jamb-FAL
89.552 in (2274.62 mm) / 35.996 in (914.3 mm)
29.499 in (749.27 mm) × 1 3/4 in (44.45 mm)
V-jamb-FAR
1/4 in (6.35 mm) / 41.5585 in (1055.59 mm)
29.499 in (749.27 mm) × 1 3/4 in (44.45 mm)
V-sill
29.8115 in (757.21 mm) / 41.5585 in (1055.59 mm)
14.06 in (357.12 mm) × 1 3/4 in (44.45 mm)
V-head
43.934 in (1115.92 mm) / 41.5585 in (1055.59 mm)
14.06 in (357.12 mm) × 1 3/4 in (44.45 mm)
Stock 120 in (3048 mm) × 48 in (1219.2 mm); Edge trim 1/4 in (6.35 mm).; kerf/separation 1/16 in (1.59 mm). The full cut order and offcuts are in the specification.
VENEER-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
V-restraint-backing
58.0565 in (1474.64 mm) / 41.5585 in (1055.59 mm)
6 1/2 in (165.1 mm) × 1 3/4 in (44.45 mm)
V-door-hinge-edge
64.619 in (1641.32 mm) / 41.5585 in (1055.59 mm)
29.185 in (741.3 mm) × 1 23/32 in (43.66 mm)
V-door-latch-edge
1/4 in (6.35 mm) / 43.371 in (1101.62 mm)
29.185 in (741.3 mm) × 1 23/32 in (43.66 mm)
V-DAL-reveal
29.4975 in (749.24 mm) / 43.371 in (1101.62 mm)
26.749 in (679.42 mm) × 1 23/32 in (43.66 mm)
V-DAR-reveal
56.309 in (1430.25 mm) / 43.371 in (1101.62 mm)
26.749 in (679.42 mm) × 1 23/32 in (43.66 mm)
V-door-bottom
93.8665 in (2384.21 mm) / 41.5585 in (1055.59 mm)
13.746 in (349.15 mm) × 1 23/32 in (43.66 mm)
V-door-top
83.1205 in (2111.26 mm) / 43.371 in (1101.62 mm)
13.746 in (349.15 mm) × 1 23/32 in (43.66 mm)
V-DAB-reveal
107.675 in (2734.95 mm) / 41.5585 in (1055.59 mm)
10.2475 in (260.29 mm) × 1 23/32 in (43.66 mm)
V-DAT-reveal
96.929 in (2462 mm) / 43.371 in (1101.62 mm)
10.2475 in (260.29 mm) × 1 23/32 in (43.66 mm)
V-DAB-front
107.239 in (2723.87 mm) / 43.371 in (1101.62 mm)
10.2475 in (260.29 mm) × 1.718 in (43.64 mm)
V-DAT-front
1/4 in (6.35 mm) / 45.15225 in (1146.87 mm)
10.2475 in (260.29 mm) × 1.718 in (43.64 mm)
V-P03L-front
10.56 in (268.22 mm) / 45.15225 in (1146.87 mm)
35.06 in (890.52 mm) × 1.2505 in (31.76 mm)
V-P03L-back
45.6825 in (1160.34 mm) / 45.15225 in (1146.87 mm)
35.06 in (890.52 mm) × 1.2505 in (31.76 mm)
V-P03R-front
80.805 in (2052.45 mm) / 45.15225 in (1146.87 mm)
35.06 in (890.52 mm) × 1.2505 in (31.76 mm)
V-P03R-back
35.3725 in (898.46 mm) / 18.8735 in (479.39 mm)
35.06 in (890.52 mm) × 1.2505 in (31.76 mm)
V-P01-front
70.495 in (1790.57 mm) / 18.8735 in (479.39 mm)
18.561 in (471.45 mm) × 1.22 in (30.99 mm)
Stock 120 in (3048 mm) × 48 in (1219.2 mm); Edge trim 1/4 in (6.35 mm).; kerf/separation 1/16 in (1.59 mm). The full cut order and offcuts are in the specification.
VENEER-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
V-P01-back
89.1185 in (2263.61 mm) / 18.8735 in (479.39 mm)
18.561 in (471.45 mm) × 1.22 in (30.99 mm)
V-P02-front
35.3725 in (898.46 mm) / 20.1865 in (512.74 mm)
18.561 in (471.45 mm) × 1.22 in (30.99 mm)
V-P02-back
53.996 in (1371.5 mm) / 20.1865 in (512.74 mm)
18.561 in (471.45 mm) × 1.22 in (30.99 mm)
V-P01-left
72.6195 in (1844.54 mm) / 20.1865 in (512.74 mm)
18 1/2 in (469.9 mm) × 1.22 in (30.99 mm)
V-P01-right
91.182 in (2316.02 mm) / 20.1865 in (512.74 mm)
18 1/2 in (469.9 mm) × 1.22 in (30.99 mm)
V-P02-left
35.3725 in (898.46 mm) / 21.469 in (545.31 mm)
18 1/2 in (469.9 mm) × 1.22 in (30.99 mm)
V-P02-right
53.935 in (1369.95 mm) / 21.469 in (545.31 mm)
18 1/2 in (469.9 mm) × 1.22 in (30.99 mm)
V-roof-front
72.4975 in (1841.44 mm) / 21.469 in (545.31 mm)
12 1/2 in (317.5 mm) × 1.22 in (30.99 mm)
V-roof-back
85.06 in (2160.52 mm) / 21.469 in (545.31 mm)
12 1/2 in (317.5 mm) × 1.22 in (30.99 mm)
V-roof-left
107.742 in (2736.65 mm) / 18.8735 in (479.39 mm)
10.439 in (265.15 mm) × 1.22 in (30.99 mm)
V-roof-right
97.6225 in (2479.61 mm) / 21.469 in (545.31 mm)
10.439 in (265.15 mm) × 1.22 in (30.99 mm)
V-P03L-vent-bottom
109.7445 in (2787.51 mm) / 20.1865 in (512.74 mm)
6 1/2 in (165.1 mm) × 1.22 in (30.99 mm)
V-P03L-vent-top
108.124 in (2746.35 mm) / 21.469 in (545.31 mm)
6 1/2 in (165.1 mm) × 1.22 in (30.99 mm)
V-P03R-vent-bottom
107.742 in (2736.65 mm) / 1/4 in (6.35 mm)
6 1/2 in (165.1 mm) × 1.22 in (30.99 mm)
V-P03R-vent-top
107.742 in (2736.65 mm) / 1.5325 in (38.93 mm)
6 1/2 in (165.1 mm) × 1.22 in (30.99 mm)
V-restraint-bottom
107.742 in (2736.65 mm) / 2.815 in (71.5 mm)
6 1/2 in (165.1 mm) × 1.22 in (30.99 mm)
Stock 120 in (3048 mm) × 48 in (1219.2 mm); Edge trim 1/4 in (6.35 mm).; kerf/separation 1/16 in (1.59 mm). The full cut order and offcuts are in the specification.
VENEER-1 · exact rough blank positions
X runs along the stock length; Y across its width, from the illustrated lower-left corner. These are stock coordinates, not assembled fastener positions. Keep every blank labeled.
ID
Stock X / Y
Rough length × width
V-restraint-top
107.742 in (2736.65 mm) / 4.0975 in (104.08 mm)
6 1/2 in (165.1 mm) × 1.22 in (30.99 mm)
V-P03L-vent-near
116.307 in (2954.2 mm) / 20.1865 in (512.74 mm)
2.439 in (61.95 mm) × 1.22 in (30.99 mm)
V-P03L-vent-far
114.6865 in (2913.04 mm) / 21.469 in (545.31 mm)
2.439 in (61.95 mm) × 1.22 in (30.99 mm)
V-P03R-vent-near
114.3045 in (2903.33 mm) / 1/4 in (6.35 mm)
2.439 in (61.95 mm) × 1.22 in (30.99 mm)
V-P03R-vent-far
114.3045 in (2903.33 mm) / 1.5325 in (38.93 mm)
2.439 in (61.95 mm) × 1.22 in (30.99 mm)
V-restraint-left
114.3045 in (2903.33 mm) / 2.815 in (71.5 mm)
1.689 in (42.9 mm) × 1.22 in (30.99 mm)
V-restraint-right
114.3045 in (2903.33 mm) / 4.0975 in (104.08 mm)
1.689 in (42.9 mm) × 1.22 in (30.99 mm)
Stock 120 in (3048 mm) × 48 in (1219.2 mm); Edge trim 1/4 in (6.35 mm).; kerf/separation 1/16 in (1.59 mm). The full cut order and offcuts are in the specification.
Use the exact fastener stations
X / Y / Z start at outside LEFT / outside FRONT / FLOOR UNDERSIDE. Direction gives the driver axis. Transfer actual clamped receiver centerlines. Include the drill point in the depth stop. Hardware samples control metal holes and countersinks.
All front-frame lamination screws are installed on the bench before the frame enters the shell. Veneer leaves head-access and metal-bearing seats clear. Hinges use four scheduled solid spacers. Door lamination screws are fitted before glazing retainers; the detached roof receives screen/support screws before it is refitted. The two actual-kit furniture screws are transferred after the physical trial; their locations are not invented here.
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J001 · SCREW-SHELL
P03L → CLB
0 / 4 / 1.47 in 0.00 / 101.60 / 37.34 mm
+X · 1 3/4 in (44.45 mm)
J002 · SCREW-SHELL
P03L → CLB
0 / 9 / 1.47 in 0.00 / 228.60 / 37.34 mm
+X · 1 3/4 in (44.45 mm)
J003 · SCREW-SHELL
P03L → CLB
0 / 14 / 1.47 in 0.00 / 355.60 / 37.34 mm
+X · 1 3/4 in (44.45 mm)
J004 · SCREW-SHELL
P03L → CLT
0 / 4 / 34.53 in 0.00 / 101.60 / 877.06 mm
+X · 1 3/4 in (44.45 mm)
J005 · SCREW-SHELL
P03L → CLT
0 / 9 / 34.53 in 0.00 / 228.60 / 877.06 mm
+X · 1 3/4 in (44.45 mm)
J006 · SCREW-SHELL
P03L → CLT
0 / 14 / 34.53 in 0.00 / 355.60 / 877.06 mm
+X · 1 3/4 in (44.45 mm)
J007 · SCREW-SHELL
P03L → CLV
0 / 16.53 / 6 in 0.00 / 419.86 / 152.40 mm
+X · 1 3/4 in (44.45 mm)
J008 · SCREW-SHELL
P03L → CLV
0 / 16.53 / 14 in 0.00 / 419.86 / 355.60 mm
+X · 1 3/4 in (44.45 mm)
J009 · SCREW-SHELL
P03L → CLV
0 / 16.53 / 22 in 0.00 / 419.86 / 558.80 mm
+X · 1 3/4 in (44.45 mm)
J010 · SCREW-SHELL
P03L → CLV
0 / 16.53 / 30 in 0.00 / 419.86 / 762.00 mm
+X · 1 3/4 in (44.45 mm)
J011 · SCREW-SHELL
P03L → FAL
0 / 0.3125 / 3 in 0.00 / 7.94 / 76.20 mm
+X · 1 3/4 in (44.45 mm)
J012 · SCREW-SHELL
P03L → FAL
0 / 0.3125 / 10 in 0.00 / 7.94 / 254.00 mm
+X · 1 3/4 in (44.45 mm)
J013 · SCREW-SHELL
P03L → FAL
0 / 0.3125 / 18 in 0.00 / 7.94 / 457.20 mm
+X · 1 3/4 in (44.45 mm)
J014 · SCREW-SHELL
P03L → FAL
0 / 0.3125 / 27 in 0.00 / 7.94 / 685.80 mm
+X · 1 3/4 in (44.45 mm)
Fastener stations · 15–28
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J015 · SCREW-SHELL
P03L → FAL
0 / 0.3125 / 33 in 0.00 / 7.94 / 838.20 mm
+X · 1 3/4 in (44.45 mm)
J016 · SCREW-SHELL
P03R → CRB
18 / 4 / 1.47 in 457.20 / 101.60 / 37.34 mm
−X · 1 3/4 in (44.45 mm)
J017 · SCREW-SHELL
P03R → CRB
18 / 9 / 1.47 in 457.20 / 228.60 / 37.34 mm
−X · 1 3/4 in (44.45 mm)
J018 · SCREW-SHELL
P03R → CRB
18 / 14 / 1.47 in 457.20 / 355.60 / 37.34 mm
−X · 1 3/4 in (44.45 mm)
J019 · SCREW-SHELL
P03R → CRT
18 / 4 / 34.53 in 457.20 / 101.60 / 877.06 mm
−X · 1 3/4 in (44.45 mm)
J020 · SCREW-SHELL
P03R → CRT
18 / 9 / 34.53 in 457.20 / 228.60 / 877.06 mm
−X · 1 3/4 in (44.45 mm)
J021 · SCREW-SHELL
P03R → CRT
18 / 14 / 34.53 in 457.20 / 355.60 / 877.06 mm
−X · 1 3/4 in (44.45 mm)
J022 · SCREW-SHELL
P03R → CRV
18 / 16.53 / 6 in 457.20 / 419.86 / 152.40 mm
−X · 1 3/4 in (44.45 mm)
J023 · SCREW-SHELL
P03R → CRV
18 / 16.53 / 14 in 457.20 / 419.86 / 355.60 mm
−X · 1 3/4 in (44.45 mm)
J024 · SCREW-SHELL
P03R → CRV
18 / 16.53 / 22 in 457.20 / 419.86 / 558.80 mm
−X · 1 3/4 in (44.45 mm)
J025 · SCREW-SHELL
P03R → CRV
18 / 16.53 / 30 in 457.20 / 419.86 / 762.00 mm
−X · 1 3/4 in (44.45 mm)
J026 · SCREW-SHELL
P03R → FAR
18 / 0.3125 / 3 in 457.20 / 7.94 / 76.20 mm
−X · 1 3/4 in (44.45 mm)
J027 · SCREW-SHELL
P03R → FAR
18 / 0.3125 / 10 in 457.20 / 7.94 / 254.00 mm
−X · 1 3/4 in (44.45 mm)
J028 · SCREW-SHELL
P03R → FAR
18 / 0.3125 / 18 in 457.20 / 7.94 / 457.20 mm
−X · 1 3/4 in (44.45 mm)
Fastener stations · 29–42
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J029 · SCREW-SHELL
P03R → FAR
18 / 0.3125 / 27 in 457.20 / 7.94 / 685.80 mm
−X · 1 3/4 in (44.45 mm)
J030 · SCREW-SHELL
P03R → FAR
18 / 0.3125 / 33 in 457.20 / 7.94 / 838.20 mm
−X · 1 3/4 in (44.45 mm)
J031 · SCREW-SHELL
P04 → CLV
1.47 / 18 / 8 in 37.34 / 457.20 / 203.20 mm
−Y · 1 3/4 in (44.45 mm)
J032 · SCREW-SHELL
P04 → CLV
1.47 / 18 / 16 in 37.34 / 457.20 / 406.40 mm
−Y · 1 3/4 in (44.45 mm)
J033 · SCREW-SHELL
P04 → CLV
1.47 / 18 / 24 in 37.34 / 457.20 / 609.60 mm
−Y · 1 3/4 in (44.45 mm)
J034 · SCREW-SHELL
P04 → CLV
1.47 / 18 / 32 in 37.34 / 457.20 / 812.80 mm
−Y · 1 3/4 in (44.45 mm)
J035 · SCREW-SHELL
P04 → CRV
16.53 / 18 / 8 in 419.86 / 457.20 / 203.20 mm
−Y · 1 3/4 in (44.45 mm)
J036 · SCREW-SHELL
P04 → CRV
16.53 / 18 / 16 in 419.86 / 457.20 / 406.40 mm
−Y · 1 3/4 in (44.45 mm)
J037 · SCREW-SHELL
P04 → CRV
16.53 / 18 / 24 in 419.86 / 457.20 / 609.60 mm
−Y · 1 3/4 in (44.45 mm)
J038 · SCREW-SHELL
P04 → CRV
16.53 / 18 / 32 in 419.86 / 457.20 / 812.80 mm
−Y · 1 3/4 in (44.45 mm)
J039 · SCREW-SHELL
P04 → CBB
5 / 18 / 1.47 in 127.00 / 457.20 / 37.34 mm
−Y · 1 3/4 in (44.45 mm)
J040 · SCREW-SHELL
P04 → CBB
9 / 18 / 1.47 in 228.60 / 457.20 / 37.34 mm
−Y · 1 3/4 in (44.45 mm)
J041 · SCREW-SHELL
P04 → CBB
13 / 18 / 1.47 in 330.20 / 457.20 / 37.34 mm
−Y · 1 3/4 in (44.45 mm)
J042 · SCREW-SHELL
P04 → CBT
3 / 18 / 34.53 in 76.20 / 457.20 / 877.06 mm
−Y · 1 3/4 in (44.45 mm)
Fastener stations · 43–56
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J043 · SCREW-SHELL
P04 → CBT
5 / 18 / 34.53 in 127.00 / 457.20 / 877.06 mm
−Y · 1 3/4 in (44.45 mm)
J044 · SCREW-SHELL
P04 → CBT
13 / 18 / 34.53 in 330.20 / 457.20 / 877.06 mm
−Y · 1 3/4 in (44.45 mm)
J045 · SCREW-SHELL
P01 → CLB
1.47 / 5.5 / 0 in 37.34 / 139.70 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J046 · SCREW-SHELL
P01 → CLB
1.47 / 11.5 / 0 in 37.34 / 292.10 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J047 · SCREW-SHELL
P01 → CLB
1.47 / 15 / 0 in 37.34 / 381.00 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J048 · SCREW-SHELL
P01 → CRB
16.53 / 5.5 / 0 in 419.86 / 139.70 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J049 · SCREW-SHELL
P01 → CRB
16.53 / 11.5 / 0 in 419.86 / 292.10 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J050 · SCREW-SHELL
P01 → CRB
16.53 / 15 / 0 in 419.86 / 381.00 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J051 · SCREW-SHELL
P01 → CFB
4 / 2 / 0 in 101.60 / 50.80 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J052 · SCREW-SHELL
P01 → CFB
8 / 2 / 0 in 203.20 / 50.80 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J053 · SCREW-SHELL
P01 → CFB
12 / 2 / 0 in 304.80 / 50.80 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J054 · SCREW-SHELL
P01 → CFB
15 / 2 / 0 in 381.00 / 50.80 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J055 · SCREW-SHELL
P01 → CBB
4 / 16.53 / 0 in 101.60 / 419.86 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J056 · SCREW-SHELL
P01 → CBB
8 / 16.53 / 0 in 203.20 / 419.86 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
Fastener stations · 57–70
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J057 · SCREW-SHELL
P01 → CBB
12 / 16.53 / 0 in 304.80 / 419.86 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J058 · SCREW-SHELL
P01 → CBB
15 / 16.53 / 0 in 381.00 / 419.86 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J059 · SCREW-SHELL
P01 → FAB
4.5 / 0.3125 / 0 in 114.30 / 7.94 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J060 · SCREW-SHELL
P01 → FAB
9 / 0.3125 / 0 in 228.60 / 7.94 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J061 · SCREW-SHELL
P01 → FAB
13.5 / 0.3125 / 0 in 342.90 / 7.94 / 0.00 mm
+Z · 1 3/4 in (44.45 mm)
J062 · SCREW-SHELL
P02 → CLT
1.47 / 5.5 / 36 in 37.34 / 139.70 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J063 · SCREW-SHELL
P02 → CLT
1.47 / 11.5 / 36 in 37.34 / 292.10 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J064 · SCREW-SHELL
P02 → CLT
1.47 / 15 / 36 in 37.34 / 381.00 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J065 · SCREW-SHELL
P02 → CRT
16.53 / 5.5 / 36 in 419.86 / 139.70 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J066 · SCREW-SHELL
P02 → CRT
16.53 / 11.5 / 36 in 419.86 / 292.10 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J067 · SCREW-SHELL
P02 → CRT
16.53 / 15 / 36 in 419.86 / 381.00 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J068 · SCREW-SHELL
P02 → CFT
4 / 2 / 36 in 101.60 / 50.80 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J069 · SCREW-SHELL
P02 → CFT
8 / 2 / 36 in 203.20 / 50.80 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J070 · SCREW-SHELL
P02 → CFT
12 / 2 / 36 in 304.80 / 50.80 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
Fastener stations · 71–84
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J071 · SCREW-SHELL
P02 → CFT
15 / 2 / 36 in 381.00 / 50.80 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J072 · SCREW-SHELL
P02 → CBT
4 / 16.53 / 36 in 101.60 / 419.86 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J073 · SCREW-SHELL
P02 → CBT
8 / 16.53 / 36 in 203.20 / 419.86 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J074 · SCREW-SHELL
P02 → CBT
12 / 16.53 / 36 in 304.80 / 419.86 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J075 · SCREW-SHELL
P02 → CBT
15 / 16.53 / 36 in 381.00 / 419.86 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J076 · SCREW-SHELL
P02 → FAT
4.5 / 0.3125 / 36 in 114.30 / 7.94 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J077 · SCREW-SHELL
P02 → FAT
9 / 0.3125 / 36 in 228.60 / 7.94 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J078 · SCREW-SHELL
P02 → FAT
13.5 / 0.3125 / 36 in 342.90 / 7.94 / 914.40 mm
−Z · 1 3/4 in (44.45 mm)
J079 · SCREW-LAMINATION
FBB → FAL
1.47 / 1.25 / 1.47 in 37.34 / 31.75 / 37.34 mm
−Y · 1 in (25.4 mm)
J080 · SCREW-LAMINATION
FBB → FAL
1.47 / 1.25 / 4 in 37.34 / 31.75 / 101.60 mm
−Y · 1 in (25.4 mm)
J081 · SCREW-LAMINATION
FBL → FAL
1.47 / 1.25 / 8 in 37.34 / 31.75 / 203.20 mm
−Y · 1 in (25.4 mm)
J082 · SCREW-LAMINATION
FBL → FAL
1.47 / 1.25 / 14 in 37.34 / 31.75 / 355.60 mm
−Y · 1 in (25.4 mm)
J083 · SCREW-LAMINATION
FBL → FAL
1.47 / 1.25 / 20 in 37.34 / 31.75 / 508.00 mm
−Y · 1 in (25.4 mm)
J084 · SCREW-LAMINATION
FBL → FAL
1.47 / 1.25 / 26 in 37.34 / 31.75 / 660.40 mm
−Y · 1 in (25.4 mm)
Fastener stations · 85–98
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J085 · SCREW-LAMINATION
FBL → FAL
1.47 / 1.25 / 32 in 37.34 / 31.75 / 812.80 mm
−Y · 1 in (25.4 mm)
J086 · SCREW-LAMINATION
FBT → FAL
1.47 / 1.25 / 34.53 in 37.34 / 31.75 / 877.06 mm
−Y · 1 in (25.4 mm)
J087 · SCREW-LAMINATION
FBB → FAR
16.53 / 1.25 / 1.47 in 419.86 / 31.75 / 37.34 mm
−Y · 1 in (25.4 mm)
J088 · SCREW-LAMINATION
FBB → FAR
16.53 / 1.25 / 4 in 419.86 / 31.75 / 101.60 mm
−Y · 1 in (25.4 mm)
J089 · SCREW-LAMINATION
FBR → FAR
16.53 / 1.25 / 8 in 419.86 / 31.75 / 203.20 mm
−Y · 1 in (25.4 mm)
J090 · SCREW-LAMINATION
FBR → FAR
16.53 / 1.25 / 14 in 419.86 / 31.75 / 355.60 mm
−Y · 1 in (25.4 mm)
J091 · SCREW-LAMINATION
FBR → FAR
16.53 / 1.25 / 20 in 419.86 / 31.75 / 508.00 mm
−Y · 1 in (25.4 mm)
J092 · SCREW-LAMINATION
FBR → FAR
16.53 / 1.25 / 26 in 419.86 / 31.75 / 660.40 mm
−Y · 1 in (25.4 mm)
J093 · SCREW-LAMINATION
FBR → FAR
16.53 / 1.25 / 32 in 419.86 / 31.75 / 812.80 mm
−Y · 1 in (25.4 mm)
J094 · SCREW-LAMINATION
FBT → FAR
16.53 / 1.25 / 34.53 in 419.86 / 31.75 / 877.06 mm
−Y · 1 in (25.4 mm)
J095 · SCREW-LAMINATION
FBB → FAB
5.5 / 1.25 / 2.5 in 139.70 / 31.75 / 63.50 mm
−Y · 1 in (25.4 mm)
J096 · SCREW-LAMINATION
FBB → FAB
11.5 / 1.25 / 2.5 in 292.10 / 31.75 / 63.50 mm
−Y · 1 in (25.4 mm)
J097 · SCREW-LAMINATION
FBT → FAT
5.5 / 1.25 / 34.53 in 139.70 / 31.75 / 877.06 mm
−Y · 1 in (25.4 mm)
J098 · SCREW-LAMINATION
FBT → FAT
11.5 / 1.25 / 34.53 in 292.10 / 31.75 / 877.06 mm
−Y · 1 in (25.4 mm)
Fastener stations · 99–112
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J099 · SCREW-LAMINATION
DBB → DAL
3.22 / 1.25 / 5.47 in 81.79 / 31.75 / 138.94 mm
−Y · 1 in (25.4 mm)
J100 · SCREW-LAMINATION
DBL → DAL
3.22 / 1.25 / 10 in 81.79 / 31.75 / 254.00 mm
−Y · 1 in (25.4 mm)
J101 · SCREW-LAMINATION
DBL → DAL
3.22 / 1.25 / 16 in 81.79 / 31.75 / 406.40 mm
−Y · 1 in (25.4 mm)
J102 · SCREW-LAMINATION
DBL → DAL
3.22 / 1.25 / 22 in 81.79 / 31.75 / 558.80 mm
−Y · 1 in (25.4 mm)
J103 · SCREW-LAMINATION
DBL → DAL
3.22 / 1.25 / 28 in 81.79 / 31.75 / 711.20 mm
−Y · 1 in (25.4 mm)
J104 · SCREW-LAMINATION
DBT → DAL
3.22 / 1.25 / 33.03 in 81.79 / 31.75 / 838.96 mm
−Y · 1 in (25.4 mm)
J105 · SCREW-LAMINATION
DBB → DAR
14.7175 / 1.25 / 5.47 in 373.82 / 31.75 / 138.94 mm
−Y · 1 in (25.4 mm)
J106 · SCREW-LAMINATION
DBR → DAR
14.7175 / 1.25 / 10 in 373.82 / 31.75 / 254.00 mm
−Y · 1 in (25.4 mm)
J107 · SCREW-LAMINATION
DBR → DAR
14.7175 / 1.25 / 16 in 373.82 / 31.75 / 406.40 mm
−Y · 1 in (25.4 mm)
J108 · SCREW-LAMINATION
DBR → DAR
14.7175 / 1.25 / 22 in 373.82 / 31.75 / 558.80 mm
−Y · 1 in (25.4 mm)
J109 · SCREW-LAMINATION
DBR → DAR
14.7175 / 1.25 / 28 in 373.82 / 31.75 / 711.20 mm
−Y · 1 in (25.4 mm)
J110 · SCREW-LAMINATION
DBT → DAR
14.7175 / 1.25 / 33.03 in 373.82 / 31.75 / 838.96 mm
−Y · 1 in (25.4 mm)
J111 · SCREW-LAMINATION
DBB → DAB
9 / 1.25 / 5.47 in 228.60 / 31.75 / 138.94 mm
−Y · 1 in (25.4 mm)
J112 · SCREW-LAMINATION
DBT → DAT
9 / 1.25 / 33.03 in 228.60 / 31.75 / 838.96 mm
−Y · 1 in (25.4 mm)
Fastener stations · 113–126
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J113 · SCREW-RETENTION
VLB → P03L
1.47 / 6.0418 / 5.22 in 37.34 / 153.46 / 132.59 mm
−X · 1 1/4 in (31.75 mm)
J114 · SCREW-RETENTION
VLB → P03L
1.47 / 8.7508 / 5.22 in 37.34 / 222.27 / 132.59 mm
−X · 1 1/4 in (31.75 mm)
J115 · SCREW-RETENTION
VLB → P03L
1.47 / 12.0016 / 5.22 in 37.34 / 304.84 / 132.59 mm
−X · 1 1/4 in (31.75 mm)
J116 · SCREW-RETENTION
VLT → P03L
1.47 / 6.0418 / 8.4708 in 37.34 / 153.46 / 215.16 mm
−X · 1 1/4 in (31.75 mm)
J117 · SCREW-RETENTION
VLT → P03L
1.47 / 8.7508 / 8.4708 in 37.34 / 222.27 / 215.16 mm
−X · 1 1/4 in (31.75 mm)
J118 · SCREW-RETENTION
VLT → P03L
1.47 / 12.0016 / 8.4708 in 37.34 / 304.84 / 215.16 mm
−X · 1 1/4 in (31.75 mm)
J119 · SCREW-RETENTION
VLSF → P03L
1.47 / 5.5 / 6.8454 in 37.34 / 139.70 / 173.87 mm
−X · 1 1/4 in (31.75 mm)
J120 · SCREW-RETENTION
VLSB → P03L
1.47 / 12.5434 / 6.8454 in 37.34 / 318.60 / 173.87 mm
−X · 1 1/4 in (31.75 mm)
J121 · SCREW-RETENTION
VRB → P03R
16.53 / 6.0418 / 5.22 in 419.86 / 153.46 / 132.59 mm
+X · 1 1/4 in (31.75 mm)
J122 · SCREW-RETENTION
VRB → P03R
16.53 / 8.7508 / 5.22 in 419.86 / 222.27 / 132.59 mm
+X · 1 1/4 in (31.75 mm)
J123 · SCREW-RETENTION
VRB → P03R
16.53 / 12.0016 / 5.22 in 419.86 / 304.84 / 132.59 mm
+X · 1 1/4 in (31.75 mm)
J124 · SCREW-RETENTION
VRT → P03R
16.53 / 6.0418 / 8.4708 in 419.86 / 153.46 / 215.16 mm
+X · 1 1/4 in (31.75 mm)
J125 · SCREW-RETENTION
VRT → P03R
16.53 / 8.7508 / 8.4708 in 419.86 / 222.27 / 215.16 mm
+X · 1 1/4 in (31.75 mm)
J126 · SCREW-RETENTION
VRT → P03R
16.53 / 12.0016 / 8.4708 in 419.86 / 304.84 / 215.16 mm
+X · 1 1/4 in (31.75 mm)
Fastener stations · 127–140
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J127 · SCREW-RETENTION
VRSF → P03R
16.53 / 5.5 / 6.8454 in 419.86 / 139.70 / 173.87 mm
+X · 1 1/4 in (31.75 mm)
J128 · SCREW-RETENTION
VRSB → P03R
16.53 / 12.5434 / 6.8454 in 419.86 / 318.60 / 173.87 mm
+X · 1 1/4 in (31.75 mm)
J129 · SCREW-RETENTION
RF → P02
5.284 / 3.5 / 34.53 in 134.21 / 88.90 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J130 · SCREW-RETENTION
RF → P02
7.4512 / 3.5 / 34.53 in 189.26 / 88.90 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J131 · SCREW-RETENTION
RF → P02
10.702 / 3.5 / 34.53 in 271.83 / 88.90 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J132 · SCREW-RETENTION
RF → P02
13.411 / 3.5 / 34.53 in 340.64 / 88.90 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J133 · SCREW-RETENTION
RB → P02
5.284 / 14.336 / 34.53 in 134.21 / 364.13 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J134 · SCREW-RETENTION
RB → P02
7.4512 / 14.336 / 34.53 in 189.26 / 364.13 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J135 · SCREW-RETENTION
RB → P02
10.702 / 14.336 / 34.53 in 271.83 / 364.13 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J136 · SCREW-RETENTION
RB → P02
13.411 / 14.336 / 34.53 in 340.64 / 364.13 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J137 · SCREW-RETENTION
RL → P02
2.575 / 5.6672 / 34.53 in 65.41 / 143.95 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J138 · SCREW-RETENTION
RL → P02
2.575 / 8.3762 / 34.53 in 65.41 / 212.76 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J139 · SCREW-RETENTION
RL → P02
2.575 / 11.627 / 34.53 in 65.41 / 295.33 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J140 · SCREW-RETENTION
RR → P02
15.5782 / 5.6672 / 34.53 in 395.69 / 143.95 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
Fastener stations · 141–154
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J141 · SCREW-RETENTION
RR → P02
15.5782 / 8.3762 / 34.53 in 395.69 / 212.76 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J142 · SCREW-RETENTION
RR → P02
15.5782 / 11.627 / 34.53 in 395.69 / 295.33 / 877.06 mm
+Z · 1 1/4 in (31.75 mm)
J143 · SCREW-RETENTION
S01 → FBB
5 / 2 / 4.47 in 127.00 / 50.80 / 113.54 mm
−Y · 1 1/4 in (31.75 mm)
J144 · SCREW-RETENTION
S02 → CFT
5 / 1.625 / 33.28 in 127.00 / 41.27 / 845.31 mm
+Z · 1 1/4 in (31.75 mm)
J145 · SCREW-RETENTION
S01 → FBB
9 / 2 / 4.47 in 228.60 / 50.80 / 113.54 mm
−Y · 1 1/4 in (31.75 mm)
J146 · SCREW-RETENTION
S02 → CFT
9 / 1.625 / 33.28 in 228.60 / 41.27 / 845.31 mm
+Z · 1 1/4 in (31.75 mm)
J147 · SCREW-RETENTION
S01 → FBB
13 / 2 / 4.47 in 330.20 / 50.80 / 113.54 mm
−Y · 1 1/4 in (31.75 mm)
J148 · SCREW-RETENTION
S02 → CFT
13 / 1.625 / 33.28 in 330.20 / 41.27 / 845.31 mm
+Z · 1 1/4 in (31.75 mm)
J149 · SCREW-GLAZING
BL + QL → DBL
3.4075 / 1.8125 / 7.5 in 86.55 / 46.04 / 190.50 mm
−Y · 1 in (25.4 mm)
J150 · SCREW-GLAZING
BL + QL → DBL
3.4075 / 1.8125 / 12.5 in 86.55 / 46.04 / 317.50 mm
−Y · 1 in (25.4 mm)
J151 · SCREW-GLAZING
BL + QL → DBL
3.4075 / 1.8125 / 17.5 in 86.55 / 46.04 / 444.50 mm
−Y · 1 in (25.4 mm)
J152 · SCREW-GLAZING
BL + QL → DBL
3.4075 / 1.8125 / 22.5 in 86.55 / 46.04 / 571.50 mm
−Y · 1 in (25.4 mm)
J153 · SCREW-GLAZING
BL + QL → DBL
3.4075 / 1.8125 / 27.5 in 86.55 / 46.04 / 698.50 mm
−Y · 1 in (25.4 mm)
J154 · SCREW-GLAZING
BL + QL → DBL
3.4075 / 1.8125 / 31.5 in 86.55 / 46.04 / 800.10 mm
−Y · 1 in (25.4 mm)
Fastener stations · 155–168
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
J155 · SCREW-GLAZING
BR + QR → DBR
14.53 / 1.8125 / 7.5 in 369.06 / 46.04 / 190.50 mm
−Y · 1 in (25.4 mm)
J156 · SCREW-GLAZING
BR + QR → DBR
14.53 / 1.8125 / 12.5 in 369.06 / 46.04 / 317.50 mm
−Y · 1 in (25.4 mm)
J157 · SCREW-GLAZING
BR + QR → DBR
14.53 / 1.8125 / 17.5 in 369.06 / 46.04 / 444.50 mm
−Y · 1 in (25.4 mm)
J158 · SCREW-GLAZING
BR + QR → DBR
14.53 / 1.8125 / 22.5 in 369.06 / 46.04 / 571.50 mm
−Y · 1 in (25.4 mm)
J159 · SCREW-GLAZING
BR + QR → DBR
14.53 / 1.8125 / 27.5 in 369.06 / 46.04 / 698.50 mm
−Y · 1 in (25.4 mm)
J160 · SCREW-GLAZING
BR + QR → DBR
14.53 / 1.8125 / 31.5 in 369.06 / 46.04 / 800.10 mm
−Y · 1 in (25.4 mm)
J161 · SCREW-GLAZING
BB + QB → DBB
6 / 1.8125 / 5.43875 in 152.40 / 46.04 / 138.14 mm
−Y · 1 in (25.4 mm)
J162 · SCREW-GLAZING
BB + QB → DBB
12 / 1.8125 / 5.43875 in 304.80 / 46.04 / 138.14 mm
−Y · 1 in (25.4 mm)
J163 · SCREW-GLAZING
BT + QT → DBT
6 / 1.8125 / 33.06125 in 152.40 / 46.04 / 839.76 mm
−Y · 1 in (25.4 mm)
J164 · SCREW-GLAZING
BT + QT → DBT
12 / 1.8125 / 33.06125 in 304.80 / 46.04 / 839.76 mm
−Y · 1 in (25.4 mm)
HP1 · H05
HP-base → FAR
16.1 / -0.03875 / 19 in 408.94 / -0.98 / 482.60 mm
+Y · 5/8 in (15.88 mm)
HP2 · H05
HP-base → FAR
16.47 / -0.03875 / 19.5 in 418.34 / -0.98 / 495.30 mm
+Y · 5/8 in (15.88 mm)
HP3 · H05
HP-base → FAR
16.57 / -0.03875 / 18.5 in 420.88 / -0.98 / 469.90 mm
+Y · 5/8 in (15.88 mm)
ST1 · H05
ST-base → DAR
14.22 / -0.03875 / 18.44 in 361.19 / -0.98 / 468.38 mm
+Y · 5/8 in (15.88 mm)
Fastener stations · 169–182
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
ST2 · H05
ST-base → DAR
15.34 / -0.03875 / 18.44 in 389.64 / -0.98 / 468.38 mm
+Y · 5/8 in (15.88 mm)
ST3 · H05
ST-base → DAR
14.22 / -0.03875 / 19.56 in 361.19 / -0.98 / 496.82 mm
+Y · 5/8 in (15.88 mm)
ST4 · H05
ST-base → DAR
15.34 / -0.03875 / 19.56 in 389.64 / -0.98 / 496.82 mm
+Y · 5/8 in (15.88 mm)
H1F1 · SCREW-RETENTION
H1-fixed + SP-H1-fixed + FAL → FBL
1.5625 / -0.17375 / 8.3425 in 39.69 / -4.41 / 211.90 mm
+Y · 1 1/4 in (31.75 mm)
H1F2 · SCREW-RETENTION
H1-fixed + SP-H1-fixed + FAL → FBL
1.3425 / -0.17375 / 9.3125 in 34.10 / -4.41 / 236.54 mm
+Y · 1 1/4 in (31.75 mm)
H1F3 · SCREW-RETENTION
H1-fixed + SP-H1-fixed + FAL → FBL
1.5625 / -0.17375 / 10.2825 in 39.69 / -4.41 / 261.18 mm
+Y · 1 1/4 in (31.75 mm)
H1D1 · SCREW-RETENTION
H1-moving + SP-H1-moving + DAL → DBL
3.0025 / -0.17375 / 8.3425 in 76.26 / -4.41 / 211.90 mm
+Y · 1 1/4 in (31.75 mm)
H1D2 · SCREW-RETENTION
H1-moving + SP-H1-moving + DAL → DBL
3.2225 / -0.17375 / 9.3125 in 81.85 / -4.41 / 236.54 mm
+Y · 1 1/4 in (31.75 mm)
H1D3 · SCREW-RETENTION
H1-moving + SP-H1-moving + DAL → DBL
3.0025 / -0.17375 / 10.2825 in 76.26 / -4.41 / 261.18 mm
+Y · 1 1/4 in (31.75 mm)
H2F1 · SCREW-RETENTION
H2-fixed + SP-H2-fixed + FAL → FBL
1.5625 / -0.17375 / 28.3425 in 39.69 / -4.41 / 719.90 mm
+Y · 1 1/4 in (31.75 mm)
H2F2 · SCREW-RETENTION
H2-fixed + SP-H2-fixed + FAL → FBL
1.3425 / -0.17375 / 29.3125 in 34.10 / -4.41 / 744.54 mm
+Y · 1 1/4 in (31.75 mm)
H2F3 · SCREW-RETENTION
H2-fixed + SP-H2-fixed + FAL → FBL
1.5625 / -0.17375 / 30.2825 in 39.69 / -4.41 / 769.18 mm
+Y · 1 1/4 in (31.75 mm)
H2D1 · SCREW-RETENTION
H2-moving + SP-H2-moving + DAL → DBL
3.0025 / -0.17375 / 28.3425 in 76.26 / -4.41 / 719.90 mm
+Y · 1 1/4 in (31.75 mm)
H2D2 · SCREW-RETENTION
H2-moving + SP-H2-moving + DAL → DBL
3.2225 / -0.17375 / 29.3125 in 81.85 / -4.41 / 744.54 mm
+Y · 1 1/4 in (31.75 mm)
Fastener stations · 183–187
Coordinates use the outside assembly datums. Named first members receive clearance holes; pine receivers receive stopped pilots. The four roof support screws seat flush in exterior 82° countersinks, with one washer, Keps nut and closed cover inside.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
H2D3 · SCREW-RETENTION
H2-moving + SP-H2-moving + DAL → DBL
3.0025 / -0.17375 / 30.2825 in 76.26 / -4.41 / 769.18 mm
+Y · 1 1/4 in (31.75 mm)
B-LB1-1 · L16
P02 + LB1 + RF → washer + locknut
4.2004 / 3.5 / 36 in 106.69 / 88.90 / 914.40 mm
−Z · 1 15/16 in (49.21 mm)
B-LB1-2 · L16
P02 + LB1 + RB → washer + locknut
4.2004 / 14.336 / 36 in 106.69 / 364.13 / 914.40 mm
−Z · 1 15/16 in (49.21 mm)
B-LB2-1 · L16
P02 + LB2 + RF → washer + locknut
8.5348 / 3.5 / 36 in 216.78 / 88.90 / 914.40 mm
−Z · 1 15/16 in (49.21 mm)
B-LB2-2 · L16
P02 + LB2 + RB → washer + locknut
8.5348 / 14.336 / 36 in 216.78 / 364.13 / 914.40 mm
−Z · 1 15/16 in (49.21 mm)
Machining envelopes
Outside assembly datums. Cut envelopes remove only their intersection with the named part. Use the operation’s actual-stock, pocket-depth and hardware trial before machining.
Cut / part
Lower X / Y / Z
Size X × Y × Z
P02-cut-1 / P02
3 in (76.2 mm) / 4 in (101.6 mm) / 35.18 in (893.57 mm)
12 in (304.8 mm) × 10 in (254 mm) × 0.92 in (23.37 mm)
P03L-cut-1 / P03L
-0.1 in (-2.54 mm) / 6 in (152.4 mm) / 5.72 in (145.29 mm)
0.92 in (23.37 mm) × 6 in (152.4 mm) × 2 in (50.8 mm)
P03R-cut-1 / P03R
17.18 in (436.37 mm) / 6 in (152.4 mm) / 5.72 in (145.29 mm)
0.92 in (23.37 mm) × 6 in (152.4 mm) × 2 in (50.8 mm)
P04-cut-1 / P04
6 in (152.4 mm) / 17.27 in (438.66 mm) / 33.905 in (861.19 mm)
6 in (152.4 mm) × 0.74 in (18.8 mm) × 1 1/4 in (31.75 mm)
FAL-cut-1 / FAL
1.0325 in (26.23 mm) / -0.01 in (-0.25 mm) / 7 13/16 in (198.44 mm)
1 3/16 in (30.16 mm) × 0.04125 in (1.05 mm) × 3 in (76.2 mm)
FAL-cut-2 / FAL
1.0325 in (26.23 mm) / -0.01 in (-0.25 mm) / 27 13/16 in (706.44 mm)
1 3/16 in (30.16 mm) × 0.04125 in (1.05 mm) × 3 in (76.2 mm)
FAR-cut-1 / FAR
15.79 in (401.07 mm) / -0.01 in (-0.25 mm) / 18 1/4 in (463.55 mm)
1.28 in (32.51 mm) × 0.04125 in (1.05 mm) × 1 1/2 in (38.1 mm)
VLB-cut-1 / VLB
0.71 in (18.03 mm) / 5 1/8 in (130.18 mm) / 4.845 in (123.06 mm)
0.135 in (3.43 mm) × 7 3/4 in (196.85 mm) × 3 3/4 in (95.25 mm)
Machining envelopes · continued
Outside assembly datums. Cut envelopes remove only their intersection with the named part. Use the operation’s actual-stock, pocket-depth and hardware trial before machining.
Cut / part
Lower X / Y / Z
Size X × Y × Z
VLT-cut-1 / VLT
0.71 in (18.03 mm) / 5 1/8 in (130.18 mm) / 4.845 in (123.06 mm)
0.135 in (3.43 mm) × 7 3/4 in (196.85 mm) × 3 3/4 in (95.25 mm)
VLSF-cut-1 / VLSF
0.71 in (18.03 mm) / 5 1/8 in (130.18 mm) / 4.845 in (123.06 mm)
0.135 in (3.43 mm) × 7 3/4 in (196.85 mm) × 3 3/4 in (95.25 mm)
VLSB-cut-1 / VLSB
0.71 in (18.03 mm) / 5 1/8 in (130.18 mm) / 4.845 in (123.06 mm)
0.135 in (3.43 mm) × 7 3/4 in (196.85 mm) × 3 3/4 in (95.25 mm)
VRB-cut-1 / VRB
17.155 in (435.74 mm) / 5 1/8 in (130.18 mm) / 4.845 in (123.06 mm)
0.135 in (3.43 mm) × 7 3/4 in (196.85 mm) × 3 3/4 in (95.25 mm)
VRT-cut-1 / VRT
17.155 in (435.74 mm) / 5 1/8 in (130.18 mm) / 4.845 in (123.06 mm)
0.135 in (3.43 mm) × 7 3/4 in (196.85 mm) × 3 3/4 in (95.25 mm)
VRSF-cut-1 / VRSF
17.155 in (435.74 mm) / 5 1/8 in (130.18 mm) / 4.845 in (123.06 mm)
0.135 in (3.43 mm) × 7 3/4 in (196.85 mm) × 3 3/4 in (95.25 mm)
VRSB-cut-1 / VRSB
17.155 in (435.74 mm) / 5 1/8 in (130.18 mm) / 4.845 in (123.06 mm)
0.135 in (3.43 mm) × 7 3/4 in (196.85 mm) × 3 3/4 in (95.25 mm)
RF-cut-1 / RF
2 3/8 in (60.33 mm) / 3 1/8 in (79.38 mm) / 35.155 in (892.94 mm)
13 1/4 in (336.55 mm) × 11 3/4 in (298.45 mm) × 0.135 in (3.43 mm)
Machining envelopes · continued
Outside assembly datums. Cut envelopes remove only their intersection with the named part. Use the operation’s actual-stock, pocket-depth and hardware trial before machining.
Cut / part
Lower X / Y / Z
Size X × Y × Z
RF-cut-2 / RF
3 1/2 in (88.9 mm) / 3 1/4 in (82.55 mm) / 35.0714 in (890.81 mm)
1 in (25.4 mm) × 3/4 in (19.05 mm) × 0.2186 in (5.55 mm)
RF-cut-3 / RF
8 in (203.2 mm) / 3 1/4 in (82.55 mm) / 35.0714 in (890.81 mm)
1 in (25.4 mm) × 3/4 in (19.05 mm) × 0.2186 in (5.55 mm)
RB-cut-1 / RB
2 3/8 in (60.33 mm) / 3 1/8 in (79.38 mm) / 35.155 in (892.94 mm)
13 1/4 in (336.55 mm) × 11 3/4 in (298.45 mm) × 0.135 in (3.43 mm)
RB-cut-2 / RB
3 1/2 in (88.9 mm) / 14 in (355.6 mm) / 35.0714 in (890.81 mm)
1 in (25.4 mm) × 3/4 in (19.05 mm) × 0.2186 in (5.55 mm)
RB-cut-3 / RB
8 in (203.2 mm) / 14 in (355.6 mm) / 35.0714 in (890.81 mm)
1 in (25.4 mm) × 3/4 in (19.05 mm) × 0.2186 in (5.55 mm)
RL-cut-1 / RL
2 3/8 in (60.33 mm) / 3 1/8 in (79.38 mm) / 35.155 in (892.94 mm)
13 1/4 in (336.55 mm) × 11 3/4 in (298.45 mm) × 0.135 in (3.43 mm)
RR-cut-1 / RR
2 3/8 in (60.33 mm) / 3 1/8 in (79.38 mm) / 35.155 in (892.94 mm)
13 1/4 in (336.55 mm) × 11 3/4 in (298.45 mm) × 0.135 in (3.43 mm)
V-roof-top-cut-1 / V-roof-top
3 in (76.2 mm) / 4 in (101.6 mm) / 35.18 in (893.57 mm)
12 in (304.8 mm) × 10 in (254 mm) × 0.92 in (23.37 mm)
Machining envelopes · continued
Outside assembly datums. Cut envelopes remove only their intersection with the named part. Use the operation’s actual-stock, pocket-depth and hardware trial before machining.
Cut / part
Lower X / Y / Z
Size X × Y × Z
V-P03L-face-cut-1 / V-P03L-face
-0.1 in (-2.54 mm) / 6 in (152.4 mm) / 5.72 in (145.29 mm)
0.92 in (23.37 mm) × 6 in (152.4 mm) × 2 in (50.8 mm)
V-P03R-face-cut-1 / V-P03R-face
17.18 in (436.37 mm) / 6 in (152.4 mm) / 5.72 in (145.29 mm)
0.92 in (23.37 mm) × 6 in (152.4 mm) × 2 in (50.8 mm)
V-back-cut-1 / V-back
6 in (152.4 mm) / 17.27 in (438.66 mm) / 33.905 in (861.19 mm)
6 in (152.4 mm) × 0.7615 in (19.34 mm) × 1 1/4 in (31.75 mm)
V-restraint-backing-cut-1 / V-restraint-backing
6 1/4 in (158.75 mm) / 17.27 in (438.66 mm) / 34.03 in (864.36 mm)
5 1/2 in (139.7 mm) × 0.1 in (2.54 mm) × 1 in (25.4 mm)
V-FAL-front-cut-1 / V-FAL-front
1.0325 in (26.23 mm) / -0.0315 in (-0.8 mm) / 7 13/16 in (198.44 mm)
1 3/16 in (30.16 mm) × 0.06275 in (1.59 mm) × 3 in (76.2 mm)
V-FAL-front-cut-2 / V-FAL-front
1.0325 in (26.23 mm) / -0.0315 in (-0.8 mm) / 27 13/16 in (706.44 mm)
1 3/16 in (30.16 mm) × 0.06275 in (1.59 mm) × 3 in (76.2 mm)
V-FAR-front-cut-1 / V-FAR-front
15.79 in (401.07 mm) / -0.0315 in (-0.8 mm) / 18 1/4 in (463.55 mm)
1.28 in (32.51 mm) × 0.06275 in (1.59 mm) × 1 1/2 in (38.1 mm)
Inspection records
Receiving and physical acceptance record
Leave blank until measured or performed. A render, calculation or automated check does not fill these fields.
Required checkpoint
Actual result / date / reviewer
H01 · Hinge mounting and removal Supplier/qualified acceptance of equal full-leaf spacers, reference 1/8 in (3.18 mm) minimum 7/64 in (2.78 mm). Actual pin head ≤3/8 in (9.53 mm), total length ≤3 7/16 in (87.31 mm). Trial twelve #8 × 1¼-inch screws, supported 100-degree swing and roof-on pin removal. No load rating.
___________________
___________________
___________________
H02 · Hasp plate support and release Actual N305-979 footprint and holes must remain on wood; reference latch-edge margin only 0.0175 in (0.44 mm). Seven #10 × 5/8 in (15.88 mm) screws and full hand release trial. Approximate metal forming is not manufacturer CAD.
___________________
___________________
___________________
Glue time: __________ · Last coating/repair: __________ Temperature / humidity: __________ · Full cure due: __________ Confirmed PSA dwell: __________ · Physical acceptance: __________
Receiving and physical acceptance record
Leave blank until measured or performed. A render, calculation or automated check does not fill these fields.
Required checkpoint
Actual result / date / reviewer
H03 · Complete veneer system Confirm species, PSA/backing, substrate/sealer, balancing, indoor environment, acclimation, pressure and dwell with supplier. Finished stack ≤0.046 in (1.17 mm); closed reveals ≥1/16 in (1.59 mm) and clear full swing. Added layers require dimensional revision.
___________________
___________________
___________________
H04 · Stock and cured glazing coupon Measure actual 0.72 in (18.29 mm) plywood, planed pine layers, acrylic and both plain EPDM rings. Confirm exact contact compatibility. Reference 5/16 in (7.94 mm) spacer yields 26% nominal foam deflection; cured coupon must seat caps with flat quiet pane and free edges, no forced screw pressure.
___________________
___________________
___________________
Glue time: __________ · Last coating/repair: __________ Temperature / humidity: __________ · Full cure due: __________ Confirmed PSA dwell: __________ · Physical acceptance: __________
Receiving and physical acceptance record
Leave blank until measured or performed. A render, calculation or automated check does not fill these fields.
Required checkpoint
Actual result / date / reviewer
H05 · Screens, steel, bolts and caps Measure half-inch cloth and wire crossings ≤3/32 in (2.38 mm), actual clear cells, recessed lands, support strips, washers and Keps nuts. Confirm cap depth and positive threads; cover tails without changing primary nut retention. Actual open-cell drilling and no trapped wire. Trial the actual 82-degree flat head in matching plywood before cutting the roof. The head must seat flush with bare wood, without splitting, crushing or excess depth. Published maximum head height 0.153 in (3.89 mm) leaves 0.567 in (14.4 mm) of reference plywood; actual product controls. Keep 1/2 in (12.7 mm) veneer access open. Prove Phillips #3 and two thin 7/16 in (11.11 mm) wrench access; reference socket envelope ≤3/4 in (19.05 mm). Tail 1/8 in (3.18 mm) – 7/32 in (5.56 mm) before ≤1/64 in (0.4 mm) chamfer, at least two full threads and ≥1/32 in (0.79 mm) unused cap depth. Treat cut steel only with an accepted compatible corrosion system. No exterior washer.
___________________
___________________
___________________
H06 · Coating, veneer balance, bond and cleaners Varathane excludes floors: obtain disposition for enclosure floor exposure/abrasion and actual cleaning system. Confirm veneer/sealer/topcoat compatibility. Observe actual glue, adhesive and finish waits. No animal-safety inference.
___________________
___________________
___________________
Glue time: __________ · Last coating/repair: __________ Temperature / humidity: __________ · Full cure due: __________ Confirmed PSA dwell: __________ · Physical acceptance: __________
Receiving and physical acceptance record
Leave blank until measured or performed. A render, calculation or automated check does not fill these fields.
Required checkpoint
Actual result / date / reviewer
H07 · Support, equipment and physical commissioning Full-base support/floor capacity, actual completed load, stability and containment need physical/qualified review. Fixture ≤2 pounds is proposed untested load; rigid rim 5½–6 in (152.4 mm), overall ≤6 in (152.4 mm), four actual strip contacts and thermal commissioning required. No species approval. Obtain qualified acceptance of the new countersunk bearing and clamp force, cap retention and thermal exposure. No torque or connection capacity is established by the digital model.
___________________
___________________
___________________
H08 · Tall-shell anti-tip installation Receive exact Hillman9976524 complete kit. Bench-prove bracket, cable, clevis, cotter, two short furniture screws and straight driver access through finished window. Direct solid-CBT bearing, actual shaft avoidance and service removal required. Confirm documented stud-wall fixing, cable reach, full load path and wall services; drywall alone is not a receiver.
___________________
___________________
___________________
Glue time: __________ · Last coating/repair: __________ Temperature / humidity: __________ · Full cure due: __________ Confirmed PSA dwell: __________ · Physical acceptance: __________
Sources, limits and upkeep
Product identity, local stock, received measurements and assembly acceptance are separate questions. Current product links and retrieval evidence are in the review packet.
Separate statuses: research, dimensions, calculations and digital validation have individual evidence. No prototype has been built; physical testing and qualified review have not been performed. Publication is separate from construction acceptance.
This is an indoor non-immersed wooden shell with no liner or water-holding claim. Keep wet areas in separate removable leakproof containers. Disconnect equipment, secure the animal elsewhere and empty the enclosure before maintenance. Follow the pictured removal and cleaning sequence.
Full exterior veneer is included in this guide’s schedule and geometry, subject to supplier balance, bond and actual-stack acceptance. Texture scans illustrate appearance; natural grain and color vary by delivered sheet.