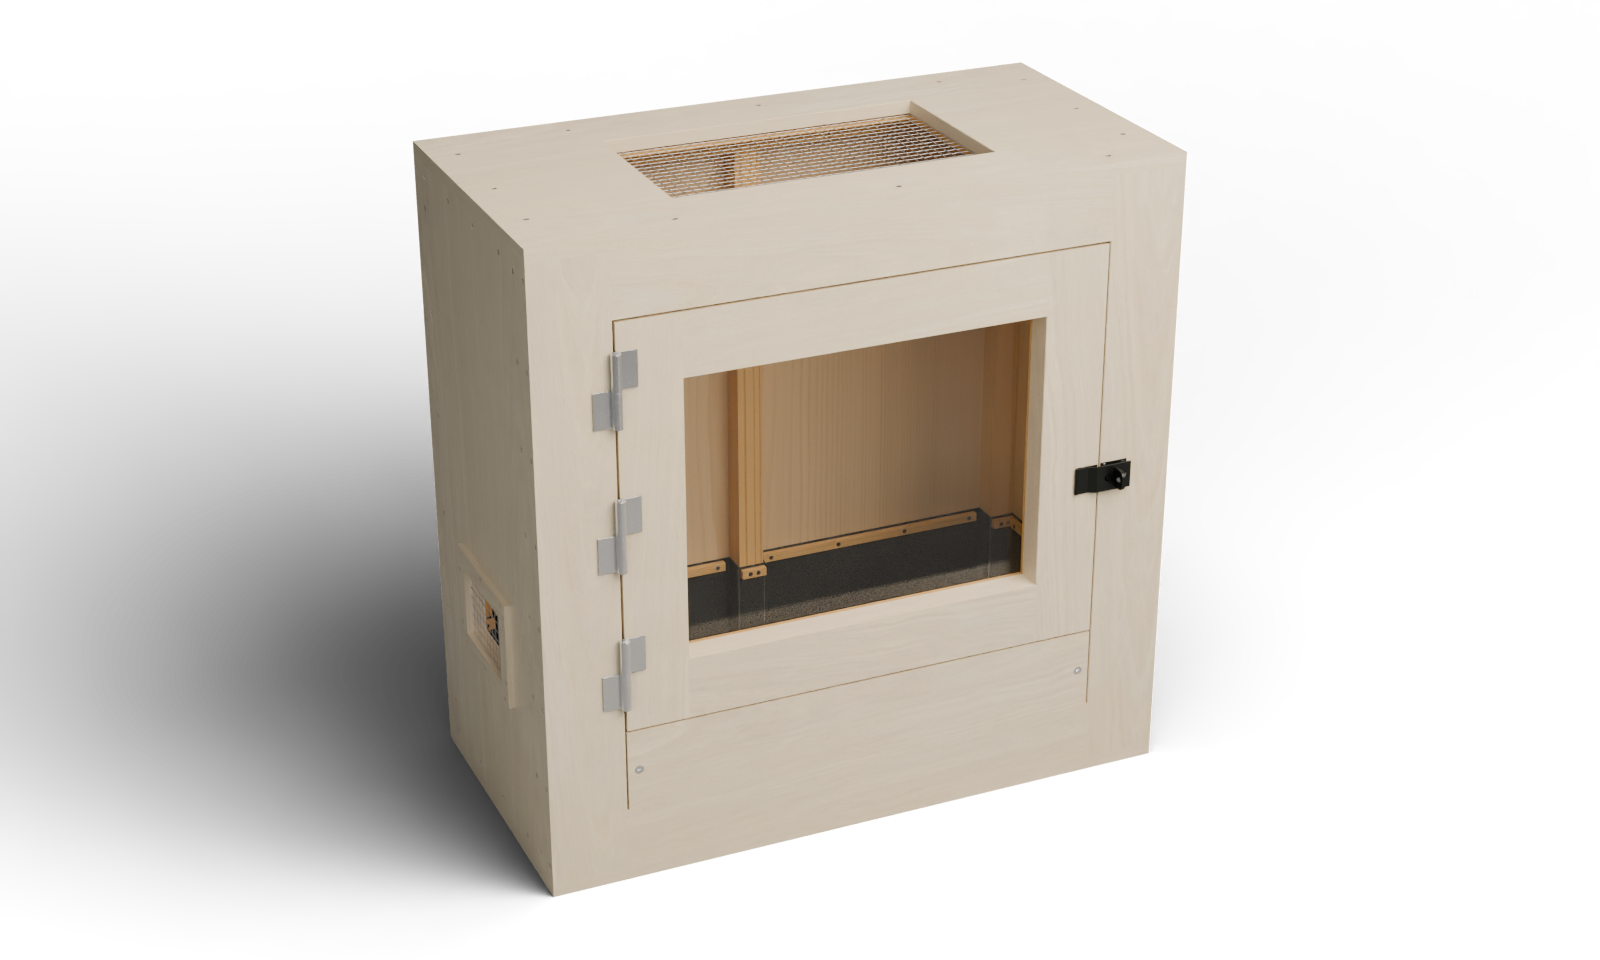
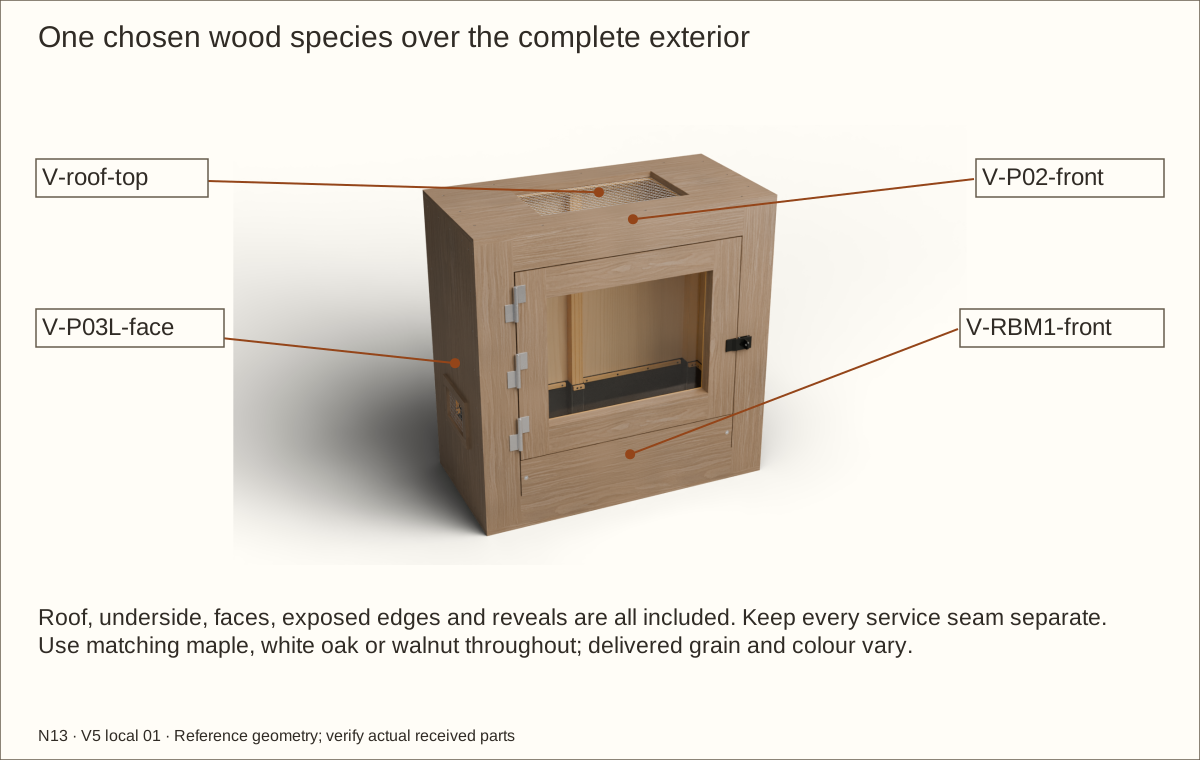
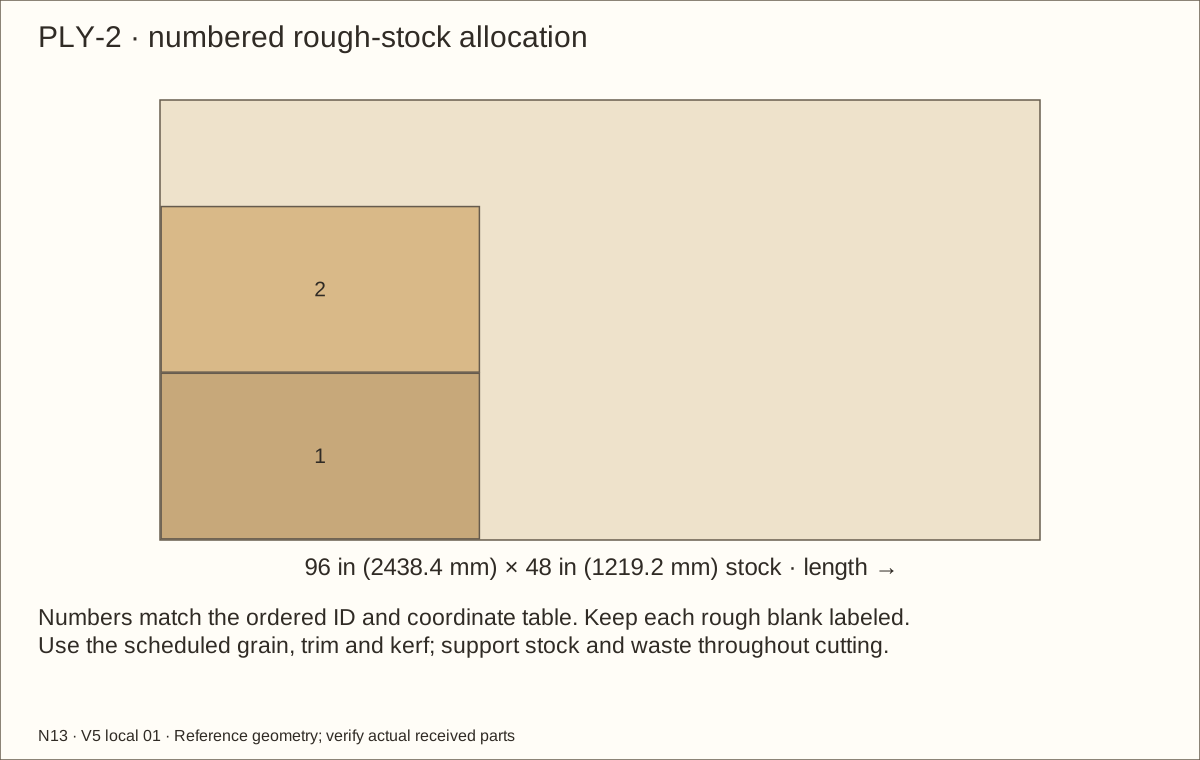
Full exterior veneer: the roof, faces, edges and reveals are included in this guide’s coordinated veneer schedule and geometry. Supplier balance, bond and actual-stack acceptance remain required. Natural grain and color vary.
About these previews
Rendered from this enclosure’s actual reference geometry. Veneer layers preserve service seams and bare hasp seats. Hinges bear on the accepted cured face veneer. The 3D viewer shows maple; these choices change the main picture. Texture scans by Jenelle van Heerden via Poly Haven, CC0 illustrate appearance and are not delivered veneer samples.
One lift-off acrylic door, a one-piece lined bed behind a removable three-layer retainer, and one screened roof opening. Follow 67 pictured operations with named parts, required waits and checks before continuing.
This is the individual N13 hinged lined design. Receive, measure and trial exact materials before dependent final cuts. A changed plywood gauge, lining, hardware or veneer system requires coordinated recalculation.
Measurement
Reference
Bare case
36 × 18 × 36 in (914.4 × 457.2 × 914.4 mm)
Reference covered wood
36.061 in (915.95 mm) × 18.061 in (458.75 mm) × 36.061 in (915.95 mm)
Maximum covered wood
36.092 in (916.74 mm) × 18.092 in (459.54 mm) × 36.092 in (916.74 mm)
External capture width
36.811 in (935 mm); allow additional hardware/service room
Finished floor / bed
Floor 53/64 in (21.03 mm) above underside; maximum total bed 6 in (152.4 mm)
Bare leaf size
27 1/4 in (692.15 mm) × 22 19/32 in (573.88 mm) × 1 1/2 in (38.1 mm)
Bare opening above retainer
27 19/32 in (700.88 mm) × 22 31/32 in (583.41 mm)
Removed-door opening
27.53275 in (699.33 mm) × 22.90775 in (581.86 mm) at reference veneer
Complete veneer layer
Reference 0.0305 in (0.77 mm); maximum 0.046 in (1.17 mm)
Datums: assembly X starts at outside LEFT, Y at outside FRONT and Z at FLOOR UNDERSIDE, unless a local part edge is explicitly named. in means inches; mm means millimetres. Exact mating decimals are retained; actual received measurements govern.
Tools, terms and safe workholding
Prepare a padded flat bench, helper, clamps, straight cauls, tape, square, marking knife, straightedge, caliper and drill depth stops. Use supported saw/router/jigsaw setups and sacrificial backing. Follow each tool maker’s guards and minimum feed lengths; never feed narrow short strips without a suitable carrier.
For retainer trials: 1-inch (25.4 mm) flat-bottom boring bit with a 5/8-inch (15.88 mm) stop, 9/32-inch (7.14 mm) through bit, 82-degree countersink, 5/32-inch (3.97 mm) hex key and 7/16-inch (11.11 mm) socket no wider than 7/8 inch (22.23 mm). Prove actual bit-point depth and driver/socket clearance on matching scrap. Use root-matched wood pilots and correct hand drivers. Mesh needs snips and edge protection; veneer needs a sharp knife and supplier-specified pressure tool. Use the acrylic maker’s accepted supported cutting and edge-finishing method.
Wear eye/hearing protection, control dust and ventilate adhesives/coatings. Protect hands while handling wire and metal; keep gloves and loose clothing away from rotating tools. Support both work and waste.
Term
Plain meaning
Cleat / lamination
Wood strip receiving screws / layers joined face to face
Jamb / header / retainer
Side of the opening / top frame member / removable front bed wall
Rear edge cut narrower for swing clearance / supported upward removal from hinge pins
PSA / RH
Pressure-sensitive adhesive / relative humidity
EPDM / mil
Ethylene propylene diene monomer rubber / one thousandth of an inch
Record the actual stock and shared heights
Plywood thickness: t = ______ in / ______ mm Compressed underlay + liner: a = ______ in / ______ mm Finished-floor elevation: F = t + a = ______
Part / elevation
Equation in inches
Reference
Floor / roof
36 × 18
36 × 18 in (914.4 × 457.2 mm)
Side height
36 − 2t
34 19/32 in (878.68 mm)
Back width
36 − 2t
34 19/32 in (878.68 mm)
Fixed frame / bare bay width
36 − 2t − 2 × 3.5
27 19/32 in (700.88 mm)
Retainer width
Bare bay width − 2 × 5/32
27 9/32 in (692.94 mm)
Retainer top
F + 8
8 53/64 in (224.23 mm)
Retainer height
F + 8 − (t + 3.5)
4 5/8 in (117.48 mm)
Maximum bed top
F + 6
6 53/64 in (173.43 mm)
Clamp screw centre
F + 7 3/8
8 13/64 in (208.36 mm)
Liner top
F + 7 3/4
8 37/64 in (217.88 mm)
These equations retain the original core and nominal frame sections. They do not automatically update all joints, hole stations, hinge axes or glazing sizes. Recalculate the entire coordinated candidate whenever a measured input changes. Transfer shared heights with a marked measuring strip.
Why the hinge face stack matters
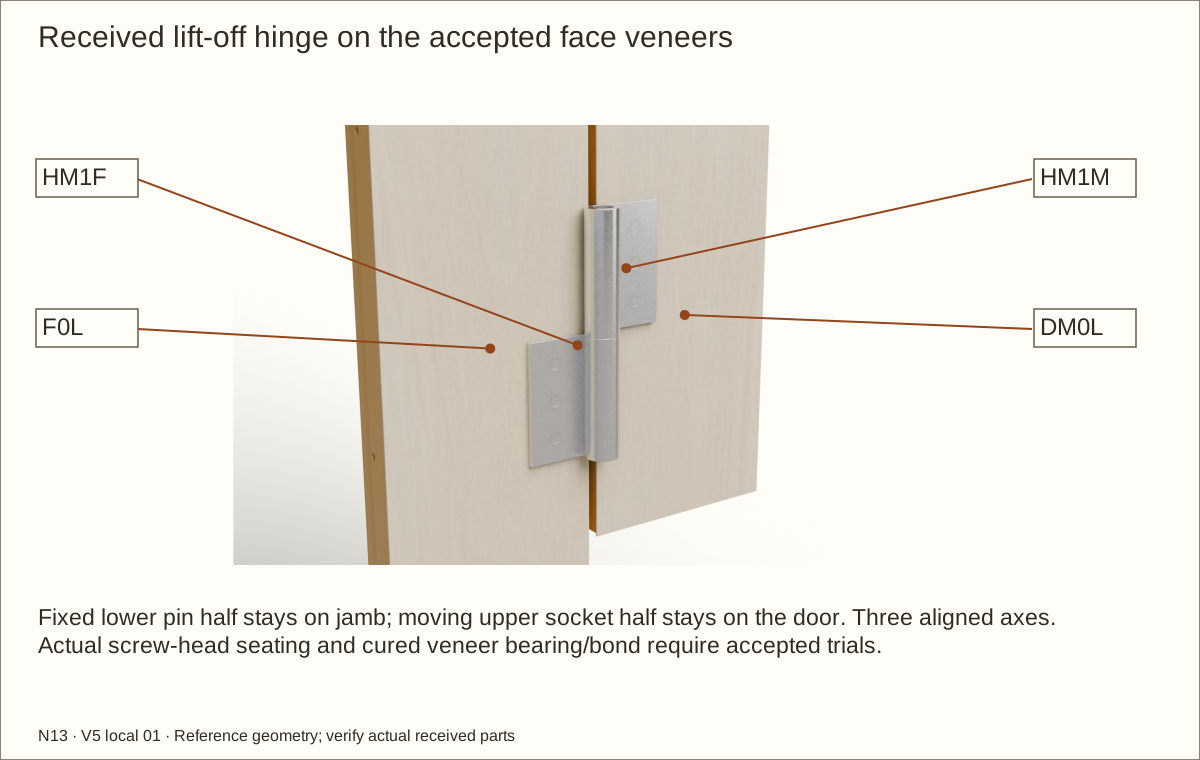
Both lift-off halves mount on equal accepted cured veneer faces
The reference barrel is tangent to its mounting plane. Recessing only the flat leaf into veneer makes that barrel rub the remaining skin. Here the complete unaltered hinge and shared axis move forward by the actual cured face stack: 0.0305 in (0.77 mm) at reference. Keep both bearing faces equally thick, flat, fully bonded and accepted for compression under the leaves. The actual screw heads, supplied holes, bond and bearing require a qualified material trial before drilling the real frame.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Qualify the support and service position — 1
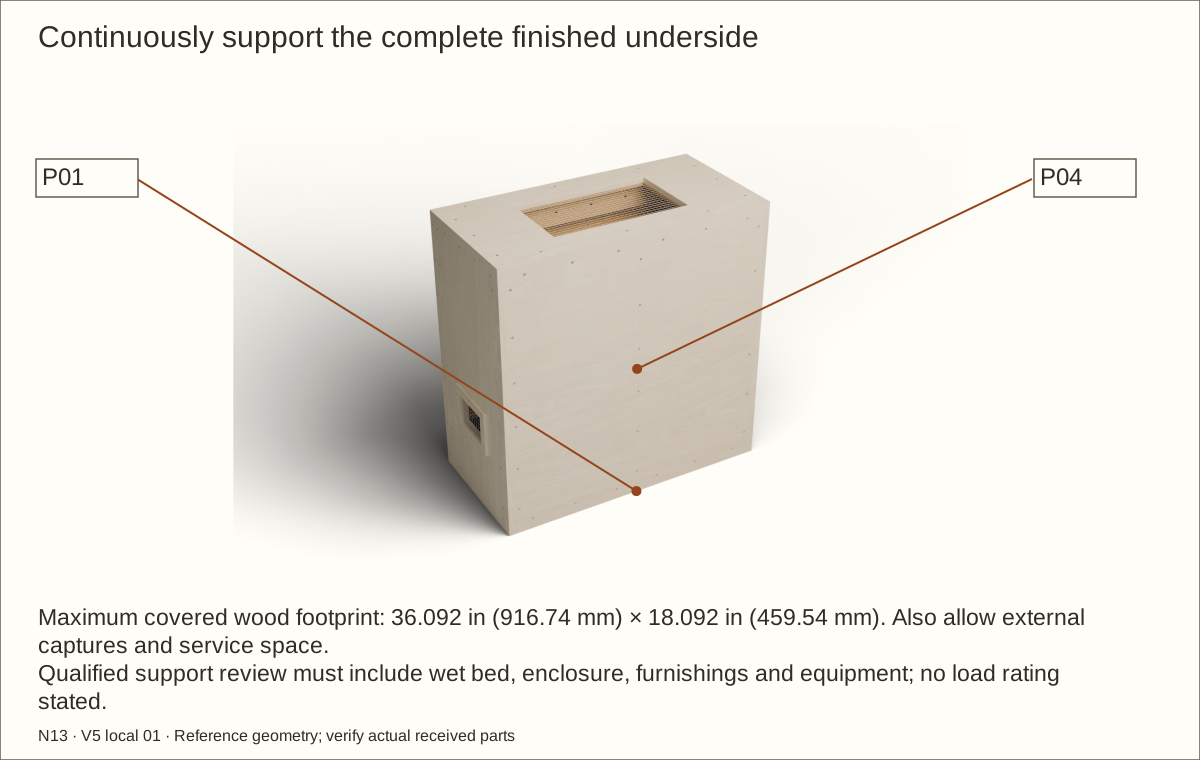
Choose a level, rigid support beneath the entire finished underside, at least 36.092 in (916.74 mm) wide × 18.092 in (459.54 mm) deep. Every edge must bear continuously. This guide does not design the stand or qualify the building floor.
The conservative bed envelope is 1.78 cubic feet (50 L), before framing displacement. At an assumed wet bulk density of 100 lb/ft³ (1602 kg/m³), the bed alone would weigh 178 lb (81 kg). Add the shell, water, rocks, furnishings and equipment when qualifying both furniture and building floor.
Check before continuing: Qualified support and the full wet-load planning assumptions are recorded before construction.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Qualify the support and service position — 2
Keep at least 32 in (812.8 mm) of clear working space in front, 6 in (152.4 mm) beside the door swing and room for complete roof removal. Allow at least 2 in (50.8 mm) upward lift above the opened leaf. The side captures make the reference width 36.811 in (935 mm); include that in the empty transport and service plan.
Place and stabilize the empty enclosure at its final location. Provide furniture restraint appropriate to that support and wall where tipping is possible. Never stack, suspend, climb on, lift or tip the loaded shell.
Check before continuing: The entire floor is supported and the load and cleaning routes have been checked before construction.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Receive and measure all materials — 1
Measure the actual thickness of the specified nominal 3/4 in (19.05 mm) plywood at several points. Check pine is 3/4 in (19.05 mm) thick and solid wood supports are 1 1/2 in (38.1 mm) square. Reject warped, split or damaged wood and knots at joints.
Receive three Sugatsune LSX-100R lift-off hinges of the same hand, one National N305-979 swivel hasp and their specified screws. Identify the lower fixed pin half and upper removable socket by the actual manufacturer drawing. Never choose the hand only from the everyday name “left-hung.” Confirm each actual metal hole accepts its specified head without unauthorized machining.
Check before continuing: Plywood gauge, liner and underlay are identified, and all three hinges match the specified hand.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Receive and measure all materials — 2
Measure the actual acrylic sold as 0.22 in (5.59 mm) thick, both separate uncompressed 1/16 in (1.59 mm) neoprene pads, and the cured film on the contact samples. The bare spacer starts at 0.351 in (8.92 mm) to leave a finished 0.345 in (8.76 mm) cavity after two 0.003 in (0.08 mm) reference contact films. The lining reference is 0.08 in (2.03 mm) compressed underlay plus 0.045 in (1.14 mm) EPDM, totaling 1/8 in (3.18 mm); measure this actual stack rather than assuming a delivered gauge.
On a spare strip, mark the underside of the floor. Above it, mark the actual plywood thickness plus the compressed lining thickness to locate the finished floor. From that finished-floor mark, measure up 6 in (152.4 mm) for the maximum bed, 8 in (203.2 mm) for the retaining-panel top and 9 in (228.6 mm) for the vent bottom. Transfer these marks to the build.
Check before continuing: All materials and handed hardware are identified; actual plywood and compressed lining thicknesses are recorded.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Support both sides of every cut and use eye/hearing/dust protection. Never reach across a running blade.
Cut and identify the plywood — 1
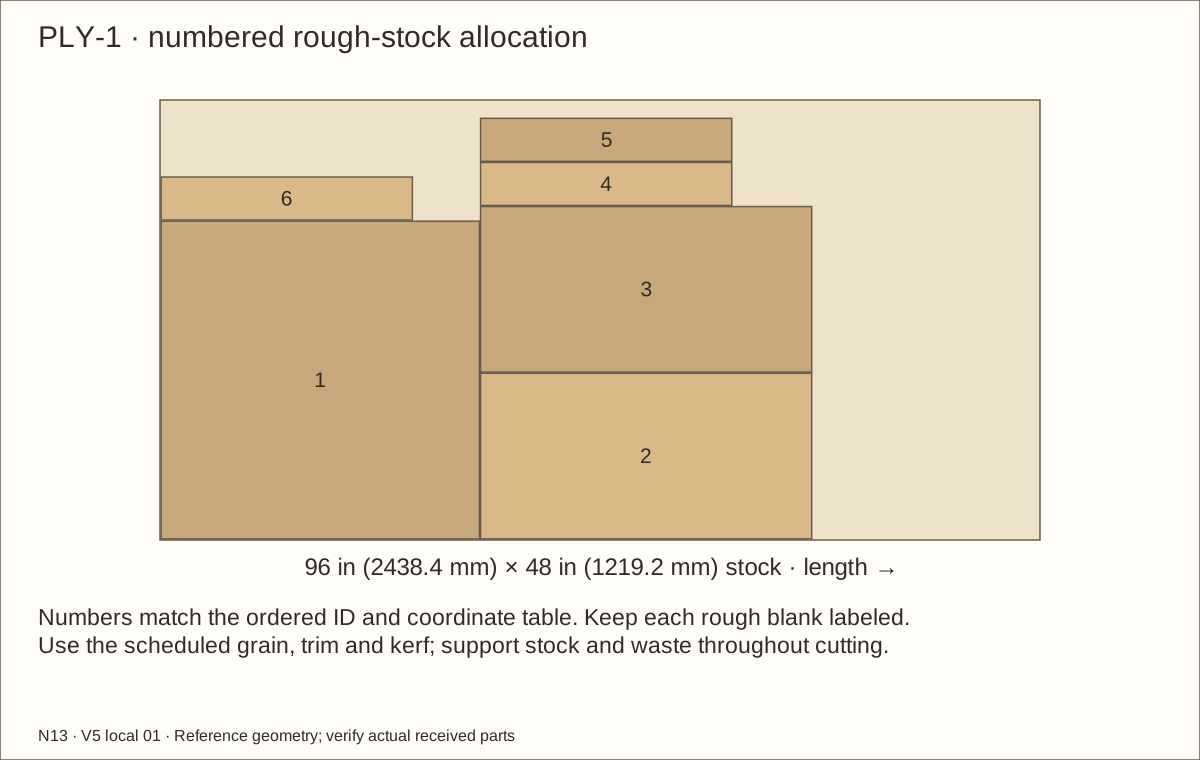
Use this build’s two plywood-sheet layouts. Establish a square edge, label the face and keep 1/8 in (3.18 mm) saw-cut waste between adjacent rough blanks. Floor P01 and roof P02 finish at 36 in (914.4 mm) × 18 in (457.2 mm) with grain along the 36 in (914.4 mm) direction. Support both sides of each cut.
For the 45/64 in (17.86 mm) reference plywood, each side finishes at 18 in (457.2 mm) × 34 19/32 in (878.68 mm) and the back at 34 19/32 in (878.68 mm) × 34 19/32 in (878.68 mm). Fit the sides between floor and roof to maintain the 36 in (914.4 mm) bare-case height, and fit the back between the actual side panels. The exact rough allowances and grain directions are in the current cut list.
Check before continuing: Floor, roof, paired side and back panels are labeled and square to the actual plywood gauge.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Support both sides of every cut and use eye/hearing/dust protection. Never reach across a running blade.
Cut and identify the plywood — 2
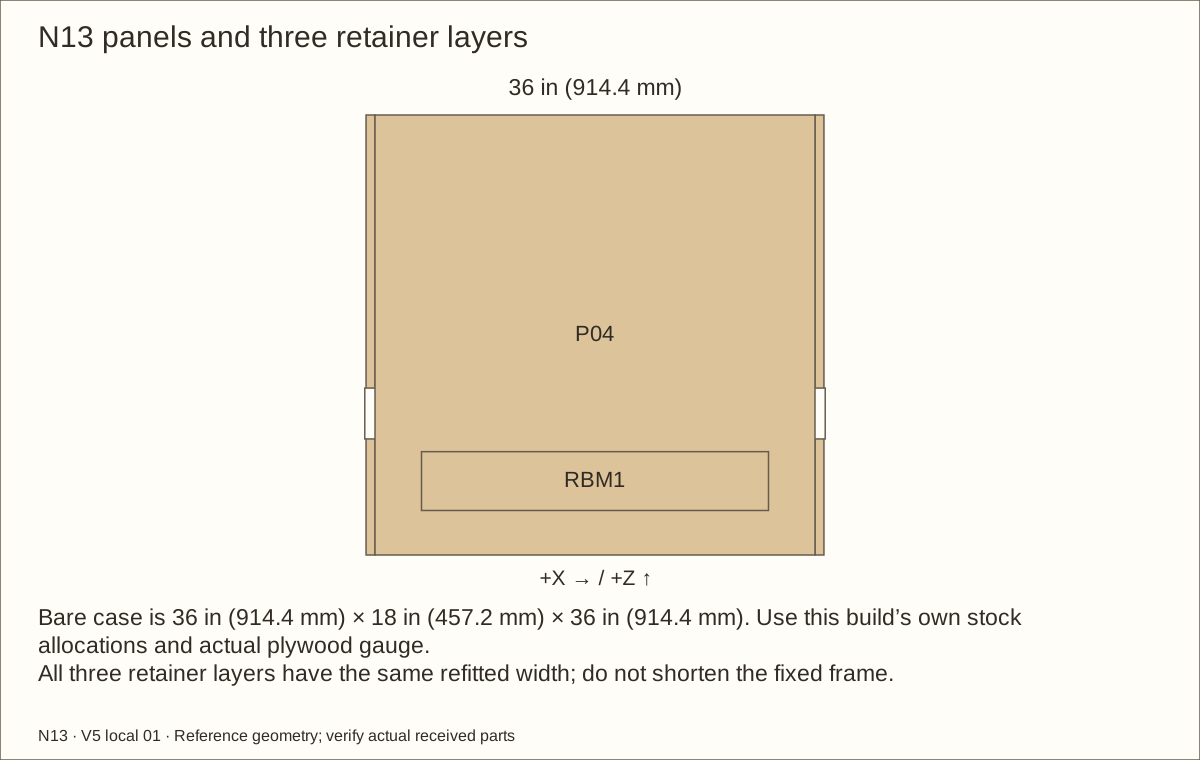
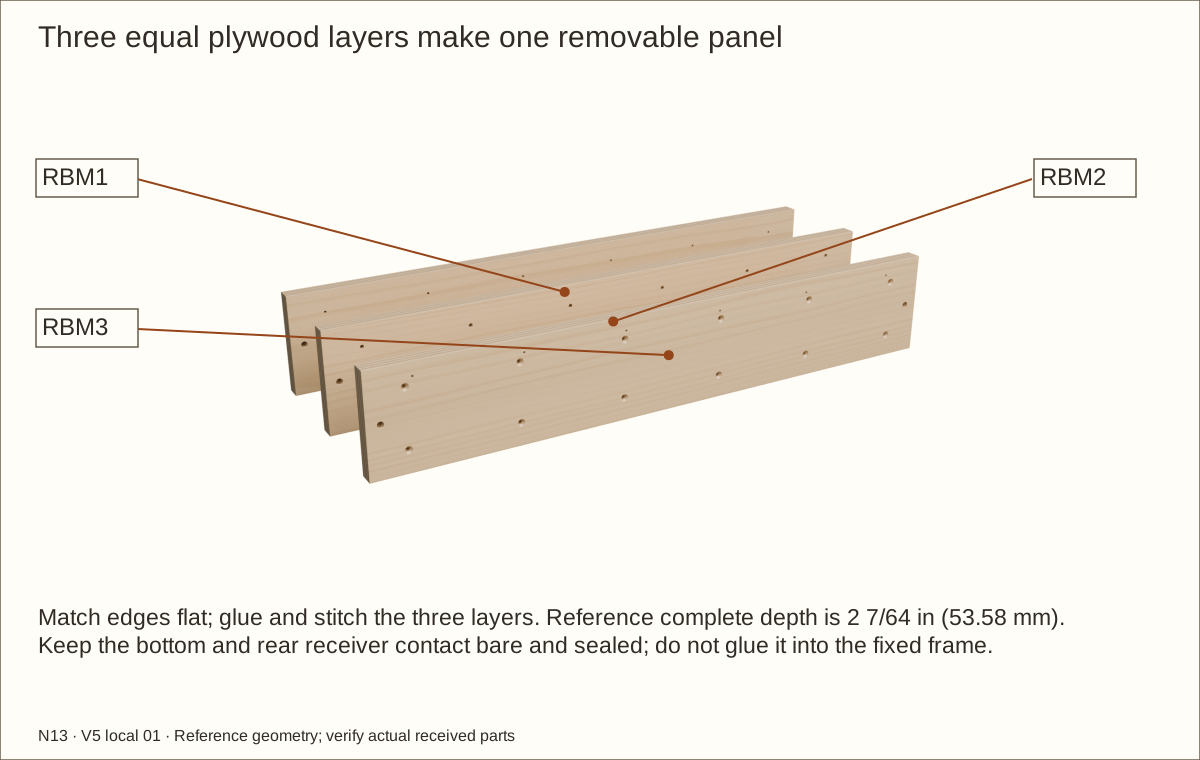
Cut the three RBM retainer layers to matching rough blanks, then fit each to 27 9/32 in (692.94 mm) wide × 4 5/8 in (117.48 mm) high at the reference gauge. Keep grain across the width. The refitted panel has 5/32 in (3.97 mm) bare space at each side for opposing veneer. Its hidden bottom bears directly on the sealed fixed kick rail; do not veneer that bearing surface.
Label each part, its inside face and its measuring edge before cutting it free. Use inch markings throughout each cut. The metric values are rounded equivalents. Sizes marked “about” are starting marks; fit them to the actual adjoining parts before the final cut.
Check before continuing: Paired side panels and all three retainer layers are square, labeled and matched.
Tools / setup: Measuring tape, square, pencil and the tools named below
Cut the roof opening and side vents — 1
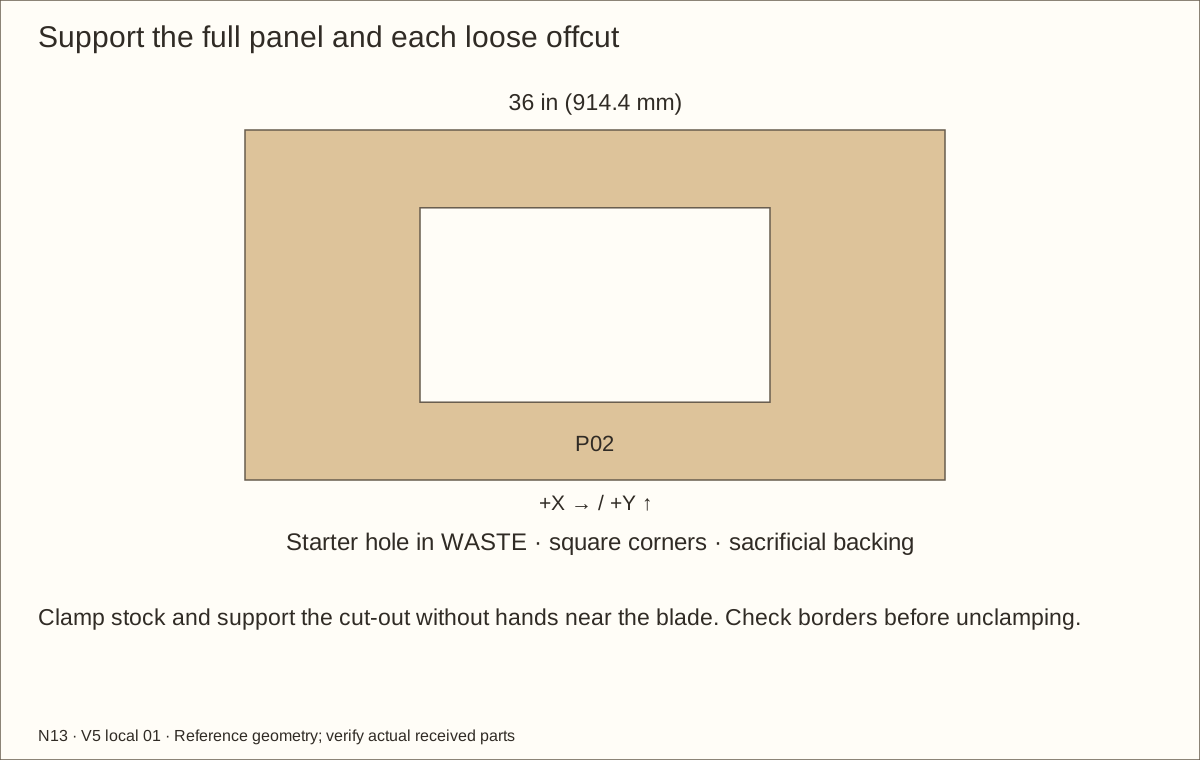
Mark one 18 in (457.2 mm) × 10 in (254 mm) roof opening, with its left edge 9 in (228.6 mm) from the left and its front edge 4 in (101.6 mm) from the front. Keep all four borders intact.
On each side, mark a 6 in (152.4 mm) × 4 in (101.6 mm) vent starting 6 in (152.4 mm) behind the front. Its bottom is 9 in (228.6 mm) above the finished-floor mark, not above the panel’s lower edge.
Check before continuing: Roof and both vent outlines match this build and its actual finished-floor datum before cutting.
Tools / setup: Measuring tape, square, pencil and the tools named below
Cut the roof opening and side vents — 2
Drill starter holes inside the waste and use a guided router or supported jigsaw. Stay inside the corner lines, ease the reveals and remove all splinters.
Dry-place the capture strips and check their screws land in solid wood outside each opening. The inner reveal stays smooth; the outer strips capture the cut wire edges.
Check before continuing: Vents begin 3 in (76.2 mm) above the maximum fill; all roof borders remain.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Plane broad supported stock first; never feed short thin strips alone.
Prepare the frame stock and thin strips — 1
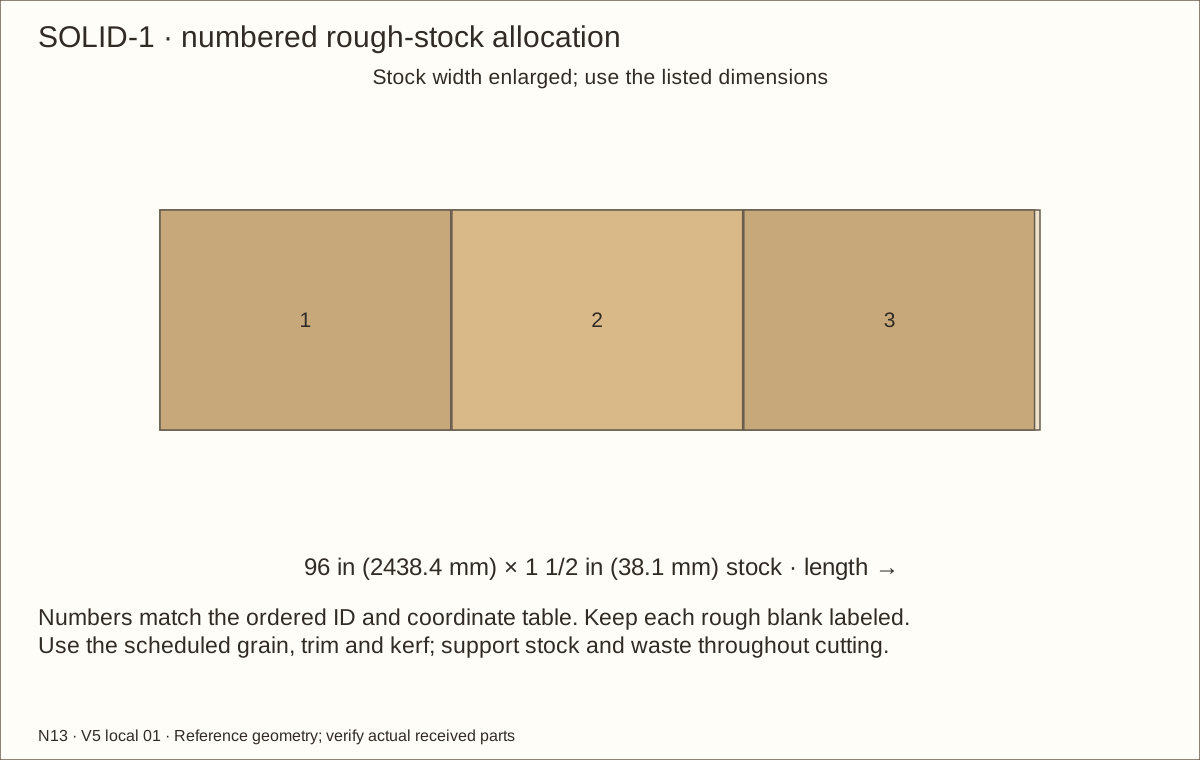
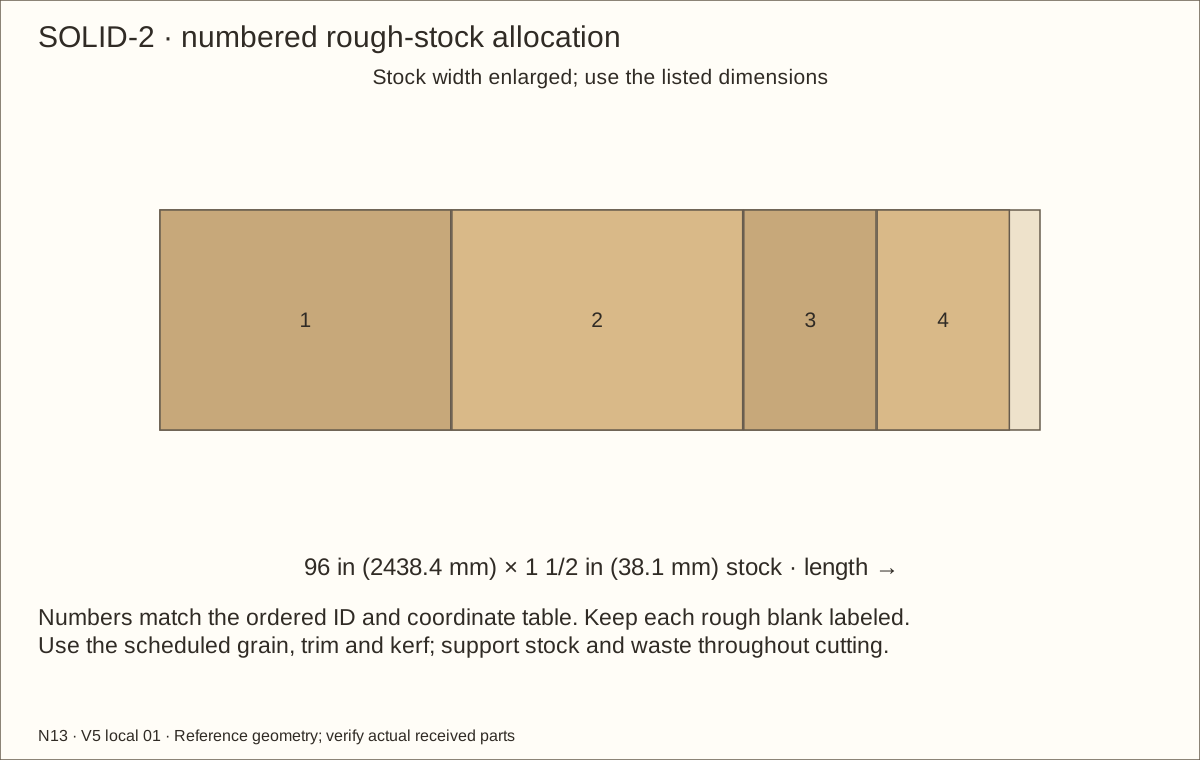
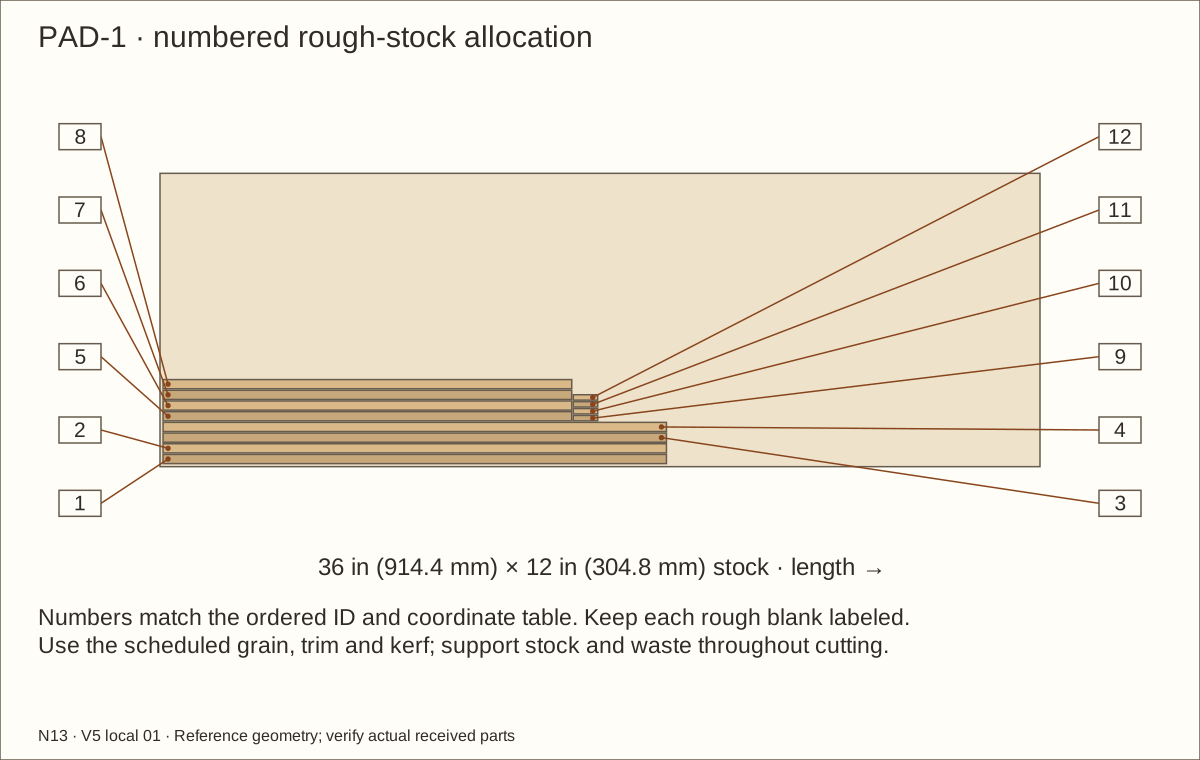
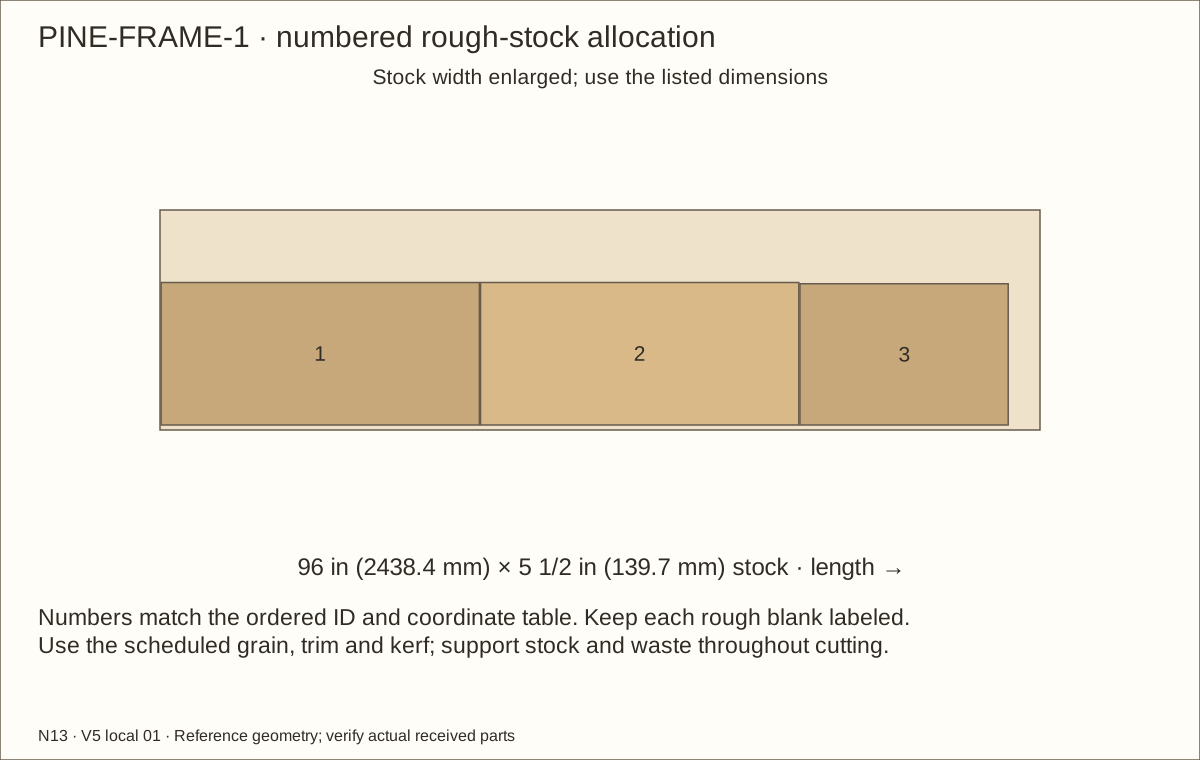
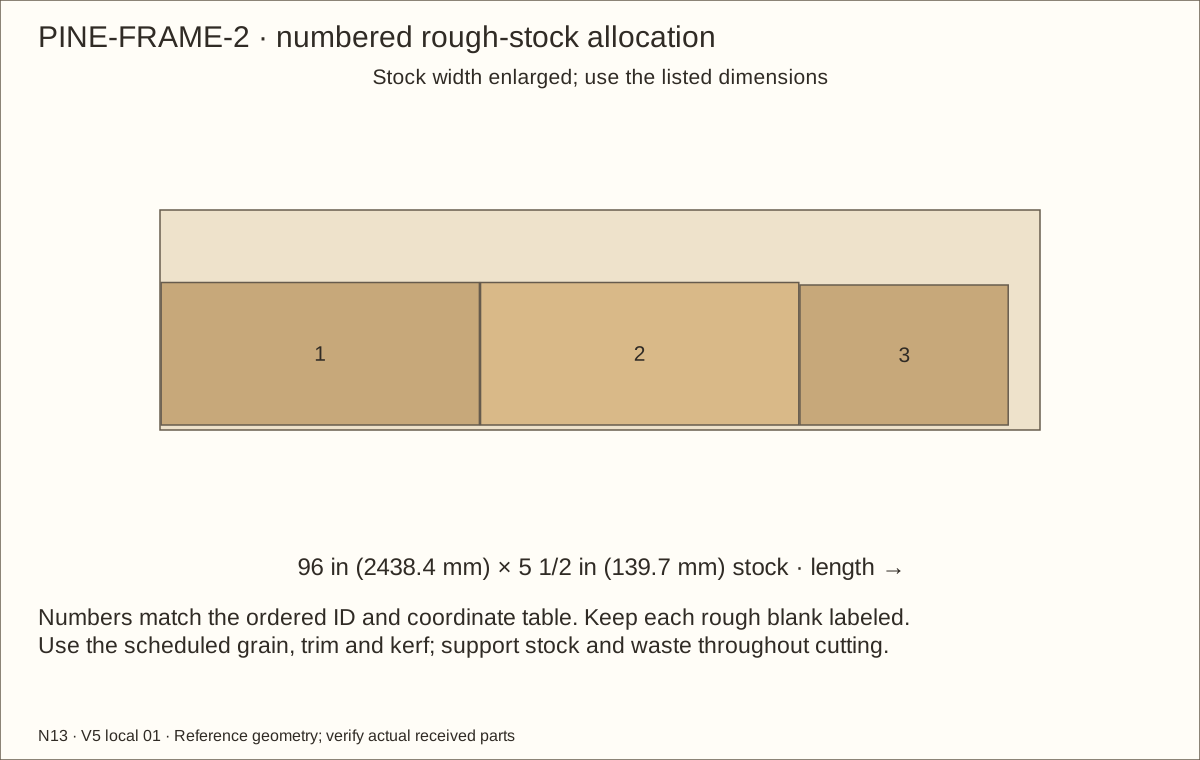
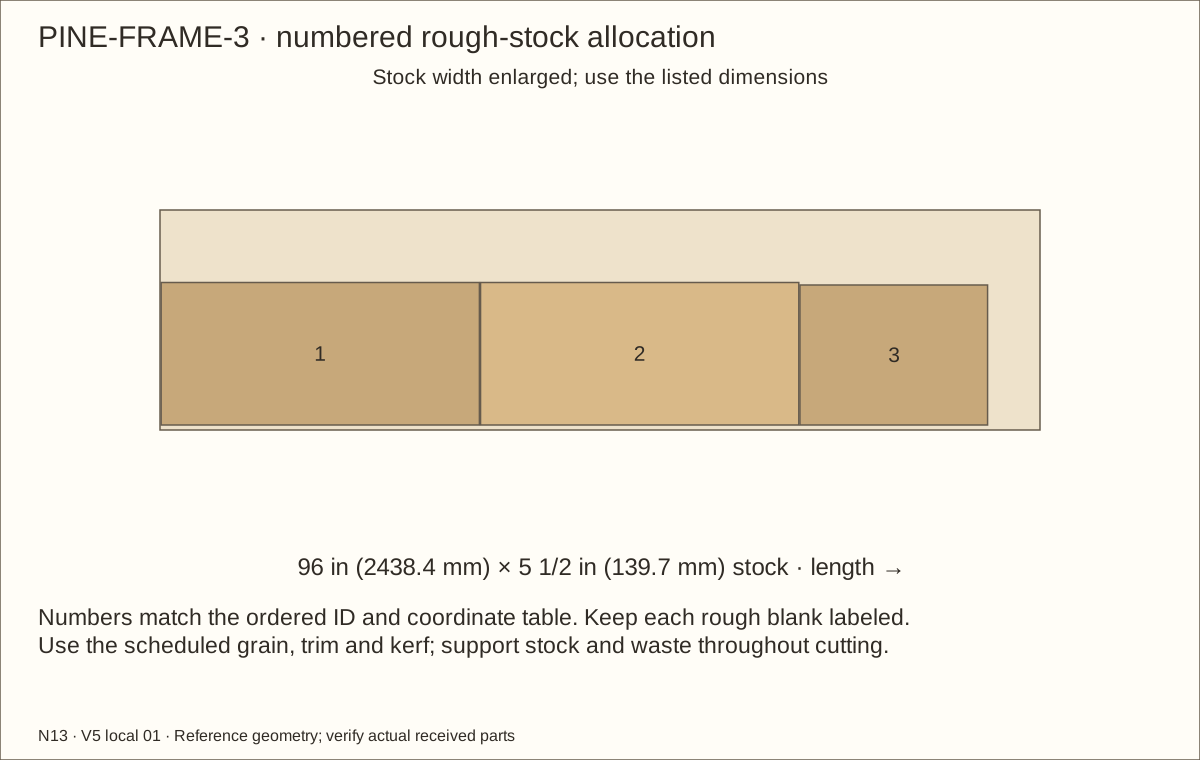
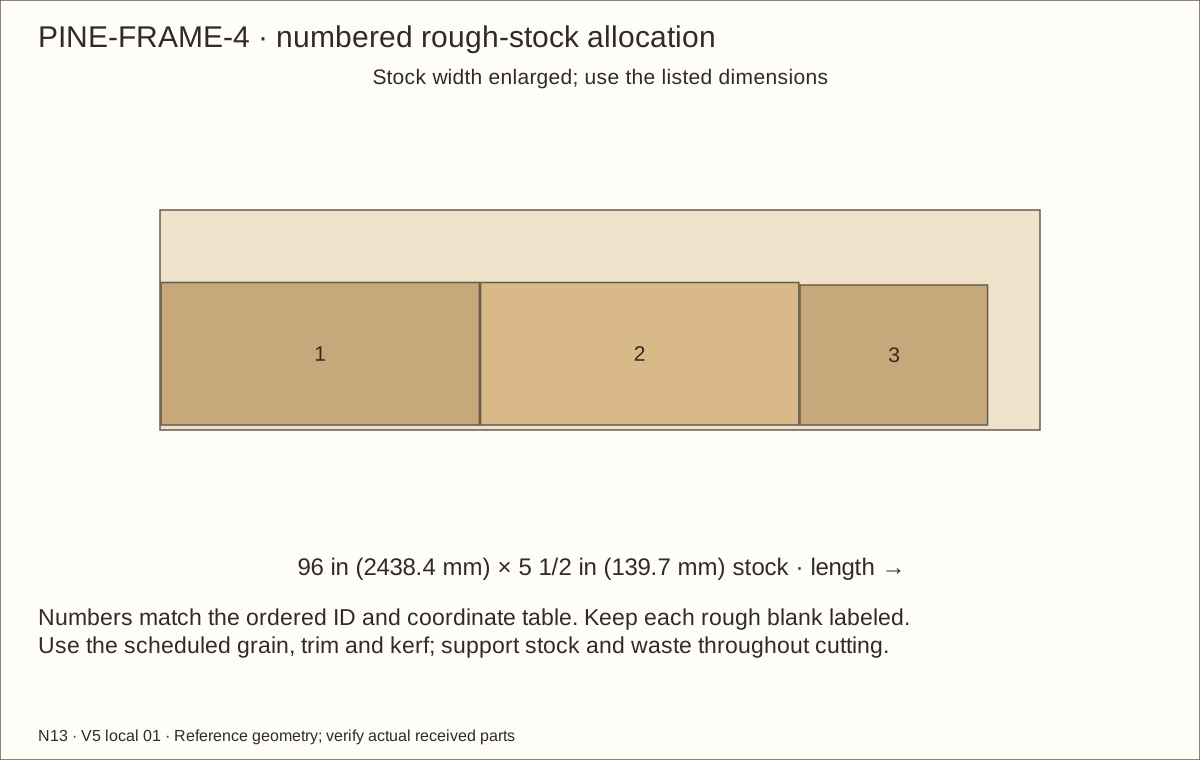
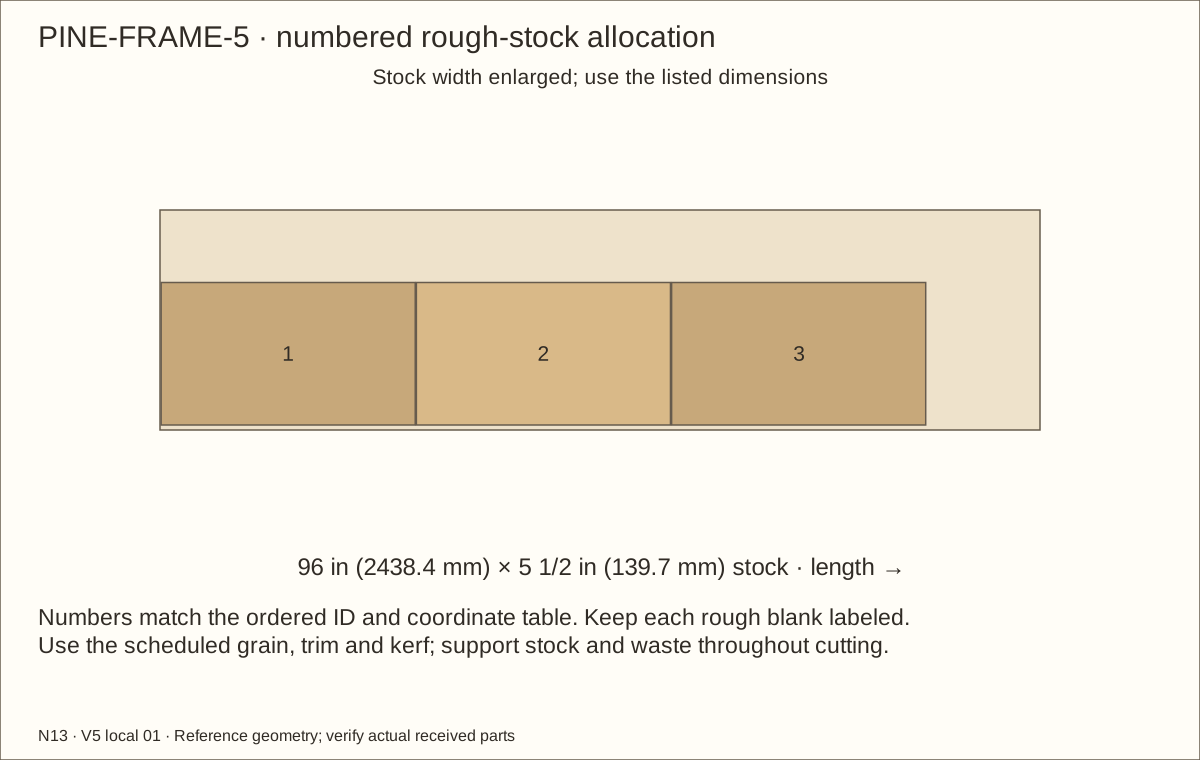
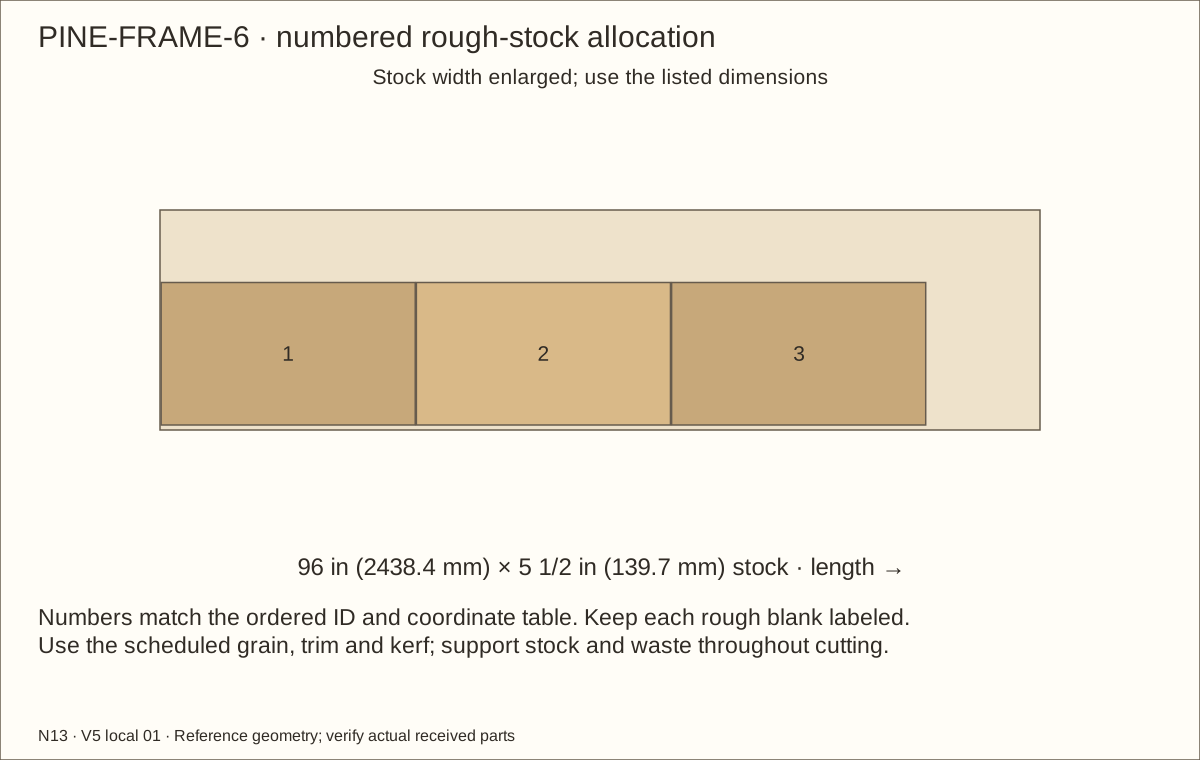
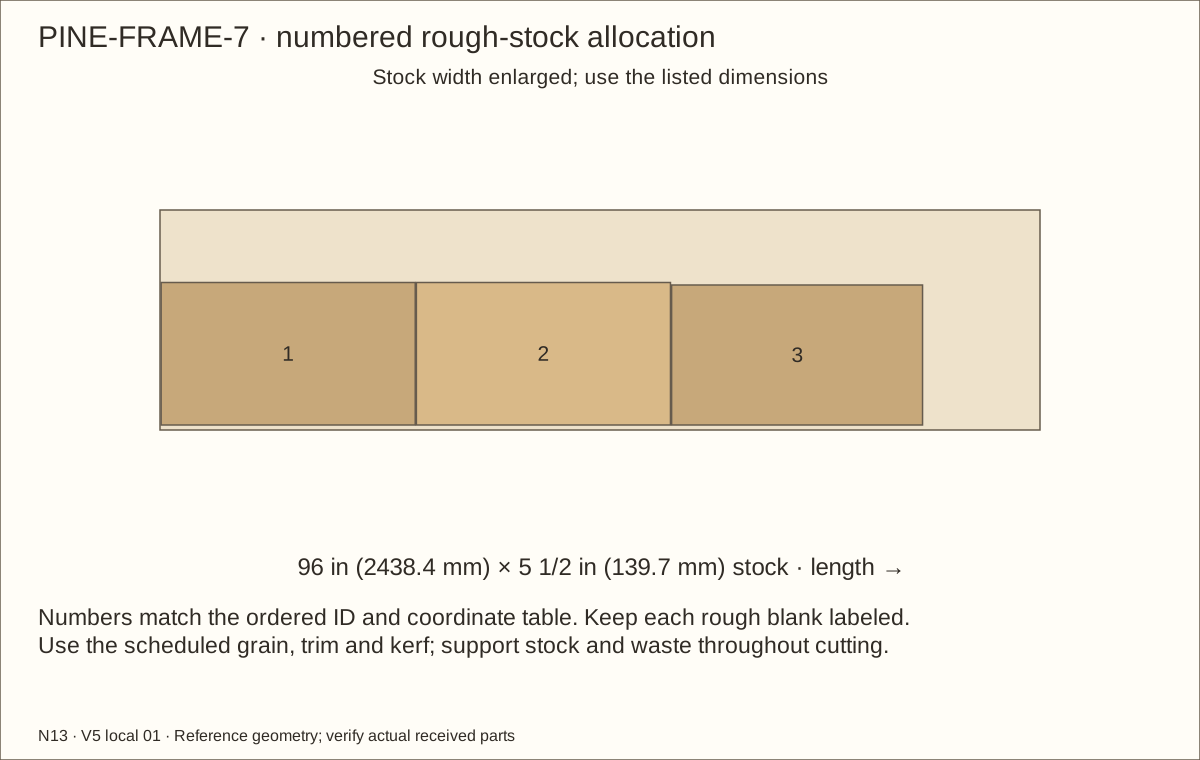
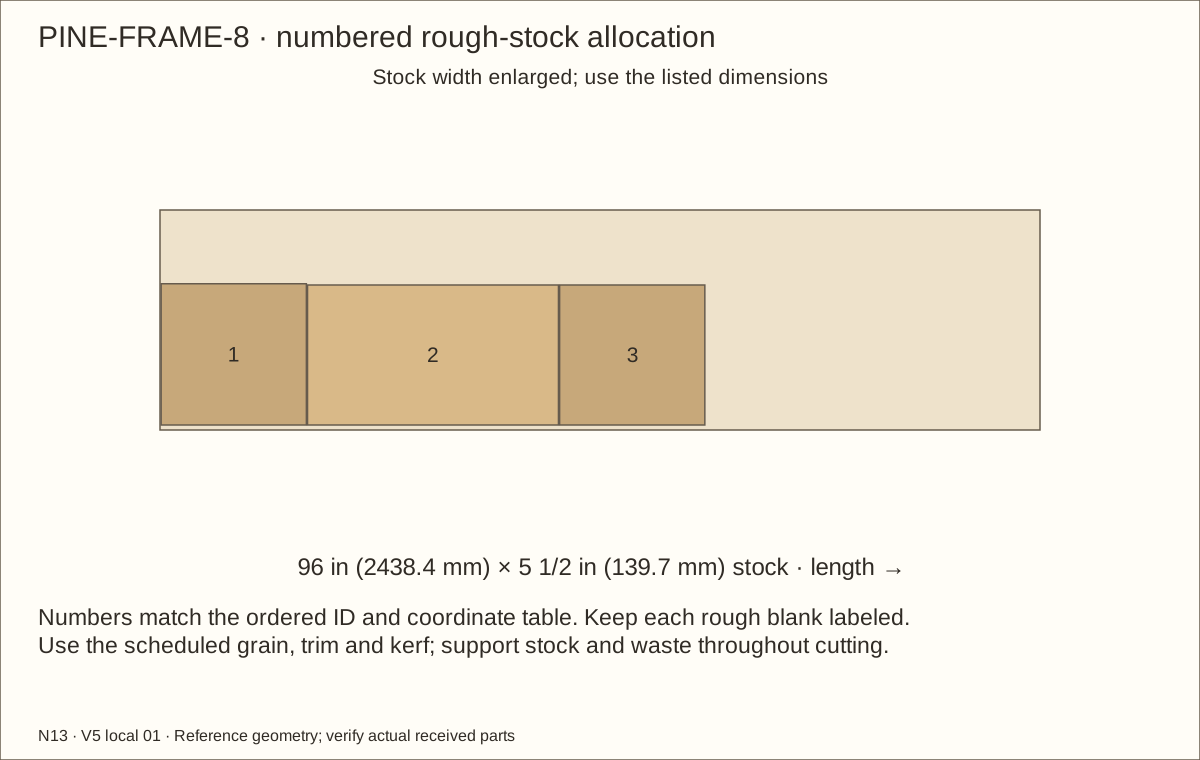
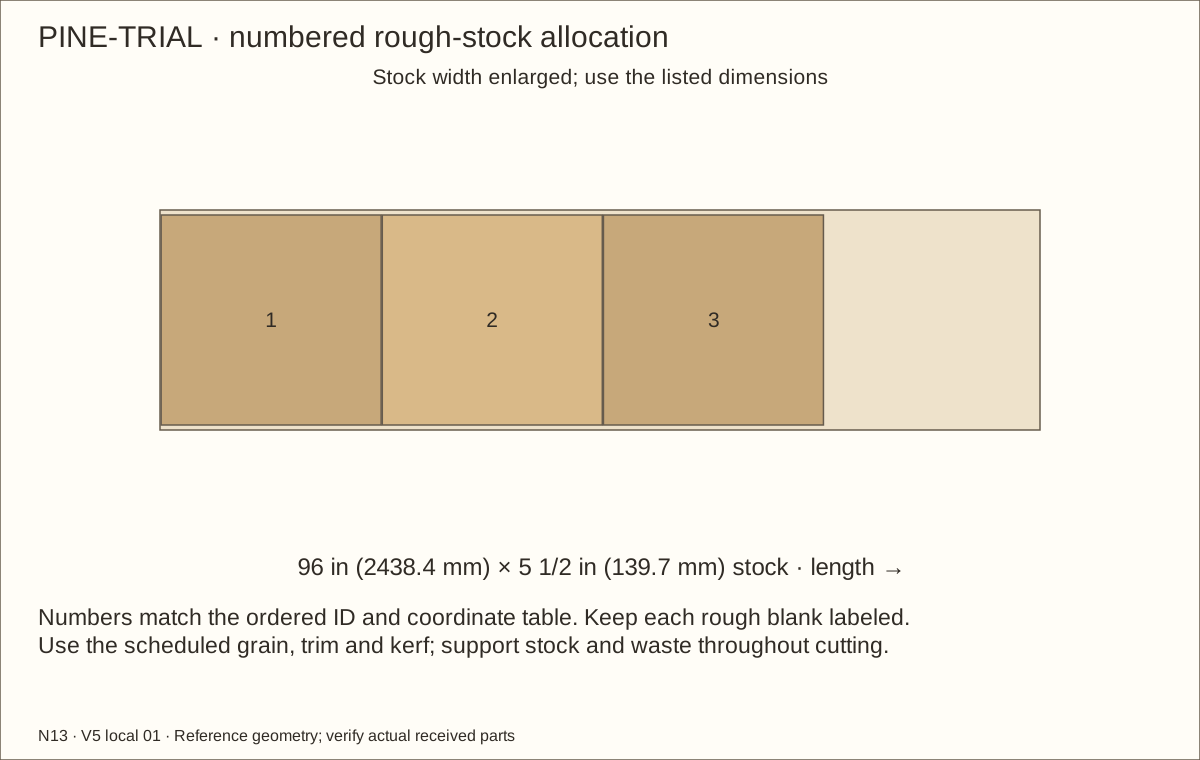
Use the current PINE-FRAME allocations for all sixteen fixed-frame pieces and eight door pieces. Start from straight 3/4 in (19.05 mm) × 5 1/2 in (139.7 mm) × 96 in (2438.4 mm) boards. Rip the assigned broad frame strips with guards, push sticks and supported stops. Keep each layer’s ID; similar lengths are not interchangeable.
From the three purchased full-section solid boards, cut the named parts to length for side, back and roof supports and both retainer receivers. Ease only exposed corners; keep mating faces square.
Check before continuing: Broad frame stock and full-section supports are identified and safely prepared for the narrow cuts.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Plane broad supported stock first; never feed short thin strips alone.
Prepare the frame stock and thin strips — 2
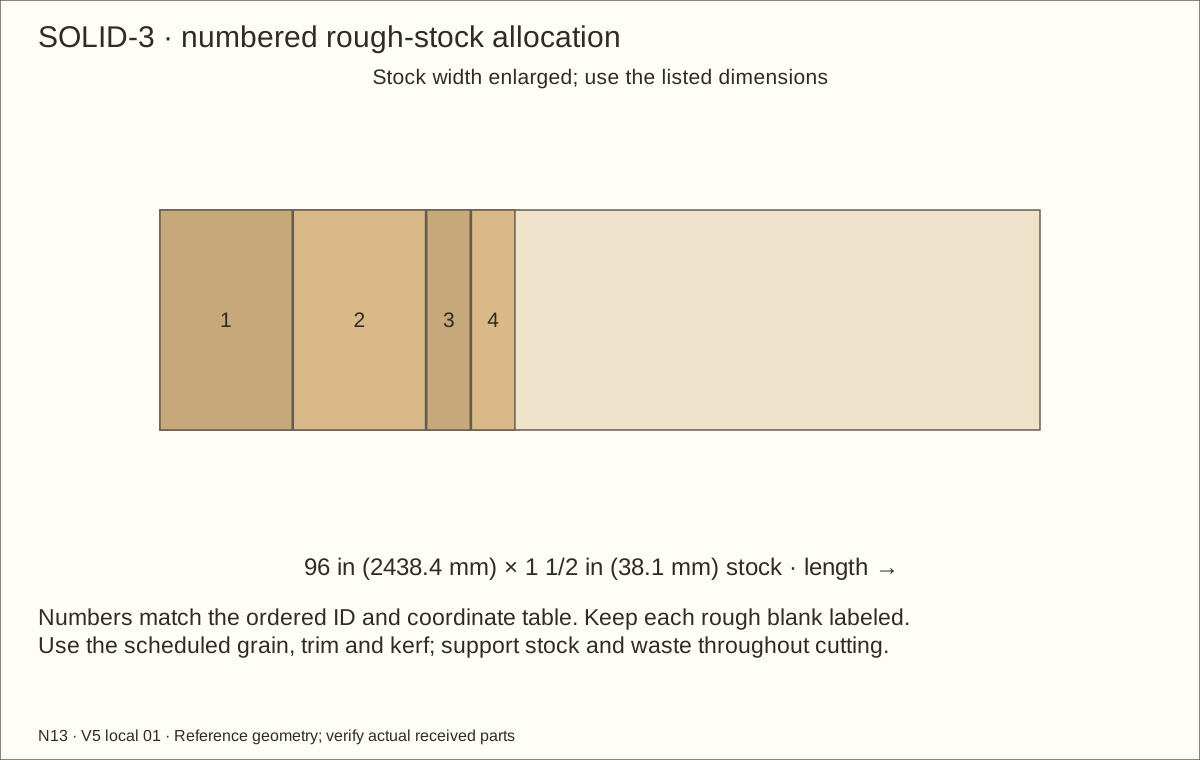
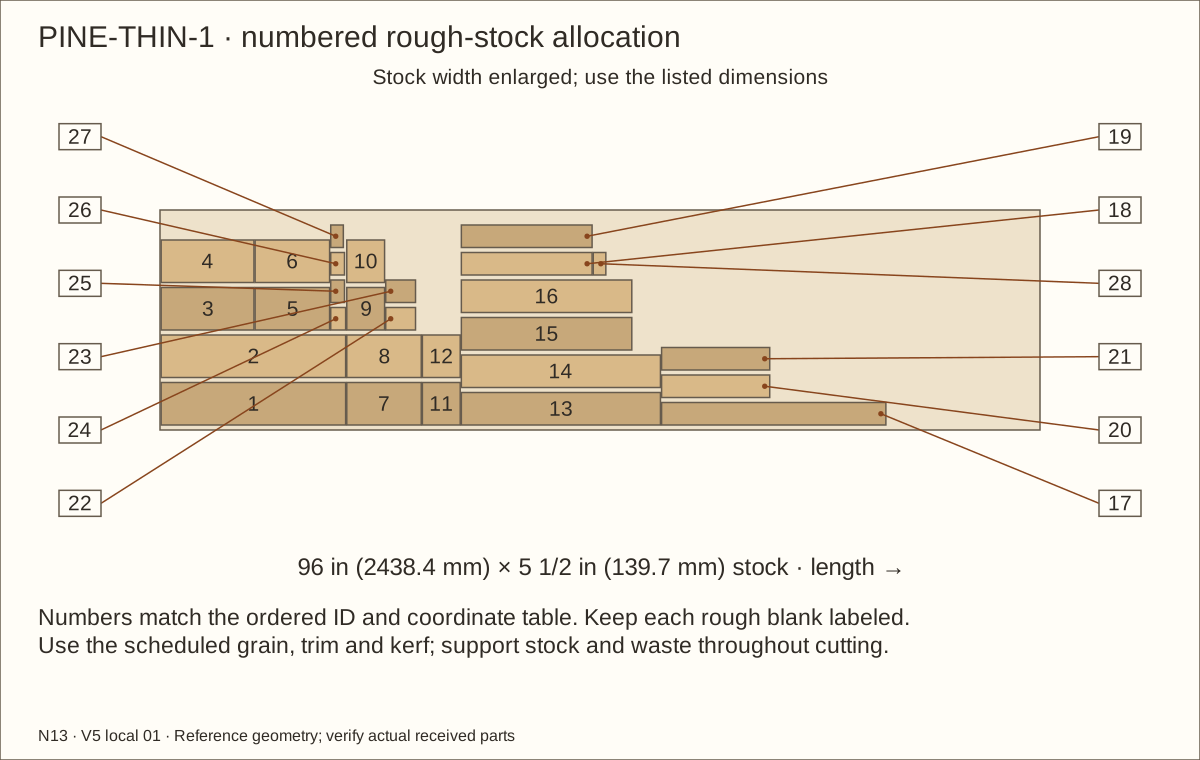
Use the PINE-THIN layouts to plane broad supported stock to 3/8 in (9.53 mm) before ripping the 1 in (25.4 mm) mesh captures and 1/2 in (12.7 mm) liner clamps. A rebate is a shallow pocket cut into a face: each wire capture needs the separate pocket operation below. Never feed a short finished strip into a thickness planer.
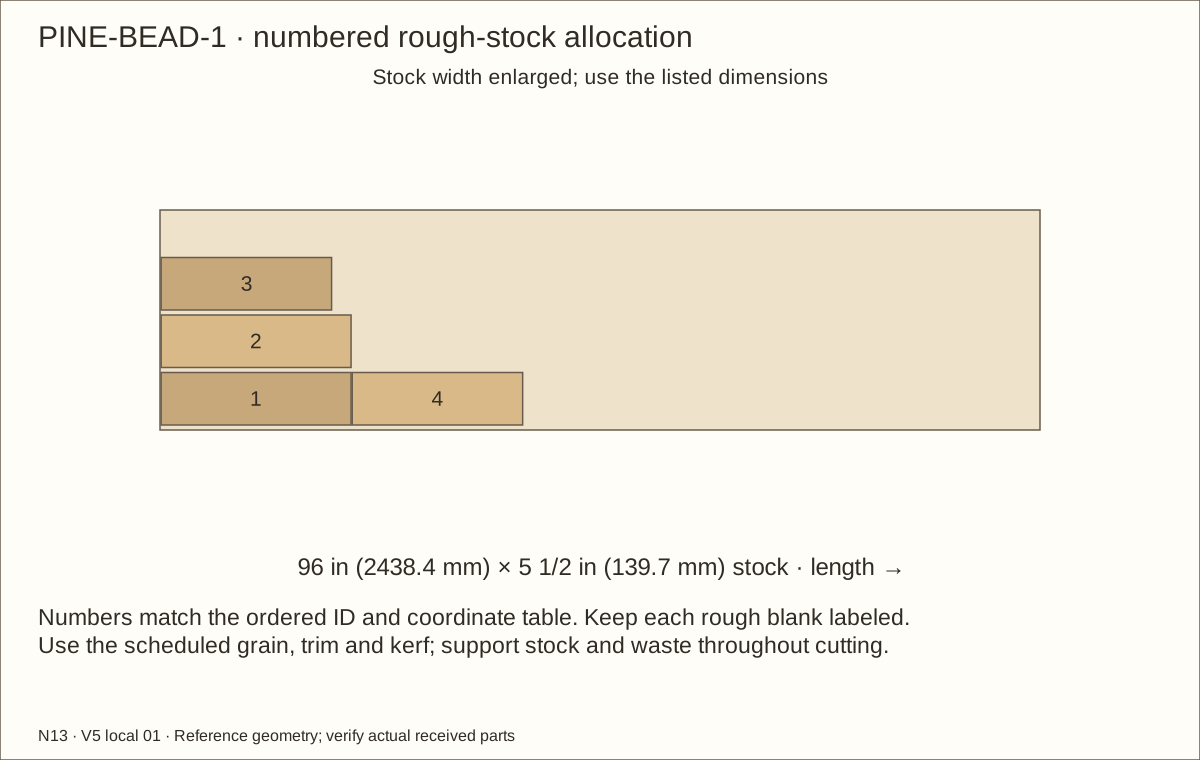
Prepare glazing spacers from 3/8 in (9.53 mm) rough thickness and removable beads from 1/4 in (6.35 mm) thickness before cutting narrow strips. Fit the spacer to the actual acrylic, pads and cured contact films; its reference bare depth is 0.351 in (8.92 mm). Preserve the listed spacer and bead widths. Use a qualified mill if the available guarded machine cannot safely support these cuts.
Check before continuing: Every wooden part matches its ID and allocation; no loose thin piece has been planed unsupported.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Glue is supplementary; every mechanical stitch is required. Keep fresh layers flat and unstressed.
Laminate the continuous front frame — 1
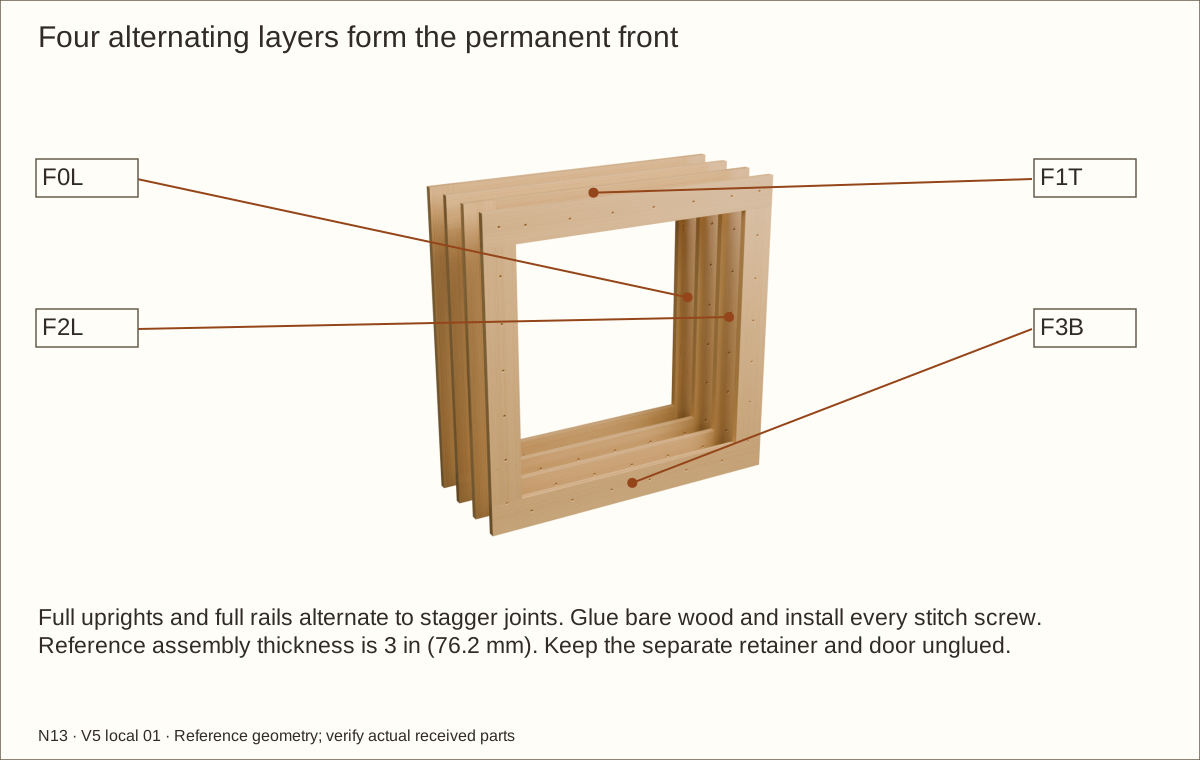
Dry-lay layer 1 with both uprights running full height; fit its split top and bottom rails between them. In layer 2, both rails run full width and the uprights fit between them. Repeat these arrangements for layers 3 and 4.
Dry-fit the fixed frame to 34 19/32 in (878.68 mm) square at the reference plywood gauge. Four 3/4 in (19.05 mm) layers make it 3 in (76.2 mm) deep. There is one 27 19/32 in (700.88 mm)-wide bay between 3 1/2 in (88.9 mm) jambs. Use matched temporary gauge blocks at both ends of the bay and compare the two frame diagonals.
Check before continuing: The four front-frame layers fit square and flat before any glue is applied.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Glue is supplementary; every mechanical stitch is required. Keep fresh layers flat and unstressed.
Laminate the continuous front frame — 2
Fit one layer at a time. Transfer its scheduled rear-entry stitch holes, clearance-drill the new layer and pilot into the preceding one. Spread Titebond III on the mating bare faces, clamp flat with straight clamping pads and fit every #8 × 1 1/4 in (31.75 mm) stitch screw before the next layer covers it. Adjacent layers use offset stations; every seam is bridged. Glue is supplementary, not a claimed structural adhesive. Glue only the layer being fitted: the published open time is 8–10 minutes at 70°F (21°C) and 50% relative humidity. Prepare all clamps and holes first; complete one interface before starting another.
Wipe squeeze-out and keep the frame flat and unstressed for at least 24 hours, longer if the received glue label or conditions require. Do not glue the removable retainer, roof or shell panels to this assembly.
Check before continuing: The full frame is 3 in (76.2 mm) deep, square and flat, with two full-height jambs and bottom kick rail.
Required wait: Glue: at least 24 hours unstressed; follow the received label
Tools / setup: Measuring tape, square, pencil and the tools named below
Laminate the unglazed door frame — 1
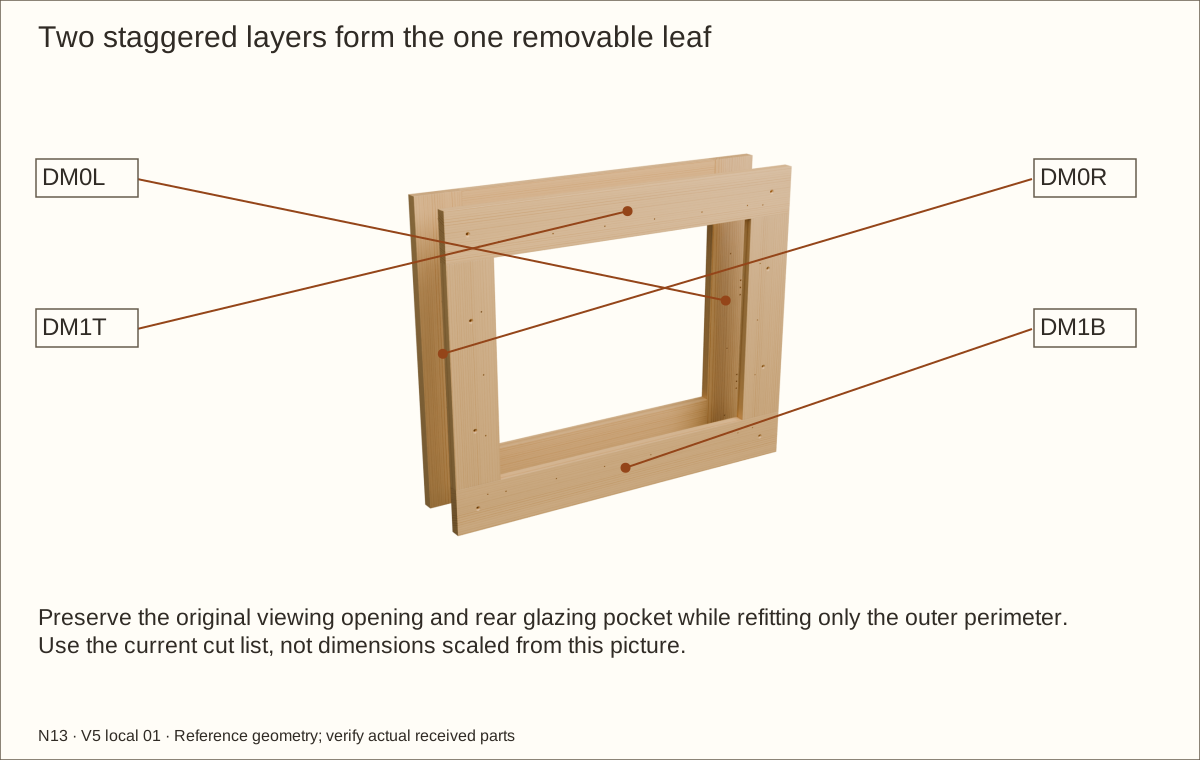
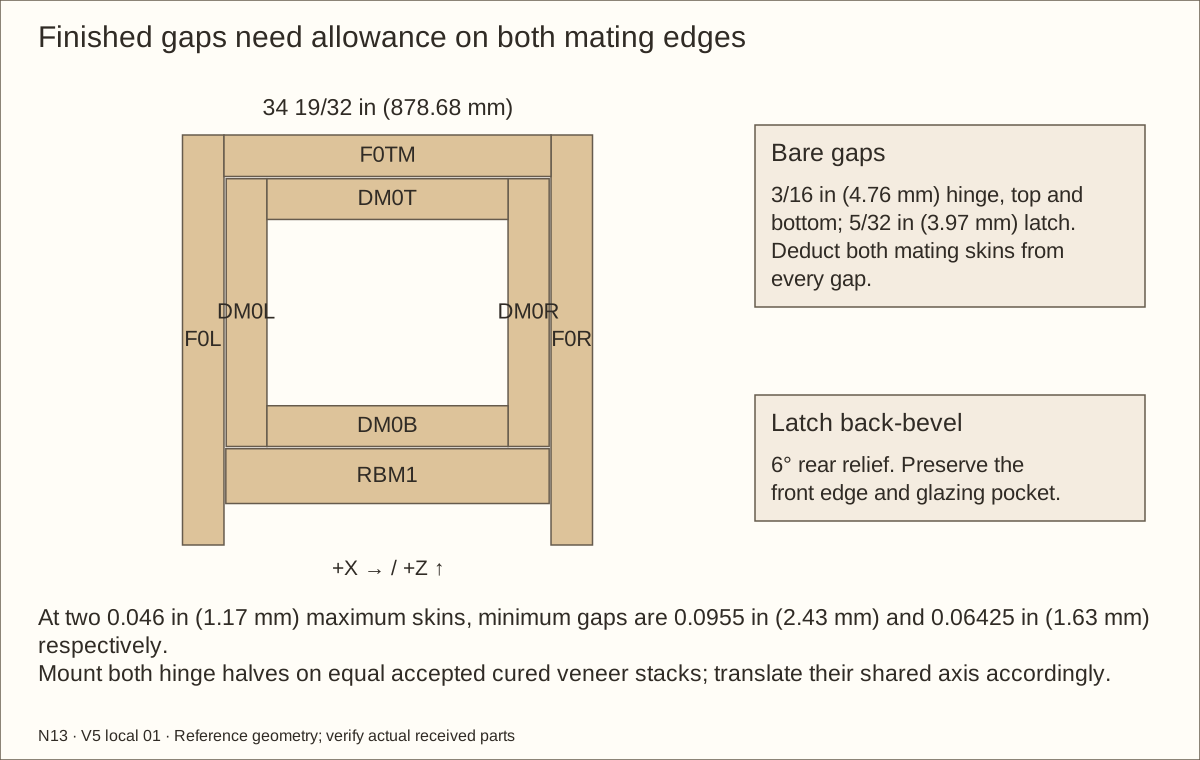
Prepare matching oversized door layers for the dry fit. After lamination and full cure, refit the outer perimeter to 27 1/4 in (692.15 mm) wide × 22 19/32 in (573.88 mm) high. Keep the original 20 11/32 in (516.73 mm) × 15 23/32 in (399.26 mm) viewing opening and every rear glazing datum unchanged. The finished bare gaps are 3/16 in (4.76 mm) at hinge, top and bottom, and 5/32 in (3.97 mm) at the latch edge.
In the front layer, uprights run full height and rails fit between them. In the rear layer, rails run full width and short uprights fit between them. Dry-fit and compare diagonals before applying glue.
Check before continuing: Both door layers fit with staggered joints; the viewing opening and rear glazing pocket remain unchanged.
Tools / setup: Measuring tape, square, pencil and the tools named below
Laminate the unglazed door frame — 2
Clearance-drill the rear layer at its eight scheduled stitch positions and pilot into the front layer. Apply Titebond III, clamp flat and fit all eight #8 × 1 1/4 in (31.75 mm) rear-entry screws per leaf. Keep the sight opening and outer edges square. Do not attach glazing yet.
Leave the leaf flat and unstressed for at least 24 hours. Mark its hinge side (left) without relying on the purchased hinge’s hand name.
Check before continuing: The door is a flat, square, 1 1/2 in (38.1 mm) thick laminated frame, ready for the unglazed fitting trial.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Keep retainer laminations distinct from the fixed frame. Do not glue the service joint.
Laminate the removable retaining panel — 1
Match RBM1–RBM3 for the single panel. Dry-stack all three face to face and check the refitted width against the actual bay. All lower edges bear on the fixed kick rail; keep 5/32 in (3.97 mm) bare side gaps for the veneer while preserving flat receiver contact at the back.
Transfer the rear-entry stitch grid while each stack is clamped. Drill #8 clearance through its rear and middle layers, then stopped pilots into the front layer. Apply Titebond III, clamp with straight clamping pads and install the scheduled #8 × 2 in (50.8 mm) screws from the rear. Their tips retain about 7/64 in (2.78 mm) front cover in the reference stack; recalculate for received thickness.
Check before continuing: The three retainer layers match, and stopped stitch pilots cannot break through their front face.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Keep retainer laminations distinct from the fixed frame. Do not glue the service joint.
Laminate the removable retaining panel — 2
Keep the panel separate from the fixed frame. No glue joins it to the receiver wood supports or bottom rail; its three internal layers are the only glued interfaces.
Clean squeeze-out, label the inside face and leave at least 24 hours unstressed, longer when the received label or conditions require. Do not hide a failed lamination beneath finish or lining. The three-layer panel remains separate from the fixed frame.
Check before continuing: Each three-layer panel remains flat and removable; its total thickness matches three layers of the actual plywood.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Unresolved hardware/material holds stop the dependent operation.
Trial the hardware and glazing — 1
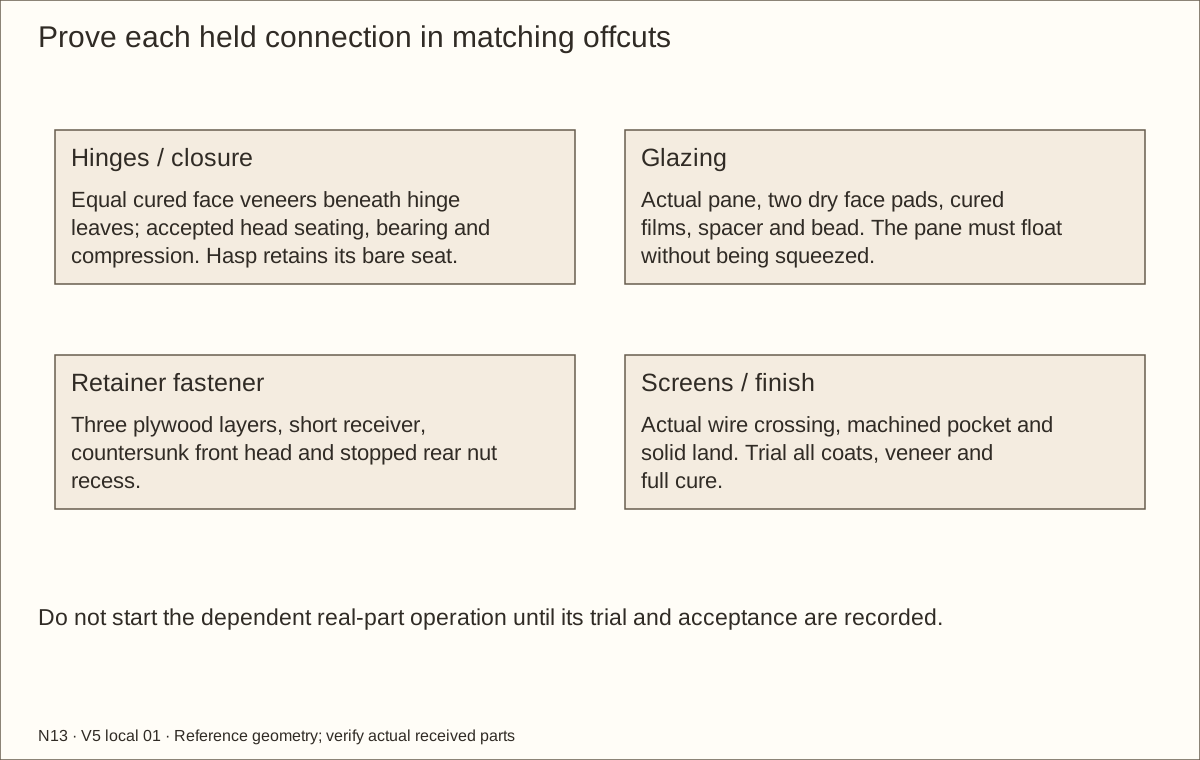
Make a hinge trial from matching offcuts at the intended finished gaps. Apply the accepted cured veneer sample continuously beneath both hinge leaves. Move both halves and the hinge axis forward by that measured face stack, 0.0305 in (0.77 mm) at reference. Obtain acceptance for full bearing, bond and compression before drilling; unequal or compressible layers require redesign. Fit the actual LSX-100R and six #6 × 1 1/4 in (31.75 mm) screws only after their head seating is accepted. Do not countersink the hinge without manufacturer approval. Pilot with a depth stop and check covered tips.
Check the fixed pin half remains below the removable socket and points upward. Prove an outward 100° swing and a 2 in (50.8 mm) lift after opening at least 90°. Measure actual pin engagement and removal travel; the drawing’s about 1 3/4 in (44.45 mm) projection is a reference.
Check before continuing: The real hinge trial proves accepted bearing, head seating, swing and supported lift-off access.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Unresolved hardware/material holds stop the dependent operation.
Trial the hardware and glazing — 2
Make a removable glazing trial with frame, actual acrylic, two dry uncompressed face pads, spacer and rear bead. Include cured films on the opposing wood contacts. Plane the spacer from 3/8 in (9.53 mm) rough stock until the installed bead bears on wood and just contacts the pads without bowing or trapping the pane. Leave the edge movement gap open.
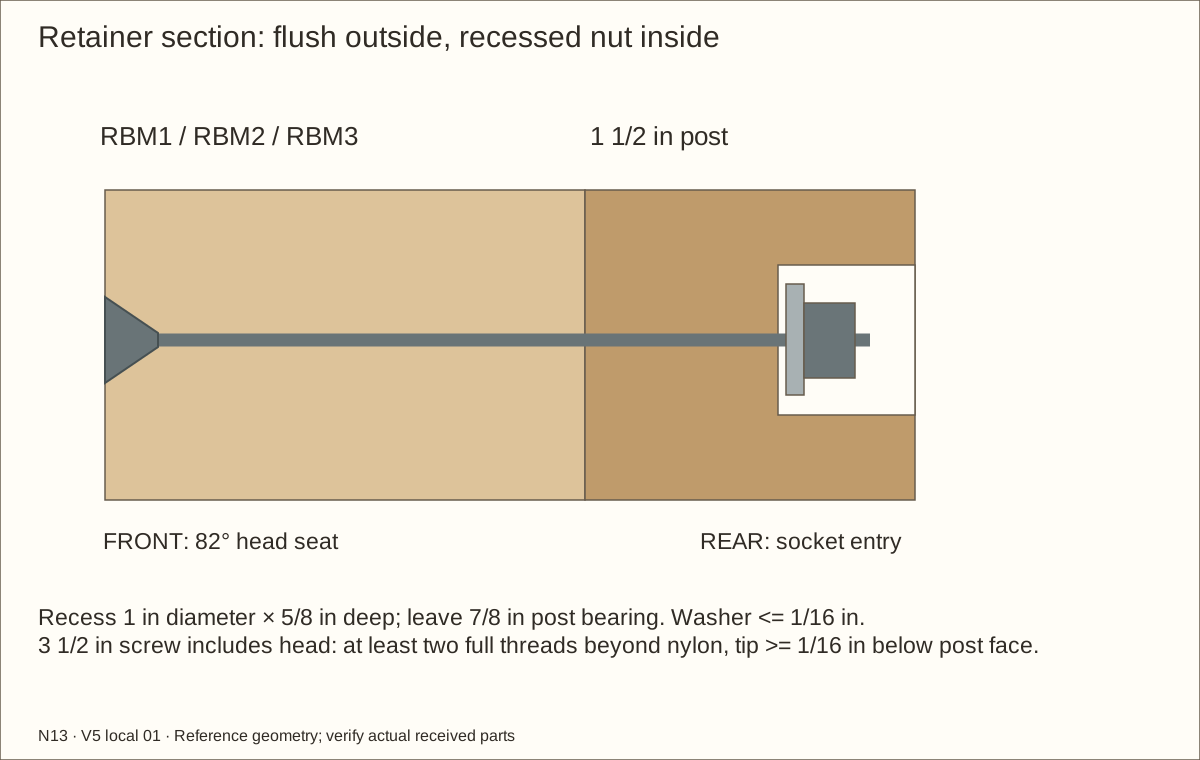
Trial a complete flush retainer connection through three actual plywood offcuts and one 1 1/2 in (38.1 mm) square receiver. Use Bolt Depot 24910 1/4-20 × 3 1/2 in (88.9 mm) socket flat-head screw, 16019 washer and 16008 nylon locknut. The length includes the head. Confirm the received 82° head, 5/32 in (3.97 mm) hex drive, washer no thicker than 1/16 in (1.59 mm) and 0.298 in (7.57 mm)–0.328 in (8.33 mm) nut before drilling real parts.
Check before continuing: All three mockups fit the supplied hardware; no irreversible full-size hole depends on an assumed product profile.
Tools / setup: Measuring tape, square, pencil and the tools named below
Attach the bottom wood supports — 1
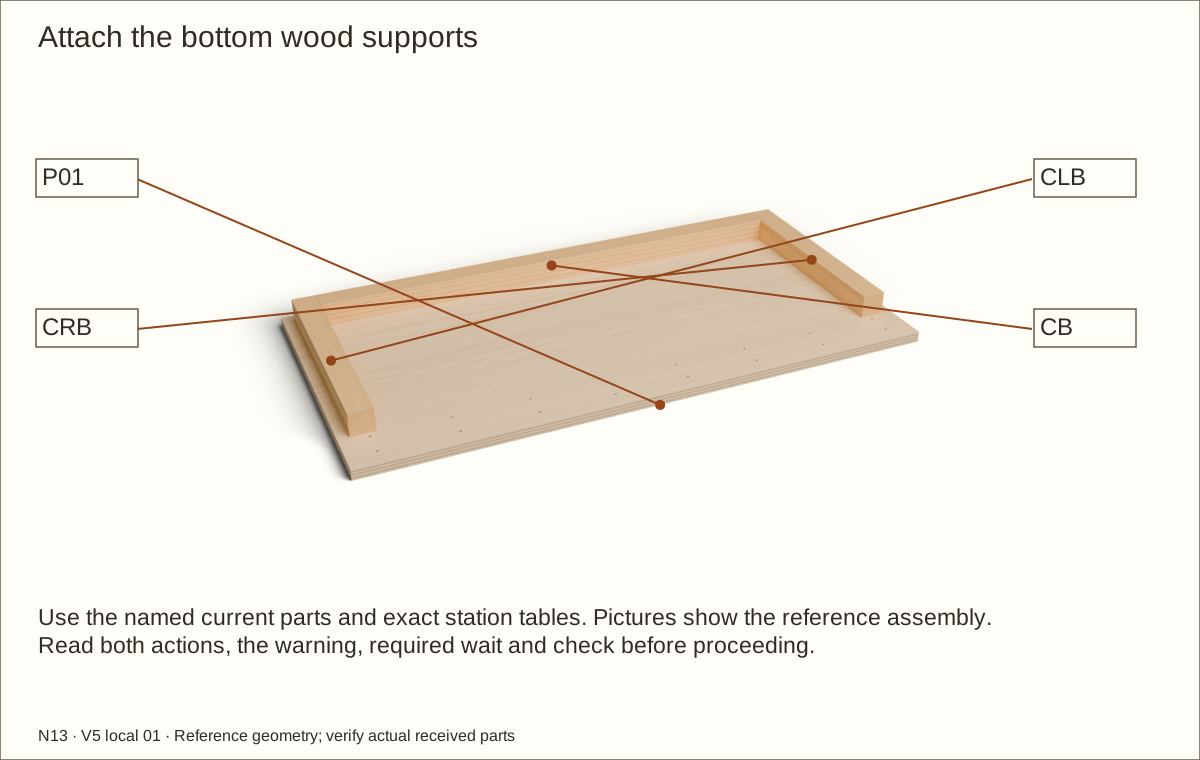
Place P01 flat on a sacrificial board. Locate CLB and CRB one plywood thickness from the side edges, starting 3 in (76.2 mm) behind the front for the laminated frame. Fit CB between them at the rear-panel position.
Transfer the matching named-part stations from the current workshop table. Drill 11/64 in (4.37 mm) clearance through P01 only and stopped 7/64 in (2.78 mm) pilot holes into the solid pine, adjusting the pilot after an offcut trial.
Check before continuing: Floor supports are clamped on the correct side of P01 and all clearance and stopped pilot holes align.
Tools / setup: Measuring tape, square, pencil and the tools named below
Attach the bottom wood supports — 2
Apply Titebond III to these three floor-wood support interfaces, clamp and drive #8 × 1 1/4 in (31.75 mm) screws from below. Seat heads flush with the underside so no head interrupts continuous support.
Check the front-frame and back-panel recesses, wipe squeeze-out and leave the assembly flat and unstressed through the glue cure.
Check before continuing: The floor sits entirely flat, with square wood supports and an unobstructed 3 in (76.2 mm) front-frame recess.
Required wait: At least 24 hours unstressed for glued wood supports
Tools / setup: Measuring tape, square, pencil and the tools named below
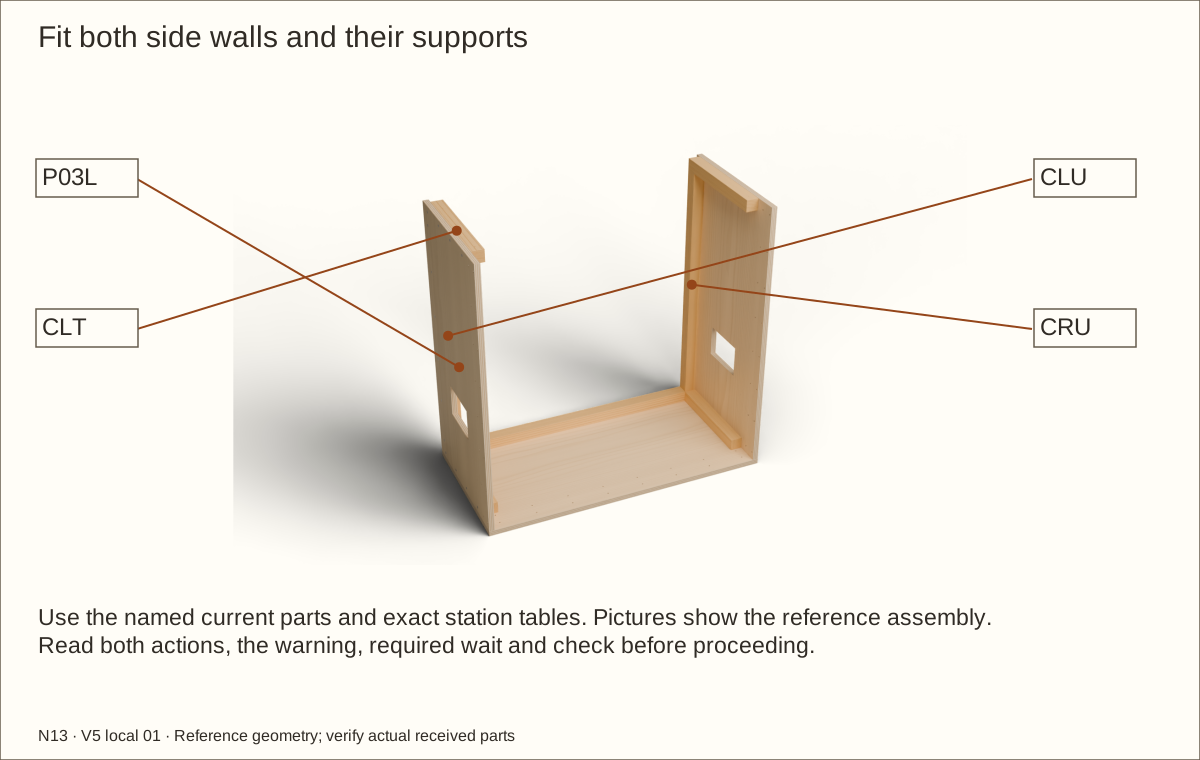
Fit both side walls and their supports — 1
Clamp each rear upright between its lower and upper wood supports. Upper wood supports start 3 in (76.2 mm) behind the front and stop at the inner face of the back panel.
With a helper, stand each wall on the floor, flush at the outer side and its front edge. Clamp the wall to its bottom wood support; do not leave it standing unsupported.
Check before continuing: Both walls sit square and flush on the supported floor with a helper controlling them.
Tools / setup: Measuring tape, square, pencil and the tools named below
Fit both side walls and their supports — 2
At the listed stations, clearance-drill through the plywood and pilot into the named pine receiver. Offset the future back screws from the side screws using the schedule; do not intersect their shafts.
Install #8 × 1 1/4 in (31.75 mm) screws and finish tightening by hand. Keep the wall joints dry during the trial so they can be disassembled for finish.
Check before continuing: Both walls are parallel and stable; all tips retain at least 1/16 in (1.59 mm) wood cover.
Tools / setup: Measuring tape, square, pencil and the tools named below
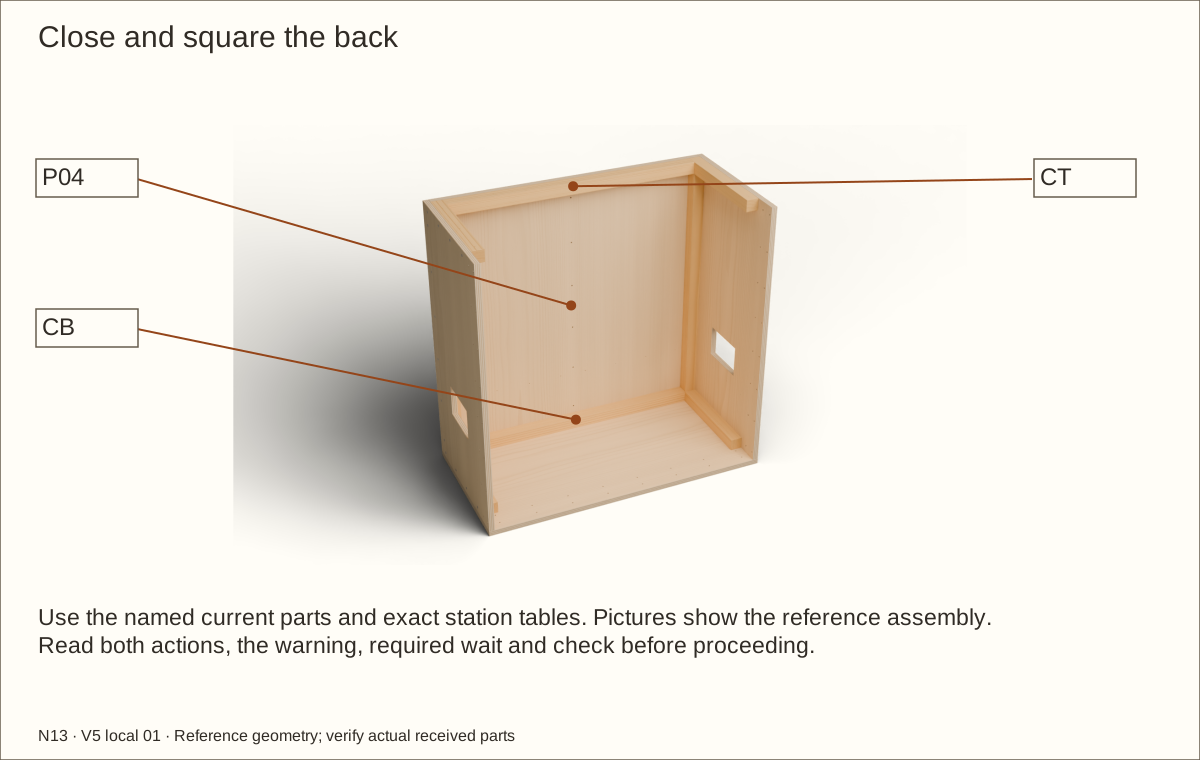
Close and square the back — 1
Fit P04 between the sides, resting on the floor and flush with their rear edges. Clamp it against CB, CT and both rear uprights.
Compare front and rear diagonals; make each pair equal within 1/16 in (1.59 mm). Correct an uneven support rather than forcing a twisted shell into position with screws.
Check before continuing: The back is seated and both diagonal pairs agree before final screw tightening.
Tools / setup: Measuring tape, square, pencil and the tools named below
Close and square the back — 2
Transfer the listed stations through the back and into the receivers. Clearance-drill the plywood and use stopped pine pilots; the offset side/back stations keep screw shafts apart.
Fit #8 × 1 1/4 in (31.75 mm) screws, then remove clamp pressure and recheck the diagonals and continuous floor bearing.
Check before continuing: The square shell stands without relying on clamps; no back screw meets a side screw.
Tools / setup: Measuring tape, square, pencil and the tools named below
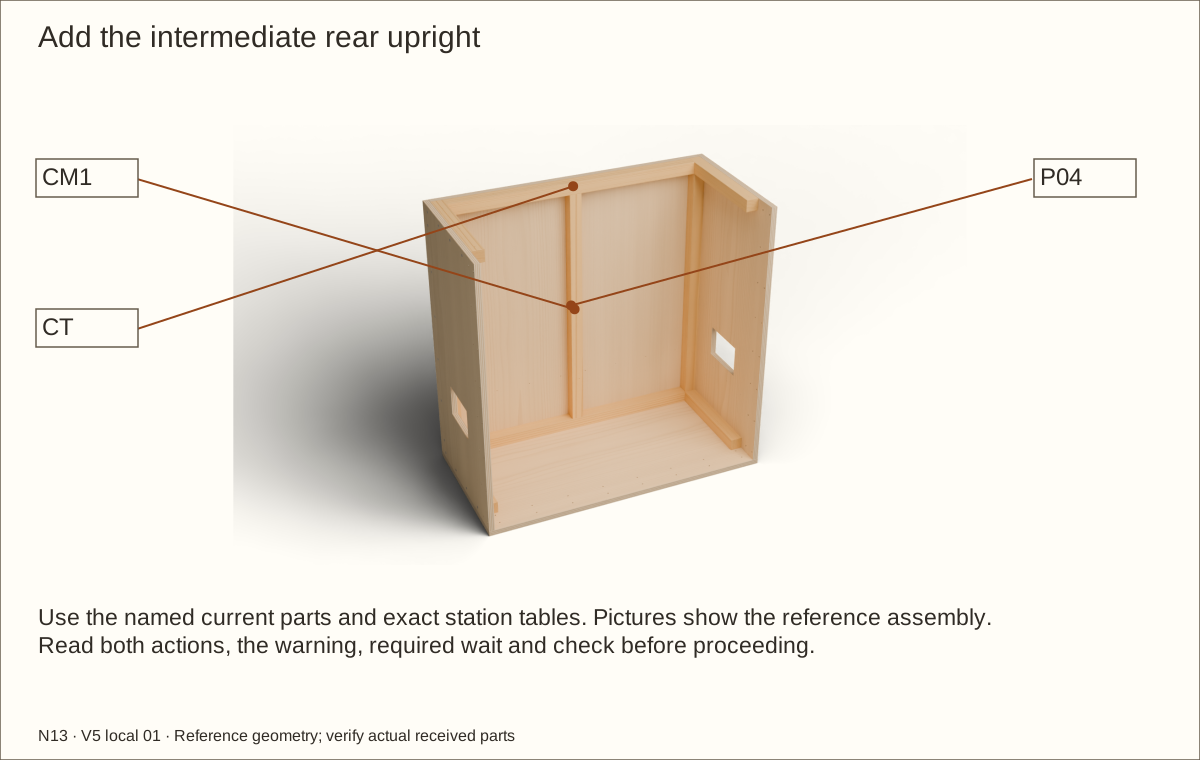
Add the intermediate rear upright — 1
Place CM1 inside the back with its centre 18 in (457.2 mm) from the left outside face. Its ends fit between the lower and upper rear wood supports.
Clamp each member straight against P04. Transfer the matching named-part stations from the current workshop table from the outside, keeping the listed offsets from the corner and horizontal wood support screws.
Check before continuing: The intermediate rear upright is straight and its actual screw stations align with supported wood.
Tools / setup: Measuring tape, square, pencil and the tools named below
Add the intermediate rear upright — 2
Drill clearance through P04 and stopped pilots into the uprights. Fasten with #8 × 1 1/4 in (31.75 mm) screws; keep the wood beneath the future membrane free from points, splinters and proud heads.
Check each upright bears at both ends and the back remains flat. These members brace the panel; they do not turn the floor into an unsupported span.
Check before continuing: Three rear uprights are in place, with continuous full-floor support still required.
Tools / setup: Measuring tape, square, pencil and the tools named below
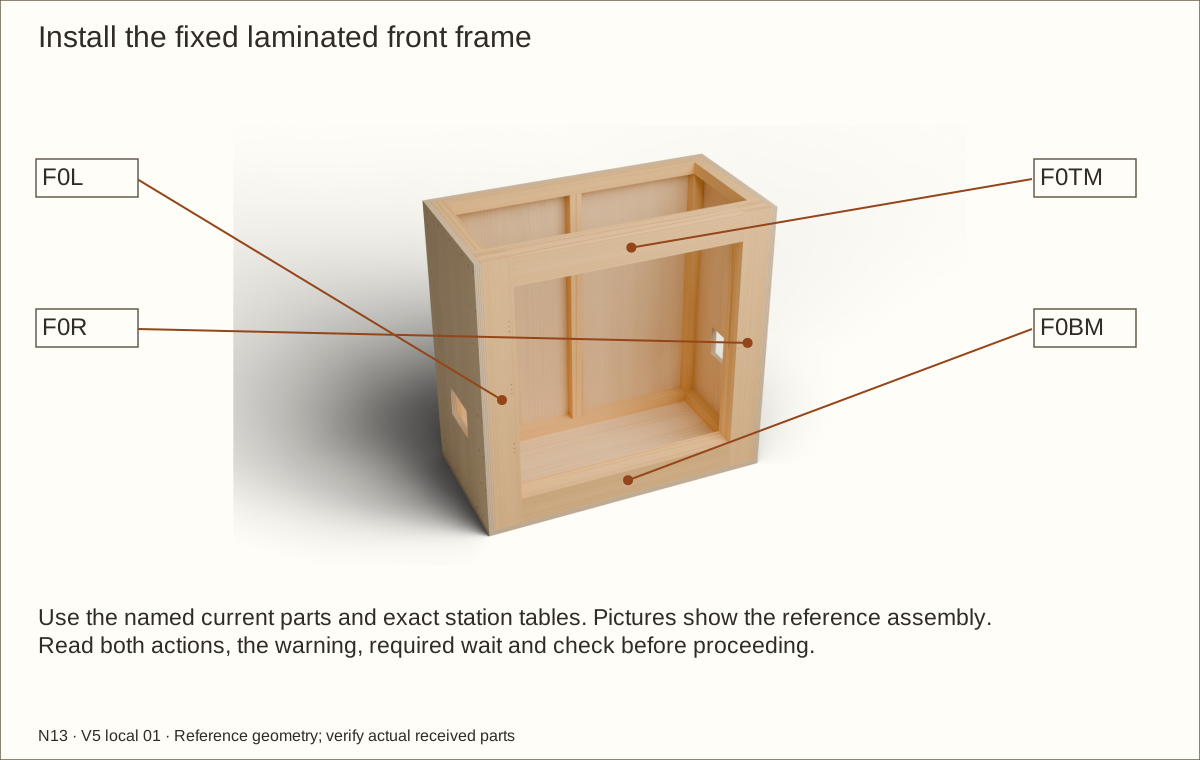
Install the fixed laminated front frame — 1
With a helper, place the cured four-layer frame in its 3 in (76.2 mm) front recess, resting on P01. Keep its outer front face flush with the side-panel fronts; check both jambs are plumb.
Clamp the frame and check the bay width, both diagonals and the top bearing surface. The sides overlap the jamb ends; there is no glue bond between the frame and shell during this trial.
Check before continuing: The permanent front is seated, clamped square and checked at both diagonals before fastening.
Tools / setup: Measuring tape, square, pencil and the tools named below
Install the fixed laminated front frame — 2
Transfer the side stations through P03L/P03R into the full jambs. Use #8 × 2 in (50.8 mm) screws, with clearance through plywood and stopped pilots into pine. Use the scheduled alternating depth lines.
While the empty assembly is safely supported, drill the floor stations from below and fasten into the bottom rail with #8 × 2 in (50.8 mm) screws. Their depth lines differ from the side screws. Return the shell to continuous support and leave the fixed frame installed for the remaining trial.
Check before continuing: The entire front frame is supported, square and attached; the jambs and kick rail are permanent.
Tools / setup: Measuring tape, square, pencil and the tools named below
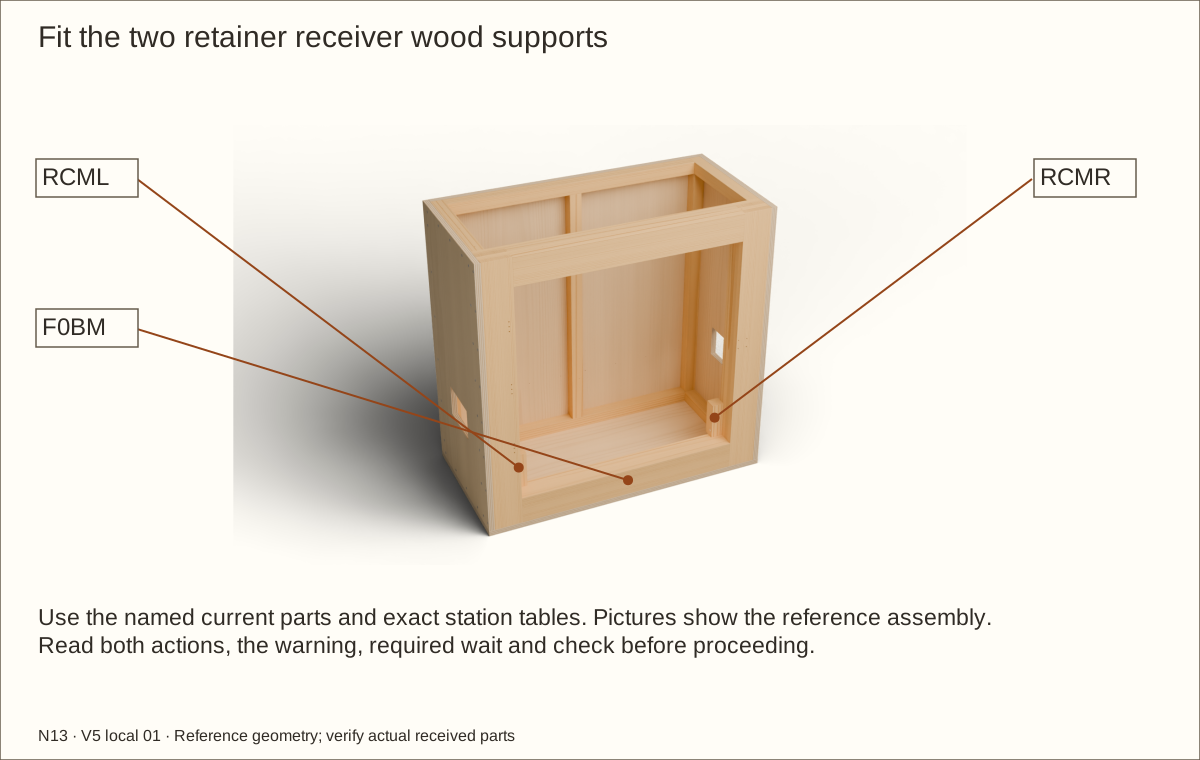
Fit the retainer receivers — 1
Fit RCML and RCMR behind the single panel bay, resting on the fixed bottom rail with their sides against the laminated jambs. Their fronts begin 2 7/64 in (53.58 mm) behind the front face, directly behind the three plywood layers. Keep both contact faces free of veneer.
Transfer both sideways screw stations per receiver. Drill #8 clearance through the receiver only, then a stopped 7/64 in (2.78 mm) trial pilot into the adjoining laminated upright.
Check before continuing: Both receivers are supported on the kick rail and their stopped sideways pilots are safe.
Tools / setup: Measuring tape, square, pencil and the tools named below
Fit the retainer receivers — 2
Drive the four #8 × 3 in (76.2 mm) screws sideways into the frame. Each passes through 1 1/2 in (38.1 mm) of receiver and engages about 1 1/2 in (38.1 mm) of frame; do not substitute the shorter shell screws.
Keep these screw heights distinct from the one future bolt height. Check the receivers are straight, immobile and free of sharp edges before placing any panel.
Check before continuing: Each receiver is fixed with two scheduled screws, and every bolt route remains clear.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Never remove either connection when the bed or any water remains. Keep recess depth and washer bearing as specified.
Fasten the removable retainer — 1
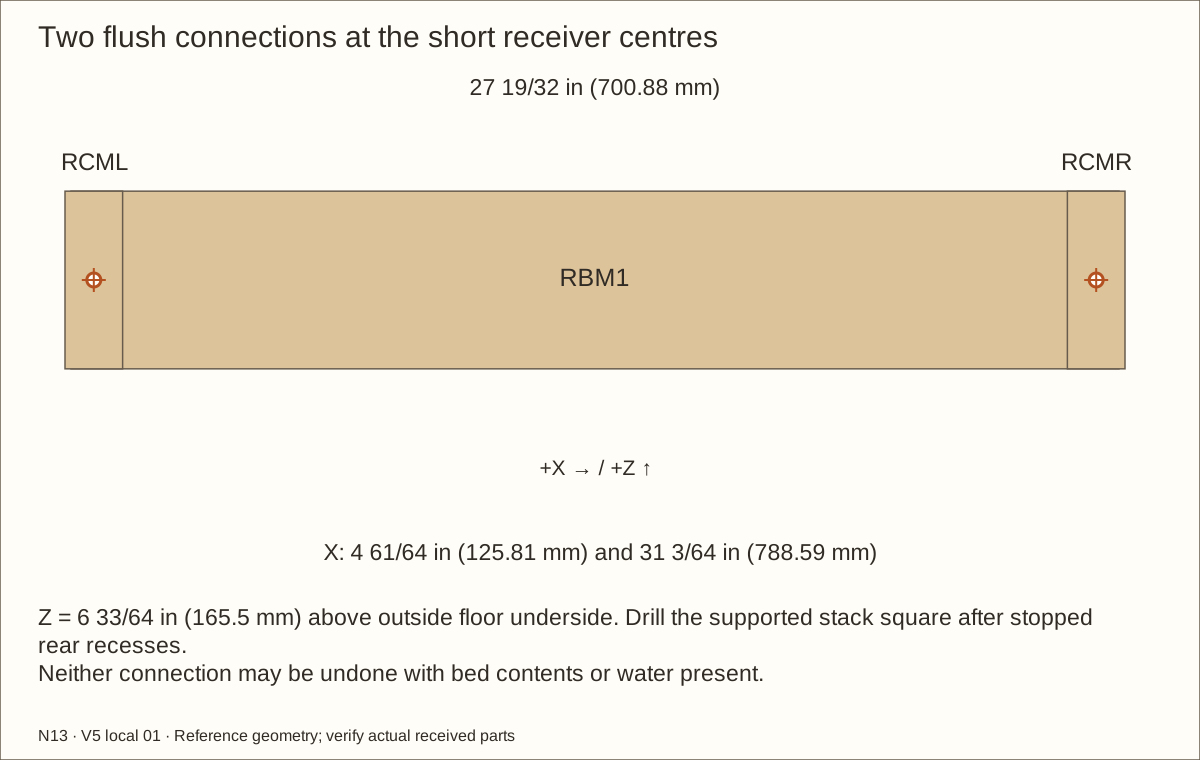
Dry-set the cured retainer on the kick rail with its front flush and top 8 in (203.2 mm) above the finished-floor mark. Keep 5/32 in (3.97 mm) bare side gaps and clamp the panel firmly against both receivers. Mark the two connection centres from the front-left floor datum: X = 4 61/64 in (125.81 mm) and 31 3/64 in (788.59 mm); Z = 6 33/64 in (165.5 mm). Both are 5 11/16 in (144.46 mm) above the reference finished floor.
On each receiver’s rear face, make the 1 in (25.4 mm)-diameter flat-bottom socket recess first, 5/8 in (15.88 mm) deep, with the loose member clamped square under a stopped bit. Leave 7/8 in (22.23 mm) of receiver thickness at the washer seat. Reassemble and clamp the stack, then drill a backed 9/32 in (7.14 mm) through bore at the matching centre. Never hold a loose short piece by hand under the bit.
Check before continuing: The matched recesses and through bores are square; both receivers retain the scheduled bearing wood.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Never remove either connection when the bed or any water remains. Keep recess depth and washer bearing as specified.
Fasten the removable retainer — 2
Countersink only the front plywood for the actual 82° flat head. The head finishes flush with bare wood, beneath the veneer face; preserve a 0.55 in (13.97 mm) circular service opening in the veneer. Insert each 3 1/2 in (88.9 mm) machine screw from the front, then fit its washer and nylon locknut inside the rear recess. Use the 5/32 in (3.97 mm) hex drive and actual 7/16 in (11.11 mm) socket; socket outside diameter must not exceed 7/8 in (22.23 mm) for this reference recess.
Support the panel and hand-tighten evenly without crushing wood or forcing stainless threads that begin to seize. Require two complete threads beyond the nylon ring and at least 1/16 in (1.59 mm) between the screw tip and receiver rear face. Trial access before lining. Do not deepen a recess, omit a washer or cut an incorrect screw to make the stack fit. Both complete connections remain installed whenever contents or liquid are present.
Check before continuing: Both flush heads are accessible; complete recessed nut stacks have two exposed threads and covered rear tips.
Tools / setup: Measuring tape, square, pencil and the tools named below
Fit the unglazed door to its bay — 1
After the fixed frame and retainer are secure, fit the cured door at 3/16 in (4.76 mm) bare hinge/top/bottom gaps and 5/32 in (3.97 mm) bare latch gap. Keep its front face flush. Reference 0.0305 in (0.77 mm) layers on both mating edges leave about 0.1265 in (3.21 mm) and 0.09525 in (2.42 mm) gaps; maximum 0.046 in (1.17 mm) layers leave 0.0955 in (2.43 mm) and 0.06425 in (1.63 mm). Recalculate actual measured layers.
Compare door and bay diagonals before trimming. Use a supported jig to back-bevel only the latch edge 6° away from the fixed jamb, keeping the front edge at its scheduled position. A back-bevel means the rear edge is slightly narrower than the front, providing swing clearance. Preserve the full glazing pocket and all receiving wood.
Check before continuing: The reference and actual finished gaps are recorded; the viewing opening and rear pocket remain unchanged.
Tools / setup: Measuring tape, square, pencil and the tools named below
Fit the unglazed door to its bay — 2
Check the rear glazing spacers and beads against the door’s wider uprights. Their wood must remain outside the pane pocket; no bead screw may pass through a pane edge or its expansion gap.
Mark the door and bay as a pair. Remove temporary spacers only when the hinges and a helper support the leaf. Acrylic remains out during this fitting stage.
Check before continuing: The reference and actual finished gaps are recorded; the viewing opening and rear pocket remain unchanged.
Tools / setup: Supported router jig, depth stop, actual wire and cured film sample
Before you begin: Qualify the actual cut wire edges and coating before assembly.
Route the side-capture wire pockets
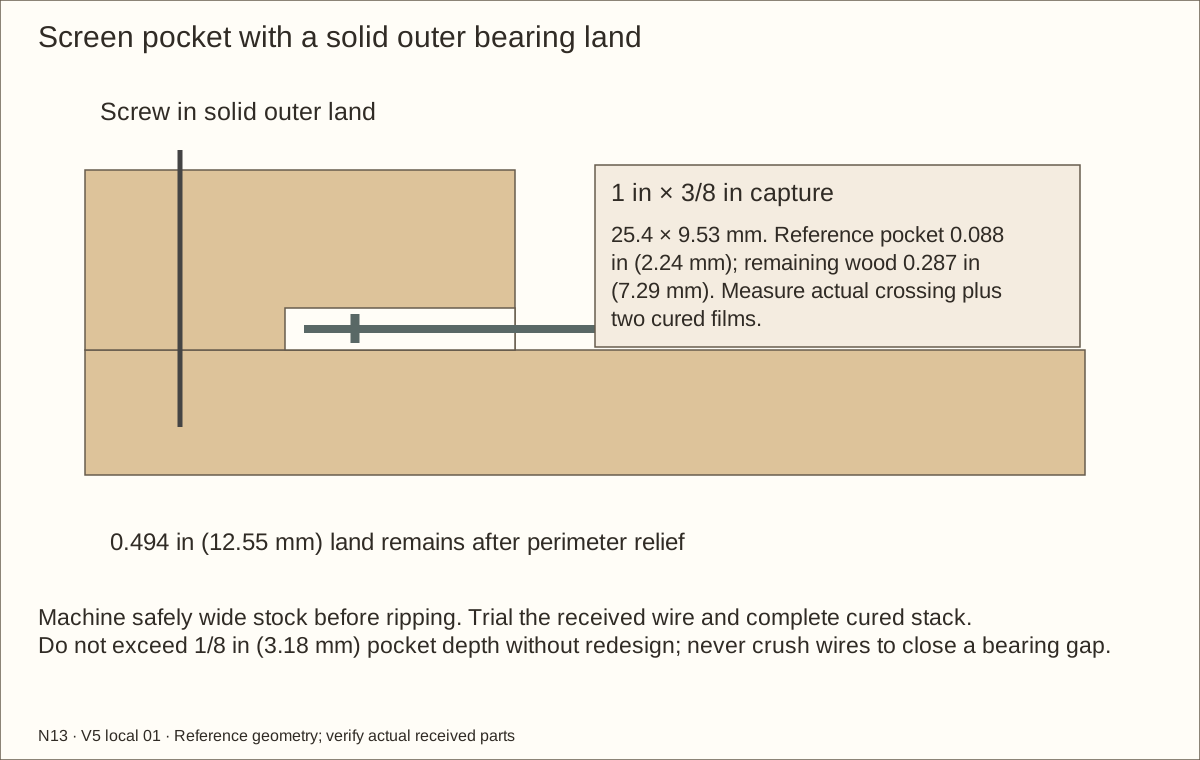
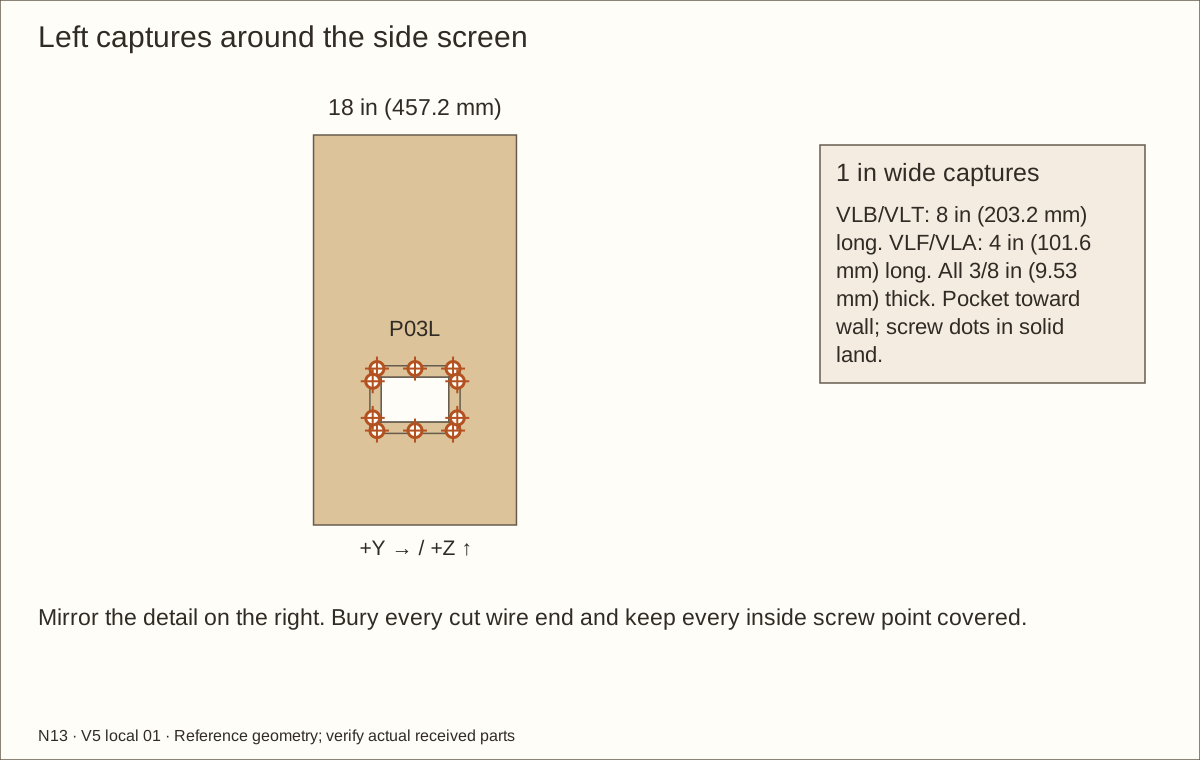
On the broad 3/8 in (9.53 mm) capture stock, lay out the pocket and separate outside bearing land. Route the wall-facing rebate with a supported guide and depth stop; do not hand-hold a loose narrow piece. Reference depth is 0.088 in (2.24 mm) for 0.082 in (2.08 mm) crossing wire plus 0.006 in (0.15 mm) cured films.
Trial the actual wire and film. Each widened 1 in (25.4 mm) capture must lie flat on its solid 0.494 in (12.55 mm) reference outer land, enclosing every cut wire end. The rebate cannot exceed 1/8 in (3.18 mm) without redesign. Drill screws through the separate land, never through wire.
Check before continuing: Capture bears flat; wire and screw paths are separate.
Tools / setup: Measuring tape, square, pencil and the tools named below
Capture the two side-vent meshes — 1
Cut two 7 in (177.8 mm) × 5 in (127 mm) mesh blanks with protected hands and snips. Flatten the edges and remove loose wire ends; do not leave a burr pointing into the enclosure.
Centre each 7 in (177.8 mm) × 5 in (127 mm) blank from outside for 1/2 in (12.7 mm) overlap beyond the original opening. Dry-seat the four widened 1 in (25.4 mm) captures with their wire pockets facing the wall; the 0.494 in (12.55 mm) reference outer land must touch solid wood. Keep all cut wire ends inside the pocket and no veneer beneath this bearing.
Check before continuing: Every side-screen cut end lies within its capture pocket and the solid outer land sits on wood.
Tools / setup: Measuring tape, square, pencil and the tools named below
Capture the two side-vent meshes — 2
Use the revised outer-land stations, clear of all wire. Clearance-drill the capture, make stopped #6 pilots into the wall, then fit #6 × 1 in (25.4 mm) screws flush at the bare wood face. Keep the head drive accessible through the veneer and at least 1/16 in (1.59 mm) interior tip cover. Do not force a strip over a wire crossing.
Inspect the entire captured perimeter. No wire end should be reachable through the inner opening or pull free when checked by hand. A smaller containment mesh opening, if required later, needs its own retained mounting and ventilation review.
Check before continuing: Both meshes are mechanically captured and the inner wood reveals are smooth.
Tools / setup: Supported router jig, depth stop and sample
Route the roof-capture wire pockets
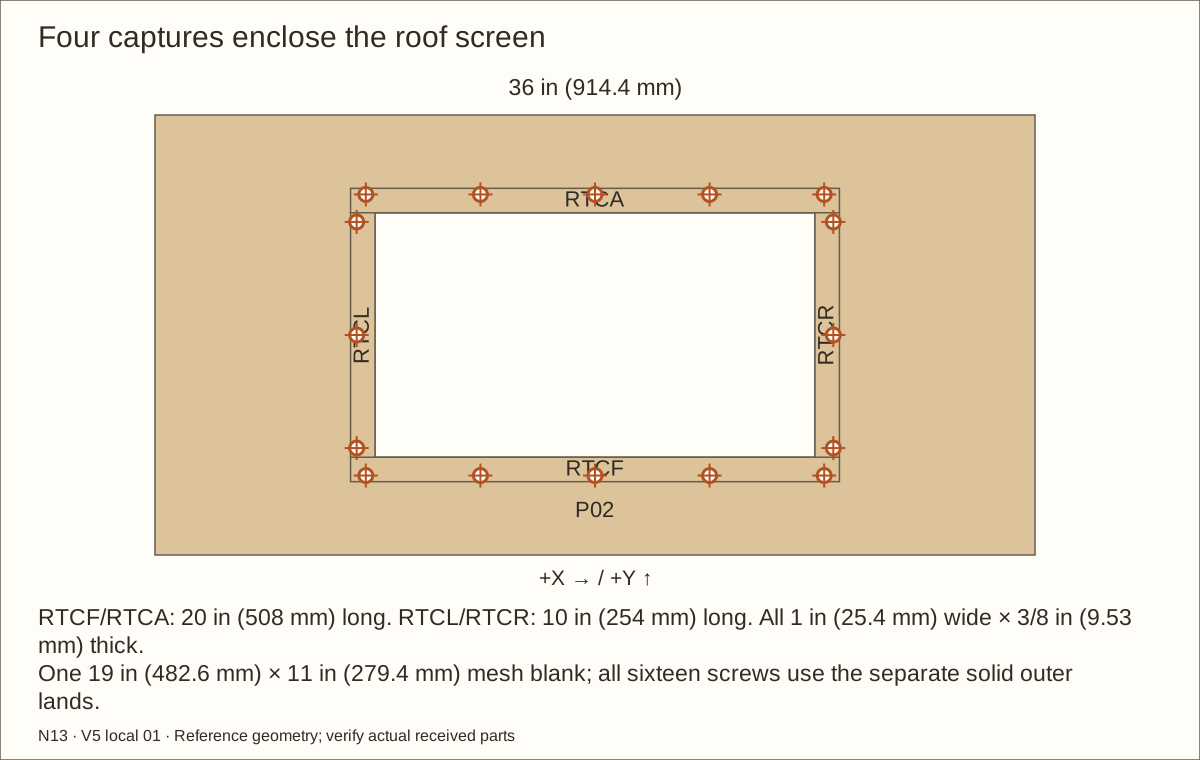
Use the same accepted wire/cured-film sample to fit the four roof captures. Cut a 0.088 in (2.24 mm) reference roof-facing rebate, preserving the 0.494 in (12.55 mm) outer bearing land and at least 1/4 in (6.35 mm) wood beneath the pocket.
Machine with broad stock and safe supported stops before cutting narrow final lengths. Dry-seat the complete 19 in (482.6 mm) × 11 in (279.4 mm) wire blank and verify all four captures bear on roof wood without rocking.
Check before continuing: Entire wire perimeter is enclosed and the solid outer lands touch P02.
Tools / setup: Measuring tape, square, pencil and the tools named below
Build the removable screened roof — 1
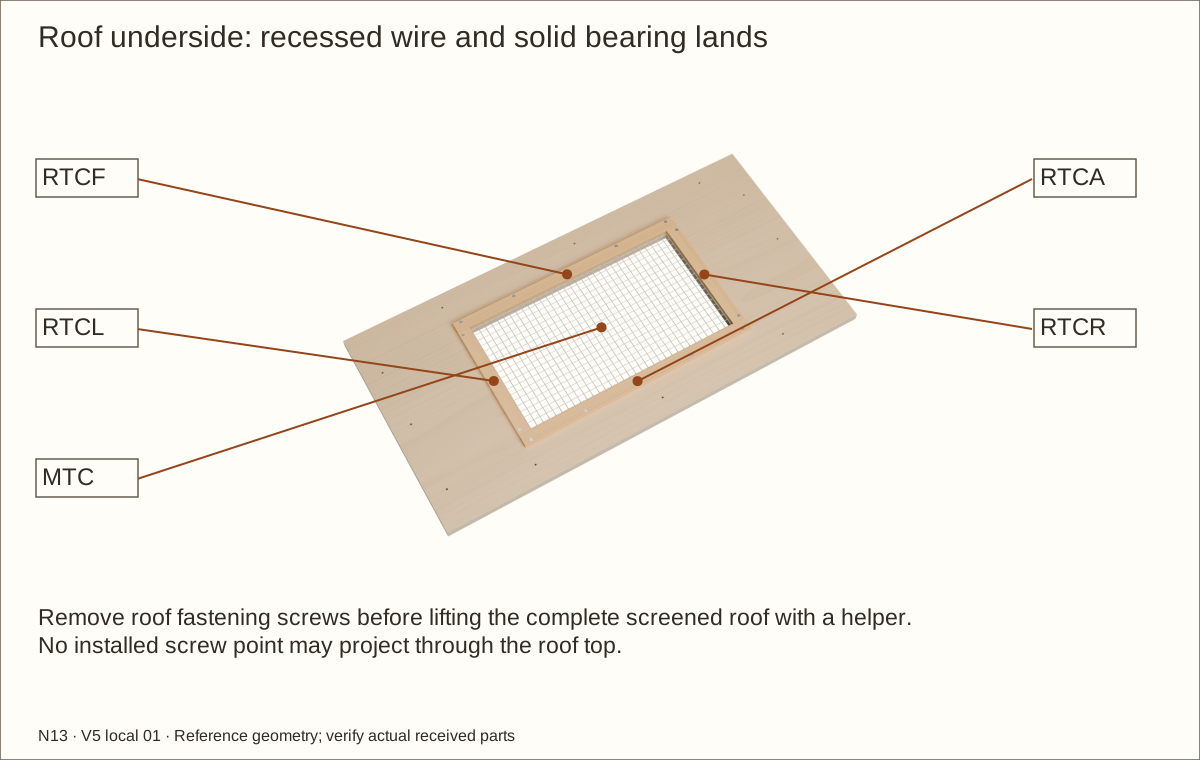
Lay P02 upside down on a padded bench. Centre one 19 in (482.6 mm) × 11 in (279.4 mm) mesh blank over the roof opening, keeping 1/2 in (12.7 mm) edge overlap.
Use the four widened captures RTCF/RTCA/RTCL/RTCR. Fit the 0.088 in (2.24 mm) reference rebate to the received two-wire crossing and cured film, leaving at least 1/4 in (6.35 mm) strip thickness without redesign. Solid outer lands bear on P02. Fit sixteen #6 × 1 in (25.4 mm) screws at the scheduled outer-land stations, with no tip through the roof top.
Check before continuing: The roof wire and all four captures fit flat without exposed cut ends or crushed wire crossings.
Tools / setup: Measuring tape, square, pencil and the tools named below
Build the removable screened roof — 2
No roof rib is needed over this single opening; the solid roof borders bear on the front frame and the side and rear upper wood supports.
Check the roof fits on the fixed front frame, side upper wood supports and rear upper wood support. Transfer its attachment stations, then set it aside for finishing. Screens carry no light fixture, climbing or lifting load.
Check before continuing: Every mesh edge is captured and the roof remains removable.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Support the leaf with a helper whenever a hinge is being fitted or released.
Hang the door on true lift-off hinges — 1
Support the unglazed door in the refitted bay at its scheduled gaps. Retain the original hinge join centres at Z = 12 29/64 in (316.31 mm), 20 5/16 in (515.94 mm) and 28 11/64 in (715.57 mm) above the floor underside. These are absolute datums; do not remeasure 3 1/2 in (88.9 mm) from the newly trimmed door ends. Align the actual three axes with a straight reference. For this bare-case trial, place removable fully cured matching veneer coupons beneath both hinge leaves. Use coupons of the accepted final face thickness, cut from the allocated trial sheet; do not attach the permanent face skins yet.
Use the received hinge as the hole template. Its fixed lower pin half mounts on the jamb and its upper removable socket mounts on the door. In this guide the single door hangs on the left jamb with LSX-100R; the LSX-100L hand is not used. Confirm the hand by the manufacturer’s fixed-half orientation.
Check before continuing: All three marked axes align; equal accepted cured coupons reproduce the intended final mounting plane.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Support the leaf with a helper whenever a hinge is being fitted or released.
Hang the door on true lift-off hinges — 2
During this trial, trace both leaves on the equal cured coupons. At final reassembly replace the coupons with continuous accepted face veneer beneath both leaves; the reference hinge axis is 0.30609055 in (7.77 mm) ahead of bare FRONT. Transfer all six holes per hinge, drill accepted stopped #6 pilots and fit #6 × 1 1/4 in (31.75 mm) screws. The complete hinge is translated forward by the measured face stack, without deforming its profile. Verify screw seating, veneer bond/compression and full flat bearing with the accepted trial before proceeding.
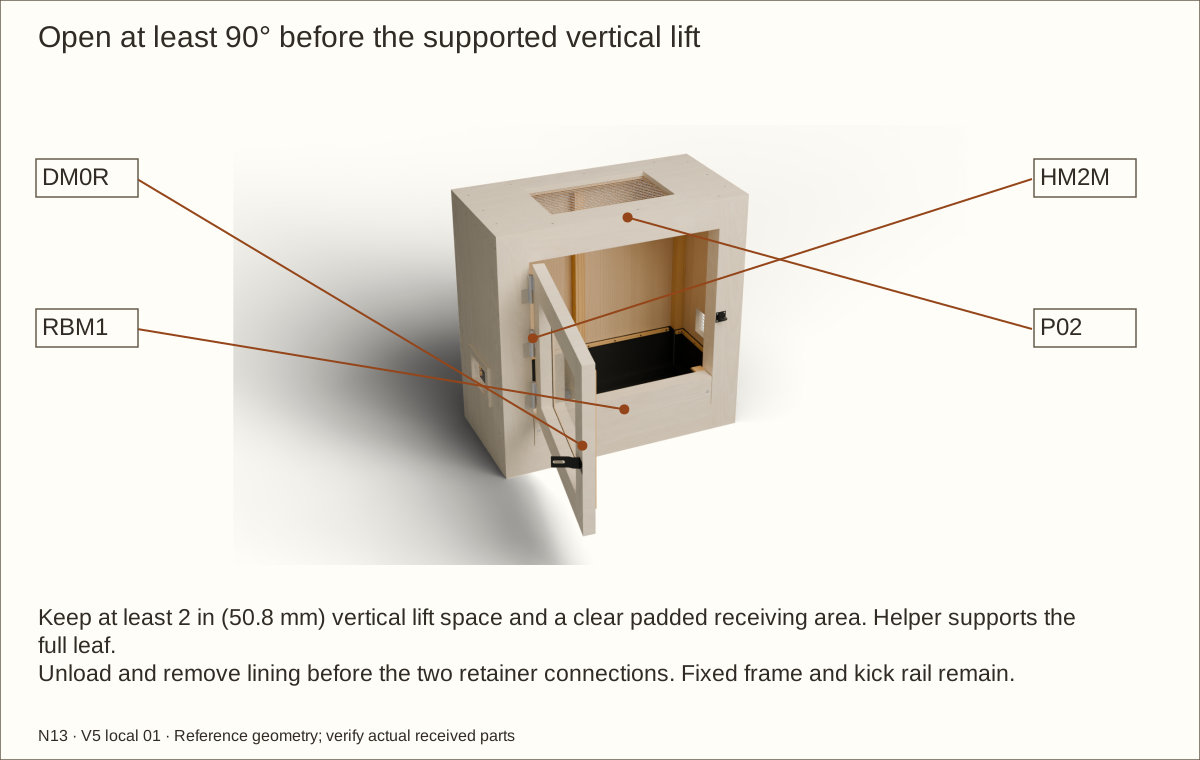
Remove the spacers while supporting the leaf. Slowly swing to 100°, checking the jambs, retainer top and rear beads. At 90° or more, support and lift 2 in (50.8 mm) to clear the pins, then refit all three sockets together. Stop and correct misalignment or binding.
Check before continuing: All three axes align; supported full swing and two-inch lift-off work without binding.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Rehearse the empty cleaning route — 1
With the enclosure empty, lift off the door and set it on padded supports. Remove the roof using a helper; do not use mesh as a handle.
With the entire bed empty, remove the lining clamps and fold liner and underlay clear of both receivers. Support the retainer, hold each front hex drive and remove the recessed interior nut and washer. Withdraw both machine screws outward and draw the panel forward. Keep the permanent frame and kick rail attached.
Check before continuing: The empty lining and complete retainer can be removed without undoing the fixed frame.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Rehearse the empty cleaning route — 2
After the door and retainer are removed, the reference bare bay is 27 19/32 in (700.88 mm) wide. Opposing maximum veneer reduces the clear width to 27.50175 in (698.54 mm). The fixed kick rail is 3 3/8 in (85.73 mm) above the reference finished floor. Trial the actual cleaning containers and tools through this route and around the rear corners.
Dry-fold liner and underlay blanks through the front corners and rear uprights. Confirm slack at every change of direction, space for the front clamps and a route to lift out the complete empty basin. Refit and tighten the retaining panel before continuing.
Check before continuing: The entire empty base can be serviced without removing the fixed frame or moving a loaded enclosure.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Prepare and fully finish the wood — 1
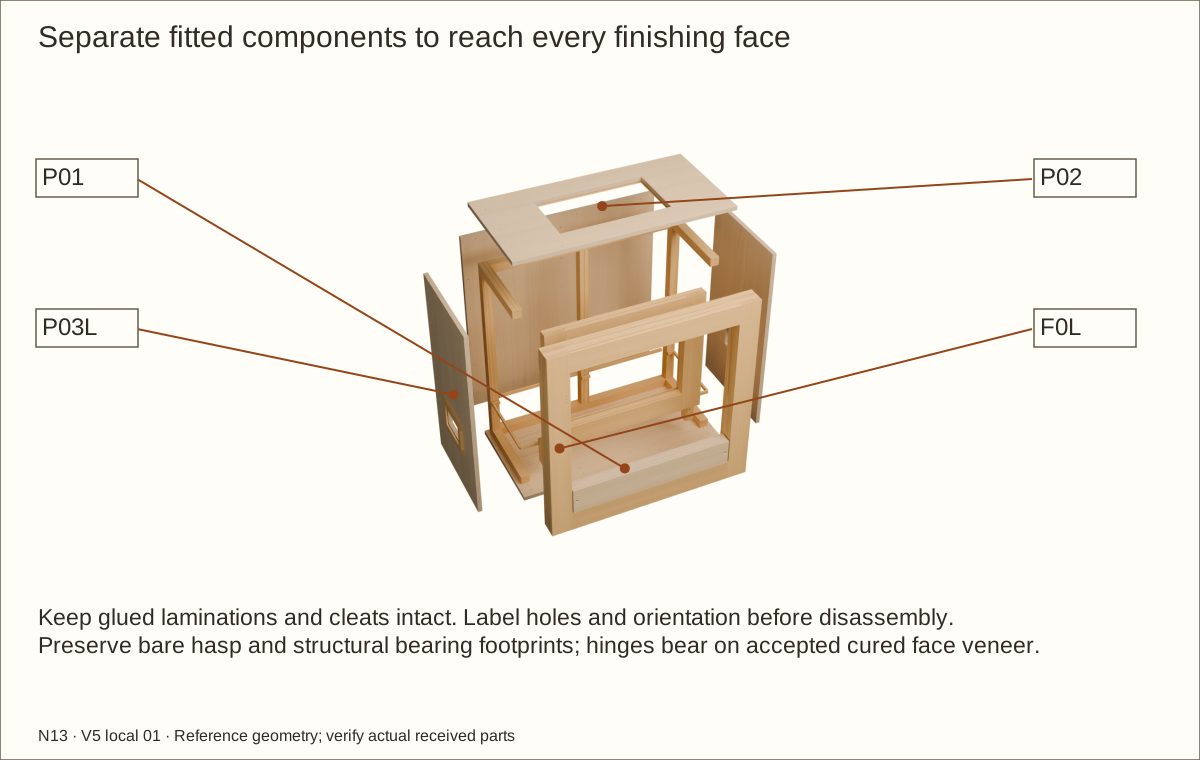
Label and remove the door, retainer, roof, hardware, meshes and lining. Disassemble dry joints as needed to reach every face, keeping all cured laminated and glued assemblies intact. Photograph orientation and protect the matched hole locations.
Ease sharp edges, repair splits and stripped receivers, sand and remove dust. Prepare accepted veneer/finish samples before the enclosure. Keep bare glue and hardware-bearing footprints masked, including the retainer underside and its receiver contact. Do not fill the service drives or stopped nut recesses.
Check before continuing: All parts are labeled, repaired, sanded and clean; protected bearing and drive areas are marked.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Prepare and fully finish the wood — 2
Apply the current Varathane Triple Thick satin label to the exposed wood and the supplier-approved presealed veneer substrate. The one-coat upper planning area is 181.5 sq ft (16.86 m²), including rectangular wood, veneer topcoat, trial and contingency. Buy 2 two-can packs; each can is one US quart (0.946 L). Extra coats or balancing layers need revised quantities.
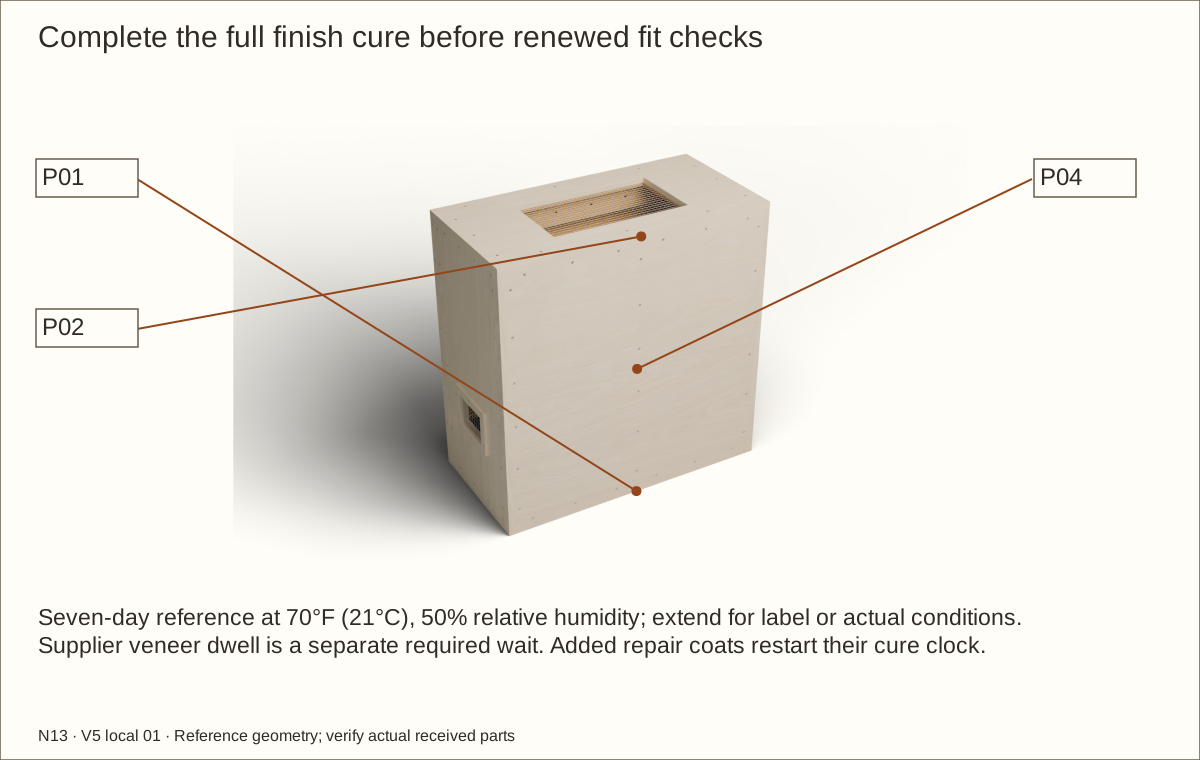
Allow the full seven-day cure at the manufacturer’s stated 70°F (21°C) and 50% relative humidity reference conditions, longer when the label or conditions require. Handle and recoat only at the permitted times. An odor check or surface dryness does not replace full cure.
Check before continuing: All wood, cut reveals and protected below-liner surfaces are covered and fully cured.
Required wait: Finish: seven days full cure at stated reference conditions; extend as required
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Do not substitute an unapproved adhesive or balancing system.
Approve and label the full exterior veneer
Choose one species for the entire enclosure: maple, white oak or walnut. Obtain written supplier acceptance for the backing/PSA, balance of each panel, actual cured substrate, service temperature/humidity and cleaners. The preview textures are appearance references, not a delivered grain sample.
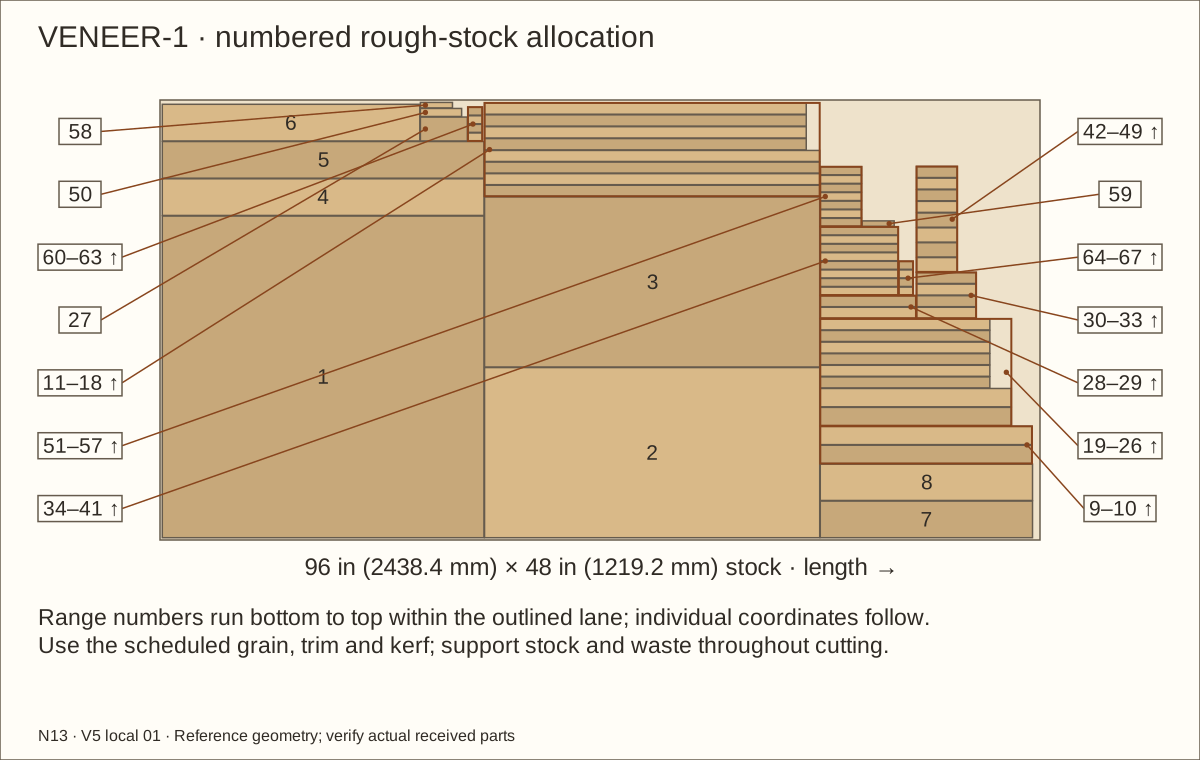
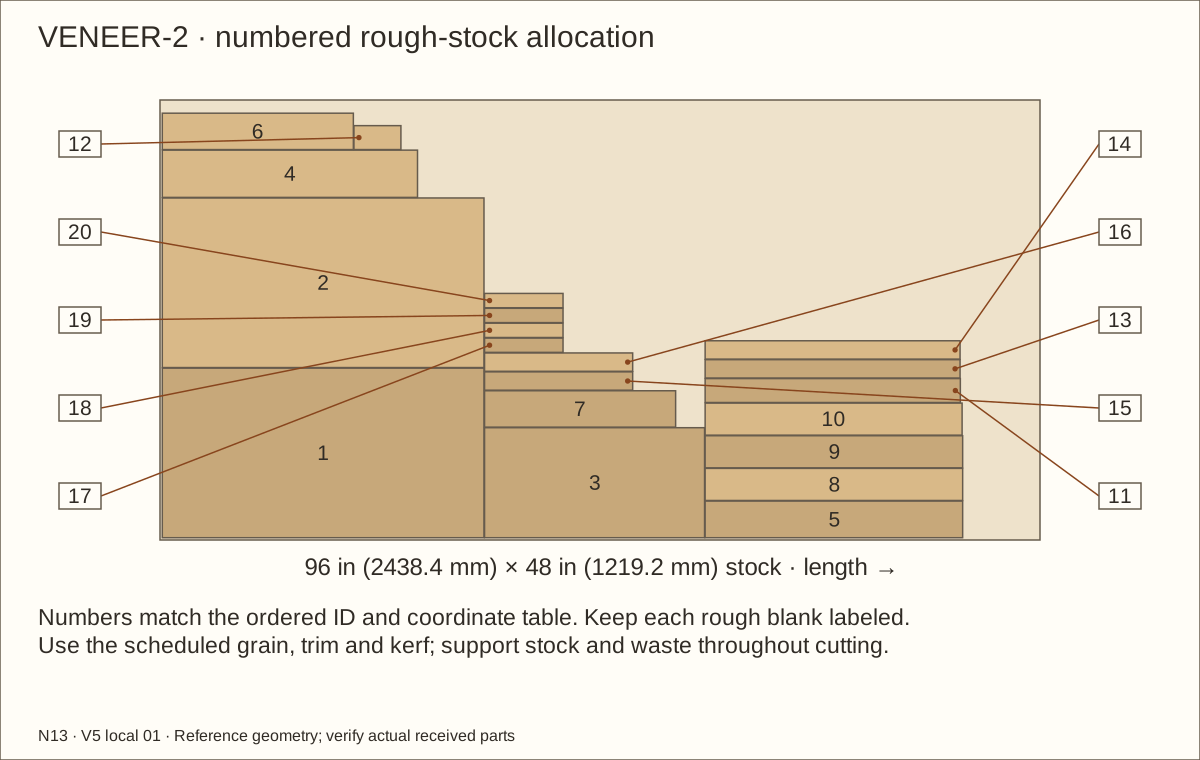
Use the veneer layouts to rough-cut labeled faces and edge/reveal strips with grain in their scheduled direction. The reference whole skin is 0.0305 in (0.77 mm) and the maximum coordinated skin is 0.046 in (1.17 mm). Measure actual cured samples; a thicker system requires new dimensions and motion checks.
Check before continuing: The selected whole system and actual thickness are accepted before sticking any full sheet.
48. Apply the skins without bridging removable parts
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Apply the skins without bridging removable parts
Acclimate and prepare the veneer and sealed substrate for the supplier’s written conditions. Follow its pressure tool, application sequence and full bond-development wait. Retain that required duration in the receiving record; this guide does not invent one. Start with a matching offcut sample and inspect bond and balance first.
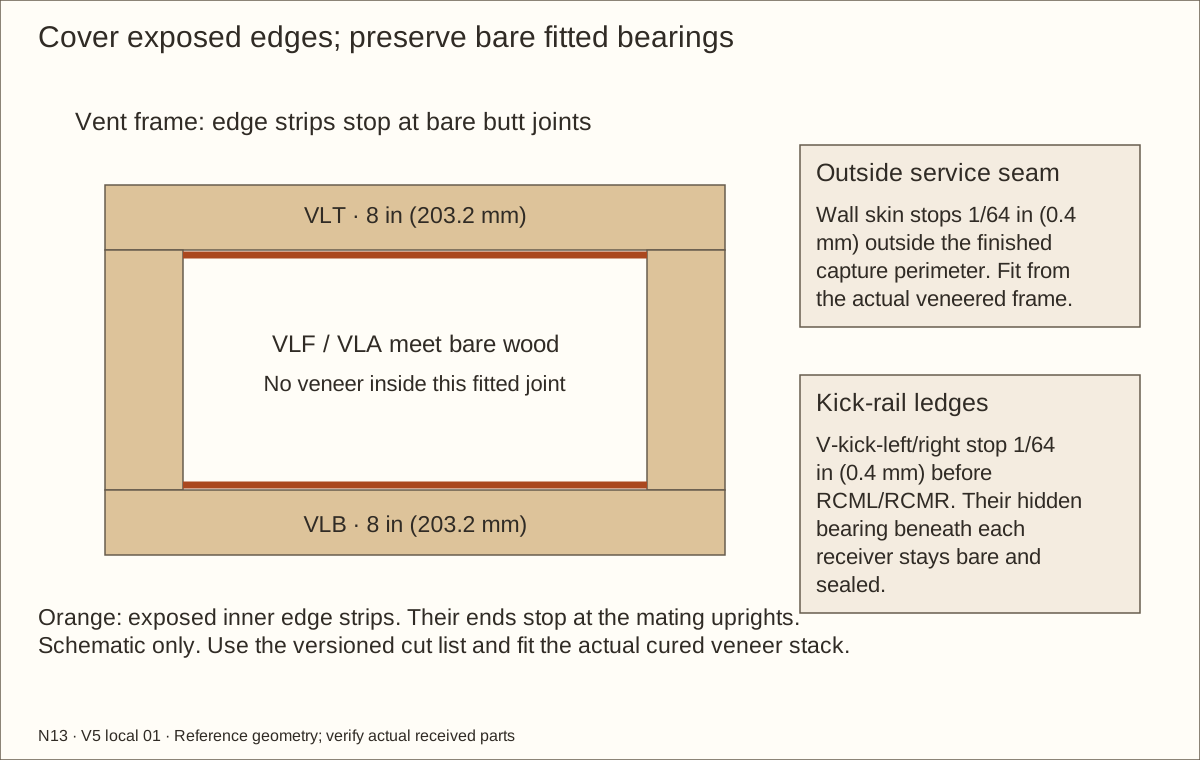
Apply each scheduled exterior face, roof surface, exposed edge and reveal separately. Stop vent edge bands at bare butt joints; fit the wall skin 1/64 in (0.4 mm) outside the finished vent-frame perimeter. Stop the two kick-rail ledge skins 1/64 in (0.4 mm) before the receivers, leaving their hidden bearings bare. Keep the retainer underside and receiver-contact faces bare and sealed; preserve all service seams, traced bare hasp footprints and 0.55 in (13.97 mm) retainer-drive openings. Trim with a supported straightedge and sharp tool without rounding the reference mating edge.
Check before continuing: All exposed plywood edges are covered, while joints, bearing seats and drives stay accessible.
Required wait: Supplier-specified acclimation, pressure and full bond-development wait; unresolved H03 must be closed first.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Topcoat and fully cure the completed veneer
Apply only the supplier-accepted clear finish to the completed veneer, exposed edges and reveals. Keep bare hasp seats, drives and future bond faces masked; hinge bearing faces retain the accepted continuous cured veneer. Follow the actual label temperature, humidity, recoat and handling limits.
Allow the Varathane full seven-day cure at 70°F and 50% relative humidity, or longer if the label/conditions require, before renewed assembly tests. Surface dryness or lack of smell is not proof of cure. Check the sample bond, panel flatness and actual completed skin again.
Check before continuing: All finishes are fully cured and the accepted actual veneer stack remains within the coordinated allowance.
Required wait: At least seven days full finish cure at stated reference conditions; extend as required.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
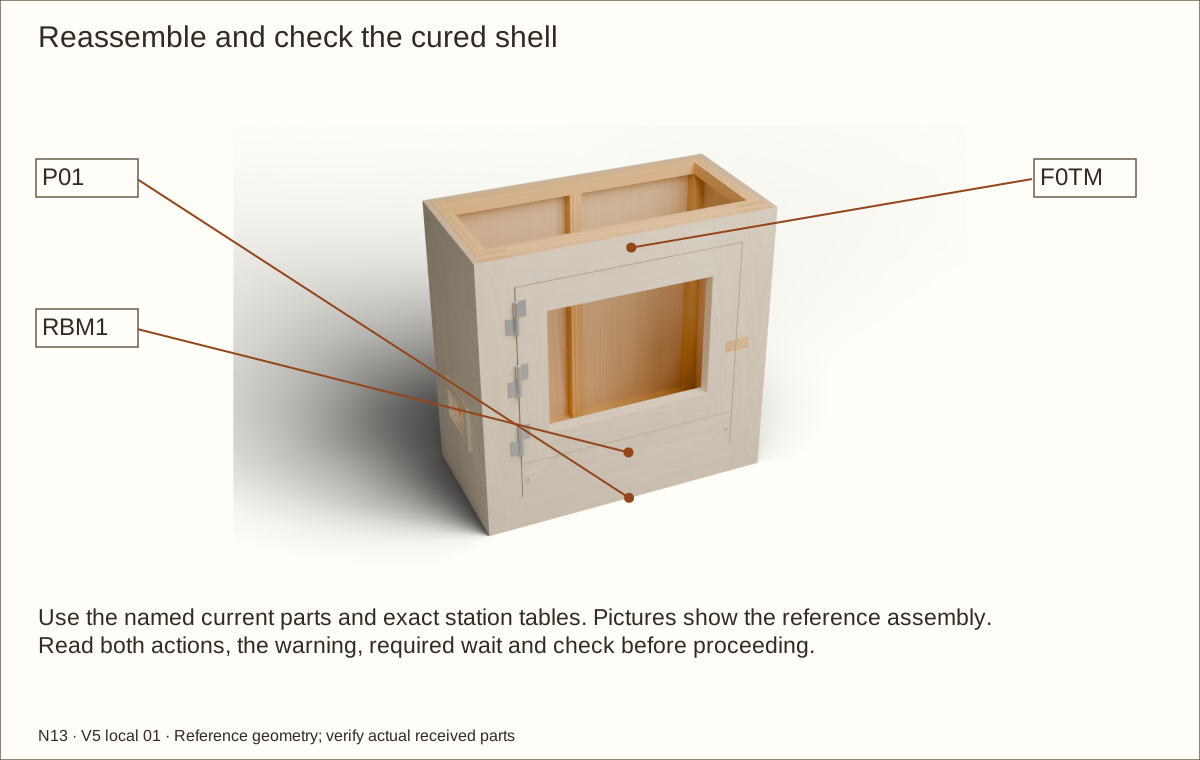
Reassemble and check the cured shell — 1
Refit the floor, sides, back, rear uprights and fixed front frame to their labeled holes. Hand-tighten the scheduled screws, checking their seating and covered tips; replace a damaged receiver properly rather than using an arbitrary longer screw.
Refit both receivers and the retainer with their complete flush screw/washer/recessed-nut stacks. Confirm two full exposed threads, recessed tip cover, square frame and continuous floor bearing without crushing the cured wood. Leave veneer drives accessible. Add loose protective underlay over both stopped rear pockets before placing the basin.
Check before continuing: The cured shell and complete retainer connections are square, accessible and seated without crushing wood.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Reassemble and check the cured shell — 2
Refit all three screened openings and the unglazed door. Repeat the complete swing and lift-off checks with the actual cured veneer stack, including the latch back-bevel and retainer-top clearance. Recheck after any adjustment; newly exposed wood needs resealing and full recure.
Remove the door and roof again for lining. Keep every bolt head smooth and add extra underlay over head seats and any hard corner that might rub the membrane.
Check before continuing: The cured shell is square and mechanically complete, with clear door motion and a smooth basin backing.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Never cut, drill or staple below the upper dry clamping band. The shallow observation is not a load test.
Fit and test the continuous basin — 1
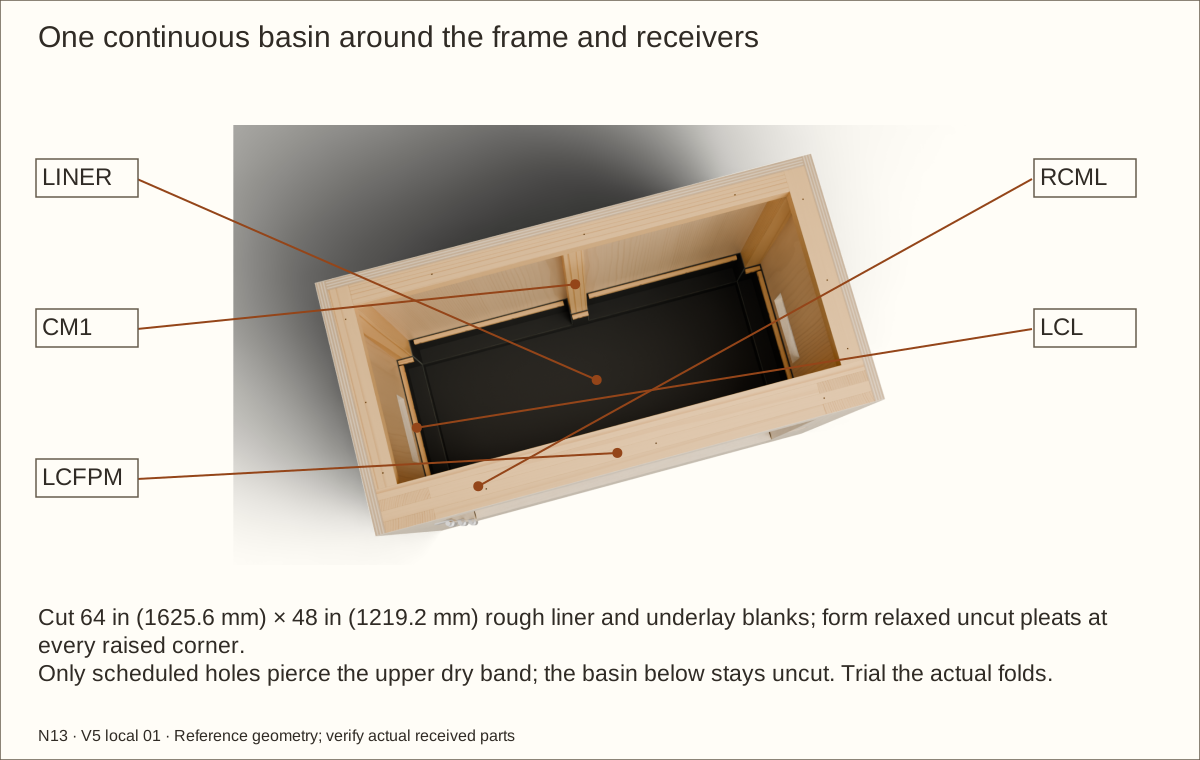
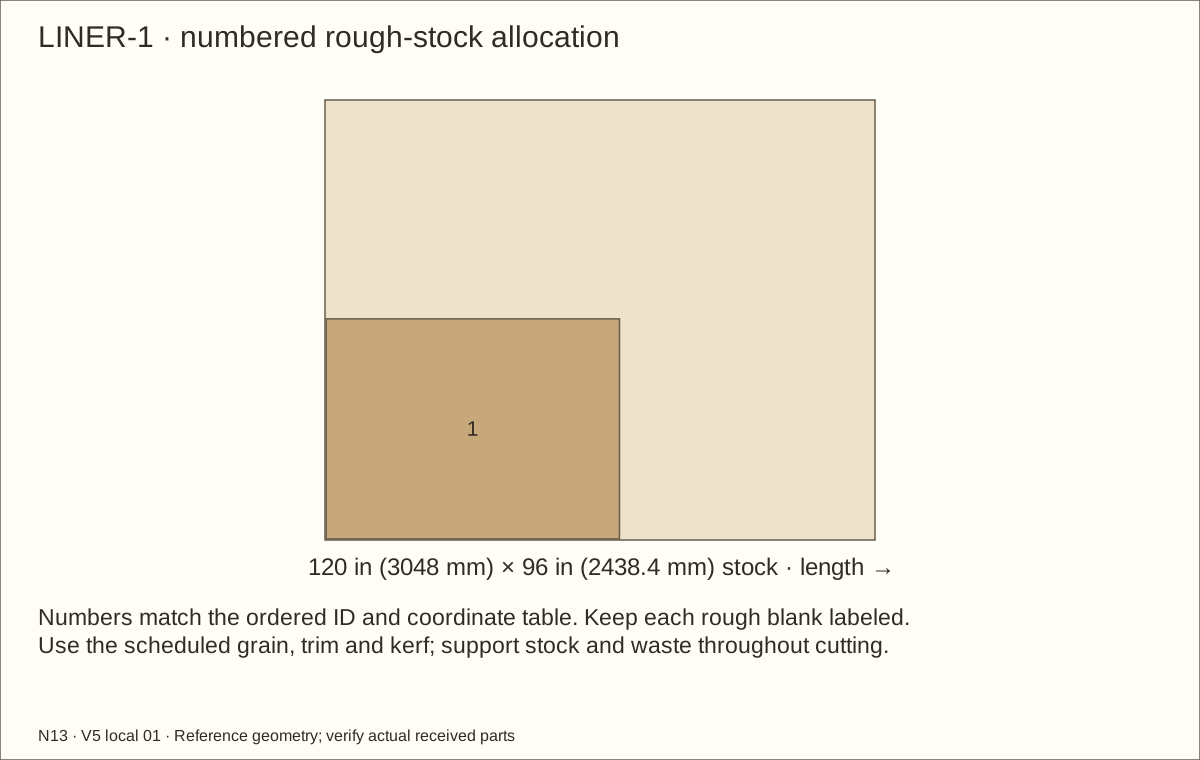
Remove the roof with a helper and lift off the supported door onto a padded bench to expose the empty basin area. Cut one 64 in (1625.6 mm) × 48 in (1219.2 mm) EPDM blank from the 96 in (2438.4 mm) × 120 in (3048 mm) liner and a matching underlay blank from the 60 in (1524 mm) × 120 in (3048 mm) underlay. Orient each long cut along its stock’s longer side. Dry-fold first; do not trim away a corner to make it lie flat.
Lay the underlay across the central floor and every raised support and eased corner, including extra loose pads over both rear nut recesses. Drape the liner above it around the two front receivers, fixed jambs and three rear uprights. Form uncut relaxed pleats; no membrane may bridge a void, stretch over a hard edge or be cut or punctured below the upper dry clamping band. Trial the real stack before clamping.
Check before continuing: The underlay protects every hard contact and the relaxed liner has no unsupported folds or cuts.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Never cut, drill or staple below the upper dry clamping band. The shallow observation is not a load test.
Fit and test the continuous basin — 2
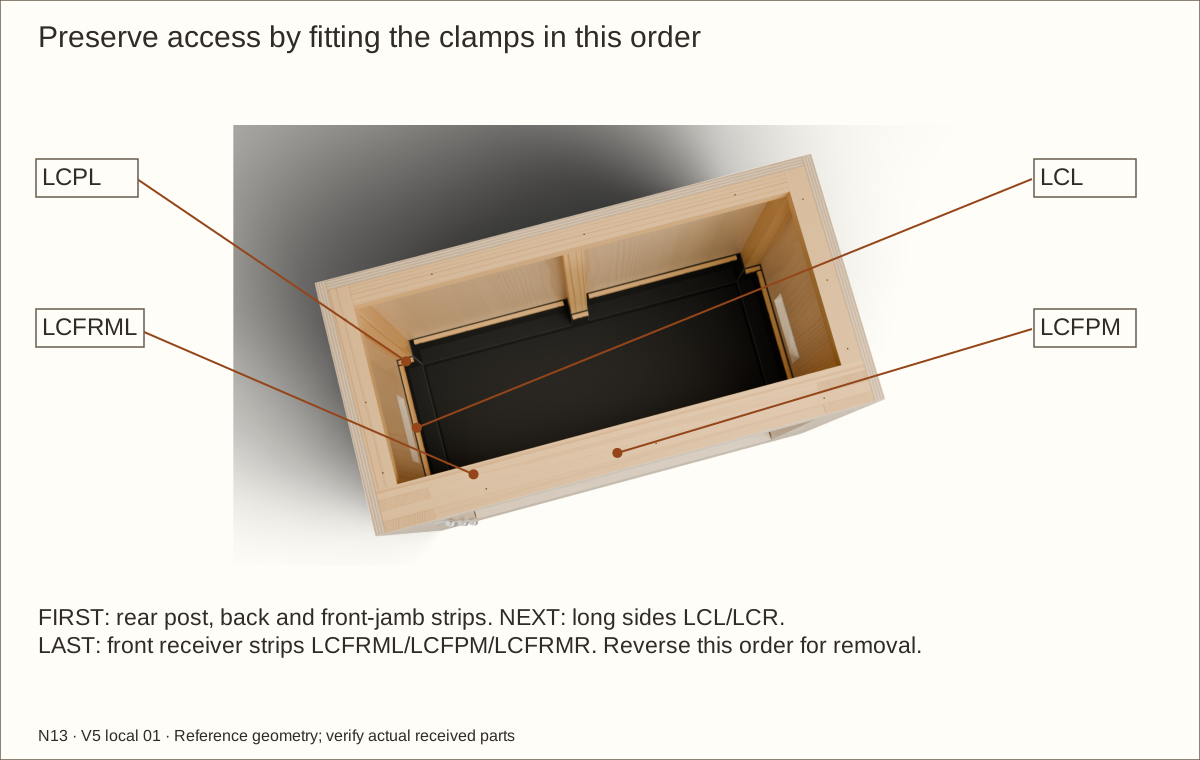
Use twelve rounded clamp strips. Their reference screw line is 7 3/8 in (187.33 mm) above the finished central floor; liner top is 7 3/4 in (196.85 mm) and maximum total bed is 6 in (152.4 mm). Fit rear post strips LCPL/LCP1/LCPR, back strips LCB1/LCB2 and front-jamb strips LCFJ1/LCFJ2 first. Fit LCL/LCR next, then front receiver strips LCFRML/LCFPM/LCFRMR last. Reverse that order for removal so every driver route stays open. Only the 36 scheduled clamp screws may pierce the dry band from 7 1/8 in (180.98 mm) to 7 5/8 in (193.68 mm) above the central liner floor. Pre-drill and deburr wood separately, remove debris, then refit the relaxed folds and press each screw through its planned station by hand before tightening. Never wind loose rubber around a drill bit. Trim only above the final top line.
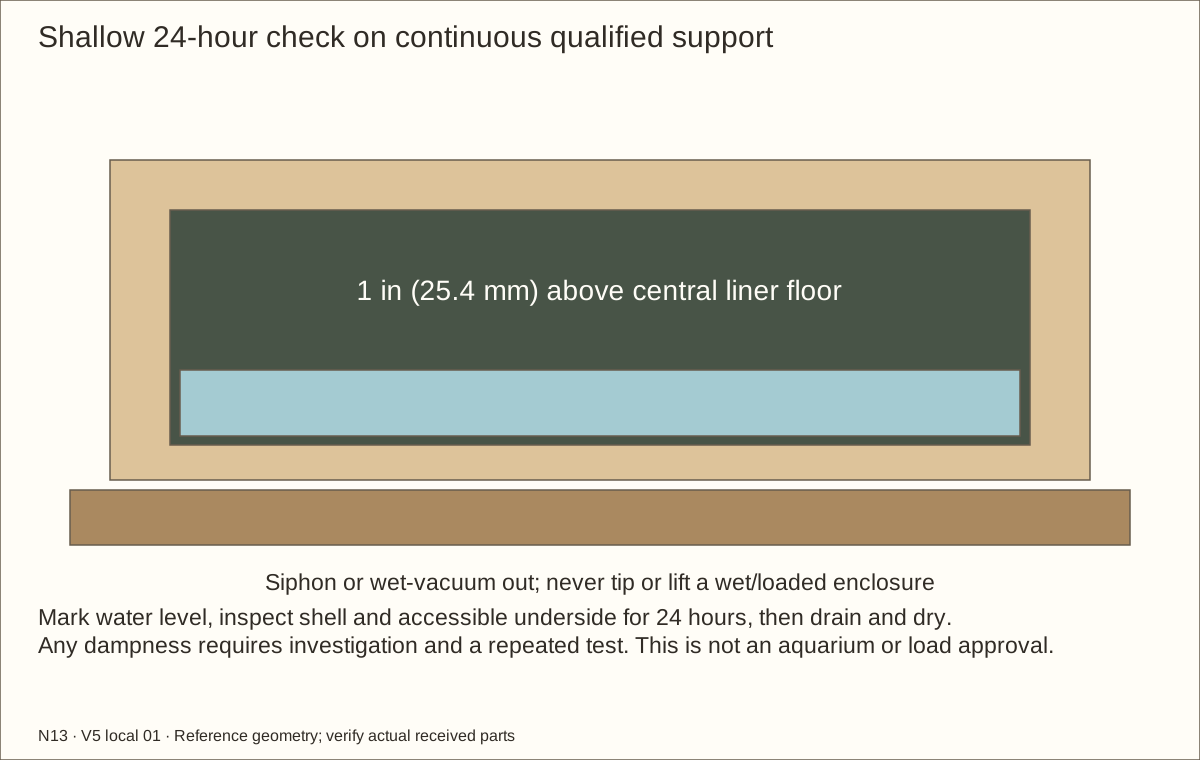
With the retaining panel fully bolted and the floor supported, add only 1 in (25.4 mm) of water for a 24-hour shallow seam-and-fold observation. Inspect accessible wood and the underside for leakage without moving the shell. Siphon or wet-vacuum the water, dry completely and correct any leak before filling. This shallow check is not a full-depth tank or structural test.
Check before continuing: The basin is continuous, slack at corners and dry beneath after the shallow test; all clamps remain removable.
Required wait: Shallow liner observation: 24 hours, followed by complete draining and drying
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Do not drill, glue, squeeze or rigidly trap the acrylic.
Cut and retain the floating acrylic pane — 1
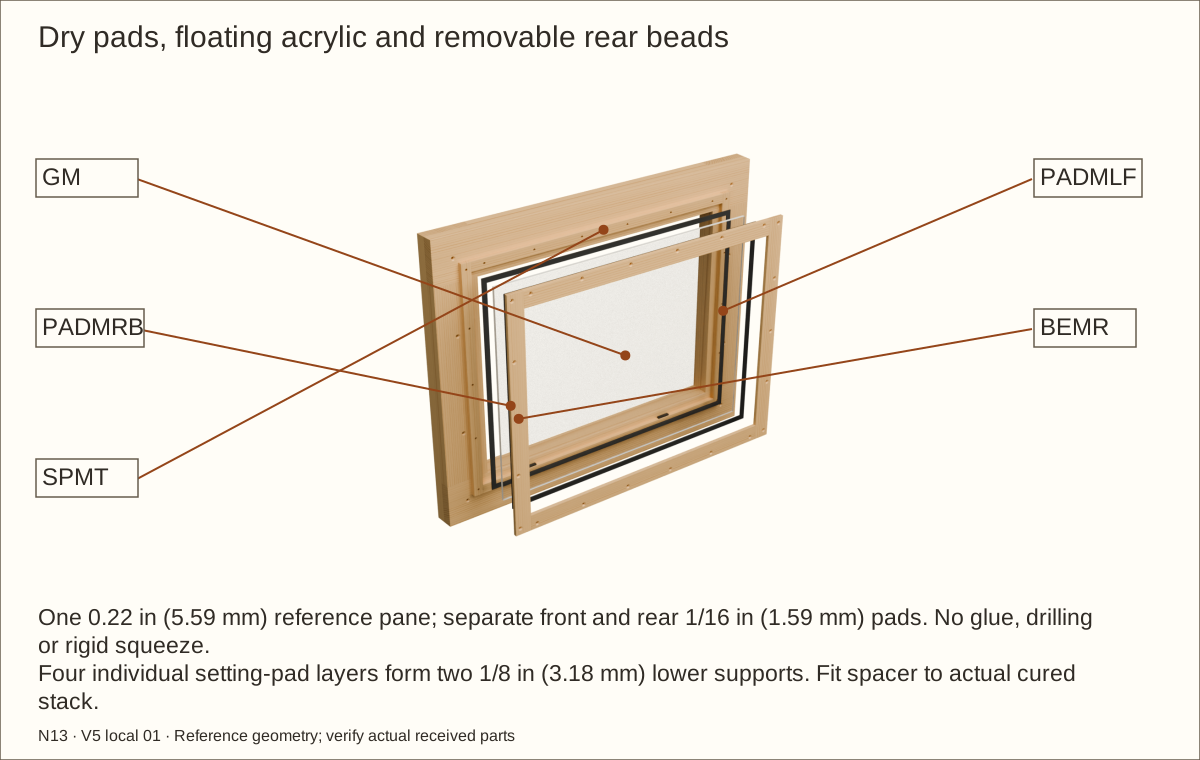
Measure the fully cured pocket and actual acrylic. The reference pane is 21 11/32 in (542.13 mm) wide × 16 23/32 in (424.66 mm) high × 0.22 in (5.59 mm) thick, from one 24 in (609.6 mm) × 48 in (1219.2 mm) sheet. Retain the masking, support the complete sheet on a clean sacrificial surface and use the acrylic maker’s accepted cutting/edge-finishing method. The actual pocket and movement allowance govern the final cut.
Fit spacers and two lower setting pads in the frame. The pocket is 1/4 in (6.35 mm) larger than the pane in width and height; centre the pane with 1/8 in (3.18 mm) at each side and top. The lower 1/8 in (3.18 mm) gap holds the two-layer setting pads. Keep the pane free to move as temperature changes.
Check before continuing: Actual pane and pads are measured and fitted to the cured pocket with open edge allowance.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Do not drill, glue, squeeze or rigidly trap the acrylic.
Cut and retain the floating acrylic pane — 2
Fit separate dry front and rear pads, then the removable beads. Mill each spacer from 3/8 in (9.53 mm) rough stock to the measured pane/pad/cured-film stack; 0.351 in (8.92 mm) bare thickness is a reference. Transfer stations through the beads and spacers into the named laminated-frame receiver outside the pane perimeter. No screw may enter the pane or its edge gap.
Use #8 × 1 1/4 in (31.75 mm) bead screws, tightening only until beads seat on spacers. Do not squeeze the pane, drill it, glue it into the pocket or fill its movement gap. Remove masking, clean with an acrylic-compatible method and inspect for cracks, bowing and free expansion space.
Check before continuing: The pane floats with edge clearance and beads seat on wood without squeezing it.
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: Do not drill, glue, squeeze or rigidly trap the acrylic.
Cut and retain the floating acrylic pane — 3
Weigh the complete finished glazed door. The revised rectangular-volume planning estimate is 16.69 lb (7.57 kg), including reference veneer and a hardware/pad/coating allowance. Rehang with a helper and repeat all swing, sag, secure-closure and lift-off checks. Hinge catalogue capacity does not certify this wooden assembly.
Check before continuing: The finished leaf is weighed and passes supported operation and removal checks.
Tools / setup: Measuring tape, square, pencil and the tools named below
Fit the door closure — 1
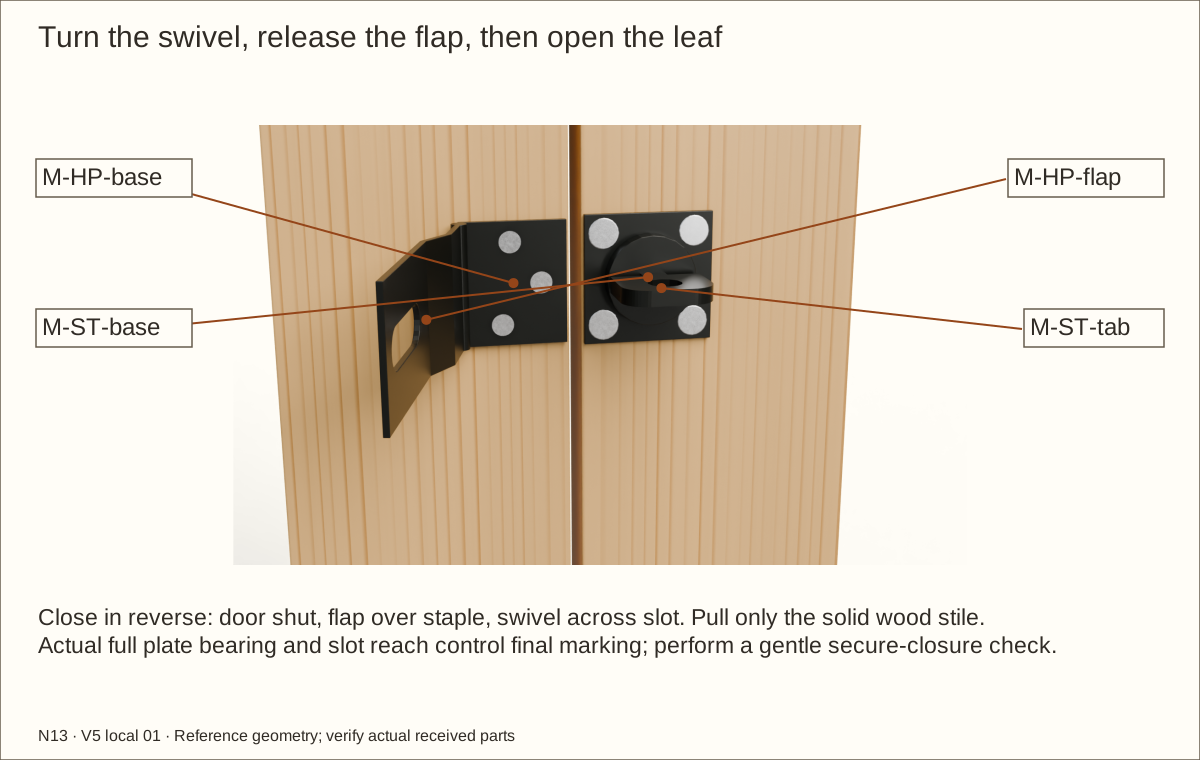
Close the glazed door. Fit the complete N305-979 hasp at the scheduled height, about 2 in (50.8 mm) below door mid-height, with its base on the right door stile and swivel plate on the fixed right jamb. This candidate shifts the complete nominal assembly 5/32 in (3.97 mm) toward the hinge side to fit the trimmed leaf; the actual full plate bearing and slot reach control final marking.
Place the swivel-staple plate on the fixed right jamb. Transfer the actual seven holes only after the slot, hinge and swivel operate freely. The model’s formed hardware is an illustration, not a drilling template.
Check before continuing: The real hasp has full bearing and reaches the staple freely before its mounting holes are drilled.
Tools / setup: Measuring tape, square, pencil and the tools named below
Fit the door closure — 2
Use the seven #10 × 5/8 in (15.88 mm) screws: clearance through the supplied plate holes and stopped pilots into solid wood. Keep at least 1/16 in (1.59 mm) wood behind each tip and all heads seated without distorting the hardware.
To open, turn the swivel in line with the slot, swing the hasp clear, then pull the solid door stile and open the leaf. To secure, close the leaf, fit the flap over the staple and turn the swivel across the slot. Do not pull on glazing. The one closure must resist a gentle pull when secured; optional padlocks are not included.
Check before continuing: The door stays closed when pulled gently and opens only after the hasp is released.
Tools / setup: Measuring tape, square, pencil and the tools named below
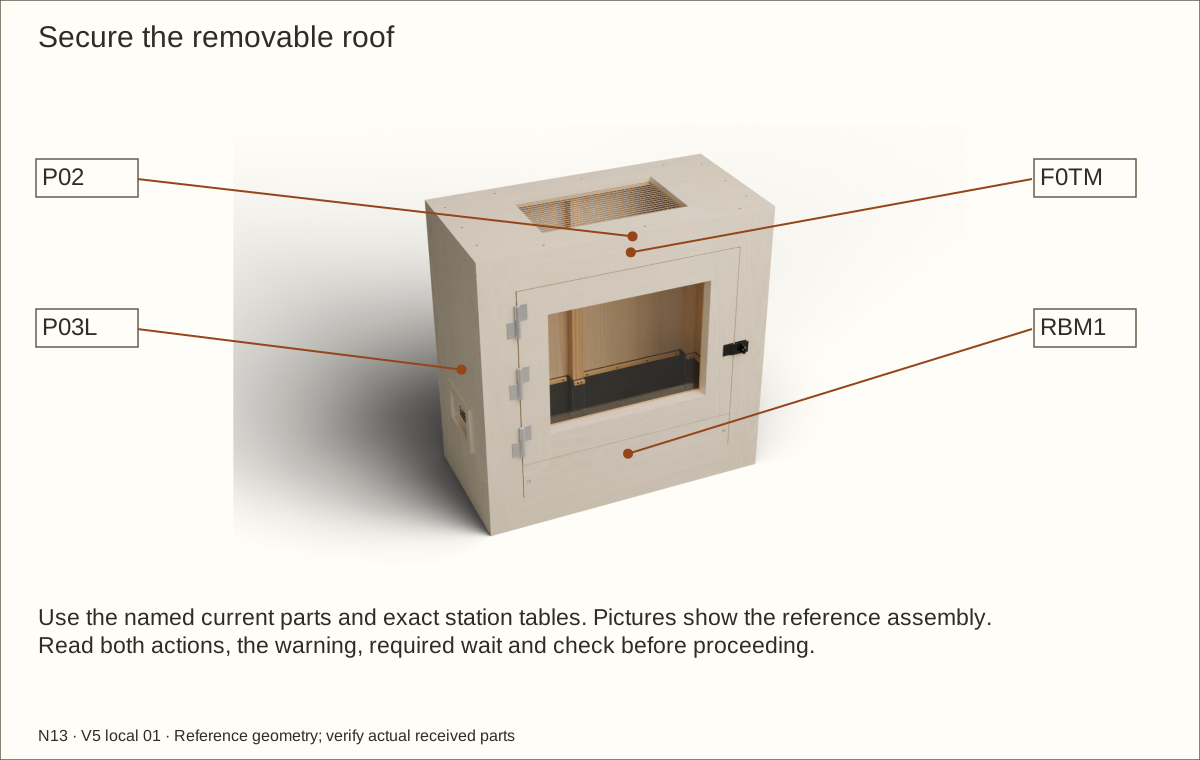
Secure the removable roof — 1
Verify the basin clamps, retained glazing, mesh and closures before placing the roof. With a helper, lower it onto the fixed front frame, both side wood supports and CT without trapping the liner or a cable.
Transfer the roof stations: three per side, three at the front and three at the back. Drill clearance through P02 and stopped pilots into the named receiver.
Check before continuing: All twelve roof clearance and stopped pilot stations match the actual receiving supports.
Tools / setup: Measuring tape, square, pencil and the tools named below
Secure the removable roof — 2
Install #8 × 1 1/4 in (31.75 mm) screws and tighten evenly by hand. Do not glue the roof. Recheck the door gaps and closure operation with the completed shell secured.
Keep screw heads reachable in the eventual equipment arrangement. Disconnect and independently support equipment before roof removal; never lift by the mesh.
Check before continuing: The roof cannot shift or lift unintentionally and the door keeps its correct fit.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Complete the construction inspection — 1
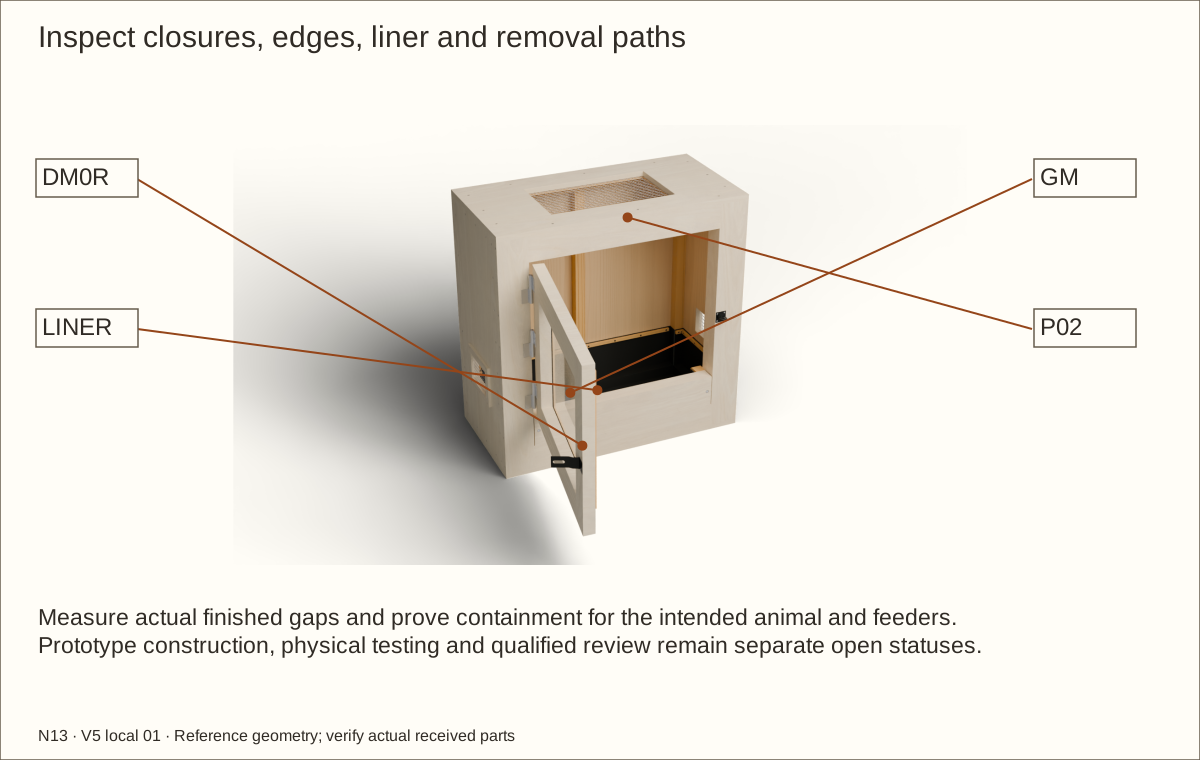
Check every screw station, both retainer bolt stacks, all three hinge assemblies, the hasp, all glazing beads, all twelve liner clamps and every mesh edge. Repair splits, burrs, stripped receivers, loose joints and exposed tips.
Measure the actual cured gaps around the door, retainer, roof and every opening. Scheduled clearances and 1/2 in (12.7 mm) mesh are construction references, not animal- or feeder-containment approval. Recheck after the roof is secured and after controlled loading on approved support.
Check before continuing: Fasteners, completed gaps and screens have been measured and entered in the construction record.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Complete the construction inspection — 2
Verify full finish cure and a dry shell beneath the shallow-tested liner. Confirm no screw, cable or drain penetrates the wet basin, and that every above-fill clamp can be accessed.
Rehearse supported removal and refitting of the single glazed door. Record its weight and actual finished clearances. For basin service: animals/equipment out, all contents and water removed, clamps off, empty liner/underlay folded clear, then both complete retainer fasteners removed and panel drawn forward. Never undo a retaining connection against loaded substrate or water.
Check before continuing: The completed construction record contains no unresolved defect; animal commissioning remains separate.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Place and measure the complete bed — 1
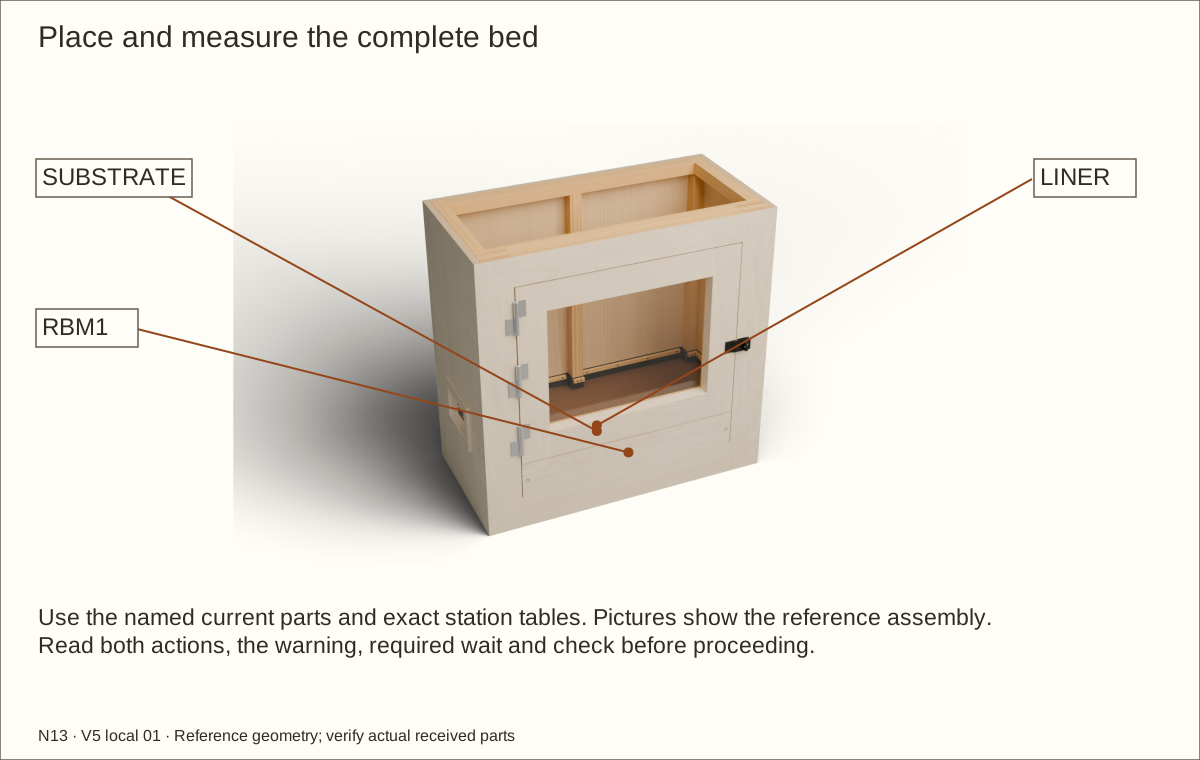
Place all permanent support and stability provisions before loading. Protect the membrane beneath hard furnishings with smooth load-spreading pads; never drag rocks or sharp tools over it.
Measure the entire bed from the finished central liner floor. Drainage, separators and substrate together must stay within 6 in (152.4 mm). For example, 2 in (50.8 mm) of drainage leaves at most 4 in (101.6 mm) for the other layers.
Check before continuing: The combined bed layers stay within the marked six-inch limit; supports and furnishings are secure.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Place and measure the complete bed — 2
The conservative uninterrupted floor rectangle is about 31 3/8 in (796.93 mm) × 11 15/16 in (303.21 mm), or 2.60 sq ft (0.24 m²). Above the full bed, about 27 in (685.8 mm) remains below the lowest upper supports before fixtures and furnishings are deducted.
Weigh the actual wet mix and record the installed total load. Watch for support deflection, changed door gaps, joint movement and liner damage during filling. Stop and unload if anything shifts. The density calculations are planning scenarios, not permission to load an unqualified stand or floor.
Check before continuing: The complete bed stays below its line with 2 in (50.8 mm) to the retainer top and documented remaining usable space.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: No animal suitability or equipment support rating is assigned by this construction guide.
Commission before animal entry — 1
Choose the intended species, life stage and occupancy against current care requirements using the measured usable interior. This 36 in (914.4 mm) × 18 in (457.2 mm) × 36 in (914.4 mm) shell is a generic construction guide and assigns no species suitability.
Qualify every gap, latch and mesh opening for the occupant and feeders. Fit a mechanically retained finer barrier where needed, then reassess ventilation, visibility and cleaning.
Check before continuing: The intended species and life stage are recorded; any finer barrier is securely fitted and its ventilation will be checked during the following environmental trials.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: No animal suitability or equipment support rating is assigned by this construction guide.
Commission before animal entry — 2
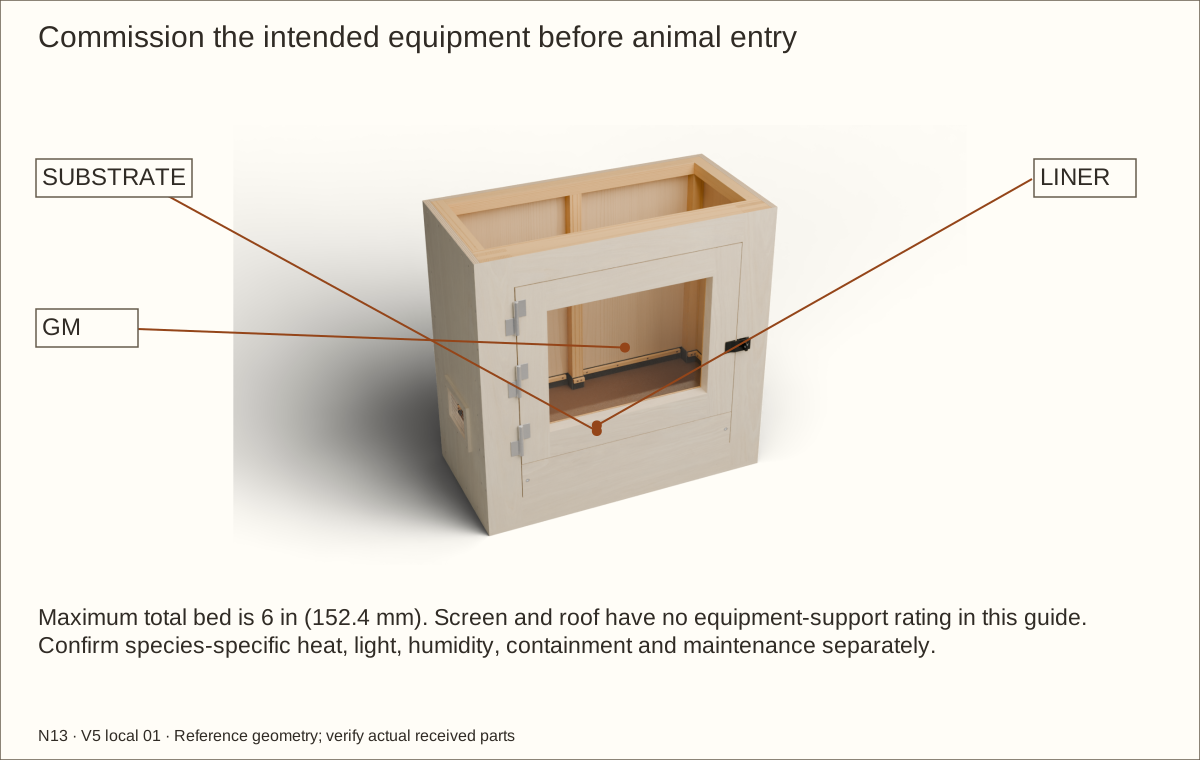
Choose heat, light, ultraviolet and control equipment for the actual habitat. An internally mounted fixture may be used when its manufacturer permits that installation and specifies its secure attachment, guard and clearances. A lamp placed above the mesh must have support qualified for that exact fixture; this guide does not rate the screen to carry it. Keep hot parts away from wood, acrylic, liner and animal contact. An exterior support stand is not required when a permitted internal installation is used.
Plan any cable route against the real connector and strain relief before cutting. Put it above the liner, finish the cut wood and fit a retained closure. Never trap a cord in the roof joint or pierce the wet basin for a cable or improvised drain.
Check before continuing: Any cable route is safely finished, mechanically secured and blocked against escape before use.
Parts: Complete enclosure, support and received inventory, as described below
Tools / setup: Measuring tape, square, pencil and the tools named below
Before you begin: No animal suitability or equipment support rating is assigned by this construction guide.
Commission before animal entry — 3
Run the complete configured habitat unoccupied through its intended day/night and wet/dry cycles. Record temperatures, humidity, ventilation, light exposure, thermostat control, safe surfaces, secure access and cleaning practicality before animal entry.
Check before continuing: Animal entry follows a separate documented species and equipment review, after construction is complete.
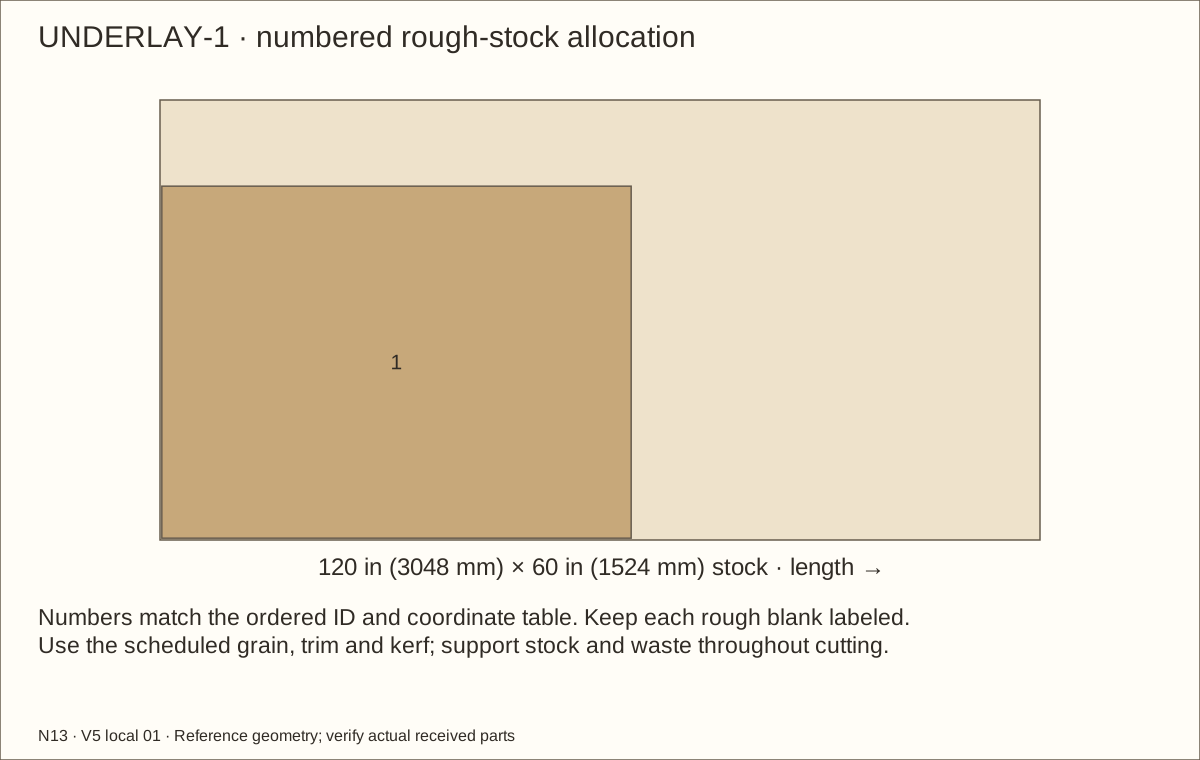
Choose ONE veneer species: two 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. Resolve receiving holds before dependent work. Product identity checks do not guarantee destination stock or physical fit.
Exact allocation in current cutting layouts, including one trial board. Plane supported broad stock before ripping; glazing spacer rough 3/8 in (9.53 mm), fit to actual 0.351 in (8.92 mm) reference bare depth.
Three full 1 1/2 in (38.1 mm) square × 96 in (2438.4 mm) boards; do not laminate these members.
Materials and hardware · continued
Choose ONE veneer species: two 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. Resolve receiving holds before dependent work. Product identity checks do not guarantee destination stock or physical fit.
One 19 in (482.6 mm) × 11 in (279.4 mm) roof blank and two 7 in (177.8 mm) × 5 in (127 mm) side blanks; two-wire reference crossing 0.082 in (2.08 mm), not a 0.025 in (0.64 mm) slab. Occupant-specific containment review remains required.
One 16-fluid-ounce (473 mL) bottle covers 13.6 sq ft (1.3 m²) of bond interfaces plus working reserve. The manufacturer excludes structural/load-bearing applications: use all scheduled mechanical stitches and do not infer a glue-only capacity.
Materials and hardware · continued
Choose ONE veneer species: two 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. Resolve receiving holds before dependent work. Product identity checks do not guarantee destination stock or physical fit.
Installed quantity is the exact source-station count; buy whole packs with spare screws.
Materials and hardware · continued
Choose ONE veneer species: two 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. Resolve receiving holds before dependent work. Product identity checks do not guarantee destination stock or physical fit.
801782 Needed 18; 100 per package; buy 1 package(s)
Eighteen installed, six per LSX-100R. Confirm received hole/head seating and supplier approval before use; do not machine proprietary hinge holes from the model.
Materials and hardware · continued
Choose ONE veneer species: two 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. Resolve receiving holds before dependent work. Product identity checks do not guarantee destination stock or physical fit.
LSX-100R Needed 3; 1 per package; buy 3 package(s)
Three on the guide’s left jamb: the manufacturer’s shown fixed pin half lies left of the axis and points upward. Sold individually, without screws. Confirm hand against the received parts, not the door name alone. The published 66 lb (30 kg) pair capacity does not rate this wood assembly or establish a multiplied three-hinge capacity.
N305-979 Needed 1; 1 per package; buy 1 package(s)
One independent closure per door. Turn the swivel across the slot to secure; align it with the slot to lift the flap. Optional padlocks are not included or required for the illustrated keyless operation.
Materials and hardware · continued
Choose ONE veneer species: two 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. Resolve receiving holds before dependent work. Product identity checks do not guarantee destination stock or physical fit.
21232102 Needed 1; 1 per package; buy 1 package(s)
One sheet supplies the 21 11/32 in (542.13 mm) × 16 23/32 in (424.66 mm) pane. Confirm full received width before cutting. Thickness is exactly 0.22 in (5.59 mm), not a nominal 1/4 in (6.35 mm) substituted without adjusting the pocket.
One 64 in (1625.6 mm) × 48 in (1219.2 mm) blank from 5 × 10-foot stock; reference compressed 0.08 in (2.03 mm) is not a measured material gauge. Add loose protection over recessed hardware.
Materials and hardware · continued
Choose ONE veneer species: two 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. Resolve receiving holds before dependent work. Product identity checks do not guarantee destination stock or physical fit.
One inside each recessed post under locknut. 5/8 in (15.88 mm) outside and 9/32 in (7.14 mm) inside diameters; receive thickness at most 1/16 in (1.59 mm) for this reference stack.
One inside each recessed post. Listed height 0.298 in (7.57 mm)–0.328 in (8.33 mm); two full threads beyond nylon, entire tail below post face. Hand-tighten to avoid stainless galling; never force seized threads.
Materials and hardware · continued
Choose ONE veneer species: two 48 × 96 in (1219.2 × 2438.4 mm) sheets. Trial stock is included. Resolve receiving holds before dependent work. Product identity checks do not guarantee destination stock or physical fit.
4 × 8 ft selected species / 3M PSA; configuration to confirm Needed 2; 1 per package; buy 2 package(s) Choose one species
Full exterior, edges/reveals and trial; supplier balance/backer/adhesive and cured-finish acceptance required
Cut list
Cut list
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
P01 · Floor
36 1/8 in (917.58 mm) × 18 1/16 in (458.79 mm) × 45/64 in (17.86 mm)
36 in (914.4 mm) × 18 in (457.2 mm) × 45/64 in (17.86 mm)
P02 · Removable roof
36 1/8 in (917.58 mm) × 18 1/16 in (458.79 mm) × 45/64 in (17.86 mm)
36 in (914.4 mm) × 18 in (457.2 mm) × 45/64 in (17.86 mm)
P03L · L wall
34 23/32 in (881.86 mm) × 18 1/16 in (458.79 mm) × 45/64 in (17.86 mm)
34 19/32 in (878.68 mm) × 18 in (457.2 mm) × 45/64 in (17.86 mm)
P03R · R wall
34 23/32 in (881.86 mm) × 18 1/16 in (458.79 mm) × 45/64 in (17.86 mm)
34 19/32 in (878.68 mm) × 18 in (457.2 mm) × 45/64 in (17.86 mm)
P04 · Back
34 23/32 in (881.86 mm) × 34 21/32 in (880.27 mm) × 45/64 in (17.86 mm)
34 19/32 in (878.68 mm) × 34 19/32 in (878.68 mm) × 45/64 in (17.86 mm)
CLB · L bottom cleat
14 27/64 in (366.32 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
14 19/64 in (363.14 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CLU · L rear upright
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31 19/32 in (802.48 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CLT · L upper cleat
14 27/64 in (366.32 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
14 19/64 in (363.14 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CRB · R bottom cleat
14 27/64 in (366.32 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
14 19/64 in (363.14 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CRU · R rear upright
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31 19/32 in (802.48 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
CRT · R upper cleat
14 27/64 in (366.32 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
14 19/64 in (363.14 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CB · Back floor cleat
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31 19/32 in (802.48 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CT · Back upper cleat
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31 19/32 in (802.48 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
CM1 · Intermediate rear upright
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
31 19/32 in (802.48 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
F0L · L full front-frame upright layer
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F0R · R full front-frame upright layer
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F0BM · Front-frame rail between uprights
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F0TM · Front-frame rail between uprights
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F1L · L full front-frame upright layer
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F1R · R full front-frame upright layer
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
F1B · Continuous front-frame rail layer
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F1T · Continuous front-frame rail layer
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F2L · L full front-frame upright layer
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F2R · R full front-frame upright layer
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F2BM · Front-frame rail between uprights
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F2TM · Front-frame rail between uprights
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F3L · L full front-frame upright layer
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F3R · R full front-frame upright layer
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F3B · Continuous front-frame rail layer
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
F3T · Continuous front-frame rail layer
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm) × 3/4 in (19.05 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
RBM1 · Removable retainer lamination
27 13/32 in (696.12 mm) × 4 11/16 in (119.06 mm) × 45/64 in (17.86 mm)
27 9/32 in (692.94 mm) × 4 5/8 in (117.48 mm) × 45/64 in (17.86 mm)
RBM2 · Removable retainer lamination
27 13/32 in (696.12 mm) × 4 11/16 in (119.06 mm) × 45/64 in (17.86 mm)
27 9/32 in (692.94 mm) × 4 5/8 in (117.48 mm) × 45/64 in (17.86 mm)
RBM3 · Removable retainer lamination
27 13/32 in (696.12 mm) × 4 11/16 in (119.06 mm) × 45/64 in (17.86 mm)
27 9/32 in (692.94 mm) × 4 5/8 in (117.48 mm) × 45/64 in (17.86 mm)
RCML · Retainer bolt receiver
4 3/4 in (120.65 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
4 5/8 in (117.48 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
RCMR · Retainer bolt receiver
4 3/4 in (120.65 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
4 5/8 in (117.48 mm) × 1 1/2 in (38.1 mm) × 1 1/2 in (38.1 mm)
ML · L vent mesh
7 in (177.8 mm) × 5 in (127 mm) × 0.082 in (2.08 mm)
7 in (177.8 mm) × 5 in (127 mm) × 0.082 in (2.08 mm)
VLB · Vent capture strip
8 1/8 in (206.38 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
8 in (203.2 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
VLT · Vent capture strip
8 1/8 in (206.38 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
8 in (203.2 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
VLF · Vent end strip
4 1/8 in (104.78 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
4 in (101.6 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
VLA · Vent end strip
4 1/8 in (104.78 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
4 in (101.6 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
MR · R vent mesh
7 in (177.8 mm) × 5 in (127 mm) × 0.082 in (2.08 mm)
7 in (177.8 mm) × 5 in (127 mm) × 0.082 in (2.08 mm)
VRB · Vent capture strip
8 1/8 in (206.38 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
8 in (203.2 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
VRT · Vent capture strip
8 1/8 in (206.38 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
8 in (203.2 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
VRF · Vent end strip
4 1/8 in (104.78 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
4 in (101.6 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
VRA · Vent end strip
4 1/8 in (104.78 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
4 in (101.6 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
MTC · Roof mesh
19 in (482.6 mm) × 11 in (279.4 mm) × 0.082 in (2.08 mm)
19 in (482.6 mm) × 11 in (279.4 mm) × 0.082 in (2.08 mm)
RTCF · Roof capture strip
20 1/8 in (511.18 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
20 in (508 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
RTCA · Roof capture strip
20 1/8 in (511.18 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
20 in (508 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
RTCL · Roof end capture
10 1/8 in (257.18 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
10 in (254 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
RTCR · Roof end capture
10 1/8 in (257.18 mm) × 1 1/16 in (26.99 mm) × 3/8 in (9.53 mm)
10 in (254 mm) × 1 in (25.4 mm) × 3/8 in (9.53 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
DM0L · Door stile layer
22 23/32 in (577.06 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
22 19/32 in (573.88 mm) × 3 7/16 in (87.31 mm) × 3/4 in (19.05 mm)
DM0R · Door stile layer
22 23/32 in (577.06 mm) × 3 17/32 in (89.69 mm) × 3/4 in (19.05 mm)
22 19/32 in (573.88 mm) × 3 15/32 in (88.11 mm) × 3/4 in (19.05 mm)
DM0B · Door rail layer
20 15/32 in (519.91 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
20 11/32 in (516.73 mm) × 3 7/16 in (87.31 mm) × 3/4 in (19.05 mm)
DM0T · Door rail layer
20 15/32 in (519.91 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
20 11/32 in (516.73 mm) × 3 7/16 in (87.31 mm) × 3/4 in (19.05 mm)
DM1L · Door stile layer
15 27/32 in (402.43 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
15 23/32 in (399.26 mm) × 3 7/16 in (87.31 mm) × 3/4 in (19.05 mm)
DM1R · Door stile layer
15 27/32 in (402.43 mm) × 3 17/32 in (89.69 mm) × 3/4 in (19.05 mm)
15 23/32 in (399.26 mm) × 3 15/32 in (88.11 mm) × 3/4 in (19.05 mm)
DM1B · Door rail layer
27 3/8 in (695.33 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
27 1/4 in (692.15 mm) × 3 7/16 in (87.31 mm) × 3/4 in (19.05 mm)
DM1T · Door rail layer
27 3/8 in (695.33 mm) × 3 1/2 in (88.9 mm) × 3/4 in (19.05 mm)
27 1/4 in (692.15 mm) × 3 7/16 in (87.31 mm) × 3/4 in (19.05 mm)
GM · Unpierced OPTIX acrylic pane
21 15/32 in (545.31 mm) × 16 25/32 in (426.24 mm) × 0.22 in (5.59 mm)
21 11/32 in (542.13 mm) × 16 23/32 in (424.66 mm) × 0.22 in (5.59 mm)
SPML · Glazing side spacer
18 19/32 in (472.28 mm) × 13/16 in (20.64 mm) × 3/8 in (9.53 mm)
18 15/32 in (469.11 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
SPMR · Glazing side spacer
18 19/32 in (472.28 mm) × 13/16 in (20.64 mm) × 3/8 in (9.53 mm)
18 15/32 in (469.11 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
SPMB · Glazing end spacer
21 23/32 in (551.66 mm) × 13/16 in (20.64 mm) × 3/8 in (9.53 mm)
21 19/32 in (548.48 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
SPMT · Glazing end spacer
21 23/32 in (551.66 mm) × 13/16 in (20.64 mm) × 3/8 in (9.53 mm)
21 19/32 in (548.48 mm) × 3/4 in (19.05 mm) × 0.351 in (8.92 mm)
BEML · Removable glazing side bead
18 19/32 in (472.28 mm) × 1 5/16 in (33.34 mm) × 1/4 in (6.35 mm)
18 15/32 in (469.11 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
BEMR · Removable glazing side bead
18 19/32 in (472.28 mm) × 1 5/16 in (33.34 mm) × 1/4 in (6.35 mm)
18 15/32 in (469.11 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
BEMB · Removable glazing end bead
20 23/32 in (526.26 mm) × 1 5/16 in (33.34 mm) × 1/4 in (6.35 mm)
20 19/32 in (523.08 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
BEMT · Removable glazing end bead
20 23/32 in (526.26 mm) × 1 5/16 in (33.34 mm) × 1/4 in (6.35 mm)
20 19/32 in (523.08 mm) × 1 1/4 in (31.75 mm) × 1/4 in (6.35 mm)
PADMLF · Dry glazing face pad
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
PADMLB · Dry glazing face pad
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
PADMRF · Dry glazing face pad
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
PADMRB · Dry glazing face pad
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
PADMBF · Dry glazing end pad
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
PADMBB · Dry glazing end pad
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
PADMTF · Dry glazing end pad
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
PADMTB · Dry glazing end pad
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm) × 1/16 in (1.59 mm)
LCL · Side liner clamp
11 51/64 in (299.64 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
11 43/64 in (296.47 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCR · Side liner clamp
11 51/64 in (299.64 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
11 43/64 in (296.47 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCFJ1 · Front liner clamp
3 1/4 in (82.55 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
3 1/8 in (79.38 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCFRML · Front liner clamp
1 3/8 in (34.93 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
1 1/4 in (31.75 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCFPM · Front liner clamp
24 15/32 in (621.51 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
24 11/32 in (618.33 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
LCFRMR · Front liner clamp
1 3/8 in (34.93 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
1 1/4 in (31.75 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCFJ2 · Front liner clamp
3 1/4 in (82.55 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
3 1/8 in (79.38 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCB1 · Back liner clamp
14.261875 in (362.25 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
14.136875 in (359.08 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCB2 · Back liner clamp
14.261875 in (362.25 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
14.136875 in (359.08 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCPL · Rear post liner clamp
1 1/2 in (38.1 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
1 3/8 in (34.93 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCP1 · Rear post liner clamp
1 5/8 in (41.28 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
1 1/2 in (38.1 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
LCPR · Rear post liner clamp
1 1/2 in (38.1 mm) × 9/16 in (14.29 mm) × 3/8 in (9.53 mm)
1 3/8 in (34.93 mm) × 1/2 in (12.7 mm) × 3/8 in (9.53 mm)
SETM0-layer-1 · Dry lower setting-pad layer 1
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
SETM0-layer-2 · Dry lower setting-pad layer 2
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
SETM1-layer-1 · Dry lower setting-pad layer 1
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
SETM1-layer-2 · Dry lower setting-pad layer 2
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm) × 1/16 in (1.59 mm)
V-floor-under · Veneer · floor-under
36.561 in (928.65 mm) × 18.561 in (471.45 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 18.061 in (458.75 mm) × 0.0305 in (0.77 mm)
V-roof-top · Veneer · roof-top
36.561 in (928.65 mm) × 18.561 in (471.45 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 18.061 in (458.75 mm) × 0.0305 in (0.77 mm)
V-P01-front · Veneer · P01-front
36.561 in (928.65 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P01-back · Veneer · P01-back
36.561 in (928.65 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P01-left · Veneer · P01-left
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
18 in (457.2 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P01-right · Veneer · P01-right
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
18 in (457.2 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P02-front · Veneer · P02-front
36.561 in (928.65 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P02-back · Veneer · P02-back
36.561 in (928.65 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
36.061 in (915.95 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P02-left · Veneer · P02-left
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
18 in (457.2 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
V-P02-right · Veneer · P02-right
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
18 in (457.2 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03L-face · Veneer · P03L-face
35 3/32 in (891.38 mm) × 18 1/2 in (469.9 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 18 in (457.2 mm) × 0.0305 in (0.77 mm)
V-P03L-front · Veneer · P03L-front
35 3/32 in (891.38 mm) × 1.233625 in (31.33 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 0.733625 in (18.63 mm) × 0.0305 in (0.77 mm)
V-P03L-back · Veneer · P03L-back
35 3/32 in (891.38 mm) × 1.233625 in (31.33 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 0.733625 in (18.63 mm) × 0.0305 in (0.77 mm)
V-P03L-vent-near · Veneer · P03L-vent-near
4.439 in (112.75 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03L-vent-far · Veneer · P03L-vent-far
4.439 in (112.75 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03L-vent-bottom · Veneer · P03L-vent-bottom
6 1/2 in (165.1 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03L-vent-top · Veneer · P03L-vent-top
6 1/2 in (165.1 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03R-face · Veneer · P03R-face
35 3/32 in (891.38 mm) × 18 1/2 in (469.9 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 18 in (457.2 mm) × 0.0305 in (0.77 mm)
V-P03R-front · Veneer · P03R-front
35 3/32 in (891.38 mm) × 1.233625 in (31.33 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 0.733625 in (18.63 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
V-P03R-back · Veneer · P03R-back
35 3/32 in (891.38 mm) × 1.233625 in (31.33 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 0.733625 in (18.63 mm) × 0.0305 in (0.77 mm)
V-P03R-vent-near · Veneer · P03R-vent-near
4.439 in (112.75 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03R-vent-far · Veneer · P03R-vent-far
4.439 in (112.75 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03R-vent-bottom · Veneer · P03R-vent-bottom
6 1/2 in (165.1 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-P03R-vent-top · Veneer · P03R-vent-top
6 1/2 in (165.1 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-back · Veneer · back
35 3/32 in (891.38 mm) × 35 3/32 in (891.38 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 34 19/32 in (878.68 mm) × 0.0305 in (0.77 mm)
V-roof-opening-left · Veneer · roof-opening-left
10.439 in (265.15 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
9.939 in (252.45 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
18 in (457.2 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
V-roof-opening-back · Veneer · roof-opening-back
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm) × 0.0305 in (0.77 mm)
18 in (457.2 mm) × 45/64 in (17.86 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
V-F0L-front · Veneer · F0L-front
35 3/32 in (891.38 mm) × 4 in (101.6 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 0.0305 in (0.77 mm)
V-F0R-front · Veneer · F0R-front
35 3/32 in (891.38 mm) × 4 in (101.6 mm) × 0.0305 in (0.77 mm)
34 19/32 in (878.68 mm) × 3 1/2 in (88.9 mm) × 0.0305 in (0.77 mm)
V-F0BM-front · Veneer · F0BM-front
28 3/32 in (713.58 mm) × 4 in (101.6 mm) × 0.0305 in (0.77 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 0.0305 in (0.77 mm)
V-F0TM-front · Veneer · F0TM-front
28 3/32 in (713.58 mm) × 4 in (101.6 mm) × 0.0305 in (0.77 mm)
27 19/32 in (700.88 mm) × 3 1/2 in (88.9 mm) × 0.0305 in (0.77 mm)
V-opening-left · Veneer · opening-left
28 3/32 in (713.58 mm) × 3 1/2 in (88.9 mm) × 0.0305 in (0.77 mm)
27 19/32 in (700.88 mm) × 3 in (76.2 mm) × 0.0305 in (0.77 mm)
V-opening-right · Veneer · opening-right
28 3/32 in (713.58 mm) × 3 1/2 in (88.9 mm) × 0.0305 in (0.77 mm)
27 19/32 in (700.88 mm) × 3 in (76.2 mm) × 0.0305 in (0.77 mm)
V-opening-head · Veneer · opening-head
28.03275 in (712.03 mm) × 3 1/2 in (88.9 mm) × 0.0305 in (0.77 mm)
27.53275 in (699.33 mm) × 3 in (76.2 mm) × 0.0305 in (0.77 mm)
V-RBM1-front · Veneer · RBM1-front
27.84225 in (707.19 mm) × 5.1555 in (130.95 mm) × 0.0305 in (0.77 mm)
27.34225 in (694.49 mm) × 4.6555 in (118.25 mm) × 0.0305 in (0.77 mm)
V-retainer-left · Veneer · retainer-left
5 1/8 in (130.18 mm) × 2 39/64 in (66.28 mm) × 0.0305 in (0.77 mm)
4 5/8 in (117.48 mm) × 2 7/64 in (53.58 mm) × 0.0305 in (0.77 mm)
V-retainer-right · Veneer · retainer-right
5 1/8 in (130.18 mm) × 2 39/64 in (66.28 mm) × 0.0305 in (0.77 mm)
4 5/8 in (117.48 mm) × 2 7/64 in (53.58 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
V-retainer-top · Veneer · retainer-top
27.84225 in (707.19 mm) × 2 39/64 in (66.28 mm) × 0.0305 in (0.77 mm)
27.34225 in (694.49 mm) × 2 7/64 in (53.58 mm) × 0.0305 in (0.77 mm)
V-kick-left · Veneer · kick-left
3 1/2 in (88.9 mm) × 0.59525 in (15.12 mm) × 0.0305 in (0.77 mm)
2 3/32 in (53.18 mm) × 0.09525 in (2.42 mm) × 0.0305 in (0.77 mm)
V-kick-right · Veneer · kick-right
3 1/2 in (88.9 mm) × 0.59525 in (15.12 mm) × 0.0305 in (0.77 mm)
2 3/32 in (53.18 mm) × 0.09525 in (2.42 mm) × 0.0305 in (0.77 mm)
V-DM0L-front · Veneer · DM0L-front
23.15475 in (588.13 mm) × 3.968 in (100.79 mm) × 0.0305 in (0.77 mm)
22.65475 in (575.43 mm) × 3.468 in (88.09 mm) × 0.0305 in (0.77 mm)
V-DM0R-front · Veneer · DM0R-front
23.15475 in (588.13 mm) × 3.99925 in (101.58 mm) × 0.0305 in (0.77 mm)
22.65475 in (575.43 mm) × 3.49925 in (88.88 mm) × 0.0305 in (0.77 mm)
V-DM0B-front · Veneer · DM0B-front
20 27/32 in (529.43 mm) × 3.968 in (100.79 mm) × 0.0305 in (0.77 mm)
20 11/32 in (516.73 mm) × 3.468 in (88.09 mm) × 0.0305 in (0.77 mm)
V-DM0T-front · Veneer · DM0T-front
20 27/32 in (529.43 mm) × 3.968 in (100.79 mm) × 0.0305 in (0.77 mm)
20 11/32 in (516.73 mm) × 3.468 in (88.09 mm) × 0.0305 in (0.77 mm)
V-door-left · Veneer · door-left
23 3/32 in (586.58 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
22 19/32 in (573.88 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-door-right · Veneer · door-right
23 3/32 in (586.58 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
22 19/32 in (573.88 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-door-bottom · Veneer · door-bottom
27.811 in (706.4 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
27.311 in (693.7 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
V-door-top · Veneer · door-top
27.811 in (706.4 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
27.311 in (693.7 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-view-left · Veneer · view-left
16.15775 in (410.41 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
15.65775 in (397.71 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-view-right · Veneer · view-right
16.15775 in (410.41 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
15.65775 in (397.71 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-view-bottom · Veneer · view-bottom
20 27/32 in (529.43 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
20 11/32 in (516.73 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-view-top · Veneer · view-top
20 27/32 in (529.43 mm) × 2 in (50.8 mm) × 0.0305 in (0.77 mm)
20 11/32 in (516.73 mm) × 1 1/2 in (38.1 mm) × 0.0305 in (0.77 mm)
V-VLB-outer · Veneer · VLB-outer
8.561 in (217.45 mm) × 1.561 in (39.65 mm) × 0.0305 in (0.77 mm)
8.061 in (204.75 mm) × 1.061 in (26.95 mm) × 0.0305 in (0.77 mm)
V-VLB-low · Veneer · VLB-low
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
8 in (203.2 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLB-high · Veneer · VLB-high
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLB-near · Veneer · VLB-near
1.561 in (39.65 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
1.061 in (26.95 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLB-far · Veneer · VLB-far
1.561 in (39.65 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
1.061 in (26.95 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
V-VLT-outer · Veneer · VLT-outer
8.561 in (217.45 mm) × 1.561 in (39.65 mm) × 0.0305 in (0.77 mm)
8.061 in (204.75 mm) × 1.061 in (26.95 mm) × 0.0305 in (0.77 mm)
V-VLT-low · Veneer · VLT-low
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLT-high · Veneer · VLT-high
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
8 in (203.2 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLT-near · Veneer · VLT-near
1.561 in (39.65 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
1.061 in (26.95 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLT-far · Veneer · VLT-far
1.561 in (39.65 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
1.061 in (26.95 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLF-outer · Veneer · VLF-outer
4.439 in (112.75 mm) × 1.561 in (39.65 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 1.061 in (26.95 mm) × 0.0305 in (0.77 mm)
V-VLF-near · Veneer · VLF-near
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLF-far · Veneer · VLF-far
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VLA-outer · Veneer · VLA-outer
4.439 in (112.75 mm) × 1.561 in (39.65 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 1.061 in (26.95 mm) × 0.0305 in (0.77 mm)
V-VLA-near · Veneer · VLA-near
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
V-VLA-far · Veneer · VLA-far
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRB-outer · Veneer · VRB-outer
8.561 in (217.45 mm) × 1.561 in (39.65 mm) × 0.0305 in (0.77 mm)
8.061 in (204.75 mm) × 1.061 in (26.95 mm) × 0.0305 in (0.77 mm)
V-VRB-low · Veneer · VRB-low
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
8 in (203.2 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRB-high · Veneer · VRB-high
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRB-near · Veneer · VRB-near
1.561 in (39.65 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
1.061 in (26.95 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRB-far · Veneer · VRB-far
1.561 in (39.65 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
1.061 in (26.95 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRT-outer · Veneer · VRT-outer
8.561 in (217.45 mm) × 1.561 in (39.65 mm) × 0.0305 in (0.77 mm)
8.061 in (204.75 mm) × 1.061 in (26.95 mm) × 0.0305 in (0.77 mm)
V-VRT-low · Veneer · VRT-low
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
6 in (152.4 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRT-high · Veneer · VRT-high
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
8 in (203.2 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRT-near · Veneer · VRT-near
1.561 in (39.65 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
1.061 in (26.95 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
Cut list · continued
One of each named ID. Rough blanks include scheduled trimming. Thickness is the prepared blank. Screen captures and liner clamps use 3/4-inch (19.05 mm) pine planed to 3/8 inch (9.53 mm) before ripping. Other parts use their listed prepared gauges; fit glazing spacers to the accepted installed stack. Reference finished sizes need actual-material fitting. V-parts represent the complete cured veneer stack. Cut the one acrylic pane only after the cured pocket, actual thickness and movement clearance are measured. SETM layer IDs are individual dry layers; two form each lower setting support.
Part
Rough length × width × prepared thickness
Reference finished size
V-VRT-far · Veneer · VRT-far
1.561 in (39.65 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
1.061 in (26.95 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRF-outer · Veneer · VRF-outer
4.439 in (112.75 mm) × 1.561 in (39.65 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 1.061 in (26.95 mm) × 0.0305 in (0.77 mm)
V-VRF-near · Veneer · VRF-near
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRF-far · Veneer · VRF-far
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRA-outer · Veneer · VRA-outer
4.439 in (112.75 mm) × 1.561 in (39.65 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 1.061 in (26.95 mm) × 0.0305 in (0.77 mm)
V-VRA-near · Veneer · VRA-near
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
V-VRA-far · Veneer · VRA-far
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm) × 0.0305 in (0.77 mm)
3.939 in (100.05 mm) × 3/8 in (9.53 mm) × 0.0305 in (0.77 mm)
LINER-BLANK · One-piece basin blank
64 in (1625.6 mm) × 48 in (1219.2 mm) × 0.045 in (1.14 mm)
64 in (1625.6 mm) × 48 in (1219.2 mm) × 0.045 in (1.14 mm)
UNDERLAY-BLANK · Protective underlay blank
64 in (1625.6 mm) × 48 in (1219.2 mm) × 0.08 in (2.03 mm)
64 in (1625.6 mm) × 48 in (1219.2 mm); measure actual compressed thickness
Workshop drawings and measurements
Lining clamp order and later service
Rear post clamps before side strips; front receiver clamps last
Installation order: LCPL, LCP1, LCPR, LCB1, LCB2, LCFJ1, LCFJ2, LCL, LCR, LCFRML, LCFPM, LCFRMR. Reverse this order for removal. Only the 36 scheduled clamp screws may pierce the dry band, from 7 1/8 in (180.98 mm) to 7 5/8 in (193.68 mm) above the central liner floor, centered at 7 3/8 in (187.33 mm). Pre-drill wood separately. Actual folded bulk and safe tools require the receiving trial. The long side strips otherwise block access to the rear post screws; the front receiver strips can block the side-strip driver route.
Observe the shallow test for 24 hours
One inch of water above the central lined floor on continuous qualified support
After accepted support and material trials, fill only to 1 in (25.4 mm) above the central liner floor. Mark the level, inspect the shell and accessible underside for 24 hours, then siphon or wet-vacuum out and dry. Investigate any dampness and repeat after repair. Never move a loaded or wet enclosure; this observation is not an aquarium or structural load approval.
PLY-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · P04
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 34 21/32 in (880.27 mm)
2 · P01
34 31/32 in (888.21 mm) / 1/8 in (3.18 mm)
36 1/8 in (917.58 mm) × 18 1/16 in (458.79 mm)
3 · P02
34 31/32 in (888.21 mm) / 18 5/16 in (465.14 mm)
36 1/8 in (917.58 mm) × 18 1/16 in (458.79 mm)
4 · RBM1
34 31/32 in (888.21 mm) / 36 1/2 in (927.1 mm)
27 13/32 in (696.12 mm) × 4 11/16 in (119.06 mm)
5 · RBM2
34 31/32 in (888.21 mm) / 41 5/16 in (1049.34 mm)
27 13/32 in (696.12 mm) × 4 11/16 in (119.06 mm)
6 · RBM3
1/8 in (3.18 mm) / 34 29/32 in (886.62 mm)
27 13/32 in (696.12 mm) × 4 11/16 in (119.06 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PLY-2 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · P03L
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 18 1/16 in (458.79 mm)
2 · P03R
1/8 in (3.18 mm) / 18 5/16 in (465.14 mm)
34 23/32 in (881.86 mm) × 18 1/16 in (458.79 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
SOLID-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · CLU
0 in (0 mm) / 0 in (0 mm)
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm)
2 · CRU
31 27/32 in (808.83 mm) / 0 in (0 mm)
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm)
3 · CB
63 11/16 in (1617.66 mm) / 0 in (0 mm)
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm).
SOLID-2 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · CT
0 in (0 mm) / 0 in (0 mm)
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm)
2 · CM1
31 27/32 in (808.83 mm) / 0 in (0 mm)
31 23/32 in (805.66 mm) × 1 1/2 in (38.1 mm)
3 · CLB
63 11/16 in (1617.66 mm) / 0 in (0 mm)
14 27/64 in (366.32 mm) × 1 1/2 in (38.1 mm)
4 · CLT
78 15/64 in (1987.15 mm) / 0 in (0 mm)
14 27/64 in (366.32 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm).
SOLID-3 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · CRB
0 in (0 mm) / 0 in (0 mm)
14 27/64 in (366.32 mm) × 1 1/2 in (38.1 mm)
2 · CRT
14 35/64 in (369.49 mm) / 0 in (0 mm)
14 27/64 in (366.32 mm) × 1 1/2 in (38.1 mm)
3 · RCML
29 3/32 in (738.98 mm) / 0 in (0 mm)
4 3/4 in (120.65 mm) × 1 1/2 in (38.1 mm)
4 · RCMR
33 31/32 in (862.81 mm) / 0 in (0 mm)
4 3/4 in (120.65 mm) × 1 1/2 in (38.1 mm)
Stock 96 in (2438.4 mm) × 1 1/2 in (38.1 mm); trim 0 in (0 mm); kerf/separation 1/8 in (3.18 mm).
MESH-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · MTC
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
19 in (482.6 mm) × 11 in (279.4 mm)
2 · ML
1/8 in (3.18 mm) / 11 1/4 in (285.75 mm)
7 in (177.8 mm) × 5 in (127 mm)
3 · MR
1/8 in (3.18 mm) / 16 3/8 in (415.93 mm)
7 in (177.8 mm) × 5 in (127 mm)
Stock 120 in (3048 mm) × 48 in (1219.2 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
ACRYLIC-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · GM
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
21 15/32 in (545.31 mm) × 16 25/32 in (426.24 mm)
Stock 48 in (1219.2 mm) × 24 in (609.6 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
VENEER-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · V-back
1/4 in (6.35 mm) / 1/4 in (6.35 mm)
35 3/32 in (891.38 mm) × 35 3/32 in (891.38 mm)
2 · V-floor-under
35 13/32 in (899.32 mm) / 1/4 in (6.35 mm)
36.561 in (928.65 mm) × 18.561 in (471.45 mm)
3 · V-roof-top
35 13/32 in (899.32 mm) / 18.8735 in (479.39 mm)
36.561 in (928.65 mm) × 18.561 in (471.45 mm)
4 · V-F0L-front
1/4 in (6.35 mm) / 35 13/32 in (899.32 mm)
35 3/32 in (891.38 mm) × 4 in (101.6 mm)
5 · V-F0R-front
1/4 in (6.35 mm) / 39 15/32 in (1002.51 mm)
35 3/32 in (891.38 mm) × 4 in (101.6 mm)
6 · V-F0BM-front
1/4 in (6.35 mm) / 43 17/32 in (1105.69 mm)
28 3/32 in (713.58 mm) × 4 in (101.6 mm)
7 · V-DM0R-front
72.02975 in (1829.56 mm) / 1/4 in (6.35 mm)
23.15475 in (588.13 mm) × 3.99925 in (101.58 mm)
8 · V-DM0L-front
72.02975 in (1829.56 mm) / 4.31175 in (109.52 mm)
23.15475 in (588.13 mm) × 3.968 in (100.79 mm)
9 · V-door-left
72.02975 in (1829.56 mm) / 8.34225 in (211.89 mm)
23 3/32 in (586.58 mm) × 2 in (50.8 mm)
10 · V-door-right
72.02975 in (1829.56 mm) / 10.40475 in (264.28 mm)
23 3/32 in (586.58 mm) × 2 in (50.8 mm)
11 · V-P01-front
35 13/32 in (899.32 mm) / 37.497 in (952.42 mm)
36.561 in (928.65 mm) × 1 13/64 in (30.56 mm)
12 · V-P01-back
35 13/32 in (899.32 mm) / 38.762625 in (984.57 mm)
36.561 in (928.65 mm) × 1 13/64 in (30.56 mm)
13 · V-P02-front
35 13/32 in (899.32 mm) / 40.02825 in (1016.72 mm)
36.561 in (928.65 mm) × 1 13/64 in (30.56 mm)
14 · V-P02-back
35 13/32 in (899.32 mm) / 41.293875 in (1048.86 mm)
36.561 in (928.65 mm) × 1 13/64 in (30.56 mm)
15 · V-P03L-front
35 13/32 in (899.32 mm) / 42.5595 in (1081.01 mm)
35 3/32 in (891.38 mm) × 1.233625 in (31.33 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/4 in (6.35 mm); kerf/separation 1/16 in (1.59 mm).
VENEER-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
16 · V-P03L-back
35 13/32 in (899.32 mm) / 43.855625 in (1113.93 mm)
35 3/32 in (891.38 mm) × 1.233625 in (31.33 mm)
17 · V-P03R-front
35 13/32 in (899.32 mm) / 45.15175 in (1146.85 mm)
35 3/32 in (891.38 mm) × 1.233625 in (31.33 mm)
18 · V-P03R-back
35 13/32 in (899.32 mm) / 46.447875 in (1179.78 mm)
35 3/32 in (891.38 mm) × 1.233625 in (31.33 mm)
19 · V-view-bottom
72.02975 in (1829.56 mm) / 12.46725 in (316.67 mm)
20 27/32 in (529.43 mm) × 2 in (50.8 mm)
20 · V-view-top
72.02975 in (1829.56 mm) / 14.52975 in (369.06 mm)
20 27/32 in (529.43 mm) × 2 in (50.8 mm)
21 · V-P01-left
72.02975 in (1829.56 mm) / 16.59225 in (421.44 mm)
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm)
22 · V-P01-right
72.02975 in (1829.56 mm) / 17.857875 in (453.59 mm)
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm)
23 · V-P02-left
72.02975 in (1829.56 mm) / 19.1235 in (485.74 mm)
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm)
24 · V-P02-right
72.02975 in (1829.56 mm) / 20.389125 in (517.88 mm)
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm)
25 · V-roof-opening-front
72.02975 in (1829.56 mm) / 21.65475 in (550.03 mm)
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm)
26 · V-roof-opening-back
72.02975 in (1829.56 mm) / 22.920375 in (582.18 mm)
18 1/2 in (469.9 mm) × 1 13/64 in (30.56 mm)
27 · V-retainer-left
28 13/32 in (721.52 mm) / 43 17/32 in (1105.69 mm)
5 1/8 in (130.18 mm) × 2 39/64 in (66.28 mm)
28 · V-roof-opening-left
72.02975 in (1829.56 mm) / 24.186 in (614.32 mm)
10.439 in (265.15 mm) × 1 13/64 in (30.56 mm)
29 · V-roof-opening-right
72.02975 in (1829.56 mm) / 25.451625 in (646.47 mm)
10.439 in (265.15 mm) × 1 13/64 in (30.56 mm)
30 · V-P03L-vent-bottom
82 17/32 in (2096.29 mm) / 24.186 in (614.32 mm)
6 1/2 in (165.1 mm) × 1 13/64 in (30.56 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/4 in (6.35 mm); kerf/separation 1/16 in (1.59 mm).
VENEER-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
31 · V-P03L-vent-top
82 17/32 in (2096.29 mm) / 25.451625 in (646.47 mm)
6 1/2 in (165.1 mm) × 1 13/64 in (30.56 mm)
32 · V-P03R-vent-bottom
82 17/32 in (2096.29 mm) / 26.71725 in (678.62 mm)
6 1/2 in (165.1 mm) × 1 13/64 in (30.56 mm)
33 · V-P03R-vent-top
82 17/32 in (2096.29 mm) / 27.982875 in (710.77 mm)
6 1/2 in (165.1 mm) × 1 13/64 in (30.56 mm)
34 · V-VLB-low
72.02975 in (1829.56 mm) / 26.71725 in (678.62 mm)
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm)
35 · V-VLB-high
72.02975 in (1829.56 mm) / 27.65475 in (702.43 mm)
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm)
36 · V-VLT-low
72.02975 in (1829.56 mm) / 28.59225 in (726.24 mm)
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm)
37 · V-VLT-high
72.02975 in (1829.56 mm) / 29.52975 in (750.06 mm)
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm)
38 · V-VRB-low
72.02975 in (1829.56 mm) / 30.46725 in (773.87 mm)
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm)
39 · V-VRB-high
72.02975 in (1829.56 mm) / 31.40475 in (797.68 mm)
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm)
40 · V-VRT-low
72.02975 in (1829.56 mm) / 32.34225 in (821.49 mm)
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm)
41 · V-VRT-high
72.02975 in (1829.56 mm) / 33.27975 in (845.31 mm)
8 1/2 in (215.9 mm) × 7/8 in (22.23 mm)
42 · V-VLF-outer
82 17/32 in (2096.29 mm) / 29.2485 in (742.91 mm)
4.439 in (112.75 mm) × 1.561 in (39.65 mm)
43 · V-VLA-outer
82 17/32 in (2096.29 mm) / 30.872 in (784.15 mm)
4.439 in (112.75 mm) × 1.561 in (39.65 mm)
44 · V-VRF-outer
82 17/32 in (2096.29 mm) / 32.4955 in (825.39 mm)
4.439 in (112.75 mm) × 1.561 in (39.65 mm)
45 · V-VRA-outer
82 17/32 in (2096.29 mm) / 34.119 in (866.62 mm)
4.439 in (112.75 mm) × 1.561 in (39.65 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/4 in (6.35 mm); kerf/separation 1/16 in (1.59 mm).
VENEER-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
46 · V-P03L-vent-near
82 17/32 in (2096.29 mm) / 35.7425 in (907.86 mm)
4.439 in (112.75 mm) × 1 13/64 in (30.56 mm)
47 · V-P03L-vent-far
82 17/32 in (2096.29 mm) / 37.008125 in (940.01 mm)
4.439 in (112.75 mm) × 1 13/64 in (30.56 mm)
48 · V-P03R-vent-near
82 17/32 in (2096.29 mm) / 38.27375 in (972.15 mm)
4.439 in (112.75 mm) × 1 13/64 in (30.56 mm)
49 · V-P03R-vent-far
82 17/32 in (2096.29 mm) / 39.539375 in (1004.3 mm)
4.439 in (112.75 mm) × 1 13/64 in (30.56 mm)
50 · V-VLF-near
28 13/32 in (721.52 mm) / 46 13/64 in (1173.56 mm)
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm)
51 · V-VLF-far
72.02975 in (1829.56 mm) / 34.21725 in (869.12 mm)
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm)
52 · V-VLA-near
72.02975 in (1829.56 mm) / 35.15475 in (892.93 mm)
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm)
53 · V-VLA-far
72.02975 in (1829.56 mm) / 36.09225 in (916.74 mm)
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm)
54 · V-VRF-near
72.02975 in (1829.56 mm) / 37.02975 in (940.56 mm)
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm)
55 · V-VRF-far
72.02975 in (1829.56 mm) / 37.96725 in (964.37 mm)
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm)
56 · V-VRA-near
72.02975 in (1829.56 mm) / 38.90475 in (988.18 mm)
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm)
57 · V-VRA-far
72.02975 in (1829.56 mm) / 39.84225 in (1011.99 mm)
4 1/2 in (114.3 mm) × 7/8 in (22.23 mm)
58 · V-kick-left
28 13/32 in (721.52 mm) / 47 9/64 in (1197.37 mm)
3 1/2 in (88.9 mm) × 0.59525 in (15.12 mm)
59 · V-kick-right
76.59225 in (1945.44 mm) / 34.21725 in (869.12 mm)
3 1/2 in (88.9 mm) × 0.59525 in (15.12 mm)
60 · V-VLB-near
33 19/32 in (853.28 mm) / 43 17/32 in (1105.69 mm)
1.561 in (39.65 mm) × 7/8 in (22.23 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/4 in (6.35 mm); kerf/separation 1/16 in (1.59 mm).
VENEER-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
61 · V-VLB-far
33 19/32 in (853.28 mm) / 44 15/32 in (1129.51 mm)
1.561 in (39.65 mm) × 7/8 in (22.23 mm)
62 · V-VLT-near
33 19/32 in (853.28 mm) / 45 13/32 in (1153.32 mm)
1.561 in (39.65 mm) × 7/8 in (22.23 mm)
63 · V-VLT-far
33 19/32 in (853.28 mm) / 46 11/32 in (1177.13 mm)
1.561 in (39.65 mm) × 7/8 in (22.23 mm)
64 · V-VRB-near
80.59225 in (2047.04 mm) / 26.71725 in (678.62 mm)
1.561 in (39.65 mm) × 7/8 in (22.23 mm)
65 · V-VRB-far
80.59225 in (2047.04 mm) / 27.65475 in (702.43 mm)
1.561 in (39.65 mm) × 7/8 in (22.23 mm)
66 · V-VRT-near
80.59225 in (2047.04 mm) / 28.59225 in (726.24 mm)
1.561 in (39.65 mm) × 7/8 in (22.23 mm)
67 · V-VRT-far
80.59225 in (2047.04 mm) / 29.52975 in (750.06 mm)
1.561 in (39.65 mm) × 7/8 in (22.23 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/4 in (6.35 mm); kerf/separation 1/16 in (1.59 mm).
VENEER-2 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · V-P03L-face
1/4 in (6.35 mm) / 1/4 in (6.35 mm)
35 3/32 in (891.38 mm) × 18 1/2 in (469.9 mm)
2 · V-P03R-face
1/4 in (6.35 mm) / 18 13/16 in (477.84 mm)
35 3/32 in (891.38 mm) × 18 1/2 in (469.9 mm)
3 · TRIAL-veneer
35 13/32 in (899.32 mm) / 1/4 in (6.35 mm)
24 in (609.6 mm) × 12 in (304.8 mm)
4 · V-RBM1-front
1/4 in (6.35 mm) / 37 3/8 in (949.33 mm)
27.84225 in (707.19 mm) × 5.1555 in (130.95 mm)
5 · V-F0TM-front
59 15/32 in (1510.51 mm) / 1/4 in (6.35 mm)
28 3/32 in (713.58 mm) × 4 in (101.6 mm)
6 · V-DM0B-front
1/4 in (6.35 mm) / 42.593 in (1081.86 mm)
20 27/32 in (529.43 mm) × 3.968 in (100.79 mm)
7 · V-DM0T-front
35 13/32 in (899.32 mm) / 12 5/16 in (312.74 mm)
20 27/32 in (529.43 mm) × 3.968 in (100.79 mm)
8 · V-opening-left
59 15/32 in (1510.51 mm) / 4 5/16 in (109.54 mm)
28 3/32 in (713.58 mm) × 3 1/2 in (88.9 mm)
9 · V-opening-right
59 15/32 in (1510.51 mm) / 7 7/8 in (200.03 mm)
28 3/32 in (713.58 mm) × 3 1/2 in (88.9 mm)
10 · V-opening-head
59 15/32 in (1510.51 mm) / 11 7/16 in (290.51 mm)
28.03275 in (712.03 mm) × 3 1/2 in (88.9 mm)
11 · V-retainer-top
59 15/32 in (1510.51 mm) / 15 in (381 mm)
27.84225 in (707.19 mm) × 2 39/64 in (66.28 mm)
12 · V-retainer-right
21 5/32 in (537.37 mm) / 42.593 in (1081.86 mm)
5 1/8 in (130.18 mm) × 2 39/64 in (66.28 mm)
13 · V-door-bottom
59 15/32 in (1510.51 mm) / 17 43/64 in (448.87 mm)
27.811 in (706.4 mm) × 2 in (50.8 mm)
14 · V-door-top
59 15/32 in (1510.51 mm) / 19 47/64 in (501.25 mm)
27.811 in (706.4 mm) × 2 in (50.8 mm)
15 · V-view-left
35 13/32 in (899.32 mm) / 16.343 in (415.11 mm)
16.15775 in (410.41 mm) × 2 in (50.8 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/4 in (6.35 mm); kerf/separation 1/16 in (1.59 mm).
VENEER-2 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
16 · V-view-right
35 13/32 in (899.32 mm) / 18.4055 in (467.5 mm)
16.15775 in (410.41 mm) × 2 in (50.8 mm)
17 · V-VLB-outer
35 13/32 in (899.32 mm) / 20.468 in (519.89 mm)
8.561 in (217.45 mm) × 1.561 in (39.65 mm)
18 · V-VLT-outer
35 13/32 in (899.32 mm) / 22.0915 in (561.12 mm)
8.561 in (217.45 mm) × 1.561 in (39.65 mm)
19 · V-VRB-outer
35 13/32 in (899.32 mm) / 23.715 in (602.36 mm)
8.561 in (217.45 mm) × 1.561 in (39.65 mm)
20 · V-VRT-outer
35 13/32 in (899.32 mm) / 25.3385 in (643.6 mm)
8.561 in (217.45 mm) × 1.561 in (39.65 mm)
Stock 96 in (2438.4 mm) × 48 in (1219.2 mm); trim 1/4 in (6.35 mm); kerf/separation 1/16 in (1.59 mm).
PAD-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · PADMBF
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm)
2 · PADMBB
1/8 in (3.18 mm) / 9/16 in (14.29 mm)
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm)
3 · PADMTF
1/8 in (3.18 mm) / 1 in (25.4 mm)
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm)
4 · PADMTB
1/8 in (3.18 mm) / 1 7/16 in (36.51 mm)
20 19/32 in (523.08 mm) × 3/8 in (9.53 mm)
5 · PADMLF
1/8 in (3.18 mm) / 1 7/8 in (47.63 mm)
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm)
6 · PADMLB
1/8 in (3.18 mm) / 2 5/16 in (58.74 mm)
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm)
7 · PADMRF
1/8 in (3.18 mm) / 2 3/4 in (69.85 mm)
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm)
8 · PADMRB
1/8 in (3.18 mm) / 3 3/16 in (80.96 mm)
16 23/32 in (424.66 mm) × 3/8 in (9.53 mm)
9 · SETM0-layer-1
16 29/32 in (429.42 mm) / 1 7/8 in (47.63 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
10 · SETM0-layer-2
16 29/32 in (429.42 mm) / 2.1575 in (54.8 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
11 · SETM1-layer-1
16 29/32 in (429.42 mm) / 2.44 in (61.98 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
12 · SETM1-layer-2
16 29/32 in (429.42 mm) / 2.7225 in (69.15 mm)
1 in (25.4 mm) × 0.22 in (5.59 mm)
Stock 36 in (914.4 mm) × 12 in (304.8 mm); trim 1/8 in (3.18 mm); kerf/separation 1/16 in (1.59 mm).
PINE-FRAME-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · F0L
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm)
2 · F0R
34 31/32 in (888.21 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm)
3 · DM0R
69 13/16 in (1773.24 mm) / 1/8 in (3.18 mm)
22 23/32 in (577.06 mm) × 3 17/32 in (89.69 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-FRAME-2 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · F1B
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm)
2 · F1T
34 31/32 in (888.21 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm)
3 · DM0L
69 13/16 in (1773.24 mm) / 1/8 in (3.18 mm)
22 23/32 in (577.06 mm) × 3 1/2 in (88.9 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-FRAME-3 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · F2L
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm)
2 · F2R
34 31/32 in (888.21 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm)
3 · DM0B
69 13/16 in (1773.24 mm) / 1/8 in (3.18 mm)
20 15/32 in (519.91 mm) × 3 1/2 in (88.9 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-FRAME-4 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · F3B
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm)
2 · F3T
34 31/32 in (888.21 mm) / 1/8 in (3.18 mm)
34 23/32 in (881.86 mm) × 3 9/16 in (90.49 mm)
3 · DM0T
69 13/16 in (1773.24 mm) / 1/8 in (3.18 mm)
20 15/32 in (519.91 mm) × 3 1/2 in (88.9 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-FRAME-5 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · F0BM
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm)
2 · F0TM
27 31/32 in (710.41 mm) / 1/8 in (3.18 mm)
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm)
3 · F1L
55 13/16 in (1417.64 mm) / 1/8 in (3.18 mm)
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-FRAME-6 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · F1R
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm)
2 · F2BM
27 31/32 in (710.41 mm) / 1/8 in (3.18 mm)
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm)
3 · F2TM
55 13/16 in (1417.64 mm) / 1/8 in (3.18 mm)
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-FRAME-7 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · F3L
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm)
2 · F3R
27 31/32 in (710.41 mm) / 1/8 in (3.18 mm)
27 23/32 in (704.06 mm) × 3 9/16 in (90.49 mm)
3 · DM1B
55 13/16 in (1417.64 mm) / 1/8 in (3.18 mm)
27 3/8 in (695.33 mm) × 3 1/2 in (88.9 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-FRAME-8 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · DM1R
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
15 27/32 in (402.43 mm) × 3 17/32 in (89.69 mm)
2 · DM1T
16 3/32 in (408.78 mm) / 1/8 in (3.18 mm)
27 3/8 in (695.33 mm) × 3 1/2 in (88.9 mm)
3 · DM1L
43 19/32 in (1107.28 mm) / 1/8 in (3.18 mm)
15 27/32 in (402.43 mm) × 3 1/2 in (88.9 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-THIN-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · RTCF
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
20 1/8 in (511.18 mm) × 1 1/16 in (26.99 mm)
2 · RTCA
1/8 in (3.18 mm) / 1 5/16 in (33.34 mm)
20 1/8 in (511.18 mm) × 1 1/16 in (26.99 mm)
3 · RTCL
1/8 in (3.18 mm) / 2 1/2 in (63.5 mm)
10 1/8 in (257.18 mm) × 1 1/16 in (26.99 mm)
4 · RTCR
1/8 in (3.18 mm) / 3 11/16 in (93.66 mm)
10 1/8 in (257.18 mm) × 1 1/16 in (26.99 mm)
5 · VLB
10 3/8 in (263.53 mm) / 2 1/2 in (63.5 mm)
8 1/8 in (206.38 mm) × 1 1/16 in (26.99 mm)
6 · VLT
10 3/8 in (263.53 mm) / 3 11/16 in (93.66 mm)
8 1/8 in (206.38 mm) × 1 1/16 in (26.99 mm)
7 · VRB
20 3/8 in (517.53 mm) / 1/8 in (3.18 mm)
8 1/8 in (206.38 mm) × 1 1/16 in (26.99 mm)
8 · VRT
20 3/8 in (517.53 mm) / 1 5/16 in (33.34 mm)
8 1/8 in (206.38 mm) × 1 1/16 in (26.99 mm)
9 · VLF
20 3/8 in (517.53 mm) / 2 1/2 in (63.5 mm)
4 1/8 in (104.78 mm) × 1 1/16 in (26.99 mm)
10 · VLA
20 3/8 in (517.53 mm) / 3 11/16 in (93.66 mm)
4 1/8 in (104.78 mm) × 1 1/16 in (26.99 mm)
11 · VRF
28 5/8 in (727.08 mm) / 1/8 in (3.18 mm)
4 1/8 in (104.78 mm) × 1 1/16 in (26.99 mm)
12 · VRA
28 5/8 in (727.08 mm) / 1 5/16 in (33.34 mm)
4 1/8 in (104.78 mm) × 1 1/16 in (26.99 mm)
13 · SPMB
32 7/8 in (835.03 mm) / 1/8 in (3.18 mm)
21 23/32 in (551.66 mm) × 13/16 in (20.64 mm)
14 · SPMT
32 7/8 in (835.03 mm) / 1 1/16 in (26.99 mm)
21 23/32 in (551.66 mm) × 13/16 in (20.64 mm)
15 · SPML
32 7/8 in (835.03 mm) / 2 in (50.8 mm)
18 19/32 in (472.28 mm) × 13/16 in (20.64 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-THIN-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
16 · SPMR
32 7/8 in (835.03 mm) / 2 15/16 in (74.61 mm)
18 19/32 in (472.28 mm) × 13/16 in (20.64 mm)
17 · LCFPM
54 23/32 in (1389.86 mm) / 1/8 in (3.18 mm)
24 15/32 in (621.51 mm) × 9/16 in (14.29 mm)
18 · LCB2
32 7/8 in (835.03 mm) / 3 7/8 in (98.43 mm)
14.261875 in (362.25 mm) × 9/16 in (14.29 mm)
19 · LCB1
32 7/8 in (835.03 mm) / 4 9/16 in (115.89 mm)
14.261875 in (362.25 mm) × 9/16 in (14.29 mm)
20 · LCL
54 23/32 in (1389.86 mm) / 13/16 in (20.64 mm)
11 51/64 in (299.64 mm) × 9/16 in (14.29 mm)
21 · LCR
54 23/32 in (1389.86 mm) / 1 1/2 in (38.1 mm)
11 51/64 in (299.64 mm) × 9/16 in (14.29 mm)
22 · LCFJ1
24 5/8 in (625.48 mm) / 2 1/2 in (63.5 mm)
3 1/4 in (82.55 mm) × 9/16 in (14.29 mm)
23 · LCFJ2
24 5/8 in (625.48 mm) / 3 3/16 in (80.96 mm)
3 1/4 in (82.55 mm) × 9/16 in (14.29 mm)
24 · LCP1
18 5/8 in (473.08 mm) / 2 1/2 in (63.5 mm)
1 5/8 in (41.28 mm) × 9/16 in (14.29 mm)
25 · LCPL
18 5/8 in (473.08 mm) / 3 3/16 in (80.96 mm)
1 1/2 in (38.1 mm) × 9/16 in (14.29 mm)
26 · LCPR
18 5/8 in (473.08 mm) / 3 7/8 in (98.43 mm)
1 1/2 in (38.1 mm) × 9/16 in (14.29 mm)
27 · LCFRML
18 5/8 in (473.08 mm) / 4 9/16 in (115.89 mm)
1 3/8 in (34.93 mm) × 9/16 in (14.29 mm)
28 · LCFRMR
47.261875 in (1200.45 mm) / 3 7/8 in (98.43 mm)
1 3/8 in (34.93 mm) × 9/16 in (14.29 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
PINE-BEAD-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · BEMB
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
20 23/32 in (526.26 mm) × 1 5/16 in (33.34 mm)
2 · BEMT
1/8 in (3.18 mm) / 1 9/16 in (39.69 mm)
20 23/32 in (526.26 mm) × 1 5/16 in (33.34 mm)
3 · BEML
1/8 in (3.18 mm) / 3 in (76.2 mm)
18 19/32 in (472.28 mm) × 1 5/16 in (33.34 mm)
4 · BEMR
20 31/32 in (532.61 mm) / 1/8 in (3.18 mm)
18 19/32 in (472.28 mm) × 1 5/16 in (33.34 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
LINER-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · LINER-BLANK
1/4 in (6.35 mm) / 1/4 in (6.35 mm)
64 in (1625.6 mm) × 48 in (1219.2 mm)
Stock 120 in (3048 mm) × 96 in (2438.4 mm); trim 1/4 in (6.35 mm); kerf/separation 0 in (0 mm).
UNDERLAY-1 · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · UNDERLAY-BLANK
1/4 in (6.35 mm) / 1/4 in (6.35 mm)
64 in (1625.6 mm) × 48 in (1219.2 mm)
Stock 120 in (3048 mm) × 60 in (1524 mm); trim 1/4 in (6.35 mm); kerf/separation 0 in (0 mm).
PINE-TRIAL · exact rough positions
Stock X runs along its length and Y across its width from the lower-left corner. These are stock coordinates, separate from assembly stations. Length follows the allocated grain.
Number / part
Stock X / Y
Rough length × width
1 · TRIAL-hinge
1/8 in (3.18 mm) / 1/8 in (3.18 mm)
24 in (609.6 mm) × 5 1/4 in (133.35 mm)
2 · TRIAL-glazing
24 1/4 in (615.95 mm) / 1/8 in (3.18 mm)
24 in (609.6 mm) × 5 1/4 in (133.35 mm)
3 · TRIAL-capture
48 3/8 in (1228.73 mm) / 1/8 in (3.18 mm)
24 in (609.6 mm) × 5 1/4 in (133.35 mm)
Stock 96 in (2438.4 mm) × 5 1/2 in (139.7 mm); trim 1/8 in (3.18 mm); kerf/separation 1/8 in (3.18 mm).
Use exact fastener stations and the assembly order
Assembly X / Y / Z start at outside LEFT / outside FRONT / FLOOR UNDERSIDE. Direction gives the driving axis. IDs are stable labels; numbers inside an ID are not a substitute for coordinates. Transfer through actual clamped mating parts and use depth stops including the drill point.
Build the glued floor and laminated front on the bench. Complete all bore, pocket, hinge and hasp trials before coating. Fit rear post strips, back strips and front-jamb strips first; LCL/LCR next; LCFRML/LCFPM/LCFRMR last. Reverse for access during removal. Use the actual safe driver and folded-material trial.
BTML1 and BTMR1 connect the three-layer retainer to RCML and RCMR
Connection / post
Centre X / Z from assembly datums
Reference stack
BTML1 / RCML
4 61/64 in (125.81 mm) / 6 33/64 in (165.5 mm)
3 1/2 in (88.9 mm) screw; 1 in (25.4 mm) rear recess diameter; 5/8 in (15.88 mm) deep
BTMR1 / RCMR
31 3/64 in (788.59 mm) / 6 33/64 in (165.5 mm)
3 1/2 in (88.9 mm) screw; 1 in (25.4 mm) rear recess diameter; 5/8 in (15.88 mm) deep
Drive from outside toward the rear. Fit the nut and washer from inside before lining. The 82-degree head seats in wood, below a separate veneer access opening. Do not fill over the service opening. The rear nut and tip remain recessed and protected by loose underlay beneath the unpunctured liner. Empty and remove the lining before later connection service.
Trial the complete retainer hardware stack
Reference screw, countersink, through bore, rear recess, washer and nylon locknut
The two 1/4-20 × 3 1/2-inch (6.35 mm nominal × 88.9 mm) machine screws are separate from the wood-screw station table. Receive Bolt Depot 24910, 16019 and 16008, measure the actual parts and prove the joint in matching offcuts. Keep at least two full threads beyond the nylon, at least 1/16 inch (1.5875 mm) clearance below the rear post face and 7/8 inch (22.225 mm) reference wood bearing thickness. Do not deepen the recess to make an incompatible part fit.
Fastener stations · 1–12
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-RCML-0 · W300
RCML → F3L
5.703125 / 2.509375 / 5.078125 in 144.86 / 63.74 / 128.98 mm
−X · 3 in (76.2 mm)
S-RCML-1 · W300
RCML → F3L
5.703125 / 2.509375 / 7.328125 in 144.86 / 63.74 / 186.13 mm
−X · 3 in (76.2 mm)
S-RCMR-0 · W300
RCMR → F3R
30.296875 / 2.509375 / 5.078125 in 769.54 / 63.74 / 128.98 mm
+X · 3 in (76.2 mm)
S-RCMR-1 · W300
RCMR → F3R
30.296875 / 2.509375 / 7.328125 in 769.54 / 63.74 / 186.13 mm
+X · 3 in (76.2 mm)
S-HM1F-0 · HINGE
HM1F + F0L → F1L
3.517594 / -0.128925 / 10.878322 in 89.35 / -3.27 / 276.31 mm
+Y · 1 1/4 in (31.75 mm)
S-HM1F-1 · HINGE
HM1F + F0L → F1L
3.517594 / -0.128925 / 11.468873 in 89.35 / -3.27 / 291.31 mm
+Y · 1 1/4 in (31.75 mm)
S-HM1F-2 · HINGE
HM1F + F0L → F1L
3.517594 / -0.128925 / 12.059424 in 89.35 / -3.27 / 306.31 mm
+Y · 1 1/4 in (31.75 mm)
S-HM1M-0 · HINGE
HM1M + DM0L → DM1L
5.013656 / -0.128925 / 12.846826 in 127.35 / -3.27 / 326.31 mm
+Y · 1 1/4 in (31.75 mm)
S-HM1M-1 · HINGE
HM1M + DM0L → DM1L
5.013656 / -0.128925 / 13.437377 in 127.35 / -3.27 / 341.31 mm
+Y · 1 1/4 in (31.75 mm)
S-HM1M-2 · HINGE
HM1M + DM0L → DM1L
5.013656 / -0.128925 / 14.027928 in 127.35 / -3.27 / 356.31 mm
+Y · 1 1/4 in (31.75 mm)
S-HM2F-0 · HINGE
HM2F + F0L → F1L
3.517594 / -0.128925 / 18.737697 in 89.35 / -3.27 / 475.94 mm
+Y · 1 1/4 in (31.75 mm)
S-HM2F-1 · HINGE
HM2F + F0L → F1L
3.517594 / -0.128925 / 19.328248 in 89.35 / -3.27 / 490.94 mm
+Y · 1 1/4 in (31.75 mm)
Fastener stations · 13–24
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-HM2F-2 · HINGE
HM2F + F0L → F1L
3.517594 / -0.128925 / 19.918799 in 89.35 / -3.27 / 505.94 mm
+Y · 1 1/4 in (31.75 mm)
S-HM2M-0 · HINGE
HM2M + DM0L → DM1L
5.013656 / -0.128925 / 20.706201 in 127.35 / -3.27 / 525.94 mm
+Y · 1 1/4 in (31.75 mm)
S-HM2M-1 · HINGE
HM2M + DM0L → DM1L
5.013656 / -0.128925 / 21.296752 in 127.35 / -3.27 / 540.94 mm
+Y · 1 1/4 in (31.75 mm)
S-HM2M-2 · HINGE
HM2M + DM0L → DM1L
5.013656 / -0.128925 / 21.887303 in 127.35 / -3.27 / 555.94 mm
+Y · 1 1/4 in (31.75 mm)
S-HM3F-0 · HINGE
HM3F + F0L → F1L
3.517594 / -0.128925 / 26.597072 in 89.35 / -3.27 / 675.57 mm
+Y · 1 1/4 in (31.75 mm)
S-HM3F-1 · HINGE
HM3F + F0L → F1L
3.517594 / -0.128925 / 27.187623 in 89.35 / -3.27 / 690.57 mm
+Y · 1 1/4 in (31.75 mm)
S-HM3F-2 · HINGE
HM3F + F0L → F1L
3.517594 / -0.128925 / 27.778174 in 89.35 / -3.27 / 705.57 mm
+Y · 1 1/4 in (31.75 mm)
S-HM3M-0 · HINGE
HM3M + DM0L → DM1T
5.013656 / -0.128925 / 28.565576 in 127.35 / -3.27 / 725.57 mm
+Y · 1 1/4 in (31.75 mm)
S-HM3M-1 · HINGE
HM3M + DM0L → DM1T
5.013656 / -0.128925 / 29.156127 in 127.35 / -3.27 / 740.57 mm
+Y · 1 1/4 in (31.75 mm)
S-HM3M-2 · HINGE
HM3M + DM0L → DM1T
5.013656 / -0.128925 / 29.746678 in 127.35 / -3.27 / 755.57 mm
+Y · 1 1/4 in (31.75 mm)
S-LAM1L-0 · W125
F1B → F0L
2.453125 / 1.5 / 3.503125 in 62.31 / 38.10 / 88.98 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1L-1 · W125
F1L → F0L
2.453125 / 1.5 / 8.435417 in 62.31 / 38.10 / 214.26 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 25–36
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LAM1L-2 · W125
F1L → F0L
2.453125 / 1.5 / 13.367708 in 62.31 / 38.10 / 339.54 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1L-3 · W125
F1L → F0L
2.453125 / 1.5 / 18.3 in 62.31 / 38.10 / 464.82 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1L-4 · W125
F1L → F0L
2.453125 / 1.5 / 23.232292 in 62.31 / 38.10 / 590.10 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1L-5 · W125
F1L → F0L
2.453125 / 1.5 / 28.164583 in 62.31 / 38.10 / 715.38 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1L-6 · W125
F1T → F0L
2.453125 / 1.5 / 33.096875 in 62.31 / 38.10 / 840.66 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1R-0 · W125
F1B → F0R
33.546875 / 1.5 / 3.503125 in 852.09 / 38.10 / 88.98 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1R-1 · W125
F1R → F0R
33.546875 / 1.5 / 8.435417 in 852.09 / 38.10 / 214.26 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1R-2 · W125
F1R → F0R
33.546875 / 1.5 / 13.367708 in 852.09 / 38.10 / 339.54 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1R-3 · W125
F1R → F0R
33.546875 / 1.5 / 18.3 in 852.09 / 38.10 / 464.82 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1R-4 · W125
F1R → F0R
33.546875 / 1.5 / 23.232292 in 852.09 / 38.10 / 590.10 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1R-5 · W125
F1R → F0R
33.546875 / 1.5 / 28.164583 in 852.09 / 38.10 / 715.38 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1R-6 · W125
F1T → F0R
33.546875 / 1.5 / 33.096875 in 852.09 / 38.10 / 840.66 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 37–48
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LAM1BM-0 · W125
F1B → F0BM
5.503125 / 1.5 / 2.453125 in 139.78 / 38.10 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1BM-1 · W125
F1B → F0BM
10.421875 / 1.5 / 2.453125 in 264.72 / 38.10 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1BM-2 · W125
F1B → F0BM
15.340625 / 1.5 / 2.453125 in 389.65 / 38.10 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1BM-3 · W125
F1B → F0BM
20.259375 / 1.5 / 2.453125 in 514.59 / 38.10 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1BM-4 · W125
F1B → F0BM
25.178125 / 1.5 / 2.453125 in 639.52 / 38.10 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1BM-5 · W125
F1B → F0BM
30.096875 / 1.5 / 2.453125 in 764.46 / 38.10 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1TM-0 · W125
F1T → F0TM
5.503125 / 1.5 / 33.546875 in 139.78 / 38.10 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1TM-1 · W125
F1T → F0TM
10.421875 / 1.5 / 33.546875 in 264.72 / 38.10 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1TM-2 · W125
F1T → F0TM
15.340625 / 1.5 / 33.546875 in 389.65 / 38.10 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1TM-3 · W125
F1T → F0TM
20.259375 / 1.5 / 33.546875 in 514.59 / 38.10 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1TM-4 · W125
F1T → F0TM
25.178125 / 1.5 / 33.546875 in 639.52 / 38.10 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM1TM-5 · W125
F1T → F0TM
30.096875 / 1.5 / 33.546875 in 764.46 / 38.10 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 49–60
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LAM2L-0 · W125
F2L → F1B
2.453125 / 2.25 / 3.803125 in 62.31 / 57.15 / 96.60 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2L-1 · W125
F2L → F1L
2.453125 / 2.25 / 8.735417 in 62.31 / 57.15 / 221.88 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2L-2 · W125
F2L → F1L
2.453125 / 2.25 / 13.667708 in 62.31 / 57.15 / 347.16 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2L-3 · W125
F2L → F1L
2.453125 / 2.25 / 18.6 in 62.31 / 57.15 / 472.44 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2L-4 · W125
F2L → F1L
2.453125 / 2.25 / 23.532292 in 62.31 / 57.15 / 597.72 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2L-5 · W125
F2L → F1L
2.453125 / 2.25 / 28.464583 in 62.31 / 57.15 / 723.00 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2L-6 · W125
F2L → F1T
2.453125 / 2.25 / 33.396875 in 62.31 / 57.15 / 848.28 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2R-0 · W125
F2R → F1B
33.546875 / 2.25 / 3.803125 in 852.09 / 57.15 / 96.60 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2R-1 · W125
F2R → F1R
33.546875 / 2.25 / 8.735417 in 852.09 / 57.15 / 221.88 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2R-2 · W125
F2R → F1R
33.546875 / 2.25 / 13.667708 in 852.09 / 57.15 / 347.16 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2R-3 · W125
F2R → F1R
33.546875 / 2.25 / 18.6 in 852.09 / 57.15 / 472.44 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2R-4 · W125
F2R → F1R
33.546875 / 2.25 / 23.532292 in 852.09 / 57.15 / 597.72 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 61–72
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LAM2R-5 · W125
F2R → F1R
33.546875 / 2.25 / 28.464583 in 852.09 / 57.15 / 723.00 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2R-6 · W125
F2R → F1T
33.546875 / 2.25 / 33.396875 in 852.09 / 57.15 / 848.28 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2BM-0 · W125
F2BM → F1B
5.803125 / 2.25 / 2.453125 in 147.40 / 57.15 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2BM-1 · W125
F2BM → F1B
10.721875 / 2.25 / 2.453125 in 272.34 / 57.15 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2BM-2 · W125
F2BM → F1B
15.640625 / 2.25 / 2.453125 in 397.27 / 57.15 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2BM-3 · W125
F2BM → F1B
20.559375 / 2.25 / 2.453125 in 522.21 / 57.15 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2BM-4 · W125
F2BM → F1B
25.478125 / 2.25 / 2.453125 in 647.14 / 57.15 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2BM-5 · W125
F2BM → F1B
30.396875 / 2.25 / 2.453125 in 772.08 / 57.15 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2TM-0 · W125
F2TM → F1T
5.803125 / 2.25 / 33.546875 in 147.40 / 57.15 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2TM-1 · W125
F2TM → F1T
10.721875 / 2.25 / 33.546875 in 272.34 / 57.15 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2TM-2 · W125
F2TM → F1T
15.640625 / 2.25 / 33.546875 in 397.27 / 57.15 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2TM-3 · W125
F2TM → F1T
20.559375 / 2.25 / 33.546875 in 522.21 / 57.15 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 73–84
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LAM2TM-4 · W125
F2TM → F1T
25.478125 / 2.25 / 33.546875 in 647.14 / 57.15 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM2TM-5 · W125
F2TM → F1T
30.396875 / 2.25 / 33.546875 in 772.08 / 57.15 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3L-0 · W125
F3B → F2L
2.453125 / 3 / 4.103125 in 62.31 / 76.20 / 104.22 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3L-1 · W125
F3L → F2L
2.453125 / 3 / 9.035417 in 62.31 / 76.20 / 229.50 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3L-2 · W125
F3L → F2L
2.453125 / 3 / 13.967708 in 62.31 / 76.20 / 354.78 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3L-3 · W125
F3L → F2L
2.453125 / 3 / 18.9 in 62.31 / 76.20 / 480.06 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3L-4 · W125
F3L → F2L
2.453125 / 3 / 23.832292 in 62.31 / 76.20 / 605.34 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3L-5 · W125
F3L → F2L
2.453125 / 3 / 28.764583 in 62.31 / 76.20 / 730.62 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3L-6 · W125
F3T → F2L
2.453125 / 3 / 33.696875 in 62.31 / 76.20 / 855.90 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3R-0 · W125
F3B → F2R
33.546875 / 3 / 4.103125 in 852.09 / 76.20 / 104.22 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3R-1 · W125
F3R → F2R
33.546875 / 3 / 9.035417 in 852.09 / 76.20 / 229.50 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3R-2 · W125
F3R → F2R
33.546875 / 3 / 13.967708 in 852.09 / 76.20 / 354.78 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 85–96
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LAM3R-3 · W125
F3R → F2R
33.546875 / 3 / 18.9 in 852.09 / 76.20 / 480.06 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3R-4 · W125
F3R → F2R
33.546875 / 3 / 23.832292 in 852.09 / 76.20 / 605.34 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3R-5 · W125
F3R → F2R
33.546875 / 3 / 28.764583 in 852.09 / 76.20 / 730.62 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3R-6 · W125
F3T → F2R
33.546875 / 3 / 33.696875 in 852.09 / 76.20 / 855.90 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3BM-0 · W125
F3B → F2BM
6.103125 / 3 / 2.453125 in 155.02 / 76.20 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3BM-1 · W125
F3B → F2BM
11.021875 / 3 / 2.453125 in 279.96 / 76.20 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3BM-2 · W125
F3B → F2BM
15.940625 / 3 / 2.453125 in 404.89 / 76.20 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3BM-3 · W125
F3B → F2BM
20.859375 / 3 / 2.453125 in 529.83 / 76.20 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3BM-4 · W125
F3B → F2BM
25.778125 / 3 / 2.453125 in 654.76 / 76.20 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3BM-5 · W125
F3B → F2BM
30.696875 / 3 / 2.453125 in 779.70 / 76.20 / 62.31 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3TM-0 · W125
F3T → F2TM
6.103125 / 3 / 33.546875 in 155.02 / 76.20 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3TM-1 · W125
F3T → F2TM
11.021875 / 3 / 33.546875 in 279.96 / 76.20 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 97–108
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LAM3TM-2 · W125
F3T → F2TM
15.940625 / 3 / 33.546875 in 404.89 / 76.20 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3TM-3 · W125
F3T → F2TM
20.859375 / 3 / 33.546875 in 529.83 / 76.20 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3TM-4 · W125
F3T → F2TM
25.778125 / 3 / 33.546875 in 654.76 / 76.20 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-LAM3TM-5 · W125
F3T → F2TM
30.696875 / 3 / 33.546875 in 779.70 / 76.20 / 852.09 mm
−Y · 1 1/4 in (31.75 mm)
S-DLAMML-0 · W125
DM1B → DM0L
6.078125 / 1.5 / 10.703125 in 154.38 / 38.10 / 271.86 mm
−Y · 1 1/4 in (31.75 mm)
S-DLAMML-1 · W125
DM1L → DM0L
6.078125 / 1.5 / 16.453125 in 154.38 / 38.10 / 417.91 mm
−Y · 1 1/4 in (31.75 mm)
S-DLAMML-2 · W125
DM1L → DM0L
6.078125 / 1.5 / 24.171875 in 154.38 / 38.10 / 613.97 mm
−Y · 1 1/4 in (31.75 mm)
S-DLAMML-3 · W125
DM1T → DM0L
6.078125 / 1.5 / 29.921875 in 154.38 / 38.10 / 760.02 mm
−Y · 1 1/4 in (31.75 mm)
S-DLAMMR-0 · W125
DM1B → DM0R
29.921875 / 1.5 / 10.703125 in 760.02 / 38.10 / 271.86 mm
−Y · 1 1/4 in (31.75 mm)
S-DLAMMR-1 · W125
DM1R → DM0R
29.921875 / 1.5 / 16.453125 in 760.02 / 38.10 / 417.91 mm
−Y · 1 1/4 in (31.75 mm)
S-DLAMMR-2 · W125
DM1R → DM0R
29.921875 / 1.5 / 24.171875 in 760.02 / 38.10 / 613.97 mm
−Y · 1 1/4 in (31.75 mm)
S-DLAMMR-3 · W125
DM1T → DM0R
29.921875 / 1.5 / 29.921875 in 760.02 / 38.10 / 760.02 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 109–120
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-RLAMM-0-0 · W200
RBM3 + RBM2 → RBM1
6.003125 / 2.109375 / 5.203125 in 152.48 / 53.58 / 132.16 mm
−Y · 2 in (50.8 mm)
S-RLAMM-0-1 · W200
RBM3 + RBM2 → RBM1
6.003125 / 2.109375 / 7.828125 in 152.48 / 53.58 / 198.83 mm
−Y · 2 in (50.8 mm)
S-RLAMM-1-0 · W200
RBM3 + RBM2 → RBM1
10.801875 / 2.109375 / 5.203125 in 274.37 / 53.58 / 132.16 mm
−Y · 2 in (50.8 mm)
S-RLAMM-1-1 · W200
RBM3 + RBM2 → RBM1
10.801875 / 2.109375 / 7.828125 in 274.37 / 53.58 / 198.83 mm
−Y · 2 in (50.8 mm)
S-RLAMM-2-0 · W200
RBM3 + RBM2 → RBM1
15.600625 / 2.109375 / 5.203125 in 396.26 / 53.58 / 132.16 mm
−Y · 2 in (50.8 mm)
S-RLAMM-2-1 · W200
RBM3 + RBM2 → RBM1
15.600625 / 2.109375 / 7.828125 in 396.26 / 53.58 / 198.83 mm
−Y · 2 in (50.8 mm)
S-RLAMM-3-0 · W200
RBM3 + RBM2 → RBM1
20.399375 / 2.109375 / 5.203125 in 518.14 / 53.58 / 132.16 mm
−Y · 2 in (50.8 mm)
S-RLAMM-3-1 · W200
RBM3 + RBM2 → RBM1
20.399375 / 2.109375 / 7.828125 in 518.14 / 53.58 / 198.83 mm
−Y · 2 in (50.8 mm)
S-RLAMM-4-0 · W200
RBM3 + RBM2 → RBM1
25.198125 / 2.109375 / 5.203125 in 640.03 / 53.58 / 132.16 mm
−Y · 2 in (50.8 mm)
S-RLAMM-4-1 · W200
RBM3 + RBM2 → RBM1
25.198125 / 2.109375 / 7.828125 in 640.03 / 53.58 / 198.83 mm
−Y · 2 in (50.8 mm)
S-RLAMM-5-0 · W200
RBM3 + RBM2 → RBM1
29.996875 / 2.109375 / 5.203125 in 761.92 / 53.58 / 132.16 mm
−Y · 2 in (50.8 mm)
S-RLAMM-5-1 · W200
RBM3 + RBM2 → RBM1
29.996875 / 2.109375 / 7.828125 in 761.92 / 53.58 / 198.83 mm
−Y · 2 in (50.8 mm)
Fastener stations · 121–132
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-CLB-0 · W125
P01 → CLB
1.453125 / 4 / 0 in 36.91 / 101.60 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CLB-1 · W125
P01 → CLB
1.453125 / 8.098958 / 0 in 36.91 / 205.71 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CLB-2 · W125
P01 → CLB
1.453125 / 12.197917 / 0 in 36.91 / 309.83 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CLB-3 · W125
P01 → CLB
1.453125 / 16.296875 / 0 in 36.91 / 413.94 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CRB-0 · W125
P01 → CRB
34.546875 / 4 / 0 in 877.49 / 101.60 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CRB-1 · W125
P01 → CRB
34.546875 / 8.098958 / 0 in 877.49 / 205.71 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CRB-2 · W125
P01 → CRB
34.546875 / 12.197917 / 0 in 877.49 / 309.83 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CRB-3 · W125
P01 → CRB
34.546875 / 16.296875 / 0 in 877.49 / 413.94 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CB-0 · W125
P01 → CB
3.203125 / 16.546875 / 0 in 81.36 / 420.29 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CB-1 · W125
P01 → CB
9.121875 / 16.546875 / 0 in 231.70 / 420.29 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CB-2 · W125
P01 → CB
15.040625 / 16.546875 / 0 in 382.03 / 420.29 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CB-3 · W125
P01 → CB
20.959375 / 16.546875 / 0 in 532.37 / 420.29 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
Fastener stations · 133–144
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-CB-4 · W125
P01 → CB
26.878125 / 16.546875 / 0 in 682.70 / 420.29 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-CB-5 · W125
P01 → CB
32.796875 / 16.546875 / 0 in 833.04 / 420.29 / 0.00 mm
+Z · 1 1/4 in (31.75 mm)
S-WL-CLB-0 · W125
P03L → CLB
0 / 4 / 1.453125 in 0.00 / 101.60 / 36.91 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLB-1 · W125
P03L → CLB
0 / 8.098958 / 1.453125 in 0.00 / 205.71 / 36.91 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLB-2 · W125
P03L → CLB
0 / 12.197917 / 1.453125 in 0.00 / 309.83 / 36.91 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLB-3 · W125
P03L → CLB
0 / 16.296875 / 1.453125 in 0.00 / 413.94 / 36.91 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLT-0 · W125
P03L → CLT
0 / 4 / 34.546875 in 0.00 / 101.60 / 877.49 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLT-1 · W125
P03L → CLT
0 / 8.098958 / 34.546875 in 0.00 / 205.71 / 877.49 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLT-2 · W125
P03L → CLT
0 / 12.197917 / 34.546875 in 0.00 / 309.83 / 877.49 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLT-3 · W125
P03L → CLT
0 / 16.296875 / 34.546875 in 0.00 / 413.94 / 877.49 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLU-0 · W125
P03L → CLU
0 / 16.546875 / 3.203125 in 0.00 / 420.29 / 81.36 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLU-1 · W125
P03L → CLU
0 / 16.546875 / 9.121875 in 0.00 / 420.29 / 231.70 mm
+X · 1 1/4 in (31.75 mm)
Fastener stations · 145–156
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-WL-CLU-2 · W125
P03L → CLU
0 / 16.546875 / 15.040625 in 0.00 / 420.29 / 382.03 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLU-3 · W125
P03L → CLU
0 / 16.546875 / 20.959375 in 0.00 / 420.29 / 532.37 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLU-4 · W125
P03L → CLU
0 / 16.546875 / 26.878125 in 0.00 / 420.29 / 682.70 mm
+X · 1 1/4 in (31.75 mm)
S-WL-CLU-5 · W125
P03L → CLU
0 / 16.546875 / 32.796875 in 0.00 / 420.29 / 833.04 mm
+X · 1 1/4 in (31.75 mm)
S-WR-CRB-0 · W125
P03R → CRB
36 / 4 / 1.453125 in 914.40 / 101.60 / 36.91 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRB-1 · W125
P03R → CRB
36 / 8.098958 / 1.453125 in 914.40 / 205.71 / 36.91 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRB-2 · W125
P03R → CRB
36 / 12.197917 / 1.453125 in 914.40 / 309.83 / 36.91 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRB-3 · W125
P03R → CRB
36 / 16.296875 / 1.453125 in 914.40 / 413.94 / 36.91 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRT-0 · W125
P03R → CRT
36 / 4 / 34.546875 in 914.40 / 101.60 / 877.49 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRT-1 · W125
P03R → CRT
36 / 8.098958 / 34.546875 in 914.40 / 205.71 / 877.49 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRT-2 · W125
P03R → CRT
36 / 12.197917 / 34.546875 in 914.40 / 309.83 / 877.49 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRT-3 · W125
P03R → CRT
36 / 16.296875 / 34.546875 in 914.40 / 413.94 / 877.49 mm
−X · 1 1/4 in (31.75 mm)
Fastener stations · 157–168
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-WR-CRU-0 · W125
P03R → CRU
36 / 16.546875 / 3.203125 in 914.40 / 420.29 / 81.36 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRU-1 · W125
P03R → CRU
36 / 16.546875 / 9.121875 in 914.40 / 420.29 / 231.70 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRU-2 · W125
P03R → CRU
36 / 16.546875 / 15.040625 in 914.40 / 420.29 / 382.03 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRU-3 · W125
P03R → CRU
36 / 16.546875 / 20.959375 in 914.40 / 420.29 / 532.37 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRU-4 · W125
P03R → CRU
36 / 16.546875 / 26.878125 in 914.40 / 420.29 / 682.70 mm
−X · 1 1/4 in (31.75 mm)
S-WR-CRU-5 · W125
P03R → CRU
36 / 16.546875 / 32.796875 in 914.40 / 420.29 / 833.04 mm
−X · 1 1/4 in (31.75 mm)
S-B-CB-0 · W125
P04 → CB
3.203125 / 18 / 1.453125 in 81.36 / 457.20 / 36.91 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CB-1 · W125
P04 → CB
9.121875 / 18 / 1.453125 in 231.70 / 457.20 / 36.91 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CB-2 · W125
P04 → CB
15.040625 / 18 / 1.453125 in 382.03 / 457.20 / 36.91 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CB-3 · W125
P04 → CB
20.959375 / 18 / 1.453125 in 532.37 / 457.20 / 36.91 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CB-4 · W125
P04 → CB
26.878125 / 18 / 1.453125 in 682.70 / 457.20 / 36.91 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CB-5 · W125
P04 → CB
32.796875 / 18 / 1.453125 in 833.04 / 457.20 / 36.91 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 169–180
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-B-CT-0 · W125
P04 → CT
3.203125 / 18 / 34.546875 in 81.36 / 457.20 / 877.49 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CT-1 · W125
P04 → CT
9.121875 / 18 / 34.546875 in 231.70 / 457.20 / 877.49 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CT-2 · W125
P04 → CT
15.040625 / 18 / 34.546875 in 382.03 / 457.20 / 877.49 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CT-3 · W125
P04 → CT
20.959375 / 18 / 34.546875 in 532.37 / 457.20 / 877.49 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CT-4 · W125
P04 → CT
26.878125 / 18 / 34.546875 in 682.70 / 457.20 / 877.49 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CT-5 · W125
P04 → CT
32.796875 / 18 / 34.546875 in 833.04 / 457.20 / 877.49 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CLU-0 · W125
P04 → CLU
1.453125 / 18 / 3.503125 in 36.91 / 457.20 / 88.98 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CLU-1 · W125
P04 → CLU
1.453125 / 18 / 9.421875 in 36.91 / 457.20 / 239.32 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CLU-2 · W125
P04 → CLU
1.453125 / 18 / 15.340625 in 36.91 / 457.20 / 389.65 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CLU-3 · W125
P04 → CLU
1.453125 / 18 / 21.259375 in 36.91 / 457.20 / 539.99 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CLU-4 · W125
P04 → CLU
1.453125 / 18 / 27.178125 in 36.91 / 457.20 / 690.32 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CLU-5 · W125
P04 → CLU
1.453125 / 18 / 33.096875 in 36.91 / 457.20 / 840.66 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 181–192
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-B-CRU-0 · W125
P04 → CRU
34.546875 / 18 / 3.503125 in 877.49 / 457.20 / 88.98 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CRU-1 · W125
P04 → CRU
34.546875 / 18 / 9.421875 in 877.49 / 457.20 / 239.32 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CRU-2 · W125
P04 → CRU
34.546875 / 18 / 15.340625 in 877.49 / 457.20 / 389.65 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CRU-3 · W125
P04 → CRU
34.546875 / 18 / 21.259375 in 877.49 / 457.20 / 539.99 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CRU-4 · W125
P04 → CRU
34.546875 / 18 / 27.178125 in 877.49 / 457.20 / 690.32 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CRU-5 · W125
P04 → CRU
34.546875 / 18 / 33.096875 in 877.49 / 457.20 / 840.66 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CM1-0 · W125
P04 → CM1
18 / 18 / 3.203125 in 457.20 / 457.20 / 81.36 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CM1-1 · W125
P04 → CM1
18 / 18 / 9.121875 in 457.20 / 457.20 / 231.70 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CM1-2 · W125
P04 → CM1
18 / 18 / 15.040625 in 457.20 / 457.20 / 382.03 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CM1-3 · W125
P04 → CM1
18 / 18 / 20.959375 in 457.20 / 457.20 / 532.37 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CM1-4 · W125
P04 → CM1
18 / 18 / 26.878125 in 457.20 / 457.20 / 682.70 mm
−Y · 1 1/4 in (31.75 mm)
S-B-CM1-5 · W125
P04 → CM1
18 / 18 / 32.796875 in 457.20 / 457.20 / 833.04 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 193–204
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-FL-0-0 · W200
P03L → F0L
0 / 0.375 / 1.703125 in 0.00 / 9.52 / 43.26 mm
+X · 2 in (50.8 mm)
S-FL-0-1 · W200
P03L → F2L
0 / 1.875 / 1.703125 in 0.00 / 47.62 / 43.26 mm
+X · 2 in (50.8 mm)
S-FL-1-0 · W200
P03L → F0L
0 / 0.375 / 6.359375 in 0.00 / 9.52 / 161.53 mm
+X · 2 in (50.8 mm)
S-FL-1-1 · W200
P03L → F2L
0 / 1.875 / 6.359375 in 0.00 / 47.62 / 161.53 mm
+X · 2 in (50.8 mm)
S-FL-2-0 · W200
P03L → F0L
0 / 0.375 / 11.015625 in 0.00 / 9.52 / 279.80 mm
+X · 2 in (50.8 mm)
S-FL-2-1 · W200
P03L → F2L
0 / 1.875 / 11.015625 in 0.00 / 47.62 / 279.80 mm
+X · 2 in (50.8 mm)
S-FL-3-0 · W200
P03L → F0L
0 / 0.375 / 15.671875 in 0.00 / 9.52 / 398.07 mm
+X · 2 in (50.8 mm)
S-FL-3-1 · W200
P03L → F2L
0 / 1.875 / 15.671875 in 0.00 / 47.62 / 398.07 mm
+X · 2 in (50.8 mm)
S-FL-4-0 · W200
P03L → F0L
0 / 0.375 / 20.328125 in 0.00 / 9.52 / 516.33 mm
+X · 2 in (50.8 mm)
S-FL-4-1 · W200
P03L → F2L
0 / 1.875 / 20.328125 in 0.00 / 47.62 / 516.33 mm
+X · 2 in (50.8 mm)
S-FL-5-0 · W200
P03L → F0L
0 / 0.375 / 24.984375 in 0.00 / 9.52 / 634.60 mm
+X · 2 in (50.8 mm)
S-FL-5-1 · W200
P03L → F2L
0 / 1.875 / 24.984375 in 0.00 / 47.62 / 634.60 mm
+X · 2 in (50.8 mm)
Fastener stations · 205–216
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-FL-6-0 · W200
P03L → F0L
0 / 0.375 / 29.640625 in 0.00 / 9.52 / 752.87 mm
+X · 2 in (50.8 mm)
S-FL-6-1 · W200
P03L → F2L
0 / 1.875 / 29.640625 in 0.00 / 47.62 / 752.87 mm
+X · 2 in (50.8 mm)
S-FL-7-0 · W200
P03L → F0L
0 / 0.375 / 34.296875 in 0.00 / 9.52 / 871.14 mm
+X · 2 in (50.8 mm)
S-FL-7-1 · W200
P03L → F2L
0 / 1.875 / 34.296875 in 0.00 / 47.62 / 871.14 mm
+X · 2 in (50.8 mm)
S-FR-0-0 · W200
P03R → F0R
36 / 0.375 / 1.703125 in 914.40 / 9.52 / 43.26 mm
−X · 2 in (50.8 mm)
S-FR-0-1 · W200
P03R → F2R
36 / 1.875 / 1.703125 in 914.40 / 47.62 / 43.26 mm
−X · 2 in (50.8 mm)
S-FR-1-0 · W200
P03R → F0R
36 / 0.375 / 6.359375 in 914.40 / 9.52 / 161.53 mm
−X · 2 in (50.8 mm)
S-FR-1-1 · W200
P03R → F2R
36 / 1.875 / 6.359375 in 914.40 / 47.62 / 161.53 mm
−X · 2 in (50.8 mm)
S-FR-2-0 · W200
P03R → F0R
36 / 0.375 / 11.015625 in 914.40 / 9.52 / 279.80 mm
−X · 2 in (50.8 mm)
S-FR-2-1 · W200
P03R → F2R
36 / 1.875 / 11.015625 in 914.40 / 47.62 / 279.80 mm
−X · 2 in (50.8 mm)
S-FR-3-0 · W200
P03R → F0R
36 / 0.375 / 15.671875 in 914.40 / 9.52 / 398.07 mm
−X · 2 in (50.8 mm)
S-FR-3-1 · W200
P03R → F2R
36 / 1.875 / 15.671875 in 914.40 / 47.62 / 398.07 mm
−X · 2 in (50.8 mm)
Fastener stations · 217–228
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-FR-4-0 · W200
P03R → F0R
36 / 0.375 / 20.328125 in 914.40 / 9.52 / 516.33 mm
−X · 2 in (50.8 mm)
S-FR-4-1 · W200
P03R → F2R
36 / 1.875 / 20.328125 in 914.40 / 47.62 / 516.33 mm
−X · 2 in (50.8 mm)
S-FR-5-0 · W200
P03R → F0R
36 / 0.375 / 24.984375 in 914.40 / 9.52 / 634.60 mm
−X · 2 in (50.8 mm)
S-FR-5-1 · W200
P03R → F2R
36 / 1.875 / 24.984375 in 914.40 / 47.62 / 634.60 mm
−X · 2 in (50.8 mm)
S-FR-6-0 · W200
P03R → F0R
36 / 0.375 / 29.640625 in 914.40 / 9.52 / 752.87 mm
−X · 2 in (50.8 mm)
S-FR-6-1 · W200
P03R → F2R
36 / 1.875 / 29.640625 in 914.40 / 47.62 / 752.87 mm
−X · 2 in (50.8 mm)
S-FR-7-0 · W200
P03R → F0R
36 / 0.375 / 34.296875 in 914.40 / 9.52 / 871.14 mm
−X · 2 in (50.8 mm)
S-FR-7-1 · W200
P03R → F2R
36 / 1.875 / 34.296875 in 914.40 / 47.62 / 871.14 mm
−X · 2 in (50.8 mm)
S-FLOORFR-0-0 · W200
P01 → F1B
1.703125 / 1.125 / 0 in 43.26 / 28.57 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-0-1 · W200
P01 → F3B
1.703125 / 2.625 / 0 in 43.26 / 66.67 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-1-0 · W200
P01 → F1B
6.359375 / 1.125 / 0 in 161.53 / 28.57 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-1-1 · W200
P01 → F3B
6.359375 / 2.625 / 0 in 161.53 / 66.67 / 0.00 mm
+Z · 2 in (50.8 mm)
Fastener stations · 229–240
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-FLOORFR-2-0 · W200
P01 → F1B
11.015625 / 1.125 / 0 in 279.80 / 28.57 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-2-1 · W200
P01 → F3B
11.015625 / 2.625 / 0 in 279.80 / 66.67 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-3-0 · W200
P01 → F1B
15.671875 / 1.125 / 0 in 398.07 / 28.57 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-3-1 · W200
P01 → F3B
15.671875 / 2.625 / 0 in 398.07 / 66.67 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-4-0 · W200
P01 → F1B
20.328125 / 1.125 / 0 in 516.33 / 28.57 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-4-1 · W200
P01 → F3B
20.328125 / 2.625 / 0 in 516.33 / 66.67 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-5-0 · W200
P01 → F1B
24.984375 / 1.125 / 0 in 634.60 / 28.57 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-5-1 · W200
P01 → F3B
24.984375 / 2.625 / 0 in 634.60 / 66.67 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-6-0 · W200
P01 → F1B
29.640625 / 1.125 / 0 in 752.87 / 28.57 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-6-1 · W200
P01 → F3B
29.640625 / 2.625 / 0 in 752.87 / 66.67 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-7-0 · W200
P01 → F1B
34.296875 / 1.125 / 0 in 871.14 / 28.57 / 0.00 mm
+Z · 2 in (50.8 mm)
S-FLOORFR-7-1 · W200
P01 → F3B
34.296875 / 2.625 / 0 in 871.14 / 66.67 / 0.00 mm
+Z · 2 in (50.8 mm)
Fastener stations · 241–252
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-VLB-0 · W100
VLB → P03L
-0.375 / 5.625 / 9.078125 in -9.52 / 142.88 / 230.58 mm
+X · 1 in (25.4 mm)
S-VLB-1 · W100
VLB → P03L
-0.375 / 9 / 9.078125 in -9.52 / 228.60 / 230.58 mm
+X · 1 in (25.4 mm)
S-VLB-2 · W100
VLB → P03L
-0.375 / 12.375 / 9.078125 in -9.52 / 314.32 / 230.58 mm
+X · 1 in (25.4 mm)
S-VLT-0 · W100
VLT → P03L
-0.375 / 5.625 / 14.578125 in -9.52 / 142.88 / 370.28 mm
+X · 1 in (25.4 mm)
S-VLT-1 · W100
VLT → P03L
-0.375 / 9 / 14.578125 in -9.52 / 228.60 / 370.28 mm
+X · 1 in (25.4 mm)
S-VLT-2 · W100
VLT → P03L
-0.375 / 12.375 / 14.578125 in -9.52 / 314.32 / 370.28 mm
+X · 1 in (25.4 mm)
S-VLF-0 · W100
VLF → P03L
-0.375 / 5.25 / 10.203125 in -9.52 / 133.35 / 259.16 mm
+X · 1 in (25.4 mm)
S-VLF-1 · W100
VLF → P03L
-0.375 / 5.25 / 13.453125 in -9.52 / 133.35 / 341.71 mm
+X · 1 in (25.4 mm)
S-VLA-0 · W100
VLA → P03L
-0.375 / 12.75 / 10.203125 in -9.52 / 323.85 / 259.16 mm
+X · 1 in (25.4 mm)
S-VLA-1 · W100
VLA → P03L
-0.375 / 12.75 / 13.453125 in -9.52 / 323.85 / 341.71 mm
+X · 1 in (25.4 mm)
S-VRB-0 · W100
VRB → P03R
36.375 / 5.625 / 9.078125 in 923.92 / 142.88 / 230.58 mm
−X · 1 in (25.4 mm)
S-VRB-1 · W100
VRB → P03R
36.375 / 9 / 9.078125 in 923.92 / 228.60 / 230.58 mm
−X · 1 in (25.4 mm)
Fastener stations · 253–264
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-VRB-2 · W100
VRB → P03R
36.375 / 12.375 / 9.078125 in 923.92 / 314.32 / 230.58 mm
−X · 1 in (25.4 mm)
S-VRT-0 · W100
VRT → P03R
36.375 / 5.625 / 14.578125 in 923.92 / 142.88 / 370.28 mm
−X · 1 in (25.4 mm)
S-VRT-1 · W100
VRT → P03R
36.375 / 9 / 14.578125 in 923.92 / 228.60 / 370.28 mm
−X · 1 in (25.4 mm)
S-VRT-2 · W100
VRT → P03R
36.375 / 12.375 / 14.578125 in 923.92 / 314.32 / 370.28 mm
−X · 1 in (25.4 mm)
S-VRF-0 · W100
VRF → P03R
36.375 / 5.25 / 10.203125 in 923.92 / 133.35 / 259.16 mm
−X · 1 in (25.4 mm)
S-VRF-1 · W100
VRF → P03R
36.375 / 5.25 / 13.453125 in 923.92 / 133.35 / 341.71 mm
−X · 1 in (25.4 mm)
S-VRA-0 · W100
VRA → P03R
36.375 / 12.75 / 10.203125 in 923.92 / 323.85 / 259.16 mm
−X · 1 in (25.4 mm)
S-VRA-1 · W100
VRA → P03R
36.375 / 12.75 / 13.453125 in 923.92 / 323.85 / 341.71 mm
−X · 1 in (25.4 mm)
S-RTCF-0 · W100
RTCF → P02
8.625 / 3.25 / 34.921875 in 219.07 / 82.55 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCF-1 · W100
RTCF → P02
13.3125 / 3.25 / 34.921875 in 338.14 / 82.55 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCF-2 · W100
RTCF → P02
18 / 3.25 / 34.921875 in 457.20 / 82.55 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCF-3 · W100
RTCF → P02
22.6875 / 3.25 / 34.921875 in 576.26 / 82.55 / 887.02 mm
+Z · 1 in (25.4 mm)
Fastener stations · 265–276
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-RTCF-4 · W100
RTCF → P02
27.375 / 3.25 / 34.921875 in 695.32 / 82.55 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCA-0 · W100
RTCA → P02
8.625 / 14.75 / 34.921875 in 219.07 / 374.65 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCA-1 · W100
RTCA → P02
13.3125 / 14.75 / 34.921875 in 338.14 / 374.65 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCA-2 · W100
RTCA → P02
18 / 14.75 / 34.921875 in 457.20 / 374.65 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCA-3 · W100
RTCA → P02
22.6875 / 14.75 / 34.921875 in 576.26 / 374.65 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCA-4 · W100
RTCA → P02
27.375 / 14.75 / 34.921875 in 695.32 / 374.65 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCL-0 · W100
RTCL → P02
8.25 / 4.375 / 34.921875 in 209.55 / 111.12 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCL-1 · W100
RTCL → P02
8.25 / 9 / 34.921875 in 209.55 / 228.60 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCL-2 · W100
RTCL → P02
8.25 / 13.625 / 34.921875 in 209.55 / 346.07 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCR-0 · W100
RTCR → P02
27.75 / 4.375 / 34.921875 in 704.85 / 111.12 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCR-1 · W100
RTCR → P02
27.75 / 9 / 34.921875 in 704.85 / 228.60 / 887.02 mm
+Z · 1 in (25.4 mm)
S-RTCR-2 · W100
RTCR → P02
27.75 / 13.625 / 34.921875 in 704.85 / 346.07 / 887.02 mm
+Z · 1 in (25.4 mm)
Fastener stations · 277–288
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-BEML-0 · W125
BEML + SPML → DM1B
6.828125 / 2.101 / 11.578125 in 173.43 / 53.37 / 294.08 mm
−Y · 1 1/4 in (31.75 mm)
S-BEML-1 · W125
BEML + SPML → DM1L
6.828125 / 2.101 / 15.945312 in 173.43 / 53.37 / 405.01 mm
−Y · 1 1/4 in (31.75 mm)
S-BEML-2 · W125
BEML + SPML → DM1L
6.828125 / 2.101 / 20.3125 in 173.43 / 53.37 / 515.94 mm
−Y · 1 1/4 in (31.75 mm)
S-BEML-3 · W125
BEML + SPML → DM1L
6.828125 / 2.101 / 24.679688 in 173.43 / 53.37 / 626.86 mm
−Y · 1 1/4 in (31.75 mm)
S-BEML-4 · W125
BEML + SPML → DM1T
6.828125 / 2.101 / 29.046875 in 173.43 / 53.37 / 737.79 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMR-0 · W125
BEMR + SPMR → DM1B
29.171875 / 2.101 / 11.578125 in 740.97 / 53.37 / 294.08 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMR-1 · W125
BEMR + SPMR → DM1R
29.171875 / 2.101 / 15.945312 in 740.97 / 53.37 / 405.01 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMR-2 · W125
BEMR + SPMR → DM1R
29.171875 / 2.101 / 20.3125 in 740.97 / 53.37 / 515.94 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMR-3 · W125
BEMR + SPMR → DM1R
29.171875 / 2.101 / 24.679688 in 740.97 / 53.37 / 626.86 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMR-4 · W125
BEMR + SPMR → DM1T
29.171875 / 2.101 / 29.046875 in 740.97 / 53.37 / 737.79 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMB-0 · W125
BEMB + SPMB → DM1B
8.203125 / 2.101 / 11.453125 in 208.36 / 53.37 / 290.91 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMB-1 · W125
BEMB + SPMB → DM1B
12.121875 / 2.101 / 11.453125 in 307.90 / 53.37 / 290.91 mm
−Y · 1 1/4 in (31.75 mm)
Fastener stations · 289–300
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-BEMB-2 · W125
BEMB + SPMB → DM1B
16.040625 / 2.101 / 11.453125 in 407.43 / 53.37 / 290.91 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMB-3 · W125
BEMB + SPMB → DM1B
19.959375 / 2.101 / 11.453125 in 506.97 / 53.37 / 290.91 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMB-4 · W125
BEMB + SPMB → DM1B
23.878125 / 2.101 / 11.453125 in 606.50 / 53.37 / 290.91 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMB-5 · W125
BEMB + SPMB → DM1B
27.796875 / 2.101 / 11.453125 in 706.04 / 53.37 / 290.91 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMT-0 · W125
BEMT + SPMT → DM1T
8.203125 / 2.101 / 29.171875 in 208.36 / 53.37 / 740.97 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMT-1 · W125
BEMT + SPMT → DM1T
12.121875 / 2.101 / 29.171875 in 307.90 / 53.37 / 740.97 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMT-2 · W125
BEMT + SPMT → DM1T
16.040625 / 2.101 / 29.171875 in 407.43 / 53.37 / 740.97 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMT-3 · W125
BEMT + SPMT → DM1T
19.959375 / 2.101 / 29.171875 in 506.97 / 53.37 / 740.97 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMT-4 · W125
BEMT + SPMT → DM1T
23.878125 / 2.101 / 29.171875 in 606.50 / 53.37 / 740.97 mm
−Y · 1 1/4 in (31.75 mm)
S-BEMT-5 · W125
BEMT + SPMT → DM1T
27.796875 / 2.101 / 29.171875 in 706.04 / 53.37 / 740.97 mm
−Y · 1 1/4 in (31.75 mm)
S-LCL-0 · W100
LCL → P03L
1.203125 / 4 / 8.203125 in 30.56 / 101.60 / 208.36 mm
−X · 1 in (25.4 mm)
S-LCL-1 · W100
LCL → P03L
1.203125 / 7.557292 / 8.203125 in 30.56 / 191.96 / 208.36 mm
−X · 1 in (25.4 mm)
Fastener stations · 301–312
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LCL-2 · W100
LCL → P03L
1.203125 / 11.114583 / 8.203125 in 30.56 / 282.31 / 208.36 mm
−X · 1 in (25.4 mm)
S-LCL-3 · W100
LCL → P03L
1.203125 / 14.671875 / 8.203125 in 30.56 / 372.67 / 208.36 mm
−X · 1 in (25.4 mm)
S-LCR-0 · W100
LCR → P03R
34.796875 / 4 / 8.203125 in 883.84 / 101.60 / 208.36 mm
+X · 1 in (25.4 mm)
S-LCR-1 · W100
LCR → P03R
34.796875 / 7.557292 / 8.203125 in 883.84 / 191.96 / 208.36 mm
+X · 1 in (25.4 mm)
S-LCR-2 · W100
LCR → P03R
34.796875 / 11.114583 / 8.203125 in 883.84 / 282.31 / 208.36 mm
+X · 1 in (25.4 mm)
S-LCR-3 · W100
LCR → P03R
34.796875 / 14.671875 / 8.203125 in 883.84 / 372.67 / 208.36 mm
+X · 1 in (25.4 mm)
S-LCFJ1-0 · W100
LCFJ1 → F3L
1.453125 / 3.5 / 8.203125 in 36.91 / 88.90 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFJ1-1 · W100
LCFJ1 → F3L
3.578125 / 3.5 / 8.203125 in 90.88 / 88.90 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFRML-0 · W100
LCFRML → RCML
4.744792 / 4.109375 / 8.203125 in 120.52 / 104.38 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFRML-1 · W100
LCFRML → RCML
5.161458 / 4.109375 / 8.203125 in 131.10 / 104.38 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFPM-0 · W100
LCFPM → RBM3
6.328125 / 2.609375 / 8.203125 in 160.73 / 66.28 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFPM-1 · W100
LCFPM → RBM3
10.996875 / 2.609375 / 8.203125 in 279.32 / 66.28 / 208.36 mm
−Y · 1 in (25.4 mm)
Fastener stations · 313–324
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LCFPM-2 · W100
LCFPM → RBM3
15.665625 / 2.609375 / 8.203125 in 397.91 / 66.28 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFPM-3 · W100
LCFPM → RBM3
20.334375 / 2.609375 / 8.203125 in 516.49 / 66.28 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFPM-4 · W100
LCFPM → RBM3
25.003125 / 2.609375 / 8.203125 in 635.08 / 66.28 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFPM-5 · W100
LCFPM → RBM3
29.671875 / 2.609375 / 8.203125 in 753.67 / 66.28 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFRMR-0 · W100
LCFRMR → RCMR
30.838542 / 4.109375 / 8.203125 in 783.30 / 104.38 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFRMR-1 · W100
LCFRMR → RCMR
31.255208 / 4.109375 / 8.203125 in 793.88 / 104.38 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFJ2-0 · W100
LCFJ2 → F3R
32.421875 / 3.5 / 8.203125 in 823.52 / 88.90 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCFJ2-1 · W100
LCFJ2 → F3R
34.546875 / 3.5 / 8.203125 in 877.49 / 88.90 / 208.36 mm
−Y · 1 in (25.4 mm)
S-LCB1-0 · W100
LCB1 → P04
3.158125 / 16.796875 / 8.203125 in 80.22 / 426.64 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCB1-1 · W100
LCB1 → P04
7.537083 / 16.796875 / 8.203125 in 191.44 / 426.64 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCB1-2 · W100
LCB1 → P04
11.916042 / 16.796875 / 8.203125 in 302.67 / 426.64 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCB1-3 · W100
LCB1 → P04
16.295 / 16.796875 / 8.203125 in 413.89 / 426.64 / 208.36 mm
+Y · 1 in (25.4 mm)
Fastener stations · 325–336
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-LCB2-0 · W100
LCB2 → P04
19.705 / 16.796875 / 8.203125 in 500.51 / 426.64 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCB2-1 · W100
LCB2 → P04
24.083958 / 16.796875 / 8.203125 in 611.73 / 426.64 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCB2-2 · W100
LCB2 → P04
28.462917 / 16.796875 / 8.203125 in 722.96 / 426.64 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCB2-3 · W100
LCB2 → P04
32.841875 / 16.796875 / 8.203125 in 834.18 / 426.64 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCPL-0 · W100
LCPL → CLU
1.286458 / 15.296875 / 8.203125 in 32.68 / 388.54 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCPL-1 · W100
LCPL → CLU
1.744792 / 15.296875 / 8.203125 in 44.32 / 388.54 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCP1-0 · W100
LCP1 → CM1
17.75 / 15.296875 / 8.203125 in 450.85 / 388.54 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCP1-1 · W100
LCP1 → CM1
18.25 / 15.296875 / 8.203125 in 463.55 / 388.54 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCPR-0 · W100
LCPR → CRU
34.255208 / 15.296875 / 8.203125 in 870.08 / 388.54 / 208.36 mm
+Y · 1 in (25.4 mm)
S-LCPR-1 · W100
LCPR → CRU
34.713542 / 15.296875 / 8.203125 in 881.72 / 388.54 / 208.36 mm
+Y · 1 in (25.4 mm)
S-ROOFL-0 · W125
P02 → CLT
1.453125 / 4 / 36 in 36.91 / 101.60 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFL-1 · W125
P02 → CLT
1.453125 / 9 / 36 in 36.91 / 228.60 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
Fastener stations · 337–348
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-ROOFL-2 · W125
P02 → CLT
1.453125 / 15 / 36 in 36.91 / 381.00 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFR-0 · W125
P02 → CRT
34.546875 / 4 / 36 in 877.49 / 101.60 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFR-1 · W125
P02 → CRT
34.546875 / 9 / 36 in 877.49 / 228.60 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFR-2 · W125
P02 → CRT
34.546875 / 15 / 36 in 877.49 / 381.00 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFF-0 · W125
P02 → F1T
8 / 1.125 / 36 in 203.20 / 28.57 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFF-1 · W125
P02 → F1T
20 / 1.125 / 36 in 508.00 / 28.57 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFF-2 · W125
P02 → F1T
32 / 1.125 / 36 in 812.80 / 28.57 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFB-0 · W125
P02 → CT
8 / 16.546875 / 36 in 203.20 / 420.29 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFB-1 · W125
P02 → CT
19 / 16.546875 / 36 in 482.60 / 420.29 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-ROOFB-2 · W125
P02 → CT
30 / 16.546875 / 36 in 762.00 / 420.29 / 914.40 mm
−Z · 1 1/4 in (31.75 mm)
S-M-HP1 · HASP
M-HP-base → DM0R
31.295625 / -0.07 / 18.3125 in 794.91 / -1.78 / 465.14 mm
+Y · 5/8 in (15.88 mm)
S-M-HP2 · HASP
M-HP-base → DM0R
30.925625 / -0.07 / 18.8125 in 785.51 / -1.78 / 477.84 mm
+Y · 5/8 in (15.88 mm)
Fastener stations · 349–353
Use the named assembly datums. Clearance passes through first members; stopped pilots enter the receivers. Received heads and thin metal webs require accepted trials.
ID / type
Through → receiver
Start X / Y / Z
Direction / length
S-M-HP3 · HASP
M-HP-base → DM0R
30.825625 / -0.07 / 17.8125 in 782.97 / -1.78 / 452.44 mm
+Y · 5/8 in (15.88 mm)
S-M-ST1 · HASP
M-ST-base → F0R
33.175625 / -0.07 / 17.7525 in 842.66 / -1.78 / 450.91 mm
+Y · 5/8 in (15.88 mm)
S-M-ST2 · HASP
M-ST-base → F0R
32.055625 / -0.07 / 17.7525 in 814.21 / -1.78 / 450.91 mm
+Y · 5/8 in (15.88 mm)
S-M-ST3 · HASP
M-ST-base → F0R
33.175625 / -0.07 / 18.8725 in 842.66 / -1.78 / 479.36 mm
+Y · 5/8 in (15.88 mm)
S-M-ST4 · HASP
M-ST-base → F0R
32.055625 / -0.07 / 18.8725 in 814.21 / -1.78 / 479.36 mm
+Y · 5/8 in (15.88 mm)
Machining removals
Local X / Y / Z begin at the named part’s minimum assembled-coordinate corner. Cut volumes extend slightly beyond an edge for a through-cut and are clipped to the part. Read orientation pictures; never use a schematic as a full-size template.
Cut / part
Local X / Y / Z
Removal size
Operation
POCKET-VLB / VLB
0.287 in (7.29 mm) / 0.494 in (12.55 mm) / 0.494 in (12.55 mm)
0.088 in (2.24 mm) × 7.012 in (178.1 mm) × 5.012 in (127.3 mm)
Wall-facing wire rebate; preserve outer wood bearing land
POCKET-VLT / VLT
0.287 in (7.29 mm) / 0.494 in (12.55 mm) / -4.506 in (-114.45 mm)
0.088 in (2.24 mm) × 7.012 in (178.1 mm) × 5.012 in (127.3 mm)
Wall-facing wire rebate; preserve outer wood bearing land
POCKET-VLF / VLF
0.287 in (7.29 mm) / 0.494 in (12.55 mm) / -0.506 in (-12.85 mm)
0.088 in (2.24 mm) × 7.012 in (178.1 mm) × 5.012 in (127.3 mm)
Wall-facing wire rebate; preserve outer wood bearing land
POCKET-VLA / VLA
0.287 in (7.29 mm) / -6.506 in (-165.25 mm) / -0.506 in (-12.85 mm)
0.088 in (2.24 mm) × 7.012 in (178.1 mm) × 5.012 in (127.3 mm)
Wall-facing wire rebate; preserve outer wood bearing land
POCKET-VRB / VRB
0 in (0 mm) / 0.494 in (12.55 mm) / 0.494 in (12.55 mm)
0.088 in (2.24 mm) × 7.012 in (178.1 mm) × 5.012 in (127.3 mm)
Wall-facing wire rebate; preserve outer wood bearing land
POCKET-VRT / VRT
0 in (0 mm) / 0.494 in (12.55 mm) / -4.506 in (-114.45 mm)
0.088 in (2.24 mm) × 7.012 in (178.1 mm) × 5.012 in (127.3 mm)
Wall-facing wire rebate; preserve outer wood bearing land
POCKET-VRF / VRF
0 in (0 mm) / 0.494 in (12.55 mm) / -0.506 in (-12.85 mm)
0.088 in (2.24 mm) × 7.012 in (178.1 mm) × 5.012 in (127.3 mm)
Wall-facing wire rebate; preserve outer wood bearing land
Machining removals · continued
Local X / Y / Z begin at the named part’s minimum assembled-coordinate corner. Cut volumes extend slightly beyond an edge for a through-cut and are clipped to the part. Read orientation pictures; never use a schematic as a full-size template.
Cut / part
Local X / Y / Z
Removal size
Operation
POCKET-VRA / VRA
0 in (0 mm) / -6.506 in (-165.25 mm) / -0.506 in (-12.85 mm)
0.088 in (2.24 mm) × 7.012 in (178.1 mm) × 5.012 in (127.3 mm)
Wall-facing wire rebate; preserve outer wood bearing land
POCKET-RTCF / RTCF
0.494 in (12.55 mm) / 0.494 in (12.55 mm) / 0.287 in (7.29 mm)
19.012 in (482.9 mm) × 11.012 in (279.7 mm) × 0.088 in (2.24 mm)
Roof-facing wire rebate; retained solid bearing land
POCKET-RTCA / RTCA
0.494 in (12.55 mm) / -10.506 in (-266.85 mm) / 0.287 in (7.29 mm)
19.012 in (482.9 mm) × 11.012 in (279.7 mm) × 0.088 in (2.24 mm)
Roof-facing wire rebate; retained solid bearing land
POCKET-RTCL / RTCL
0.494 in (12.55 mm) / -0.506 in (-12.85 mm) / 0.287 in (7.29 mm)
19.012 in (482.9 mm) × 11.012 in (279.7 mm) × 0.088 in (2.24 mm)
Roof-facing wire rebate; retained solid bearing land
POCKET-RTCR / RTCR
-18.506 in (-470.05 mm) / -0.506 in (-12.85 mm) / 0.287 in (7.29 mm)
19.012 in (482.9 mm) × 11.012 in (279.7 mm) × 0.088 in (2.24 mm)
Roof-facing wire rebate; retained solid bearing land
ROOF-OPEN-P02-0 / P02
9 in (228.6 mm) / 4 in (101.6 mm) / -0.1 in (-2.54 mm)
18 in (457.2 mm) × 10 in (254 mm) × 0.903125 in (22.94 mm)
Supported through-cut; preserve original N13 opening coordinates
VENT-P03L-0 / P03L
-0.1 in (-2.54 mm) / 6 in (152.4 mm) / 9 1/8 in (231.78 mm)
0.903125 in (22.94 mm) × 6 in (152.4 mm) × 4 in (101.6 mm)
Supported through-cut; preserve original N13 opening coordinates
Machining removals · continued
Local X / Y / Z begin at the named part’s minimum assembled-coordinate corner. Cut volumes extend slightly beyond an edge for a through-cut and are clipped to the part. Read orientation pictures; never use a schematic as a full-size template.
Cut / part
Local X / Y / Z
Removal size
Operation
VENT-P03R-0 / P03R
-0.1 in (-2.54 mm) / 6 in (152.4 mm) / 9 1/8 in (231.78 mm)
0.903125 in (22.94 mm) × 6 in (152.4 mm) × 4 in (101.6 mm)
Supported through-cut; preserve original N13 opening coordinates
NUT-RECESS-RCML / RCML
1/4 in (6.35 mm) / 7/8 in (22.23 mm) / 1 13/16 in (46.04 mm)
Cylindrical removal; bounding extent 1 in (25.4 mm) × 5/8 in (15.88 mm) × 1 in (25.4 mm) (use the stated diameter and depth, not a rectangular pocket)
Stopped 1-inch flat-bottom recess from rear post face, 5/8-inch deep; remaining wood 7/8 inch. Rehearse the actual socket before final drilling.
NUT-RECESS-RCMR / RCMR
1/4 in (6.35 mm) / 7/8 in (22.23 mm) / 1 13/16 in (46.04 mm)
Cylindrical removal; bounding extent 1 in (25.4 mm) × 5/8 in (15.88 mm) × 1 in (25.4 mm) (use the stated diameter and depth, not a rectangular pocket)
Stopped 1-inch flat-bottom recess from rear post face, 5/8-inch deep; remaining wood 7/8 inch. Rehearse the actual socket before final drilling.
Cutting diagrams
PLY-1 · numbered stock allocation
Numbers match the ordered ID and exact stock-coordinate table
Numbers match the ordered ID and exact stock-coordinate table
Dedicated full-width trial board; form thickness before ripping narrow parts
Inspection records
Receiving and physical acceptance record
Leave actual results blank until measured or performed. Calculations and renders do not complete a physical record.
Checkpoint
Actual result / date / reviewer
H01 · before hardware drilling Receive three same-hand LSX-100R hinges, exact screws and N305-979 hasp. Verify maker drawing, hole/head seating, full bearing on equal cured veneer faces, aligned axes, head and rear-tip cover, full swing and 2 in (50.8 mm) lift-off. No supplier approval or physical trial received.
___________________
___________________
___________________
H02 · before wood cutting Measure plywood gauge, straight square solid wood, stock dimensions and kerf. Refit door perimeter and retainer sides while retaining glazing pocket and hidden structural bearing. No dimensions are received measurements.
___________________
___________________
___________________
Glue applied: __________ · Coating/repair time: __________ Temperature / humidity: __________ · Full cure due: __________ PSA supplier dwell: __________ · Liner test dates: __________
Receiving and physical acceptance record
Leave actual results blank until measured or performed. Calculations and renders do not complete a physical record.
Checkpoint
Actual result / date / reviewer
H03 · before veneer purchase Confirm chosen species, PSA/backer, panel balance, cured Varathane compatibility, acclimation, pressure, dwell, temperature/humidity and cleaner exposure. Prove bond and compression stability beneath the hinge leaves. Recalculate for every changed layer.
___________________
___________________
___________________
H04 · before capture routing Measure actual welded crossing and cured film. Trial 0.088 in (2.24 mm) reference rebate, at most 1/8 in (3.18 mm) without redesign, with full solid bearing and covered cut wires.
___________________
___________________
___________________
Glue applied: __________ · Coating/repair time: __________ Temperature / humidity: __________ · Full cure due: __________ PSA supplier dwell: __________ · Liner test dates: __________
Receiving and physical acceptance record
Leave actual results blank until measured or performed. Calculations and renders do not complete a physical record.
Checkpoint
Actual result / date / reviewer
H05 · before finish and lining Complete all drilling, head seats and driver/socket access trials before coating. Flush retainer connection, stopped nut recess and liner protection require received-stack acceptance. Reseal and fully recure any later exposed wood. For revised retainer: received 3 1/2 in (88.9 mm) flat-head screw, washer <=1/16 in (1.59 mm) and locknut 0.298 in (7.57 mm)–0.328 in (8.33 mm). Trial 1 in (25.4 mm) diameter x 5/8 in (15.88 mm) stopped rear recess, socket access, two complete exposed threads and tail >=1/16 in (1.59 mm) below post face. Retain 7/8 in (22.23 mm) post thickness at the washer seat. No torque or connection capacity inferred.
___________________
___________________
___________________
H06 · before glazing cutting Measure actual 0.22 in (5.59 mm) acrylic, uncompressed neoprene pads and cured films; fit spacer from 3/8 in (9.53 mm) rough stock. Preserve expansion and supported lower edge; no rigid squeeze or drilled pane. Weigh finished door and repeat supported swing/lift trial.
___________________
___________________
___________________
Glue applied: __________ · Coating/repair time: __________ Temperature / humidity: __________ · Full cure due: __________ PSA supplier dwell: __________ · Liner test dates: __________
Receiving and physical acceptance record
Leave actual results blank until measured or performed. Calculations and renders do not complete a physical record.
Checkpoint
Actual result / date / reviewer
H07 · before loading Qualified review of wood connections, door support, retainer and continuous base/furniture/building floor under weighed wet contents. No capacity derives from the hinge catalogue or bed arithmetic. Qualified connection review must include the countersunk front bearing and recessed interior post bearing, not the previous carriage-bolt geometry.
___________________
___________________
___________________
H08 · before animal entry Full finish cure; construction, secure closure, pinch/edge/escape/mesh, maintenance and stability tests. Separate species/equipment heat/light/humidity commissioning; no animal suitability assigned.
___________________
___________________
___________________
Glue applied: __________ · Coating/repair time: __________ Temperature / humidity: __________ · Full cure due: __________ PSA supplier dwell: __________ · Liner test dates: __________
Receiving and physical acceptance record
Leave actual results blank until measured or performed. Calculations and renders do not complete a physical record.
Checkpoint
Actual result / date / reviewer
H09 · before liner installation Material suitability and compressed underlay/fold bulk trial around fixed frame, two receivers and three rear posts; uncut wet-zone folds. One-inch water observation for 24 hours only after qualified support; no aquarium approval.
___________________
___________________
___________________
Glue applied: __________ · Coating/repair time: __________ Temperature / humidity: __________ · Full cure due: __________ PSA supplier dwell: __________ · Liner test dates: __________
Sources, separate statuses and maintenance
Current product identity and source evidence are in the construction review packet. Quantities, geometry and instructions belong only to N13.
Separate statuses: research, reference dimensions, calculations and digital validation each have their own evidence. No prototype has been built. Physical testing and qualified review have not been performed. Publication does not replace these construction checks.
For maintenance, relocate occupants, isolate equipment and remove all water and contents. Release the hasp and open at least 90 degrees before the helper-supported 2-inch (50.8 mm) vertical lift. Remove the front receiver clamp strips, then long side strips, then rear post and remaining short strips. Fold the empty basin clear before releasing both retainer nuts and screws. Refit in the reverse accepted order and repeat affected cure, shallow leak, door, mesh and containment checks.
Veneer scans by Jenelle van Heerden via Poly Haven illustrate maple, white oak and walnut appearance. Delivered grain and colour vary. The full exterior veneer system, including hinge bearing, remains subject to supplier/qualified bond, balance and actual-stack acceptance.